8 Unique Facts About Thread Forming Taps
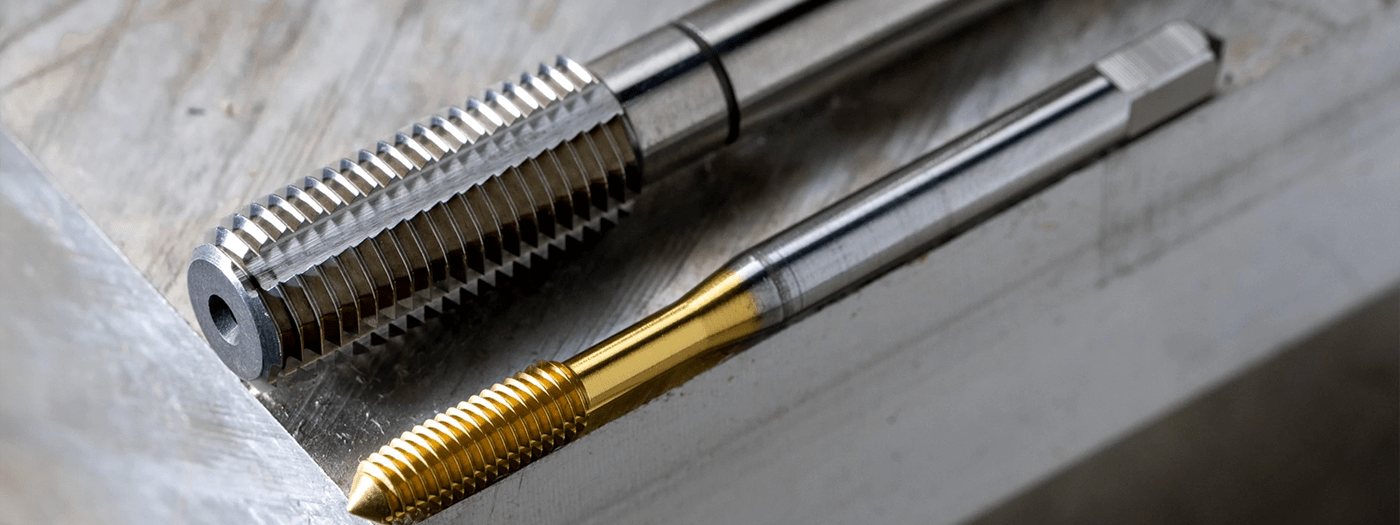
Unlike most CNC cutting tools, Thread Forming Taps, otherwise known as Form Taps, Forming Taps, or Roll Taps, work by molding the workpiece rather than cutting it. Because of this, Form Taps do not contain any flutes, as there is no cutting action taking place, nor are there any chips to evacuate. Below are 8 unique facts of Thread Forming Taps (and some may surprise you).
1. Chips Aren’t Formed
When using a Form Tap, chips are not formed, nor is any part material evacuated (Yes, you read that right). With thread forming, the tool is void of any flutes, as chip evacuation is not a concern. Form Taps quite literally mold the workpiece, rather than cut it, to produce threads. Material is displaced within a hole to make way for the threads being formed.
Increase Your Tapping Efficiency 20x With Titan USA’s Thread Form Taps
2. Cutting Oils Allow for Reduced Friction & Heat Generation
Did you know that Thread Forming Taps require good lubrication? But why is that the case if chips are not being evacuated, and how does lubrication enter the part with such a limited area between the tool and the perimeter of the hole being threaded? Despite the fact that chips aren’t being formed or evacuated, cutting oils aid the Form Tap as it interacts with the part material, and reduces friction and heat generation. Lube vent grooves are narrow channels engineered into the side of Forming Taps that are designed to provide just enough room for lubricant to make its way into – and out of – a part.
3. Only Certain Materials Are Recommended for Thread Forming
Not all materials are well suited for Thread Forming Taps. In fact, attempting to use a tap in the wrong material can result in significant part and tool damage. The best materials for this unique type of operation include aluminum, brass, copper, 300 stainless steel, and leaded steel. In other words, any material that leaves a stringy chip is a good candidate for cold forming threads. Materials that leave a powdery chip, such as cast iron, are likely too brittle, resulting in ineffective, porous threads.
4. Threads Produced Are Stronger Than Conventional Tapping Threads
Thread forming produces much stronger threads than conventional tapping methods, due to the displacements of the grain of the metal in the workpiece. Further, cutting taps produce chips, which may interfere with the tapping process.
5. Chip Evacuation is Never a Concern With Thread Forming
In conventional tapping applications, as with most machining applications, chip evacuation is a concern. This is especially true in blind holes, or holes with a bottom, as chips created at the very bottom of the hole oftentimes have a long distance to travel before being efficiently evacuated. With form taps, however, chip removal is never a concern.
6. Form Taps Offer Extended Tool Life
Thread Forming Taps are incredibly efficient, as their tool life is substantial (Up to 20x longer than cutting taps), as they have no cutting edges to dull. Further, Thread Forms can be run at faster speeds (Up to 2x faster than Cutting Taps).
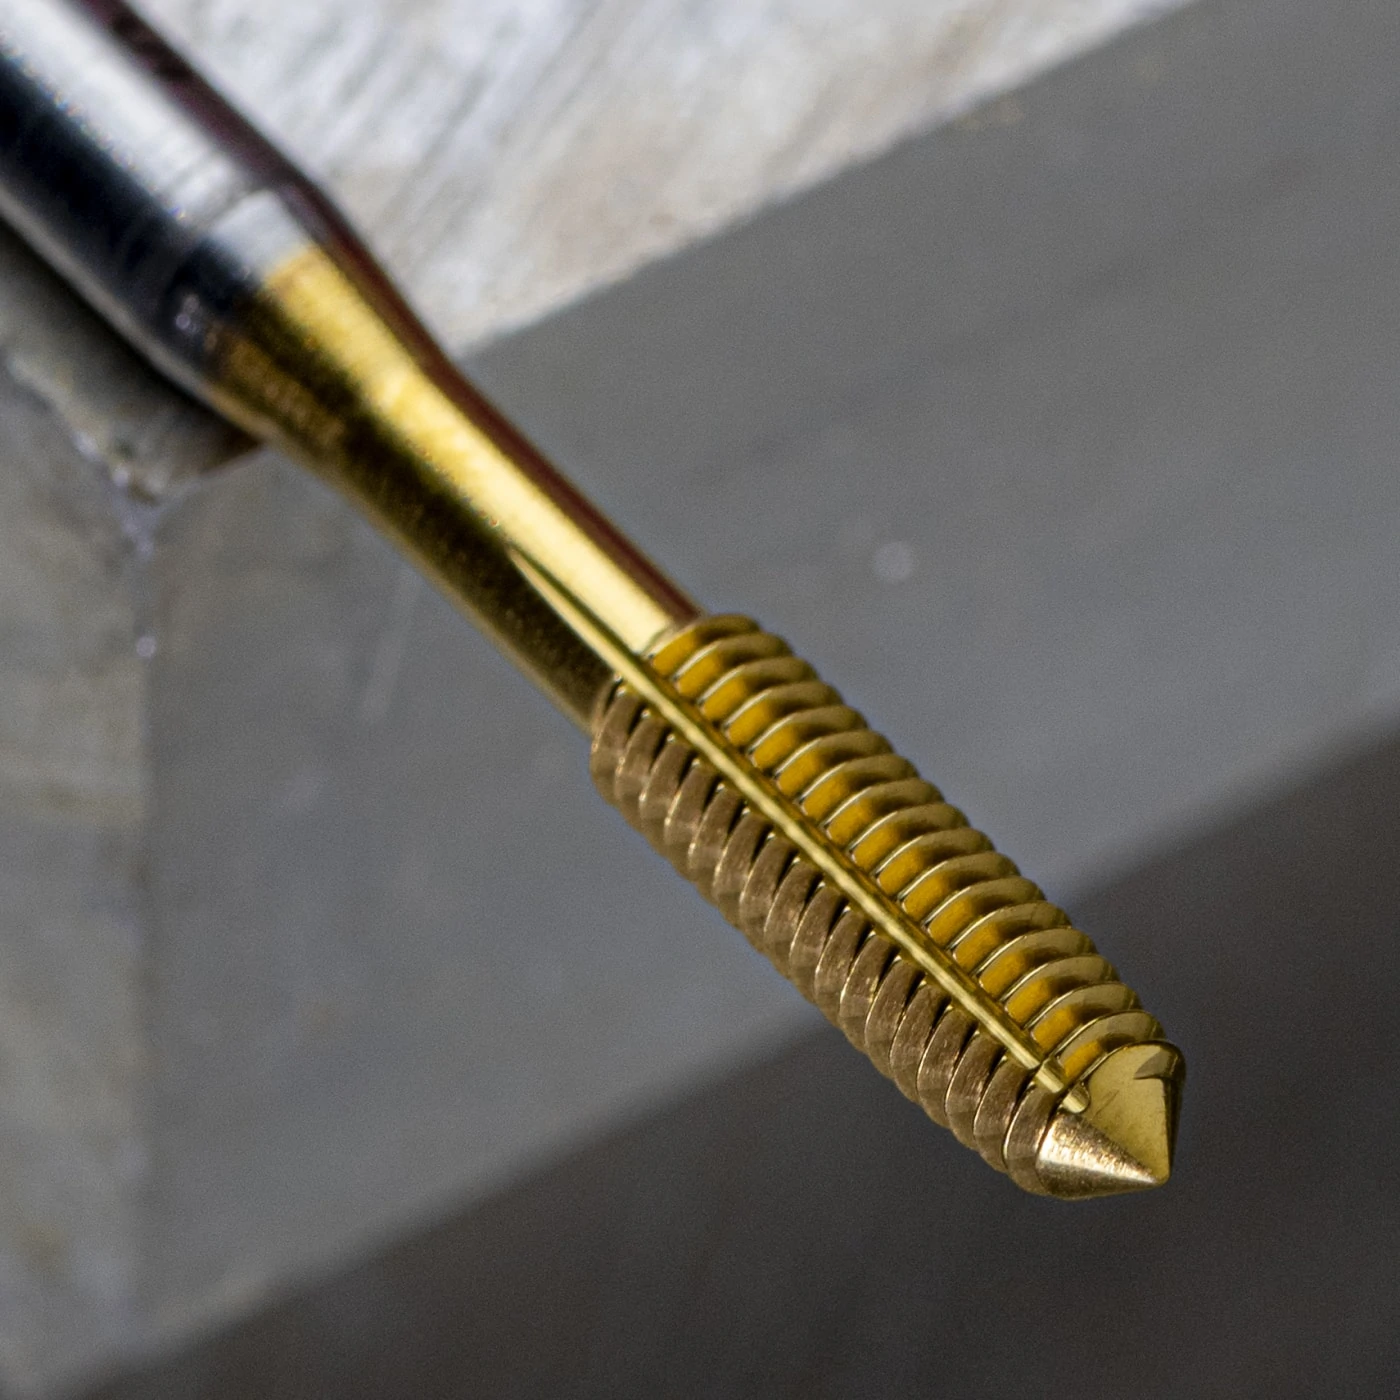
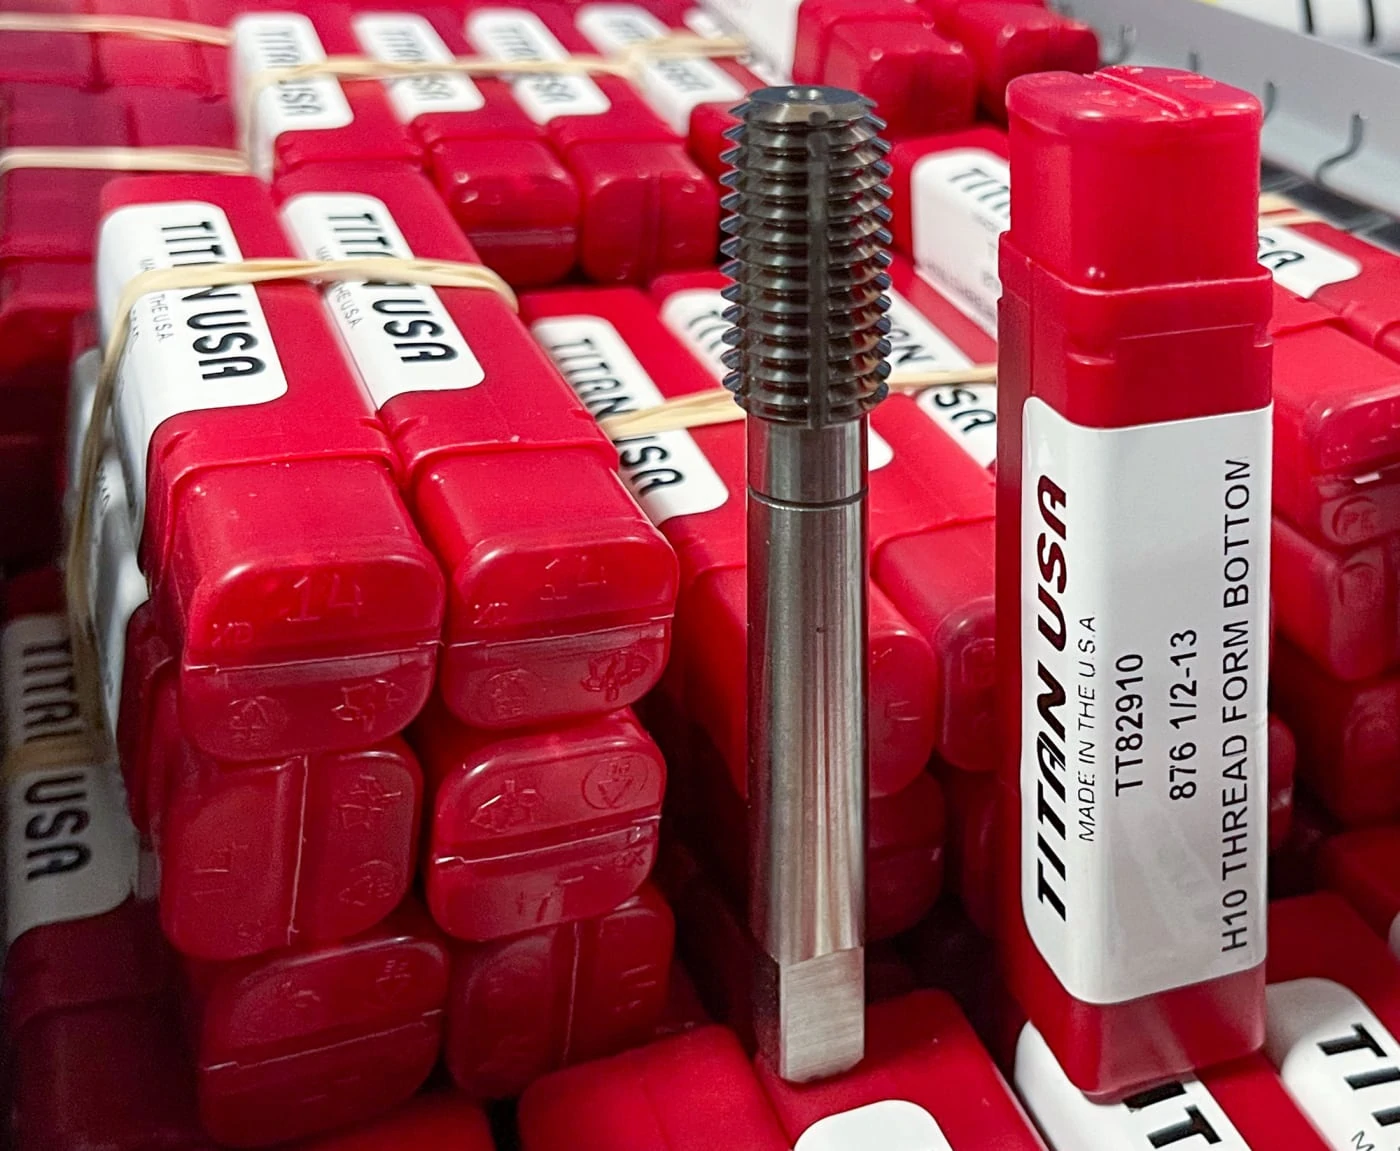
Pro Tip: To prolong tool life even further, opt for a coated tool. Titan USA Form Taps, for example, are fully stocked in both uncoated and TiN coated styles.
7. A Simple Formula Will Help You Find the Right Drill Size
When selecting a Tap, you must be familiar with the following formula, which will help a machinist determine the proper drill size needed for creating the starter hole, before a Thread Forming Tap is used to finish the application:
Drill Size = Major Diameter – [(0.0068 x desired % of thread) / Threads Per Inch]
Drill Size (mm) = Major Diameter – [(0.0068 x desired % of thread x pitch (mm)]
8. Thread Forming Taps Need a Larger Hole Size
- Thread Form Taps require a larger pre-tap hole size than a cutting tap. This is because these tools impact the sides of the hole consistently during the thread forming process. If the pre-tap hole size is too small, the tool would have to work too hard to perform its job, resulting in excessive tool wear, torque, and possible breakage.
As an example, a ¼-20 cut tap requires a #7 drill size for the starter hole, whereas a ¼-20 roll tap requires a #1 drill size for 65% thread.


I learned quite a lot about thread-forming taps by reading this post. Thanks for publishing the post about unique facts of thread-forming taps. I will share the article with my colleagues.
Another interesting tidbit: A form tap may slightly raise (a couple thousandths of an inch) the area surrounding the top and bottom surfaces of the hole. A larger chamfer will help eliminate this raised area resulting a flatter, more even surface after form tapping. Or you can just stone or grind the surface after tapping if a larger chamfer is unacceptable.
Can you freehand tap with thread-forming taps?
We would not suggest it, it would require an extremely steady hand.
you can Jennifer if you use a tap center to keep your tap strait
Excellent article … thank you for putting that together, and for sharing it!
Hi There,
Excellent Blog, Thanks a lot for sharing about Thread Forming Taps. I have been looking for so long for this type of information.
Keep Sharing….
I have worked with formed threads on some of our assemblies and I’m not a fan. If the drilled hole is slightly too large, it seem that a double helix can form.
I’ve been programming for almost ten years, been using roll form taps for about 6 years and never once have seen a “double helix” from the minor diameter being oversize. Usually, a oversize minor dia. prior to tapping – will result in the pitch diameter and minor diameter being oversize after tapping (leading to the acceptance of a no-go thread gauge).
A “double helix” condition could only be possible if the threads had multiple start angles. I’m not entirely positive why you would be noticing a “double helix” forming within your threads but my theories are
1) the tap is programmed to go back into the same hole twice – leading to different start angles
2) (less likely) the tap is spinning within the collet during the tapping operation
Roll form taps are phenomenal if used properly. If I were you I would look closer into the root cause. Good luck
Thanks for the reply. My experience with roll tapped holes is on the user end only. I have never used a roll tap to thread a hole. The problem I was referring to was an improperly formed crest on the rolled thread. The displaced metal didn’t fully form into the crest but left, what looked like with an eye loupe, a second, smaller helical pattern on the incompletely formed crest. In the instance I’m primarily referring to, it even caused difficulty starting the screw. My guess as to why this happened is an oversized hole to start with leaving not enough metal to displace into the crest. Does this seem consistent with your experience in actually using roll taps to thread holes?
Hello Eric. Yes that can happen, but it’s not really a problem of the forming taps. You could say forming taps require a tighter tolerance hole in that regard, but the hole should not be that much oversized anyway, even when using regular taps.
Eric,
You have found what I believe is the greatest downside to thread form tapping. If all you ever do is run the machine that taps the hole it likely goes unnoticed but if you are involved in doing the assembly work that employs a formed thread where the tap drill / hole was slightly large you get what looks like a double helix. This apparent dbl. helix is the result of the thread crest being incomplete as there was insufficient material to upset and you actually end up with a slight trough or valley where the crest should be. The finer the thread the better roll taps work but if there is not enough material to complete the thread, they are a TERROR to assemble even for experienced operators.
Your article states: a ¼-20 roll tap requires a #1 drill size for 65% thread. What is a 65% thread ? Is a greater percent of thread possible or important ?
Hello Jonny,
Great question! The percentage of thread refers to the percentage of height where basic thread height and external and internal threads are engaged. The percentage of thread is calculated by finding your total engaged length (EL) and your total overall length (OL). You then divide EL by OL and multiply by 100 to get your percentage, so your equation looks like this, Percentage of Thread = EL/OL*100. Some jobs require a certain thread percentage but if nothing is specified we suggest using between a 60%-75% thread percentage to help your tool last longer.
Does Titan offer STI FORMING TAPS as standards?
Hello Paul,
Yes Titan USA stocks STI Forming Taps as standards. Here is the link to the general purpose taps https://www.titancuttingtools.com/products/tapping/general-purpose-taps
With the tap drill formulas referenced (see below) …
What “Class of fit” (Inch “H” value) (Metric “D” value) is this formula written for?
If you have a low H or D the hole should be smaller.
If you have a High H or D the hole should be larger.
Drill Size = Major Diameter – [(0.0068 x desired % of thread) / Threads Per Inch]
Drill Size (mm) = Major Diameter – [(0.0068 x desired % of thread x pitch (mm)]
Hello Brian,
Great question! The formula is for a standard tap, 1/4 – 20 H6 being the standard. For each H-limit above or below you would add or subtract .0005. For H7 it is +.0005, for H5 it is -.0005.
can you roll tap with a rigid holder or do you need a spring holder?
Hello Steve,
Yes, rigid holders can be used to roll tap.
Thanks Guy
Can thread forming taps be used to repair existing threads?
Including threads in material that was powder coat painted after the original hole was taped.
Hey Stephen,
This would not be possible. Since you are reshaping the material and the material is now powdered coated, you will not have the required material to be able to form your new thread, and instead form your thread on the paint itself.
Looking to tap into fiberglass besides keeping tap cool and not use coolant. My plan is to use cooling air to keep tap cool. My question is being it’s a blind hole would it be best to form tap??? Tapped hole size being. 1 1/8-12 UNC-2B depth of thread is 1.250 deep.
Thanks
is there any special CNC programming F&S required for the tapping with form taps?
These 8 unique facts about thread forming taps are very beneficial for us. Like cutting oils allow for reduced friction, how a simple formula can help you find the right drill size and the threads produced are stronger than conventional tapping threads.
Is there any special requirement for foam tapping?
Are thread forming taps ok to use to chase threads in cast iron and aluminum? I am looking for something a bit better than thread chasers as far as quality.
Hi Craig,
Thread forming taps have no cutting and edge and do not produce chips. You should be able to chase an existing thread with this tool, although thread forming taps are not designed to remove burrs.
This post was really enlightening! I had no idea that thread forming taps could create stronger threads by displacing material. The fact that they can reduce the risk of chips clogging the hole is also a game changer for efficiency. Thanks for sharing these unique insights!
Great read! I had no idea that thread forming taps could create stronger threads without cutting. The benefits of reduced chip load are really intriguing. Thanks for sharing these unique insights!
This post is a fantastic deep dive into thread forming taps! I had no idea that they could significantly reduce material waste and improve strength in threaded holes. The fact about their versatility in different types of materials was particularly eye-opening. Thanks for sharing these unique insights!