8 Ways You’re Killing Your End Mill
Running It Too Fast or Too Slow Can Impact Tool Life
Determining the right speeds and feeds for your tool and operation can be a complicated process, but understanding the ideal speed (RPM) is necessary before you start running your machine to ensure proper tool life. Running a tool too fast can cause suboptimal chip size or even catastrophic tool failure. Conversely, a low RPM can result in deflection, bad finish, or simply decreased metal removal rates. If you are unsure what the ideal RPM for your job is, contact the tool manufacturer.
Feeding It Too Little or Too Much
Another critical aspect of speeds and feeds, the best feed rate for a job varies considerably by tool type and workpiece material. If you run your tool with too slow of a feed rate, you run the risk of recutting chips and accelerating tool wear. If you run your tool with too fast of a feed rate, you can cause tool fracture. This is especially true with miniature tooling.
Using Traditional Roughing
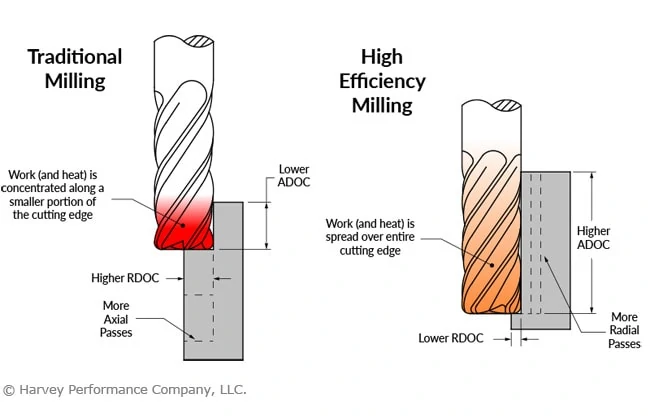
While traditional roughing is occasionally necessary or optimal, it is generally inferior to High Efficiency Milling (HEM). HEM is a roughing technique that uses a lower Radial Depth of Cut (RDOC) and a higher Axial Depth of Cut (ADOC). This spreads wear evenly across the cutting edge, dissipates heat, and reduces the chance of tool failure. Besides dramatically increasing tool life, HEM can also produce a better finish and higher metal removal rate, making it an all-around efficiency boost for your shop.
Using Improper Tool Holding and its Effect on Tool Life
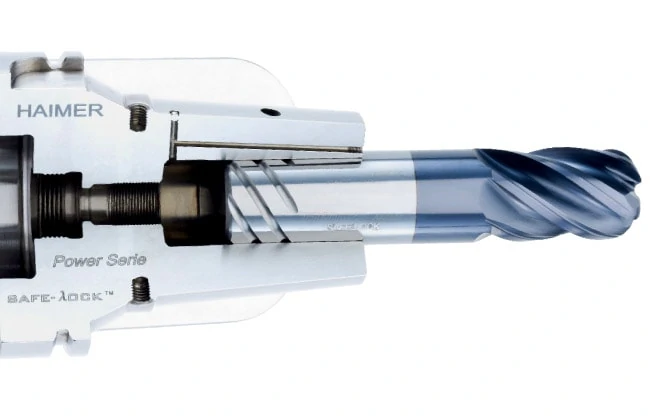
Proper running parameters have less of an impact in suboptimal tool holding situations. A poor machine-to-tool connection can cause tool runout, pullout, and scrapped parts. Generally speaking, the more points of contact a tool holder has with the tool’s shank, the more secure the connection. Hydraulic and shrink fit tool holders offer increased performance over mechanical tightening methods, as do certain shank modifications, like Helical’s ToughGRIP shanks and the Haimer Safe-Lock™.
Not Using Variable Helix/Pitch Geometry
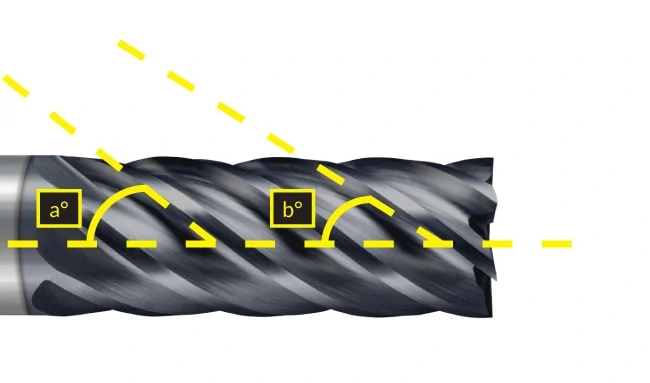
A feature on a variety of high performance end mills, variable helix, or variable pitch, geometry is a subtle alteration to standard end mill geometry. This geometrical feature ensures that the time intervals between cutting edge contact with the workpiece are varied, rather than simultaneous with each tool rotation. This variation minimizes chatter by reducing harmonics, which increases tool life and produces superior results.
Choosing the Wrong Coating Can Wear on Tool Life
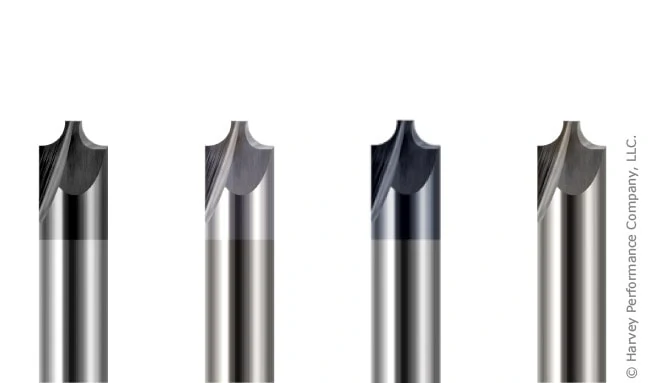
Despite being marginally more expensive, a tool with a coating optimized for your workpiece material can make all the difference. Many coatings increase lubricity, slowing natural tool wear, while others increase hardness and abrasion resistance. However, not all coatings are suitable to all materials, and the difference is most apparent in ferrous and non-ferrous materials. For example, an Aluminum Titanium Nitride (AlTiN) coating increases hardness and temperature resistance in ferrous materials, but has a high affinity to aluminum, causing workpiece adhesion to the cutting tool. A Titanium Diboride (TiB2) coating, on the other hand, has an extremely low affinity to aluminum, and prevents cutting edge build-up and chip packing, and extends tool life.
Using a Long Length of Cut
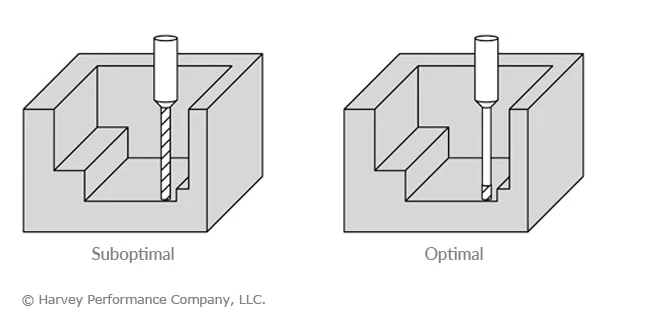
While a long length of cut (LOC) is absolutely necessary for some jobs, especially in finishing operations, it reduces the rigidity and strength of the cutting tool. As a general rule, a tool’s LOC should be only as long as needed to ensure that the tool retains as much of its original substrate as possible. The longer a tool’s LOC the more susceptible to deflection it becomes, in turn decreasing its effective tool life and increasing the chance of fracture.
Free Resource: Download the 50+ Page High Efficiency Milling (HEM) Guidebook Today
Choosing the Wrong Flute Count
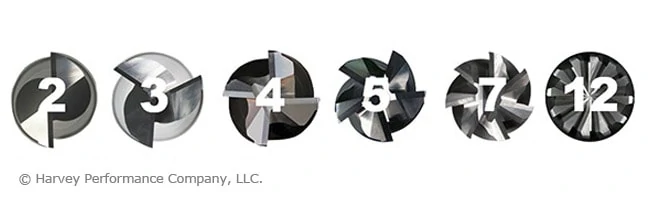
As simple as it seems, a tool’s flute count has a direct and notable impact on its performance and running parameters. A tool with a low flute count (2 to 3) has larger flute valleys and a smaller core. As with LOC, the less substrate remaining on a cutting tool, the weaker and less rigid it is. A tool with a high flute count (5 or higher) naturally has a larger core. However, high flute counts are not always better. Lower flute counts are typically used in aluminum and non-ferrous materials, partly because the softness of these materials allows more flexibility for increased metal removal rates, but also because of the properties of their chips. Non-ferrous materials usually produce longer, stringier chips and a lower flute count helps reduce chip recutting. Higher flute count tools are usually necessary for harder ferrous materials, both for their increased strength and because chip recutting is less of a concern since these materials often produce much smaller chips.




Google randomly showed me this article and it directly pertained to issues I was battling in the shop the other night! I’m a new-ish home shop machinist and this definitely helped. Keep the tips coming!!
Would you recommend high efficiency milling for a manual machine? If so, which would be better: A solid holder or a R8 collet? Assuming there is no pullout problems with the R8 that is.
Hi Anthony,
HEM on a manual machine might be tough due to the tool paths, but one can still engage the entire LOC axially and take a light radial depth of cut for a pre-existing slot of roughing along the side of a workpiece or pocket. HEM slotting on a manual machine may be difficult due to the trochoidal milling tool path that is used. The holder usually depends on the tool size — larger tools should use a solid holder, while smaller tools should use an R8 collet. Collets have higher dynamic stiffness, and lower static stiffness, than solid holders, so they are preferred when using a tool at high speeds.
Please give our tech team a call if you have any further questions, and we’d be happy to help!
thanks for this, I’ve always using this tool in my woodwork shop and it is been a hassle.
I’ll try and use high efficiency milling with my tools. That way they last longer. Thanks for the help, this will save me a lot of money.
What about coolant, I see a lot of the videos are w/o coolant. Is this for the videos sake or do some of these roughers work better w/o coolant?
Hey
What is TiB2 coating,
This coating used on which type of material machining
Hi Vaishnav,
Please refer to our linked blog post on TiB2 coating for more information. This post explains when and when not to use TiB2 coating.