
Applying HEM to Micromachining
The following is just one of several blog posts relevant to High Efficiency Milling and Micromachining. To achieve a full understanding of this popular machining method, view any of the additional HEM posts below!
Introduction to High Efficiency Milling I High Speed Machining vs. HEM I How to Combat Chip Thinning I Diving into Depth of Cut I How to Avoid 4 Major Types of Tool Wear I Intro to Trochoidal Milling
Benefits of Using HEM with Miniature Tooling
High Efficiency Milling (HEM) is a technique for roughing that utilizes a lower Radial Depth of Cut (RDOC), and a higher Axial Depth of Cut (ADOC). This delays the rate of tool wear, reducing the chance of failure and prolonging tool life while boosting productivity and Material Removal Rates (MRR). Because this machining method boosts MRR, miniature tooling (<.125”) and micromachining is commonly overlooked for HEM operations. Further, many shops also do not have the high RPM capabilities necessary to see the benefits of HEM for miniature tooling. However, if used properly, miniature tooling can produce the same benefits of HEM that larger diameter tooling can.
Benefits of HEM:
- Extended tool life and performance.
- Faster cycle times.
- Overall cost savings
Preventing Common Challenges in Micromachining
Utilizing miniature tooling for HEM, while beneficial if performed correctly, presents challenges that all machinists must be mindful of. Knowing what to keep an eye out for is a pivotal first step to success.
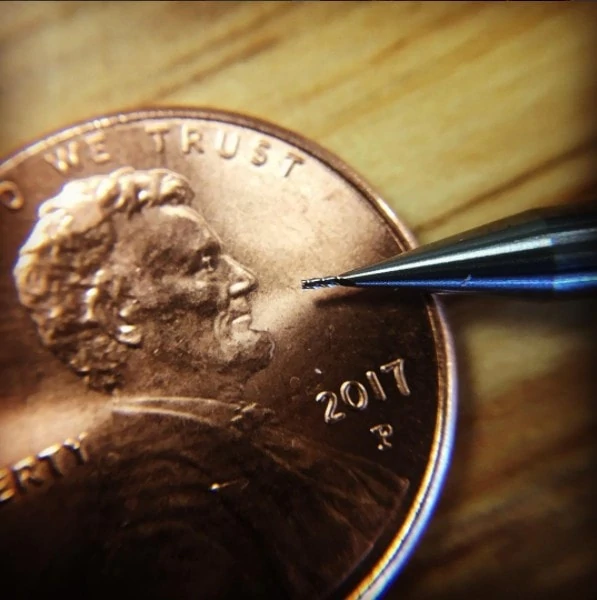
Tool Fragility & Breakage with Miniature Tooling
Breakage is one of the main challenges associated with utilizing high efficiency micromachining with miniature tools due to the fragility of the tool. Spindle runout and vibration, tool deflection, material inconsistencies, and uneven loading are just some of the problems which can lead to a broken tool. To prevent this, more attention must be paid to the machine setup and material to ensure the tools have the highest chance of success.
As a general rule, HEM should not be considered when using tools with cutting diameters less than .031”. While possible, HEM may still be prohibitively challenging or risky at diameters below .062”, and your application and machine must be considered carefully.
Techniques to Prevent Tool Failure:
- Ensure workpiece is secure and supported.
- Use the shortest overall length and length of cut as possible.
- Check tool runout in the spindle and utilize shrink fit holders if possible.
- Choose a coating optimized for your material.
Managing Excessive Heat & Thermal Shock in Micromachining
Due to the small nature of miniature tooling and the high running speeds they require, heat generation can quickly become an issue. When heat is not controlled, the workpiece and tooling may experience thermal cracking, melting, burning, built up edge, or warping.
To combat high heat, coolant is often used to decrease the surface temperature of the material as well as aid in chip evacuation and lubricity. However, care must be taken to ensure that using coolant doesn’t cool the material too quickly or unevenly. If an improper coolant method is used, thermal shock can occur. Thermal shock happens when a material expands unevenly, creating micro fractures that propagate throughout the material and can crack, warp, or change the physical properties of the material.
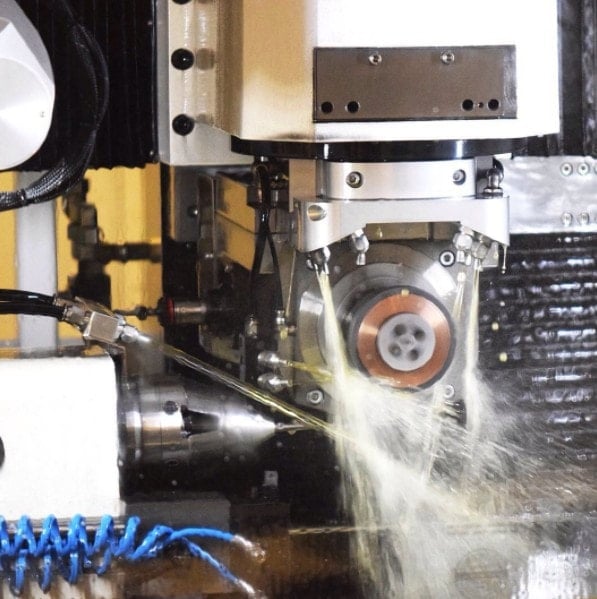
Techniques to Prevent Heat & Thermal Shock:
- Run your coated tool dry or with compressed air while ensuring sufficient chip evacuation.
- Choose a coating optimized for your material.
- Use tooling with geometry specific to your workpiece material.
- Decrease speed (RPM).
Key Takeaways
If performed properly, miniature tooling micromachining (<.125”) can reap the same benefits of HEM that larger diameter tooling can: reduced tool wear, accelerated part production rates, and greater machining accuracy. However, more care must be taken to monitor the machining process and to prevent tool fragility, excessive heat, and thermal shock.
Check out this example of HEM toolpaths (trochoidal milling) being run with a 3/16″ Harvey Tool End Mill in aluminum.


One thing to watch out for when using HFM techniques for micromachining is fretting or false brinelling, which can occur when an axis makes repeated motions of less than the bearing spacing. A ballscrew based machine can incur damage on the ballscrews and thrust bearings in a remarkably short time, requiring potentially costly repair. I had to have a set of thrust bearings replaced on a two-year-old machine after using a dynamic path to cut a dozen small slots in each of two dozen parts. Linear motor based machines are far more resistant to this type of damage.
I like how you said that an important part of micromachining is having a tool that is specific to the material you are using. Having a good tip would be really helpful because it would allow you to use any kind of material necessary. That way you can make anything you need to in order to please your clients!