Ball Nose Milling Strategy Guide

June 26, 2017/8 Comments/in CNC Machining, Harvey Tool, Machining 101, Machining Techniques, Milling, Quick Tips, Tool Selection/by Harvey Performance Company

Ball Nose Milling Without a Tilt Angle

Ball nose end mills are ideal for machining 3-dimensional contour shapes typically found in the mold and die industry, the manufacturing of turbine blades, and fulfilling general part radius requirements. To properly employ a ball nose end mill (with no tilt angle) and gain the optimal tool life and part finish, follow the 2-step process below (see Figure 1).
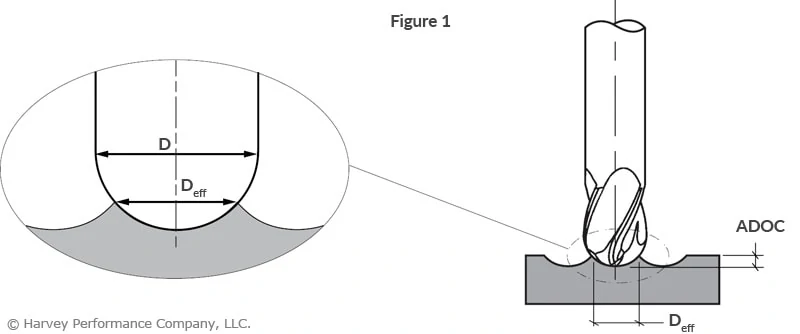
infographic of ball nose milling parameters without tilt angle

Shop Harvey Tool’s Vast Selection of Ball Profile End Mills – Click Here to Get Started

Step One: Calculate Your Effective Cutting Diameter

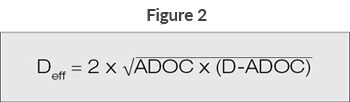
A ball nose end mill’s Effective Cutting Diameter (Deff) differs from its actual cutting diameter when utilizing an Axial Depth of Cut (ADOC) that is less than the full radius of the ball. Calculating the effective cutting diameter can be done using the chart below that represents some common tool diameters and ADOC combinations or by using the traditional calculation (see Figure 2).
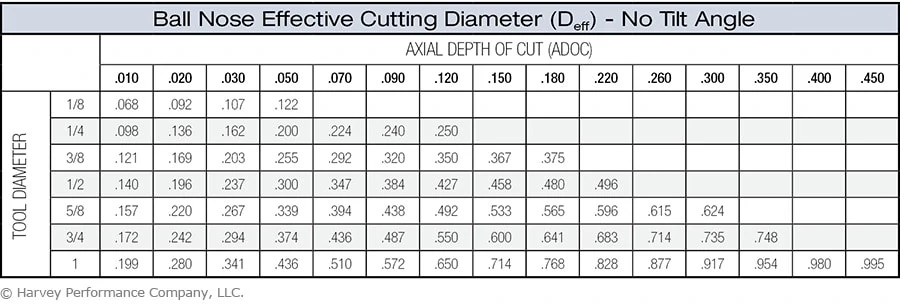
ball nose effective cutting diameter chart
ball nose cutting diameter calculation

Step Two: Calculate Your Compensated Speed

Given the new effective cutting diameter a “Compensated Speed” will need to be calculated. If you are using less than the cutter diameter, then its likely your RPM’s will need to be adjusted upward (see Figure 3).
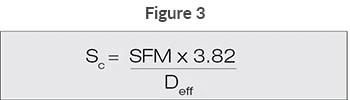
ball nose compensated speed calculation

KEY
ADOC = Axial Depth of Cut
D = Cutting Diameter
Deff = Effective Cutting Diameter
R = Tool Radius (Dia./2)
RDOC = Radial Depth of Cut
SFM = Surface Feet per Minute
Sc = Compensated Speed


Ball Nose Milling With a Tilt Angle

If possible, it is highly recommended to use ball nose end mills on an incline (ß) to avoid a “0” SFM condition at the center of the tool, thus increasing tool life and part finish (Figure 4). For ball nose optimization (and in addition to tilting the tool), it is highly recommended to feed the tool in the direction of the incline and utilize a climb milling technique.
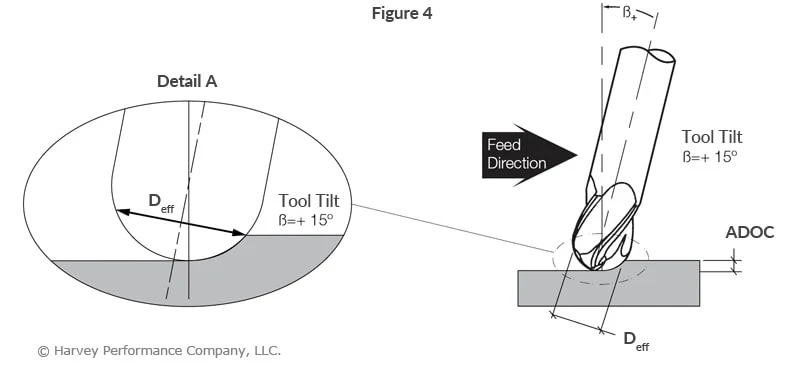
ball nose milling infographic of adoc with tilt angle

To properly employ a ball nose end mill with a tool angle and gain the most optimal tool life and part finish, follow the 2-step process below.
Step One: Calculate Your Effective Cutting Diameter

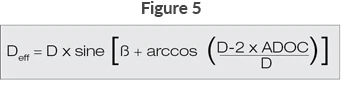
The chart below that represents some common effective cutting diameters and ADOCs at a 15º tilt angle. Otherwise, the traditional calculation below may be used (see Figure 5).
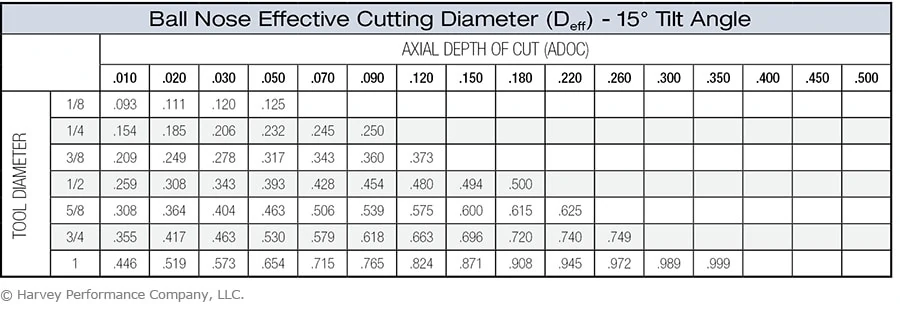
ball nose effective cutting diameter chart
ball nose cutting diameter calculation

Step Two: Calculate Your Compensated Speed

Given the new effective cutting diameter a compensated speed will need to be calculated. If you are using less than the cutter diameter, then its likely your RPM’s will need to be adjusted upward (see Figure 6).
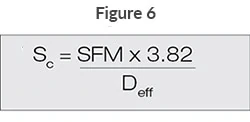
ball nose compensated speed calculation

KEY
Deff = Effective Cutting Diameter
SFM = Mfg Recommended Surface Feet per Minute
Sc = Compensated Speed

print
Guest Logo
Harvey Performance Company
Harvey Performance Company’s team of engineers works together to ensure that your every machining challenge – from tool selection and application support to designing the perfect custom tool for your next job – is rectified with a thoughtful, comprehensive solution.
Share this entry
  • Share on Facebook
  • Share on X
  • Share on WhatsApp
  • Share on Pinterest
  • Share on LinkedIn
  • Share on Reddit
  • Share by Mail
https://www.harveyperformance.com/wp-content/uploads/2017/06/Feature-Image-Ball-Nose-Milling-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-06-26 16:30:432023-10-12 08:57:06Ball Nose Milling Strategy Guide
You might also like
coolant What You Need to Know About Coolant for CNC Machining
Michigan FSAE University of Michigan Formula SAE Racing Team
work hardening Work Hardening and When it Should Scare You
Traditional vs Free Cutting Honeycomb Core Tools
Spot Drilling: The First Step to Precision Drilling
flute count Why Flute Count Matters
8 replies
  1. Zidane Shepard
    Zidane Shepard says:
    September 21, 2017 at 5:11 pm

    Thank you for this milling strategy guide. I especially appreciate your insight on milling with a tilt angle. I was unaware that this could extend the life of the bit. I will keep this in mind while milling in the future.

    Reply
  2. jhcstools
    jhcstools says:
    December 29, 2018 at 1:46 am

    Thank you for sharing this method which I haven’t learned before. It’s helpful for me to learn a lot.

    Reply
  3. Jordan
    Jordan says:
    November 25, 2020 at 1:53 pm

    Faced with the choice of climb milling or moving in the direction of the incline, which is preferable for surface finish?

    Reply
    • Guy Petrillo
      Guy Petrillo says:
      November 25, 2020 at 2:16 pm

      Great question Jordan! When your main concern is surface finish we recommend using the climb milling strategy

      Reply
  4. Tyron Geyser
    Tyron Geyser says:
    November 8, 2023 at 4:51 am

    Could you perhaps assist with this in metric?

    Reply
  5. Justin Tokarsky
    Justin Tokarsky says:
    June 10, 2024 at 2:54 pm

    If anyone is looking to add this to excel…

    =B44*SIN(RADIANS(B45+DEGREES(ACOS(1-((2*B46)/B44)))))

    Where:
    B44 is the Diameter of Cutter
    B45 is Angle in Degrees
    B46 is Depth of Cut

    Reply
  6. Marc
    Marc says:
    July 25, 2024 at 12:19 pm

    They don’t talk of feed. is there feed/tooth adjustment?

    Reply
    • Greg Schranze
      Greg Schranze says:
      August 23, 2024 at 11:52 am

      Hi Marc,

      The adjustment is calculated with the “SC – Compensated Speed” part of the article. This post covers finding your Effective Cutter Diameter which you can linearly interpolate against the speeds and feeds chart to get your RPM. Speeds and Feeds are thus calculated after the fact. Please refer to the Speeds and Feeds 101 article here.

      Reply

Leave a Reply

Want to join the discussion?
Feel free to contribute!

Leave a Reply Cancel reply

Your email address will not be published. Required fields are marked *

BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top