Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Mastering Precision: Pilot Drills in CNC Machining

December 10, 2024/4 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Machining Techniques, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Emily Van Volkom

When it comes to achieving precision in CNC drilling applications, the choice of tools and techniques can make a significant difference in the outcome. One essential element that often doesn’t get the spotlight it deserves is the Pilot Drill. This blog post will explore the importance of pilot drills, their applications, and best practices for integrating them into your CNC machining processes.
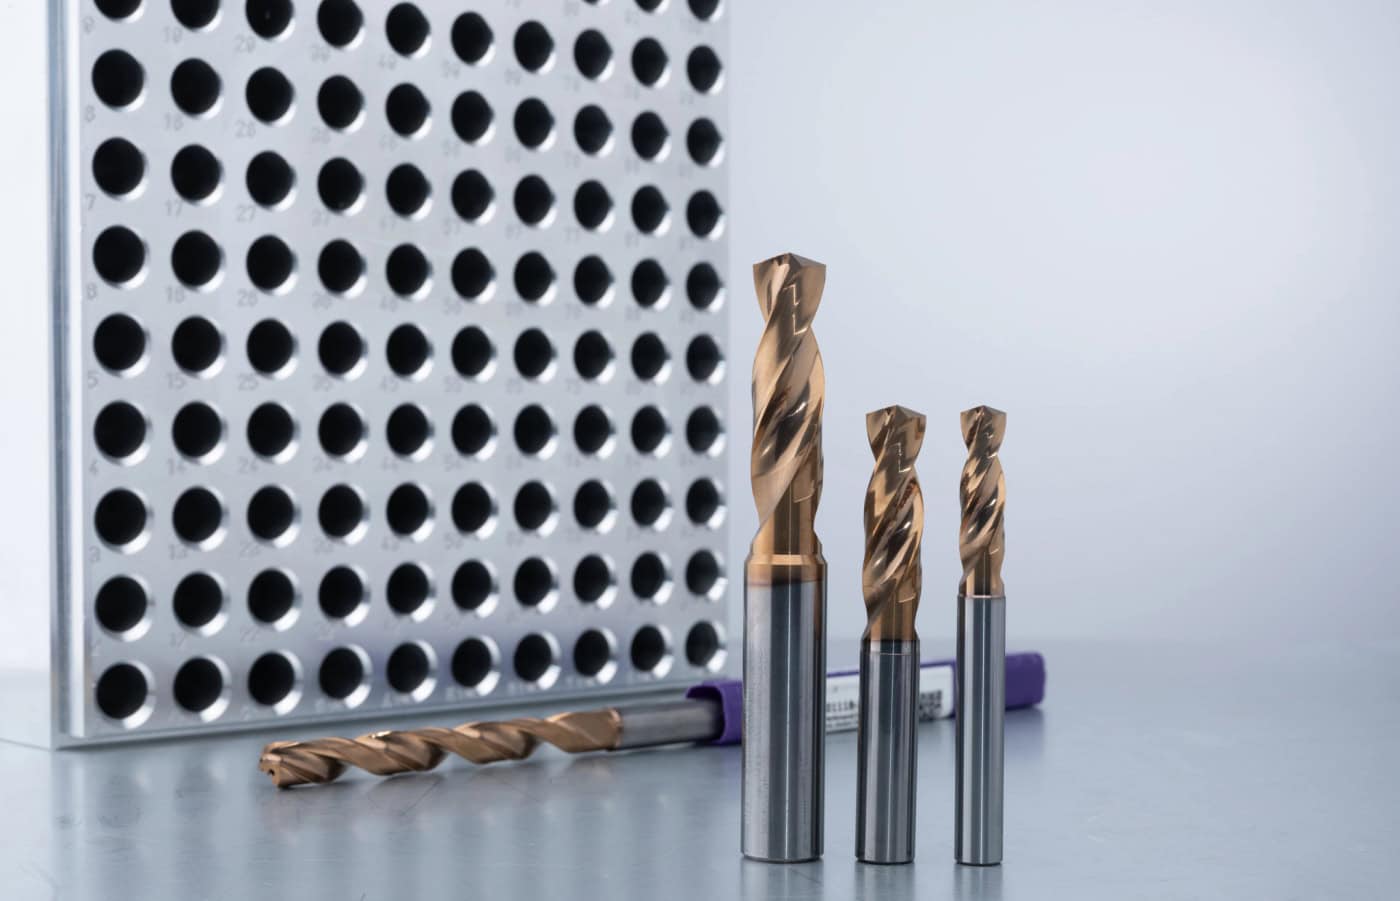
What is a Pilot Drill?

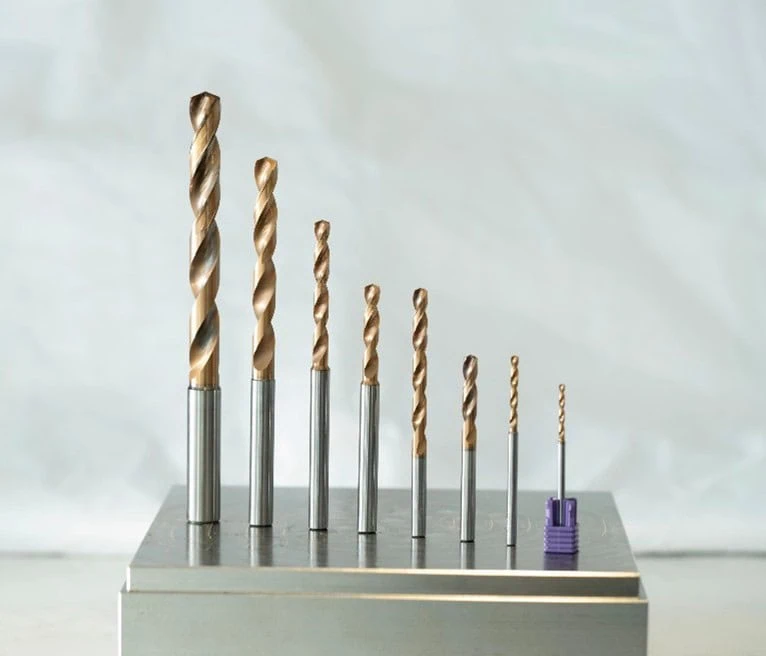
A pilot drill is used to create a guide hole in deep drilling applications where precision is required. This guide hole keeps the drill on center, maintaining straightness throughout the cut. By creating a pilot hole, machinists can also improve the quality of the finished product and extend the life of their tools.

The Importance of Pilot Drills in CNC Machining

1. Enhanced Accuracy

The primary advantage of using a pilot drill is the enhanced accuracy it provides. When working with harder materials or complex geometries, a small pilot hole helps maintain the alignment of the longer drill, reducing the risk of misalignment and defects.

2. Extended Tool Life

Using a pilot drill can significantly extend the life of your deep-hole drilling tools. By first creating a pilot hole, the chasing drill experiences less stress, reducing wear and tear, and the chance of breakage, ultimately leading to cost savings from longer tool life.

3. Improved Chip Removal

Pilot drilling can enhance chip removal, particularly in deep-hole drilling scenarios. The smaller pilot hole allows for better coolant flow, which is crucial for effective chip evacuation and maintaining optimal cutting temperatures.
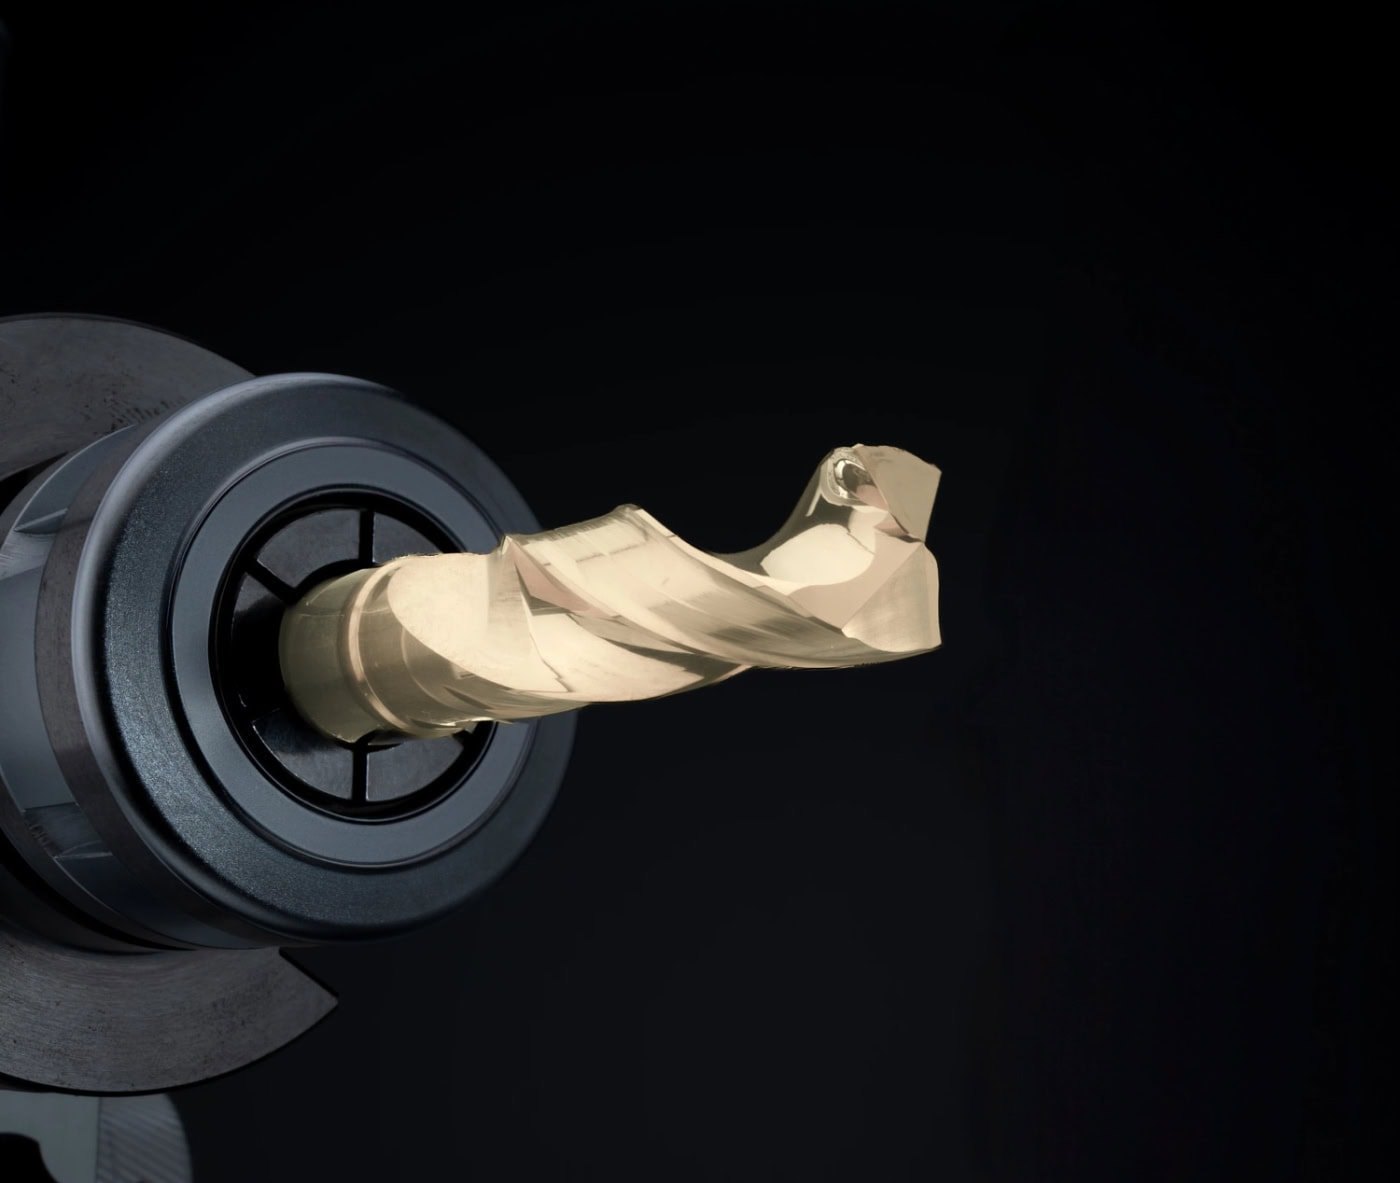
Applications of Pilot Drills

Pilot drills are versatile and can be used in various applications, including:

  1. Deep-hole Drilling: Pilot holes create a guide when drilling deep holes for improved centering and straightness.
  2. Tapping Operations: A pilot hole can facilitate easier and more accurate tapping.
  3. Reaming: When preparing for reaming operations, a pilot drill can ensure the hole is properly aligned and sized.
  4. Screw and Bolt Holes: Pilot holes are essential for ensuring screws and bolts are inserted correctly and securely.

Best Practices for Using Pilot Drills

1. Application      

Piloting is recommended for tighter tolerance holes when drilling at depths of 8xD or greater. Valor Holemaking provides a custom tolerance of +0.0002/+0.0005 (+0.005mm/+0.013mm) to create the perfect oversized guide hole for their traditional drill lines capable of drilling 8xD or greater. Valor Holemaking’s Pilot Drills also include a +2/+1 deg angle tolerance to ensure a larger angle than the chasing drill. Piloting depth is recommended as 3xD for all applications drilling 8xD or greater.

2. Choose the Right Size and Point Angle

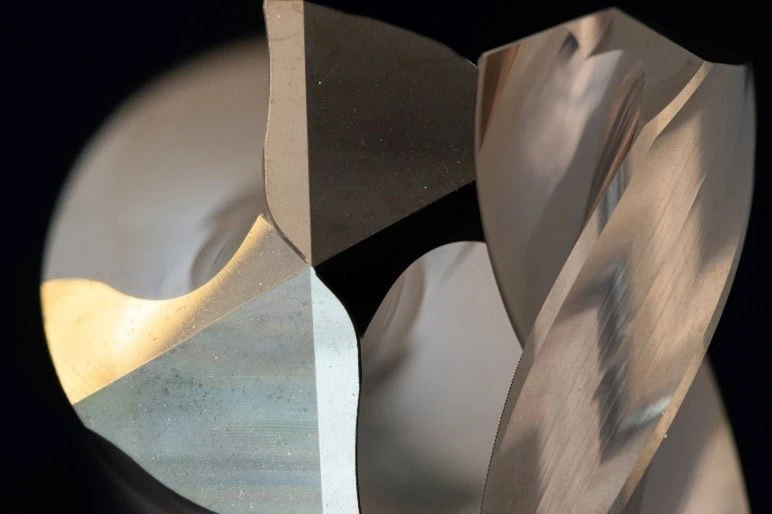
Selecting the appropriate size for your pilot drill is crucial. As a rule of thumb, the diameter of the pilot hole should be slightly larger than the diameter of the final hole. This allows for optimal support for the chasing drill while preventing excessive material removal. The pilot drill’s point angle should be equal to or larger than the succeeding drill. This allows the tip of the succeeding drill to engage the material before the flank does (see figure below).

3. Optimize Feed Rates

When using a pilot drill, ensure that the feed rates are optimized for both the pilot and the larger drill. Adjusting the feed rate can improve performance and reduce the risk of tool breakage. Valor Holemaking’s downloadable speeds and feeds tables and Machining Adviser Pro are excellent resources, and you can always consult Valor Holemaking’s Tech Team for further assistance!

4. Use Proper Coolants

Effective cooling and lubrication are vital in metal machining. Ensure that your pilot drill is adequately cooled with flood coolant or adjust speeds and feeds to maintain tool integrity and enhance cutting performance.

5. Maintain Tool Condition

Regularly check the condition of your pilot drills. Worn or damaged pilot drills can lead to inaccuracies and affect the performance of subsequent operations.

6. Integrate with CNC Programming

Incorporate pilot drilling into your CNC programs to ensure that it’s executed at the right stage of your machining process. Program one revolution or brief dwell at the bottom of the pilot hole to ensure a clean surface. This will help streamline operations and improve overall efficiency.


Conclusion

Pilot drills may seem like a small detail in the larger scope of CNC machining, but their impact on precision, tool life, and overall efficiency is significant. By understanding their importance and implementing best practices, machinists can enhance their processes and achieve superior results. Whether you’re a seasoned CNC operator or just starting out, incorporating pilot drills into your workflow is a smart move that can lead to greater accuracy and success in metal machining.
https://www.harveyperformance.com/wp-content/uploads/2024/12/Featured-Image-Pilot-Drills-IMG.jpg 525 1400 Emily Van Volkom http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Emily Van Volkom2024-12-10 13:53:412025-01-30 09:11:16Mastering Precision: Pilot Drills in CNC Machining

Mastering CNC Drilling: Geometries and Key Factors

August 9, 2024/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Holemaking, Large Featured, Machining 101, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Harvey Performance Company

Selecting the proper drill for a specific application is essential to ensuring a successful cnc drilling job. Achieving a perfectly machined hole can often be challenging. There are many machining woes that can occur when drilling into a material. These can greatly affect hole quality, and regardless of the material being machined, there is often zero margin for error to ensure all components meet specifications.

To ensure you are selecting and using the correct drill, you need not only a deep understanding of drill geometries, but also the factors that influence the performance of the drill and quality of the hole. In this comprehensive guide, we’ll dive into drill geometries, while also exploring the performance factors that determine CNC drilling results. Furthermore, we’ll connect these to the strategic decisions that drive the tool selection process, so you can gain a competitive edge at the spindle.

Performance Factors Influencing CNC Drilling Success

Part Material

Different materials require different drill geometries and cutting speeds to maintain hole quality and prevent excessive wear. With different types of materials, whether it be a softer non-ferrous material like aluminum or a harder ferrous material like stainless steels, you’ll face different challenges as you manufacture your part. To ensure that you’re getting the best performance and tool life possible features and geometries must be considered.

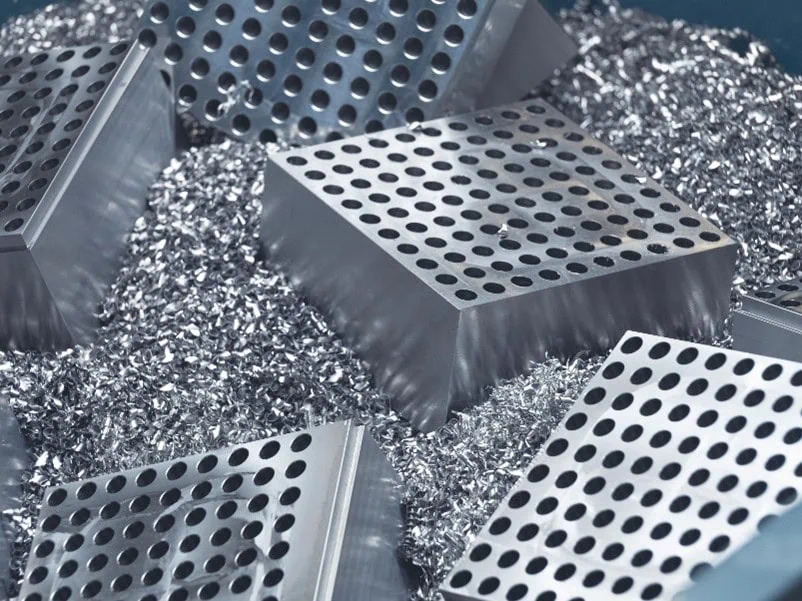
metal blocks that have many holes from cnc drilling operations

CNC Drill Geometries

It is important to understand the different geometries of a drill to understand how they affect an application. For an in depth dive into drill geometries, read 10 CNC Drill Geometries Every Machinist Must Know. This breaks down the unique aspects of geometries and how they affect the cnc drilling process.

Drill Geometries and Drill Walking

CNC drill walking occurs when a drill lacks sufficient engagement with the material. This causes it to deviate from its intended tool path, leading to inaccuracies in hole placement and dimensions. This occurs due to various factors, often including improper drill geometry choice. Understanding how different drill geometries influence drill walking is crucial to ensure you’re achieving precision and consistency in every hole.

Point Angles

The point angle dictates cutting forces and chip evacuation. Choosing the right angle, such as 118° or 135°, based on material hardness, ensures efficient drilling and prevents walking. The shallower the point angle, the better the distribution of cutting forces on the material. Higher angles walk less, as the point grabs into the material easier. Machinists must weight these options when choosing the proper drill.

Web Thickness

Web thickness is the distance between cutting edges or flutes at the face of the drill. This is where stability is generated in a tool. Webs that are too thin can increase the likelihood of breakages, while webs that are too thick will generate unnecessary cutting forces. Finding the proper blend of stability and cutting force is a common struggle for machinists.

CNC Drill Length Considerations

Flute and overall length impact stability and chip evacuation. Matching these lengths to drilling depth prevents deflection and enhances hole quality.

While it may be easiest to purchase a long drill that will work in a variety of scenarios, it is not the best choice to ensure precision. Machinists should best match their required depth to the effective depth of a drill. This ensures that the tool will be as rigid as possible, generating the straightest holes.

As tool length increases, rigidity decreases. Therefore, a properly matched drill will be as rigid as the situation allows. This affords the machinist with the best possible outcome for their unique drilling application.

Coolant-Through Drilling

Proper cooling and lubrication extends tool life and ensures excellent hole quality. If your machine is equipped with the option to run through spindle coolant tooling, it can be extremely beneficial to your application. Unlike an end mill, where chips often have the ability to evacuate outward from the tool, the chips in a drilling operating are held captive inside the feature as it’s being drilled. Here, chips are only able to evacuate through the drill fluting

Through spindle coolant not only cools and lubricates a drill at the point of material removal, but also forcibly evacuates the chips. This can increase your tool’s life while reducing or removing the need for peck cycles all together. This means faster cycle times and higher production rates for your product.

On the other hand, coolant can be fed externally, and sprayed onto the tooling. This will aid in cooling and lubricity. The downside is it is less efficient than utilizing a coolant-through drill. In deep hole drilling applications, external coolant is often ineffective for chip evacuation efforts, and is not the ideal choice for the best results.

Speeds & Feeds

Optimizing speeds & feeds is essential for efficient and accurate drilling. There is not a “one size fits all approach” for speeds & feeds, as all tools and materials require a slightly different approach.

Finding the right balance for each material prevents tool wear and ensures effective chip evacuation. Valor Holemaking offers comprehensive starting parameters in the form of Speeds & Feeds Charts and each tool is also supported by Machining Advisor Pro. This tool allows machinist to custom generate speeds & feeds based off the exact tool path, material, and machine setup.

Rigidity and Stability

A sturdy machining setup reduces vibrations during drilling, improving hole quality. The same can be said about the drill within. A rigid tool is a stable tool, especially as the depth requirements increase. Stability is especially important for drilling heavy-duty materials. This can be impacted by several factors, most importantly the quality of the tool and its design, as well as its chip management capabilities. High precision and high-performance solid carbide drills are designed for the utmost rigidity to ensure repeatability time after time and part after part.

Software and Programming

CNC programming software simplifies creating and editing drilling programs. Compatibility with common CAD/CAM software streamlines integration. Much like machine quality, proper programming is an important step in ensuring precision in CNC drilling applications. CAD/CAM integration ensures the correct dimensions are input to the software to best ensure the tool correctly fits the required parameters.

Exploring CNC Drilling Geometries & Key Factors: Wrapped Up

There are many different drill geometries and factors that can directly impact a drill’s performance and hole quality. Understanding these features can greatly assist in your tool selection process, allowing you to improve productivity and hole quality, so you can gain a competitive edge at the spindle. Drilling is often the most precise aspect of machining, so mastering geometries is critical to success.

https://www.harveyperformance.com/wp-content/uploads/2024/08/Featured-Image-Mastering-CNC-Drilling.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-08-09 14:34:572025-11-12 16:00:33Mastering CNC Drilling: Geometries and Key Factors

HSS vs Cobalt vs Carbide: Choosing a Tool Substrate

July 31, 2024/0 Comments/in CNC Machining, Large Featured, Titan USA, Tool Information Guides, Tool Selection/by Allison House

Do you know which cutting tool substrate is right for you? Popular cutting tool manufacturers, such as Titan USA, oftentimes sell high speed steel, cobalt, and solid carbide cutting tools – but which is right for your application? This article will serve as a guide to the benefits of each material, and the best choice for specific applications.

At the same time, do you understand the differences of high speed steel vs cobalt vs carbide? Follow along for the key differences of the three substrates.

High Speed Steel Tooling

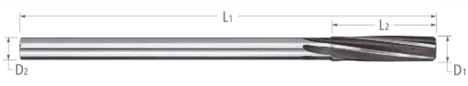
Titan USA High speed steel reamer with callouts

When it comes to high speed steel tooling, this will be the most economical choice among the three substrate options. The above image shows a Titan USA High Speed Steel Reamer.

High speed steel is known for its high working hardness and excellent toughness. While maintaining a rigid set up should always be a priority, high speed steel tooling can excel in situations where a rigid set-up can’t be obtained, and where there is potential for excessive tool holder overhang. The toughness of high speed steel over cobalt and solid carbide makes it less prone to brittle fracture or chipping. These tools can be used in a variety of ferrous materials, such as steel and iron, and non-ferrous materials such as brass, copper, and aluminum alloys.  However, high speed steel should not be used in hardened versions of these materials.

This substrate is not without its drawbacks, too, though. High speed steel tooling will need to be run at slower cutting speeds than cobalt or solid carbide tooling, which could potentially make it less ideal for high production runs.

Cobalt Tooling

Titan usa cobalt reamer with dimension callouts


For most situations, cobalt is going to offer an intermediate option when compared to high speed steel and solid carbide options. The image above shows a Titan USA Cobalt Reamer.

Cobalt can be run even faster than high speed steel tooling. It can also be used in most hardened and abrasive materials such as bronze, stainless steel, cast iron, and titanium.

However, a cobalt bit will not retain its edge sharpness for as long as a solid carbide bit, and it will be more prone to brittle failure than high speed steel tooling in non-rigid set ups.

If you have a desire to run at faster running parameters than what high speed steel tooling offers, or if you are running in a hardened material, cobalt may be your next consideration. While it will typically have a higher cost than high speed steel tooling, it would be a more economical option than solid carbide.   


Solid Carbide Tooling

Titan USA Carbide reamer with dimension callouts

Solid carbide will be the premier material substrate offered for most cutting tool selections, as it offers high edge sharpness that allows tooling to be run at the fastest running parameters offered among the three material substrates. The above image shows a Titan USA Solid Carbide Reamer.

Although solid carbide tends to be the most expensive substrate option, the ability to run at high speeds and feeds allows you to reduce your cutting time. This increased productivity can prove to be more economical for higher production jobs. Solid carbide tooling is going to have the highest heat and wear resistance, allowing the tooling to last longer and require less replacement.

Further, solid carbide is a good choice when dealing with hardened materials or high temp alloys. For example, it can be used in hardened steels, titanium alloys, and nickel alloys up to 45RC. When paired with material specific tool geometries and coatings, solid carbide can even be used in materials up to 68Rc.

One downside to solid carbide tooling is that its high hardness can make it more susceptible to brittle failure and therefore may not be a good choice when dealing with non-rigid set ups. For example, solid carbide can be more prone to chipping or breaking when encountering interrupted cuts, vibrations, or shocks.

Substrate Options

Substrate Options

When browsing the different material options offered by Titan USA, this article can act as a helpful guide for choosing the right tool for your application.  For more information on the different tooling styles offered in high speed steel, solid carbide, and cobalt, please visit the Titan USA website at https://www.titancuttingtools.com/ .

Sources:

  1. Chitnis, Rohit. “HSS vs Cobalt vs Carbide Drill Bits: What to Choose.” Benchmark Abrasives, Benchmark Abrasives, 29 June 2022, benchmarkabrasives.com/blogs/news/hss-vs-cobalt-vs-carbide-drill-bits-what-to-choose.
  2. “A Comprehensive Guide to Pros and Cons of Carbide Tools and HSS.” TJ Grinding, 8 May 2018, tjgrinding.com/blog-post/comprehensive-guide-pros-and-cons-carbide-tools-and-hss.
  3. “High-Speed Steel vs Carbide Tools: AIMS Industrial.” AIMS Industrial Supplies, www.aimsindustrial.com.au/blog/hss-vs-carbide. Accessed 17 June 2024.
  4. Startoolinc. “The Difference between High speed steel & Carbide End Mills.” Tool Talk, 11 Feb. 2020, tooltalk.blog/the-difference-between-high-speed-steel-carbide-end-mills/#:~:text=Compared%20to%20HSS%2C%20carbide%20tools,to%20face%20milling%20and%20beyond.
https://www.harveyperformance.com/wp-content/uploads/2024/07/Featured-Image-Selecting-Cutting-Tool-Substrate.jpg 525 1400 Allison House http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Allison House2024-07-31 16:29:122025-11-12 15:58:06HSS vs Cobalt vs Carbide: Choosing a Tool Substrate

Aerospace Drill Type Classifications Explained

July 31, 2024/0 Comments/in Drilling, Drilling & Holemaking, Small Featured, Titan USA, Tool Information Guides/by Ryan O'Connell

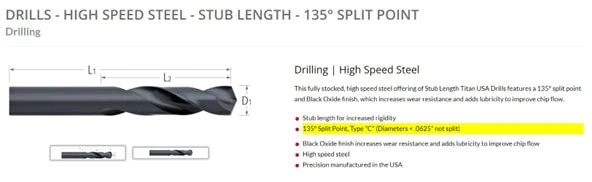
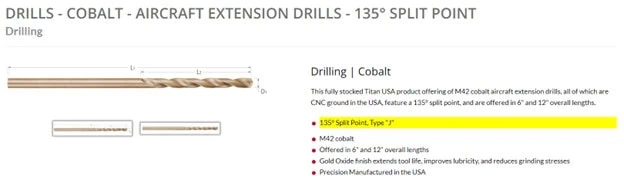
When browsing Titan USA’s selection of available drill bits, you may come across descriptions like “Type B,” “Type C,” or “Type J.” The following will serve to explain the origins of these designations and what each “Type” means; information that will help you when selecting the optimal drill bit for your operation.

Origin of Drill Type Classifications

The drill “Types” referenced above are creations of the National Aerospace Specification Committee (NASC), a subset of the Aerospace Industries Association (AIA). The Committee is responsible for the creation and maintenance of part standards for aerospace parts and components within AIA’s National Aerospace Standards (NAS) library. These part standards are recognized for meeting the high strength, close tolerance, and rigorous acceptance testing requirements of the aerospace industry.[1]

Aerospace Drill Standards & Types

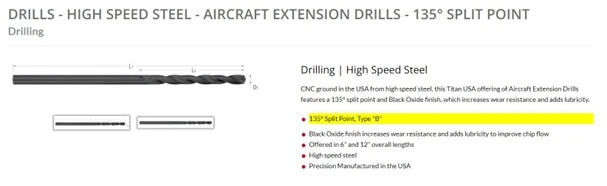
The NASC identifies three different “standards” for drills: NAS907, NAS937, and NAS965. Each of these standards can be broken down into different “types.” The “standard” represents the size range and shank options, and the “type” represents a unique combination of other attributes including material, surface treatment, web construction, back taper, point type, and lengths. For example, NAS 937 drills have a size range of Ø1/8” through Ø1/2” and the following shank options: Straight, straight w/ tri flats, quick change, reduced shank, reduced shank with tri flats, and Tang. Type B within that same standard would indicate that the material is High Speed Steel (M2 or M7), that the drill has a bright finish, a web construction where thickness increases uniformly at 0.017” ± 0.003” per inch taper, a back taper of 0.0002” to 0.0005” per inch for all diameters, a P-3 (135°) split point, and a jobber or aircraft extension length.

All the drills that call out a type in Titan USA’s catalog are NAS907 standard drills as they all have drill diameters of 1/16” through 1/2” and straight shanks. Below are examples of Titan USA drills of types B, C, and J within that standard:

Type B

screenshot from titan cutting tools of an aerospace type b drill

Type C

Screenshot from Titan Cutting tools of an aerospace type c drill

Type J

Screenshot from Titan Cutting Tools of a Type J aerospace drill

Choosing the right drill bit for your job is key to ensuring accuracy and efficiency in any project, and knowing what these type designations represent can help you identify the size and material that’s right for you more quickly.

Do you have an application that requires a miniature drill? Learn about Selecting the Right Harvey Tool Miniature Drill.


  1. [1] National Aerospace Standards Committee (NASC). “About NASC.” Aerospace Industries Association, www.aia-aerospace.org/membership/committees/national-aerospace-standards-committee-nasc/. Accessed [April 26, 2024].
https://www.harveyperformance.com/wp-content/uploads/2024/07/Featured-Image-Drill-Type-Classifications.jpg 525 1400 Ryan O'Connell http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Ryan O'Connell2024-07-31 16:29:102025-11-12 16:01:32Aerospace Drill Type Classifications Explained

Corner Comparison: Corner Chamfer vs. Corner Radius

July 8, 2024/0 Comments/in CNC Machining, Milling, Milling, Tool Geometry, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

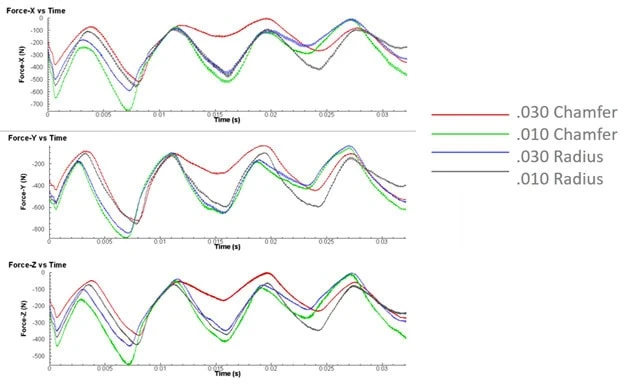
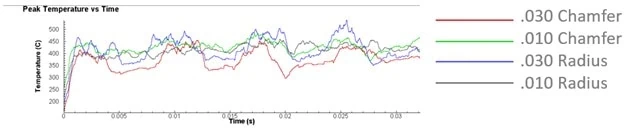
Using Finite Element Analysis (FEA) simulations by Third Wave Systems’ AdvantEdge CAE product, we tested different end mill corner geometries to compare their effects on both the tool and the workpiece. We studied and compared four 4 flute tools with either a 0.010” or 0.030” radius or chamfer. All tools were tested in 304 stainless steel at 1865 RPM, 244 SFM, and 0.0045 IPT for one revolution.

Both Corner Radius and Corner Chamfer tools offer advantages over Square End Mills by improving tool strength and reducing wear, though their benefits vary. One drawback of corner radius end mills is chip thinning along the radius, which can generate excess heat due to changes in chip thickness. This can lead to premature tool wear, poor surface finish, and potential work hardening. On the other hand, Corner Chamfers have the disadvantage of sharp corners where the chamfer meets the outer diameter (OD) and the end of the tool, causing local stress concentrations.

Force Analysis

The graphs above demonstrate the force exerted on the tool during cutting and how the corner size impacts the required force. As each flute engages, the forces peak in each direction. The 0.010” Chamfer generates the greatest force, while the 0.030” Chamfer requires the least. The forces with the radiused tools are very similar and fall between those of the two chamfered tools.

Temperature Analysis

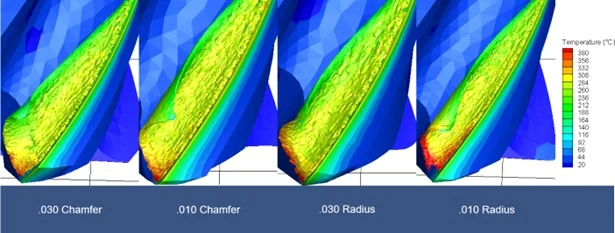
The peak tool temperature graph shows the impact of chip thinning on corner radius tools and the overall corner size. The 0.030” Radius generated the most heat, while the 0.030” Chamfer generated the least. The temperature differences between the 0.010” Chamfer and 0.010” Radius was minimal, with the 0.010” Radius generated slightly less heat.

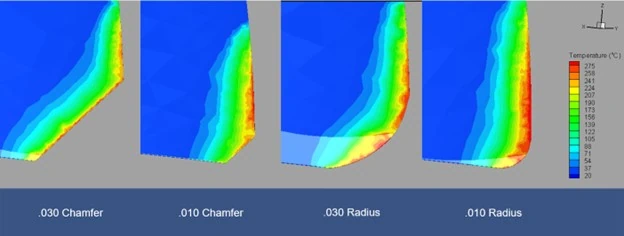
Chip and Workpiece Temperature

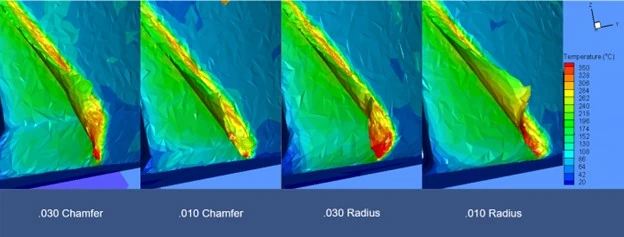
Understanding the temperature of the chip and workpiece is crucial for assessing tool performance. The contours above illustrate that the most heat is generated along the 0.030” Radius, followed by the 0.010” Radius. Corner Chamfer tools performed better, maintaining a lower overall temperature due to the absence of chip thinning.

Stress Analysis

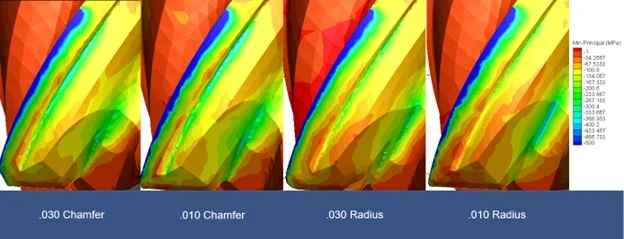
The minimum principal stress on the backside of the flute indicates areas prone to tool failure. While there were slight differences between the chamfers and radii, the most notable finding was the reduction in stress with increased corner break size.

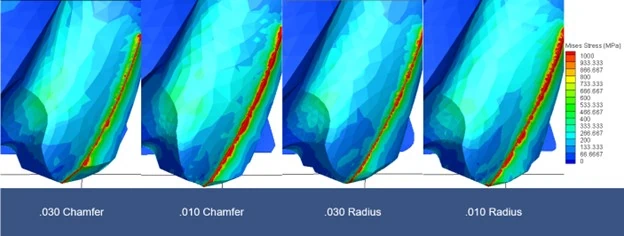
Similarly, the Mises stress analysis shows where stress is concentrated within the tool, potentially leading to failure. Again, the most significant observation was the reduction in stress with larger corner breaks.

Corner Chamfer vs. Corner Radius: Wrapped Up

Considering all factors, the 0.030” Corner Chamfer proved to be the best overall tool for 304 stainless steel. This is partly due to 304’s tendency to work harden, making excess heat generation particularly detrimental. When working with heat-sensitive materials, Corner Chamfer tools are preferable, especially during roughing, as they generate less heat due to the absence of chip thinning. Although there are minor stress concentrations at the sharp corners of Corner Chamfer tools, these are outweighed by the benefits of reduced heat generation. Larger radii exacerbate chip thinning’s impact on heat generation. While both tool styles offer advantages over square end mills, Corner Chamfer tools are more beneficial in high-heat applications where work hardening and tool wear are concerns.

Harvey Tool offers a range of Corner Chamfer Tools, with sizes ranging from 0.047” to 0.500” and various chamfer sizes to suit different applications.

https://www.harveyperformance.com/wp-content/uploads/2024/07/Featured-Image-FEA-Corner-Comparison.jpg 525 1399 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-07-08 12:15:282024-07-12 12:45:27Corner Comparison: Corner Chamfer vs. Corner Radius

Recycling Carbon Fiber: Importance & Process

July 8, 2024/0 Comments/in CNC Machining, Composites, How-To's, Material Specific, Milling, Trending Now/by Sarah Wasson

Carbon fiber is a woven cloth made of crystalline filaments of carbon cured with a polymer, which can be layered and shaped around a mold. It is an ideal material due to its impressive strength-to-weight ratio , meaning it’s very strong, but not heavy. Carbon fiber is five times lighter than steel with an equal elastic modulus, making it a better choice for many applications. Further, it is corrosion-resistant, non-flammable, and non-toxic, properties that make it an ideal material to use in aerospace, medical, construction, and military industries.

Machining Carbon Fiber

Machining Carbon Fiber can be challenging. The layered structure of the carbon fiber material can lead to delamination, uncut fibers, fiber tear-out, uneven tool wear, and poor surface finishes. Luckily, many cutting tool companies, like CoreHog, specially design tooling with different geometries that can help eliminate these manufacturing problems:

  • Straight Flute End Mills: Apply all the cutting forces radially, which helps prevent delamination.
  • Compression Cutters: Create opposite cutting forces, stabilizing material removal and preventing delamination, fiber pullout, and burrs along the surface.
  • Chipbreaker Cutters: Shear the fibers and shorten the chips, preventing fiber buildup around the cutter.
  • Diamond Cut End Mills: Utilize both left-hand and right-hand flutes to break up and shear through the fibers, ideal for roughing and profiling carbon fiber.

Explore CoreHog’s Wide Offering of Composite-Laminate Cutters, each specially engineered to cut difficult-to-machine laminate materials like carbon fiber.

Common Carbon Fiber Applications

In the aerospace industry, carbon fiber is used in plane structures to replace alloys, creating lighter planes and thus, reducing fuel consumption. Recreational sports also utilize carbon fiber to decrease weight. It is often seen as a leading material in skis, bikes, and tennis rackets, as the lighter weight can help improve performance. In professional sports leagues like Formula 1 and NASCAR, carbon fiber has grown in prevalence in recent years. Another advantageous quality of carbon fiber is its suitability in X-ray machines, allowing imaging to pass through without interruption, making it useful in many medical devices and implants.

Recycling Carbon Fiber

Why is Recycling Carbon Fiber Difficult?

Carbon fiber sheets require a significant amount of energy to produce. These large sheets are then cut down to the part size needed, and the excess material is often discarded, increasing waste production. This material is not biodegradable and is typically sent to a landfill where it will remain permanently. Further complicating recycling, carbon fiber is built to hold its shape and strength and cannot be melted down and reshaped like many plastics. When recycled, its properties are heavily degraded, rendering it useless for applications that experience heavy forces or loads.

How is Carbon Fiber Recycled?

Solvolysis

Solvolysis uses a chemical solvent to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces, increasing the surface area. The solvent, chosen based on the polymers used in the carbon fiber, breaks down the polymer chains, separating the carbon fiber from the polymer. Techniques like centrifugation are used to separate the substances. The carbon fiber can be further purified to restore its properties and then combined with virgin fibers to create new fabric or used by itself. This process enables the recovery of carbon fiber without sacrificing material properties.

Pyrolysis

Pyrolytic utilizes heat to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces and then heated in a controlled environment with limited or no oxygen. At high temperatures, the polymer undergoes thermal decomposition, producing gases, vapors, and char. The gases and vapors can be used as an energy source or further processed, while the char, which is carbon fiber and any original additives, is purified to ensure mechanical properties are maintained. The resulting carbon fiber can be used alone or combined with virgin fibers. Pyrolysis is effective for high-quality fiber recovery and energy recovery from gas byproducts.

Carbon Fiber Considerations

As we innovate with new technology, it is important to consider its impact on our planet. Carbon fiber is an amazing material that can improve many aspects across industries; however, the waste generated is not going anywhere but a landfill. Many companies are investing in producing high-quality recycled carbon fiber. With a shift in focus to designing closed-loop systems for composite materials, the future looks bright.

https://www.harveyperformance.com/wp-content/uploads/2024/07/Feature-Image-Recyling-Carbon-Fiber-IMG.jpg 525 1400 Sarah Wasson http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Sarah Wasson2024-07-08 12:00:402024-07-12 12:46:58Recycling Carbon Fiber: Importance & Process

Traditional vs Free Cutting Honeycomb Core Tools

May 16, 2024/0 Comments/in CNC Machining, Composites, Machining Techniques, Material Specific, Milling, Tool Geometry, Tool Selection/by Harvey Performance Company

Precision cutting plays a pivotal role in the manufacturing of honeycomb core. CoreHog, a leading provider of composite cutting solutions, offers two distinct styles of Honeycomb Core Finishing Tools: Traditional Finishing Core Tools and Free Cutting Tools. In this post, we explore the advantages and limitations of both Traditional Finishing Core Tools and Free Cutting Core Tools, helping you determine the right choice for your unique manufacturing needs.

CoreHog’s Large Core Finishing Tool

Advantages of Traditional Honeycomb Finishing Tools:

CoreHog’s Finishing Core Tools are designed to handle substantial cutting tasks, efficiently. With three size ranges available, they excel at removing high volumes of material and boast excellent tool life, making them ideal for production applications.

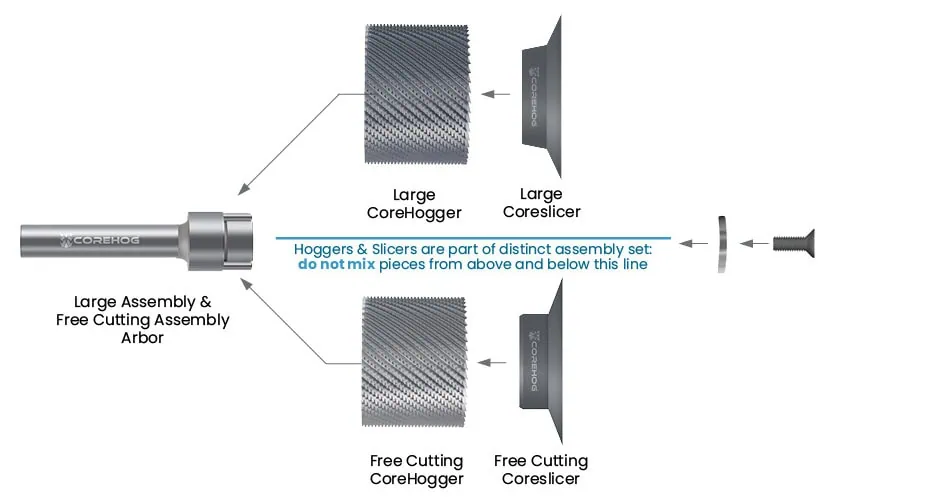
assembly infographic of corehog's honeycomb core finishing tools

Assembly Configuration of CoreHog’s Large & Free Cutting Finishing Core Tools


However, these tools may pose limitations in specific applications. Traditional tools exert tool pressure, but depending on the tool geometry and part profile, the pressure may be too much for the part. This becomes more pronounced when cutting knife edge features such as chamfers and bevels, where the pressure exerted by the tool can cause the part to arch, dislodging it from the table, and ultimately causing it to deviate from specifications.

Introducing Free Cutting Core Finishing Tools:­­

To address the limitations of traditional honeycomb core finishing tools when cutting knife edge features, CoreHog offers Free Cutting Finishing Core Tools. The innovative design reduces tool pressure seen in both the Coreslicer and CoreHogger. The Free Cutting Coreslicer features a more acute and sharper angle, reducing the upward pressure exerted on the part during cutting.

 Differentiation of angle between the Large Coreslicer and the Free Cutting Coreslicer

Further, these tools feature a CoreHogger with a reduced diameter, allowing for greater offset between the CoreHogger and Coreslicer. This allows the Coreslicer to be more forward and free cutting, engaging with the material prior to the CoreHogger and reducing the resulting pressure typically exhibited by the CoreHogger.  

large and free cutting honeycomb core finishing tools

Reduced diameter design of Free Cutting CoreHogger decreases tool pressure on the part.

When to Use Free Cutting Tools:

CoreHog’s Free Cutting Core Finishing Tools are particularly well-suited for applications involving chamfering, beveling, and cutting angled profiles in honeycomb core materials. By reducing pressure and preventing lifting on the part, these tools ensure precise cuts without compromising part quality.

­­Traditional vs. Free Cutting Core Finishing Tool: Summarized

In conclusion, choosing the right cutting tool is crucial for achieving precise results in composite manufacturing. While traditional finishing core tools excel in handling substantial tasks, they may pose challenges when cutting angled profiles in honeycomb core materials. CoreHog’s Free Cutting Core Finishing Tools offer a solution by minimizing pressure on the part, making them ideal for chamfering, beveling, and most other angled profiles. However, in finicky applications where the knife edge part is extremely shallow, a Valve Stem Cutter may still be necessary to achieve your desired cut. By understanding your specific cutting requirements, you can select the most suitable tool for your application, ensuring optimal results in your honeycomb manufacturing processes.

https://www.harveyperformance.com/wp-content/uploads/2024/05/Feature-Image-Free-Cutting-Core-Tools.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-05-16 14:41:282025-11-20 09:49:41Traditional vs Free Cutting Honeycomb Core Tools

Maximize Efficiency With Micro 100 Tool Holders

April 12, 2024/0 Comments/in Micro 100, Turning/by Harvey Performance Company

The Micro 100 Spring 2024 Product Catalog will feature hundreds of new products, including a significant increase to its offering of both standard-style and quick change-style tool holders. These unique additions include several Double-Ended styles: Standard Double-Ended Similar ID, Standard Double-Ended Dissimilar ID, Standard Double-Ended ER, Quick Change Double-Ended Similar ID, Quick Change Double-Ended Dissimilar ID, and Quick Change Double-Ended ER.

These new Double-Ended Holders were designed to be utilized with each other to reduce set up time, and eliminate the time a machinist often spends searching for the correct size tool holder.

As an example, when a Swiss Machine is loaded with multiple combinations of holders, such as a Similar ID, Dissimilar ID, Standard with ER, and Quick Change with ER, a machinist can have all of the ID connections they require residing right in the machine, thereby reducing time spent searching for a correct holder. Holders can be flipped end-for-end to utilize a different size ID at the spindle of your choosing, and – if programmed properly from part-to-part, minimal tool position changes would be required.

The following animations are designed to provide a look at the functionality of each holder style, and the unique benefits they provide for machinists.

Standard Double-Ended Similar ID Holders

In the above animation of Standard Double-Ended Similar ID Holders, the holder enters from the left side of the screen and shows how a standard style turning tool can be entered from each end, and secured with a set screw on each side. Please note that this holder requires tools with the same shank diameter size be utilized on each side.

On the right side, the screw is then removed and the tool is removed, slightly, from the holder, before the set screw is replaced. This showcases that the tool can be positioned in several different ways in this holder, and can accommodate a project with any reach length.

Shop Standard Double-Ended Similar ID Holders

Standard Double-Ended Dissimilar ID Holders

With the Standard Double-Ended Dissimilar ID Holders, the same benefits apply as with the Standard Double-Ended Similar ID Holders. The only difference between the two styles is that one end of the Dissimilar ID Style Holders accommodates a shank diameter size one size larger than the other. Overhang can be set to meet customers’ reach and harmonics requirements.

Shop Standard Double-Ended Dissimilar ID Holders

Standard Double-Ended ER Holders

[

With Standard Double-Ended ER Holders, we see the holder enter from left, and a standard tool is first inserted into the “B Side” of the holder. Then, we see a tool inserted into a Micro 100 ER Collet, before it’s connected to the “A Side” of the holder. This holder provides maximum versatility to machinists who need to utilize a rotating-type tool in static applications, such as for drilling, reaming, or spotting.

Shop Standard Double-Ended ER Holders

Quick Change Double-Ended Similar ID Holders

Designed to be used with Micro 100’s Quick Change Tooling, these Quick Change Double-Ended Similar ID Holders work by inserting a tooling with the same shank diameters into each side, until it reaches an internal locating and locking pin. A set screw then secures the tools in place on each side. Note that because of the locating and locking pin, reaches cannot be adjusted with Quick Change holders.

Shop Quick Change Double-Ended Similar ID Holders

Quick Change Double-Ended Dissimilar ID Holders

In this animation, a Micro 100 Quick Change tool with a ¼” shank diameter is inserted into the “A Side” of the holder. A Micro-Quik tool with a shank diameter one size larger, 5/16”, is then inserted into the “B Side.” Both sides are then locked into place with a set screw.

Shop Quick Change Double-Ended Dissimilar ID Holders

Quick Change Double-Ended ER Holders

In the above animation of Micro 100’s Quick Change Double-Ended ER Holders, a Micro-Quik tool is inserted into the “B Side,” and locked into place with a set screw, before a Micro-Quik drill is inserted into a Micro 100 ER Collet, before being screwed into the “A Side” of the holder.

Similar to the standard style of this holder, this allows one end of the holder to house a rotating tool in static applications.

Shop Quick Change Double-Ended ER Holders

Quick Change Double-Ended Holders in Machine

In this animation, three Quick Change Double-Ended holders slide into the Y-Axis tooling block, and screws tighten down to lock the holders in place. The Quick Change Double-Ended Dissimilar ID Holder is removed from the Y-Axis tooling block, and flipped around, showcasing the ability of most of Micro 100’s Double-Ended Holders to be flipped end-for-end without having to take apart the assembly, reducing the amount of set up time needed between tool changes. Next, the ER Collet, Nut, and Spotting Drill are removed from the Quick Change Double-Ended ER Holder and replaced with a Miniature Drill, highlighting the ability to change tools on the ER end without having to remove the holder from the machine.

Shop Quick Change Double-Ended ER Holders
https://www.harveyperformance.com/wp-content/uploads/2024/04/M100-Holders-Blog-Featured.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-04-12 11:02:582025-11-20 09:48:23Maximize Efficiency With Micro 100 Tool Holders

Multi-Axis Finishers: The Key to Amazing Surface Finish

March 29, 2024/0 Comments/in CNC Machining, Helical Solutions, Large Featured, Tool Information Guides, Tool Selection/by Tom Pyle

A Key to Improving Surface Finish

In today’s Manufacturing Industry, part finish and machining efficiency are key to a successful machine shop. It’s no surprise, therefore, that the popularity Multi-Axis Finishers has never been greater. Helical Solutions is a leader in the manufacturing of Multi-Axis Finishers, and its customers utilize this impressive tool when faced with extremely high surface finish requirements, oftentimes swapping out a traditional Ball End Mill to dramatically improve finish while minimizing cycle times.

Multi-Axis Finisher Basic Principles

A Multi-Axis Finisher can be easily recognized by its large radius included in the profile of the tool. With a larger radius, a far greater stepover can be used pass-to-pass while keeping the same cusp height as a Ball End Mill. This decreases the cycle time by a known value called the Benefit Multiple.

A Multi-Axis Finisher with a Benefit Multiple of 8 will reduce the cycle time to 1/8 of the cycle time for a Ball End Mill of the same shank diameter – an 87.5% time savings! If a Multi-Axis Finisher is used with the same pass-to-pass stepover as a Ball End Mill, the finish will be drastically improved due to exponentially smaller cusp heights. Most situations allow both reduced cycle time and improved surface finish to be achieved.

The images below show the comparison of a ball end mill to an Oval Shape Multi-Axis Finisher with a benefit multiple of 4.

Due to their large radii, Multi-Axis Finishers are best suited for wide open, flowing, and somewhat flat surfaces. Smaller spaces, especially tight corners, will generally not see as much benefit from these tools due to limited use of the major radius.

Multi-Axis Finisher Tool Selection

The Manufacturing Industry’s leader in Multi-Axis Finishers, Helical Solutions offers 3 distinct profiles, each fully stocked and available to ship the day of purchase.

Oval Form Multi-Axis Finishers

The oval form includes 2 tangential radii and offers the most versatility in smaller spaces where a slightly varied approach angle is required, such as impellers or fan blades.

Taper Form Multi-Axis Finishers

The taper form includes 3 tangential radii and a taper angle. It allows for the largest radius, and therefore greatest potential improvement of finish and reduction of cycle time. They are best used where a specific approach angle is needed and where maximum performance gain is desired.

Lens Form Multi-Axis Finishers

The lens form includes 2 tangential radii on the end of the tool and is used for work mostly on the face of a part. Tilt angles of approximately 5 degrees are recommended for these tools to avoid working on-center.

Programming Multi-Axis Finishers

Programming Multi-Axis Finishers requires some additional consideration compared to a typical end mill. Luckily, many modern CAM packages offer support for these unique profiles, including many of Helical’s CAM partners. Each software has their own name for these toolpaths, so reach out to your CAM or Helical sales rep to find how you can program yours!

For more information on Multi-Axis Finishers, and to learn if this advantageous tool is right for you, read our Multi-Axis Finishers Q&A.

https://www.harveyperformance.com/wp-content/uploads/2024/03/Featured-Image-Multi-Axis-Finisher-Keys-to-Surface-Finish-1.jpg 525 1400 Tom Pyle http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Pyle2024-03-29 10:27:002024-04-24 09:17:44Multi-Axis Finishers: The Key to Amazing Surface Finish

10 CNC Drill Geometries Every Machinist Must Know

December 11, 2023/2 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Holemaking, How-To's, Quick Tips/by Harvey Performance Company

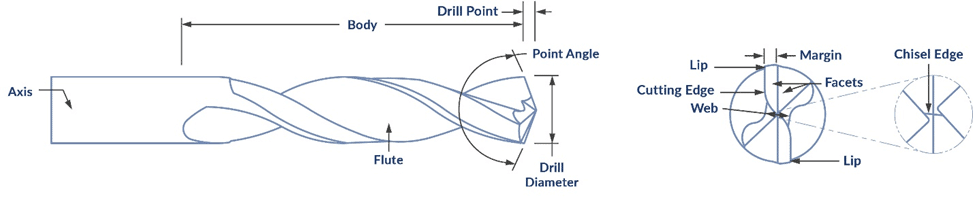
A CNC drill has many different features and geometries that directly impact the tool’s performance, productivity, and tool life in the specific material it’s machining. It is important to understand the different geometries of a drill to ensure you’re not only recognizing how they affect an application, but also which geometries you should be looking for when selecting your next drill. For continued success a machinist must know all aspects that goes into a cnc drill geometry.
1.    Point Angle

This drill geometry refers to the angle of the cutting edge of the drill. As the point angle increases on a drill, the radial forces decrease, making the angle size a huge factor in what type of material the drill is optimized for and what types of applications should be run. The smaller the point angle, the better it will perform in through hole applications. This is because the smaller angle reduces the axial forces, allowing less of the chip to be pushed out and more cutting to occur.

118° & 120° Point Angle

Many machinists opt for this angle when machining soft gummy materials.

135° Point Angle

This point angle size is an excellent choice for machining aluminum and stainless steels.

140° Point Angle

This larger point angle size is great for machining steels.

150° Point Angle

Large angles are often used for spot drilling applications, but the optimal spot drill angle is determined by the size of the angle of the final drill being used. Selecting the proper spot drill is essential to eliminating the chance of drill walking and ensuring a more accurate final product. Learn which spot angle should be used for your next drilling job in this in-depth guide.

2.    Chisel and Cutting Edges


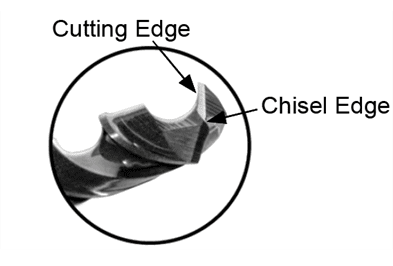
Although the chisel edge of a CNC drill does not provide any cutting action, it is responsible for the centering of the drill, as it extrudes the material towards the cutting edges. The cutting edges are then able to start the process of producing chips, which then travel up the flutes of the drill.

3.    Flutes

The most recognizable part of a drill is its flutes. They are the deep grooves that allow for chip evacuation to occur. When one thinks of a drill, they are likely imagining a spiral flute drill. These spiral flutes complement the point angle, chisel edge, and the cutting edges. They work like an elevator system to lift the chips out of the hole, allowing them to provide excellent chip evacuation. They work great in most material types and provide good hole quality.

4.    Helix Angle

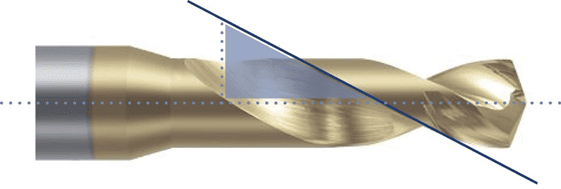
The helix angle is the angle formed by the leading edge of the land with a plane containing the axis of the drill. The main function of the helix angle is to transfer the chips out of the hole and a specific angle is relevant to the type of material that is being machined in and the particular application being run.

Low Helix

A low helix of 12° – 22° is recommended for materials like cast iron, brass, and hardened steels. In these “short chipping” materials, the chips move more freely, and the coolant provides enough assistance to properly evacuate the chips out of the hole.

Medium Helix

The most widely used helix angles are medium as they provide optimal chip evacuation and strength to the drill. Medium helix angles range from 28° – 32° and are recommended for any general purpose drilling applications.

High Helix

A high helix angle of 34° – 38° is recommended for long chipping material such as softer non-ferrous materials like brass, aluminum, and plastics. Drills with a high helix are also beneficial in deep hole applications as the chips can evacuate more easily.

5.    Web Thickness (Core)

The web is the core section of the drill body, which connects the two flutes. The thickness of the web determines the torsional strength of a drill. A drill with a larger web diameter will have more torsional strength than a drill with a smaller web diameter.

The proper web thickness is determined by the material type to be machined. Long chipping materials will require a drill with a smaller web thickness to provide adequate clearance for chip removal. When drilling short chipping materials such as cast iron, the drill web can be increased for additional strength.

6.    Corner Chamfer


A corner chamfer or radius is often added to eliminate the sharp edge at the intersection of the flutes and the outside diameter of a drill. This helps to eliminate material breakout when exiting a hole, while also helping to reduce the size of the entrance and exit burrs. This feature is also widely known to significantly extend tool life.

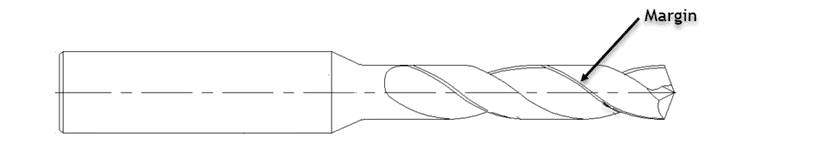
7.    Drill Margin

Margin(s) are the surfaces along the outer diameter of the drill which provide stability to the hole as they support the radial forces that are directed radially by the drill point.

Size of Drill Margin

The size of the margin will determine the overall quality of the hole. Wide marginswill stabilize the drill better, hold a tighter hole diameter tolerance, and improve the circularity of the hole. Narrow margins reduce friction and heat, eliminate work hardening, mitigate built-up edge, and provide better tool life.

Number of Drill Margins

The number of margins on a drill is usually determined by the type of hole being machined. Single margin drills are very common in non-interrupted holes. Double or triple margin drills are common in interrupted or intersecting holes. The more margins there are, the better the guidance is to help the drill stay straight through interrupted cuts, cross holes, and irregular or angled surfaces on exit. While adding margins does provide these benefits for irregular style cuts, they also increase friction, which causes the drill to produce more heat. This causes wear to be accelerated, reducing the life of the tool.

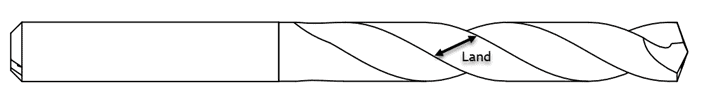
8.    Land of a Drill

The land is the outer portion of the body of the drill between two adjacent flutes. Land width will determine how much torsional force a drill can withstand before catastrophic failure. The smaller the land is, the more chip space there is, producing less torsional strength. The larger the land is, the less chip space there is, providing more torsional strength.

9.    Coolant-Through Channels


Not only do coolant-through channels offer any drilling application a multitude of benefits, but they are also highly recommended for hole depths that exceed 4XD (4 times diameter). Coolant-Through Drills allow for higher speed and feed rate capabilities, increased lubricity, better chip control, improved surface finish, and enhanced tool life.

10.  Shank

The shank is a very important yet overlooked drill geometry as it is the drive mechanism and is what is mounted into a Tool Holder. It is essential that the shank is held to proper diameter tolerance and considerations are being made depending on the holder being used. For example, a shank with an h6 tolerance is essential when a shrink fit style tool holder is being used.

Learning the different geometries of a CNC drill can greatly assist you in ensuring you are selecting the right drill for your next job, while understanding the functions of these features will allow you to trouble shoot any potential machining hiccups you may encounter in your future CNC drilling applications.

https://www.harveyperformance.com/wp-content/uploads/2023/12/Valor-SteelDrill-001-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2023-12-11 11:52:362025-01-28 16:04:3910 CNC Drill Geometries Every Machinist Must Know
Page 2 of 12‹1234›»
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top