Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Micro 100 Broaching Tools: Everything You Need to Know

November 20, 2025/0 Comments/in Large Featured, Micro 100, Tool Information Guides, Tool Selection, Turning/by Steven Velazquez

With the release of Micro 100’s 2025 Spring Catalog comes a new family of broaching tools, marking their debut within both the Micro 100 and Harvey Performance brands. Alongside this tooling launch are several differences in application methods and recommended running parameters.

What is Broaching?

Broaching, while performed in a lathe, is slightly different from the classic boring and grooving operations we encounter daily.

In a traditional turning operation, the workpiece rotates while the tool remains stationary. In a broaching operation, neither the workpiece nor the tool spins. Instead, the tool advances toward the workpiece and removes material in very small increments, similar to planing a block of wood.

Micro 100’s Offering

All broaches come on a Micro 100 Quick-Change shank, with sizes ranging from .1875” to .375”, depending on the broach size. These QC broaching tools are coolant-fed to promote better chip evacuation. An optional nACRo coating is available, enhancing resistance to wear and heat, which is especially useful in applications involving difficult-to-machine materials.

Keyway Broaches

Keyway broaches, as their name suggests, are used to cut keyways commonly found in power transmission applications involving gears and pulleys.
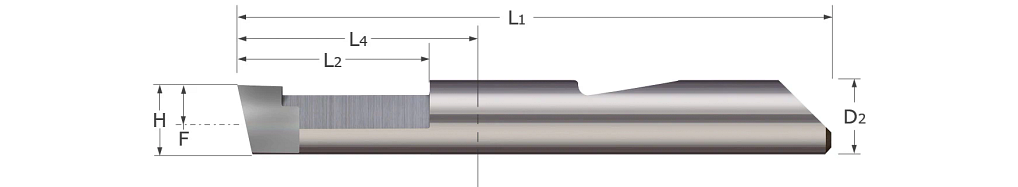
Micro 100 offers two styles of keyway broaches, available in both standard and metric sizing. This offering provides machinists with a range of sizes that are necessary to meet their application needs.

Imperial Offering

Micro 100’s standard-sized broaches come in widths of .0938”, .1250”, .1875”, and .2500”. Maximum broach depths of .500”, 1.000”, or 1.500” are available, depending on the broach width.

Metric Offering

Our metric keyway broaches are available in nominal widths from 2 mm to 6 mm. Each size is measured according to the desired fit and offered in C11, JS9, or P9 tolerance grades.

C11 reflects a “loose fit” tolerance, useful in applications where the keyway may be exposed to corrosion, dust, or other contaminants, or where deformation may occur.

JS9 represents a “normal fit”—not a press fit, but not a loose fit either. This is often required in situations where the key needs to be adjusted or shifted without much force or difficulty.

The tightest of the three offered tolerance classes is P9, which represents a “press fit.” In this case, the keyway is cut slightly smaller than the key, forcing it into the slot to create a very tight and secure connection.

Square Broaching

Micro 100 also offers square broaching tools. These broaches, like the keyway style, are pushed into the workpiece and remove material in multiple passes. They are primarily used to create the square socket found at the top of certain screws, commonly seen in machinery, construction, or other industrial applications.

Our square broaches come in metric sizes and can cut square holes ranging from 1.5 mm to 4.0 mm. When examining the geometry of these tools, you’ll notice they are cut to one corner of the square profile. Unlike keyway broaches, they must be rotated 90° when one corner is cut to create the remainder of the square form.

Although they have a fixed broach width, our square broaches are capable of cutting a range of square sizes. Take our QBRSQ-1520, for example—it features a .056” width and can cut squares from .059” to .078” (1.5 mm to 2.0 mm). When selecting a tool, it’s important to base your choice on the desired finished hole size, rather than the width of the cutter itself.

Hexagonal Broaching

The final option in Micro 100’s broaching lineup is our hexagonal broach style. These tools function similarly to the square broaches mentioned earlier, with the form created in six portions. Our hexagonal broaches can cut forms as small as .078” (2.0 mm) and up to .315” (8.0 mm). As with the square broaches, it’s important to select a tool based on the desired finish size of the hole, rather than the tooth width itself.

Hexagonal holes are often designed to work in conjunction with Allen keys. They are also commonly used for socket head cap screws. These fasteners are widely used across various industries, including automotive and construction settings.

What to do Before Making Your First Chips

Before making a cut with Micro 100’s broaching tools, there are a few important things to ensure are in place. Due to the high force involved in broaching, your machine should be equipped with a mechanical spindle lock. This lock helps achieve a higher-quality finish and, more importantly, improves feature accuracy.

The use of coolant is also strongly encouraged whenever possible, as it helps increase tool life, improve surface finish, and enhance chip evacuation. If your application requires broaching within a blind hole, be sure to create a cross hole or relief groove at the bottom of the hole to allow chips to evacuate properly.

Mastering Square & Hexagonal Broaching

To begin, the broach dimensions must be measured accurately and programmed into the machine. Ensure the tool is positioned at the 12 o’clock location to allow proper chip evacuation.

If cutting a hexagonal profile, the pre-drill should be approximately 1.035 times the desired feature size (1.1× for a square profile).

Before the first pass is made, visually check the tool path by positioning the tool at the starting point of the stroke, and program a stop there to verify correct alignment.

After each pass, ensure the tool is radially clear of the groove before fully retracting it. On the final return stroke, completely remove the broach from the hole. Finally, rotate the workpiece by 60 degrees—90 degrees for a square profile—and repeat the cutting process for the remaining corners.

Best Practices for Keyway Broaching

Keyway broaches require an additional calculation to determine the correct starting position for the first pass. An example calculation is provided below.
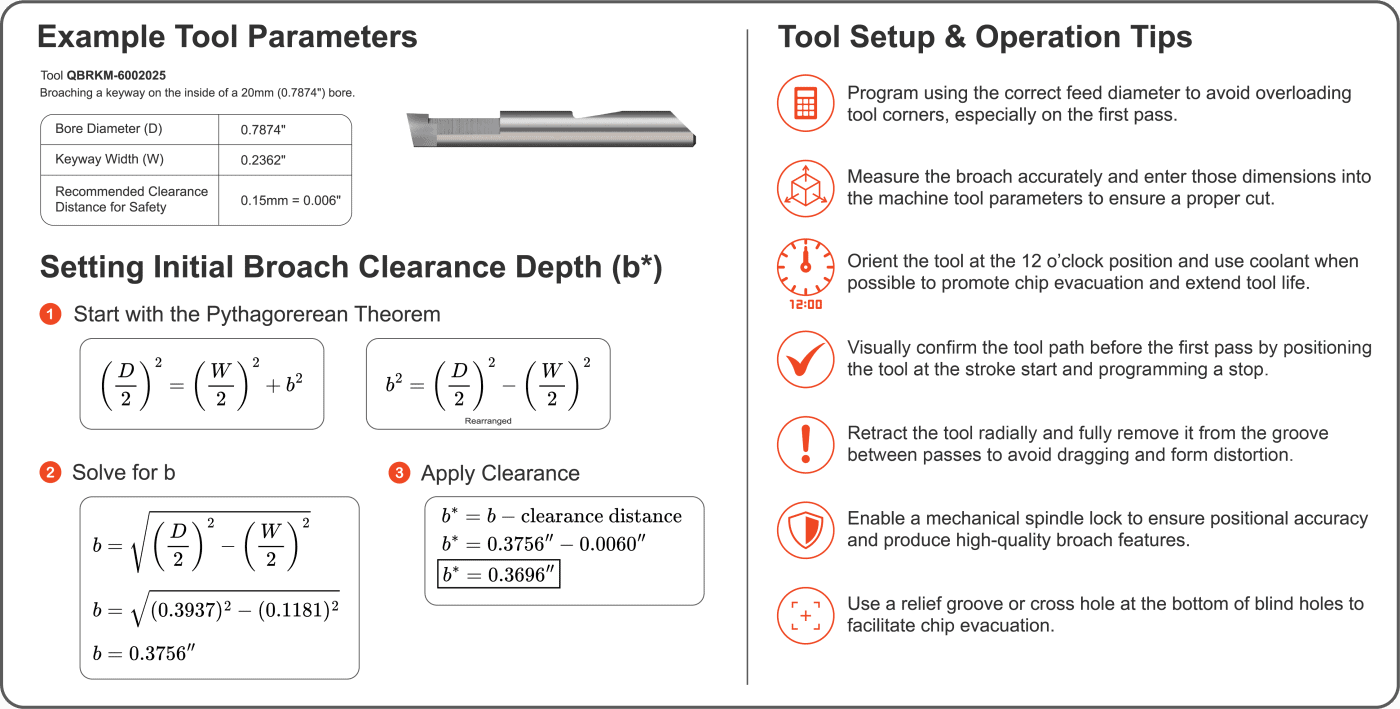
After the initial pass is completed, continue cutting normally until the desired keyway size is met. As with square and hex broaching, ensure the tool is radially clear of the groove after each pass before retracting. On the final return stroke, completely remove the broach from the hole.

In Summary

Micro 100s offering of broaching tools is fit for a large variety of broaching applications you may come across. Whether square, standard, or hexagonal, metric or imperial, Micro 100 has the tools to help you cut every step of the way.

To see the full range of tooling that Micro 100 has to offer, please visit our website micro100.com.

For any further questions regarding our broaching tools or Micro 100 as a whole, please don’t hesitate to call us at +1 844-393-8665 or email us at [email protected].

https://www.harveyperformance.com/wp-content/uploads/2025/11/Broaching-Featured-Image-Rev-01.jpg 525 1400 Steven Velazquez http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Steven Velazquez2025-11-20 11:30:002025-12-03 14:09:16Micro 100 Broaching Tools: Everything You Need to Know

Maximize Efficiency With Micro 100 Tool Holders

April 12, 2024/0 Comments/in Micro 100, Turning/by Harvey Performance Company

The Micro 100 Spring 2024 Product Catalog will feature hundreds of new products, including a significant increase to its offering of both standard-style and quick change-style tool holders. These unique additions include several Double-Ended styles: Standard Double-Ended Similar ID, Standard Double-Ended Dissimilar ID, Standard Double-Ended ER, Quick Change Double-Ended Similar ID, Quick Change Double-Ended Dissimilar ID, and Quick Change Double-Ended ER.

These new Double-Ended Holders were designed to be utilized with each other to reduce set up time, and eliminate the time a machinist often spends searching for the correct size tool holder.

As an example, when a Swiss Machine is loaded with multiple combinations of holders, such as a Similar ID, Dissimilar ID, Standard with ER, and Quick Change with ER, a machinist can have all of the ID connections they require residing right in the machine, thereby reducing time spent searching for a correct holder. Holders can be flipped end-for-end to utilize a different size ID at the spindle of your choosing, and – if programmed properly from part-to-part, minimal tool position changes would be required.

The following animations are designed to provide a look at the functionality of each holder style, and the unique benefits they provide for machinists.

Standard Double-Ended Similar ID Holders

In the above animation of Standard Double-Ended Similar ID Holders, the holder enters from the left side of the screen and shows how a standard style turning tool can be entered from each end, and secured with a set screw on each side. Please note that this holder requires tools with the same shank diameter size be utilized on each side.

On the right side, the screw is then removed and the tool is removed, slightly, from the holder, before the set screw is replaced. This showcases that the tool can be positioned in several different ways in this holder, and can accommodate a project with any reach length.

Shop Standard Double-Ended Similar ID Holders

Standard Double-Ended Dissimilar ID Holders

With the Standard Double-Ended Dissimilar ID Holders, the same benefits apply as with the Standard Double-Ended Similar ID Holders. The only difference between the two styles is that one end of the Dissimilar ID Style Holders accommodates a shank diameter size one size larger than the other. Overhang can be set to meet customers’ reach and harmonics requirements.

Shop Standard Double-Ended Dissimilar ID Holders

Standard Double-Ended ER Holders

[

With Standard Double-Ended ER Holders, we see the holder enter from left, and a standard tool is first inserted into the “B Side” of the holder. Then, we see a tool inserted into a Micro 100 ER Collet, before it’s connected to the “A Side” of the holder. This holder provides maximum versatility to machinists who need to utilize a rotating-type tool in static applications, such as for drilling, reaming, or spotting.

Shop Standard Double-Ended ER Holders

Quick Change Double-Ended Similar ID Holders

Designed to be used with Micro 100’s Quick Change Tooling, these Quick Change Double-Ended Similar ID Holders work by inserting a tooling with the same shank diameters into each side, until it reaches an internal locating and locking pin. A set screw then secures the tools in place on each side. Note that because of the locating and locking pin, reaches cannot be adjusted with Quick Change holders.

Shop Quick Change Double-Ended Similar ID Holders

Quick Change Double-Ended Dissimilar ID Holders

In this animation, a Micro 100 Quick Change tool with a ¼” shank diameter is inserted into the “A Side” of the holder. A Micro-Quik tool with a shank diameter one size larger, 5/16”, is then inserted into the “B Side.” Both sides are then locked into place with a set screw.

Shop Quick Change Double-Ended Dissimilar ID Holders

Quick Change Double-Ended ER Holders

In the above animation of Micro 100’s Quick Change Double-Ended ER Holders, a Micro-Quik tool is inserted into the “B Side,” and locked into place with a set screw, before a Micro-Quik drill is inserted into a Micro 100 ER Collet, before being screwed into the “A Side” of the holder.

Similar to the standard style of this holder, this allows one end of the holder to house a rotating tool in static applications.

Shop Quick Change Double-Ended ER Holders

Quick Change Double-Ended Holders in Machine

In this animation, three Quick Change Double-Ended holders slide into the Y-Axis tooling block, and screws tighten down to lock the holders in place. The Quick Change Double-Ended Dissimilar ID Holder is removed from the Y-Axis tooling block, and flipped around, showcasing the ability of most of Micro 100’s Double-Ended Holders to be flipped end-for-end without having to take apart the assembly, reducing the amount of set up time needed between tool changes. Next, the ER Collet, Nut, and Spotting Drill are removed from the Quick Change Double-Ended ER Holder and replaced with a Miniature Drill, highlighting the ability to change tools on the ER end without having to remove the holder from the machine.

Shop Quick Change Double-Ended ER Holders
https://www.harveyperformance.com/wp-content/uploads/2024/04/M100-Holders-Blog-Featured.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-04-12 11:02:582025-11-20 09:48:23Maximize Efficiency With Micro 100 Tool Holders

5 Boring Bar Mistakes That Cause Lathe Chatter

September 8, 2022/4 Comments/in CNC Machining, Large Featured, Micro 100, Turning/by Harvey Performance Company

Boring bar applications are very popular in the lathe and CNC machining industry, as they provide a shop with extreme diversity and accuracy. Running a boring bar properly, however, is essential to ensuring you’re maximizing shop efficiency and achieving outstanding part finish. There are many mistakes that can be made when running boring bars and many that cause excessive machining vibrations or lathe chatter that must be avoided. Learn the five mistakes that could be causing tool chatter in your boring applications and how you can stop this lathe chatter once and for all.

Mistakes Causing Lathe Chatter

Using a Dull Cutter

Boring with a worn-out tool significantly increases cutting forces generated by the cut, potentially leading to lathe chatter. The more a tool is run, the more chance it has for galling, or in other words, built-up edge (BUE), making it imperative to inspect your boring bar before each application. BUE occurs when material is welded onto the cutting tool due to high friction and heat generation during a CNC machining operation. This condition is not desirable because it leads to poor tool life and increased vibrations due to an uneven cutting edge. Stocking your tool crib with great quality boring bars can help reduce BUE by providing a sharp, long lasting cutting edge, catered for your exact application. Learn other ways to reduce BUE in your turning applications, today.

Shows zoomed in effects of built-up edge and wear failure on carbide boring bar which leads to lathe chatter
Image Source: Carbide inserts Wear Failure modes. | machining4.eu, 2022

Utilizing Incorrect Speeds & Feeds

Like many applications, using improper turning speeds & feeds can lead to poor performance. In boring applications, using too high of a chip load can cause deflection, greatly increasing the chances of tool failure. Using too low of a chip load doesn’t allow the tool to cut enough, which causes the tool to bounce off the material, leading to increased tool wear and poor part finish. Discovering the right balance for using chip load is crucial in order to produce a more efficient cut.

lathe turning speeds and feeds

When running a boring bar, it is imperative to use the speeds & feeds recommended for the tool being used. Micro 100 provides downloadable and printer-friendly Speeds & Feeds for all Standard and Quick Change Micro-Quik turning tools.

Lacking Workpiece Support

A main cause of chatter in lathe applications is lack of support on the workpiece. If a workpiece is not properly supported when entering a boring application, the tool will begin to chatter. Not only is it essential to confirm the proper workholding device is being used, but it’s also important to ensure that your setup is as rigid as possible. Learn more about workholding styles and considerations to make sure you’re supporting your workpiece properly in your next boring application.

Uneven Tool Holding

Similarly, tool holding also plays a vital role in the performance of a boring bar application. It is important to select a tool holder that accommodates the tooling being used and is as rigid as possible. Using an improper method of tool holding can lead to tool runout, which occurs when the tool or holder deviates too far off its axis.

Understanding the overall rigidity of your system is a critical step in understanding how to best reduce lathe chatter.

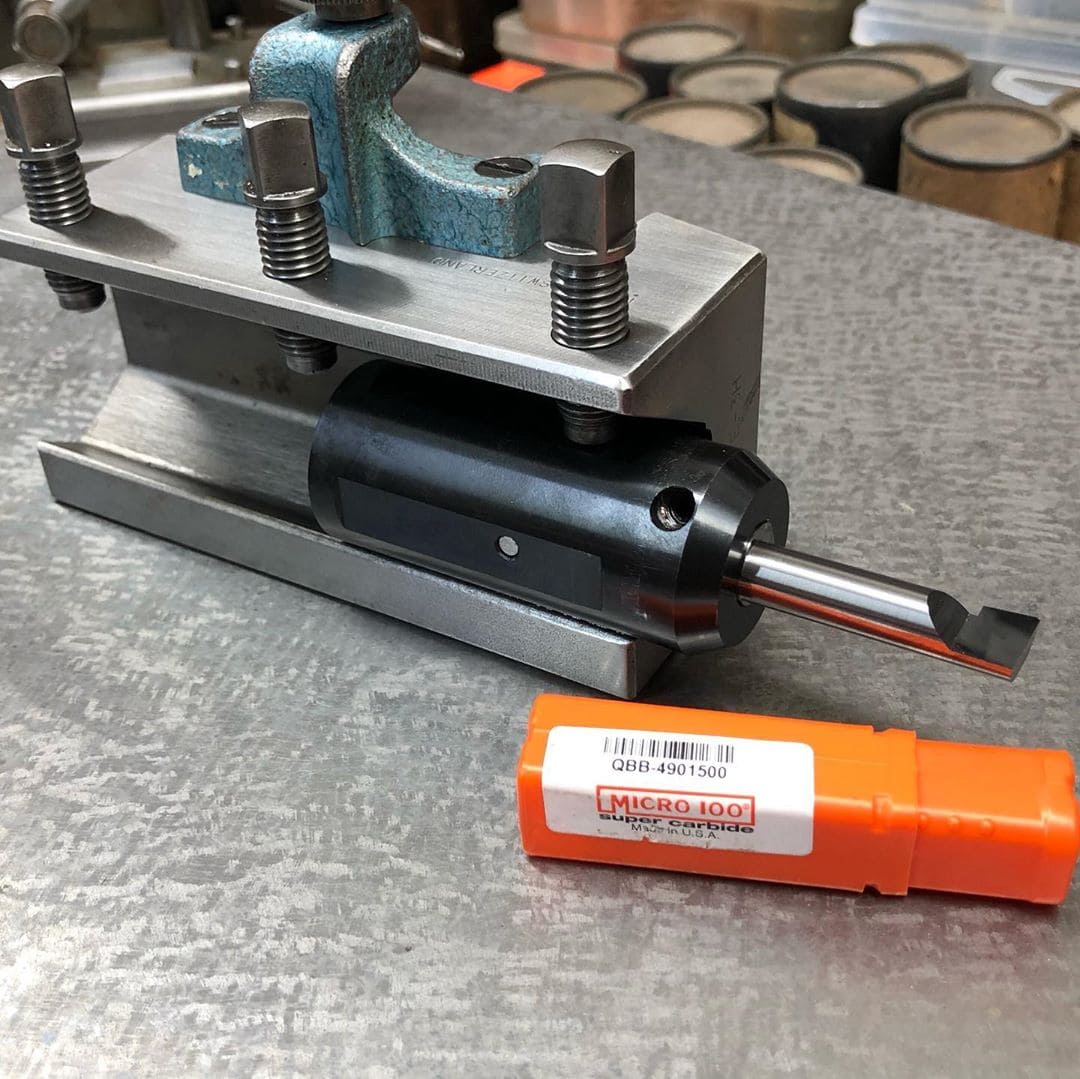
Micro-Quik tool holder with a tool inserted and pointing towards workpiece
Image Source: @abom79

Many machinists opt for tools that promote machining efficiency by boosting the speed at which tool changes occur. For example cutting tool manufacturer Micro 100 offers Micro-Quik Holders, which offer unmatched rigidity, axial and radial repeatability, tip-to-tip consistency, and part-to-part accuracy in tool changes totaling fewer than 30 seconds.

Drilling an Improper Starter Hole

Before starting a boring application, drilling the proper hole is vital to ensuring that the boring bar has sufficient contact with the workpiece to properly stabilize the cut.

If a hole is too large, the boring bar could deflect off of the workpiece. If the hole is too small, there will not be enough clearance for the tool, increasing chances of tool wear and possibly tool failure.

When selecting a drill to prepare the workpiece for your boring applications, there are two dimensions that should be considered: the Head Width and the Minimum Bore Diameter.

Boring bar with line drawing showing where different dimensions are located on the tool

The Head Width, or “H” value on the above line drawing, is the actual width of the boring tool. The Minimum Bore Diameter is a calculated dimension slightly larger in size compared to the head with that is associated with the smallest drill size that should be used to start a boring application. It is recommended to opt for a drill that is the same or slightly larger than the Minimum Bore Diameter of the boring bar being used, to ensure there is proper clearance for the cutting edge.

Utilizing an Inefficient Coolant Strategy

If coolant isn’t aimed properly on the workpiece or if improper coolant is being used, tool life and quality part finish can be significantly reduced. Additionally, if coolant lines are aimed directly at the bore, the pressure of the coolant holds the chips in the bore, causing them to evacuate improperly. This then causes chip recutting, leading to lathe chatter and finish problems.

Opting for a Plumbed and Ported Tool Holder can mitigate this problem, ensuring chips are being properly evacuated out of the cut.

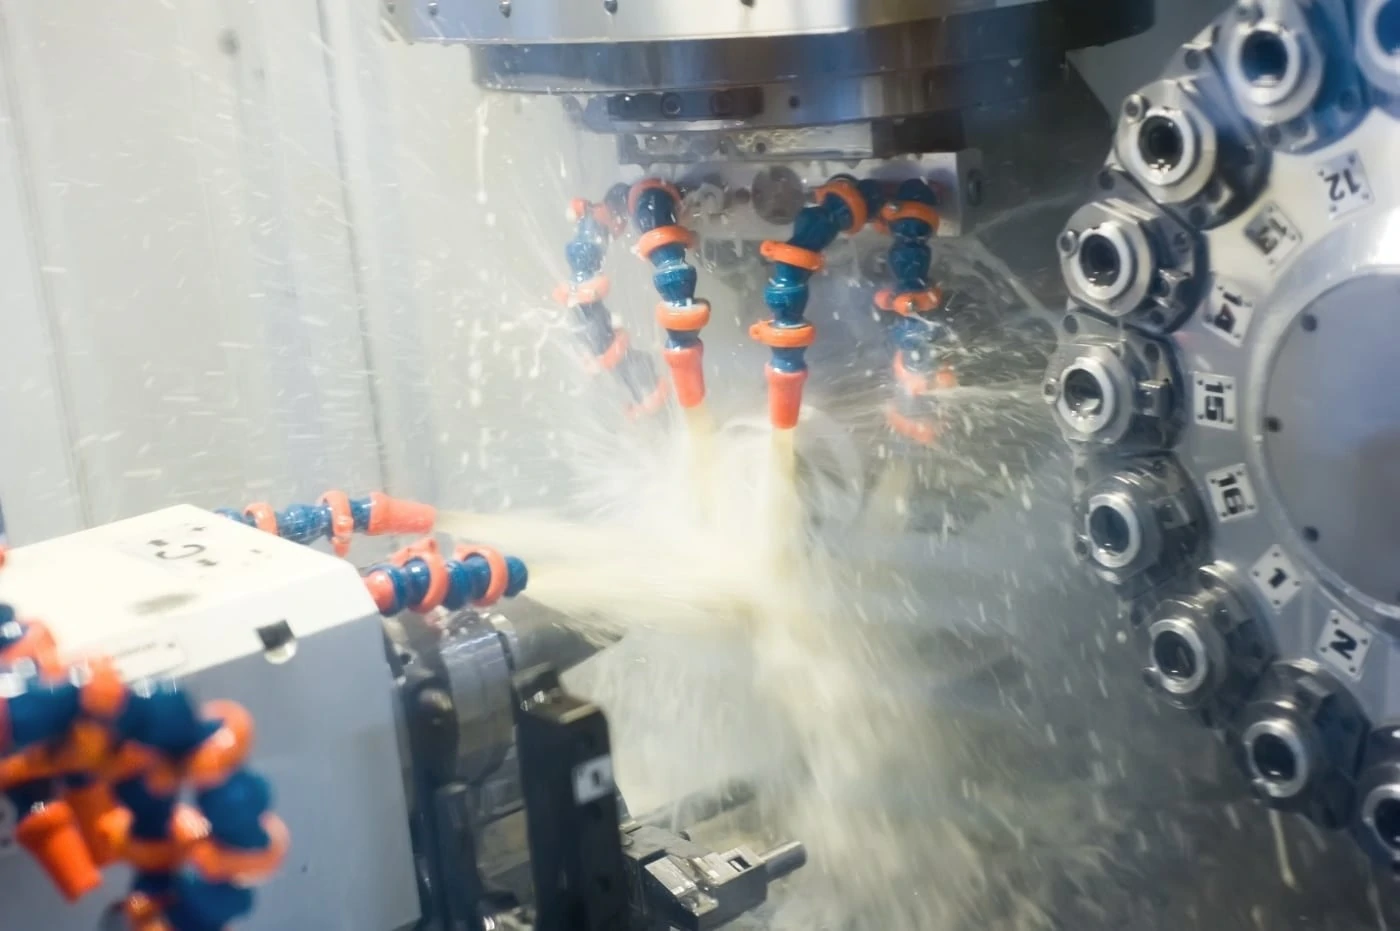
coolant being sprayed onto a part during a cnc machining operation

Machinists generally utilize Flood or High Pressure coolant methods for chip removal. Flood coolant uses low pressure to create lubricity and aid in chip evacuation. On the other hand, high pressure coolant delivers instant cooling of a part and quickly shoots chips away to prevent recutting.

https://www.harveyperformance.com/wp-content/uploads/2022/09/Featured-Image-Boring-Bar-Chatter.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2022-09-08 14:20:092025-11-12 15:58:455 Boring Bar Mistakes That Cause Lathe Chatter

Understanding Micro 100 Micro-Quik Tool Holders

July 19, 2021/0 Comments/in Large Featured, Machining 101, Machining Techniques, Micro 100, Tool Selection, Turning/by Harvey Performance Company

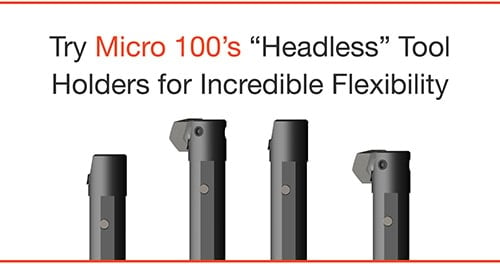
Did you know that, along with supplying the machining industry with premier turning tools, Micro 100 also fully stocks tool holders for its proprietary Micro-Quik Quick Change Tool Holder System? In fact, Micro 100’s Spring 2021 Product Catalog introduced new “headless” style tool holders, which are revolutionizing the machine setup process for turning operations.

This “In the Loupe” guide is designed to provide you with insight for navigating Micro 100’s offering, and to help you select the optimal holder style for your operation.

Micro 100 ad showing four different tool holders

Understanding Micro 100’s Micro-Quik

Micro 100’s Micro-Quik is unlike any other tool change system you may have seen from other tool manufacturers because of its incredible axial and radial repeatability and its ease of use. This foolproof system delivers impressive repeatability, tip-to-tip consistency, and part-to-part accuracy, all the while resulting in tool changes that are 90 % faster than conventional methods.

In all, a tool change that would regularly take more than 5 minutes is accomplished in fewer than 30 seconds.

Micro 100 Quick Change Tool Holder Selection

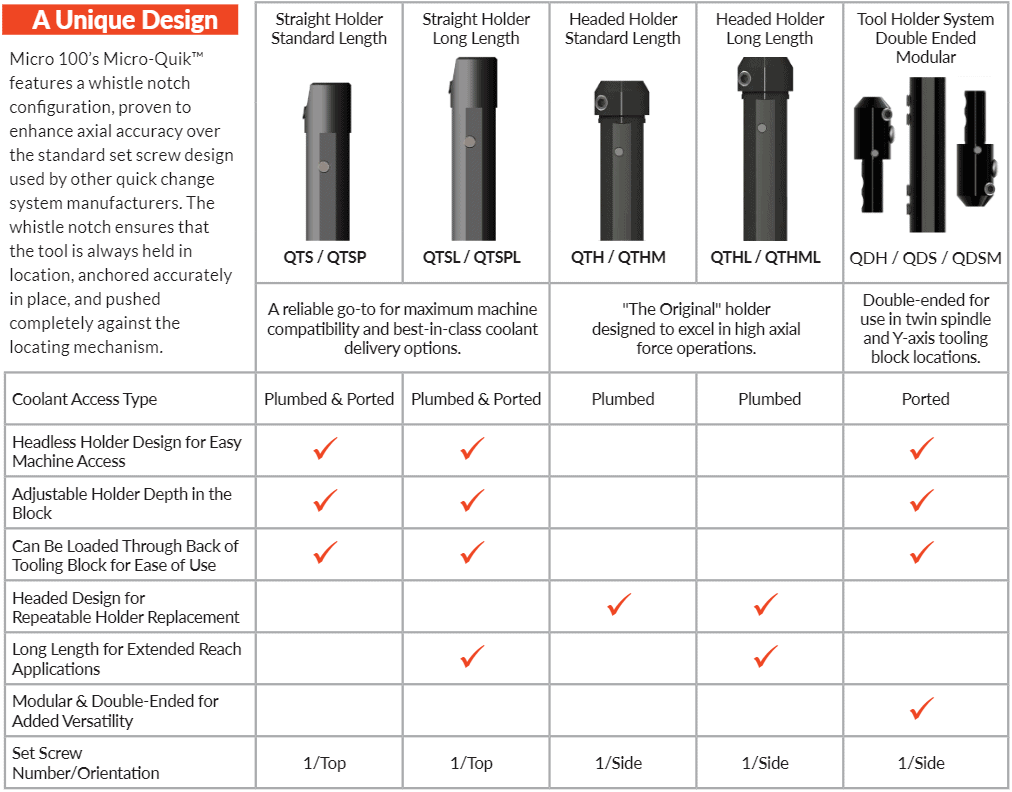
Straight Style, Headless Tool Holders

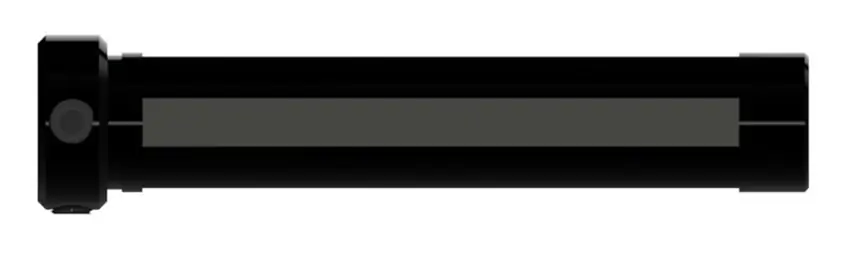
When using a straight style tool holder, you will enjoy significantly enhanced versatility during the machine set up process. These holders are engineered specifically for use in any Swiss, standard lathe, or multi-function lathe, and allow for adjustable holder depth in a tooling block. Radial coolant access ports provide easier access to coolant and the ability to utilize coolant through functionality in tooling blocks that share a static and live tool function, and cannot be plumbed through the back of the holder. Further, their headless design allows for installation through the backside of the tooling block in machines where the work envelope is limited, allowing for a simplified installation process.

Created by Harvey Performance Company Application Engineers, the following videos outline the simple process for inserting each style of Micro 100 Straight Tool Holder into a tooling block.

Micro 100 Straight Holder, Plumbed Style (QTS / QTSL)

In the video, you’ll notice that the first step is to place your Micro-Quik tool in this quick change holder, and align it with the locating pin. Then, tighten the locating and locking screw into the whistle notch. This forces the tool against the locking pin, and allows for repeatable accuracy, every time. From there, the quick change tool holder can be installed as a unit into a tooling block. When desired tool position is achieved, set screws can be tightened to lock the holder in place.

Micro 100 Straight Holder, Plumbed & Ported Style (QTSP / QTSPL)

This unique Micro 100 quick change tool holder style is plumbed and ported, allowing for enhanced versatility and coolant delivery efficiency. The setup process using this style of holder is also simple. First, place your Micro 100 quick change tool into the holder, and align it with the locating pin. From there, tighten the locating and locking screw into the whistle notch, forcing the tool against the locating pin and allowing for repeatable accuracy, every time. When plumbed coolant is being used, remove the plumbed plug in the back of the holder, and connect the appropriate coolant adapter and line. Then, the holder can be installed as a unit into the tooling block and locked into place with set screws.

When using ported coolant, make sure that the coolant plug in the back of the holder is tightly installed. Then, be sure to only use one of the radial ports. Simply plug the two that aren’t in use. Install the provided porting adapter to allow for coolant access. Porting options allow for coolant capabilities in machine areas where coolant is not easily accessible.

Headed Tool Holders

headed quick change tool holder

Micro 100’s original quick change tool holder for its Micro-Quik system, this style of tool holder for lathe applications features a unique “3 point” locking and locating system to ensure repeatability. When conducting a tool change with this tool holder style, you must follow a simple, 3-step process:

  1. Loosen the tool holder’s set screw
  2. Remove the used tool from the holder
  3. Insert the new tool and retighten the set screw

These headed holders are plumbed through the back of the holder for NPT coolant connection and are available in standard length and long length styles.

Try Micro 100’s “Headless” Tool Holders for Incredible Flexibility

Double-Ended Modular Tool Holder System

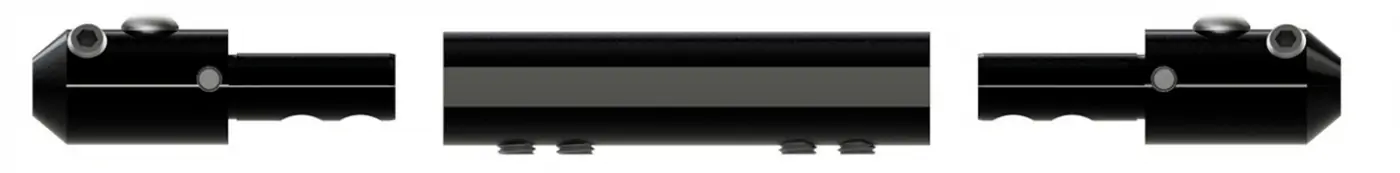
double ended quick change tool holder

For twin spindle and Y-axis tooling block locations, Micro 100 fully stocks a double-ended modular system. Similar to its single-ended counterparts, this modular is headless, meaning it enhances machine access during the tool block installation process, and the holder depth can be adjusted while in the block. Because this system is double-ended, however, there is obviously no plumbed coolant option through the end of the tool. Instead, coolant is delivered via an external coolant port, the adapter for which is included in the purchase of the modular system. Right hand and left hand tool holders are designed so the set screws are facing the operator for easy access. Both right and left hand styles are designed for right hand turning.

Enjoy Quick Change Tool Holding Confidence & Ease of Use

When opting for a quick change system, machinists long for simplicity, versatility, and consistency. Though many manufacturers have a system of their own, Micro 100’s Micro-Quik sets itself apart with axial and radial repeatability, and tip-to-tip consistency. Further, Micro 100 fully stocks several quick change tool holder options, allowing a machinist to select the style that best fits their application.

Micro100 also manufactures and stocks a wide variety of boring tools for the Micro-Quik. Click here to learn more.

For more information on selecting the appropriate quick change tool holder for your job, view our selection chart or call an experienced Micro 100 technical engineer at 800-421-8065.

quick change tool holder selection chart for Micro100
https://www.harveyperformance.com/wp-content/uploads/2021/07/Featured-Image-Quick-Change-Holders-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2021-07-19 11:28:002025-11-20 09:49:56Understanding Micro 100 Micro-Quik Tool Holders

The 3 Critical Factors of Turning Speeds and Feeds

May 13, 2021/4 Comments/in Machining 101, Machining Techniques, Micro 100, Small Featured, Turning/by Harvey Performance Company

Many factors come into play when determining a proper turning speeds and feeds and depth of cut strategy for turning operations. While three of these factors – the ones we deemed to be among the most critical – are listed below, please note that there are many other considerations that are not listed, but that are also important. For instance, safety should always be the main focus of any machining operation, as improper cutting tool parameters can test a machine’s limits, resulting in an accident that can potentially cause significant bodily harm.

Machine condition, type, capabilities, and set-up are all significantly important to an overall successful turning operation, as is turning tool and holder selection.

Turning Speeds and Feeds Factor 1: Machine Condition

The condition of your machine should always be considered prior to beginning a machining operation on a lathe. Older machines that have been used for production operations where hard or abrasive materials are machined tend to have a large amount of backlash, or wear, on the machine’s mechanical parts. This can cause it to produce less than optimal result and may require that a tooling manufacturer’s recommended speeds and feeds parameters need to be dialed back a bit, as to not run the machine more aggressively than it can handle.

turning machine engaging with workpiece

Factor 2: Machine Type and Capabilities

Before dialing in turning speeds and feeds, one must understand their machine type and its capabilities. Machines are programmed differently, depending on the type of turning center being used: CNC Lathe or Manual Lathe.

CNC Lathe Turning Centers

With this type of machine, the part and tool have the ability to be set in motion.

CNC lathe turning centers can be programmed as a G96 (constant surface footage) or G97 (constant RPM). With this type of machine, the maximum allowable RPM can be programmed using a G50 with an S command. For example, inputting a G50 S3000 into your CNC program would limit the maximum RPM to 3,000. Further, with CNC Lathe Turning Centers, the feed rate is programmable and can be changed at different positions or locations within a part program.

Manual Lathe Turning Centers

With this type of machine, only the part is in motion, while the tool remains immobile.

For manual lathe turning centers, parameters are programmed a bit differently. Here, the spindle speed is set at a constant RPM, and normally remains unchanged throughout the machining operation. Obviously, this puts more onus on a machinist to get speed correct, as an operation can quickly be derailed if RPM parameters are not optimal for a job. Like with CNC lathe turning centers, though, understanding your machine’s horsepower and maximum feed rate is critical.

Factor 3: Machine Set-Up

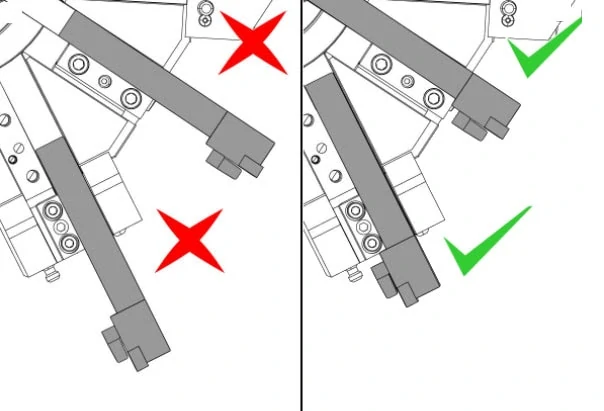
image demonstrating proper tool setup beside depiction of excessive tool stickout
Excessive Tool Stickout. Digital Image, Hass Automation. https://www.haascnc.com/service/troubleshooting-and-how-to/troubleshooting/lathe-chatter—troubleshooting.html

Machining Conditions

When factoring in your machine set-up, machining conditions must be considered. Below are some ideal conditions to strive for, as well as some suboptimal machining conditions to avoid for dialing in proper turning speeds and feeds.

Ideal Machining Conditions for Turning Applications

  • The workpiece clamping or fixture is in optimal condition, and the workpiece overhang is minimized to improve rigidity.
  • Coolant delivery systems are in place to aid in the evacuation of chips from a part and help control heat generation.

Suboptimal Machining Conditions for Turning Applications

  • Utilizing turning tools that are extended for reach purposes, when not necessary, causing an increased amount of tool deflection and sacrificing the rigidity of the machining operations.
  • The workpiece clamping or fixturing is aged, ineffective, and in poor condition.
  • Coolant delivery systems are missing, or are ineffective
  • Machine does not feature any guarding or enclosures, resulting in safety concerns.

Cutting Tool & Tool Holder Selection

As is always the case, cutting tool and tool holder selection are pivotal. Not all turning tool manufacturers are the same, either. The best machinists develop longstanding relationships with tooling manufacturers, and are able to depend on their input and recommendations. Micro 100, for example, has manufactured the industry’s highest quality turning tools for more than 50 years. Further, its tool holder offering includes multiple unique styles, allowing machinists to determine the product that’s best for them.

lathe tool holder next to micro 100 tool product packaging
Pro Tip: Be sure to take into consideration the machine’s horsepower and maximum feed rate when determining running parameters.

Bonus: Common Turning Speeds and Feeds Application Terminology

Vc= Cutting Speed

n= Spindle Speed

Ap=Depth of Cut

Q= Metal Removal Rate

G94 Feedrate IPM (Inches Per Minute)

G95 Feedrate IPR (Inches Per Revolution)

G96 CSS (Constant Surface Speed)

G97 Constant RPM (Revolutions Per Minute)

https://www.harveyperformance.com/wp-content/uploads/2021/05/turning-speeds.jpg 370 987 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2021-05-13 15:54:582023-09-27 10:45:04The 3 Critical Factors of Turning Speeds and Feeds

Save Time With Quick Change Tooling

April 10, 2020/2 Comments/in CNC Machining, Drilling & Holemaking, Micro 100, Specialty Tools, Tool Information Guides, Tool Selection, Turning/by Harvey Performance Company

Making a manual tool change on any CNC machine is never a timely or rewarding process. Typically, a tool change in a standard holder can take up to 5 minutes. Add that up a few times, and suddenly you have added significant minutes to your production time.

As CNC machine tool and cutting tool technology has advanced, there are more multi-functional tools available to help you avoid tool changes. However, sometimes it just isn’t feasible, and multiple tool changes are needed. Luckily, Micro 100 has developed a revolutionary new method to speed up tool changes significantly.

What is the Micro-Quik Tooling System?

Developed in Micro 100’s world-class grinding facility in Meridian, Idaho, the Micro 100 Micro-Quik tooling system is held to the same standards and tight tolerances as all of the Micro 100 carbide tooling.

The quick change tooling system allows for highly repeatable tool changes that save countless hours without sacrificing performance. This system combines a unique tool holder with a unique tool design to deliver highly repeatable and accurate results.

Each quick change tool holder features a locating/locking set screw to secure the tool and a locating pin which helps align the tool for repeatability. Removing a tool is as simple as loosening the set screw and inserting its replacement.

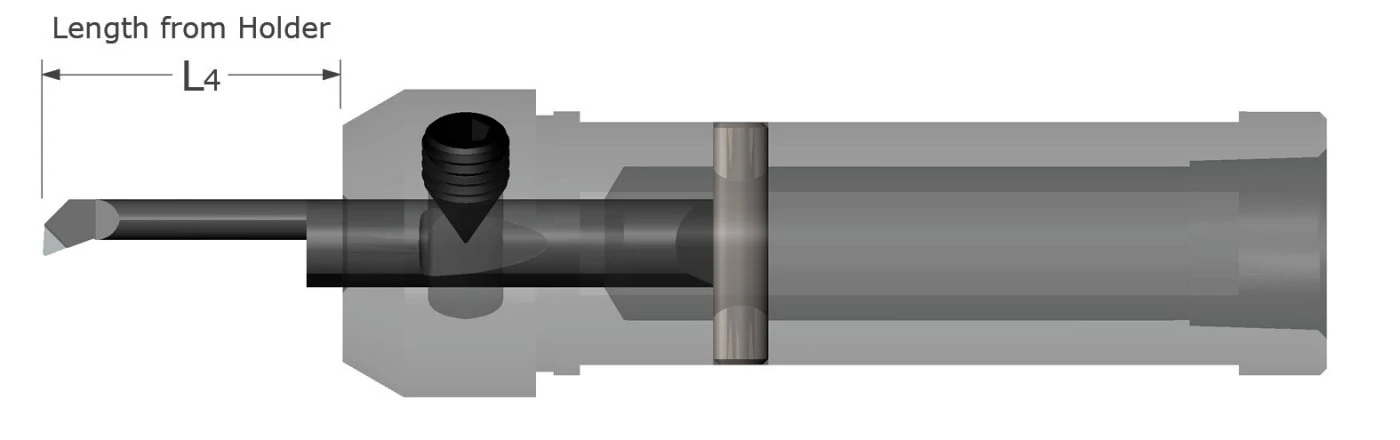
depiction of removing tool from quick change system

During tool changes, the precision ground bevel on the rear of the tool aligns with a locating pin inside the tool holder. The distance from this locational point to the tip of the tool is highly controlled under tight tolerances, meaning that the Micro-Quik tooling system ensures a very high degree of tool length and centerline repeatability. The “L4” dimension on all of our quick change tools, as seen in the image above, remains consistent across the entire product line. Check out the video below for a demonstration of the Micro 100 Micro-Quik system in action!

Quick Change Tooling Benefits

quick change system with micro 100 boring bar close up image

The most obvious benefit to using Micro 100’s Micro-Quik Quick Change Tooling System is the time savings that come with easier tool changes. By using the quick change holders in combination with quick change tooling, it is easy to reduce tool changes from 5 minutes to under 30 seconds, resulting in a 90% decrease in time spent swapping out tools. This is a significant benefit to the system, but there are benefits once the tool is in the machine as well.

As mentioned above, the distance from the locational point on each tool shank to the tip of the tool is highly controlled, meaning that regardless of which type of tool you insert into the holder, your stick out will remain the same. This allows you to have confidence in the tooling and does not require additional touch offs, which is another major time saver.

assortment of boring bars with quick change system

By removing additional touch-offs and tool changes from your workflow, you also reduce the chances for human or machine error. Improper touch-offs or tool change errors can cause costly machine crashes and result in serious repairs and downtime. With the Micro 100 Micro-Quik Quick Change Tooling System, initial setups become much easier, allowing you to hit the cycle start button with total confidence for each run.

By making a few simple changes to your tool holding configurations and adopting the Micro-Quik system, your shop can save thousands in time saved, with less machine downtime and increased part production. To learn more about the Micro 100 Micro-Quik cutting tools and tool holders, please visit Micro 100.

https://www.harveyperformance.com/wp-content/uploads/2020/04/Feature-Image-Quick-Change-Tooling-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2020-04-10 08:00:002023-10-05 08:58:22Save Time With Quick Change Tooling

How Boring Bar Geometries Impact Cutting Operations

October 23, 2019/8 Comments/in CNC Machining, Holemaking, Micro 100, Tool Information Guides, Tool Selection, Turning/by Robert Keever

Boring is a turning operation that allows a machinist to make a pre-existing hole bigger through multiple iterations of internal boring. It has a number of advantages over traditional hole finishing methods:

  • The ability to cost-effectively produce a hole outside standard drill sizes
  • The creation of more precise holes, and therefore tighter tolerances
  • A greater finish quality
  • The opportunity to create multiple dimensions within the bore itself
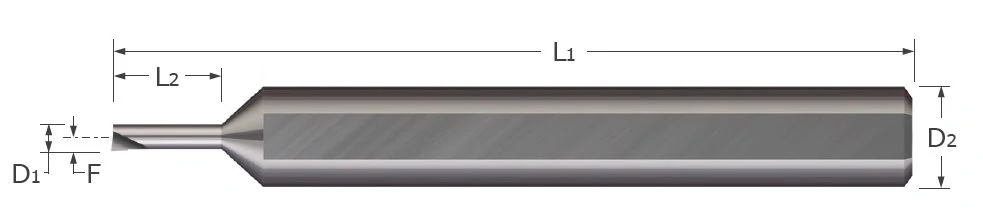
boring bar dimension explanation

Solid carbide boring bars, such as those offered by Micro 100,  have a few standard dimensions that give the tool basic functionality in removing material from an internal bore. These include:

Minimum Bore Diameter (D1): The minimum diameter of a hole for the cutting end of the tool to completely fit inside without making contact at opposing sides

Maximum Bore Depth (L2): Maximum depth that the tool can reach inside a hole without contact from the shank portion

Shank Diameter (D2): Diameter of the portion of the tool in contact with the tool holder

Overall Length (L1): Total length of the tool

Centerline Offset (F): The distance between a tool’s tip and the shank’s centerline axis

Micro100 Continues to Set the Standard for Boring Bars, Shop Today.

Tool Selection

In order to minimize tool deflection and therefore risk of tool failure, it is important to choose a tool with a max bore depth that is only slightly larger than the length it is intended to cut. It is also beneficial to maximize the boring bar and shank diameter as this will increase the rigidity of the tool. This must be balanced with leaving enough room for chips to evacuate. This balance ultimately comes down to the material being bored. A harder material with a lower feed rate and depths of cut may not need as much space for chips to evacuate, but may require a larger and more rigid tool. Conversely, a softer material with more aggressive running parameters will need more room for chip evacuation, but may not require as rigid of a tool.

Geometries

In addition, they have a number of different geometric features in order to adequately handle the three types of forces acting upon the tool during this machining process. During a standard boring operation, the greatest of these forces is tangential, followed by feed (sometimes called axial), and finally radial. Tangential force acts perpendicular to the rake surface and pushes the tool away from the centerline. Feed force does not cause deflection, but pushes back on the tool and acts parallel to the centerline. Radial force pushes the tool towards the center of the bore.

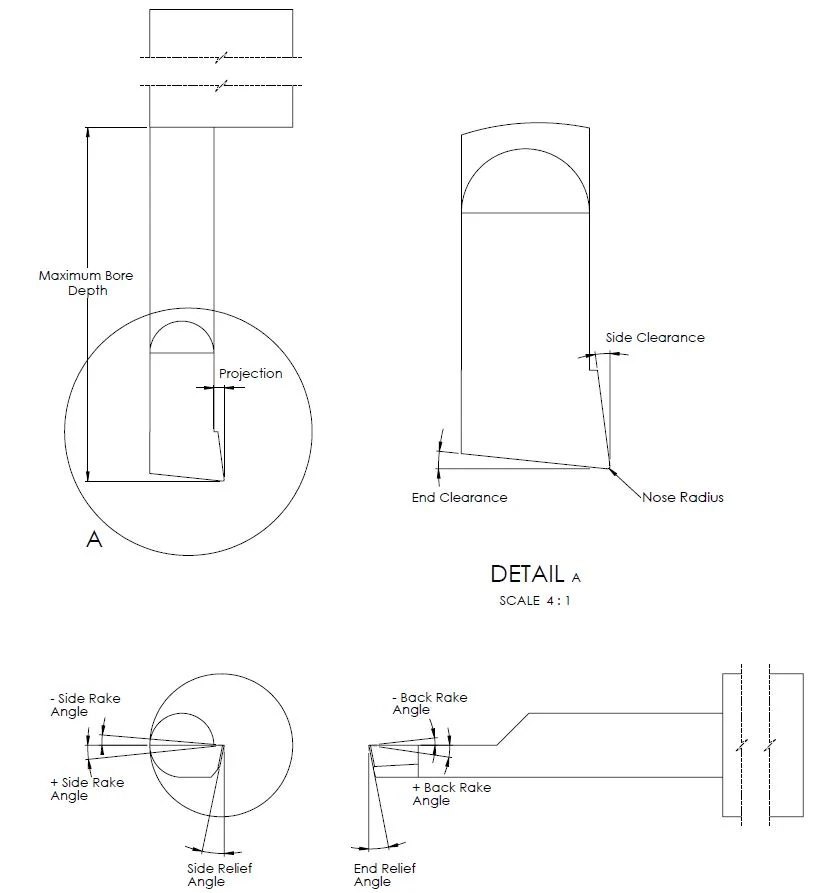
Defining the Geometric Features of a Boring Bar:

Nose Radius: the roundness of a tool’s cutting point

Side Clearance (Radial Clearance): The angle measuring the tilt of the nose relative to the axis parallel to the centerline of the tool

End Clearance (Axial Clearance): The angle measuring the tilt of the end face relative to the axis running perpendicular to the centerline of the tool

Side Rake Angle: The angle measuring the sideways tilt of the side face of the tool

Back Rake Angle: The angle measuring the degree to which the back face is tilted in relation to the centerline of the workpiece

Side Relief Angle: The angle measuring how far the bottom face is tilted away from the workpiece

End Relief Angle: The angle measuring the tilt of the end face relative to the line running perpendicular to the center axis of the tool

boring bar geometric features

Effects of Geometric Features on Cutting Operations:

Nose Radius: A large nose radius makes more contact with the workpiece, extending the life of the tool and the cutting edge as well as leaving a better finish. However, too large of a radius will lead to chatter as the tool is more exposed to tangential and radial cutting forces.

Another way this feature affects the cutting action is in determining how much of the cutting edge is struck by tangential force. The magnitude of this effect is largely dependent on the feed and depth of cut. Different combinations of depth of cuts and nose angles will result in either shorter or longer lengths of the cutting edge being exposed to the tangential force. The overall effect being the degree of edge wear. If only a small portion of the cutting edge is exposed to a large force it would be worn down faster than if a longer portion of the edge is succumb to the same force. This phenomenon also occurs with the increase and decrease of the end cutting edge angle.

End Cutting Edge Angle: The main purpose of the end cutting angle is for clearance when cutting in the positive Z direction (moving into the hole). This clearance allows the nose radius to be the main point of contact between the tool and the workpiece. Increasing the end cutting edge angle in the positive direction decreases the strength of the tip, but also decreases feed force. This is another situation where balance of tip strength and cutting force reduction must be found. It is also important to note that the angle may need to be changed depending on the type of boring one is performing.

Side Rake Angle: The nose angle is one geometric dimension that determines how much of the cutting edge is hit by tangential force but the side rake angle determines how much that force is redistributed into radial force. A positive rake angle means a lower tangential cutting force as allows for a greater amount of shearing action. However, this angle cannot be too great as it compromises cutting edge integrity by leaving less material for the nose angle and side relief angle.

Back Rake Angle: Sometimes called the top rake angle, the back rake angle for solid carbide boring bars is ground to help control the flow of chips cut on the end portion of the tool. This feature cannot have too sharp of a positive angle as it decreases the tools strength.

Side and End Relief Angles: Like the end cutting edge angle, the main purpose of the side and end relief angles are to provide clearance so that the tools non-cutting portion doesn’t rub against the workpiece. If the angles are too small then there is a risk of abrasion between the tool and the workpiece. This friction leads to increased tool wear, vibration and poor surface finish. The angle measurements will generally be between 0° and 20°.

Boring Bar Geometries Summarized

Boring bars have a few overall dimensions that allow for the boring of a hole without running the tool holder into the workpiece, or breaking the tool instantly upon contact. Solid carbide boring bars have a variety of angles that are combined differently to distribute the 3 types of cutting forces in order to take full advantage of the tool. Maximizing tool performance requires the combination of choosing the right tool along with the appropriate feed rate, depth of cut and RPM. These factors are dependent on the size of the hole, amount of material that needs to be removed, and mechanical properties of the workpiece.

https://www.harveyperformance.com/wp-content/uploads/2019/10/Feature-Image-Boring-Bar-Geometries-IMG.jpg 525 1400 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2019-10-23 14:03:002022-12-12 08:59:23How Boring Bar Geometries Impact Cutting Operations
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top