Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

The Key Differences Between Helical’s Tool Coatings

November 13, 2025/0 Comments/in CNC Machining, Helical Solutions, Large Featured, Tool Coatings, Tool Selection/by Michaela Martell

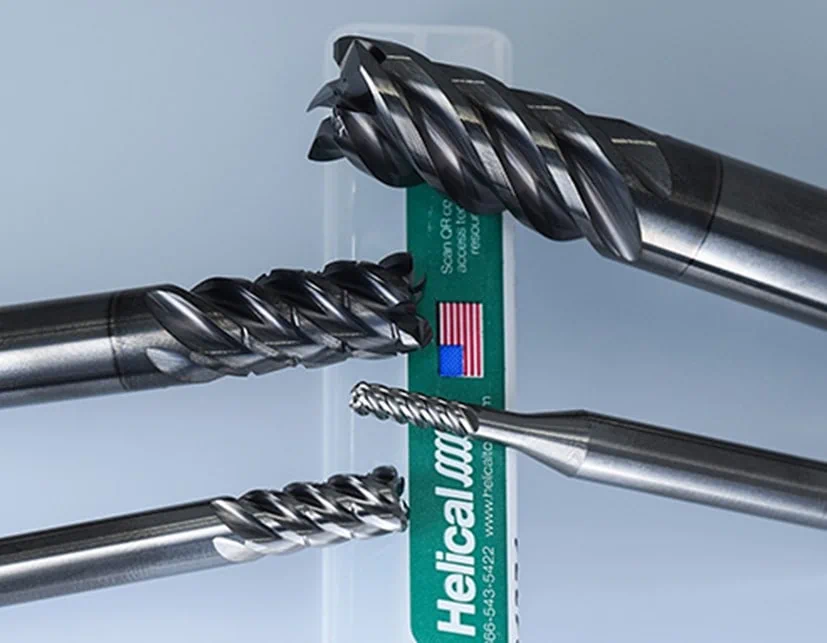
Tool coatings are added to protect against the forces that wear down cutting tools. They play a critical role in CNC machining by reducing heat generation and friction while enhancing overall tool performance. Below is an overview of Helical Solutions’ coating options, including which tool families they pair with, the applications they’re best suited for, and helpful application tips.

Helical Solutions demonstrates its commitment to performance by delivering high-performance carbide end mills and tools designed to reduce cycle times, improve part finishes, and extend tool life. This is achieved through a focus on exceptional quality and innovation, utilizing precision CNC manufacturing, advanced design techniques, and a world-class team of engineers and technical experts. Helical Solutions aims to be a true superior product performance, and responsive technical support.

The following information will help machinists understand the differences between Helical’s coating options and how to select the right one based on material and application.

What Are Tool Coatings and Why Are They Important?
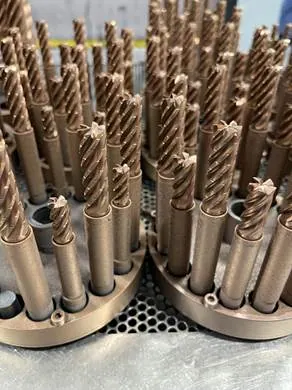
Tool coatings are applied to a tool’s cutting surface through a process called PVD (Physical Vapor Deposition). PVD and CVD are two different types of coating applications, with PVD being the common process for Helical’s tools.

This near-vacuum process distributes micron-thick layers evenly onto a properly prepared tool, helping it maintain a sharper cutting edge. When selecting tool coatings, machinists should consider material type, coolant use, and how the

material and operation may affect the cutting edges. Understanding these factors is essential to extending tool life.

Some key benefits of coatings include improved thermal resistance, better chip evacuation, increased lubricity (which allows chips to slide more easily down the flute), and higher microhardness. These properties reduce tool wear, enhance performance in material-specific applications, and extend tool life during production runs.

Helical’s coating lineup is designed with specific materials and applications in mind. Selecting the right coating for your job can have a major impact on tool life, heat control, and overall performance.

How to Choose the Right Coating:

Choosing the proper coating for your application is crucial, as each Helical coating is optimized for specific materials. Consider the following when selecting:
– What material are you machining?
– Will the material work harden quickly under heat?
– What is its coefficient of friction?
– Will you be using coolant?
– What is your expected tool life for this production run?

Application Tips:

Coatings in Coolant Applications:

Most coatings perform better with coolant, but there are exceptions.

Tplus performs well in many materials, but when cutting hardened steels, the combination of high heat and coolant can cause thermal shock, resulting in tool fractures.

In composites and non-metallic materials—often machined with Dplus—using coolant can create a slurry and increase wear between the tool and workpiece. For these materials, dry machining is generally preferred.

Zplus vs. Nplus vs. Dplus

For aluminum and non-ferrous applications, coatings are found on Helical’s HVAL and HMAF tool families.

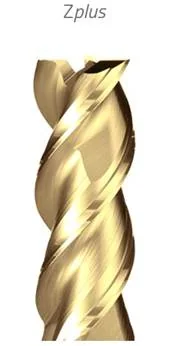
– Zplus is Helical’s longstanding coating for aluminum and non-ferrous materials.
– Nplus improves tool life compared to Zplus and features a harder, smoother coating—ideal for larger production jobs in tougher materials.
– Dplus is a tetrahedral amorphous carbon coating known for extreme wear resistance and performance in abrasive materials. For shops seeking a DLC-style coating, Dplus is Helical’s recommendation.

Uncoated (or bright) tools can be used in aluminum applications, but adding a coating generally improves productivity and helps prevent material from welding onto the tool.

Aplus vs. Tplus
– Aplus is a tough, multi-layer coating that enhances adhesion, edge retention, and heat resistance. It performs best in steels under 45 Rc. Helical’s HSV, HEV, and HSF tool families are excellent choices with this coating. Aplus is not recommended for aluminum, as it can cause galling (when material adheres to the tool), negatively impacting cutting performance and chip evacuation.

– Tplus is a premium coating offering top-tier performance in ferrous materials. It has a slight edge over Aplus, particularly in stainless steels and nickel alloys, and is optimal for cutting materials between 45 Rc and 65 Rc. It supports higher temperatures, maintains edge retention, and reduces wear. However, due to its hardness, it may generate more heat—and, as mentioned earlier, coolant can sometimes lead to thermal shock in these conditions.
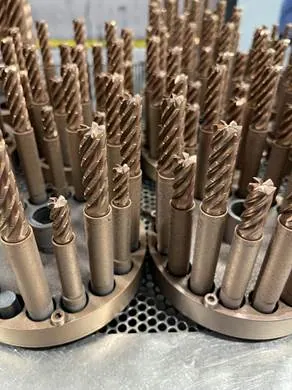
tplus coated helical end mills in holders following the coating process

Tplus has also shown success in titanium applications. Both Aplus and Tplus are suitable choices for these materials. You can find Tplus coatings on Helical’s HSV, HEV, and HVSS-6 tool families. The HVSS-6 line, in particular, has proven optimal for cutting 316 stainless steels.

There are no setup differences between these coatings when programming your machine. Speeds and feeds depend on the specific toolpath and family used, though coatings generally allow for higher cutting speeds. Choosing the correct coating for your material results in longer tool life and more efficient production.

Tool Storage Recommendations

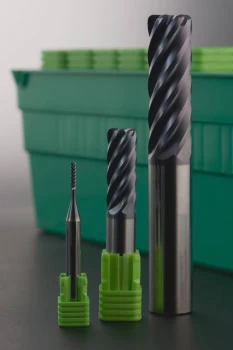
helical end mills in clear cases with green tops

For best results, Helical recommends storing tools in individual padded tubes rather than in shared bins. This prevents damage to flutes, cutting edges, and coatings. A clean, dry environment helps maintain tool quality and ensures consistent performance over time.

Conclusion

Tool coatings are essential for optimizing performance based on the material being machined. Helical’s coatings are engineered, tested, and proven to deliver the best results across specific materials and applications. By pairing the right tool family and coating, machinists can improve machining efficiency, enhance part quality, and extend tool life.

For more insights on cutting tool coatings, watch this episode of In the Loupe TV: Cutting Tool Coatings.

If you have additional questions about coatings or specific applications, contact Helical’s technical team for guidance at 1-866-543-5422 or by email. Helical’s experts are ready to help you find the ideal tool and coating combination for your needs.

https://www.harveyperformance.com/wp-content/uploads/2025/11/Helical-Tool-Coatings.jpg 525 1400 Michaela Martell http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Michaela Martell2025-11-13 09:29:232025-11-13 16:47:39The Key Differences Between Helical’s Tool Coatings

HREM vs HEM: Titanium Milling Test Results

July 30, 2025/2 Comments/in CNC Machining, Harvey Tool, Helical Solutions, High Efficiency Milling, Large Featured, Machining Techniques, Milling/by Harvey Performance Company

Harvey Performance Company’s Don Grandt Employs a Novel “Heavy Radial Efficiency Milling” or “HREM” Technique to Boost Tool Life and Minimize Heat Generation in Titanium

For all the characteristics that make Titanium ideal for extreme conditions, such as its high strength, low density, and corrosion resistant properties, it also makes it very difficult to machine. A modern approach to machining, High Efficiency Milling (HEM), helps. It involves using the theory of chip thinning by applying a smaller Radial Depth of Cut (RDOC), and a larger Axial Depth of Cut (ADOC). This method puts the vast majority of an end mill’s cutting edge to work, evenly distributing heat throughout it. An HEM toolpath works by taking more radial passes with a lower RDOC.

But from experience, Harvey Performance Company National Applications Engineer and “Cutting Tool Counselor,” Don Grandt, has found that there’s a better way to machine titanium. Rather than HEM, Don employs a strategy he calls “Heavy Radial Efficiency Milling (HREM)”, something he’s developed over time with a tried and true “Theory, Science, Experience (TSE) Triple Knowledge Approach” to machining.

The Theory:

In switching from a regular toolpath to a standard HEM toolpath, machinists are permitted to increase the surface foot and boost material removal rates because there is less heat generated at the cutting edge due to the lighter radial depth of cut being utilized.

In titanium, specifically, recommended parameters for HEM are often in the ballpark of 400-500 SFM and 121-152 M/Min, with a radial step over of 6% of the cutting diameter. This allows you to increase the speed to achieve higher feed rates.

However, Don has noticed that most of the heat is coming from the SFM or M/Min when machining titanium, and not the RDOC, thus prematurely fatiguing the cutting edge of the tool in HEM toolpaths. He uses the “MRR Triangle” to compensate for this.

In a 2022 episode of In the Loupe TV, a collection of videos Don creates to educate the machining industry on popular machining methods, tips, tricks, and more, he dives into the Material Removal Rate Triangle, explaining that it’s a representation of how IPM, ADOC, and RDOC interact.

“Each one of these things…contributes to your MRR, material removal rate. I know I don’t want to change that, I don’t want to stop it, and I don’t want to slow the customer down. So what do I do?

Three things (IPM, ADOC, and RDOC) are bringing in the heat. Which one’s causing the most heat? That’s what I want to find out. Because guess what? If I find out which one’s causing the most heat, and I can bring that down, then I can bring one of my other things over, adjust it, keep my MRR, and stay productive.”

In this case, Don opts to increase the RDOC while running the tool at lower SFM-M/MIN, the backbone of the “HREM” toolpath. An illustration of this toolpath, compared to a traditional and standard HEM toolpath, is below.

The Science:

While Don’s strategy can be utilized using any End Mill for Titanium, including Harvey Tool’s offering of Variable Pitch End Mills for Titanium Alloys, the below comparison of HEM vs. HREM toolpaths showcases a 6 Flute Helical Solutions End Mill for Titanium.

HEM vs. HREM Parameters Comparison (3.51 Cubes of Material)

HEM Parameters for ½”, 6 Flute Tool in Ti6AL4VHREM Parameters for ½”, 6 Flute Tool in Ti6AL4v
ADOC1.01.0
RDOC.030/6% Stepover.130/27% Stepover
SFM400220
RPM30561680
FPT.0064.0026
IPM11827
Spindle Load31%40%

This chart compares an HEM toolpath to an HREM toolpath, using the same Helical Solutions End Mill in Ti6AL4V Titanium.

Notice that in this independent study, the ADOC remains consistent, the IPM decreases, but the RDOC is substantially increased.

The change in parameters, utilizing the MRR Triangle as a model, generates consistent results in both time and MRR output, so what’s the benefit of making the change? Tool life. And again, it boils down to heat generation.

Toolpath Results

Traditional HEM Strategy

“HREM” Strategy

HEM Parameters for ½”, 6 Flute Tool in Ti6AL4VHREM Parameters for ½”, 6 Flute Tool in Ti6AL4v
Max Tangential Force228397
Peak Tool Temperature1,218° F / 660° C857° F / 458° C
Cubes of Material Removed3.51 Cubes of Ti6AL4V3.51 Cubes of Ti6AL4V

Here, we can identify that, though more max tangential force is applied to the tool in the HREM method, significantly less heat is generated.

While any cutting tool will generate heat, controlling it is pivotal to prolonging the life of your tool.

The Experience:

From the example above, where the same Helical Solutions End Mill for Titanium was utilized, you can see that by simply increasing the RDOC and slowing down the feed, while accommodating the chip with more flutes, the MRR remains consistent but the cutting edge of the tool faired much better. 

Toolpath Results

HEM Example

HREM Example

Before Utilizing an HREM Strategy

While HREM can be beneficial in extending the life of your cutting tool when machining titanium, there are several things that machinists must be mindful of before beginning. Notably, an HREM strategy will add more tangential force to your setup, meaning that fixturing, horsepower, and bending force must be properly accounted for.

In addition, the longer the tool’s length of cut, the less radial there is to be had. This means that if a tool’s length of cut is 2x the diameter, the maximum RDOC will be 27%. With 2.5x length of cut, the maximum radial will only be 20%. As the length of cut increases, the radial decreases, meaning that machinists must make adjustments accordingly to reduce the SFM and, in turn, reduce heat generation and built-up edge (BUE).

Harvey Performance Company Brand Tooling Best Suited for HREM

Leading cutting tool brands Helical Solutions and Harvey Tool offer several cutting tool options specifically designed for the machining of Titanium Alloys. Helical’s offering is extensive, with options ranging from roughers to 5, 6, 7, and multi-flute finishers. Included in this range of fully stocked product is the popular HVTI-6 line, which is optimized specifically for advanced machining toolpaths, such as HEM and HREM, in Titanium.

Harvey Tool’s Material Specific End Mill offering includes options for Titanium Alloys, as well. Featuring variable pitch geometry, options include both square and corner radius profiles. A new Variable Pitch End Mills for Titanium Alloys – Ball offering is set to be released in August 2025.

In Conclusion

By rethinking conventional titanium machining strategies, Don’s “Heavy Radial Efficiency Milling” (HREM) approach challenges the standard High Efficiency Milling (HEM) model with proven results. Through his “Theory, Science, Experience” methodology, Don demonstrates that increasing radial engagement while reducing surface speed can significantly lower tool temperatures and extend tool life, all without sacrificing productivity. Backed by data and real-world trials, HREM offers a compelling alternative for shops looking to optimize titanium machining performance in the most demanding applications.

Copyright © 2025 Harvey Performance Company, LLC. All rights reserved. This article may not be reproduced or distributed without permission.

https://www.harveyperformance.com/wp-content/uploads/2025/07/1400x525-Featured-Image-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-07-30 10:26:362026-03-31 09:47:34HREM vs HEM: Titanium Milling Test Results

A Closer Look at Helical Solutions’ Tapered End Mills

January 29, 2025/0 Comments/in CNC Machining, Helical Solutions, Machining 101, Machining Techniques, Milling, Specialty Tools, Tool Geometry, Tool Information Guides, Tool Selection/by Thomas Donahue

Helical Solutions offers a variety of Tapered End Mills designed to enhance performance and efficiency in tapered wall applications. In this blog post, we’ll dive into the geometry of tapered end mills and explore their common applications to understand when they could be utilized to optimize your CNC machining application.

Tapered End Mill Geometry

Tapered End Mills bring many advantages to machining compared to standard end mills, but what is a Tapered End Mill? A standard end mill will have the same cutting diameter throughout the whole length of cut, whereas a taper mills starts at the shank or neck at a larger diameter and tapers down at a specific angle.

The angle of the taper can vary, but Helical Solutions’ tools feature angles ranging from .05° to 5°, which allows for a broad spectrum of cutting operations. A tapered length of cut or tapered neck can also provide increased strength and rigidity, compared to that of a standard end mill. Having a tapered length of cut makes it easier to create flat tapered walls on 3-axis machines and leads to a better finish.

Tapered End Mill

Standard End Mill

Common Taper Mill Applications

Tapered End Mills are used in any machining process that requires an angled surface. These tools are engineered for light profiling and finishing applications in mold and die pockets and other tapered wall applications.

Mold & Die Applications

Mold and die applications are a mass production manufacturing method that consists of shaping different types of metals and other materials. Molds are used to shape metals, allowing them to become solid in the mold, while dies use a mechanical force to cut the material into the desired shape.

A couple examples of mold and die applications are plastic bottles, car body parts, electronic components, cutlery, coins, and metal stamping parts.

Mold Tool & Die Example

Tapered End Mills Profiles

Taper mills are great for profiling with the ball nose version, and for light finishing and creating required draft angles with the square version. Which style is right for you?

Ball Nose Taper Mills

Ball Nose Tapered End Mills are great for profiling because the full radius at the bottom eliminates sharp edges, which leads to a smoother process.

Square Profile Tooling

The square version of the tapered end mill has a higher flute count and helix angle with a sharp cutting edge. This is better for light finishes on the walls of tools.

The draft angle determined in the design process is the amount of mold design can be tapered. A draft angle is a strategic angle or slope designed in the mold. The tapered angle in the tool allows for the draft angle to be formed easier compared to a straight shanked end mill. Having a draft angle in the mold allows for easier removal of the part so it does not get stuck to the mold.

Helical Solutions’ Tapered End Mills

Helical Solutions’ offering of Tapered End Mills feature a tapered profile design, variable pitch geometry for reduced harmonics and increased feed rates, and Aplus coating for increased performance in Cast Iron, Steel, and even Stainless Steel. These tools are offered in a 4 Flute Ball style, and a 5 Flute Square style, so you can select the end profile that best suits your specific toolpath.

Helical’s Tapered End Mills

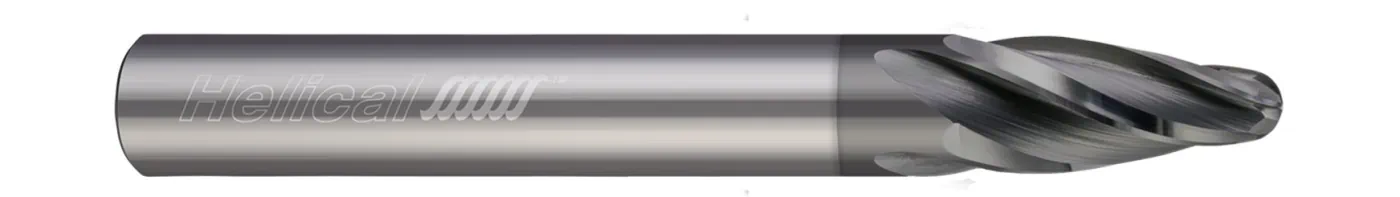
4 Flute Ball (HTPR-4)

Helical’s 4 Flute Ball Tapered End Mills (HTPR-4) are fully stocked in 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a ball nose profile, allowing them to excel in a variety of different applications from 3D contouring and profiling to slotting. A Ball Nose End Mill has a full form radius, allowing machinists to utilize the entire radius when contouring and finishing a 3D surface.

5 Flute Square (HPTR-5)

Helical’s 5 Flute Square Tapered End Mills (HTPR-5) is also is also fully stocked 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a square profile for more precise finishing and the 5 flute design creates a larger core, allowing for better tool strength in roughing applications.

Taper Mill Tooling Wrapped-up

By understanding the unique features and advantages of this tooling, machinists can make informed decisions and achieve superior results in their projects. These feature unique geometry that enhances machining capabilities and ensures reliability and accuracy across a range of tapered wall applications.

https://www.harveyperformance.com/wp-content/uploads/2025/01/DSC_0434.jpg 525 1400 Thomas Donahue http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Thomas Donahue2025-01-29 15:55:382025-01-30 09:14:54A Closer Look at Helical Solutions’ Tapered End Mills

Multi-Axis Finisher Q&A

March 29, 2024/2 Comments/in Helical Solutions, How-To's, Large Featured, Machining 101, Machining Techniques/by Tom Pyle

What is a Multi-Axis Finisher?

A tool that uses an extremely large radius to increase finishing performance in two different ways, depending on the needs of the machinist. Either the Multi-Axis Finisher will provide a better surface finish than a traditional Ball End Mill in the same amount of time, or will provide the same surface finish in far less time than a traditional Ball End Mill. A middle ground with improved surface finish and reduced cycle time is also easily achievable.

What Are Other Names for Multi-Axis Finishers?

Multi-Axis Finishers are oftentimes referred to as Barrel Cutters or Conical Barrel Mills or Circle Segment Cutters, among many others.

What Are the Different Forms of Multi-Axis Finishers, and How Do They Differ?

There are several different forms of Multi-Axis Finishers, including Lens, Taper, Oval, and Barrel. With a Lens Form, there’s a large radius on the end of the tool that’s in line with the tool axis. Taper Form, in contrast, has three tangential radii and a large radius defined at a specific angle relative to the tool axis. An Oval Form has two tangential radii, offering additional angle flexibility, while a Barrel Form has a large radius on the OD of the tool.

The most significant benefit is oftentimes observed utilizing a Taper Form Multi-Axis Finisher, as the radius of this tool can become vastly large on this form, while the others are more limited. However, this great benefit also comes with the least amount of flexibility in terms of approach to a workpiece.

What Are the Benefits of a Multi-Axis Finisher?

There are two clear benefits to using a Multi-Axis Finisher, compared to a Ball End Mill: Increased surface finish, and reduced cycle time (Or most likely both, concurrently).

What is a Benefit Multiple?

Helical Solutions is the industry’s premier manufacturer of Multi-Axis Finishers, and the Benefit Multiple is a significant reason why. Helical specifies the theoretical benefit that can be seen with its Multi-Axis Finishers, providing machinists direct insight into the gains that can be realized with these tools.

Benefit Multiple refers to the Cusp Height, correlated directly with the theoretically-achievable surface finish. Assuming the same cusp height from a Ball End Mill to a Multi-Axis Finisher, the Benefit Multiple relates to the time savings that could be seen in a machinists’ toolpath. For example, a Benefit Multiple of 4 would result in a toolpath ¼ as long as for a Ball End Mill of the same diameter. The stepover pass-to-pass would be 400% as much as a Ball End Mill to keep the same cusp.

When Should I Not Use a Multi-Axis Finisher?

Multi-Axis Finishers are best applied to wide-open surface areas; or large, smooth contours rather than small features or tight areas. Application of these tools will always be on a case-by-case basis. For help with your specific application, contact Helical Solutions Technical Support at 866-543-5422.

How Can I Get the Most Out of My Multi-Axis Finisher?

Multi-Axis finishers are best utilized when working further towards the OD of the tool. Tapered Form Multi-Axis Finishers are the most obvious choice for this, as its nose radius is small and has the least amount of efficiency. Similarly to a ball end mill, working near the center will have limited cutting ability, while the OD of the tool will see the full surface footage of the programmed RPM.

Taper Form Multi-Axis Finishers should be used when tilted at the specified taper angle. Oval Form Multi-Axis Finishers should be used towards the OD. Lens Form Multi-Axis Finishers should be tilted to avoid working on-center.

Lens Form Multi-Axis Finishers Look Like a High Feed End Mill. Can I Use it That Way?


Yes. However, there are differences in the form, and while a Lens Form Multi-Axis Finisher could theoretically be used as a High Feed End Mill, the two tools are not interchangeable.  A High Feed End Mill would not be the best choice for Multi-Axis Finishing, nor would a Lens Form Multi-Axis Finisher be our first recommendation for feed milling.

Do I need special software to program Multi-Axis Finishers?

Yes. A number of years ago, there were only a few CAM software packages that supported the programming of these specific forms. Nowadays, most CAM software providers have some degree of support for this method. Two of the first CAM software offerings to support this were MasterCAM and Hypermill, though many additional options exist today.

Why haven’t I heard of Multi-Axis Finishers Until Now?

In the grand scheme of things, Multi-Axis Finishers provide a very new approach to finishing, having been developed within the last handful of years.  Similar to High Efficiency Milling, these tools offer a new technique to approach your workpiece, offering increased efficiency and reduced cycle times.  Compared to the history of milling, modern tool manufacturing and CAM software have only just become able to program these unique forms.  Multi-axis finishers are positioned to revolutionize the world of finishing.

For more information on Multi-Axis Finishers, visit Multi-Axis Finishers: The Key to Amazing Surface Finish.

https://www.harveyperformance.com/wp-content/uploads/2024/03/Featured-Image-Multi-Axis-Finishers-QA.jpg 525 1400 Tom Pyle http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Pyle2024-03-29 10:27:012024-11-07 16:12:11Multi-Axis Finisher Q&A

Multi-Axis Finishers: The Key to Amazing Surface Finish

March 29, 2024/0 Comments/in CNC Machining, Helical Solutions, Large Featured, Tool Information Guides, Tool Selection/by Tom Pyle

A Key to Improving Surface Finish

In today’s Manufacturing Industry, part finish and machining efficiency are key to a successful machine shop. It’s no surprise, therefore, that the popularity Multi-Axis Finishers has never been greater. Helical Solutions is a leader in the manufacturing of Multi-Axis Finishers, and its customers utilize this impressive tool when faced with extremely high surface finish requirements, oftentimes swapping out a traditional Ball End Mill to dramatically improve finish while minimizing cycle times.

Multi-Axis Finisher Basic Principles

A Multi-Axis Finisher can be easily recognized by its large radius included in the profile of the tool. With a larger radius, a far greater stepover can be used pass-to-pass while keeping the same cusp height as a Ball End Mill. This decreases the cycle time by a known value called the Benefit Multiple.

A Multi-Axis Finisher with a Benefit Multiple of 8 will reduce the cycle time to 1/8 of the cycle time for a Ball End Mill of the same shank diameter – an 87.5% time savings! If a Multi-Axis Finisher is used with the same pass-to-pass stepover as a Ball End Mill, the finish will be drastically improved due to exponentially smaller cusp heights. Most situations allow both reduced cycle time and improved surface finish to be achieved.

The images below show the comparison of a ball end mill to an Oval Shape Multi-Axis Finisher with a benefit multiple of 4.

Due to their large radii, Multi-Axis Finishers are best suited for wide open, flowing, and somewhat flat surfaces. Smaller spaces, especially tight corners, will generally not see as much benefit from these tools due to limited use of the major radius.

Multi-Axis Finisher Tool Selection

The Manufacturing Industry’s leader in Multi-Axis Finishers, Helical Solutions offers 3 distinct profiles, each fully stocked and available to ship the day of purchase.

Oval Form Multi-Axis Finishers

The oval form includes 2 tangential radii and offers the most versatility in smaller spaces where a slightly varied approach angle is required, such as impellers or fan blades.

Taper Form Multi-Axis Finishers

The taper form includes 3 tangential radii and a taper angle. It allows for the largest radius, and therefore greatest potential improvement of finish and reduction of cycle time. They are best used where a specific approach angle is needed and where maximum performance gain is desired.

Lens Form Multi-Axis Finishers

The lens form includes 2 tangential radii on the end of the tool and is used for work mostly on the face of a part. Tilt angles of approximately 5 degrees are recommended for these tools to avoid working on-center.

Programming Multi-Axis Finishers

Programming Multi-Axis Finishers requires some additional consideration compared to a typical end mill. Luckily, many modern CAM packages offer support for these unique profiles, including many of Helical’s CAM partners. Each software has their own name for these toolpaths, so reach out to your CAM or Helical sales rep to find how you can program yours!

For more information on Multi-Axis Finishers, and to learn if this advantageous tool is right for you, read our Multi-Axis Finishers Q&A.

https://www.harveyperformance.com/wp-content/uploads/2024/03/Featured-Image-Multi-Axis-Finisher-Keys-to-Surface-Finish-1.jpg 525 1400 Tom Pyle http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Pyle2024-03-29 10:27:002024-04-24 09:17:44Multi-Axis Finishers: The Key to Amazing Surface Finish

Maximizing Tool Life with Helical’s Dplus Coating

January 29, 2024/0 Comments/in Helical Solutions, Tool Information Guides, Tool Selection/by Harvey Performance Company

Choosing the correct tool coating is extremely important when machining highly abrasive materials like composites, graphite, aluminum alloys, and other non-ferrous materials. Proper coating selection will result in maximized tool life and a higher quality final part. When searching for a coating, it is imperative to find one that has high hardness and maintains a sharp cutting edge, like Helical Solutions’ Dplus coating. This post will explore what Dplus coating is (and isn’t), and when it might help you gain a competitive edge at the spindle.

What is Helical Solutions’ Dplus Coating?

Helical’s Dplus is a premium coating, specially engineered to extend tool life when machining materials ranging from aerospace aluminums to graphite or abrasive composites. It has a Tetrahedral Amorphous Carbon (taC) bond structure, which delivers remarkable enhancements in tool life compared to traditional DLC coatings.

Helical’s Dplus coating is applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a near-vacuum and distributes micron-thick layers evenly onto a properly prepared tool. Since this coating is applied via a PVD process, it is inherently different than true diamond created through Chemical Vapor Deposition (CVD) processes. While this means it can be outlasted by CVD diamond, Dplus is a thinner coating allowing it to have a sharper cutting edge.

For more information on the PVD coating process, read PVD Coating vs. CVD: Two Common Coating Application Methods.

When Should a Machinist Use Dplus Coating?

When Machining Highly Abrasive Materials

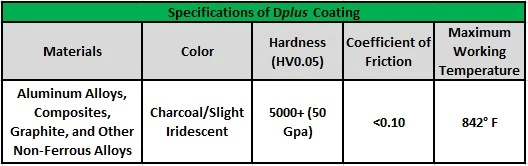
Dplus is an excellent choice when working in abrasive non-ferrous materials like graphite and high-silicon aluminums. It is an extremely hard coating (50 Gpa), which enables it to remain strong against abrasive materials. It also has a very low coefficient of friction, allowing for optimal lubricity. This reduces the risk of built-up edge and ensures chips can be easily evacuated out of the flute valleys.

In Production Runs

The combination of Dplus being an extremely hard and sharp coating, makes it a true winner when it comes to tool life. Using a coated tool in extended production runs can pay dividends at the spindle, especially when working in highly abrasive non-ferrous materials.  

Although Dplus takes the spot as Helical’s highest performing coating for non-ferrous materials, it may not be needed in certain applications. Its high hardness and abrasion resistance may be necessary for long production jobs, but may not be necessary for shorter jobs and one-off parts.

When Should a Machinist NOT Use Dplus Coating?

In High Temperature Applications

Although Dplus coating provides outstanding tool life and sharpness, it can’t be run at extremely high temperatures. This coating should not be run in any ferrous material or high temperature aerospace alloys.

Key Takeaways

Featuring an exceptionally low coefficient of friction and extremely high hardness, Helical’s Dplus coating maintains a sharp cutting edge, while still resisting abrasion, making it an excellent choice in low temperature applications of highly abrasive non-ferrous materials.

For more information on Helical Solutions’ coatings, visit https://www.helicaltool.com/resources/tool-coatings.

https://www.harveyperformance.com/wp-content/uploads/2024/01/Featured-Image-Dplus-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-01-29 11:05:582025-01-30 09:06:02Maximizing Tool Life with Helical’s Dplus Coating

Helical Nplus Coating: Advantages and Performance

April 28, 2022/0 Comments/in Helical Solutions, Tool Information Guides, Tool Selection/by Harvey Performance Company

When it comes to machining difficult materials like high-silicon aluminums, abrasive copper alloys, and other non-ferrous and aluminum alloys, finding a coating that improves performance and increases tool life can be difficult. When machining in aluminum-based materials, machinists often opt for an uncoated tool due to the sharp cutting edge needed. Uncoated tools may give you the sharpest edge possible, but Helical’s Nplus coating helps combat wear and keep your edge sharp for longer, allowing you to win at the spindle and gain a competitive edge.  

What is Helical Solutions’ Nplus Coating?

Helical’s Nplus coating is applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a near-vacuum and distributes micron-thick layers evenly onto a properly prepared tool.

For more information on the PVD coating process, read PVD Coating vs. CVD: Two Common Coating Application Methods.

Nplus is a premium coating, specially engineered to extend tool life when machining non-ferrous and aluminum alloys. 

nplus coating chart
The above image was taken from Helical Solutions’ Coating Chart.

When Should a Machinist Use Nplus Coating?

When Machining Non-ferrous and Aluminum Alloys

Helical’s Nplus coating is optimized for machining difficult aluminum alloys and other abrasive non-ferrous materials, as its composition doesn’t react with aluminum as some other coatings do. This coating possesses many advantageous qualities, including its high hardness (40 GPa), which provides excellent edge retention to ensure that your tool stays sharp for longer. Also, its high working temperatures (2,012°) and its thickness (1-4 µm) provide further wear resistance when tackling these difficult-to-machine materials.

Nplus coated Helical end mills

When Working in High Temperature Non-Ferrous Applications

When machining in many non-ferrous and aluminum alloys, high temperatures can become an issue. Nplus is specially designed to withstand temperatures up to 2,012°, allowing tooling to run at the high temperatures these abrasive materials require, without degrading them.

When Machining Large Production Runs

Machining materials like wrought aluminum, cast aluminum, graphite, and other non-ferrous alloys can quickly end the life of your tool, costing time and money. Nplus coating is specially engineered to extend tool life in these materials, allowing your tool to stay in the spindle for longer. This calls for less tool changes, creating a more efficient process flow in your large production runs.

Helical’s Nplus Coated Tooling

Helical’s 5 Flute End Mills for Aluminum

Introduced in Helical’s Spring 2022 Catalog, Helical’s 5 Flute End Mills for Aluminum are specially engineered for optimal performance in High Efficiency Milling (HEM) of aerospace aluminum alloys and other non-ferrous alloys. They’re offered in two unique styles, both fully stocked in Helical’s Nplus coating:

5 Flute – Corner Radius  – Variable Pitch – Chipbreaker Rougher

5 Flute – Corner Radius – Variable Pitch – End Mill

Helical’s Multi-Axis Finishers for Aluminum

Also introduced in Helical’s Spring 2022 catalog, this offering of Multi-Axis Finishers feature a specially defined profile for massive reductions in cycle times and vastly improved surface finish when machining aluminum.  They’re offered in 3 styles, all fully stocked in Helical’s Nplus coating to ensure excellent finish in abrasive aluminums and extended tool life in a wide variety of non-ferrous materials.

Multi-Axis Finishers – 3 Flute – Lens Form

Multi-Axis Finishers – 4 Flute – Taper Form

Multi-Axis Finishers – 4 Flute – Oval Form

For more information on Helical Solutions’ coatings, visit https://www.helicaltool.com/resources/tool-coatings.

https://www.harveyperformance.com/wp-content/uploads/2022/04/Feature-Image-Nplus-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2022-04-28 08:51:022025-11-12 15:51:11Helical Nplus Coating: Advantages and Performance

Machining Nickel Alloys: Common Mistakes to Avoid

April 4, 2022/1 Comment/in CNC Machining, Helical Solutions, Large Featured, Material Specific/by Will Lauzon


Nickel-based alloys are growing in popularity across many industries such as aerospace, automotive, and energy generation due to their unique and valuable mechanical and chemical properties. Nickel alloys exhibit high yield and tensile strengths at low weights and have high corrosion resistance in acidic and high temperature environments. Because of these advantageous properties, nickel alloys have increasingly become popular in machine shops.

Unfortunately, nickel alloys have a reputation for creating issues at the spindle. These metals present themselves to be problematic as they easily work harden. Further, nickel alloys generate high temperatures during machining, and have gummy chips that can weld onto cutting tools, creating built-up edge (BUE). Fortunately, with the correct approach, one can be successful in cutting nickel alloys.

Work Hardening

Across machine shops, nickel alloys are notorious for being difficult to machine. This reputation stems, largely, from work hardening, or a metal’s microhardness increasing due to the addition of heat. According to the Nickel Development Institute, this heat is generated through friction and plastic deformation of the metal. As the metal is cut, the friction between the cutting tool and workpiece generates heat which is concentrated around the cutting area.

Simultaneously, the metal is being physically worked. This means that as it is being machined, it is experiencing plastic deformation, which is a physical property that measures how much a material can be deformed to the point that it cannot return to its original shape.

This physical working of a nickel alloy increases its hardness faster than it does most other metals. The combination of high heat generation and physical work quickly increases the alloy’s hardness, causing tools to dull quickly and fail. This may result in scrapped parts and broken tools.

8 flute HVNI End Mill for Machining Nickel Alloys
Shown above is Helical Solutions’ End Mill for Nickel Alloys. This tool, engineered to excel in Inconel 718 and other nickel-based superalloys, is fully stocked in 6 and 8 flute styles.

Tool Adhesion

As nickel alloys are being machined and heat is generated, chips tend to become stringy and weld themselves to a tool’s cutting edge. This phenomenon, built up edge or BUE, rounds the cutting edge of the tool, resulting in poor cuts and increased friction, thus further contributing to work hardening. An example of BUE is seen in the image below.

Zoomed in display of built-up edge on End Mill Flutes
On the above tool, chips from the workpiece (Inconel 718) have welded onto the cutting edge, severely decreasing the tool’s effectiveness. Image Source: International Journal of Extreme Manufacturing

Built-up edge also speeds up tool wear, as the rotational forces involved in the cut increase. Now that the cutting edge is rounded from welded chips, a blunt tool is being forced into the workpiece.

With a blunt edge, the cutting motion changes from a shearing action to plowing. In other words, instead of cutting through the metal, the tool is pushing the material, resulting in poor cuts and increased friction.

Excessive Heat Generation

With poor cutting, internal heat of the tool rises, which can cause thermal cracking, defined by cracks that form perpendicular to the cutting edge. The fractures within the tool are created by extreme internal tool temperature fluctuations.

As a cutting tool rapidly overheats while cutting nickel alloys, cracks may form which can lead to catastrophic tool failure. With high temperatures, galling may also occur, which is characterized by pieces of the tool flaking off due to the same adhesion that causes BUE. As the tool is being welded to the workpiece and the machine continues to rotate it, pieces of the tool may start to break off resulting in tool failure.

Overcoming Nickel Alloy Difficulties

Temperature Control and Coolant Usage

The first step to effectively machine nickel alloys is to keep temperatures manageable as the workpiece is cut. Using high pressure coolant is mandatory. Coolant pressure should be 1000 psi or greater. This high pressure concentrating on the cutting zone of the workpiece will dissipate heat within both the cutting tool and workpiece. By doing so, the chances of work hardening lessen.

High pressure coolant will also aid in clearing out chips from the cutting area. Those hot gummy chips are responsible for BUE. Removing them as quickly as possible reduces the risk of BUE forming on the cutting edge. Additionally, chip removal is important to avoid chip recutting.

Chips absorb much of the heat and often work harden themselves. Recutting these hardened chips will dull the cutting edge resulting in poor cuts and decrease tool life. In general, water-based cutting fluids are preferable as they have higher heat removal rates and have a lower viscosity, which is needed for high metal removal operations.

Using the Proper Techniques

To also assist with heat removal, utilize climb milling techniques, where possible. When climb milling, the chip thickness is at its maximum at the beginning of the cut and tapers off until the cut is complete. Due to this, less heat is generated, as the cutting tool does not rub on the workpiece. Most of the heat from the cut is transferred into the chip.

Selecting the Proper Tooling and Coating

The next step is selecting the right end mill. Your end mill of choice should have a proper tool coating, such as Helical’s Tplus coating. Tool coatings are specifically engineered to improve tool performance by reducing friction, increasing tool microhardness, and extending tool life.

Next is selecting flute count. Tools used for nickel alloys need to be rigid to withstand the cutting forces present when machining high hardness alloys. Therefore, higher flute counts are necessary. If using traditional roughing toolpaths, your end mill should have at least 6 flutes. With 6 flutes, there is sufficient flute valley depth to allow for chip evacuation, while having a larger core diameter keeps the tool strong and rigid.

For finishing operations and instances of implementing high efficiency milling, higher flute counts should be considered. A tool used this way should have 8 flutes to provide excellent surface finish.

Helical’s End Mills for Nickel Alloys

CNC tooling manufacturer Helical Solutions’ End Mills for Nickel Alloys product offering, its HVNI tool family, specializes in machining nickel alloys as it exhibits these key tool features.

Four Helical Solutions End Mills for Nickel Alloys positioned over a Helical product container
The tools shown above are Helical Solutions’ End Mills for Nickel Alloys. These tools are coated in Tplus for high hardness, resulting in improved tool life and increased strength,

With its Tplus coating and variable pitch to minimize chatter, these solid carbide end mills are engineered to perform in all grades of nickel alloys. Coupled with their geometry to maximize cutting performance, Helical’s End Mills for Nickel Alloys utilize faster speeds and feeds, which are readily available on the Helical Solutions’ website and Machining Advisor Pro.

For more information about the chemical make-up, uses, and categorization of nickel alloys, read “In the Loupe’s” post “Understanding Nickel Alloys: Popularity, Chemical Composition, & Classification”.

https://www.harveyperformance.com/wp-content/uploads/2022/04/Feature-Image-Nickel-Alloys-2-IMG.jpg 525 1400 Will Lauzon http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Will Lauzon2022-04-04 11:44:542025-11-20 09:47:58Machining Nickel Alloys: Common Mistakes to Avoid

Understanding Nickel Alloys and Their Properties

April 4, 2022/2 Comments/in Helical Solutions, Material Specific/by Will Lauzon

What is Nickel Alloy?

Nickel-based alloys have been a cornerstone of manufacturing for decades, desirable for their broad range of varying resistances to heat, oxidation, and corrosion. Nickel alloys also have a high strength-to-weight ratio and superior electrical conductor abilities. Because of these mechanical and chemical properties, they are primarily used in aerospace, oil, electrical, and chemical industries.

Understanding this valuable metal and how to properly machine it is imperative to delivering an optimal final part.

cnc machining nickel alloys
Machining Nickel Alloys. Image source: IMS-Stainless.com

Nickel Alloy Chemical Composition and Classification

Nickel is commonly found in the form of an alloy, as its crystalline structure allows the element to be paired well with other metals. These atoms are arranged in a face centered cubic lattice; this structure is shown in figure 1 below.

Drawing that shows lattice structure of Nickel
Lattice structure of Nickel. Image source: PriyamStudyCentre.com

The Atomic Configuration of Nickel

According to Priyam Study Centre’s Learning Chemistry, an open face lattice has the highest atomic packing number (the number of atoms per unit volume) of any metallic lattice configuration, with an atom present at each of the 6 faces and 8 corners of the cube. This structure is largely responsible for nickel’s strength and ability to create strong metallic bonds to chromium, cobalt, iron, and molybdenum, the most common metals found in these alloys.

Categorization of Nickel Alloys

According to City Special Metals’ article on Machining Nickel and Nickel Alloys, nickel alloys are organized into five main categories: Groups A through E. These groups are determined through the percentage of nickel present, as well as the most prominent metal that the nickel is chemically bonded with.

Table 1 displays the breakdown of these groups, showing each group’s chemical composition and a few examples of common types of nickel alloys found in that category.

GroupPercentage of NickelPaired MetalsExamples
Group A95% and greaterAlmost pure nickelNickel 200, 201, 205, and 212
Group B29% to 42%CopperMonel 400, Invar 36
Group C70% to 75%Chromium and ironInconel 600, Monel K-500, and Nickel 270
Group D50% to 56%Chromium and ironInconel 718, Inconel 625, and Hastelloy C-22
Group E63%Copper and ironMonel R405 is the only Nickel alloy in this category
Table 1: Categories of nickel alloys and their chemical compositions. Table data source: Machining Nickel and Nickel Alloys: A Guide from CSM; Nickel Based Alloys: Everything You Need to Know.

Significance of Understanding Composition

Understanding your workpiece material is just as important as understanding your machinery and tools. According to Global Market Insights (GMI), the nickel alloy market has been growing over 4% each year since 2017, and this growth is seeing an upward trend. As these alloys increase in popularity and demand, knowing the chemical compositions and classification of your specific workpiece will play a key role in successfully machining it.

Fabricating products made of nickel alloys present common struggles in every machine shop. Learn how to select proper tooling and implement machining techniques to overcome these challenges by reading CNC Machining Nickel Alloys: Avoiding All-Too-Common Mishaps.

https://www.harveyperformance.com/wp-content/uploads/2022/04/Feature-Image-Nickel-Alloys-1-IMG.jpg 525 1400 Will Lauzon http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Will Lauzon2022-04-04 11:34:292025-11-20 09:50:25Understanding Nickel Alloys and Their Properties

4 Key Benefits of Combination Feed & HEM End Mills

February 15, 2022/1 Comment/in Helical Solutions, Large Featured/by Harvey Performance Company

Designed to conquer machine limitations and other common machining issues, combination and multifunctional tooling are highly coveted by machinists. These tools often integrate multiple geometries and flute designs to tackle wider varieties of machining applications with the same tool. This means fewer tools and tool changes are needed within a job, reducing complexity and increasing shop flexibility.

Taking these Issues and limitations into consideration, Harvey Performance Company’s Engineering Team went to work to design a new series of end mills referred to as Helical Solutions’ Combination High Feed & HEM End mills. This product series offers a feature set that will solve the four common issues listed below along with a few other issues that machinists commonly experience in the spindle.

For most shops, machine limitations cause longer, costlier, and more complicated jobs. If you are reading this article, you may know exactly what we are talking about. Machinists have a job that needs to be completed and end up having to add another operation. They find themselves improvising on tooling to complete an operation. This is because their machine has a limited number of tool stations, less than adequate horsepower, or several other limitations. Many times, this will impact operations in a negative way by increasing overall cost or reducing the quality of parts. As the name suggests, Helical’s Combination Feed & HEM tooling has been designed to excel in both applications without requiring a tool change. The end profile is non-center cutting for high feed applications, while the offset chipbreaker OD geometry excels in high efficiency milling strategies.

Helical Solutions Combination Feed & HEM end mill

How This Tool Addresses Machine Limitations

A common issue present in a fair number of shops is a limited number of tool stations available. The Combination Feed & HEM products afford the ability to do multiple roughing and finishing operations with one tool, using only one tool position. This eliminates the need to try to blend tools or control multiple offsets in your machining operation.

A second machine limitation that may affect your tool choice is you machine horsepower. The high feed end geometry and the chipbreaker OD geometry are both designed to reduce the amount of power required. This opens up new opportunities within light duty and low horsepower machines, offering more flexibility to your shop.

Cut Down Part Cycle Times

In a shop, long cycle times negatively impact productivity and machine availability. As the manufacturing industry becomes more competitive and as jobs become more demanding, the need for reducing cycle times becomes even more important.

The Combination Feed & HEM End Mills allow the use of both High Feed and High Efficiency milling strategies that provide high metal removal rates in your operations.  Increased material removal rates lead directly to reduced cycle times, plus the versatility of these tools helps to avoid time-consuming tool changes.

Click Here to Watch Helical’s Combination Feed & HEM Mill Be Pushed to the Limits

Limiting Complexity and Increasing Ease of Use

With today’s machined parts growing in complexity, programming can become cumbersome with multiple machining strategies and many tools required.  Finding ways to reduce the complexity of programming can help an entire job run smoother through your shop.

These Combination Feed & HEM End Mills provide an increased ease of use. This gives you the ability to conquer multiple operations with one tool. This eliminates the need to program and set-up multiple tools, boosting productivity

Helical Solutions Combination Feed & HEM end mill laying over a product container

Cutting Down on Costs

Another common issue is the cost of purchasing tooling. The Combination Feed & HEM End Mills offer a feature set that allows the consolidation of tooling and operations. Reducing the number of different tools needed for your application can reduce the overall cost of your operations substantially.

Feed/HEM Product Capabilities and Application Areas

Helical’s Combination Feed & HEM End mills are designed to tackle a broad range of demanding operations in a wide variety of steel types. As these products were engineered to solve machine limitation issues, the end geometry excels across a variety of operations. These include High-Feed milling operations, machining bores, closed or open pockets, internal or external contours, etc. The peripheral geometry was engineered with flexibility in mind. This allows the use of an HEM (High Efficiency Machining) toolpath to achieve high metal removal rates while maintaining great chip control as well as most traditional roughing and finishing strategies.

Helical Solutions Combination Feed & HEM end mill laying over a product container

The versatility of these tools can be easily illustrated with a long list of applications:

  1. High efficiency milling
  2. High feed slotting
  3. High feed roughing
  4. Milling in open and closed pockets
  5. Internal and external profiling
  6. Helical ramping and interpolation
  7. Rough and finish profile milling
  8. Offset plunge milling in slots and deep pockets
  9. Traditional roughing operations
  10. Contouring and profiling operations

Commonly, machinists would need a range of specialty tooling to complete different aspects of a job. This requires long cycle times, and higher costs when all the necessary tools are considered. As most shops suffer from a limited number of available tool stations, combination mills aid in alleviating this pressure. These tools are designed to excel and conquer.

Conquer Machine Limitations and Shop Issues

Helical’s Combination Feed & HEM End Mills were designed with versatility in mind. The major benefit of these tools is addressing machine limitations and the common issues presented above. These tools will provide you with a feature set that will allow you to combine operations, reduce cycle times, reduce cost, reduce scrap, and expand your machines capabilities. Let Helical impress you with the Combination Feed & HEM line of end mills.

https://www.harveyperformance.com/wp-content/uploads/2022/02/Feature-Image-Combo-Feed-HEM-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2022-02-15 15:52:512023-09-21 14:11:204 Key Benefits of Combination Feed & HEM End Mills
Page 1 of 3123
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top