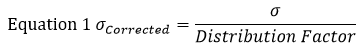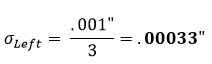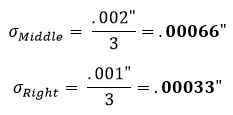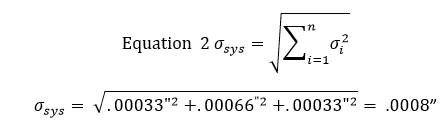
Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Advance Your Machining Career With 8 Expert Tips

August 19, 2019/7 Comments/in How-To's, Quick Tips/by Harvey Performance Company

Since we began shining a light on Harvey Performance Company brand customers via “In the Loupe’s,” Featured Customer posts, more than 20 machinists have been asked to share insight relevant to how they’ve achieved success in advancing their machining career. Each Featured Customer post includes interesting and useful information on a variety of machining-related subjects, including prototyping ideas, expanding a business, getting into machining, advantages and disadvantages of utilizing different milling machine types, and more. This post compiles 8 useful tips from our Featured Customers on ways to advance your machining career.

Tip 1: Be Persistent – Getting Your Foot in the Door is Half the Battle

With machining technology advancing at the amazing rate that it is, there is no better time to become a machinist. It is a trade that is constantly improving, and offers so many opportunities for young people. Eddie Casanueva of Nueva Precision first got into machining when he was in college, taking a job at an on-campus research center for manufacturing systems to support himself.

“The research center had all the workings of a machine shop,” Eddie said. “There were CNC mills, lathes, injection molding machines, and more. It just looked awesome. I managed to get hired for a job at minimum wage sweeping the shop floor and helping out where I could.

As a curious student, I would ask a million questions… John – an expert machinist – took me under his wing and taught me lots of stuff about machining. I started buying tools and building out my toolbox with him for a while, absorbing everything that I could.”

One of the best things about becoming a machinist is that there is a fairly low entry barrier. Many machinists start working right out of high school, with 12-18 months of on-the-job training or a one to two year apprenticeship. Nearly 70% of the machinist workforce is over the age of 45. The Bureau of Labor Statistics is predicting a 10% increase in the machinist workforce with opportunities for 29,000 additional skilled machinists by 2024, so it is certainly a great time to get your foot in the door.

Tip 2: Keep an Open Mind – If You Can Think of It, You Can Machine It

Being open-minded is crucial to becoming the best machinist you can be. By keeping an open mind, Oklahoma City-based company Okluma’s owner Jeff Sapp has quickly earned a reputation for his product as one of the best built and most reliable flashlights on the market today. Jeff’s idea for Okluma came to him while riding his motorcycle across the country.

“I had purchased what I thought was a nice flashlight for $50 to carry with me on the trip. However, two days in to the trip the flashlight broke. Of course, it was dark and I was in the middle of nowhere trying to work on my bike. I’m happy to pay for good tools, but that wasn’t what happened. Not only was there no warranty for replacement, there was no way to fix it. It was just made to be thrown away. That whole attitude makes me angry. When I got home, I decided I was going to put my new skills to work and design and build my own flashlight, with the goal of never running into an issue like I had on my trip ever again. I started by making one for myself, then four, then twenty. That was four years ago. Now I have my own business with one employee and two dogs, and we stay very busy.”

An awesome side benefit to working as a machinist is that you have all the resources to create anything you can dream of, like Jeff did with Okluma.
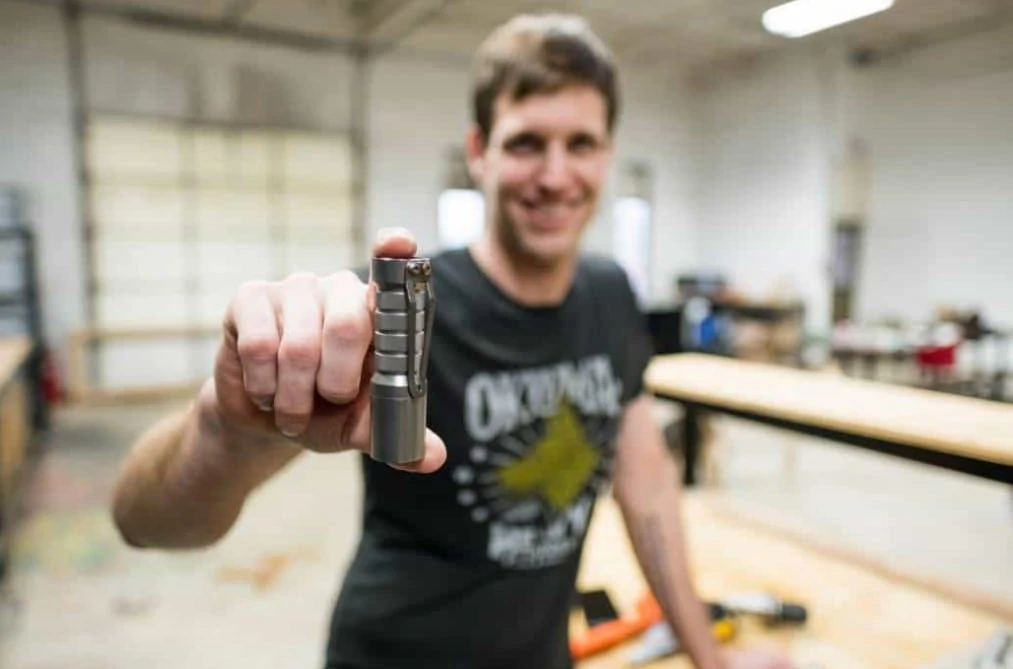
machining career

Image courtesy of Okluma.

Tip 3: Be Patient – Take Time to Ensure Your Job is Setup Correctly before Beginning

The setup process is a huge part of machining, but is often overlooked. Alex Madsen, co- owner of M5 Micro in Minnesota, has been working in manufacturing for more than 11 years. Alex is also a part owner of World Fabrication, and owns his own job shop called Madsen Machine and Design. Alex has spent countless hours perfecting his setup to improve his part times.

“It is certainly challenging to use little tools, but the key is to not get discouraged. You should plan on lots of trial and error; breaking tools is just a part of the game. You may buy ten end mills and break six, but once you dial one in it will last the rest of the job.

You should also make sure to put extra time and effort into understanding your machine when working on micromachining jobs. You need to know where there is any backlash or issues with the machine because with a tiny tool, even an extra .0003” cut can mean the end of your tool. When a difference of one tenth can make or break your job, you need to take your time and be extra careful with your machine, tool inspection, and programming before you hit run.”

Tip 4: Effort Pays Off In Your Machining Career – Long Hours Result in Shop Growth

Success isn’t earned overnight. That is especially true in the machining world. Becoming a good machinist takes a great deal of sacrifice, says Josh from Fleet Machine Co. in Gloucester, MA.

“Opening your own shop involves more than learning how to program and machine. You also need to be willing to sacrifice some of your free time by working long hours to build your business from the ground up. Being a great machinist is important, but you also need to understand the basics of business, and you need to be able to sell your service and maintain a certain level of quality to keep your customers coming back.”

Working hard is a common theme we hear from our featured customers. Brothers Geordan and Nace Roberts of Master Machine Manufacturing have similar advice.

“We often need to work odd hours of the day to maintain the business, but we do it in a way that makes sure we have our family time. There are many times where we will go home, have dinner and hang out with the family, and wait until they are all sleeping to go back to work until two or three a.m. We will get back home later that morning to sleep a little and have breakfast with the family and send them on their way before heading back into the shop.” Starting and growing a business takes time. Every machinist starts from the beginning and through hard work and determination, grows their business.
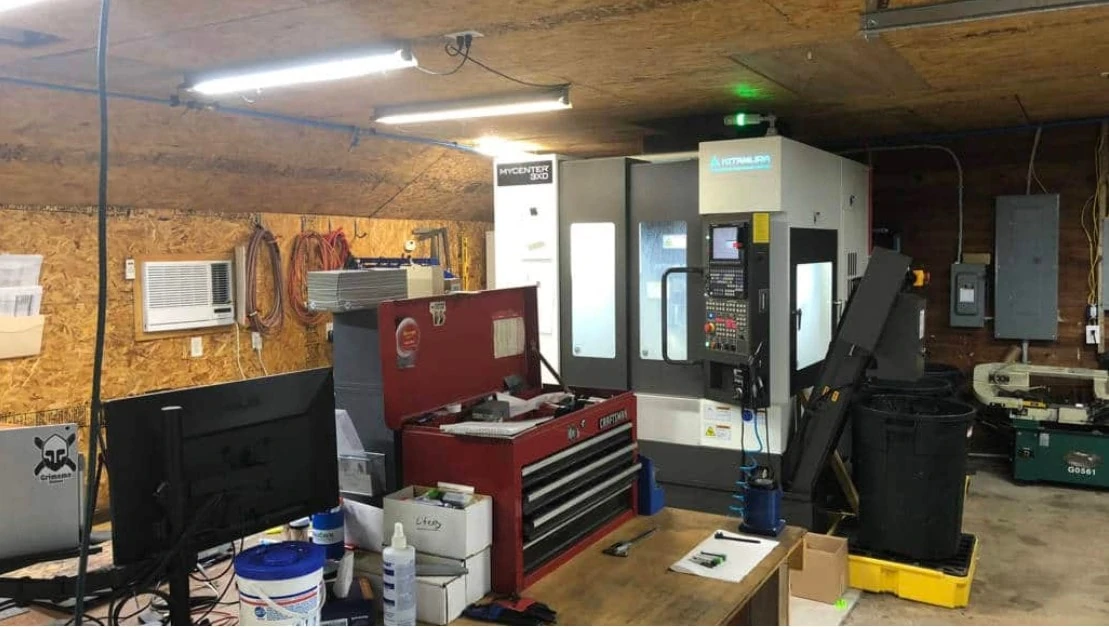
Liberty Machine cnc mill

Image courtesy of Liberty Machine Inc.

Tip 5: Utilize Tooling from Quality Manufacturers – All Tooling Isn’t Created Equal

When it comes down to it, tooling is singlehandedly the biggest choice you will make in your machining career. Grant Hughson, manufacturing engineer at Weiss Watch Company who works as a manufacturing instructor in his spare time, reflected on the importance of tooling.

“Tool to tool accuracy and performance is vital in this business, especially with our extremely tight tolerances. High quality tools make sure that we get the same performance time after time without needing to scrap parts. This saves us valuable time and money.”

While opting for cheaper tooling can appear to be beneficial when just starting out, before long, machinists are losing time and money because of unpredictability. Jonathan from TL Technologies echoed this point, saying:

“We feel that if we invested so much in these high-end machining centers, it would be criminal to put insufficient tooling and holders into them. We found that by selecting the proper tool with the appropriate sciences behind it we have been able to create products with a cost per cut that is not only competitive, but required to stay current. By keeping the quality as high as possible on the part making side of things, we’ve insured as much ease and reliability into our downstream process as we could. Quality tooling also provides predictability and added safety into the workflow. High-quality carbide tooling is the lifeblood of the business.”

Additional Thoughts Regarding Boosting Your Machining Career With Tooling:

Don’t Cheap Out

  • “The additional cost is always worth the payoff in the end knowing that you have a tool that will produce quality parts and shave valuable minutes off your cycle times. The slightly higher cost of the Harvey/Helical product is small change compared to the long term cost savings associated with their performance” – Seth, Liberty Machine

Consistency is Key

  • “We know the performance we are going to get from the tools is consistent, and we can always rely on getting immaculate finishes. While using the Harvey Tool and Helical product, we can confidently walk away from the machine and come back to a quality finished part every time.” – Bennett, RIT Baja SAE

Superior Specialty Tools

  • “One of the greatest things that I’ve experienced over the past year and a half is flexibility. We’ve asked for some specific tools to be made typically, the lead times that we found were beyond what we needed. We went through the Helical specials division and had them built within a couple of weeks. That was a game changer for us.” – Tom, John Force Racing

“Having high quality tooling like Helical is essential. Helical tools help us maintain a much higher machining efficiency because of the outstanding tool life, while also achieving more aggressive run times. In addition, we are able to consistently keep high tolerances, resulting in a better final product.” – Cameron, Koenig Knives

Tip 6: Get With the Times – Join the Social Media Community

Social media is a valuable tool for machinists. With ever-increasing popularity in networks such as Facebook, LinkedIn, Twitter, and Instagram, there will always be an audience to showcase new and unique products to. We asked a few of our featured customers how they incorporated social media into their machining career and the benefits that come along with it.

“A lot of our sales come through Instagram or Facebook, so I would recommend those platforms to anyone who is trying to start a business,” Jeff from Okluma said. “We have also had a lot of success collaborating with others in the community. Typically it is something we couldn’t do ourselves, or they couldn’t do themselves, so we share the labor and collaborate on some really cool items.”

Tip 7: Value Your Customers – Always Put Them First

“In the Loupe’s” featured customers repeatedly emphasized the importance of putting customers first. It’s a simple concept to master, and pays off immensely as you advance in your machining career. Repeat customers tell you that you are doing something right, said Brian Ross, owner of Form Factory.

“We have kept our customers happy and consistently deliver parts on time, so we get a lot of repeat business. Word definitely gets around on how you treat people so we try to treat everyone with respect and honesty which is key to running a good business.” Jeff from Okluma takes great pride in his customer service, saying “we only sell direct to consumers through our website so we can control our lifetime warranty. It has worked really well for us so far, so we have no plans to change that right now. I care more about our customers than any retailer is able to.”
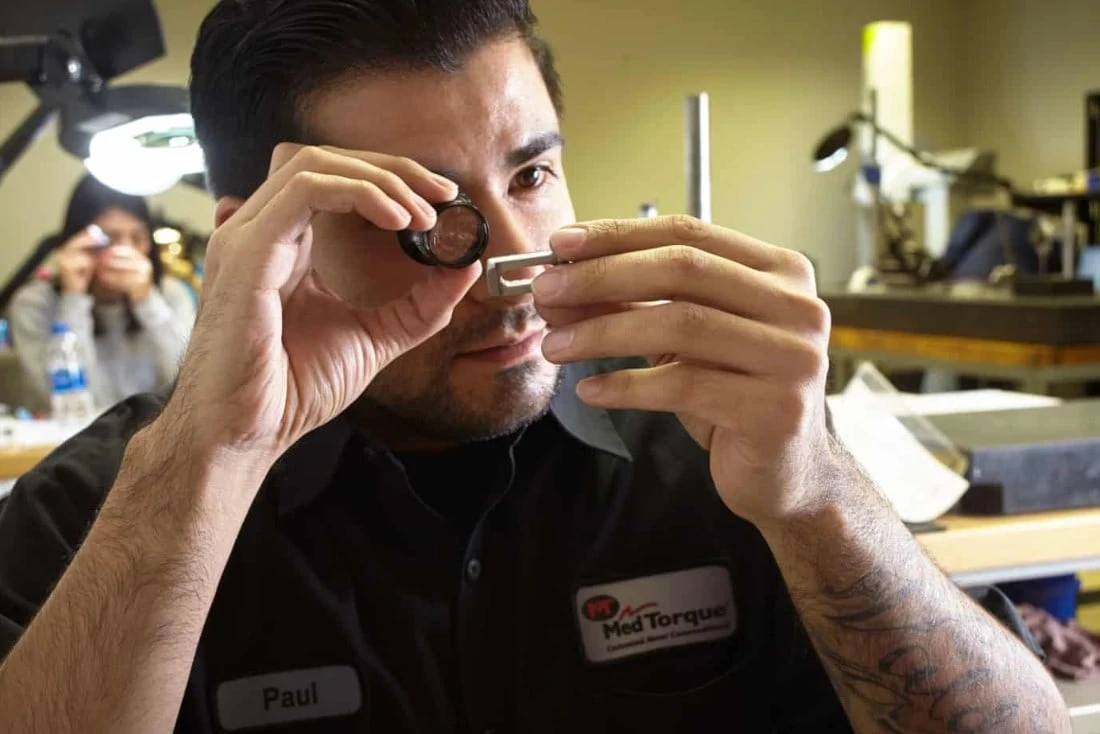
man examining machined part for machining career

Image courtesy of MedTorque.

Tip 8: Never Stop Learning – Ask Questions Whenever You Can as Your Machining Career Advances

Hopefully some of these tips from our featured customers stuck with you in exploring a machining career. To leave you with a quote from of Seth Madore, owner of Liberty Machine, “Don’t stop learning. Keep your ears open and your mouth shut,” “That old guy in the shop has likely forgotten more than you will ever learn. The amount of tools in your Kennedy box doesn’t mean you’re a good machinist. Some of the best toolmakers I knew had small boxes with only the common tools. Learn how to excel with limited resources. Ask questions, and own up to your mistakes.”
https://www.harveyperformance.com/wp-content/uploads/2019/08/Feature-Image-8-Tips-From-Machining-Pros-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-08-19 09:30:212025-11-12 15:55:51Advance Your Machining Career With 8 Expert Tips

Machining Precious Metals

July 1, 2019/10 Comments/in How-To's, Machining Techniques, Material Specific/by Robert Keever

Precious metals can be particularly difficult to machine due to their wide range of material properties and high cost if a part has to be scrapped. The following article will introduce these elements and their alloys as well as provide a guide on how to machine them effectively and efficiently.

About the Elements

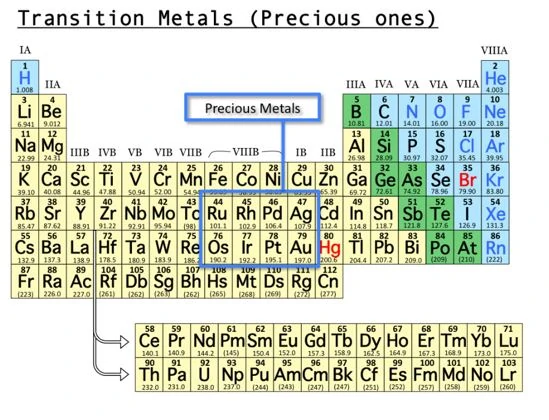
Sometimes called “noble” metals, precious metals consist of eight elements that lie in the middle of the periodic table (seen below in Figure 1). The eight metals are:

  1. Ruthenium (Ru)
  2. Rhodium (Rh)
  3. Palladium (Pd)
  4. Silver (Ag)
  5. Osmium (Os)
  6. Iridium (Ir)
  7. Platinum (Pt)
  8. Gold (Au)

These elements are some of the rarest materials on earth, and can therefore be enormously expensive. Gold and silver can be found in pure nugget form, making them more easily available. However, the other six elements are typically found mixed in the raw ore of the four metals they sit below on the periodic table: Iron (Fe), Cobalt (Co), Nickel (Ni), and Copper (Cu). These elements are a subset of precious metals and are generally called Platinum Group Metals (PGM). Because they are found together in raw ore, this makes mining and extraction difficult, dramatically increasing their cost. Because of their high price tag, machining these materials right the first time is incredibly important to a shop’s efficiency.

periodic table with a box around the 8 precious metals

Figure 1: Periodic table with the 8 precious metals boxed in blue. Image source: clearscience.tumblr.com

Basic Properties and Compositions of Precious Metals

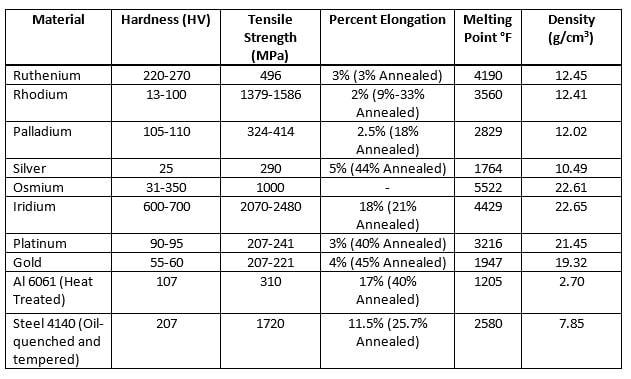
Precious metals have notable material properties as they are characteristically soft, ductile, and oxidation resistant. They are called “noble” metals because of their resistance to most types of chemical and environmental attack. Table 1 lists a few telling material properties of precious metals in their elemental form. For comparison purposes, they are side-by-side with 6061 Al and 4140 Steel. Generally, only gold and silver are used in their purest form as the platinum group metals are alloys that consist mainly of platinum (with a smaller composition of Ru, Rh, Pa, Os, Ir). Precious metals are notable for being extremely dense and having a high melting point, which make them suitable for a variety of applications.

Table 1: Cold-worked Material Properties of Precious Metals, 4140 Steel and 6061 Aluminum 

material properties of precious metals in relation to 6061 and 4140

Common Machining Applications of Precious Metals

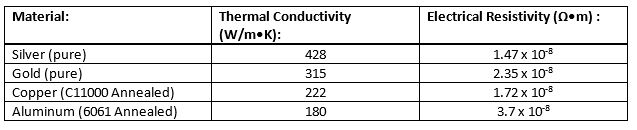
Silver and gold have particularly favorable thermal conductivity and electrical resistivity. These values are listed in Table 2, along with CC1000 (annealed copper) and annealed 6061 aluminum, for comparison purposes. Copper is generally used in electrical wiring because of its relatively low electrical resistivity, even though silver would make a better substitute. The obvious reason this isn’t the general convention is the cost of silver vs. copper. That being said, copper is generally plated with gold at electrical contact areas because it tends to oxide after extended use, which lowers its resistivity. As stated before, gold and the other precious metals are known to be resistant to oxidation. This corrosion resistance is the main reason that they are used in cathodic protection systems of the electronics industry.

Table 2: Thermal Conductivity and Electrical Resistivity of Ag, Au, Cu, and Al 

thermal conductivity of silver, gold, copper, and aluminum

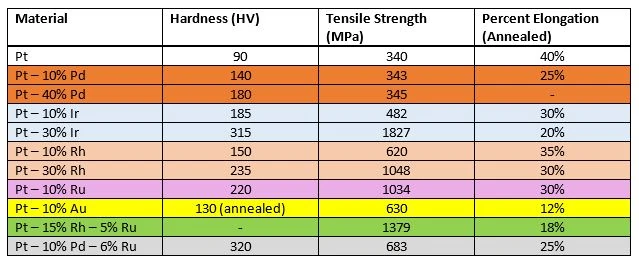
Platinum and its respective alloys offer the most amount of applications as it can achieve a number of different mechanical properties while still maintaining the benefits of a precious metal (high melting point, ductility, and oxidation resistance). Table 3 lists platinum and a number of other PGMs each with their own mechanical properties. The variance of these properties depends on the alloying element(s) being added to the platinum, the percentage of alloying metal, and whether or not the material has been cold-worked or annealed. Alloying can significantly increase the tensile strength and hardness of a material while decreasing its ductility at the same time. The ratio of this tensile strength/hardness increase to ductility decrease depends on the metal added as well as how much is added, as seen in Table 3. Generally this depends on the particle size of the element added as well as its natural crystalline structure. Ruthenium and Osmium have a specific crystal structure that has a significant hardening effect when added to platinum. Pt-Os alloys in particular are extremely hard and practically unworkable, which doesn’t yield many real-world applications. However, the addition of the other 4 PGMs to platinum allow for a range of mechanical properties with various usages.

Table 3: PGM material properties (Note: the hardness and tensile strength are cold worked values) 

pgm material properties

Platinum and its alloys are biocompatible, giving them the ability to be placed in the human body for long periods of time without causing adverse reactions or poisoning. Therefore, medical devices including heart muscle screw fixations, stents, and marker bands for angioplasty devices are made from platinum and its alloys. Gold and palladium are also commonly used in dental applications.

Pt-Ir alloys are noticeably harder and stronger than any of the other alloys and make excellent heads for spark plugs in the automobile industry. Rhodium is sometimes added to Pt-Ir alloys to make the material less springy (as they are used as medical spring wire) while also increasing its workability. Pt and Pt-Rh wire pairs are extremely effective at measuring temperatures and are therefore used in thermocouples.

Machining Precious Metals

The two parameters that have the most effect when machining are hardness and percent elongation. Hardness is well-known by machinists and engineers across the manufacturing industry as it indicates a material’s resistance to deformation or cutting. Percent elongation is a measurement used to quantify material ductility. It indicates to a designer the degree to which a structure will deform plastically (permanently) before fracture. For example, a ductile plastic such as ultrahigh molecular weight polyethylene (UHMWPE) has a percent elongation of 350-525%, while a more brittle material such as oil-quenched and tempered cast iron (grade 120-90-02) has a percent elongation of about 2%. Therefore, the greater the percent elongation, the greater the material’s “gumminess.” Gummy materials are prone to built-up edge and have a tendency to produce long stringy chips.
Tools for Precious Metals

Material ductility makes a sharp cutting tool essential for cutting precious metals. Variable Helix for Aluminum Alloy tools can be used for the softer materials such as pure gold, silver, and platinum.

variable helix square aluminum end mill from harvey tool

Figure 2: Variable Helix Square End Mill for Aluminum Alloys

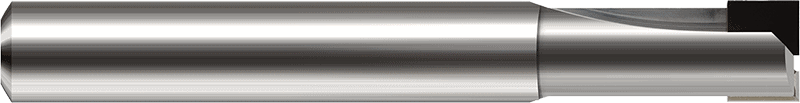
Higher hardness materials still require a sharp cutting edge. Therefore, one’s best option is to invest in a PCD Diamond tool. The PCD wafer has the ability to cut extremely hard materials while maintaining a sharp cutting edge for a relatively long period of time, compared to standard HSS and carbide cutting edges.

harvey tool pcd diamond square end mill

Figure 3: PCD Diamond Square End Mill

Speeds and Feeds charts:

speeds and feeds chart for precious metals

Figure 4: Speeds and Feeds for precious metals when using a Square Non-ferrous, 3x LOC

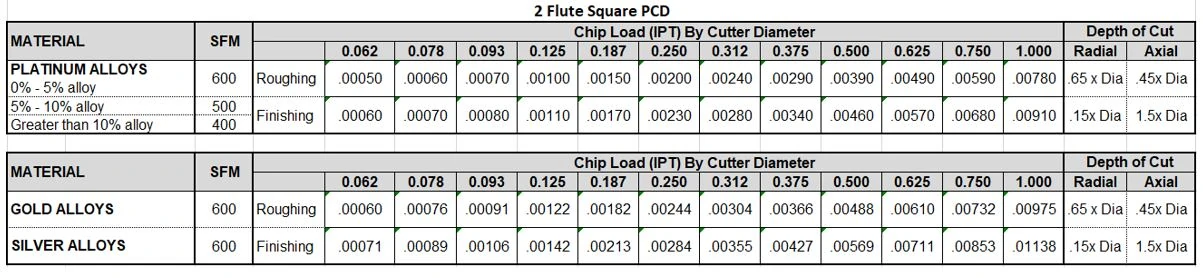
speeds and feeds chart for precious metals with a pcd end mill

Figure 5: Speeds and Feeds for precious metals when using a 2-Flute Square PCD end mill

https://www.harveyperformance.com/wp-content/uploads/2020/07/Machining-Precious-Metals.jpg 600 1599 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2019-07-01 12:58:512023-10-24 10:50:51Machining Precious Metals

How to Extend the Life of Your End Mill

December 5, 2018/2 Comments/in CNC Machining, High Efficiency Milling, How-To's, Machining Techniques, Milling, Quick Tips/by Harvey Performance Company

Breaking and damaging an end mill is oftentimes an avoidable mistake that can be extremely costly for a machine shop. To save time, money, and your end mill it is important to learn some simple tips and tricks to extend tool life.

Properly Prepare Before the Tool Selection Process

The first step of any machining job is selecting the correct end mill for your material and application. However, this doesn’t mean that there should not be an adequate amount of legwork done beforehand to ensure the right decision on a tool is being made. Harvey Tool, Helical Solutions, Titan USA, and Corehog have thousands of different tools for different operations – a vast selection which, if unprepared – can easily result in selecting a tool that’s not the best for your job. To start your preparation, answer the 5 Questions to Ask Before Selecting an End Mill to help you quickly narrow down your selection and better understand the perfect tool you require.

Understand Your Tooling Requirements

It’s important to understand not only what your tool needs, but also general best practices to avoid common machining mishaps. For instance, it is important to use a tool with a length of cut only as long as needed, as the longer a tools length of cut is, the greater the chance of deflection or tool bending, which can decrease its effective life.

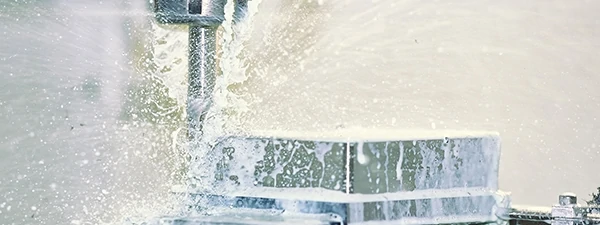
end mill being fed coolant cutting into a workpiece to extend tool life

Another factor to consider is the coating composition on a tool. Harvey Tool and Helical Solutions offer many varieties of tool coatings for different materials. Some coatings increase lubricity, slowing tool wear, while others increase the hardness and abrasion resistance of the tool. Not all coatings increase your tool’s life in every material, however. Be wary of coatings that don’t perform well in your part’s material – such as the use of AlTiN coating in Aluminum (Both coating and material are aluminum-based and have a high affinity for each other, which can cause built-up edge and result in chip evacuation problems).

Consider Variable Helix & Pitch Geometry

A feature on many of our high performance end mills is variable helix or variable pitch geometry, which have differently-spaced flutes. As the tool cuts, there are different time intervals between the cutting edges contacting the workpiece, rather than simultaneously on each rotation. The varying time intervals minimizes chatter by reducing harmonics, increasing tool life and producing better results.

Ensure an Effective Tool Holding Strategy

Another factor in prolonging tool life is proper tool holding. A poor tool holding strategy can cause runout, pullout, and scrapped parts. Generally, the most secure connection has more points of contact between the tool holder and tool shank. Hydraulic and Shrink Fit Tool Holders provide increased performance over other tightening methods.

three different end mills in tool holders

Helical also offers shank modifications to all stocked standards and special quotes, such as the ToughGRIP Shank, which provides added friction between the holder and the shank of the tool for a more secure grip; and the Haimer Safe-Lock™, which has grooves on the shank of the tool to help lock it into place in a tool holder.

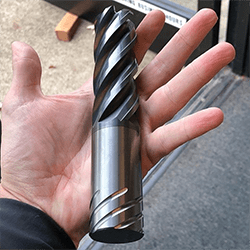
massive helical end mill in machinists hand

Trust Your Running Parameters, and their Source

After selecting the correct end mill for your job, the next step is to run the tool at the proper speeds and feeds.

Run at the Correct Speed

Understanding the ideal speed to run your machine is key to prolonging tool life. If you run your tool too fast, it can cause suboptimal chip size, ineffective chip evacuation, or even total tool failure. Adversely, running your tool too slowly can result in deflection, bad finish, or decreased metal removal rates.

Push at the Best Feed Rate

Another critical parameter of speeds and feeds is finding the best possible feed rate for your job, for sake of both tool life and achieving maximum shop efficiency. Pushing your tool too aggressively can result in breakage, but being too conservative can lead to recutting chips and excess heat generation, accelerating tool wear.

Use Parameters from Your Tooling Manufacturer

A manufacturer’s speeds and feeds calculations take into account every tool dimension, even those not called out in a catalog and readily available to machinists. Because of this, it’s best to rely on running parameters from tooling manufacturers. Harvey Tool offers speeds and feeds charts for every one of its more than 21,000 tools featured in its catalog, helping machinists to confidently run their tool the first time.

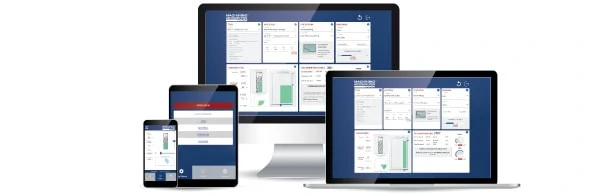
Harvey Performance Company offers the Machining Advisor Pro application, a free, cutting-edge resource that generates custom running parameters for optimized machining with all of Helical Solutions’ and Harvey Tool’s products.

machining advisor pro graphic for pc, laptops, and other devices

Opt for the Right Milling Strategy: Climb vs Conventional

There are two ways to cut material when milling: Climb Milling and Conventional Milling. In conventional milling, the cutter rotates against the feed. In this method, chips will start at theoretical zero and increase in size. Conventional milling is usually recommended for tools with higher toughness, or for breaking through case hardened materials.

In Climb Milling, the cutter rotates with the feed. Here, the chips start at maximum width and decrease, causing the heat generated to transfer into the chip instead of being left in the tool or work piece. Climb milling also produces a cleaner shear plane, causing less rubbing, decreasing heat, and improving tool life. When climb milling, chips will be removed behind the cutter, reducing your chances of recutting.

Utilize High Efficiency Milling

High Efficiency Milling (HEM), is a roughing technique that uses the theory of chip thinning by applying a smaller radial depth of cut (RDOC) and a larger axial depth of cut (ADOC). The parameters for HEM are similar to that of finishing, but with increased speeds and feeds, allowing for higher material removal rates (MRR). HEM utilizes the full length of cut instead of just a portion of the cutter, allowing heat to be distributed across the cutting edge, maximizing tool life and productivity. This reduces the possibility of accelerated tool wear and breakage.

Decide On Coolant Usage & Delivery

Coolant can be an extremely effective way to protect your tool from premature wear and possible tool breakage. There are many different types of coolant and methods of delivery to your tool. Coolant can come in the form of compressed air, water-based, straight oil-based, soluble oil-based, synthetic or semi-synthetic. It can be delivered as mist, flood, high pressure or minimum quantity lubricant.

Appropriate coolant type and delivery vary depending on your application and tool. For example, using a high pressure coolant with miniature tooling can lead to tool breakage due to the fragile nature of extremely small tools. In applications of materials that are soft and gummy, flood coolant washes away the long stringy chips to help avoid recutting and built-up edge, preventing extra tool wear.

Extend Your Tool’s Life

The ability to maximize tool life saves you time, money and headaches. To get the best possible outcome from your tool, you first need to be sure you’re using the best tool for your job. Once you find your tool, ensure that your speeds and feeds are accurate and are from your tooling manufacturer. Nobody knows the tools better than they do. Finally, think about how to run your tool: the rotation of your cutter, whether utilizing an HEM approach is best, and how to introduce coolant to your job.

https://www.harveyperformance.com/wp-content/uploads/2018/12/Featured-Image-Life-of-End-Mill-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-12-05 11:28:212023-10-24 09:56:33How to Extend the Life of Your End Mill

Effective Ways to Reduce Heat Generation

October 25, 2018/1 Comment/in High Efficiency Milling, How-To's, Machining Techniques, Quick Tips/by Harvey Performance Company

Any cutting tool application will generate heat, but knowing how to counteract it will improve the life of your tool. Heat can be good and doesn’t need to totally be avoided, but controlling heat will help prolong your tool life. Sometimes, an overheating tool or workpiece is easy to spot due to smoke or deformation. Other times, the signs are not as obvious. Taking every precaution possible to redirect heat will prolong your tool’s usable life, avoid scrapped parts, and will result in significant cost savings.

Reduce Heat Generation with HEM Tool Paths

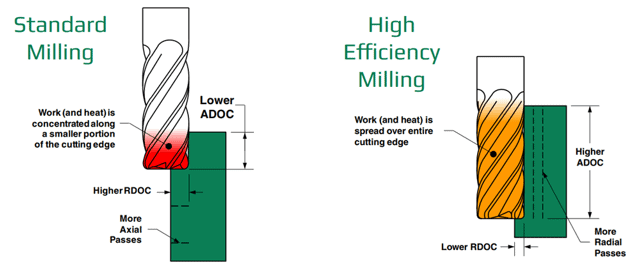
High Efficiency Milling (HEM), is one way a machinist should explore to manage heat generation during machining. HEM is a roughing technique that uses the theory of chip thinning by applying a smaller radial depth of cut (RDOC) and a larger axial depth of cut (ADOC). HEM uses RDOC and ADOC similar to finishing operations but increases speeds and feeds, resulting in greater material removal rates (MRR). This technique is usually used for removing large amounts of material in roughing and pocketing applications. HEM utilizes the full length of cut and more effectively uses the full potential of the tool, optimizing tool life and productivity. You will need to take more radial passes on your workpiece, but using HEM will evenly spread heat across the whole cutting edge of your tool, instead of building heat along one small portion, reducing the possibility of tool failure and breakage.

heat generation in standard versus hem milling and their associated depths of cut

Chip Thinning Awareness

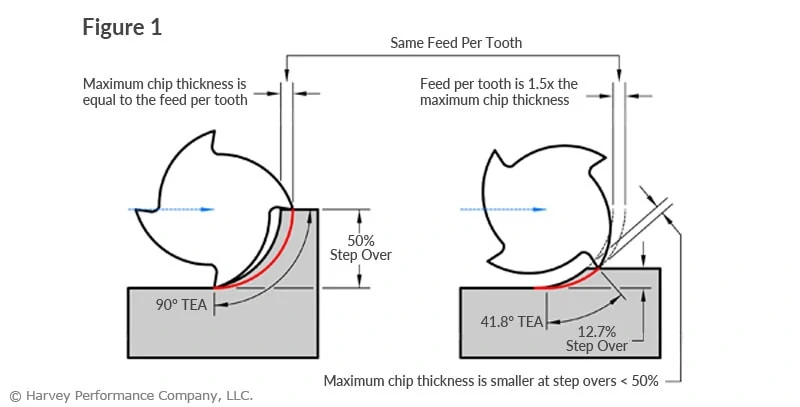
Chip thinning occurs when tool paths include varying radial depths of cut, and relates to chip thickness and feed per tooth. HEM is based off of the principal of chip thinning. However, if not properly executed, chip thinning can cause a lot of heat generation. When performing HEM, you effectively reduce your stepover and increase your speeds and feeds to run your machine at high rates. But if your machine isn’t capable of running high enough speeds and feeds, or you do not adjust accordingly to your reduced stepover, trouble will occur in the form of rubbing between the material and tool. Rubbing creates friction and mass amounts of heat which can cause your material to deform and your tool to overheat. Chip thinning can be good when used correctly in HEM, but if you fall below the line of reduced stepover without higher speeds and feeds, you will cause rubbing and tool failure. Because of this, it’s always important to be aware of your chips during machining. Understanding chip thinning is paramount to success in in machining.

infographic showcasing chip thinning in relation to step over

Consider Climb Milling

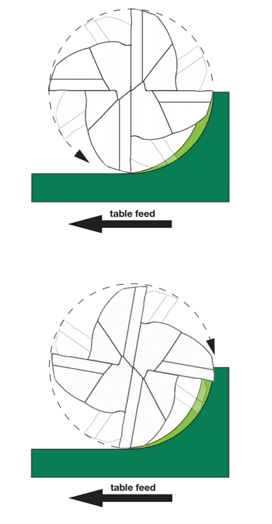
There are two ways to cut materials when milling: conventional milling and climb milling. The difference between the two is the relationship of the rotation of the cutter to the direction of feed. In climb milling, the cutter rotates with the feed, as opposed to conventional milling where the cutter rotates against the feed.

When conventional milling, chips start at theoretical zero and increase in size, causing rubbing and potentially work hardening. For this reason, it’s usually recommended for tools with higher toughness or for breaking through case hardened materials.

In climb milling, the chip starts at maximum width and decreases, causing the heat generated to transfer into the chip instead of the tool or workpiece. When going from max width to theoretical zero, heat will be transferred to the chip and pushed away from the workpiece, reducing the possibility of damage to the workpiece. Climb milling also produces a cleaner shear plane which will cause less tool rubbing, decreasing heat and improving tool life. When climb milling, chips are removed behind the cutter, reducing your chances of re-cutting. climb milling effectively reduces heat generated to the tool and workpiece by transferring heat into the chip, reducing rubbing and by reducing your chances of re-cutting chips.

infographic showing climb versus conventional milling in feed path and end mill direction

Utilize Proper Coolant Methods

If used properly, coolant can be an extremely effective way to keep your tool from excessive heat generation. There are many different types of coolant and different ways coolant can be delivered to your tool. Coolant can be compressed air, water-based, straight oil-based, soluble oil-based, synthetic or semi-synthetic. It can be delivered as mist, flood, high pressure or minimum quantity lubricant.

Different applications and tools require different types and delivery of coolant, as using the wrong delivery or type could lead to part or tool damage. For instance, using high pressure coolant with miniature tooling could lead to tool breakage. In materials where chip evacuation is a major pain point such as aluminum, coolant is often used to flush chips away from the workpiece, rather than for heat moderation. When cutting material that produces long, stringy chips without coolant, you run the risk of creating built-up edge from the chips evacuating improperly. Using coolant will allow those chips to slide out of your toolpath easily, avoiding the chance of re-cutting and causing tool failure. In materials like titanium that don’t transfer heat well, proper coolant usage can prevent the material from overheating. With certain materials, however, thermal shock becomes an issue. This is when coolant is delivered to a very hot material and decreases its temperature rapidly, impacting the material’s properties. Coolant can be expensive and wasteful if not necessary for the application, so it’s important to always make sure you know the proper ways to use coolant before starting a job.

Importance of Controlling Heat Generation

Heat can be a tool’s worst nightmare if you do not know how to control it. High efficiency milling will distribute heat throughout the whole tool instead of one small portion, making it less likely for your tool to overheat and fail. By keeping RDOC constant throughout your toolpath, you will decrease the chances of rubbing, a common cause of heat generation. Climb milling is the most effective way to transfer heat into the chip, as it will reduce rubbing and lessen the chance of re-chipping. This will effectively prolong tool life. Coolant is another method for keeping temperatures moderated, but should be used with caution as the type of coolant delivery and certain material properties can impact its effectiveness.

https://www.harveyperformance.com/wp-content/uploads/2018/10/Feature-Image-Reduce-Heat-Generation-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-10-25 11:26:402025-02-12 09:59:35Effective Ways to Reduce Heat Generation

How to Maximize High Balance End Mills

August 20, 2018/1 Comment/in CNC Machining, Helical Solutions, High Efficiency Milling, How-To's, Machining Techniques, Tool Selection/by Harvey Performance Company

High speed machining is becoming increasingly widespread in machine shops all over the world due to the proven benefits of greater efficiency and productivity through increased spindle speeds and metal removal rates.  However, at such high spindle speeds, otherwise negligible errors and imperfections can cause negative effects such as reduced tool life, poor surface finish, and wear on the machine itself. Many of these negative effects stem from an increase in total centrifugal forces leading to vibration, commonly referred to in the industry as chatter. A key contributor to vibrations and one of the more controllable factors, is tool unbalance.

Why Balance is Critical to Machining

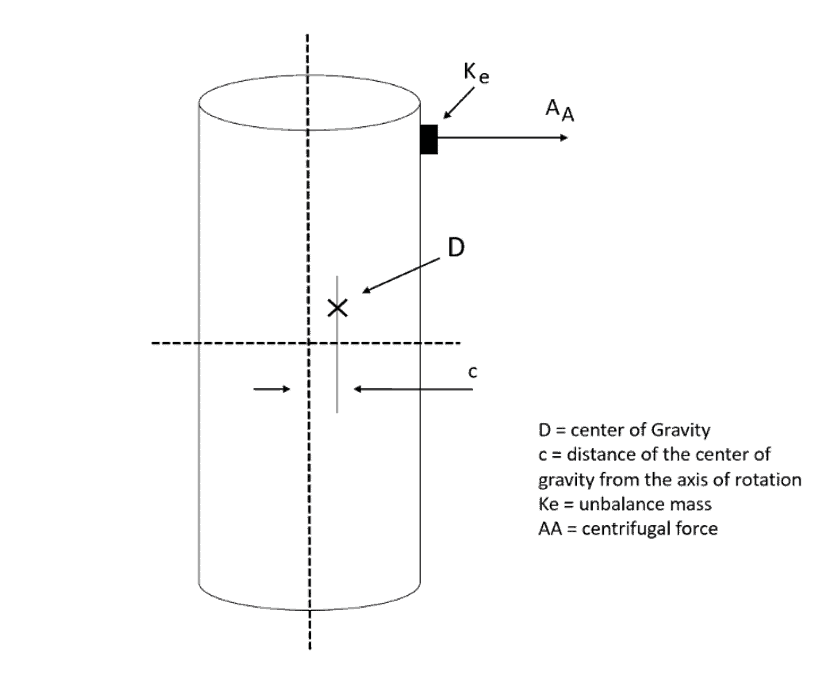
Unbalance is the extent to which the tool’s center of mass diverges from its axis of rotation.  Small levels of unbalance may be indistinguishable at lower RPMs, but as centrifugal force increases, small variations in the tool’s center of mass can cause substantial detrimental effects on its performance. High Balance End Mills are often used to help solve the problem of vibrations at the increased spindle speeds. Balancing is used to make compensation for the intrinsic unsymmetrical distribution of mass, which is typically completed by removing mass of a calculated amount and orientation.

infographic showcasing all aspects axii for high balance machining

Image Source: Haimer; Fundamentals of Balancing

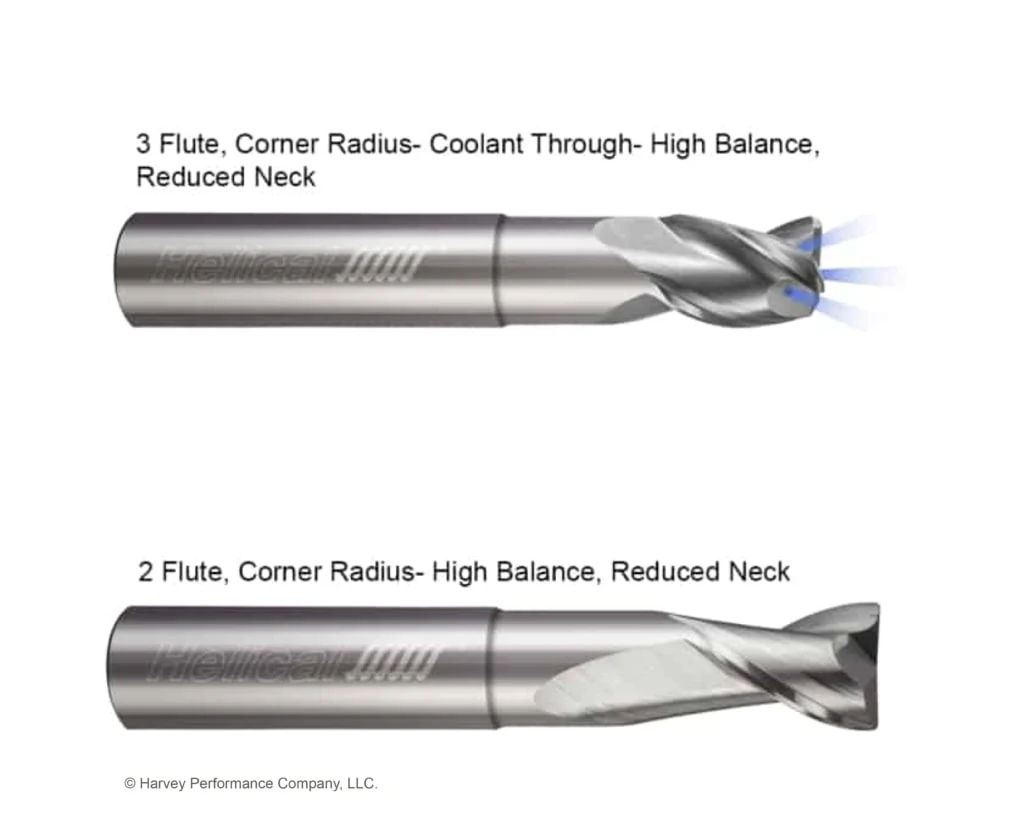
Helical Solutions offers High Balance End Mills in both 2 and 3 flute options (see Figure 2), square and corner radius, along with coolant-through on the 3 fluted tools. These end mills are balanced at the industry standard of G2.5 at 33,000 RPM: G stands for the potential damage due to unbalance, which can be expressed as “Balancing Quality Grade” or G and 2.5 is the vibration velocity in MM per second. These tools are designed specifically to increase performance in highly balanced machining centers that are capable of elevated RPMs and feed rates. With high balance tooling, improved surface finishes are also achieved due to reduced vibrations during the machining process. Additionally, these end mills have been designed around current high-end tool holding, and come in a variety of neck lengths at specific overall lengths. These dimensional combinations result in maximum rigidity and reduced excess stick out, allowing for optimal performance and the ability to push the tools to the limit.
cnc high balance end mills in both 2 and 3 flute designs

High Balanced Tooling Cost Benefits

Machinists who choose to use High Balance End Mills will see certain benefits at the spindle, but also in their wallets. Cost benefits of opting to run this type of tool include:

  • Longer tool life
  • Longer spindle lifetime
  • Reduced machine down time

Utilizing Tap Testers

What Tap Testers Do

Vibrations are your applications worst enemy, especially at elevated RPMs and feed rates. Using resources such as a Tap Tester can help decrease vibrations and allow you to get the most out of your High Balance End Mills by generating cutting performance predictions and chatter limits.

How Tap Testing Works

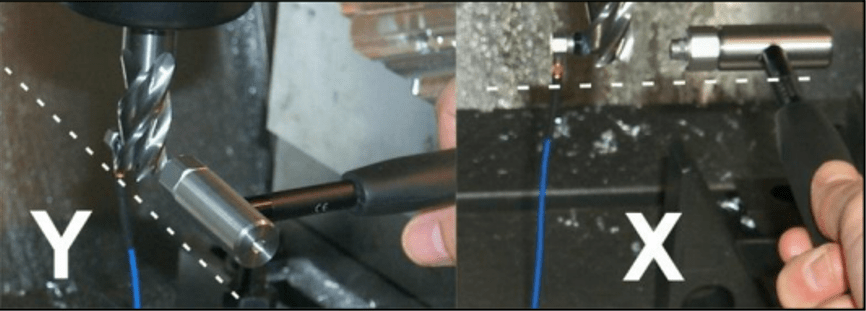
how to properly tap test a cnc tool

Image Source: Manufacturing Automation Laboratories Inc.

Tap Testing generates cutting performance predictions and chatter limits. In a tap test, the machine-tool structure is “excited,” or tested, by being hit with an impulse hammer. In milling, the machine-tool structure is usually flexible in all three directions: X, Y, and Z, but in milling applications where High Balance Tooling is used, the flexibility is commonly only considered in two planes – the X and Y directions. By hitting the X and Y directions with the impulse hammer, the impact will excite the structure over a certain frequency range that is dependent on the hammer’s size, the type of tool being used, and the structure itself. The frequencies generated from the initial hit will produce enough information that both the impact force measurement and the displacement/accelerometer measurement are available. Combining these two measurements will result in the Frequency Response Function, which is a plot of the dynamic stiffness of the structure in frequencies.

After the information from the Tap Test is gathered, it will then process the information into useful cutting parameters for all spindles speeds such as cut depths, speed rates, and feed rates. In knowing the optimum running parameters, vibrations can be minimized and the tool can be utilized to its full potential.

High Balanced Tooling Summarized

Keeping vibrations at bay during the machining process is extremely important to machining success. Because one cause of vibration is tool unbalance, utilizing a balanced tool will result in a smoother job, a cleaner final product, and a longer life of both the tool and spindle. Machinists who choose to use High Balance Tooling can utilize a Tap Tester, or a method for generating the perfect running parameters for your tool and machine setup to ensure that machining vibration is as minimal as possible.

https://www.harveyperformance.com/wp-content/uploads/2018/08/Featured-Image-Maximize-High-Balance-End-Mills-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-08-20 14:08:412023-10-24 10:46:29How to Maximize High Balance End Mills

Best Practices of Tolerance Stacking

August 10, 2018/10 Comments/in CNC Machining, High Efficiency Milling, How-To's, Machining 101, Machining Techniques/by Robert Keever

Tolerance stacking, also known as tolerance stack-up, is a critical step in manufacturing that determines how individual part tolerances combine to affect overall accuracy. In precision machining, this analysis is crucial for ensuring tools maintain their functional requirements in the cut while still remaining cost-effective to produce. In essence, tolerances are combined or “stacked-up” as a cumulative equation in machining to ensure feasibility.

Understanding tolerance stacking is crucial for three key reasons: preventing manufacturing failures, optimizing production costs, and ensuring consistent quality across high-volume production runs. This post provides comprehensive analysis methods, practical examples, and best practices for managing tolerances.

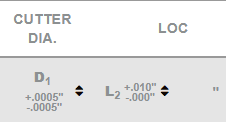
After a tolerance is identified on the dimension of a part, it is important to test whether that tolerance would work with the chosen tool’s tolerances: either the upper end or lower end. These tool tolerances are often called out within tool dimension charts. An example can be seen on a Harvey Tool Miniature Square End Mill where the tolerance of +.00005″ and -.0005″ is shown at the Cutter Diameter dimension.

Chart of end mill cutter diameter with tolerance callouts

A part or assembly can be subject to inaccuracies when its tolerances are stacked up incorrectly. Therefore, proper manufacturing tolerance calculation is paramount in winning at the spindle. Starting with a tolerance stack-up analysis prior to machining ensures parts are achievable with current setups, reducing scrapped parts. Continue reading to explore the importance of proper tolerance stacking, common pitfalls, and equations to ensure success.

Why Tolerance Analysis Matters in Manufacturing

Tolerances directly influence the cost and performance of a product. The tighter the tolerance, the more precise a finished part becomes. Tighter tolerances also make a machined part more difficult to manufacture and therefore often more expensive. With this in mind, it is important to find a balance between manufacturability of the part, its functionality, and its cost.

Tips for Successful Tolerance Stacking

Avoid Using Tolerances That are Unnecessarily Small

As stated above, tighter tolerances lead to a higher manufacturing cost as the part is more difficult to make. This higher cost is often due to the increased amount of scrapped parts that can occur when dimensions are found to be out of tolerance. The cost of high quality tool holders and tooling with tighter tolerances can also be an added expense.

Additionally, unnecessarily small tolerances will lead to longer manufacturing times, as more work goes in to ensure that the part meets strict criteria during machining, and after machining in the inspection process.

Be Careful Not to Over Dimension a Part

When an upper and lower tolerance is labeled on every feature of a part, over-dimensioning can become a problem.

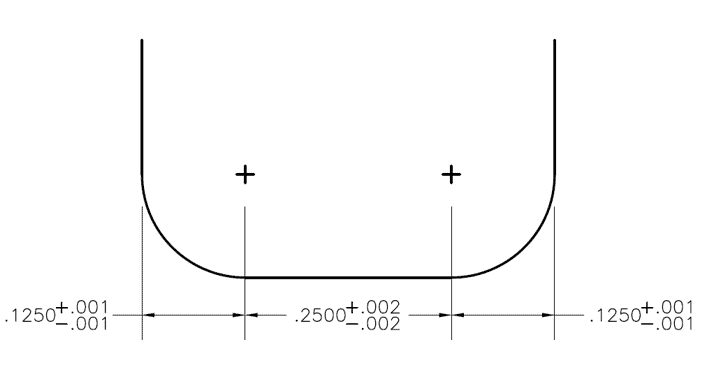
For example, a corner radius end mill with a right and left corner radii might have a tolerance of +/- .001”, and the flat between them has a .002” tolerance. In this case, the tolerance window for the cutter diameter would be +/- .004”, but is oftentimes miscalculated during part dimensioning. Further, placing a tolerance on this callout would cause it to be over dimensioned, and thus the reference dimension “REF” must be left to take the tolerance’s place.

close up of a shaped of slot from a corner radius end mill and its tolerances
Figure 1: Shape of slot created by a corner radius end mill

Utilize Statistical Tolerance Analysis:

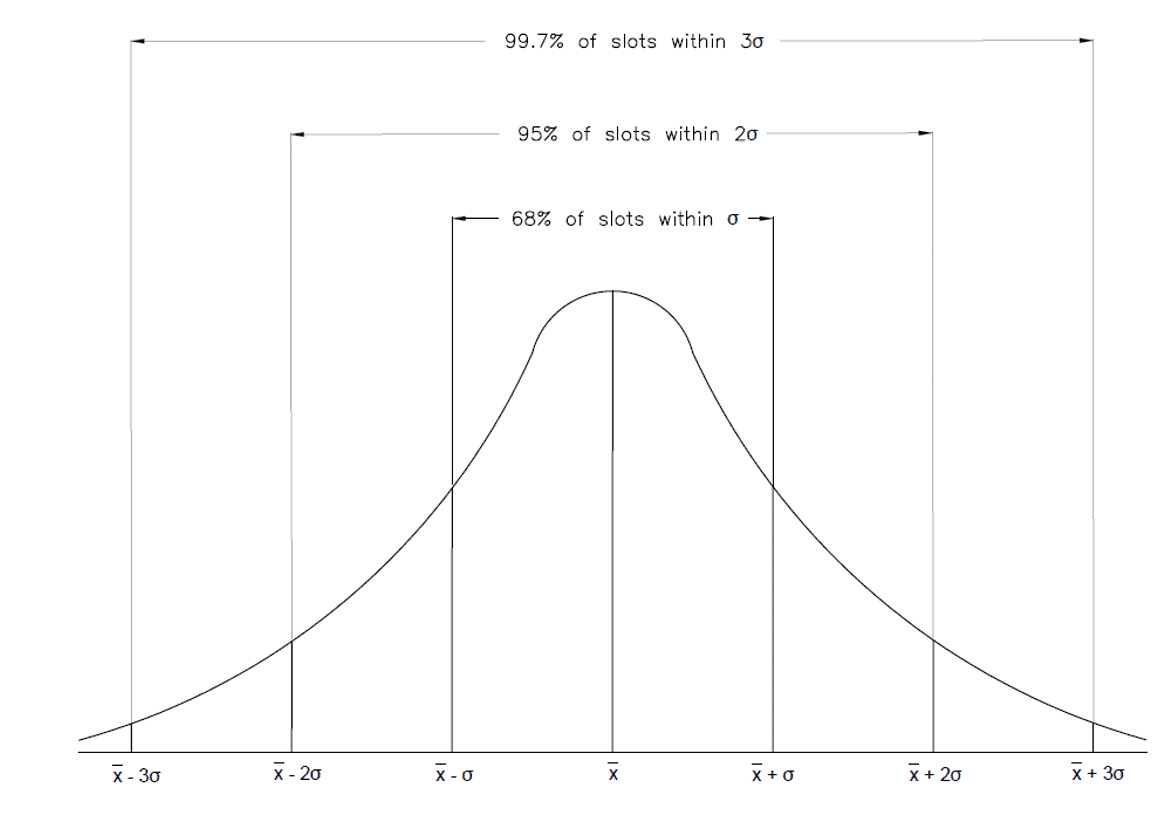
Statistical analysis looks at the likelihood that all three tolerances would be below or above the dimensioned slot width, based on a standard deviation. This probability is represented by a normal probability density function, which can be seen in figure 2 below. By combining all the probabilities of the different parts and dimensions in a design, we can determine the probability that a part will have a problem, or fail altogether, based on the dimensions and tolerance of the parts. Generally this method of analysis is only used for assemblies with four or more tolerances.

stacking tolerances
                                                               Figure 2: Tolerance Stacking: Normal distribution

Before starting a statistical tolerance analysis, you must calculate or choose a tolerance distribution factor. The standard distribution is 3 . This means that most of the data (or in this case tolerances) will be within 3 standard deviations of the mean. The standard deviations of all the tolerances must be divided by this tolerance distribution factor to normalize them from a distribution of 3  to a distribution of 1 . Once this has been done, the root sum squared can be taken to find the standard deviation of the assembly.

Think of it like a cup of coffee being made with 3 different sized beans. In order to make a delicious cup of joe, you must first grind down all of the beans to the same size so they can be added to the coffee filter. In this case, the beans are the standard deviations, the grinder is the tolerance distribution factor, and the coffee filter is the root sum squared equation. This is necessary because some tolerances may have different distribution factors based on the tightness of the tolerance range.

The statistical analysis method is used if there is a requirement that the slot must be .500” wide with a +/- .003” tolerance, but there is no need for the radii (.125”) and the flat (.250”) to be exact as long as they fit within the slot. In this example, we have 3 bilateral tolerances with their standard deviations already available. Since they are bilateral, the standard deviation from the mean would simply be whatever the + or – tolerance value is. For the outside radii, this would be .001” and for the middle flat region this would be .002”.

For this example, let’s find the standard deviation (σ) of each section using equation 1. In this equation represents the standard deviation.

standard deviation

The standard assumption is that a part tolerance represents a +/- 3  normal distribution. Therefore, the distribution factor will be 3. Using equation 1 on the left section of figure 1, we find that its corrected standard deviation equates to:

tolerance stacking

This is then repeated for the middle and right sections:

standard deviation

After arriving at these standard deviations, we input the results into equation 2 to find the standard deviation of the tolerance zone. Equation 2 is known as the root sum squared equation.

root sum squared equation for tolerance stack up analysis

At this point, it means that 68% of the slots will be within a +/- .0008” tolerance. Multiplying this tolerance by 2 will result in a 95% confidence window, where multiplying it by 3 will result in a 99% confidence window.

68% of the slots will be within +/- .0008”

95% of the slots will be within +/- .0016”

99% of the slots will be within +/- .0024”

These confidence windows are standard for a normal distributed set of data points. A standard normal distribution can be seen in Figure 2 above.

Statistical tolerance analysis should only be used for assemblies with greater than 4 toleranced parts. A lot of factors were unaccounted for in this simple analysis. This example was for 3 bilateral dimensions whose tolerances were representative of their standard deviations from their means. In standard statistical tolerance analysis, other variables come into play such as angles, runout, and parallelism, which require correction factors.

Did You Know that Harvey Performance Company Brands Partner With the Industry’s Premier Cam Software Providers to Deliver Tooling Libraries?

Click Here to Learn More

Use Worst Case Analysis:

Worst case analysis is the practice of adding up all the tolerances of a part to find the total part tolerance. When performing this type of analysis, each tolerance is set to its largest or smallest limit in its respective range. This total tolerance can then be compared to the performance limits of the part to make sure the assembly is designed properly. This is typically used for only 1 dimension (Only 1 plane, therefore no angles involved) and for assemblies with a small number of parts.

Worst case analysis can also be used when choosing the appropriate cutting tool for your job, as the tool’s tolerance can be added to the parts tolerance for a worst case scenario. Once this scenario is identified, the machinist or engineer can make the appropriate adjustments to keep the part within the dimensions specified on the print.

It should be noted that the worst case scenario rarely ever occurs in actual production. While these analyses can be expensive for manufacturing, it provides peace of mind to machinists by guaranteeing that all assemblies will function properly. Often this method requires tight tolerances because the total stack up at maximum conditions is the primary feature used in design. Tighter tolerances intensify manufacturing costs due to the increased amount of scrapping, production time for inspection, and cost of tooling used on these parts.

Example of worst case scenario in context to Figure 1:

Find the lower specification limit.

For the left corner radius

.125” – .001” = .124”

For the flat section

.250” – .002” = .248”

For the right corner radius

.125” – .001” = .124”

Add all of these together to the lower specification limit:

.124” + .248” + .124” = .496”

Find the upper specification limit:

For the left corner radius

.125” + .001” = .126”

For the flat section

.250” + .002” = .252”

For the right corner radius

.125” + .001” = .126”

Add all of these together to the lower specification limit:

.126” + .252” + .126” = .504”

Subtract the two and divide this answer by two to get the worst case tolerance:

(Upper Limit – Lower Limit)/2 = .004”

Therefore the worst case scenario of this slot is .500” +/- .004”.

https://www.harveyperformance.com/wp-content/uploads/2018/08/Featured-Image-Tolerance-Stacking-IMG.jpg 525 1400 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2018-08-10 08:35:112024-10-28 16:20:05Best Practices of Tolerance Stacking

Tool Deflection & Its Remedies

May 3, 2018/6 Comments/in CNC Machining, How-To's, Machining 101, Troubleshooting Tips/by Jacob Concepcion

What is Tool Deflection?

Every machinist must be aware of tool deflection, as too much deflection can lead to catastrophic failure in the tool or workpiece. Deflection is the displacement of an object under a load causing curvature and/or fracture.

For Example: When looking at a diving board at rest without the pressure of a person’s weight upon it, the board is straight. But as the diver progresses down further to the end of the board, it bends further. Deflection in tooling can be thought of in a similar way.

Signs of Tool Deflection

  • Shortened tool life and/or tool breakage
  • Subpar surface finish
  • Part dimensional inaccuracies

Tool Deflection Remedies

Minimize Overhang

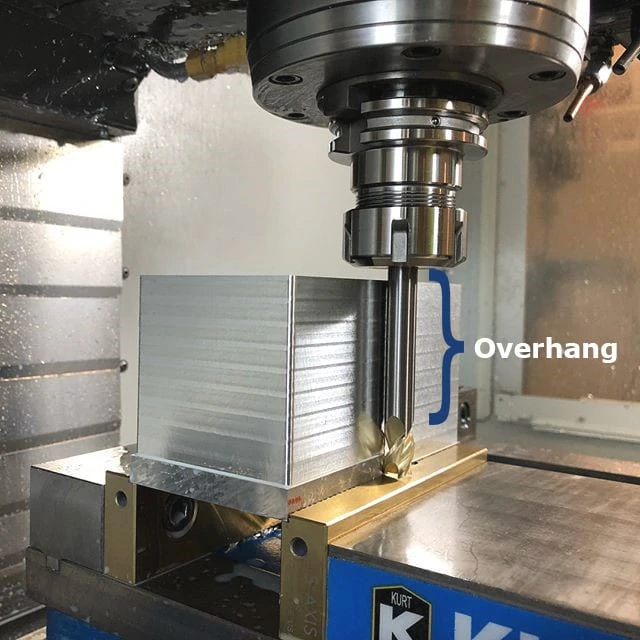
Overhang refers to the distance a tool is sticking out of the tool holder. Simply, as overhang increases, the tool’s likelihood of deflection increases. The larger distance a tool hangs out of the holder, the less shank there is to grip, and depending on the shank length, this could lead to harmonics in the tool that can cause fracture. Simply put, For optimal working conditions, minimize overhang by chucking the tool as much as possible.

extended reach tool in tool holder with overhang depth called out
Image Source: @NuevaPrecision

Long Flute vs. Long Reach

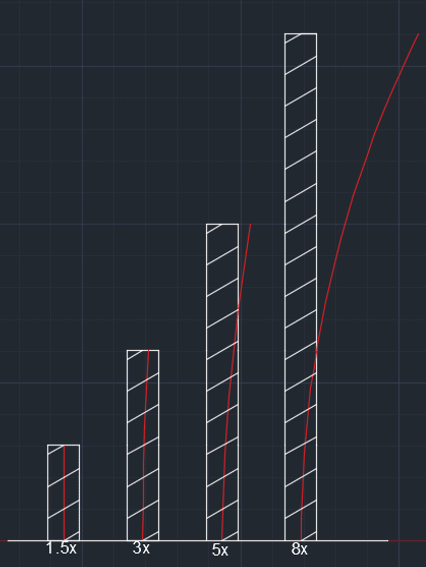
Another way to minimize deflection is having a full grasp on the differences between a long flute and a long reach tool. The reason for such a difference in rigidity between the two is the core diameter of the tool. The more material, the more rigid the tool; the shorter the length of flute, the more rigid the tool and the longer the tool life. While each tooling option has its benefits and necessary uses, using the right option for an operation is important.

The below charts illustrate the relationship between force on the tip and length of flute showing how much the tool will deflect if only the tip is engaged while cutting. One of the key ways to get the longest life out of your tool is by increasing rigidity by selecting the smallest reach and length of cut on the largest diameter tool.

tool deflection in relation to length of tool

tool deflection graph

Click Here to Learn More About Proper Tool Holding and Runout

When to Opt for a Long Reach Tool

Reached tools are typically used to remove material where there is a gap that the shank would not fit in, but a noncutting extension of the cutter diameter would. This length of reach behind the cutting edge is also slightly reduced from the cutter diameter to prevent heeling (rubbing of noncutting surface against the part). Reached tools are one of the best tools to add to a tool crib because of their versatility and tool life.

long reach ball end mill
Long Reach Tool: Variable Helix End Mills for Exotic Alloys – Ball – Long Reach, Stub Flute

When to Opt for a Long Flute Tool

Long Flute tools have longer lengths of cut and are typically used for either maintaining a seamless wall on the side of a part, or within a slot for finishing applications. The core diameter is the same size throughout the cutting length, leading to more potential for deflection within a part. This possibly can lead to a tapered edge if too little of the cutting edge is engaged with a high feed rate. When cutting in deep slots, these tools are very effective. When using HEM, they are also very beneficial due to their chip evacuation capabilities that reached tools do not have.

long flute end milling tool
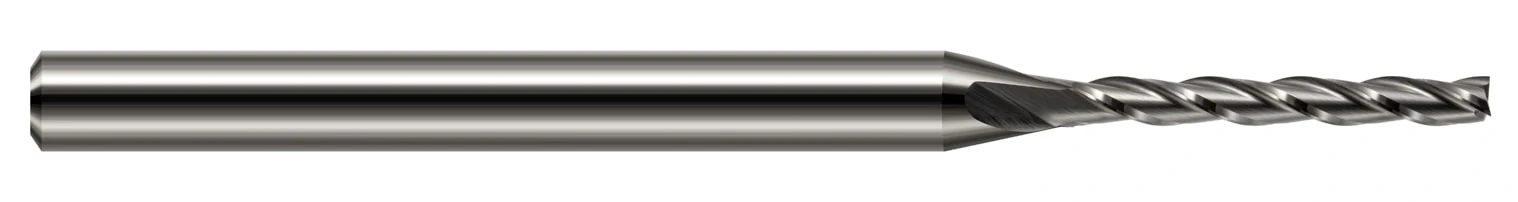
Long Flute Tool: Miniature End Mills – Square Long Flute

Deflection & Tool Core Strength

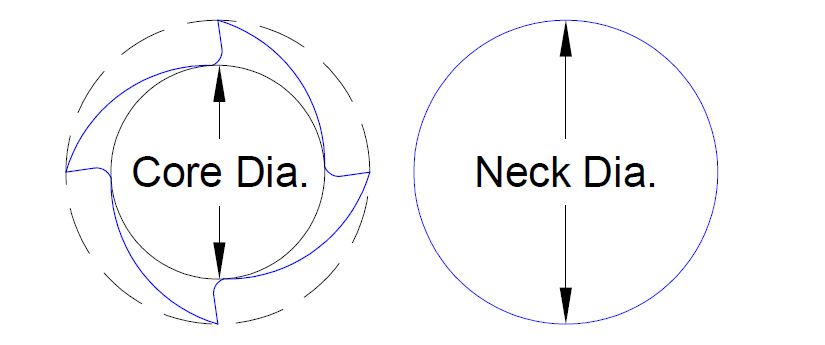
Diameter is an important factor when calculating deflection. Machinists oftentimes use the cutter diameter in the calculation of long flute tools, when in actuality the core diameter (shown below) is the necessary dimension. This is because the fluted portion of a tool has an absence of material in the flute valleys. For a reached tool, the core diameter would be used in the calculation until its reached portion, at which point it transitions to the neck diameter. When changing these values, it can lower deflection to a point where it is not noticeable for the reached tool but could affect critical dimensions in a long flute tool.

core diameter vs neck diameter infographic

Deflection Summarized

Tool deflection can cause damage to your tool and scrap your part if not properly accounted for prior to beginning a job. Be sure to minimize the distance from the tool holder to the tip of the tool to keep deflection to a minimum. For more information on ways to reduce tool deflection in your machining, view Diving into Depth of Cut.

https://www.harveyperformance.com/wp-content/uploads/2018/05/Featured-Image-Tool-Deflection-IMG.jpg 525 1400 Jacob Concepcion http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Jacob Concepcion2018-05-03 09:42:392024-03-05 16:25:18Tool Deflection & Its Remedies

Choosing the Right Pecking Cycle Approach

April 19, 2018/1 Comment/in CNC Machining, Holemaking, How-To's, Machining 101/by Harvey Performance Company

Utilizing a proper pecking cycle strategy when drilling is important to both the life of your tool and its performance in your part. Recommended cycles vary depending on the drill being used, the material you’re machining, and your desired final product.

Start to Boost Your Accuracy with Harvey Tool’s Drilling Guidebook.

What are Pecking Cycles?

Rather than drill to full drill depth in one single plunge, pecking cycles involve several passes – a little at a time. Peck drilling aids the chip evacuation process, helps support tool accuracy while minimizing walking, prevents chip packing and breakage, and results in a better all around final part.

Recommended Pecking Cycles / Steps

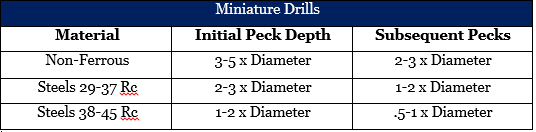
Miniature Drills

miniature drill pecking cycles

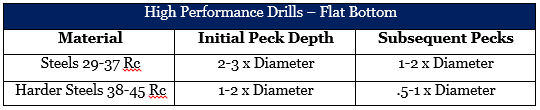
High Performance Drills – Flat Bottom

high performance drill pecking cycles

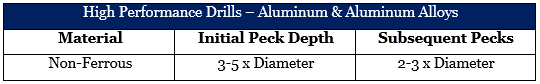
High Performance Drills – Aluminum & Aluminum Alloys

aluminum pecking cycles

Note: For hole depths 12x or greater, a pilot hole of up to 1.5X Diameter is recommended.

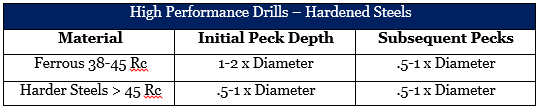
High Performance Drills – Hardened Steels

hardened steels chart
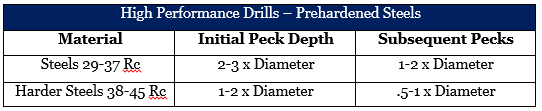
High Performance Drills – Prehardened Steels

prehardened steels chart

Key Pecking Cycle Takeaways

From the above tables, it’s easy to identify how recommended peck drilling cycles change based on the properties of the material being machined. Unsurprisingly, the harder the material is, the shorter the recommended pecking depths are. As always, miniature drills with a diameter of less than .010″ are extremely fragile and require special precautions to avoid immediate failure. For help with your specific job, contact the Harvey Tool Technical Team at 800-645-5609 or [email protected]

https://www.harveyperformance.com/wp-content/uploads/2018/04/Featured-Image-Pecking-Cycle-IMG-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-04-19 07:44:542022-01-17 10:16:34Choosing the Right Pecking Cycle Approach

3 Steps to Shutting up Tool Chatter

November 8, 2017/26 Comments/in CNC Machining, How-To's, Quick Tips, Troubleshooting Tips/by Harvey Performance Company

What is Chatter in Machining?

Cutting tools undergo a great deal of force during the machining process, which cause vibrations – also known as chatter or harmonics. Avoiding these vibrations entirely is not possible, though minimizing them is pivotal for machining success. Vibrations become damaging when proper machining steps are not followed. This leads to strong, part-ruining chatter. In these situations, parts have what is known as “chatter marks,” or clear vibration marks along the surface of a part. Tools can experience an increased rate of wear due to excess vibration.

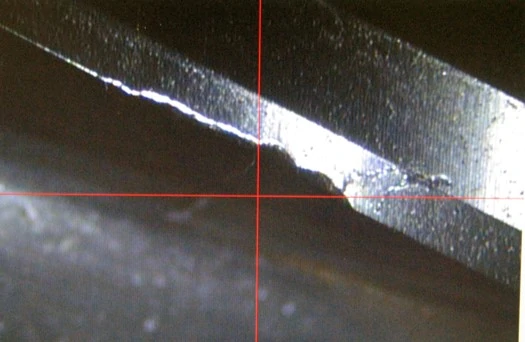
zoomed in image of excessive tool wear from cnc machining
An example of a tool with excessive wear.

Shut Up Tool Chatter With Harvey Tool’s Material Specific Tooling

How to Reduce Chatter in Machining

Select the Right Tool for Your Job

It seems elementary, but selecting the best tool for your application can be confusing. With so many different geometric styles for tooling – overall length, length of cut, reach, number of flutes – it can sometimes be difficult to narrow down one specific tool for your job. Oftentimes, machinists opt for general purpose tooling that can perform a variety of operations, overlooking the option that’s optimized for one material and job.

Use Material Specific Tooling

Opting for Material Specific Tooling is helpful, as each material has different needs. For example, steels are machined differently than aluminum materials. Everything from the chip size, to chip evacuation, is different. Variable Helix or Variable Pitch designs help to minimize chatter by reducing harmonics, which are caused by the cutting edge having repeated contact with the workpiece. In order to reduce harmonics, the time intervals between flute contact with the workpiece are varied.

helical reduced neck tool in cnc machine next to part

Consider Tool Length

Overall length is another important factor to consider when deciding on a tool for your job. The more overhang, or length the tool hangs from the spindle, the less secure the spindle-to-tool connection is, and the more vibration. Ensuring that your tool is only as long as needed for your operation is important to minimizing chatter and harmonics. If machining deep within a part, opt for reached tooling or an extended reach tool holder to help solidify the connection.

Ensure a Secure Connection

Tool Holder & Shank Relationship

When it comes to secure tool holding approaches, both the tool shank and the collet are important. A loose tool, unsurprisingly, has more ability to move, or vibrate, during machining. With this in mind, Helical offers Shank Configurations to help the connection including the ToughGRIP Shank, which replaces a smooth, mirror-like surface with a rougher, coarser one for increased friction. Helical is also a licensee of the HAIMER Safe-Lock™, added grooves on the shank of a tool that work opposite of the spindle rotation, securely fastening the tool in place.

image of three end mills secured in their respective tool holders

Choosing Collet Types

Machinists must also know the different types of collets available to them to identify if a better solution might be necessary. For example, Hydraulic Tool Holders or Shrink Fit Tool Holders promote a stronger connection than a Mechanical Spindle Tightening method.

For more information, see Key Tool Holding Considerations

harvey tool material specific tooling ad with 4 end mills pictured side-by-side

Selecting a Chatter Minimizing Strategy

How a tool is run can mean the difference between stellar job results and a ruined part. This includes both the parameters a tool is run at, as well as the direction by which it rotates – either a Conventional Milling or a Climb Milling technique. The key distinction between these two methods lies in the relationship between the cutter’s rotation and the direction of the feed.

Conventional Milling

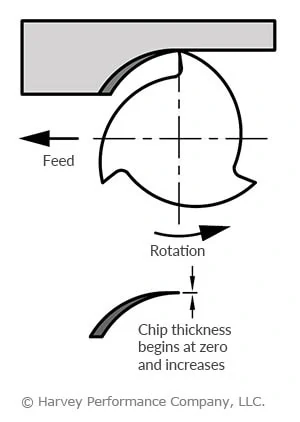
In conventional milling, the chip width starts from zero and increases gradually, causing the process of heat generation onto the workpiece rather than the chips. Heat generation causes deformities and tool failure such as work hardening, creating more headaches for a machinist. For this reason, conventional milling is generally only recommended for tools with high toughness or for breaking into case hardened materials.

conventional milling example with feed and rotation direction showcasing chip thickness

Climb Milling

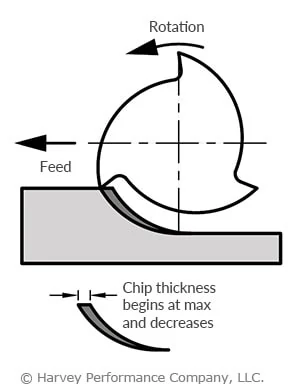
Most modern machine shops will use a climb milling technique, or when the chip width starts at its maximum and decreases during the cut. Climb Milling will offer a more consistent cut than traditional methods, and puts less stress on the tool. Think of it like weight lifting – doing the heavy lifting will be easiest at the beginning of your workout. Similarly, a cut in which the thickest chip is removed first helps the tool maintain its strength. Because the chip cutting process is more swift, vibrations are minimized.

climb milling illustration with rotation and feed directions and chip thickness relation

For more information, see Climb Milling Vs. Conventional Milling

In Conclusion

Vibrations are unavoidable during the machining process, but minimizing them can mean the difference between successful machining and scrapped parts. Following three simple rules can help to keep your chatter and harmonics under control, including: Selecting the right tool, ensuring a secure machine-tool connection, and using it in a climb milling strategy. Both Harvey Tool and Helical Solutions have tools that can help, including shank modifications and Variable Helix or Variable Pitch end mills.

https://www.harveyperformance.com/wp-content/uploads/2017/11/Feature-Image-Tool-Chatter-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-11-08 09:30:472023-12-01 16:08:473 Steps to Shutting up Tool Chatter

Avoid Composite Delamination With Compression Cutters

September 12, 2017/0 Comments/in CNC Machining, Composites, How-To's, Machining Techniques, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

Composites are a group of materials made up of at least two unique constituents that, when combined, produce mechanical and physical properties favorable for a wide array of applications. These materials usually contain a binding ingredient, known as a matrix, filled with particles or fibers called reinforcements. Composites have become increasingly popular in the Aerospace, Automotive, and Sporting Goods industries because they can combine the strength of metal, the light weight of plastic, and the rigidity of ceramics.

Unfortunately, composite materials present some unique challenges to machinists. Many composites are very abrasive and can severely reduce tool life, while others can melt and burn if heat generation is not properly controlled. Even if these potential problems are avoided, the wrong tool can leave the part with other quality issues, including delamination.

While composites such as G10 and FR4 are considered “fibrous”, composites can also be “layered,” such as laminated sheets of PEEK and aluminum. Layered composites are vulnerable to delamination, when the layers of the material are separated by a tool’s cutting forces. This yields less structurally sound parts, defeating the purpose of the combined material properties in the first place. In many cases, a single delaminated hole can result in a scrapped part.

Using Compression Cutter End Mills in Composite Materials

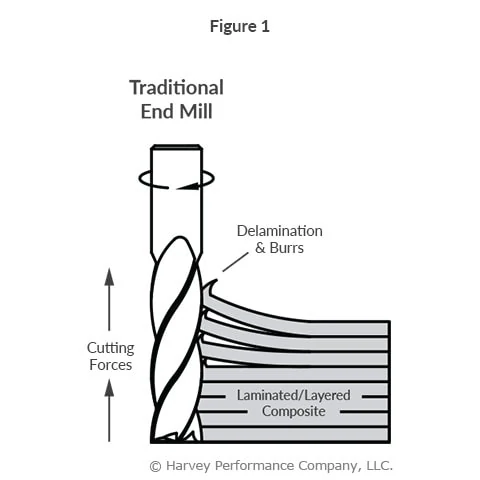
Composite materials are generally machined with standard metal cutting end mills, which generate exclusively up or down cutting forces, depending on if they have right or left hand flute geometry. These uni-directional forces cause delamination (Figure 1).

infographic of delamination with traditional end mill due to upward cutting forces

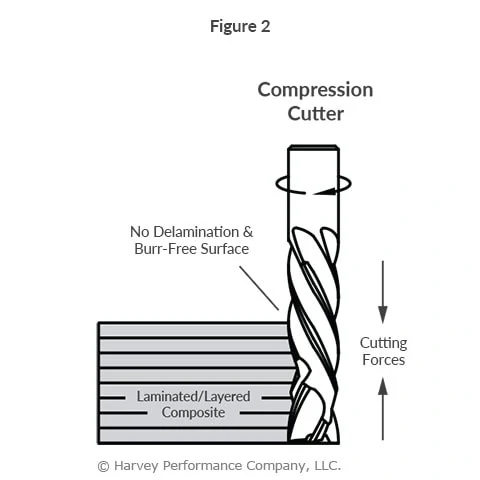
Conversely, compression cutters are designed with both up and down-cut flutes. The top portion of the length of cut, closest to the shank, has a left hand spiral, forcing chips down. The bottom portion of the length of cut, closest to the end, has a right hand spiral, forcing chips up. When cutting, the opposing flute directions generate counteracting up-cut and down-cut forces. The opposing cutting forces stabilize the material removal, which compresses the composite layers, combatting delamination on the top and bottom of a workpiece (Figure 2).

infographic of no delamination due to even cutting forces with compression cutter end mill

Since compression cutters do not pull up or press down on a workpiece, they leave an excellent finish on layered composites and lightweight materials like plywood. It is important to note, however, that compression cutters are suited specifically to profiling, as the benefits of the up and down-cut geometry are not utilized in slotting or plunging operations.

Something as simple as choosing a tool suited to a specific composite material can have significant effects on the quality of the final part. Consider utilizing tools optimized for different composites and operations or learn how to select the right drill for composite holemaking.

https://www.harveyperformance.com/wp-content/uploads/2017/09/Feature-Image-Compression-Cutters-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-09-12 16:00:532025-11-12 16:00:14Avoid Composite Delamination With Compression Cutters
Page 2 of 3123
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top