Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Drill Substrate Guide: HSS vs Cobalt vs Carbide

February 5, 2026/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Tool Selection/by Isabella Luciano

Drilling applications require careful consideration of material, production volume, and machine setup to ensure optimal hole quality, tool life, and cost. Harvey Performance Company offers drills in three primary substrates: carbide, cobalt, and high-speed steel (HSS). This guide breaks down the differences between the drilling substrate options and helps you choose the right tool for your specific application.

Solid Carbide Drills

Advantages of Carbide Drills

  1. Extreme Hardness and Wear Resistance
    • Carbide drills maintain sharp cutting edges longer than HSS or cobalt, even in abrasive materials. This reduces tool changes and helps to maintain consistent hole quality.
  2. High Heat Tolerance
    • Carbide can withstand cutting temperatures above 2,100°F (1,150°C), allowing higher speeds and feeds for faster material removal and shorter cycle times.
  3. Precision Machining
    • Carbide maintains tight tolerances and excellent surface finish in hard steels, tool steels, ceramics, composites, and high-temperature alloys, making it ideal for precise, high-performance applications.
  4. Long-term Cost Efficiency
    • Although the initial cost is higher, carbide’s longer tool life reduces frequent tool changes, lowering overall costs in high-volume production.

Drawbacks of Carbide as a Drill Substrate

  1. Brittle Nature
    • Carbide is more prone to chipping or breaking if the machine setup is not rigid, feed rates are too aggressive, or vibration is present.
  2. Regrinding Requirements
    • Carbide usually requires CNC grinding equipment for precise sharpening, unlike HSS, which can often be reground using conventional machines.
  3. Initial Investment
    • Carbide has a higher upfront cost, which may not be justified for use in short runs or soft materials, where less expensive HSS or cobalt drills can provide adequate performance.

What are the Ideal Applications for Carbide Drills?

Carbide drills excel in:

  • Large production runs requiring consistent tool life
  • Hard materials above 45 HRC, such as tool steels and high-temperature alloys
  • Applications requiring high-speed cutting and maximum material removal
  • Situations demanding precise hole tolerances and surface finish

Example: Valor Holemaking High Performance Carbide Drills are engineered to provide unmatched precision and repeatability in difficult-to-machine materials. Material-specific geometries and coolant-through designs improve heat management and tool life in demanding applications.

High Speed Steel (HSS) Drills

Advantages of HSS Drills

  1. Tough and Durable
    • High Speed Steel is the least brittle of the three materials, reducing the risk of breakage during less rigid setups.
  2. Easier to Regrind
    • HSS Drills can be sharpened and reconditioned using conventional grinding equipment, which reduces shop complexity and cost.
  3. Cost-Effective
    • The lower cost-per-tool makes HSS ideal for small jobs or low-volume production where long-term tool life is less critical.
  4. Versatile for Soft Materials
    • HSS performs well in most non-ferrous metals providing reliable results for general-purpose machining without the higher cost of harder substrates.

Drawbacks of High Speed Steel Drills

  1. Limited Heat Tolerance
    • High Speed Steel Drills can only handle cutting temperatures up to 1,100°F (600°C), restricting cutting speeds and material removal rates.
  2. Shorter Tool Life
    • HSS Edges dull faster than cobalt or carbide, requiring more frequent replacement, affecting productivity.
  3. Not Ideal for Very Hard Materials
    • High speed steel tools cannot reliably machine steels above 45 HRC or high-temperature alloys.

What are the Ideal Applications for HSS Drills?

HSS drills are ideal for:

  • Soft materials like aluminum, brass, and other non-ferrous metals
  • Small production runs or one-off jobs where tool life is less critical
  • Shops without CNC grinding capability
  • Situations where cost and ease of regrind outweigh long-term performance

Example: Titan USA High Speed Steel Drills provide reliable performance for general-purpose machining and softer materials, offering versatility for low- to medium-volume operations.

Cobalt Drills

Advantages to Cobalt Drilling

  1. Intermediate Hardness
    • Cobalt is harder than HSS but less brittle than carbide, providing a balance of toughness and wear resistance.
  2. Higher Heat Resistance
    • Cutting temperatures up to 1,580–1,616°F (860–880°C) enable faster speeds and feeds than HSS.
  3. Moderate Cost
    • Cobalt drills offer longer tool life than HSS without the higher upfront cost of carbide.
  4. Capability for Harder Materials
    • Can machine steels up to 58 HRC, handling materials that high speed steel struggles with, while remaining more forgiving than carbide.

Cobalt Drill Disadvantages

  1. Less Wear-Resistant than Carbide
    • While cobalt drills are harder than HSS, they are still not as wear-resistant as carbide. In extremely abrasive materials, cobalt drills will wear much faster than solid carbide, which can increase tool changes and impact long-term cost in high-production runs.
  2. Slightly More Brittle than HSS
    • Cobalt is harder than HSS, making it more prone to chipping or breakage. Regrinding may require careful handling or CNC equipment to maintain geometry.
  3. Not Suitable for Extreme High-Temperature Alloys or Very Hard Materials
    • Cobalt cannot maintain performance in very hard steels or high-temperature alloys. Carbide is needed for materials above 60 HRC or extreme heat applications.

What Applications are Ideal for Cobalt Drills?

Cobalt drills work well for:

  • Medium-volume jobs with harder materials
  • Applications requiring more speed and heat tolerance than HSS
  • Shops seeking a balance of cost, tool life, and performance

Example: Titan USA Cobalt Drills are a solid choice for harder-to-machine materials that do not require carbide, providing longevity and moderate speed capabilities.

What Factors Influence What Drill Substrate to Choose?

Every drilling job is unique, and the optimal drill substrate depends on your specific requirements. Key considerations include:

  • Material Hardness
  • Production Volume and Job Size
  • Machine Rigidity
  • Budget
  • Regrinding Capabilities
  • Desired Cutting Speed and Material Removal Rate

No drill fits every job, and these factors are intended as a guide to help machinists choose the right substrate to improve efficiency, precision, and cost-effectiveness.

https://www.harveyperformance.com/wp-content/uploads/2026/02/TitanUSA-Drills-033-PM-0325-001.jpg 525 1400 Isabella Luciano http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Isabella Luciano2026-02-05 16:22:522026-02-05 16:22:56Drill Substrate Guide: HSS vs Cobalt vs Carbide

The Benefits of Combined Drill & Countersinks

April 4, 2025/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Tom Delaney

Two of the most frequently recurring operations across a variety of applications are CNC drilling and countersinking. Since these two processes are often interdependent, managing space in the tool crib and time lost on tool changes can become cumbersome when using dedicated tools for each operation. Using combined drill and countersinks eliminates these concerns and has become a go-to tool across machine shops.  

valor holemaking combined drill and countersink tools on a table with a slide caliper and ruler
Variety of Combined Drill & Countersinks

What is a Combination Drill & Countersink Tool?

A Combined Drill & Countersink is a specialized tool designed to perform two critical operations in one step: drilling a hole and creating a countersink. These tools are typically short and rigid, ideal for producing either a shallow conic or a center hole. Their double-ended design minimizes downtime by enabling quick transitions between tasks.

Valor Holemaking’s Combined Drill & Countersink

Key Features of Combined Drill & Countersinks

They feature a smaller drilling pilot and larger diameter countersink. The drill pilot resembles a spot drill, making it useful for predrilling applications. The stub length of the drill mitigates deflection and ensures accurate location of a hole’s center. When preparing a spot hole for a longer drill, it prevents walking or wobbling off-center. 

Common Applications for Combined Drill & Countersinks

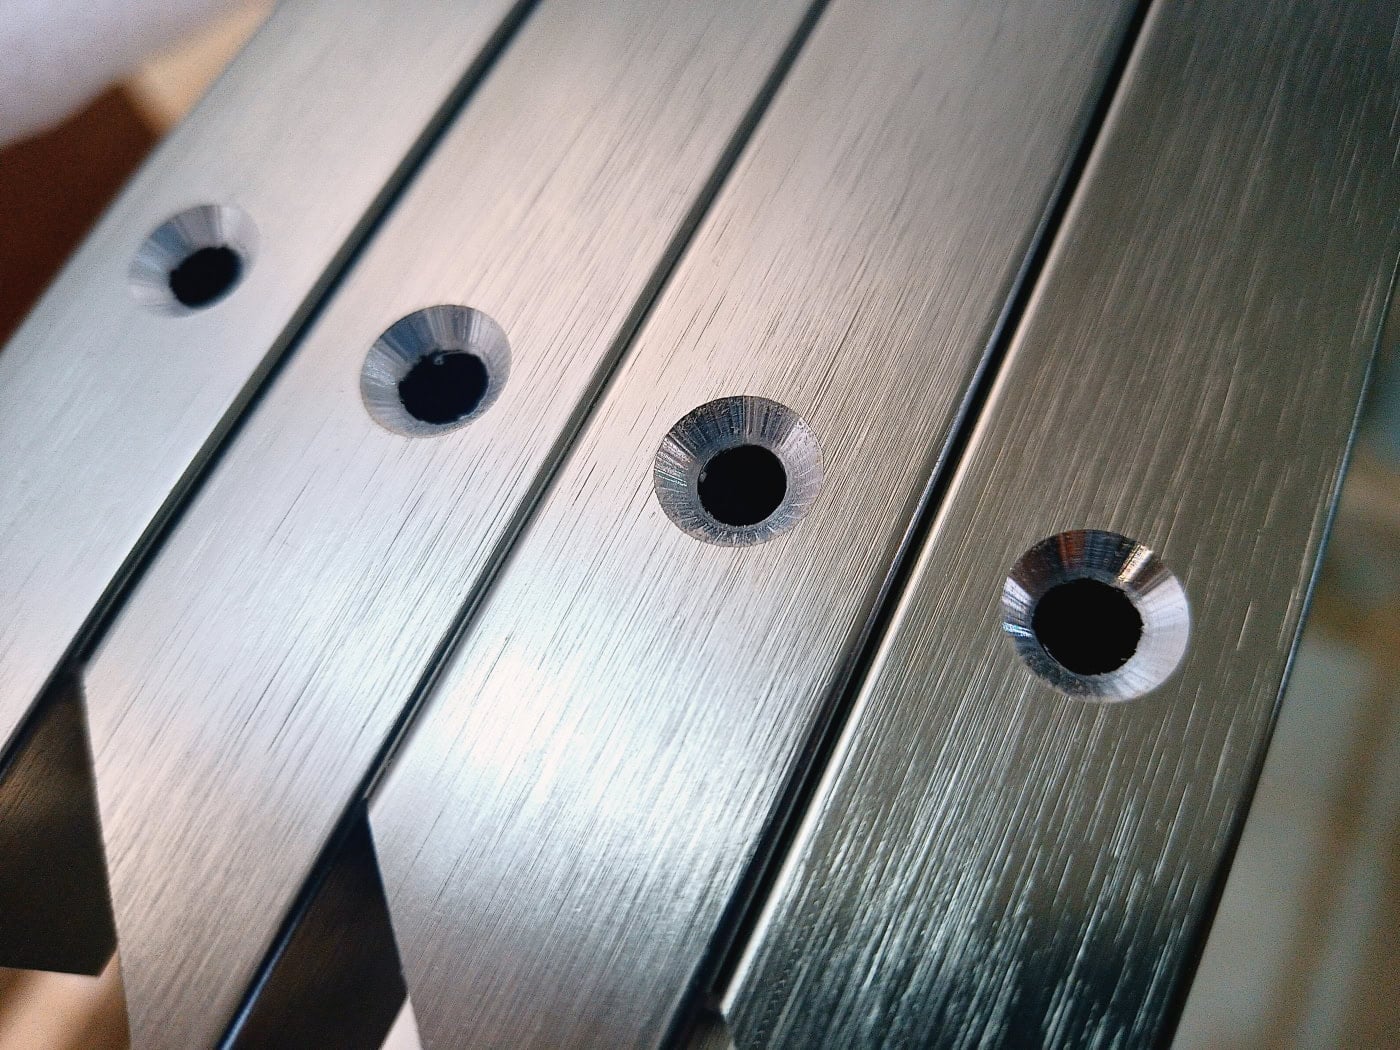
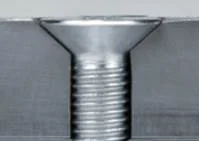
Many holemaking applications begin with spotting and end with countersinking, making combination multi-functional tools cost-effective and time efficient. As the tool drills into the material, the larger countersink diameter chamfers the top edges, allowing fasteners to sit flush with the surface.

Where and How to Use a Combined Drill & Countersink

The primary use of a combined drill and countersink is to create center holes in materials that will be turned between two centers. These centers help accurately position a workpiece along its axis between a lathe chuck and tailstock. Live centers are used in applications requiring a high level of concentricity and support. They typically feature a 60° included angle, which is the angle most combined drills and countersinks are manufactured with. For this reason, combined drill and countersinks are often referred to as center drills.

Combined drill and countersinks are also essential in any application where screws need to sit flush in the workpiece. Holes need to be drilled and countersunk across all industries. Flush-mounted fasteners are required in applications such as aircraft panels and structural components, automotive engine components, boat hulls and marine components, electronic device housings, and covers of all types.

Example of countersunk hole

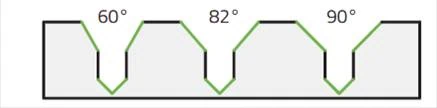
Types of Combination Drill/sinks: 60°, 82°, and 90° Angles

Harvey Tool and Valor Holemaking offer combined drill and countersinks in 60°, 82°, and 90° included angles. While 60° tools are most commonly used for center drilling, 82° and 90° included angles are designed to match the angles of the most popular flat and oval head screws. These tools allow users to create countersunk fastener holes in a single step.

Important Tips for Running Combination Drills

When running a combined drill-and-countersink, it is important to ensure that chiploads (IPR) are based on the drill diameter. Since the drill diameter is always smaller than the chamfer area, it is safer to use parameters designed for the drill portion of the tool rather than calculating an effective cutter diameter for the chamfer.

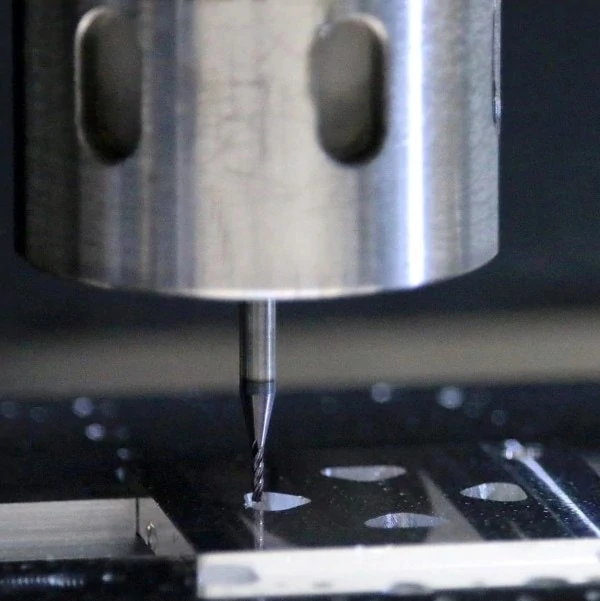
Valor Holemaking Combined Drill & Countersink in the Spindle

Why These Tools Are Essential in Machining

Combined drill & countersinks are cost-effective and efficient tools to have in your arsenal. Whether you’re preparing a workpiece for turning between centers, spot drilling, or creating countersunk holes for fasteners, these reliable tools complete the job quickly and effectively.

https://www.harveyperformance.com/wp-content/uploads/2025/04/Benefits-of-Combined-Countersink-Featured-Image.jpg 525 1400 Tom Delaney http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Delaney2025-04-04 11:38:162025-11-10 12:55:06The Benefits of Combined Drill & Countersinks

Mastering Precision: Pilot Drills in CNC Machining

December 10, 2024/4 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Machining Techniques, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Emily Van Volkom

When it comes to achieving precision in CNC drilling applications, the choice of tools and techniques can make a significant difference in the outcome. One essential element that often doesn’t get the spotlight it deserves is the Pilot Drill. This blog post will explore the importance of pilot drills, their applications, and best practices for integrating them into your CNC machining processes.

What is a Pilot Drill?

A pilot drill is used to create a guide hole in deep drilling applications where precision is required. This guide hole keeps the drill on center, maintaining straightness throughout the cut. By creating a pilot hole, machinists can also improve the quality of the finished product and extend the life of their tools.

The Importance of Pilot Drills in CNC Machining

1. Enhanced Accuracy

The primary advantage of using a pilot drill is the enhanced accuracy it provides. When working with harder materials or complex geometries, a small pilot hole helps maintain the alignment of the longer drill, reducing the risk of misalignment and defects.

2. Extended Tool Life

Using a pilot drill can significantly extend the life of your deep-hole drilling tools. By first creating a pilot hole, the chasing drill experiences less stress, reducing wear and tear, and the chance of breakage, ultimately leading to cost savings from longer tool life.

3. Improved Chip Removal

Pilot drilling can enhance chip removal, particularly in deep-hole drilling scenarios. The smaller pilot hole allows for better coolant flow, which is crucial for effective chip evacuation and maintaining optimal cutting temperatures.

Applications of Pilot Drills

Pilot drills are versatile and can be used in various applications, including:

  1. Deep-hole Drilling: Pilot holes create a guide when drilling deep holes for improved centering and straightness.
  2. Tapping Operations: A pilot hole can facilitate easier and more accurate tapping.
  3. Reaming: When preparing for reaming operations, a pilot drill can ensure the hole is properly aligned and sized.
  4. Screw and Bolt Holes: Pilot holes are essential for ensuring screws and bolts are inserted correctly and securely.

Best Practices for Using Pilot Drills

1. Application      

Piloting is recommended for tighter tolerance holes when drilling at depths of 8xD or greater. Valor Holemaking provides a custom tolerance of +0.0002/+0.0005 (+0.005mm/+0.013mm) to create the perfect oversized guide hole for their traditional drill lines capable of drilling 8xD or greater. Valor Holemaking’s Pilot Drills also include a +2/+1 deg angle tolerance to ensure a larger angle than the chasing drill. Piloting depth is recommended as 3xD for all applications drilling 8xD or greater.

2. Choose the Right Size and Point Angle

Selecting the appropriate size for your pilot drill is crucial. As a rule of thumb, the diameter of the pilot hole should be slightly larger than the diameter of the final hole. This allows for optimal support for the chasing drill while preventing excessive material removal. The pilot drill’s point angle should be equal to or larger than the succeeding drill. This allows the tip of the succeeding drill to engage the material before the flank does (see figure below).

3. Optimize Feed Rates

When using a pilot drill, ensure that the feed rates are optimized for both the pilot and the larger drill. Adjusting the feed rate can improve performance and reduce the risk of tool breakage. Valor Holemaking’s downloadable speeds and feeds tables and Machining Adviser Pro are excellent resources, and you can always consult Valor Holemaking’s Tech Team for further assistance!

4. Use Proper Coolants

Effective cooling and lubrication are vital in metal machining. Ensure that your pilot drill is adequately cooled with flood coolant or adjust speeds and feeds to maintain tool integrity and enhance cutting performance.

5. Maintain Tool Condition

Regularly check the condition of your pilot drills. Worn or damaged pilot drills can lead to inaccuracies and affect the performance of subsequent operations.

6. Integrate with CNC Programming

Incorporate pilot drilling into your CNC programs to ensure that it’s executed at the right stage of your machining process. Program one revolution or brief dwell at the bottom of the pilot hole to ensure a clean surface. This will help streamline operations and improve overall efficiency.


Conclusion

Pilot drills may seem like a small detail in the larger scope of CNC machining, but their impact on precision, tool life, and overall efficiency is significant. By understanding their importance and implementing best practices, machinists can enhance their processes and achieve superior results. Whether you’re a seasoned CNC operator or just starting out, incorporating pilot drills into your workflow is a smart move that can lead to greater accuracy and success in metal machining.


https://www.harveyperformance.com/wp-content/uploads/2024/12/Featured-Image-Pilot-Drills-IMG.jpg 525 1400 Emily Van Volkom http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Emily Van Volkom2024-12-10 13:53:412025-01-30 09:11:16Mastering Precision: Pilot Drills in CNC Machining

How to Select a Spindle

October 24, 2019/5 Comments/in Getting Started, How-To's, Machining Techniques/by Ben Holm

When trying to develop efficient processes, many machinists and programmers turn to tool selection first. It is true that tooling can often make a big difference in machining time, and speeds and feeds, but did you know that your machine’s spindle can have an equally impactful effect? The legs of any CNC machine, spindles are comprised of a motor, a taper for holding tools, and a shaft that will hold all of the components together. Often powered by electricity, spindles rotate on an axis which receives its input from the machine’s CNC controller.

Why is Choosing the Right Spindle Important?

Choosing the right spindle to machine your workpiece with is of very high importance to a successful production run. As tooling options continue to grow, it is important to know what tooling your spindle can utilize. Large diameter tools such as large end mills or face mills typically require slower spindle speeds and take deeper cuts to remove vast amounts of material. These applications require supreme machine rigidity and require a spindle with high torque.

Contrastingly, smaller diameter tools will need a higher-speed spindle. Faster speeds and feeds deliver better surface finishes and are used in a variety of applications. A good rule of thumb is that an end mill that is a half inch or smaller will run well with lower torque.

Types of CNC Spindles

After finding out what you should look for in a spindle, it is time to learn about your different options. Spindles typically vary by the type, style of the taper, or its size. The taper is the conical portion of the tool holder that fits inside of the opening of the spindle. Every spindle is designed to mate with a certain taper style and size.

properly selecting a spindle

CAT and BT Holders

This is the most widely utilized holder for milling in the United States. Referred to as “V-flange holders,” both of these styles need a retention knob or pull stud to be secured within the machine spindle. The BT (metric style) is popular overseas.

HSK Holders

This type of holder is a German standard known as “hollow shank taper.” The tapered portion of the holder is much shorter than its counterparts. It also engages the spindle in a different way and does not require a pull stud or retention knob. The HSK holder is utilized to create repeatability and longer tool life – particularly in High Efficiency Milling (HEM) applications.

All of these holders have benefits and limitations including price, accuracy, and availability. The proper selection will depend largely on your application requirements.

Torque vs. Horsepower

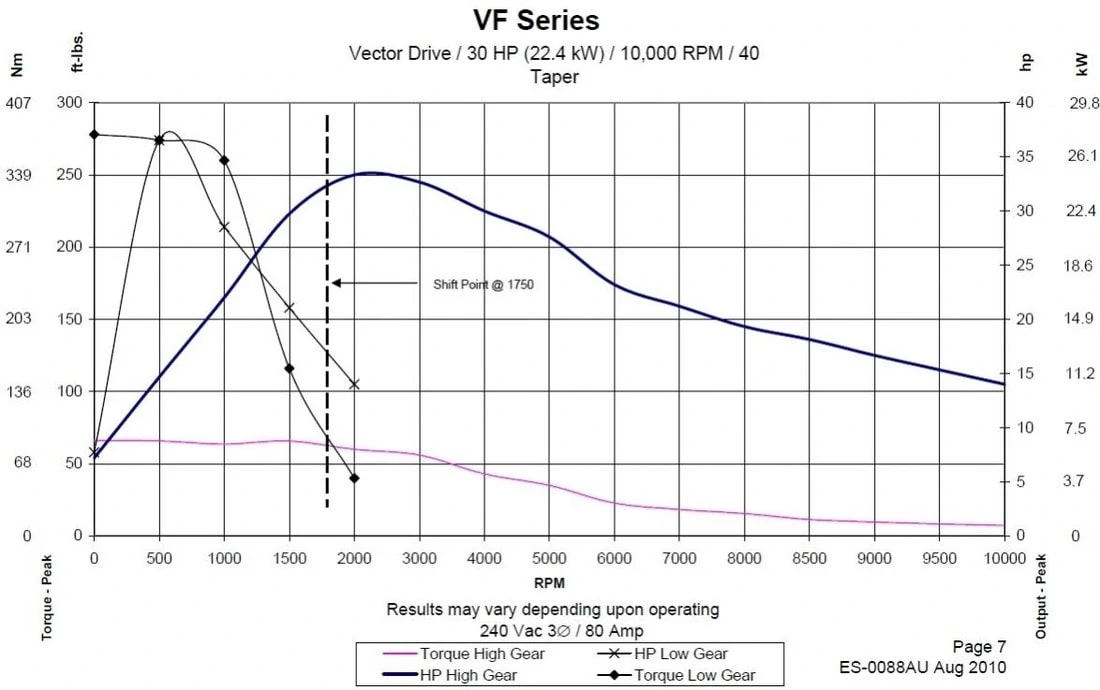
Torque is defined as force perpendicular to the axis of rotation across a distance. It is important to have high torque capabilities when using an end mill larger than ½ inch, or when machining a difficult material such as Inconel. Torque will help put power behind the cutting action of the tool.

Horsepower refers to the amount of work being done. Horsepower is important for smaller diameter end mills and easy-to-machine materials like aluminum.

You can think of torque as a tractor: It can’t go very fast, but there is a lot of power behind it. Think of horsepower as a racecar: It can go very fast but cannot pull or push.

Torque-Horsepower Chart

Every machine and spindle should come with a torque horsepower chart. These charts will help you understand how to maximize your spindle for torque or horsepower, depending on what you need:

Haas spindle horsepower and torque chart
Image Source: HAAS Machine Manual

Proper Spindle Size

The size of the spindle and shank taper corresponds to the weight and length of the tools being used, as well as the material you are planning to machine. CAT40 is the most commonly used spindle in the United States. These spindles are great for utilizing tools that have a ½ inch diameter end mill or smaller in any material. If you are considering using a 1 inch end mill in a material like Inconel or Titanium, a CAT50 would be a more appropriate choice. The higher the taper angle is, the more torque the spindle is capable of.

While choosing the correct tool for your application is important, choosing a tool your spindle can utilize is paramount to machining success. Knowing the amount of torque required will help machinists save a lot of headaches.

https://www.harveyperformance.com/wp-content/uploads/2019/10/Feature-Image-Select-Spindle-IMG-3.jpg 525 1400 Ben Holm http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Ben Holm2019-10-24 13:21:212022-06-08 11:13:34How to Select a Spindle

Workholding Styles & Considerations

October 18, 2018/0 Comments/in CNC Machining, Getting Started, Machining 101, Machining Techniques, Milling, Tech Tips/by Robert Keever

Machinists have a number of variables to consider when setting up devices for a machining operation. When it comes to cnc workholding, there are some major differences between holding a loosely toleranced duplicate part with a 10-minute cycle time and holding a tightly toleranced specialized part with a 10-hour cycle time. Determining which method works best for your machining job is essential to maintaining an efficient operation.

CNC Workholding Devices

Ideal workholding devices have easily repeatable setups. For this reason, some machines have standard workholding devices. Vises are generally used with milling machines while chucks or collets are used when running a lathe machine. Sometimes, a part may need a customized cnc workholding setup in order to secure the piece properly during machining. Fixtures and jigs are examples of customized devices.

Fixtures and Jigs

A jig is a work holding device that holds, supports and locates a workpiece and guides the cutting tool into a specific operation (usually through the use of one or more bushings). A fixture is essentially the same type of device, but the main difference is that it does not guide the cutting tool into a specified operation. Fixtures are typically used in milling operations while jigs are generally used in drilling, reaming, tapping and boring. Jigs and fixtures are more precise relative to standard cnc workholding devices, which leads to tighter tolerances. They can also be indexable, allowing them to control the cutting tool movement as well as workpiece movement. Both jigs and fixtures are made up of the same basic components: fixture bodies, locators, supports, and clamps.

The 4 Fixture Bodies

There are 4 basic types of fixture bodies: faceplates, baseplates, angle plates, and tombstones.

Faceplates: Typically used in lathe operations, where components are secured to the faceplate and then mounted onto the spindle.

Baseplates: Common in milling and drilling operations and are mounted to the worktable.

Angle plates: Two plates perpendicular to each other but some are adjustable or customized to change the angle of the workpiece.

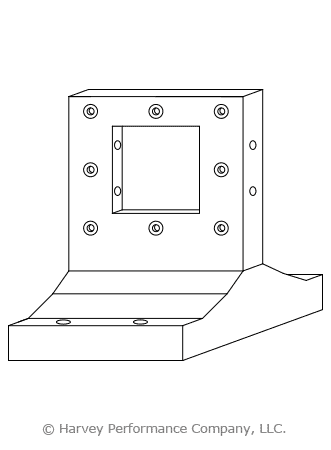
Tombstones: Large vertically oriented rectangular fixtures that orients a workpiece perpendicular to the worktable. Tombstones also have two sides to accommodate multiple parts.

cnc tombstone work holding fixture body

Locators

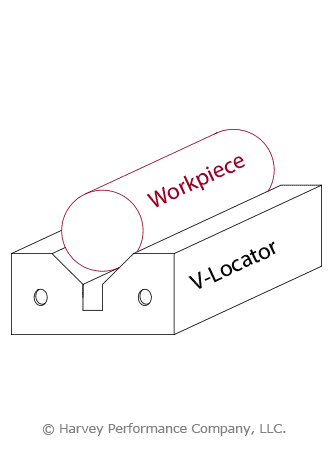
Locators are characterized by four criteria: assembled, integral, fixed, and adjustable. Assembled locators, can be attached and removed from the fixture, which is contrary to integral locators that are built into the fixture. Fixed locators allow for no moving components, while adjustable locators permit movement through the use of threads and/or springs, and can adjust to a workpiece’s size. These can be combined to provide the appropriate rigidity-assembly convenience ratio. For example, a V-locator fixture is the combination of assembled and fixed locators. It can be secured to a fixture but has no moving components.

cnc workholding showcasing a workpiece in v-locator

Supports

Supports do exactly what their name suggests, they support the workpiece during the machining process to avoid workpiece deformation. These components can double as locators and also come fixed, adjustable and integral, or assembled. Generally, supports are placed under the workpiece during manufacturing but this also depends on the geometry of the workpiece, the machine being operated and where the cutting tool will make contact. Supports can come in different shapes and sizes. For example, rest buttons are smaller support components used in series either from underneath the workpiece or from the sides. Concurrently, parallel supports are placed on either side of the part to provide general support.

cnc material support with parallel supports and rest buttons

Clamps

Clamps are devices used for strengthening or holding things together, and come in different shapes, sizes and strengths. Vises and chucks have movable jaws and are considered standard clamps. One atypical example is the toggle clamp, which has a pivot pin that acts as a fulcrum for a lever system. One of the more convenient types is a power clamping system. There are two type of power clamping methods: hydraulic and pneumatic.

cnc workholding clamps

Example of a standard fixture setup.

Hydraulic Workholding Systems

Hydraulic Systems create a gripping force by attaining power from compressing a liquid. This type of power clamp is generally used with larger workpieces as it usually takes up less space relative to pneumatic clamps.

Pneumatic clamps

Pneumatic clamps attain their gripping force from the power created by a compressed gas (usually air). These systems are generally bulkier and are used for smaller workpieces that require less room on the worktable. Power clamping offers a few advantages over conventional clamping. First, these systems can be activated and deactivated quickly to save on changeover time. Second, they place uniform pressure on the part, which help prevent errors and deformation. A significant disadvantage they pose is the cost of a system but this can be quickly offset by production time saved.

Key Guidelines to Follow

Lastly, there are a few guidelines to follow when choosing the appropriate CNC workholding fixture or jig setup.

Ensure Proper Tolerancing

The tolerances of the workholding device being used should be 20%-50% tighter than those of the workpiece.

Utilize Acceptable Locating & Supporting Pieces

Locating and supporting pieces should be made of a hardened material to prevent wear and allow for several uses without the workpieces they support falling out of tolerance. Supports and locators should also be standardized so that they can be easily replaced.

Place Workholding Clamps in Correct Locations

Clamps should be placed above the locations of supports to allow the force of the clamp to pass into the support without deforming the workpiece. Clamps, locators and supports should also be placed to distribute cutting forces as evenly as possible throughout the part. The setup should allow for easy clamping and not require much change over time

Maximize Machining Flexibility

The design of the fixture or jigs should maximize the amount of operations that can be performed in one orientation. During the machining operation, the setup should be rigid and stable.

Bottom Line

Workholding can be accomplished in a number of different ways and accomplish the same task of successfully gripping a part during a machining operation with the end result being in tolerance. The quality of this workholding may differ greatly as some setups will be more efficient than others. For example, there is no reason to create an elaborate jig for creating a small slot down the center of a rectangular brick of aluminum; a vise grip would work just fine. Maximizing the efficiency and effectiveness of an operators’ cnc workholding setup will boost productivity by saving on changeover, time as well as cost of scrapped, out of tolerance parts.

https://www.harveyperformance.com/wp-content/uploads/2018/10/Featured-Image-Workholding-Styles-IMG.jpg 525 1400 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2018-10-18 08:44:202023-10-24 10:41:29Workholding Styles & Considerations

5 Questions to Ask Before Selecting an End Mill

October 16, 2018/0 Comments/in CNC Machining, Getting Started, Machining 101, Machining Techniques, Tool Selection/by Harvey Performance Company

Few steps in the machining process are as important as proper end mill selection. Complicating the process is the fact that each individual tool has its own unique geometries, each pivotal to the eventual outcome of your part. We recommend asking yourself 5 key questions before beginning the tool selection process. In doing so, you can ensure that you are doing your due diligence in selecting the best tool for your application. Taking the extra time to ensure that you’re selecting the optimal tool will reduce cycle time, increase tool life, and produce a higher quality product.

Question 1: What Material Am I Cutting?

Knowing the material you are working with and its properties will help narrow down your end mill selection considerably. Each material has a distinct set of mechanical properties that give it unique characteristics when machining. For instance, plastic materials require a different machining strategy – and different tooling geometries – than steels do. Choosing a tool with geometries tailored towards those unique characteristics will help to improve tool performance and longevity.

Harvey Tool stocks a wide variety of High Performance Miniature End Mills. Its offering includes tooling optimized for hardened steels, exotic alloys, medium alloy steels, free machining steels, aluminum alloys, highly abrasive materials, plastics, and composites. If the tool you’re selecting will only be used in a single material type, opting for a material specific end mill is likely your best bet. These material specific tools provide tailored geometries and coatings best suited to your specific material’s characteristics. But if you’re aiming for machining flexibility across a wide array of materials, Harvey Tool’s miniature end mill section is a great place to start.

Shop Harvey Tool’s Massive Offering of Fully Stocked Miniature End Mills

Helical Solutions also provides a diverse product offering tailored to specific materials, including Aluminum Alloys & Non-Ferrous Materials; and Steels, High-Temp Alloys, & Titanium. Each section includes a wide variety of flute counts – from 2 flute end mills to Multi-Flute Finishers, and with many different profiles, coating options, and geometries.

Question 2: Which Operations Will I Be Performing?

An application can require one or many operations. Common machining operations include:

  • Traditional Roughing
  • Slotting
  • Finishing
  • Contouring
  • Plunging
  • High Efficiency Milling

By understanding the operations(s) needed for a job, a machinist will have a better understanding of the tooling that will be needed. For instance, if the job includes traditional roughing and slotting, selecting a Helical Solutions Chipbreaker Rougher to hog out a greater deal of material would be a better choice than a Finisher with many flutes.

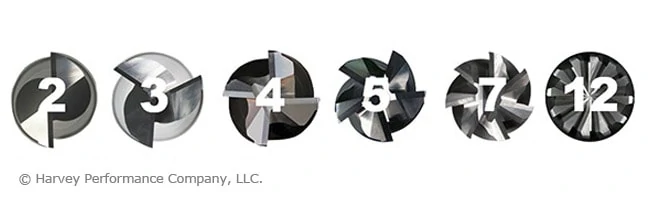
Question 3: How Many Flutes Do I Need?

One of the most significant considerations during end mill selection is determining proper flute count. Both the material and application play an important role in this decision.

Material:

When working in Non-Ferrous Materials, the most common options are the 2 or 3-flute tools. Traditionally, the 2-flute option has been the desired choice because it allows for excellent chip clearance. However, the 3-flute option has proven success in finishing and High Efficiency Milling applications, because the higher flute count will have more contact points with the material.

Ferrous Materials can be machined using anywhere from 3 to 14-flutes, depending on the operation being performed.

Application:

Traditional Roughing: When roughing, a large amount of material must pass through the tool’s flute valleys en route to being evacuated. Because of this, a low number of flutes – and larger flute valleys – are recommend. Tools with 3, 4, or 5 flutes are commonly used for traditional roughing.

Slotting: A 4-flute option is the best choice, as the lower flute count results in larger flute valleys and more efficient chip evacuation.

Finishing: When finishing in a ferrous material, a high flute count is recommended for best results. Finishing End Mills include anywhere from 5-to-14 flutes. The proper tool depends on how much material remains to be removed from a part.

High Efficiency Milling: HEM is a style of roughing that can be very effective and result in significant time savings for machine shops. When machining an HEM toolpath, opt for 5 to 7-flutes.

graphic showcasing the tool face of end mills from 2 to 12 flutes

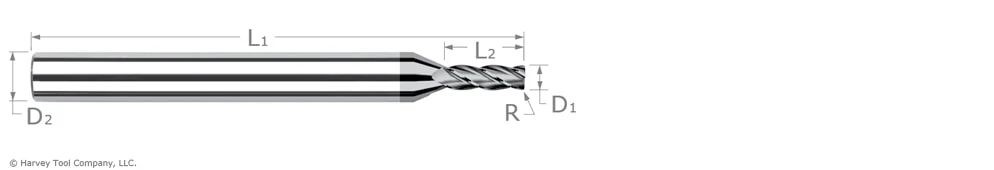
Question 4: What Specific Tool Dimensions are Needed?

After specifying the material you are working in, the operation(s) that are going to be performed, and the number of flutes required, the next step is making sure that your end mill selection has the correct dimensions for the job. Examples of key considerations include cutter diameter, length of cut, reach, and profile.

Cutter Diameter

The cutter diameter is the dimension that will define the width of a slot, formed by the cutting edges of the tool as it rotates. Selecting a cutter diameter that is the wrong size – either too large or small – can lead to the job not being completed successfully or a final part not being to specifications.  For example, smaller cutter diameters offer more clearance within tight pockets, while larger tools provide increased rigidity in high volume jobs.

Length of Cut & Reach

The length of cut needed for any end mill should be dictated by the longest contact length during an operation. This should be only as long as needed, and no longer. Selecting the shortest tool possible will result in minimized overhang, a more rigid setup, and reduced chatter. As a rule of thumb, if an application calls for cutting at a depth greater than 5x the tool diameter, it may be optimal to explore necked reach options as a substitute to a long length of cut.

Tool Profile

The most common profile styles for end mills are square, corner radius, and ball. The square profile on an end mill has flutes with sharp corners that are squared off at 90°. A corner radius profile replaces the fragile sharp corner with a radius, adding strength and helping to prevent chipping while prolonging tool life. Finally, a ball profile features flutes with no flat bottom, and is rounded off at the end creating a “ball nose” at the tip of the tool. This is the strongest end mill style.  A fully rounded cutting edge has no corner, removing the mostly likely failure point from the tool, contrary to a sharp edge on a square profile end mill. An end mill profile is often chosen by part requirements, such as square corners within a pocket, requiring a square end mill.  When possible, opt for a tool with the largest corner radius allowable by your part requirements. We recommend a corner radii whenever your application allows for it. If square corners are absolutely required, consider roughing with a corner radius tool and finishing with the square profile tool.

end mill graphic with dimension callouts

Question 5: Should I Use a Coated Tool?

When used in the correct application, a coated tool will help to boost performance by providing the following benefits:

  • More Aggressive Running Parameters
  • Prolonged Tool life
  • Improved Chip Evacuation

Harvey Tool and Helical Solutions offer many different coatings, each with their own set of benefits. Coatings for ferrous materials, such as AlTiN Nano or TPlus, typically have a high max working temperature, making them suitable for materials with a low thermal conductivity. Coatings for non-ferrous applications, such as TiB2 or ZPlus, have a low coefficient of friction, allowing for easier machining operations. Other coatings, such as Amorphous Diamond or CVD Diamond Coatings, are best used in abrasive materials because of their high hardness rating.

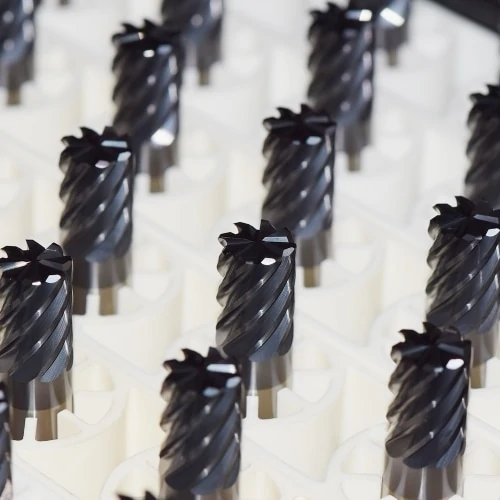
multiple end mills after being coated, zoomed in on cutting faces

Ready to Decide on an End Mill

There are many factors that should be considered while looking for the optimal tooling for the job, but asking the aforementioned five key question during the process will help you to make the right decision. As always, The Harvey Performance Company Technical Service Department is always available to provide recommendations and walk you through the tool selection process, if need be.

Harvey Tool Technical Support: 800-645-5609

Helical Solutions Technical Support: 866-543-5422

https://www.harveyperformance.com/wp-content/uploads/2018/10/Feature-Image-5-Questions-IMG-2.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-10-16 09:00:242023-10-24 10:42:255 Questions to Ask Before Selecting an End Mill

5 Ways Your Shop is Inefficient

March 5, 2018/2 Comments/in Getting Started, Machining 101, Machining Techniques, Troubleshooting Tips/by Harvey Performance Company

5 Ways Your Shop is Inefficient

In today’s ultracompetitive industry, every machine shop seeks even the slightest edge to gain an advantage on their competition and boost their bottom line. However, what many machinists don’t know is that improving their shop’s efficiency might be easier than they thought. The following five ways your shop is inefficient will provide a clear starting point of where to look for machinists desperate to earn a competitive edge.

Premature Tool Decay / Tool Failure

If you’re finding that your tools are failing or breaking at an unacceptable rate, don’t mistake it for commonplace. It doesn’t have to be. Prolonging the life of your tooling starts with finding not just the right tool, but the best one; as well as running it in a way to get its optimal performance. Many machinists mistake premature tool failure with running parameters that were too aggressive. In fact, not pushing the tool to its full potential can actually cause it to decay at an accelerated rate in certain situations.

Tool failure can occur in many different ways: Abrasive Wear, Chipping, Thermal Cracking or Tool Fracture, just to name a few. Understanding each type and its causes can help you to quickly boost your shop’s efficiency by minimizing downtime and saving on replacement tool costs.

close up view of excessive tool wear on a cutting edge

An example of a tool with excessive wear

For more information on tool wear, view Avoiding 4 Major Types of Tool Wear.

Subpar Part Finish

Your shop spends money to employ machinists, run machines, and buy cutting tools. Get your money’s worth, lead the industry, and ensure that you’re providing your customers with the highest quality product. Not only will this help to keep your buyer-seller relationship strong, but it will allow you the flexibility to increase your prices in the future, and will attract prospective customers.

Many factors influence part finish, including the material and its hardness, the speeds and feeds you’re running your tool at, tool deflection, and the tool-to-workpiece orientation.

For more information on ways to improve your part finish, view our Part Finish Reference Guide.

Inefficient Coolant Usage

One often forgotten expense of a machine shop is coolant – and it can be pricey. A 55-gallon drum of coolant can run more than $1,500. What’s worse is that coolant is often applied in excess of what’s required for the job. In fact, some machines even feature a Minimum Quantity Lubricant (MQL) functionality, which applies coolant as an extremely fine mist or aerosol, providing just enough coolant to perform a given operation effectively. While drowning a workpiece in coolant, known as a “Flood Coolant,” is sometimes needed, it is oftentimes utilized on jobs that would suffice with much less.

For more information about coolants and which method of application might be best for your job, view What You Need to Know About Coolant for CNC Machining.

Not Taking Advantage of Tool Versatility

Did you know that several CNC cutting tools can perform multiple operations? For example, a Chamfer Mill can chamfer, bevel, deburr, and countersink. Some Chamfer Mills can even be used as a Spotting Drill. Of course, the complexity of the job will dictate your ability to reap the benefits of a tool’s versatility. For instance, a Spotting Drill is obviously the best option for spotting a hole. If performing a simple operation, though, don’t go out of your way to buy additional tooling when what’s already in your carousel can handle it.

two helical solutions chamfer mills

To learn more about versatile tools that can perform multiple applications, check out Multi-Functional Tools Every Shop Should Have.

High Machine Downtime Makes Your Shop Inefficient

What use is a machine that’s not running beside making your shop inefficient? Minimizing machine downtime is a key way to ensure that your shop is reaching its efficiency pinnacle. This can be accomplished a variety of ways, including keeping like-parts together. This allows for a simple swap-in, swap-out of material to be machined by the same cutting tool. This saves valuable time swapping out tooling, and lets your machine to do its job for more time per workday. Production planning is a key factor to running an efficient machine shop.

https://www.harveyperformance.com/wp-content/uploads/2018/03/Featured-Image-Shop-Inefficient-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-03-05 14:30:062023-10-12 14:34:385 Ways Your Shop is Inefficient

Milling Machines vs. Lathe Machines

February 22, 2018/28 Comments/in CNC Machining, Getting Started, Machining 101, Micro 100, Milling, Quick Tips/by Harvey Performance Company

Most modern manufacturing centers have both milling machines and lathe machines. Each machine follows the same machining principle, known as subtractive machining, where you begin with a block of material and then shape that material into the desired specifications. How the part is actually shaped is the key difference between the two machines. Understanding the differences in more depth will help in putting the right part in the right machine to maximize their capabilities.

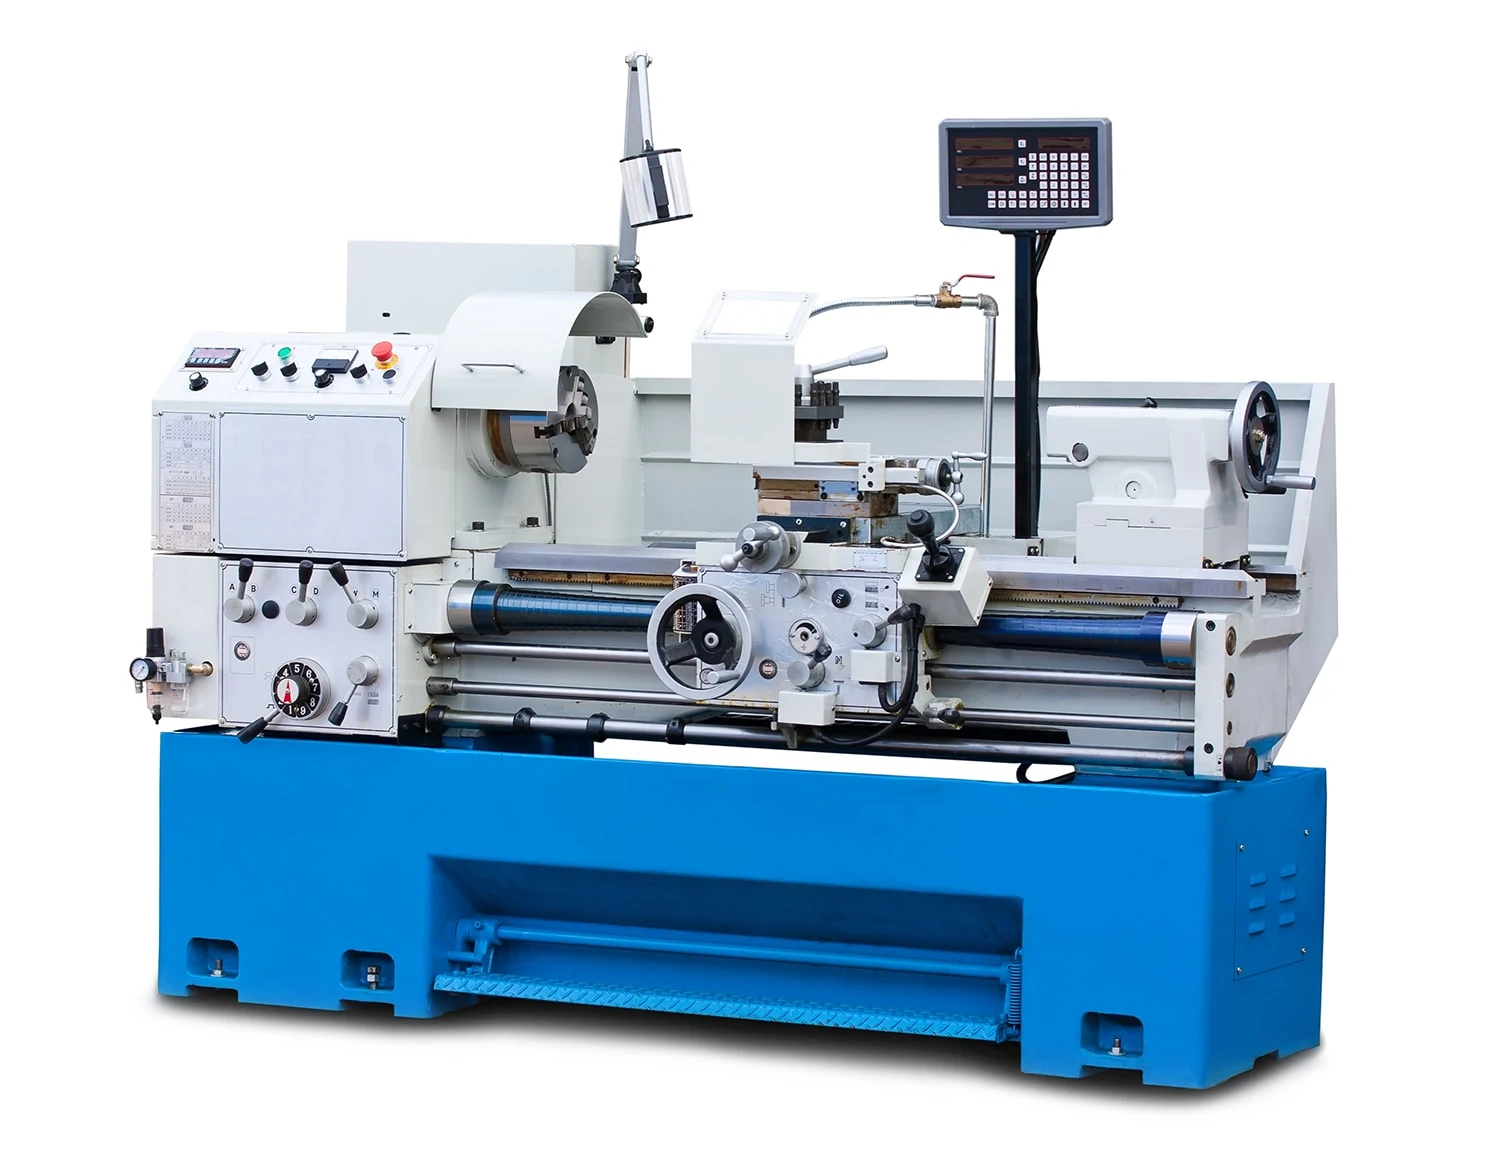
white and blue cnc lathe

An Example of a Lathe Machine

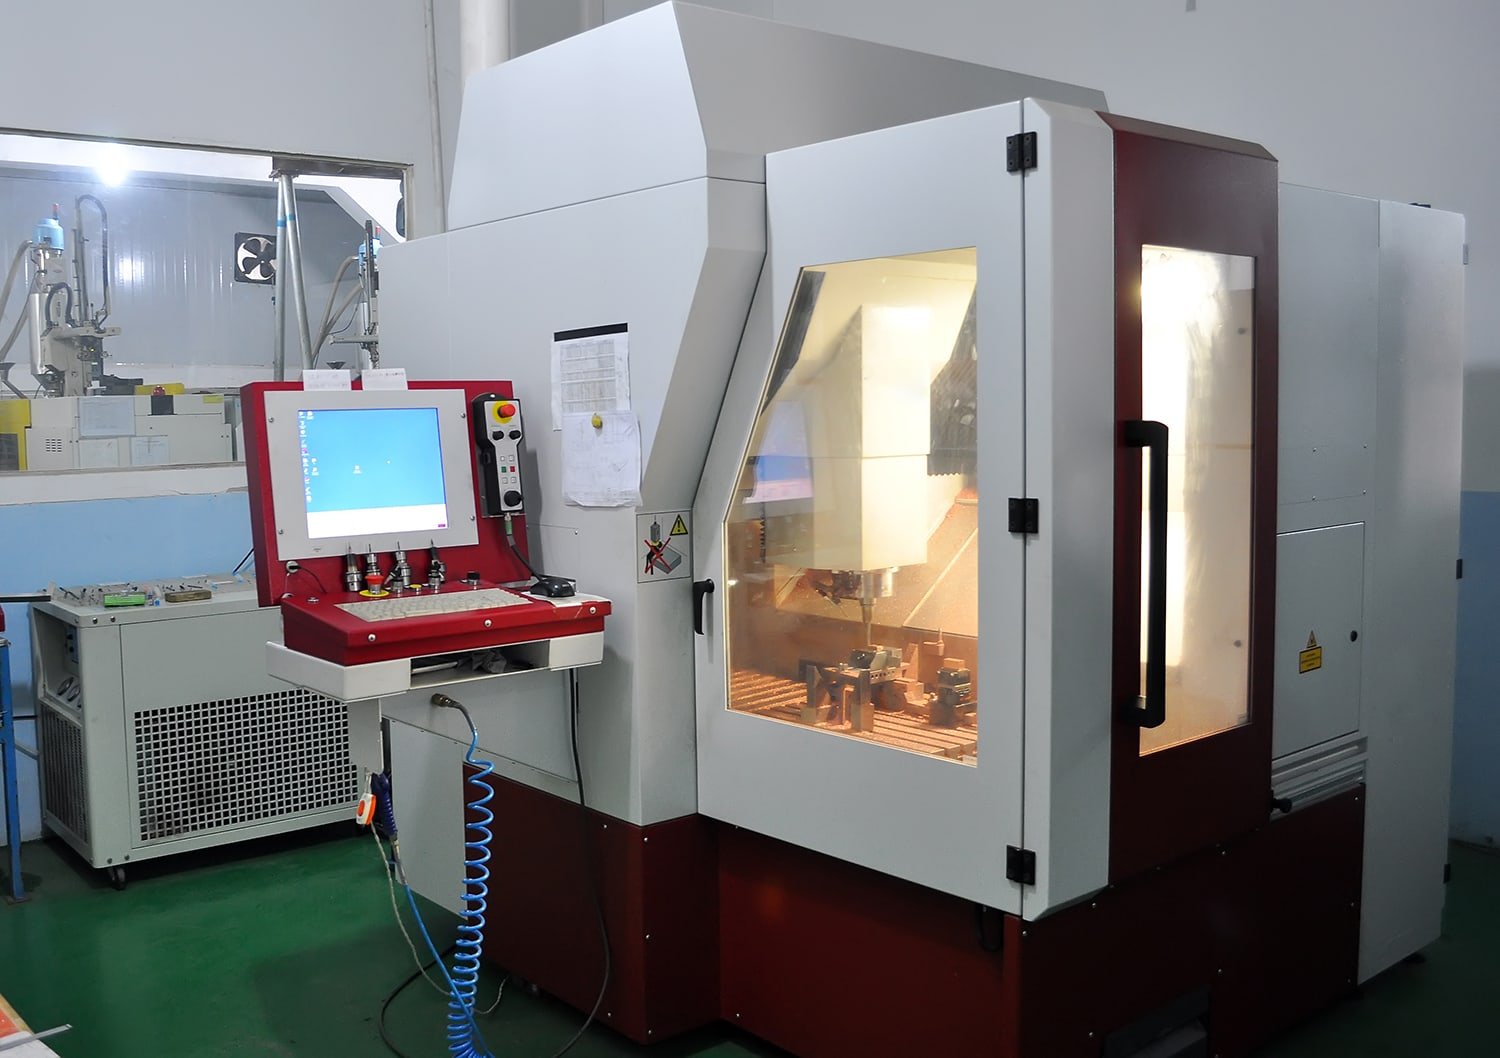
cnc milling machine

An Example of a Milling Machine

Operation

The major difference between a milling machine and a lathe machine is the relationship of the workpiece and the tool.

Lathe Machines

In a lathe, the workpiece that is being machined spins about it’s axis, while the cutting tool does not. This is referred to as “turning”, and is effective for creating cylindrical parts. Common operations done on a lathe include drilling, boring, threading, ID and OD grooving, and parting. When looking to create quick, repeatable, and symmetrical cylindrical parts, the lathe machine is the best choice.

adjustable boring bar turning a part in a cnc lathe

Milling Machines

The opposite is true for milling machines. The tool in a milling machine rotates about its axis, while the workpiece does not. This allows the tool to approach the workpiece in many different orientations that more intricate and complex parts demand. If you can program it, you can make it in a milling machine as long as you have the proper clearance and choose the proper tooling.

cnc multi axis machine machining a turbine part

Best Practice

The best reason to use a milling machine for an upcoming project is the versatility. The tooling options for a milling machine are endless, with hundreds of available specialty cutting tools and various styles of end mills which make sure you are covered from start to finish on each job. A mill can also cut more complex pieces than a lathe. For example, it would impossible to efficiently machine something like an intake manifold for an engine on a lathe. For intricate parts like that, a milling machine would be required for successful machining.

While lathe machines are more limited in use than a milling machine, they are superior for cylindrical parts. While a mill can make the same cuts that a lathe does, it may need multiple setups to create the same part. When continuous production of cylindrical parts is necessary, a lathe will outperform the mill and increase both performance and efficiency.

https://www.harveyperformance.com/wp-content/uploads/2018/02/Featured-Image-Milling-vs-Lathe-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-02-22 15:23:302024-02-09 10:21:59Milling Machines vs. Lathe Machines

Work Hardening and When it Should Scare You

October 30, 2017/5 Comments/in CNC Machining, Getting Started, Machining 101, Material Specific, Troubleshooting Tips/by Harvey Performance Company

What Is Work Hardening

Work hardening is often an unintentional part of the machining process, where the cutting tool generates enough heat in one area to harden the workpiece. It results in plastic deformation which alters the physical structure of the metal being machined. This altered structure affects the machinability of the chosen metal and acts similarly to heat treating. When this occurs the generated speeds and feed requirements will be changed, creating a potential for inefficiency. This makes for a much more difficult machining process and can lead to scrapped parts, broken tools, and serious headaches.

Soften Up Work Hardening With Machining Advisor Pro’s Customizable Speeds and Feeds

What Causes Work Hardening

During machining, the friction between the tool and the workplace generates heat. The heat that is transferred to the workpiece causes the structure of the material to change and in turn harden the material. The degree to which it is hardened depends on the amount of heat being generated in the cutting action and the properties of the material, such as carbon content and other alloying elements. The most influential of these alloying elements include Manganese, Silicon, Nickel, Chromium, and Molybdenum.

While the hardness change will be the highest at the surface of the material, the thermal conductivity of the material will affect how far the hardness changes from the surface of the material.

titanium packed ball bearing

Often times, the thermal properties of a material that makes it appealing for an application are also the main cause of its difficulty to machine. For example, the favorable thermal properties of titanium that allow it to function as a jet turbine are the same properties that cause difficulty in machining it.

Major Problems

Heat Generation

As previously stated, metal work hardening can create some serious problems when machining. The biggest issue is heat generated by the cutting tool and transferring to the workpiece, rather than to the chips. When the heat is transferred to the workpiece, it can cause deformation which will lead to scrapped parts. Stainless Steels and High-Temp Alloys are most prone to work hardening, so extra precaution is needed when machining in these materials.

stringy chips in front of an end mill in the cut

Improper Speeds and Feeds

One other issue that scares a lot of machinists is the chance that a workpiece can harden to the point that it becomes equally as hard as the cutting tool. This is often the case when improper speeds and feeds are used. Incorrect speeds and feeds will cause more rubbing and less cutting, resulting in more heat generation passed to the workpiece. In these situations, machining can become next to impossible, and serious tool wear and eventual tool breakage are inevitable if the tool continues to be fed the same way.

Harvey tool ad for work hardening and speeds and feeds

How To Avoid Work Hardening

There are a few main keys to avoid work hardening: correct speeds and feeds, performing climb milling, selecting appropriate tool coatings, and proper coolant usage. As a general rule of thumb, talking to your tooling manufacturer and using their recommended speeds and feeds is essential for machining success.

Speeds and Feeds

Speeds and feeds become an even bigger priority when you want to avoid heat and tool rubbing, which can both cause serious work hardening. More cutting power and a constant feed rate keeps the tool moving and prevents heat from building up and transferring to the workpiece. The ultimate goal is to get the heat to transfer to the chips, and minimize the heat that is transferred into workpiece and avoiding any deformation of parts. Prior to machining, you should be setting guidelines for each cutting tool to ensure you receive the highest output without compromising on part finish or tool life.

Climb Milling

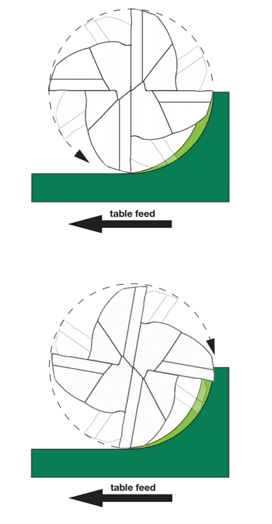
Conventional milling and climb milling are the two ways to perform CNC cutting operations. In climb milling, the cutter rotates with the feed, while in conventional milling the cutter rotates against the feed. However during conventional milling, the chip width starts at zero then increases thus generating heat at the workpiece. This results in work hardening and faster tool wear over time. On the other hand, climb milling begins at maximum chip width and decreases which transfers heat to the chip rather than the tool or workpiece. Climb milling is advantageous because there is less tool rubbing, minimized chance of chip recutting, and enhanced tool life.

drawing that displays conventional milling vs climb milling in cnc cutting operations

Tool Coating

While friction is often the main culprit of heat generation, the appropriate coating for the material may help combat the severity. Many coatings for ferrous materials reduce the amount of friction generated during cutting action. This added lubricity will reduce the friction on the cutting tool and workpiece, therefore transferring the heat generated to the chip, rather than to the workpiece. Tool coatings also create a natural separation between carbide and the workpiece. This minimizes the internal temperature of the carbide as heat is transferred into the chips and workpiece.

Coolant

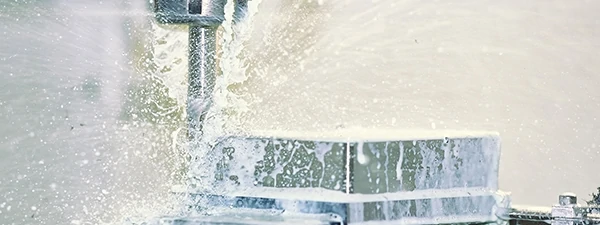
Proper coolant usage helps to control the temperature in a cutting operation. Machinists generally choose between using Flooding or High Pressure Coolant options. Flooding the workpiece with coolant may be necessary to maintain the proper temperature, especially when machining in stainless steels and high-temp alloys. This low pressure method creates lubricity to flush chips and avoid chip recutting which commonly damages cutting tools.

high pressure coolant spraying on a part and workpiece during a cnc cutting operation

On the other hand, high pressure coolant delivers enhanced levels of chip evacuation and instant cooling of a part. However, one must be cautious of potentially breaking miniature diameter tooling when using this method due to the higher pressures. Coolant-fed tools can also help to reduce the heat at the contact point, lessening work hardening. While coolant-fed tools are typically a custom modification, saving parts from the scrap heap and using more machine time for the placement part will see the tool pay for itself over time.

https://www.harveyperformance.com/wp-content/uploads/2017/10/Featured-Image-Work-Hardening-Should-Scare-You-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-10-30 16:00:482023-11-10 14:17:50Work Hardening and When it Should Scare You

Key Tool Holding Considerations

September 5, 2017/0 Comments/in CNC Machining, Getting Started, Machining 101, Machining Techniques, Tools In Action, Troubleshooting Tips/by Harvey Performance Company

Each tool holder style has its own unique properties that must be considered prior to beginning a machining operation. A secure machine-to-tool connection will result in a more profitable shop, as a poor connection can cause tool runout, pull-out, scrapped parts, damaged tools, and exhausted shop resources. An understanding of tool holders, shank features, and best practices is therefore pivotal for every machinist to know to ensure reliable tool holding.

Types of Tool Holding

The basic concept of any tool holder is to create a compression force around the cutting tool’s shank that is strong, secure, and rigid. These come in a variety of styles, each with its own spindle interface, taper for clearance, and compression force methods.

Mechanical Spindle Tightening

The most basic way in which spindle compression is generated is by simple mechanical tightening of the holder itself, or a collet within the holder. The downside of this mechanical tightening method of the spindle is its limited number of pressure points. With this style, segments of a collet collapse around the shank, and there is no uniform, concentric force holding the tool around its full circumference.

end mill in tool holder within a cnc machine

Hydraulic Tool Holders

Other methods create a more concentric pressure, gripping the tool’s shank over a larger surface area. Hydraulic tool holders create this scenario. They are tightened via a pressurized fluid inside the bore of the holder, creating a more powerful clamping force on the shank.

Shrink Fit Tool Holders

Shrink fit tool holders are another high quality tool holding mechanism. This method works by using the thermal properties of the device to expand its opening slightly larger than the shank of the tool. The tool is placed inside the holder, after which the holder is allowed to cool, contracting down close to its original size and creating a tremendous compressive force around the shank. Since the expansion of the bore in the tool holder is minuscule, a tight tolerance is needed on the shank to ensure it can fit every time. Shank diameters with h6 tolerances ensure the tool will always work properly and reliably with a shrink fit holder.

A post shared by Helical Tool (@helicaltools) on Aug 9, 2017 at 5:42am PDT

Types of Shank Modifications

Along with choosing correctly when it comes to tool holding options, tool shanks can be modified to promote a more secure machine-to-tool connection. These modifications can include added grooves on the shank, flats, or even an altered shank surface to aid in gripping strength.

Weldon Flats

A Weldon flat can be used to create additional strength within the tool holder. The tool holder locks a tool in place with a set screw pushing on a flat area on the tool shank. Weldon flats offer a good amount of pull-out prevention due to the set screw sitting in the recessed shank flat. Often seen as an outdated method of tool holding, this method is most effective for larger, stronger tools where runout is less of a concern.

ToughGRIP Shanks

Helical Solutions offers a ToughGRIP shank modification to its customers, which works by increasing the friction of the shank – making it easier to grip for the tool holder. This modification roughs the shank’s surface while maintaining h6 shrink fit tolerance.

Haimer Safe-Lock™

In the Haimer Safe-Lock system, special drive keys in the chuck interface with grooves in the shank of the tool to prevent pull-out. The end mill effectively screws into the tool holder, which causes a connection that only becomes more secure as the tool is running. Haimer Safe-Lock™ maintains h6 shank tolerances, ensuring an even tighter connection with shrink fit holders.

haimer safe-lock tool holder up close

Key Takeaways

While choosing a proper cutter and running it at appropriate running parameters are key factors to a machining operation, so too is the method used. If opting for an improper tool holding method, one can experience tool pull-out, tool runout, and scrapped jobs. Effective tool holding will prevent premature tool failure and allow machinists to feel confident while pushing the tool to its full potential.

https://www.harveyperformance.com/wp-content/uploads/2017/09/Feature-Image-Tool-Holder-Considerations-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-09-05 16:54:202024-02-12 11:21:42Key Tool Holding Considerations
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top