Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Machining Precious Metals

July 1, 2019/10 Comments/in How-To's, Machining Techniques, Material Specific/by Robert Keever

Precious metals can be particularly difficult to machine due to their wide range of material properties and high cost if a part has to be scrapped. The following article will introduce these elements and their alloys as well as provide a guide on how to machine them effectively and efficiently.

About the Elements

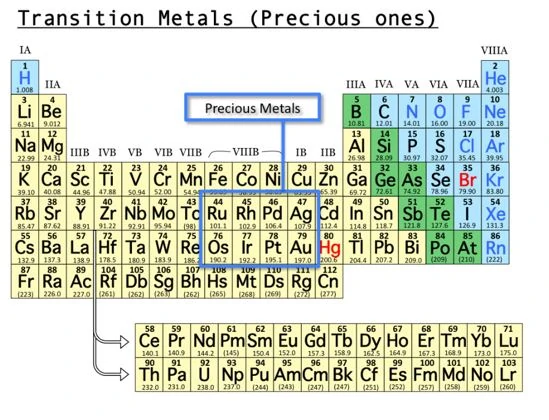
Sometimes called “noble” metals, precious metals consist of eight elements that lie in the middle of the periodic table (seen below in Figure 1). The eight metals are:

  1. Ruthenium (Ru)
  2. Rhodium (Rh)
  3. Palladium (Pd)
  4. Silver (Ag)
  5. Osmium (Os)
  6. Iridium (Ir)
  7. Platinum (Pt)
  8. Gold (Au)

These elements are some of the rarest materials on earth, and can therefore be enormously expensive. Gold and silver can be found in pure nugget form, making them more easily available. However, the other six elements are typically found mixed in the raw ore of the four metals they sit below on the periodic table: Iron (Fe), Cobalt (Co), Nickel (Ni), and Copper (Cu). These elements are a subset of precious metals and are generally called Platinum Group Metals (PGM). Because they are found together in raw ore, this makes mining and extraction difficult, dramatically increasing their cost. Because of their high price tag, machining these materials right the first time is incredibly important to a shop’s efficiency.
periodic table with a box around the 8 precious metals

Figure 1: Periodic table with the 8 precious metals boxed in blue. Image source: clearscience.tumblr.com

Basic Properties and Compositions of Precious Metals

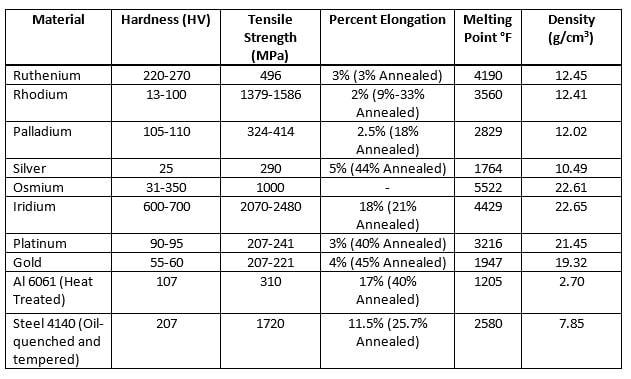
Precious metals have notable material properties as they are characteristically soft, ductile, and oxidation resistant. They are called “noble” metals because of their resistance to most types of chemical and environmental attack. Table 1 lists a few telling material properties of precious metals in their elemental form. For comparison purposes, they are side-by-side with 6061 Al and 4140 Steel. Generally, only gold and silver are used in their purest form as the platinum group metals are alloys that consist mainly of platinum (with a smaller composition of Ru, Rh, Pa, Os, Ir). Precious metals are notable for being extremely dense and having a high melting point, which make them suitable for a variety of applications.

Table 1: Cold-worked Material Properties of Precious Metals, 4140 Steel and 6061 Aluminum 
material properties of precious metals in relation to 6061 and 4140

Common Machining Applications of Precious Metals

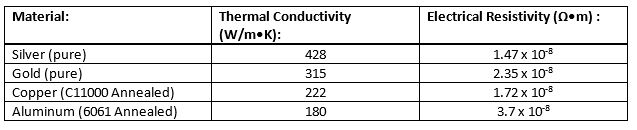
Silver and gold have particularly favorable thermal conductivity and electrical resistivity. These values are listed in Table 2, along with CC1000 (annealed copper) and annealed 6061 aluminum, for comparison purposes. Copper is generally used in electrical wiring because of its relatively low electrical resistivity, even though silver would make a better substitute. The obvious reason this isn’t the general convention is the cost of silver vs. copper. That being said, copper is generally plated with gold at electrical contact areas because it tends to oxide after extended use, which lowers its resistivity. As stated before, gold and the other precious metals are known to be resistant to oxidation. This corrosion resistance is the main reason that they are used in cathodic protection systems of the electronics industry.

Table 2: Thermal Conductivity and Electrical Resistivity of Ag, Au, Cu, and Al 
thermal conductivity of silver, gold, copper, and aluminum

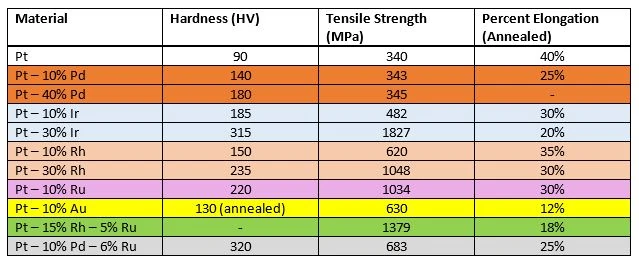
Platinum and its respective alloys offer the most amount of applications as it can achieve a number of different mechanical properties while still maintaining the benefits of a precious metal (high melting point, ductility, and oxidation resistance). Table 3 lists platinum and a number of other PGMs each with their own mechanical properties. The variance of these properties depends on the alloying element(s) being added to the platinum, the percentage of alloying metal, and whether or not the material has been cold-worked or annealed. Alloying can significantly increase the tensile strength and hardness of a material while decreasing its ductility at the same time. The ratio of this tensile strength/hardness increase to ductility decrease depends on the metal added as well as how much is added, as seen in Table 3. Generally this depends on the particle size of the element added as well as its natural crystalline structure. Ruthenium and Osmium have a specific crystal structure that has a significant hardening effect when added to platinum. Pt-Os alloys in particular are extremely hard and practically unworkable, which doesn’t yield many real-world applications. However, the addition of the other 4 PGMs to platinum allow for a range of mechanical properties with various usages.

Table 3: PGM material properties (Note: the hardness and tensile strength are cold worked values) 
pgm material properties

Platinum and its alloys are biocompatible, giving them the ability to be placed in the human body for long periods of time without causing adverse reactions or poisoning. Therefore, medical devices including heart muscle screw fixations, stents, and marker bands for angioplasty devices are made from platinum and its alloys. Gold and palladium are also commonly used in dental applications.

Pt-Ir alloys are noticeably harder and stronger than any of the other alloys and make excellent heads for spark plugs in the automobile industry. Rhodium is sometimes added to Pt-Ir alloys to make the material less springy (as they are used as medical spring wire) while also increasing its workability. Pt and Pt-Rh wire pairs are extremely effective at measuring temperatures and are therefore used in thermocouples.

Machining Precious Metals

The two parameters that have the most effect when machining are hardness and percent elongation. Hardness is well-known by machinists and engineers across the manufacturing industry as it indicates a material’s resistance to deformation or cutting. Percent elongation is a measurement used to quantify material ductility. It indicates to a designer the degree to which a structure will deform plastically (permanently) before fracture. For example, a ductile plastic such as ultrahigh molecular weight polyethylene (UHMWPE) has a percent elongation of 350-525%, while a more brittle material such as oil-quenched and tempered cast iron (grade 120-90-02) has a percent elongation of about 2%. Therefore, the greater the percent elongation, the greater the material’s “gumminess.” Gummy materials are prone to built-up edge and have a tendency to produce long stringy chips.

Tools for Precious Metals

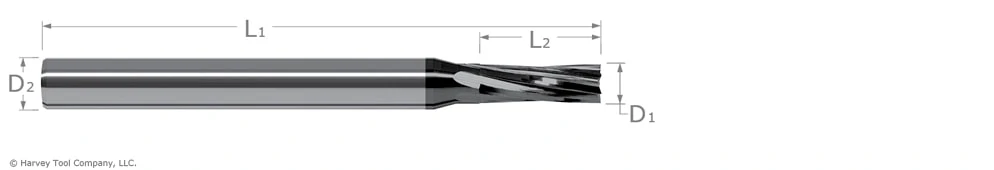
Material ductility makes a sharp cutting tool essential for cutting precious metals. Variable Helix for Aluminum Alloy tools can be used for the softer materials such as pure gold, silver, and platinum.

variable helix square aluminum end mill from harvey tool

Figure 2: Variable Helix Square End Mill for Aluminum Alloys

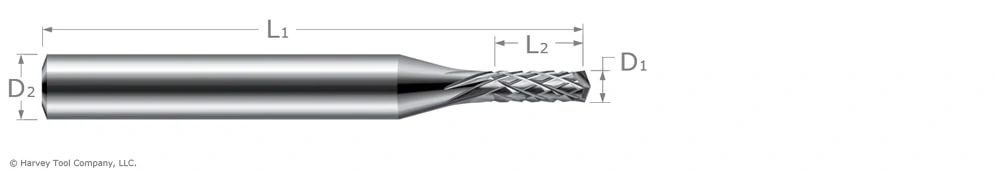
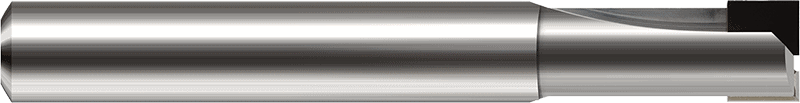
Higher hardness materials still require a sharp cutting edge. Therefore, one’s best option is to invest in a PCD Diamond tool. The PCD wafer has the ability to cut extremely hard materials while maintaining a sharp cutting edge for a relatively long period of time, compared to standard HSS and carbide cutting edges.
harvey tool pcd diamond square end mill

Figure 3: PCD Diamond Square End Mill

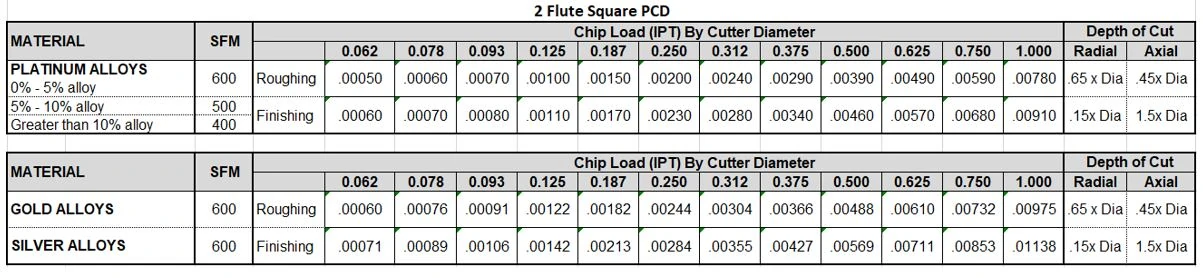
Speeds and Feeds charts:

speeds and feeds chart for precious metals

Figure 4: Speeds and Feeds for precious metals when using a Square Non-ferrous, 3x LOC
speeds and feeds chart for precious metals with a pcd end mill

Figure 5: Speeds and Feeds for precious metals when using a 2-Flute Square PCD end mill
https://www.harveyperformance.com/wp-content/uploads/2020/07/Machining-Precious-Metals.jpg 600 1599 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2019-07-01 12:58:512023-10-24 10:50:51Machining Precious Metals

What to Know About Helical Solution’s Zplus Coating

April 1, 2019/0 Comments/in Aluminum, CNC Machining, Helical Solutions, Machining Techniques, Material Specific, Tool Coatings, Tool Selection/by Harvey Performance Company

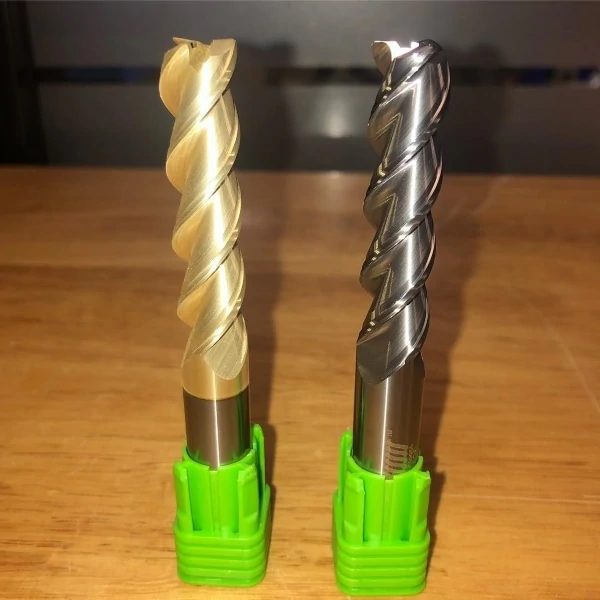
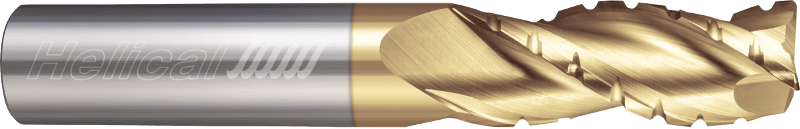
Non-ferrous and non-metallic materials are not usually considered difficult to machine, and therefore, machinists often overlook the use of tool coatings. But while these materials may not present the same machining difficulties as hardened steels and other ferrous materials, a coating can still vastly improve performance in non-ferrous applications. For instance, materials such as aluminum and graphite can cause machinists headaches because of the difficulty they often create from abrasion. To alleviate these issues in non-ferrous machining applications, a popular coating choice is Helical Solution’s Zplus coating.

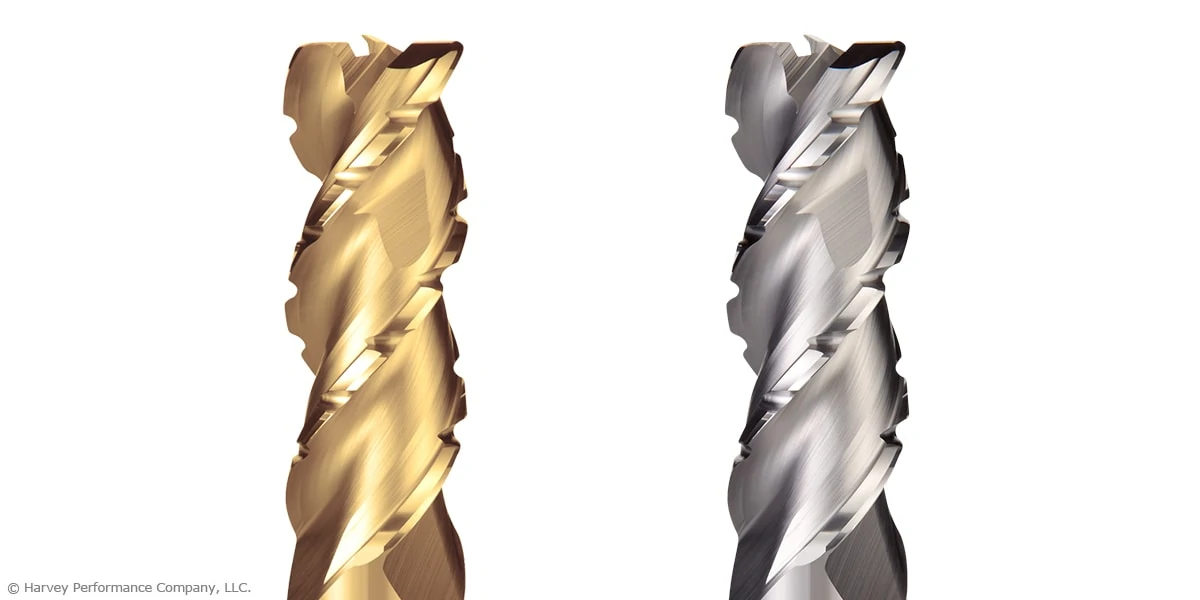
zplus coated helical chipbreaker end mill
What is Helical Solutions’ Zplus Coating?

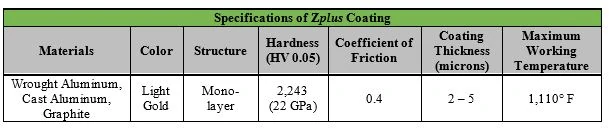
Helical’s Zplus is a Zirconium Nitride-based coating, applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a vacuum and forms layers only microns thick onto the properly prepared tool. Zirconium Nitride does not chemically react to a variety of non-ferrous metals, increasing the lubricity of the tool and aiding in chip evacuation.

zplus coating specification chart

When Should a Machinist Use Helical Solution’s Zplus?

Working with Abrasive Materials

While Zplus was created initially for working in aluminum, its hardness level and maximum working temperature of 1,110°F enables it to work well in abrasive forms of other non-ferrous materials, as well. This coating decreases the coefficient of friction between the tool and the part, allowing it to move easier through more abrasive materials. This abrasion resistance decreases the rate of tool wear, prolonging tool life.

Concerns with Efficient Chip Evacuation

One of the primary functions of this coating is to increase the smoothness of the flutes of the tool, which allows for more efficient chip removal. By decreasing the amount of friction between the tool and the material, chips will not stick to the tool, helping to prevent chip packing. The increased lubricity and smoothness provided by the coating allows for a higher level of performance from the cutting tool. Zplus is also recommended for use in softer, gummy alloys, as the smooth surface encourages maximum lubricity within the material – this decreases the likelihood of those gummier chips sticking to the tool while machining.

Large Production Runs

Uncoated tools can work well in many forms of non-ferrous applications. However, to get a genuinely cost-effective tool for your job, the proper coating is highly recommended. Large production runs are known for putting a lot of wear and tear on tools due to their increased use, and by utilizing an appropriate coating, there can be a significant improvement in the tools working life.

3 flute corner radius end mill for aluminum
When is Zplus Coating Not Beneficial to My Application?

Finishing Applications

When your parts finish is vital to its final application, a machinist may want to consider going with an uncoated tool. As with any coating, ZrN will leave a very minor rounded edge on the tip of the cutting edge. The best finish often requires an extremely sharp tool, and an uncoated tool will have a sharper cutting edge than its coated version.

https://www.harveyperformance.com/wp-content/uploads/2019/04/Feature-Image-Zplus-Coatings-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-04-01 03:17:542023-10-24 10:53:44What to Know About Helical Solution’s Zplus Coating

What to Know About Harvey Tool’s TiB2 Coating

March 8, 2019/0 Comments/in Aluminum, CNC Machining, Harvey Tool, Material Specific, Milling, Tool Coatings, Tool Selection/by Harvey Performance Company

Aluminum and magnesium alloys are common materials found in machine shops worldwide, and are known as an “easier” material to machine. However, machinists can still experience hiccups while machining this material if they are not prepared with the proper tooling.. When working with aluminum and magnesium alloys, it is important to choose a coating that will work to extend your tool’s life and aid in the removal of chips. A popular choice for this material bucket is Harvey Tool’s TiB2 coating.

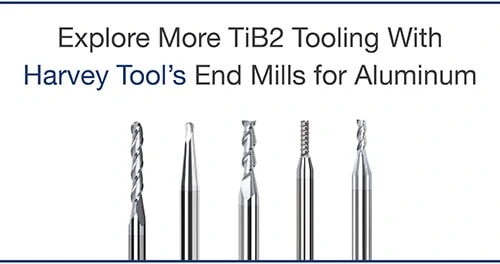
Explore More TiB2 Tooling With Harvey Tool’s End Mills for Aluminum

What is Harvey Tool’s TiB2 Coating?

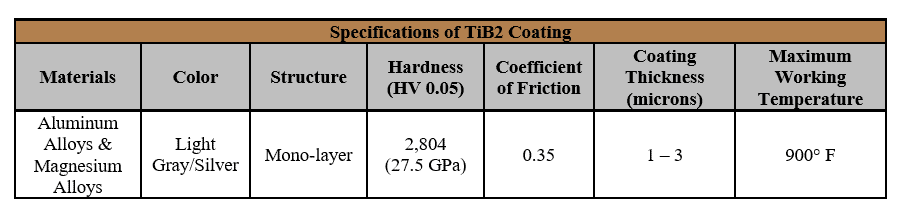
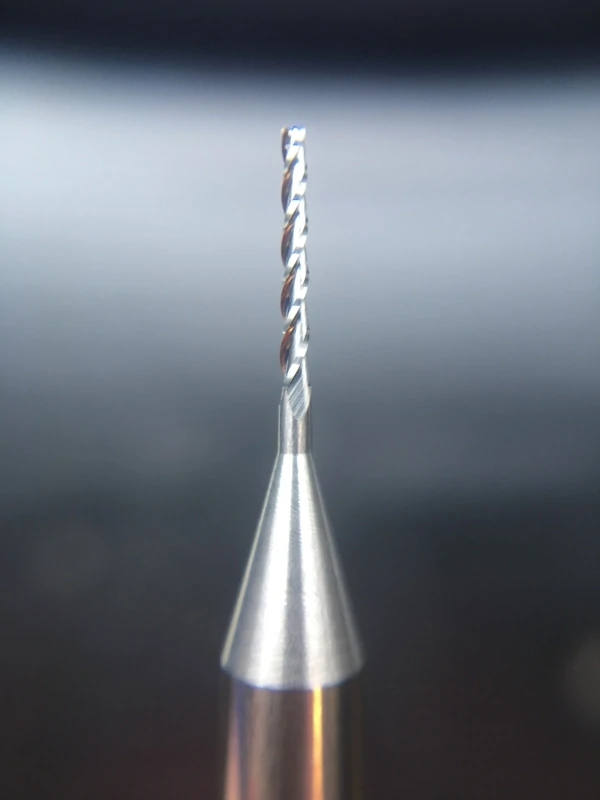
Harvey Tool’s TiB2 coating is a Titanium Diboride, ceramic-based coating that provides superb erosion resistance during machining. TiB2 is added to a tool by a method called Physical Vapor Deposition (PVD), which is conducted in a vacuum where particles are vaporized and applied onto a surface, forming thin layers of material onto the properly-prepped tool. This method enables the coating to be corrosion and tarnish resistant.

TiB2 Coating Specification chart

TiB2 is identified in Harvey Tool’s product catalog with a “-C8” following the sku number. It can be found offered in Harvey Tool’s lines of Variable Helix End Mills for Aluminum Alloys and Miniature High Performance Drills for Aluminum Alloys.

When Should a Machinist Use TiB2 Coating?

Chip Evacuation Concerns

TiB2 has an extremely low affinity to aluminum, which helps with the chip evacuation process. Simply, chips of a material are able to evacuate through chip valleys easier if they don’t have a high affinity to the coating being used. TiB2 coating does not chemically react with aluminum and magnesium, which allows for smoother chip evacuation, as the chips do not stick to the coating and create issues such as chip packing. This is a common machining mishap that can cause both part and tool damage, quickly derailing a machining operation. By using a coating that increases the lubricity of the tool, chips will not have a surface to stick to and will more smoothly evacuate from the flutes of the tool.

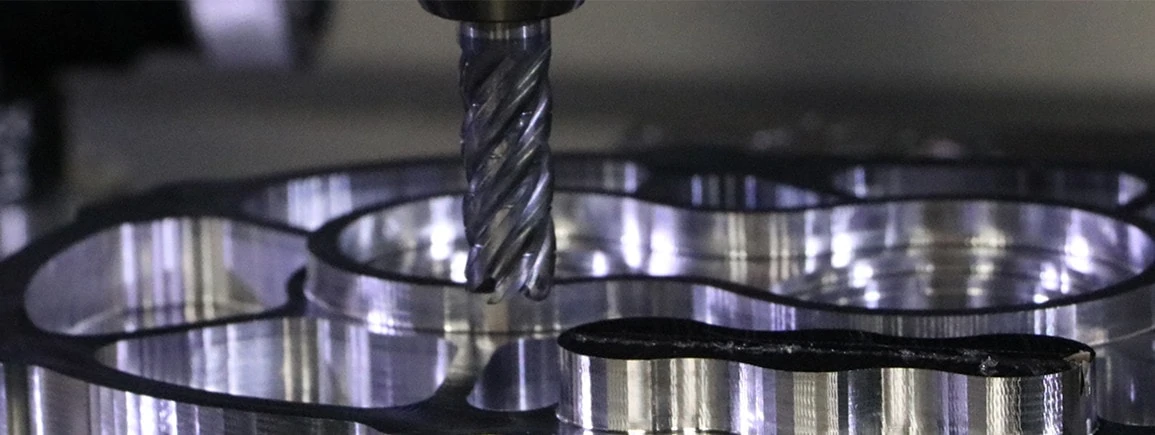
tib2 coated cnc end mill
Large Production Runs

While an uncoated tool may work fine in some applications, not all applications can succeed without a tool coating. When working with large production runs where the tools need to hold up through the process of machining large numbers of parts, using a coating is always recommended because they extend the life of your tool.

When is TiB2 Coating Not Beneficial to My Application?

Extremely Abrasive Materials

During the PVD coating process, tools can reach a temperature in excess of 500° F, which can cause the toughness of the carbide to drop slightly. This process does not normally compromise the performance of the tool due to the coating being placed over the carbide. The coating then protects the slightly weakened edge and increases tool performance in recommended materials. Micro-fractures only start appearing when the tool is being run incredibly fast through highly abrasive materials, leading to a decrease in the life of the tool.

Extremely Soft Materials

The coating, while only a few microns thick at most, still provides an ever-so-slight rounded edge to the cutting edge of the tools it is placed on. It is important to take this into consideration, as using the sharpest tools possible when working with materials such as soft plastics is recommended. The sharpest edge possible decreases the likelihood of any “pushing” that might occur on the material and increases the likelihood of proper “shearing” when machining.

When Finish Is Vital

If your part’s finish is imperative to the final product, an uncoated tool may work better for your application. A coating, like stated above, creates a microscopic rounded surface to the cutting edge of the tool. When running tools at finishing speeds and feeds in materials like aluminum, a sharp edge can create the difference between a finished part that does – or does not – pass final inspection.

https://www.harveyperformance.com/wp-content/uploads/2019/03/Feature-Image-TiB2-Coatings-IMG-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-03-08 09:14:352023-10-24 10:54:05What to Know About Harvey Tool’s TiB2 Coating

How Material Specific Tooling Pays Off

February 1, 2019/0 Comments/in CNC Machining, Harvey Tool, Machining 101, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Harvey Performance Company

A machinist is faced with many questions while selecting the proper tool for their job. One key decision that must be made is whether a material specific tool is appropriate and necessary for the application that’s going to be performed – whether the benefits of using this type of tool outweigh the higher price tag than that of a tool designed for use in a variety of materials. There are four main categories to consider when deciding whether a material specific tool is your best bet: internal tool geometry, coatings, material removal rates (MRR), and cost.

When to Utilize Material Specific Tooling

Are you a machinist in a shop that deals primarily with one type of material? Or, do you generally change materials frequently throughout the day? Further, how many parts do you make at a time? These are questions you must ask yourself prior to making a tooling decision.

Material Specific Tooling is best utilized where several parts are being machined of the same material. For instance, if your shop is machining 1,000 plastic parts, it would be in your best interest to opt for a tool designed for this material as your tooling would not only last longer but perform better. If machining flexibility is paramount for your shop, if you’re only machining a few parts, or if part finish is not of high importance, a regular end mill may suffice.
Pros and Cons of Material Specific Tooling

There are pros and cons to purchasing a Material Specific Tool.

Pros:

  • Tool geometry designed for the material you’re working in to achieve the best results.
  • Coating optimized for the material you’re cutting.
  • More aggressive speeds and feeds, and boosted MRR as a result.
  • Increased tool life.

Cons:

  • Higher upfront cost, though long term savings are possible if used in proper situations.
  • Less opportunity for flexibility. While most end mills may be suitable for use in many jobs and many machines, Material Specific End Mills are engineered for use in specific materials

Special Benefits of Material Specific Tooling

A Unique Internal Tool Geometry

Many manufacturers supply tooling designed for use in specific material buckets. For instance, Harvey Tool has distinct catalog sections for material specific tooling for Hardened Steels, Exotic Alloys, Medium Alloy Steels, Free Machining Steels, Aluminum Alloys, Plastics, Diamond Tooling for Non-Ferrous Materials, and Composites. The special geometry of tools found in these sections is optimized to allow the tool to perform optimally in its select material group.

For instance, a machinist may be faced with a dilemma while preparing to machine a plastic part. While an end mill found in Harvey Tool’s Miniature End Mill section could certainly machine this material, Harvey Tool’s end mill offering designed to machine plastics feature a high rake, high relief design. This is ideal for plastics because you want to effectively cut and form chips while the strength of the tool is less of a concern. The high rake and high relief creates a sharp cutting edge that would quickly break down in metals. However, in plastics, this effectively shears the material and transfers the heat into the chip to produce a great finish in your part.
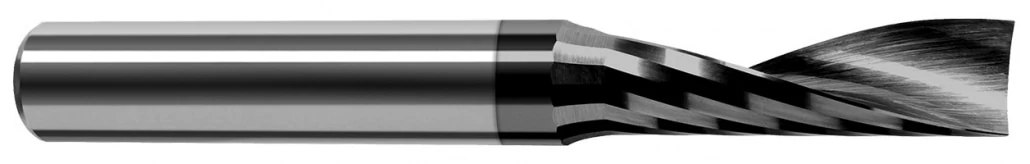
single flute end mill for pastics
Harvey Performance Company, LLC.

Specific Coatings & Substrates for Optimal Performance

One key benefit of opting for a material specific tool is the ability to utilize the best coating option available for that material. Tool coatings serve many functions, including improved lubricity, increased tool life, and a higher-quality part finish. In addition, coated tools can typically be run around 10% faster than uncoated tools.

While many manufacturers will specially coat a standard end mill at your request, this takes added time and cost. In its Material Specific catalog sections, Harvey Tool offers coated tools stocked and ready to ship. For instance, their Hardened Steels and Exotic Alloys categories utilize AlTiN Nano coating. This is a unique nanocomposite coating that has a max working temperature of 2,100° F and shows improved performance in materials such as Hardened Steels, Titanium Alloys, and Inconel, among others.

Increased Material Removal Rates

Because Material Specific Tooling features optimal tool geometry for a job, running parameters are generally able to be more aggressive. Any machinist knows that Material Removal Rates (MRR), is the metric that’s most closely related to shop efficiency, as the more material removed from a part in a given period of time, the faster parts are made and the higher the shop output.

The following example compares running parameters of end mills from Harvey Tool’s Miniature End Mill and Material Specific End Mill Sections. You can notice that while key geometries between the two tools are identical, and are in use in the same material with the same operation, the chip load (+25%), linear feed rate (+33%), and depth of cut (+43%) are boosted. This allows for more material to be removed in a shorter period of time.

Miniature End Mill

Part Number: 836408

Description: 3 Flute 1/8 inch diameter 3x LOC Square Stub & Standard

Material: 6061 Aluminum

Application: Slotting

Speed: 10,000 RPM

Chip Load: .00124 IPT

Linear Feed: 37.2 IPM

DOC: .04375

harvey tool miniature end mill

Material Specific End Mill

Part Number: 942308

Description: 3 Flute 1/8 inch diameter 3x LOC Square Variable Helix for Aluminum Alloys

Material: 6061 Aluminum

Application: Slotting

Speed: 10,000 RPM

Chip Load: .00165 IPT

Linear Feed: 49.5 IPM

DOC: .0625

harvey tool miniature variable helix end mill

Harvey Performance Company, LLC.

Extensive Cost Savings

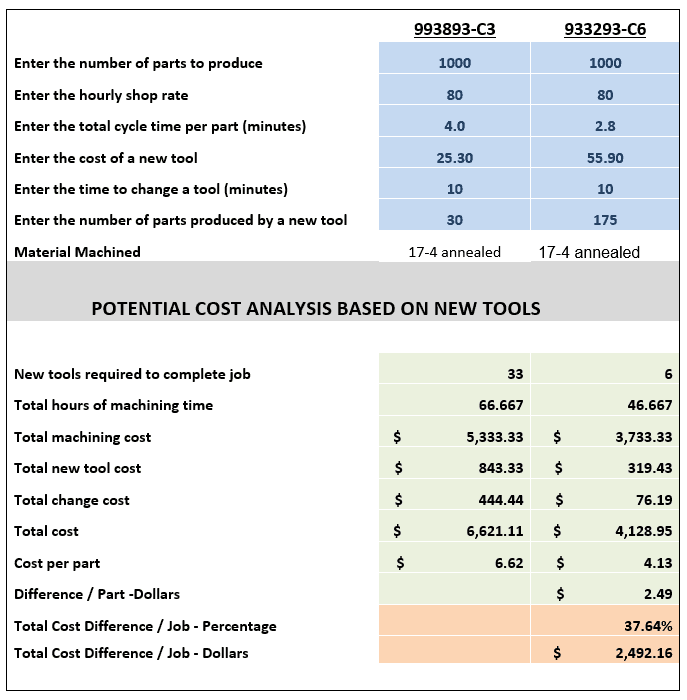
The following chart displays a cost analysis breakdown between a tool found in the Miniature End Mill section, item 993893-C3; and a tool found in the Material Specific End Mill section, item 933293-C6. When compared for the machining of 1,000 parts, the overall savings is nearly $2,500.

material specific tooling benefit chart in cost savings

Material Specific Tooling Summarized

In conclusion, Material Specific End Mills have many benefits, but are best utilized in certain situations. While the initial cost of these tools are higher, they can work to save your shop time and money in the long run by lasting longer and producing more parts over a given period of time.

https://www.harveyperformance.com/wp-content/uploads/2019/02/Feature-Image-Material-Specific-Tooling-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-02-01 08:43:172024-11-07 16:17:45How Material Specific Tooling Pays Off

Slaying Stainless Steel: Machining Guide

June 19, 2018/17 Comments/in CNC Machining, Helical Solutions, Material Specific, Tech Tips, Trending Now/by Harvey Performance Company

Stainless steel can be as common as Aluminum in many shops, especially when manufacturing parts for the aerospace and automotive industries. It is a fairly versatile material with many different alloys and grades which can accommodate a wide variety of applications. However, milling steel can also be immensely difficult. Stainless steels are notorious end mill assassins, so dialing in your speeds and feeds and selecting the proper tool is essential for machining success.

stainless steel machining

Material Properties

Stainless steels are high-alloy steels with superior corrosion resistance to carbon and low-alloy steels. This is largely due to their high chromium content, with most grades of stainless steel alloys containing at least 10% of the element.

Stainless steel can be broken out into one of five categories: Austenitic, Ferritic, Martensitic, Precipitation Hardened (PH), and Duplex. In each category, there is one basic, general purpose alloy. From there, small changes in composition are made to the base in order to create specific properties for various applications.

For reference, here are the properties of each of these groupings, as well as a few examples of the popular grades and their common uses.

CategoryPropertiesPopular GradesCommon Uses
AusteniticNon-magnetic, outstanding corrosion and heat resistance.304, 316Food processing equipment, gutters, bolts, nuts, and other fasteners.
FerriticMagnetic, lower corrosion and heat resistance than Austenitic.430, 446Automotive parts and kitchen appliances.
MartensiticMagnetic, moderate corrosion resistance – not for severe corrosion.416, 420, 440Knives, firearms, surgical instruments, and hand tools.
Precipitation Hardened (PH)Strongest grade, heat treatable, severe corrosion resistance.17-4 PH, 15-5 PHAerospace components.
DuplexStronger mixture of both Austenitic and Ferritic.244, 2304, 2507Water treatment plants, pressure vessels.

Tool Selection

Choosing the correct tooling for your application is crucial when machining stainless steel. Roughing, finishing, slotting, and high efficiency milling toolpaths can all be optimized for stainless steel by choosing the correct style of end mill.

Traditional Roughing

For traditional roughing, a 4 or 5 flute end mill is recommended. 5 flute end mills will allow for higher feed rates than their 4 flute counterparts, but either style would work well for roughing applications. Below is an excellent example of traditional roughing in 17-4 Stainless Steel.

Slotting

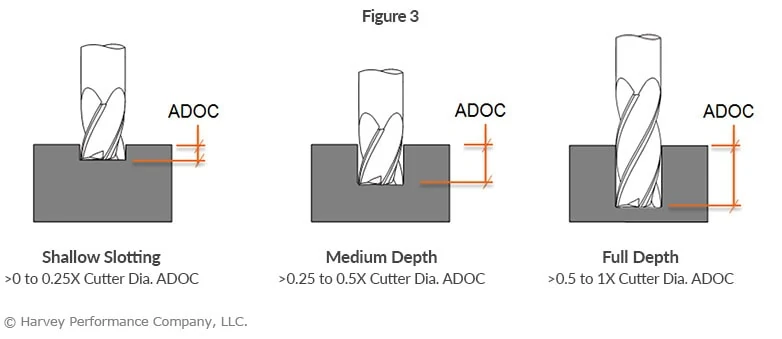
The axial engagement of a tool in a slotting operation should be suitable for the specific tool employed, as depicted in Figure 3. Employing an unsuitable method may result in tool deflection, potential damage, and compromised part quality. Chip evacuation is going to be key for slotting in stainless steel. For this reason, 4 flute tools are the best choice because the lower flute count allows for more efficient chip evacuation. Tools with chipbreaker geometry also make for effective slotting in stainless steel, as the smaller chips are easier to evacuate from the cut.

Finishing

When finishing stainless steel parts, a high flute count and/or high helix is required for the best results. Finishing end mills for stainless steel will have a helix angle over 40 degrees, and a flute count of 5 or more. For more aggressive finishing toolpaths, flute count can range from 7 flutes to as high as 14. Below is a great example of a finishing run in 17-4 Stainless Steel.

High Efficiency Milling

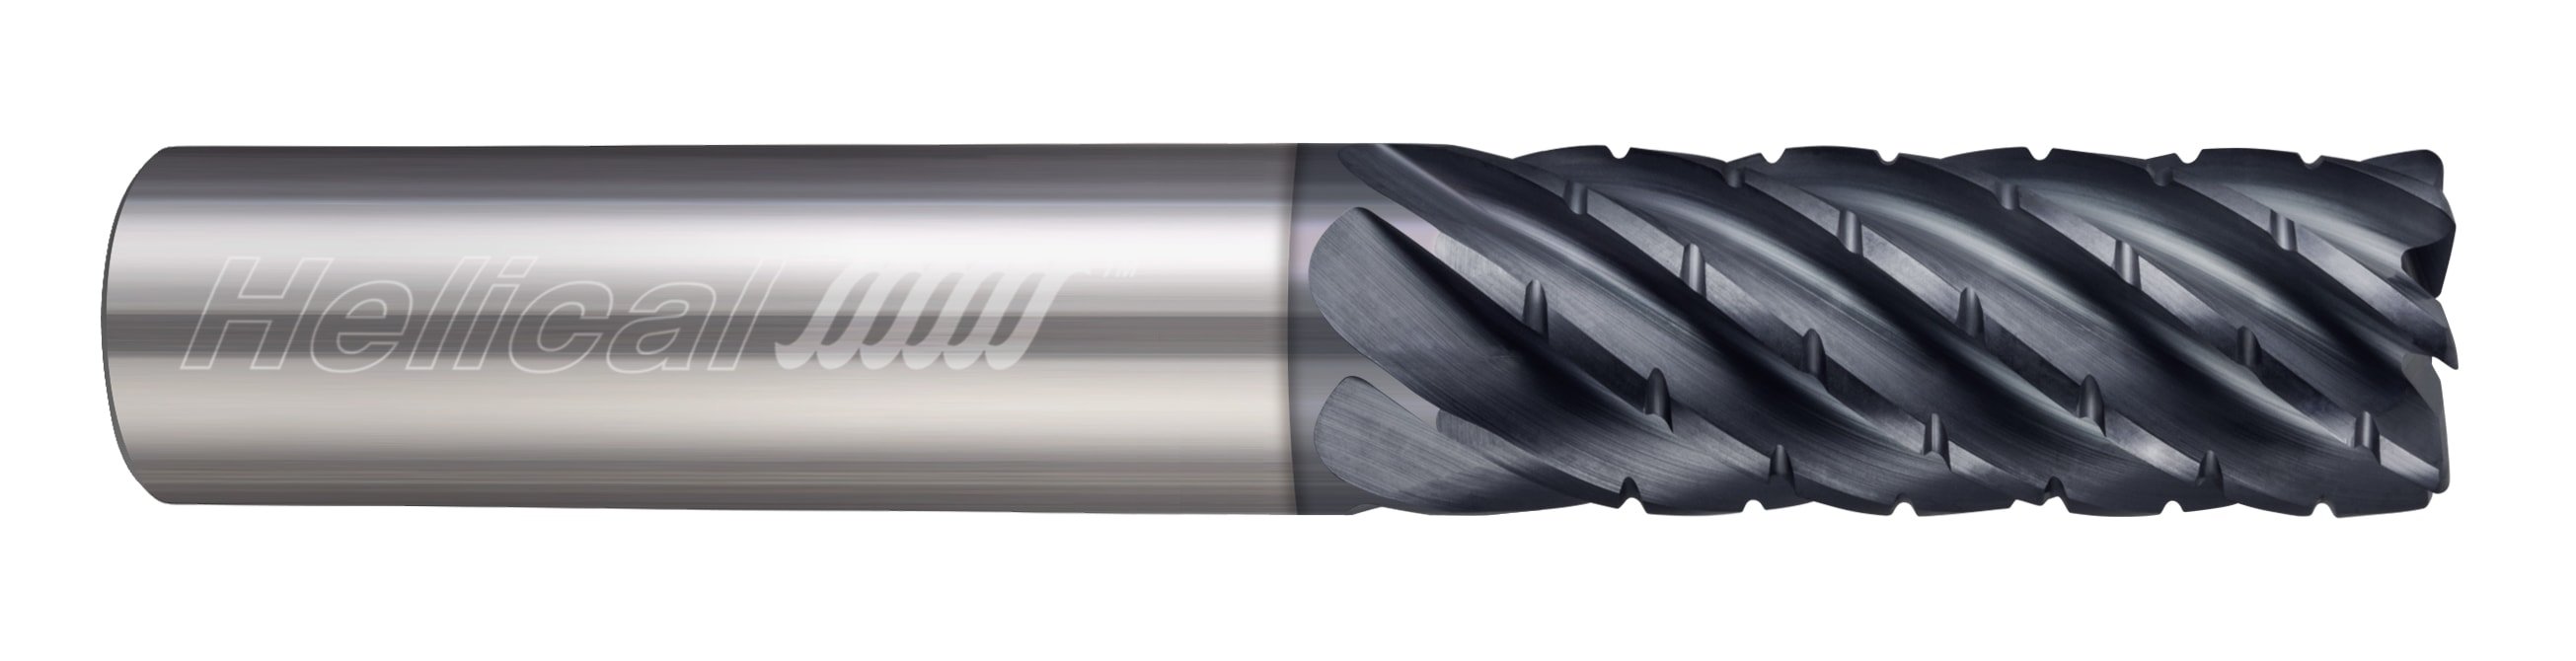
High Efficiency Milling (HEM) can be a very effective machining technique in stainless steels if the correct tools are selected. Chipbreaker roughers would make an excellent choice, in either 5 or 7 flute styles, while standard 5-7 flute, variable pitch end mills can also perform well in HEM toolpaths.

helical solutions chipbreaker end mill for hem in stainless steel

HEV-5

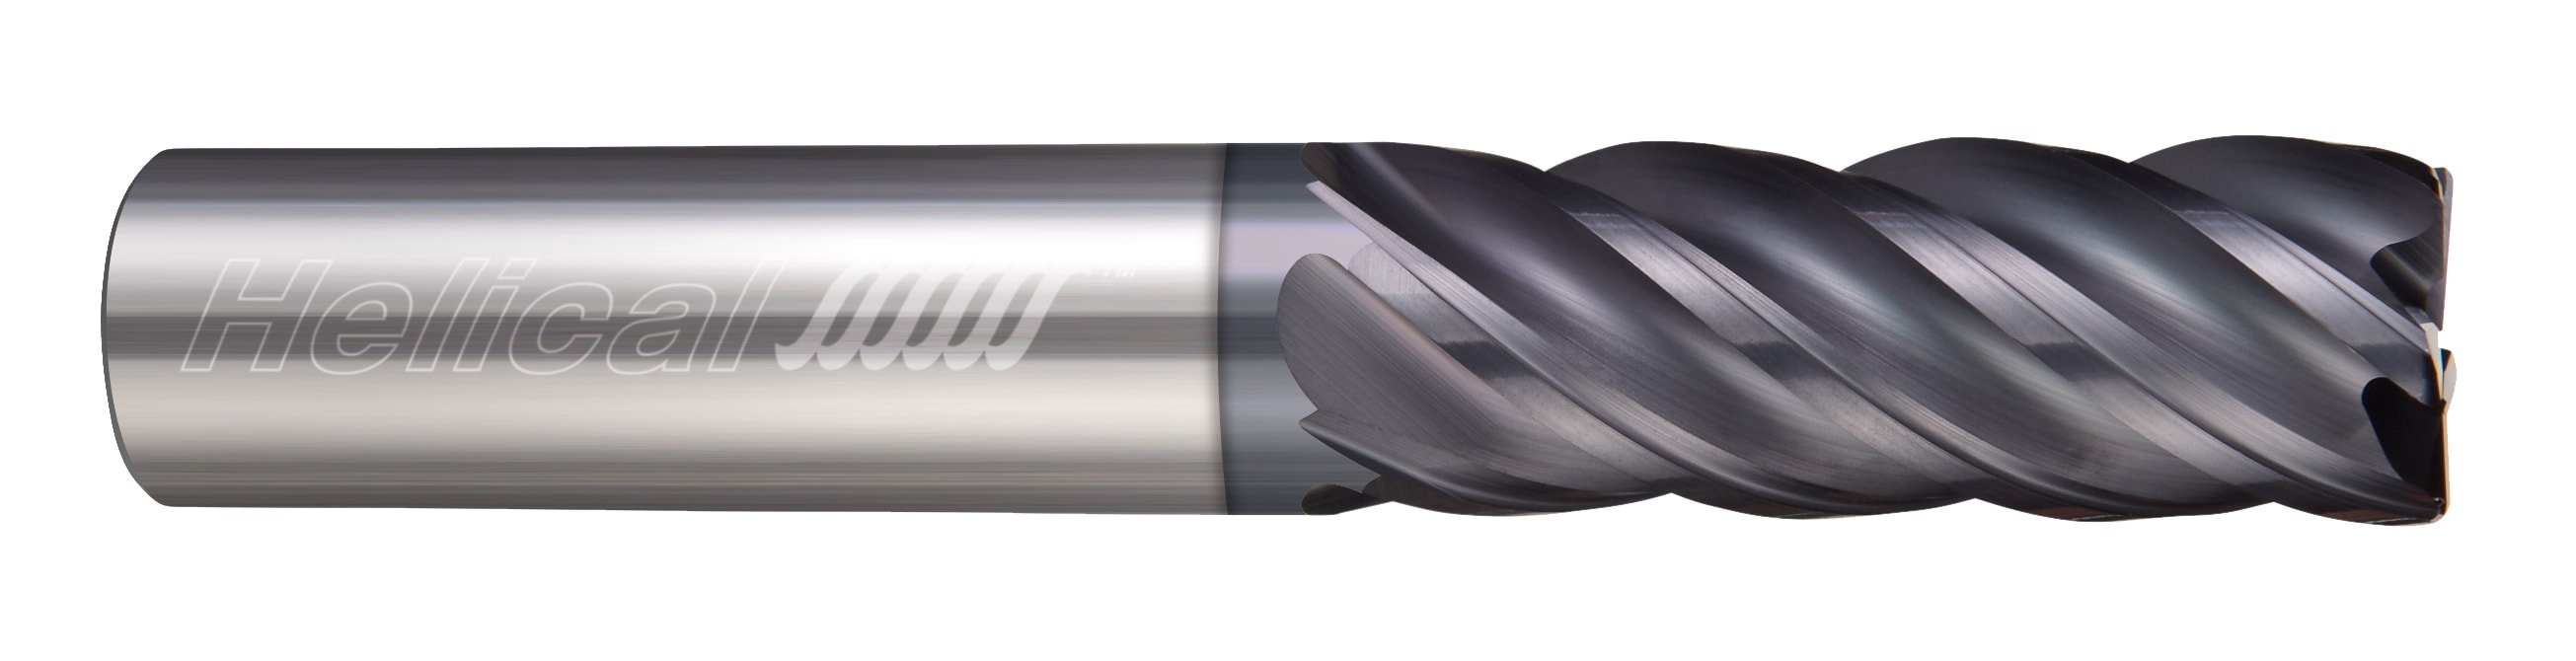
Helical Solutions offers the HEV-5 end mill, which is an extremely versatile tool for a variety of applications. The HEV-5 excels in finishing and HEM toolpaths, and also performs well above average in slotting and traditional roughing. Available in square, corner radius, and long reach styles, this well-rounded tool is an excellent choice to kickstart your tool crib and optimize it for stainless steel machining.

5 flute hem end mill for stainless steel

Running Parameters

While tool selection is a critical step to more effective machining, dialing in the proper running parameters is equally important. There are many factors that go into determining the running parameters for stainless steel machining, but there are some general guidelines to follow as a starting point.

Generally speaking, when machining stainless steels a SFM of between 100-350 is recommended, with a chip load ranging between .0005” for a 1/8” end mill up to .006” for a 1” end mill. A full breakdown of these general guidelines is available here.

Machining Advisor Pro

Machining Advisor Pro is a cutting edge resource designed to precisely calculate running parameters for high performance Helical Solutions end mills in materials like stainless steel, aluminum, and much more. Simply input your tool, your exact material grade, and machine setup and Machining Advisor Pro will generate fully customizable running parameters. This free resource allows you to push your tools harder, faster, and smarter to truly dominate the competition.

machining advisor pro ad

Dial In Your Stainless Steel Machining Application With Helical Solutions’ Machining Advisor Pro

In Conclusion

Stainless steel machining doesn’t have to be hard. By identifying the proper material grade for each part, selecting the perfect cutting tool, and optimizing running parameters, headaches from milling steel can become a thing of the past.

https://www.harveyperformance.com/wp-content/uploads/2018/06/Feature-Image-Slaying-Stainless-Steel-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-06-19 15:30:022023-12-15 15:25:56Slaying Stainless Steel: Machining Guide

Ideal Tooling for Machining Composites

May 21, 2018/0 Comments/in CNC Machining, Composites, Material Specific, Tool Selection/by Harvey Performance Company

Composite Materials

A material is classified as a composite if it is made up of at least two unique constituents that when combined yield beneficial physical and mechanical properties for a number of different applications. A binding agent that is the matrix material is filled with either particles or fibers of a second material that act as reinforcements. The combination of strength, weight, and rigidity make composites extremely useful for the automotive, aerospace, and power generation industry. Often the matrix material of particulate-reinforced composites is some form of plastic, and the reinforcement material is either glass or carbon particles. These are sometimes called “filled plastics,” and are typically very abrasive materials. Many composites are layered with varying fiber orientations, which increase the strength of the material and are called fiber-reinforced composites.

Common Problems When Machining Composites

  1. Delamination of composite layers
  2. Uncut Fibers
  3. Fiber tear-out
  4. Uneven tool wear
  5. Poor surface finish due to “competing” materials

These problems are all caused by unique conditions created by composite materials, and can be very tricky to correct.  The simple fact of cutting a combination of multiple materials at the same time introduces many factors that make it difficult to strike the right balance of the proper tool for the job and appropriate running parameters.  The following tool styles provide solutions for a wide array of composite concerns.  Composite Drilling Applications can face the same issues, and proper drill choice can help as well.

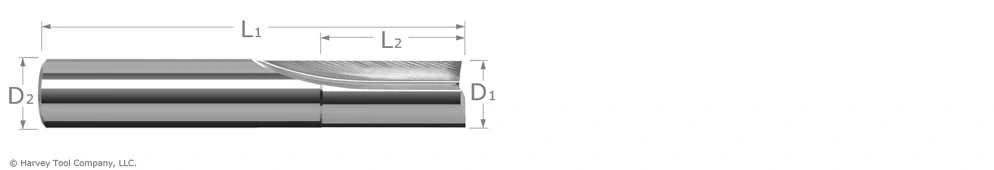
Straight Flute End Mill

Straight Flute Composite Cutters are designed to prevent delamination of layered materials by applying all cutting forces radially, eliminating axial forces from a typical helical cutting edge. Cutting action is improved with a high positive rake angle for shearing fibers and eccentric relief for improved edge life. Shallow ramping operations can be performed with this tool, but the largest benefits are seen in peripheral milling applications.

straight flute end mill

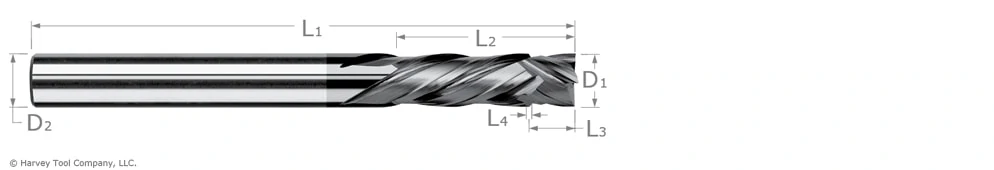
Compression Cutters

The Compression Cutter consists of an up cut and down cut helix. The top portion of the length of cut has right-hand cutting teeth with a left-hand spiral. The lower portion of the length of cut has right-hand cutting teeth with a right-hand spiral. This creates opposing cutting forces to stabilize the material removal process when cutting layered composites to prevent delamination, fiber pullout, and burs along the surface. Compression of the top and bottom of the workpiece keeps the layered bonded together.

compression cutter end mill

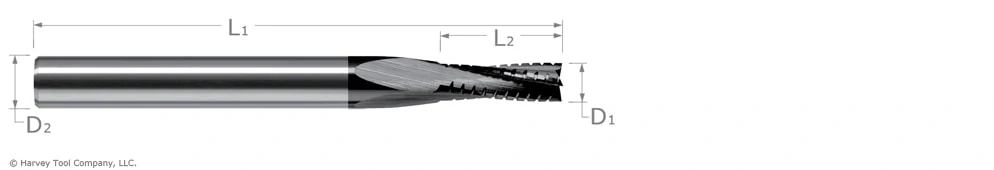
Chipbreaker Cutter

The Chipbreaker Cutter is ideally suited for roughing and profiling composites with a high percentage of fiber fill. The notch-like chipbreakers shear fibers and shorten chips for improved material evacuation. This specialized geometry is great for keeping chips small and avoiding “nesting” of stringy fibrous chips around the cutter.

chipbreaker for composite materials

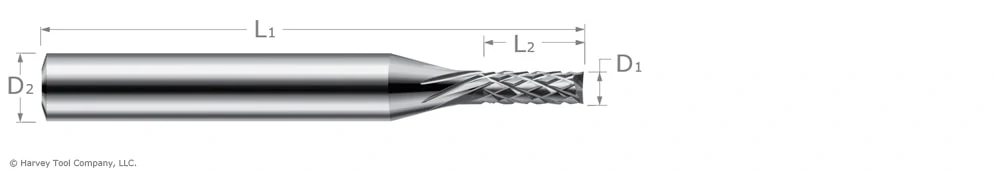
Diamond Cut End Mill

Diamond Cut Composite Cutters come in two different geometries: End Mill Style and Drill Mill Style. Although the end mill style tool is center cutting, the drill mill style has a 140° point angle, making it more suitable for plunge cutting. This is great for clearing out pockets in the middle of composite sheets.

diamond cut end mill for composites

End Mills for Composites – Diamond Cut – End Mill Style

diamond cut drill mill for composites

End Mills for Composites – Diamond Cut – Drill Mill Style

Both the end mill and drill mill style share the same downcut geometry on the outside diameter. This diamond cut tool receives its name from the combination of left-hand and right-hand teeth. The tool is predominantly a downcut style – a geometry that allows for these tools to effectively rough and profile high fiber reinforced or filled composites, breaking up chips and shearing through fibers.

Diamond Cut vs. Chipbreaker Style

The diamond cut tools have a higher flute count, which some may intuitively think would lead to a better finish, but this is not the case as this line of tools contains right-hand and left-hand teeth. There is a trade-off between an increased ability to shear fibers and leaving a poorer finish. The chipbreaker style tool, although not as effective as shearing fibers, is ultimately designed for the same purpose but leaves a better finish as all of the flutes are facing the same direction.

Composite Finisher

The Composite Finisher has optimized geometry for finishing in composite. A slow helix and high flute count for more contact points ultimately renders a smooth finish by minimizing fraying of fiber-reinforced and layered materials.

finishing end mill for composites

Coating or No Coating?

Composite materials, especially those with glass or carbon fiber, can be particularly abrasive and have a tendency to wear down the cutting edge of carbide tools. If one is looking to achieve the best tool life and maintain a sharp cutting edge, then choosing an Amorphous Diamond coated tool is the best option. This thin coating improves lubricity and wear resistance over its uncoated counterpart. Using a tool with CVD diamond coating can be very beneficial in extreme cases, when fiber fill percentage is very large. This is a true diamond coating, and offers the best abrasion resistance, but a slightly less sharp cutting edge as it is a thicker coating. PCD diamond tooling offers the best tool life. If it a solid diamond wafer brazed to a carbide shank, and can maintain the sharpest edge of any diamond tooling. However, PCD is limited to straight flutes, and can come at a higher price.

Composite materials are being increasingly utilized in today’s manufacturing world for their impressive strength to weight ratio. This growth has stimulated innovative techniques of cutting composites seen in the tool choices above. Harvey Tool’s variety of geometries helps any machine shop tackle composite cutting applications and will continue to offer groundbreaking solutions to these types of manufacturing problems.

https://www.harveyperformance.com/wp-content/uploads/2018/05/Feature-Image-Machining-Composites-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-05-21 15:10:122025-09-08 11:13:01Ideal Tooling for Machining Composites

Attacking Aluminum: a Machining Guide

April 24, 2018/11 Comments/in Aluminum, CNC Machining, Helical Solutions, Material Specific, Milling, Tech Tips/by Harvey Performance Company

Aluminum is one of the most commonly machined materials, as most forms of the material feature excellent machinability, and is thus a commonly used material in manufacturing. Because of this, the competition for aluminum machining can be intense. Understanding the basics behind tool selection, running parameters, and advanced milling techniques for aluminum can help machinists earn a competitive advantage.

Material Properties

Aluminum is a highly formable, workable, lightweight material. Parts made from this material can be found in nearly every industry. Additionally, Aluminum has become a popular choice for prototypes due to its low-cost and flexibility.

Aluminum is available in two basic forms: Cast and Wrought. Wrought Aluminum is typically stronger, more expensive, and contains a lower percentage of outside elements in its alloys. Wrought Aluminum is also more heat-resistant than Cast and has a higher level of machinability.

Cast Aluminum has less tensile strength but with a higher flexibility. It costs less, and has higher percentages of outside elements (silicon, magnesium, etc.) in its alloys, making it more abrasive than Wrought.

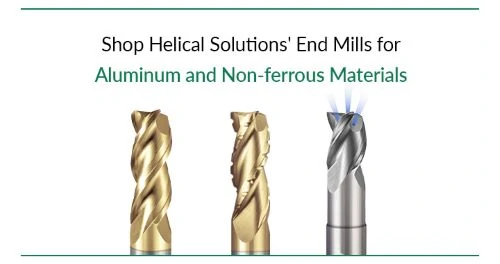
Shop Helical Solutions’ End Mills for Aluminum & Non-ferrous Materials

Tool Geometry

There are a few coating options available for Aluminum tooling, including the popular gold-colored ZrN (Zirconium Nitride) and the lesser known but highly effective TiB2 (Titanium Diboride). Uncoated tooling can also provide solid machining performance. However, the real key to high performance machining in Aluminum is knowing the proper flute count and helix angle required for your operation.

Flute Count

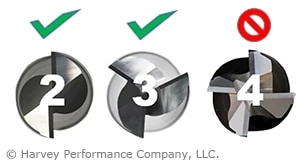
End mills for aluminum are often available in either 2 flute or 3 flute styles. With higher flute counts, it would become difficult to evacuate chips effectively at the high speeds at which you can run in aluminum. This is because aluminum alloys leave a large chip, and chip valleys become smaller with each additional flute on an end mill.

2, 3, and 4 flute count for aluminum

Traditionally, 2 flute end mills have been the preferred choice for Aluminum. However, 3 flute end mills have proven to be more successful in many finishing operations, and with the right parameters they can also work successfully as roughers. While much of the debate between 2 and 3 flute end mills for Aluminum boils down to personal preference, the operation, rigidity, and desired material removal rates can also have an effect on tool selection.

Helix Angles

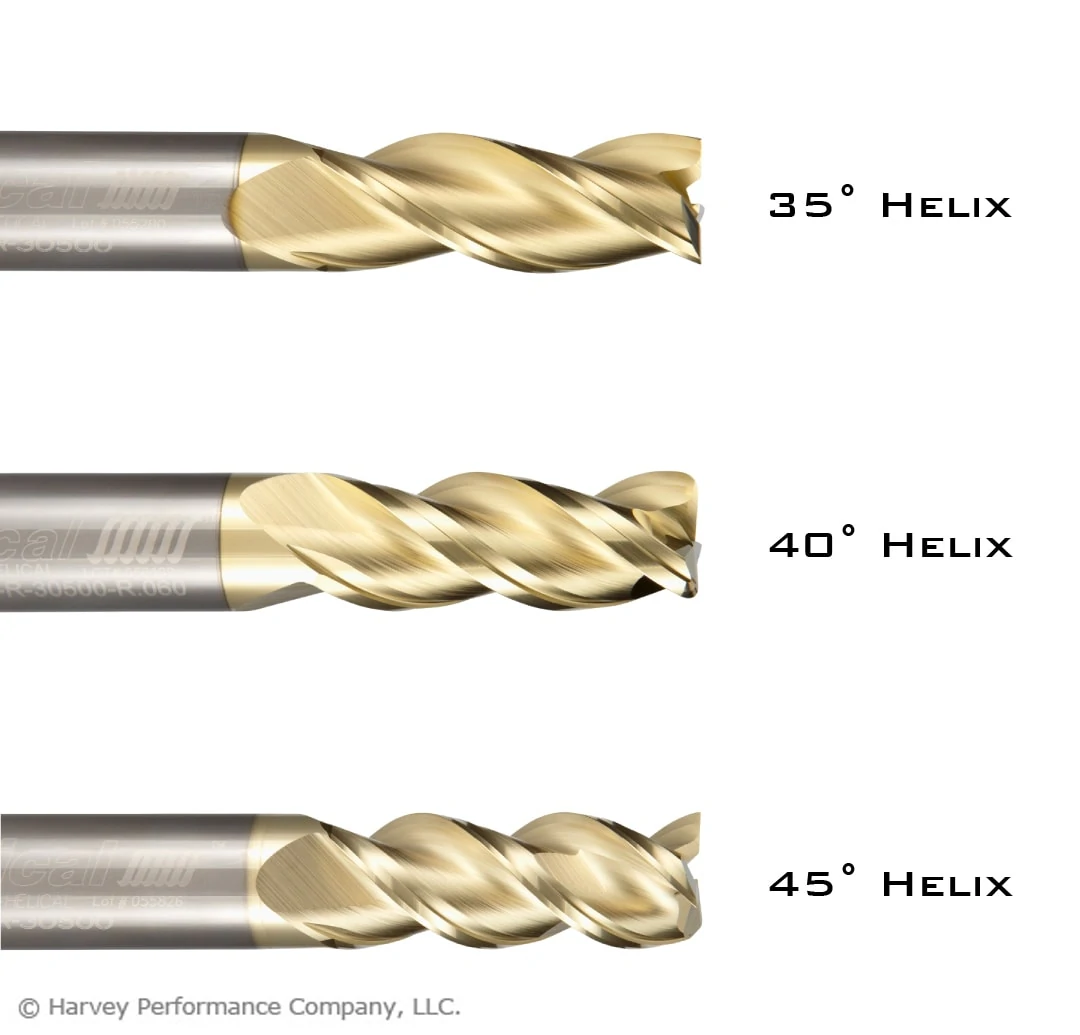
The helix angle of a tool is measured by the angle formed between the centerline of the tool and a straight line tangent along the cutting edge. Cutting tools for aluminum typically feature higher helix angles than standard end mills. Specialized helix angles for Aluminum are typically either 35°, 40°, or 45°. Variable helix tools are also available and make a great choice for reducing chatter and harmonics while also increasing material removal rates.

35, 40, and 45 degree helix choices for Aluminum Machining end mills

A helix angle of 35° or 40° is a good choice for traditional roughing and slotting applications. A 45° helix angle is the preferred choice for finishing, but also for High Efficiency Milling toolpaths as the high helix angle wraps around the tool faster and makes for a more aggressive cut.

Tooling Options

When machining aluminum, standard 2 or 3 flute tools will often get the job done. However, for certain applications and machine setups there are some more tooling options to consider for even better performance.

helical solutions end mills for aluminum and non-ferrous materials ad

Chipbreaker Tooling

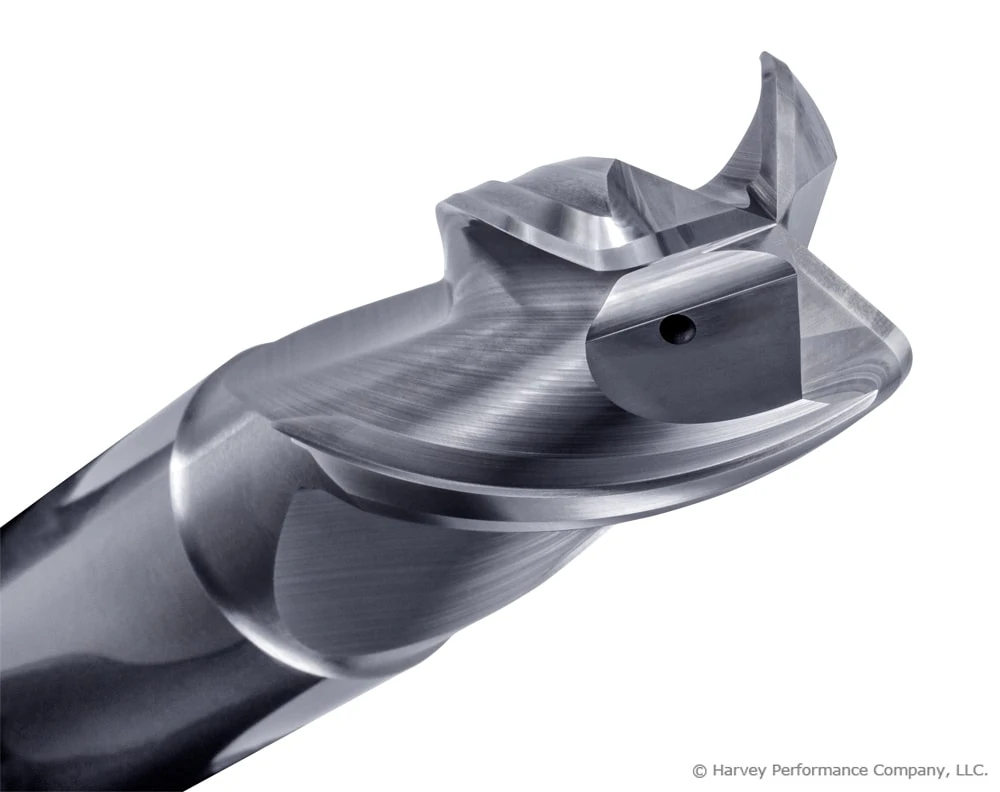
One of the most important things to consider when machining aluminum (and many other materials) is effective chip evacuation. Standard 2-3 flute end mills running at recommended speeds and feeds and proper chip loads can evacuate chips fairly well. However, 3 flute chipbreaker tooling can run at increased speed and feed rates for even better performance. The unique offset chip breaker geometry creates smaller chips for optimal evacuation while still leaving a semi-finished surface.

two Chipbreaker Aluminum end mills

These tools are excellent for more advanced toolpaths like High Efficiency Milling, which is another important tool for a successful aluminum machining experience.

High Balance End Mills

High balance end mills are designed to significantly increase performance in highly balanced machining centers capable of elevated RPMs and feed rates. These tools are precision balanced specifically for high velocity machining in aluminum (up to 33,000 RPM).

Zoomed in image of helical solutions High Balance coolant through Tool for Aluminum

Helical Solutions offers high balance tooling in standard 2 flute styles, as well as coolant-through 3 flute styles for reduced heat, enhanced chip evacuation, and increased material removal rates. These tools, like the chipbreakers, are also an excellent choice for High Efficiency Milling toolpaths.

Running Parameters

Setting the right parameters for aluminum applications is vital to optimizing productivity and achieving better machining results. Since aluminum is an easier material to machine, pushing your machine to its limits and getting the most out of your tool is vital to stay ahead of the competition and keep winning business.

While there are many factors that go into the parameters for every job, there are some general guidelines to follow when machining aluminum. For cast aluminum alloys (i.e. 308, 356, 380), a surface footage of 500-1000 SFM is recommended, with RPMs varying based on cutter diameter. The basic calculation to find a starting point for RPMs would be (3.82 x SFM) / Diameter.

In wrought aluminum alloys (i.e. 2024, 6061, 7075), a surface footage of 800-1500 SFM is recommended, with the same calculation being used to find a starting point for RPMs.

High Efficiency Milling

High Efficiency Milling, commonly known as HEM, is a strategy that is rapidly gaining popularity in the manufacturing industry. Many CAM programs are now including HEM toolpaths, and while virtually any machine can perform HEM, the CNC controller must feature a fast processor to keep up with the additional lines of code. A great example of High Efficiency Milling toolpaths in Aluminum can be seen below.

At its core, HEM is a roughing technique that utilizes a low Radial Depth of Cut (RDOC) and a high Axial Depth of Cut (ADOC) to take full advantage of the cutting edge of the tool. To learn more about how High Efficiency Milling can increase your efficiency, extend your tool life to keep costs down, and get greater performance for aluminum (and other materials), click here to download the HEM Guidebook.

In Summary

Aluminum is a versatile material with a high level of machinability, but it should not be overlooked. Understanding the best ways to tackle it is important for achieving the desired results. Optimizing your tool crib, machine setups, and toolpaths for aluminum is essential to stay ahead of the competition and make your shop more efficient.

https://www.harveyperformance.com/wp-content/uploads/2018/04/Featured-Image-Attacking-Aluminum-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-04-24 16:00:122024-11-07 16:32:38Attacking Aluminum: a Machining Guide

Work Hardening and When it Should Scare You

October 30, 2017/5 Comments/in CNC Machining, Getting Started, Machining 101, Material Specific, Troubleshooting Tips/by Harvey Performance Company

What Is Work Hardening

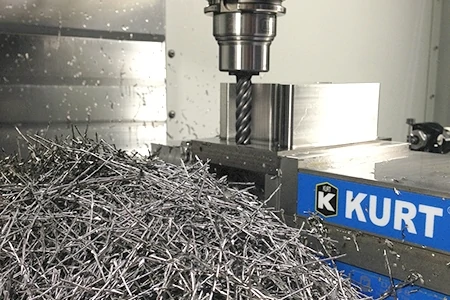
Work hardening is often an unintentional part of the machining process, where the cutting tool generates enough heat in one area to harden the workpiece. It results in plastic deformation which alters the physical structure of the metal being machined. This altered structure affects the machinability of the chosen metal and acts similarly to heat treating. When this occurs the generated speeds and feed requirements will be changed, creating a potential for inefficiency. This makes for a much more difficult machining process and can lead to scrapped parts, broken tools, and serious headaches.

Soften Up Work Hardening With Machining Advisor Pro’s Customizable Speeds and Feeds

What Causes Work Hardening

During machining, the friction between the tool and the workplace generates heat. The heat that is transferred to the workpiece causes the structure of the material to change and in turn harden the material. The degree to which it is hardened depends on the amount of heat being generated in the cutting action and the properties of the material, such as carbon content and other alloying elements. The most influential of these alloying elements include Manganese, Silicon, Nickel, Chromium, and Molybdenum.

While the hardness change will be the highest at the surface of the material, the thermal conductivity of the material will affect how far the hardness changes from the surface of the material.

titanium packed ball bearing

Often times, the thermal properties of a material that makes it appealing for an application are also the main cause of its difficulty to machine. For example, the favorable thermal properties of titanium that allow it to function as a jet turbine are the same properties that cause difficulty in machining it.

Major Problems

Heat Generation

As previously stated, metal work hardening can create some serious problems when machining. The biggest issue is heat generated by the cutting tool and transferring to the workpiece, rather than to the chips. When the heat is transferred to the workpiece, it can cause deformation which will lead to scrapped parts. Stainless Steels and High-Temp Alloys are most prone to work hardening, so extra precaution is needed when machining in these materials.

stringy chips in front of an end mill in the cut

Improper Speeds and Feeds

One other issue that scares a lot of machinists is the chance that a workpiece can harden to the point that it becomes equally as hard as the cutting tool. This is often the case when improper speeds and feeds are used. Incorrect speeds and feeds will cause more rubbing and less cutting, resulting in more heat generation passed to the workpiece. In these situations, machining can become next to impossible, and serious tool wear and eventual tool breakage are inevitable if the tool continues to be fed the same way.

Harvey tool ad for work hardening and speeds and feeds

How To Avoid Work Hardening

There are a few main keys to avoid work hardening: correct speeds and feeds, performing climb milling, selecting appropriate tool coatings, and proper coolant usage. As a general rule of thumb, talking to your tooling manufacturer and using their recommended speeds and feeds is essential for machining success.

Speeds and Feeds

Speeds and feeds become an even bigger priority when you want to avoid heat and tool rubbing, which can both cause serious work hardening. More cutting power and a constant feed rate keeps the tool moving and prevents heat from building up and transferring to the workpiece. The ultimate goal is to get the heat to transfer to the chips, and minimize the heat that is transferred into workpiece and avoiding any deformation of parts. Prior to machining, you should be setting guidelines for each cutting tool to ensure you receive the highest output without compromising on part finish or tool life.

Climb Milling

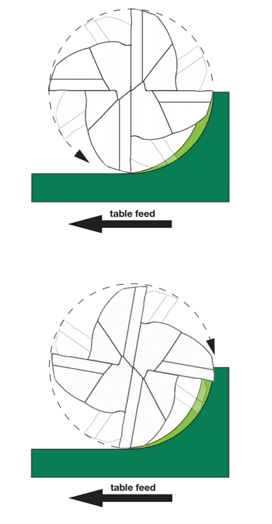
Conventional milling and climb milling are the two ways to perform CNC cutting operations. In climb milling, the cutter rotates with the feed, while in conventional milling the cutter rotates against the feed. However during conventional milling, the chip width starts at zero then increases thus generating heat at the workpiece. This results in work hardening and faster tool wear over time. On the other hand, climb milling begins at maximum chip width and decreases which transfers heat to the chip rather than the tool or workpiece. Climb milling is advantageous because there is less tool rubbing, minimized chance of chip recutting, and enhanced tool life.

drawing that displays conventional milling vs climb milling in cnc cutting operations

Tool Coating

While friction is often the main culprit of heat generation, the appropriate coating for the material may help combat the severity. Many coatings for ferrous materials reduce the amount of friction generated during cutting action. This added lubricity will reduce the friction on the cutting tool and workpiece, therefore transferring the heat generated to the chip, rather than to the workpiece. Tool coatings also create a natural separation between carbide and the workpiece. This minimizes the internal temperature of the carbide as heat is transferred into the chips and workpiece.

Coolant

Proper coolant usage helps to control the temperature in a cutting operation. Machinists generally choose between using Flooding or High Pressure Coolant options. Flooding the workpiece with coolant may be necessary to maintain the proper temperature, especially when machining in stainless steels and high-temp alloys. This low pressure method creates lubricity to flush chips and avoid chip recutting which commonly damages cutting tools.

high pressure coolant spraying on a part and workpiece during a cnc cutting operation

On the other hand, high pressure coolant delivers enhanced levels of chip evacuation and instant cooling of a part. However, one must be cautious of potentially breaking miniature diameter tooling when using this method due to the higher pressures. Coolant-fed tools can also help to reduce the heat at the contact point, lessening work hardening. While coolant-fed tools are typically a custom modification, saving parts from the scrap heap and using more machine time for the placement part will see the tool pay for itself over time.

https://www.harveyperformance.com/wp-content/uploads/2017/10/Featured-Image-Work-Hardening-Should-Scare-You-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-10-30 16:00:482023-11-10 14:17:50Work Hardening and When it Should Scare You

Avoid Composite Delamination With Compression Cutters

September 12, 2017/0 Comments/in CNC Machining, Composites, How-To's, Machining Techniques, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

Composites are a group of materials made up of at least two unique constituents that, when combined, produce mechanical and physical properties favorable for a wide array of applications. These materials usually contain a binding ingredient, known as a matrix, filled with particles or fibers called reinforcements. Composites have become increasingly popular in the Aerospace, Automotive, and Sporting Goods industries because they can combine the strength of metal, the light weight of plastic, and the rigidity of ceramics.

Unfortunately, composite materials present some unique challenges to machinists. Many composites are very abrasive and can severely reduce tool life, while others can melt and burn if heat generation is not properly controlled. Even if these potential problems are avoided, the wrong tool can leave the part with other quality issues, including delamination.

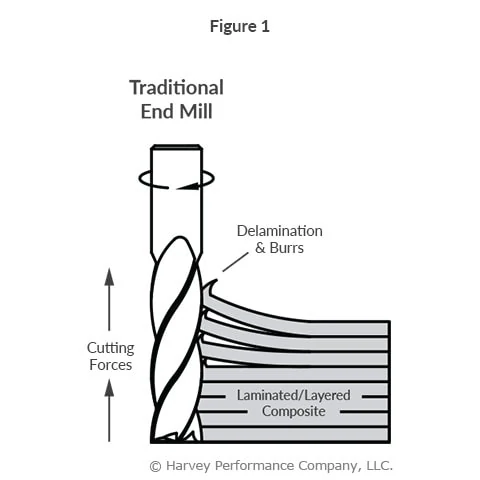
While composites such as G10 and FR4 are considered “fibrous”, composites can also be “layered,” such as laminated sheets of PEEK and aluminum. Layered composites are vulnerable to delamination, when the layers of the material are separated by a tool’s cutting forces. This yields less structurally sound parts, defeating the purpose of the combined material properties in the first place. In many cases, a single delaminated hole can result in a scrapped part.

Using Compression Cutter End Mills in Composite Materials

Composite materials are generally machined with standard metal cutting end mills, which generate exclusively up or down cutting forces, depending on if they have right or left hand flute geometry. These uni-directional forces cause delamination (Figure 1).

infographic of delamination with traditional end mill due to upward cutting forces

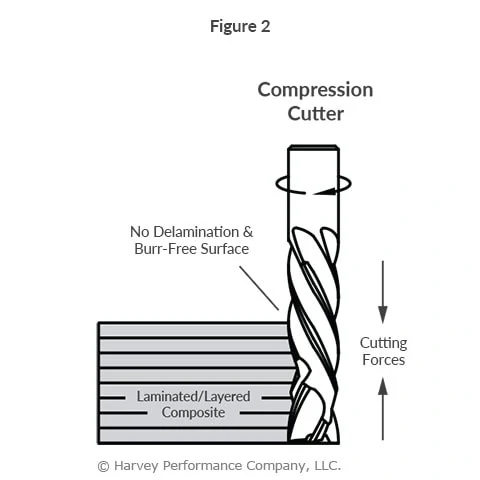
Conversely, compression cutters are designed with both up and down-cut flutes. The top portion of the length of cut, closest to the shank, has a left hand spiral, forcing chips down. The bottom portion of the length of cut, closest to the end, has a right hand spiral, forcing chips up. When cutting, the opposing flute directions generate counteracting up-cut and down-cut forces. The opposing cutting forces stabilize the material removal, which compresses the composite layers, combatting delamination on the top and bottom of a workpiece (Figure 2).

infographic of no delamination due to even cutting forces with compression cutter end mill

Since compression cutters do not pull up or press down on a workpiece, they leave an excellent finish on layered composites and lightweight materials like plywood. It is important to note, however, that compression cutters are suited specifically to profiling, as the benefits of the up and down-cut geometry are not utilized in slotting or plunging operations.

Something as simple as choosing a tool suited to a specific composite material can have significant effects on the quality of the final part. Consider utilizing tools optimized for different composites and operations or learn how to select the right drill for composite holemaking.

https://www.harveyperformance.com/wp-content/uploads/2017/09/Feature-Image-Compression-Cutters-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-09-12 16:00:532025-11-12 16:00:14Avoid Composite Delamination With Compression Cutters

Tackling Titanium: Machining Tips and Techniques Guide

August 8, 2017/6 Comments/in CNC Machining, Gummy Materials, Helical Solutions, Machining Techniques, Material Specific, Milling, Tech Tips/by Tom Pyle

In today’s manufacturing industry, titanium and its alloys have become staples in aerospace, medical, automotive, and firearm applications. This popular metal is resistant to rust and chemicals, is recyclable, and is extremely strong for its weight. However, there are several challenges that must be considered when machining titanium and selecting the appropriate tools and parameters for the job.

Titanium Varieties

Titanium is available in many varieties, including nearly 40 ASTM grades, as well as several additional alloys. Grades 1 through 4 are considered commercially pure titanium with varying requirements on ultimate tensile strength. Grade 5 (Ti6Al4V or Ti 6-4) is the most common combination, alloyed with 6 percent aluminum and 4 percent vanadium. Although titanium and its alloys are often grouped together, there are some key differences between them that must be noted before determining the ideal machining approach.

Titanium 6AL4V chips with helical hvti end mill

Helical Solutions’ HVTI End Mill is a great choice for high efficiency toolpaths in Titanium.

Titanium Concerns

Workholding

Although titanium may have more desirable material properties than your average steel, it also behaves more flexibly, and is often not as rigid as other metals. This requires a secure grip on titanium workpieces, and as rigid a machine setup as is possible. Other considerations include avoiding interrupted cuts, and keeping the tool in motion at all times of contact with the workpiece. Dwelling in a drilled hole or stopping a tool next to a profiled wall will cause the tool to rub – creating excess heat, work-hardening the material, and causing premature tool wear.

Heat Generation

Heat is a formidable enemy, and heat generation must be considered when selecting speeds and feeds. While commercially pure grades of titanium are softer and gummier than most of its alloys, the addition of alloying elements typically raises the hardness of titanium. This increases concerns regarding generated heat and tool wear. Maintaining a larger chipload and avoiding unnecessary rubbing aids with tool performance in the harder titanium alloys, and will minimize the amount of work hardening produced. Choosing a lower RPM, paired with a larger chipload, can provide a significant reduction in temperature when compared to higher speed options. Due to its low conduction properties, keeping temperatures to a minimum will put less stress on the tool and reduce wear. Using high-pressure coolant is also an effective method to reduce heat generation when machining titanium.

mitsubishi evo camshaft cutters machine from titanium with helical solutions end mill

These camshaft covers were custom made in titanium for Mitsubishi Evos.
Photo courtesy of @RebootEng (Instagram)

Galling and Built-Up Edge

The next hurdle to consider is that titanium has a strong tendency to adhere to a cutting tool, creating built up edge. This is a tricky issue which can be reduced by using copious amounts of high pressure coolant aimed directly at the cutting surface. The goal is to remove chips as soon as possible to prevent chip re-cutting, and keep the flutes clean and clear of debris. Galling is a big concern in the commercially pure grades of titanium due to their “gummy” nature. This can be addressed using the strategies mentioned previously, such as continuing feed at all times of workpiece contact, and using plenty of high-pressure coolant.

Titanium Solutions

While the primary concerns when machining titanium and its alloys may shift, the methods for mitigating them remain somewhat constant. The main ideas are to avoid galling, heat generation, work hardening, and workpiece or tool deflection. Use a lot of coolant at high pressure, keep speeds down and feeds up, keep the tool in motion when in contact with the workpiece, and use as rigid of a setup as possible.

In addition, selecting a proper tool coating can help make your job a successful one. With the high heat being generated during titanium machining operations, having a coating that can adequately deal with the temperature is key to maintaining performance through an operation. The proper coating will also help to avoid galling and evacuate chips effectively. Coatings such as Harvey Tool’s Aluminum Titanium Nitride (AlTiN Nano) produce an oxide layer at high temperatures, and will increase lubricity of the tool.

Tooling Solutions

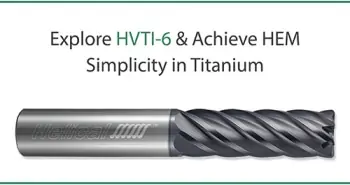
Helical Solutions offers the HVTI-6 line of tooling optimized for High Efficiency Milling (HEM) in Titanium and its alloys. Helical’s HVTI-6 features its Aplus coating which offers added lubricity and high temperature resistance for improved tool life and faster speeds and feeds.

As titanium and its many alloys continue to grow in use across various industries, more machinists will be tasked with cutting this difficult material. However, heat management and appropriate chip evacuation, when paired with the correct coating, will enable a successful run and profitable tool life.

machining titanium

https://www.harveyperformance.com/wp-content/uploads/2017/08/Featured-Image-Tackling-Titanium-IMG.jpg 525 1400 Tom Pyle http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Pyle2017-08-08 16:00:512025-11-12 15:53:48Tackling Titanium: Machining Tips and Techniques Guide
Page 3 of 41234
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top