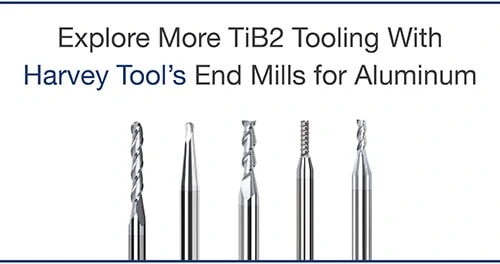
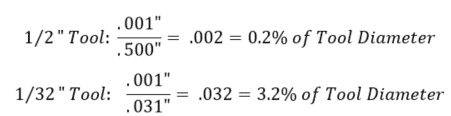Complex parts require more than a single operation. Features such as contours, chamfers, engraved details, and precision holes often demand multiple tooling strategies working together throughout the machining process.
In the video below, watch a single component progress from a block of Ti-6Al-4V to a finished part through more than 10 machining applications, each supported by specialized Harvey Tool solutions.
Explore the full range of solutions available in the 2026 Harvey Tool Catalog, featuring more than 31,000 miniature and specialty cutting tools designed to support even the most demanding applications.
https://www.harveyperformance.com/wp-content/uploads/2026/02/Feature-Image-Harvey-Tool-2026-Catalog-Video-IMG.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2026-02-27 15:07:592026-03-31 09:47:45Machining a Complex Part with Harvey Tool
CNC engraving is a process that removes a small amount of material to create detailed images or shapes. Many manufacturers use this method for labeling parts or creating complex designs; however, not everyone is aware of the key techniques necessary for optimal results. When using an engraving tool, it is essential to consider several challenges that could affect both the tool and the operation.
Advantages of CNC Engraving
Compared to other engraving methods, CNC engraving is fast, consistent, and cost-effective. Thanks to their repeatability, CNC machines deliver consistent results when paired with a high-quality engraving tool. We suggest running the tool at a minimum of 6,000 RPM.
If your machine supports it, increasing the RPM can lead to even greater results. Running at lower speeds can negatively impact tool life. Choosing the right engraving tool requires considering production volume and tool engagement time. Key factors such as tip design, angle, and coating play a crucial role in maximizing efficiency and durability.
Proper Engraver Tool Selection
Most machinists understand that a square-corner end mill does not last as long as a corner-radius or ball-end mill due to its fragile cutting edge.
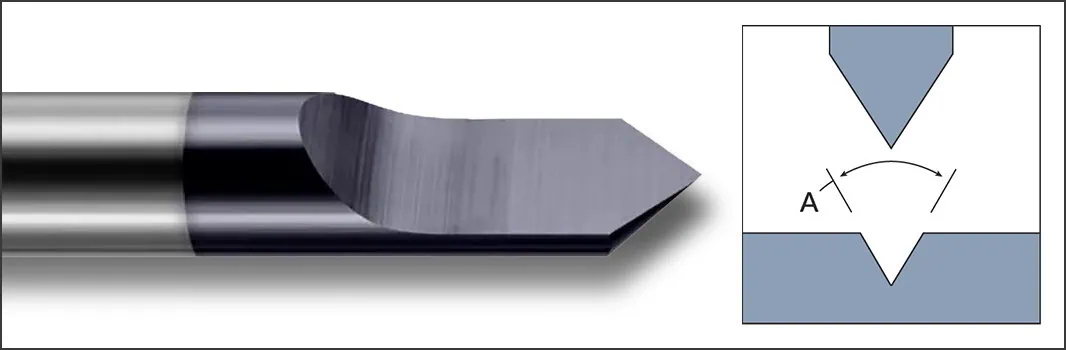
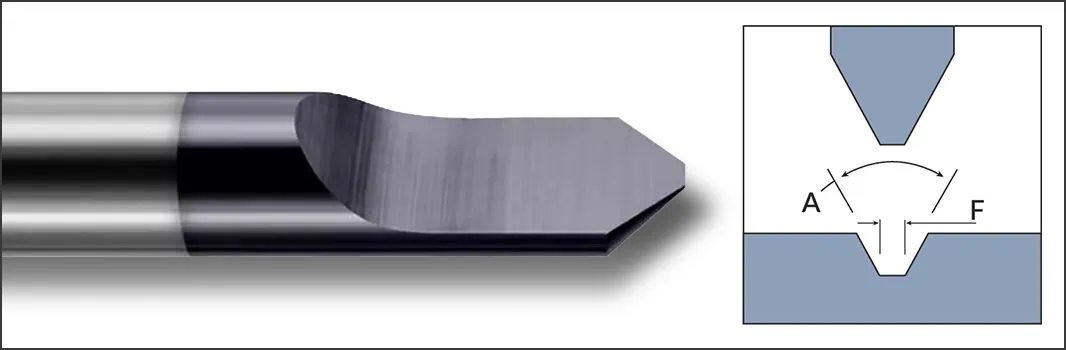
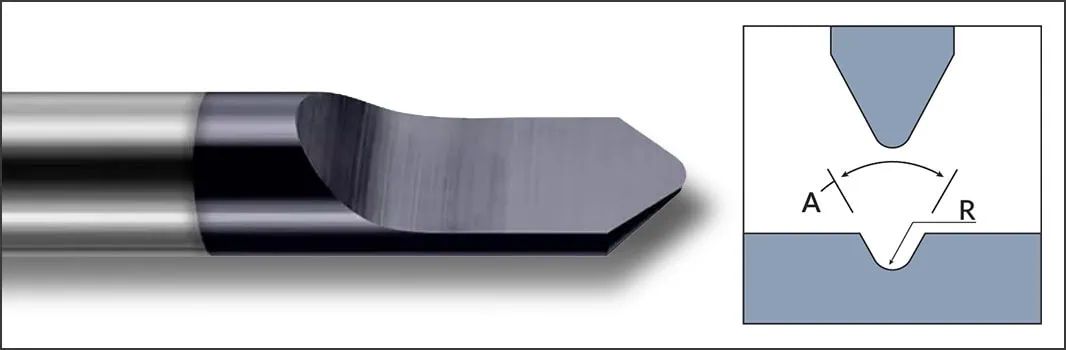
The same principle applies to CNC engraving tools. An engraver that comes to a sharp point is more fragile than one with a tipped-off or radius tip. For long production runs, consider using a tip-off or rounded tip design, as these geometries distribute cutting forces more evenly across the cutting edge, improving tool longevity. A tip-flat design will last longer than a pointed tip but not as long as a radius tip. If high-detail work is required, a pointed tip is preferable because it provides greater precision.
Similar to tip geometry, the engraving angle plays a critical role in visibility. The environment in which the engraving is used affects how well it can be seen. If the engraving is exposed to harsh conditions with elements like snow, mud, or dirt, debris can accumulate in the grooves, making it difficult to see and clean. A larger angle creates a wider groove, improving visibility and ease of cleaning.
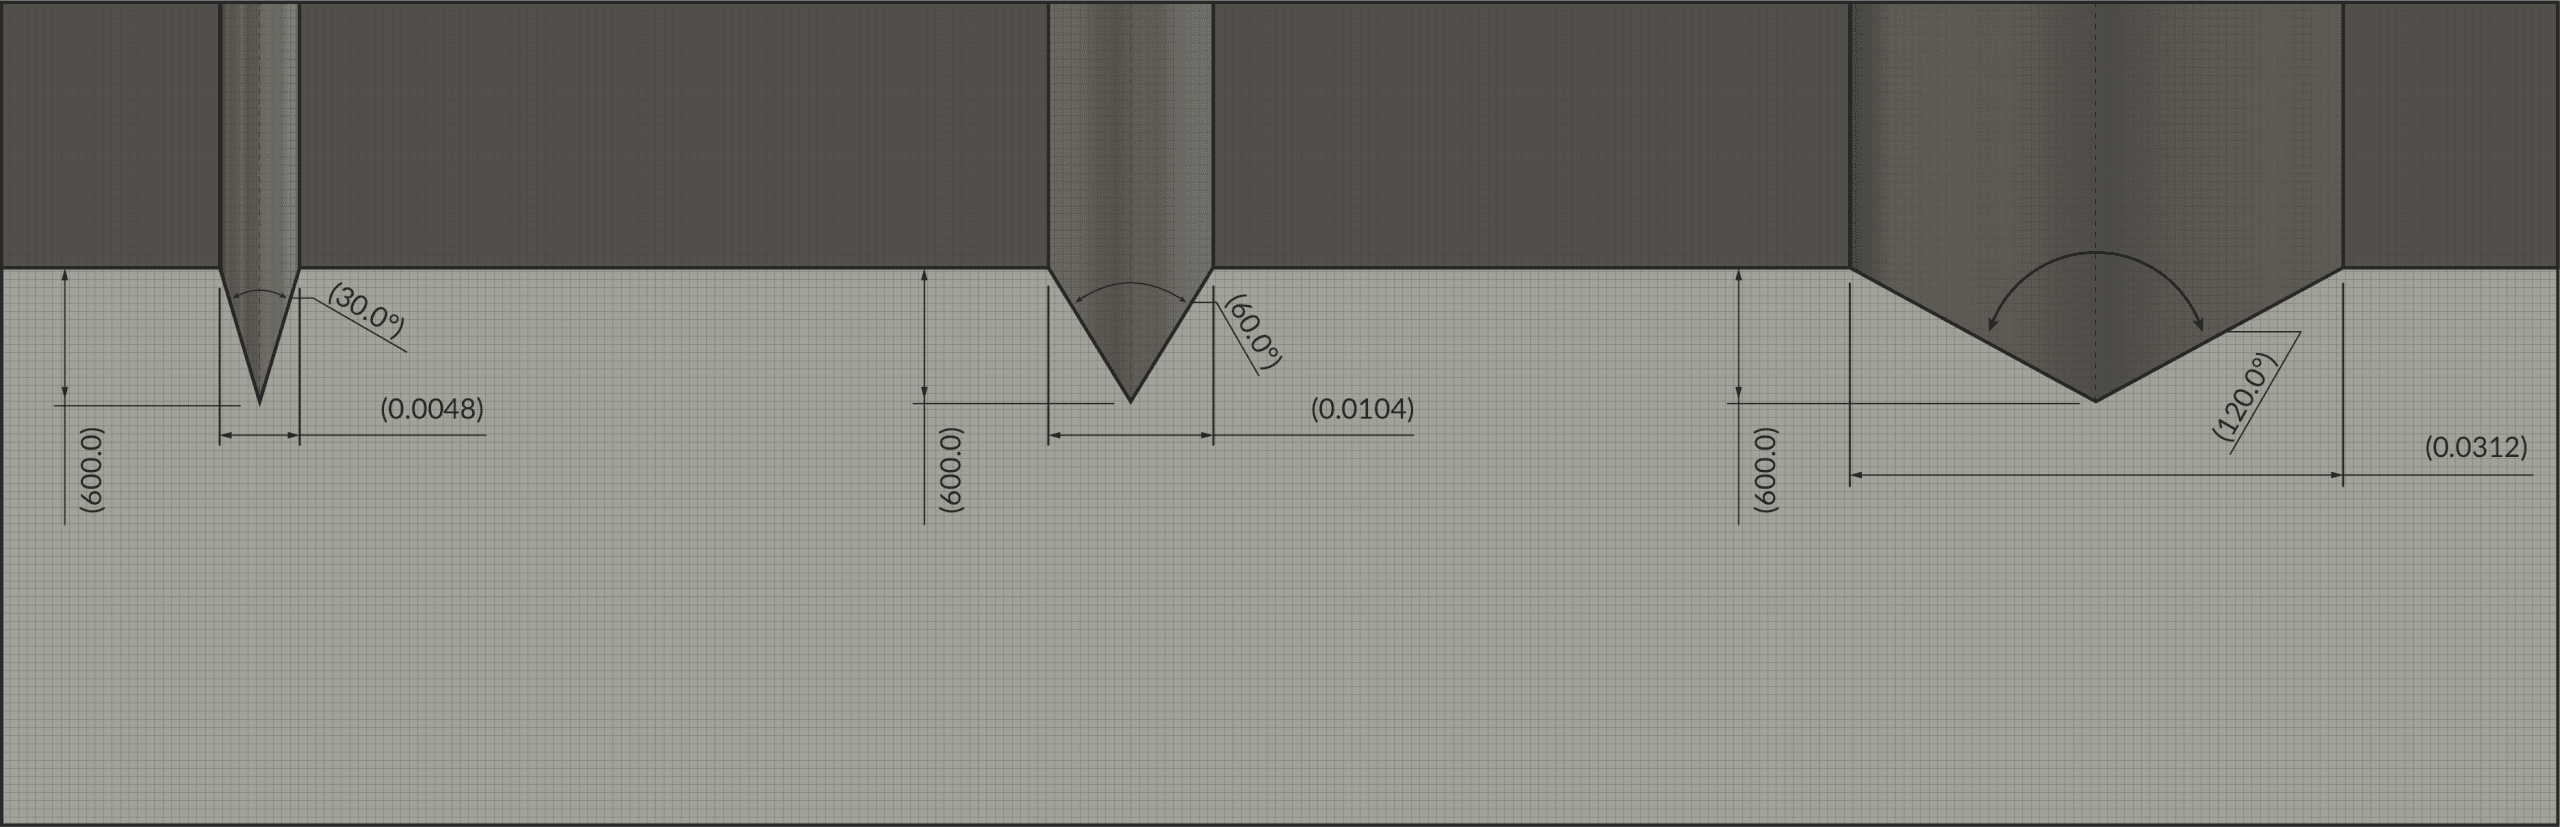
The image below illustrates three different engraving angles offered by Harvey: the leftmost groove is 30° included, the middle groove is 60° included, and the rightmost groove is 120° included. Each of these engravings is only 0.009 inches deep.
Notice that the 120° engraving is more visible at a distance due to increased surface exposure. If a job requires precision and detail, a smaller angle is preferable. While geometry significantly impacts engraving visibility and tool longevity, another key factor in tool performance is the choice of coating.
Choosing a Tool Coating
A coated engraving tool will last longer than an uncoated one because the coating provides a protective barrier between the tool and the workpiece. Additionally, coatings help reduce heat absorption, increase lubricity, and decrease tool wear. Selecting the right coating depends on the material being machined.
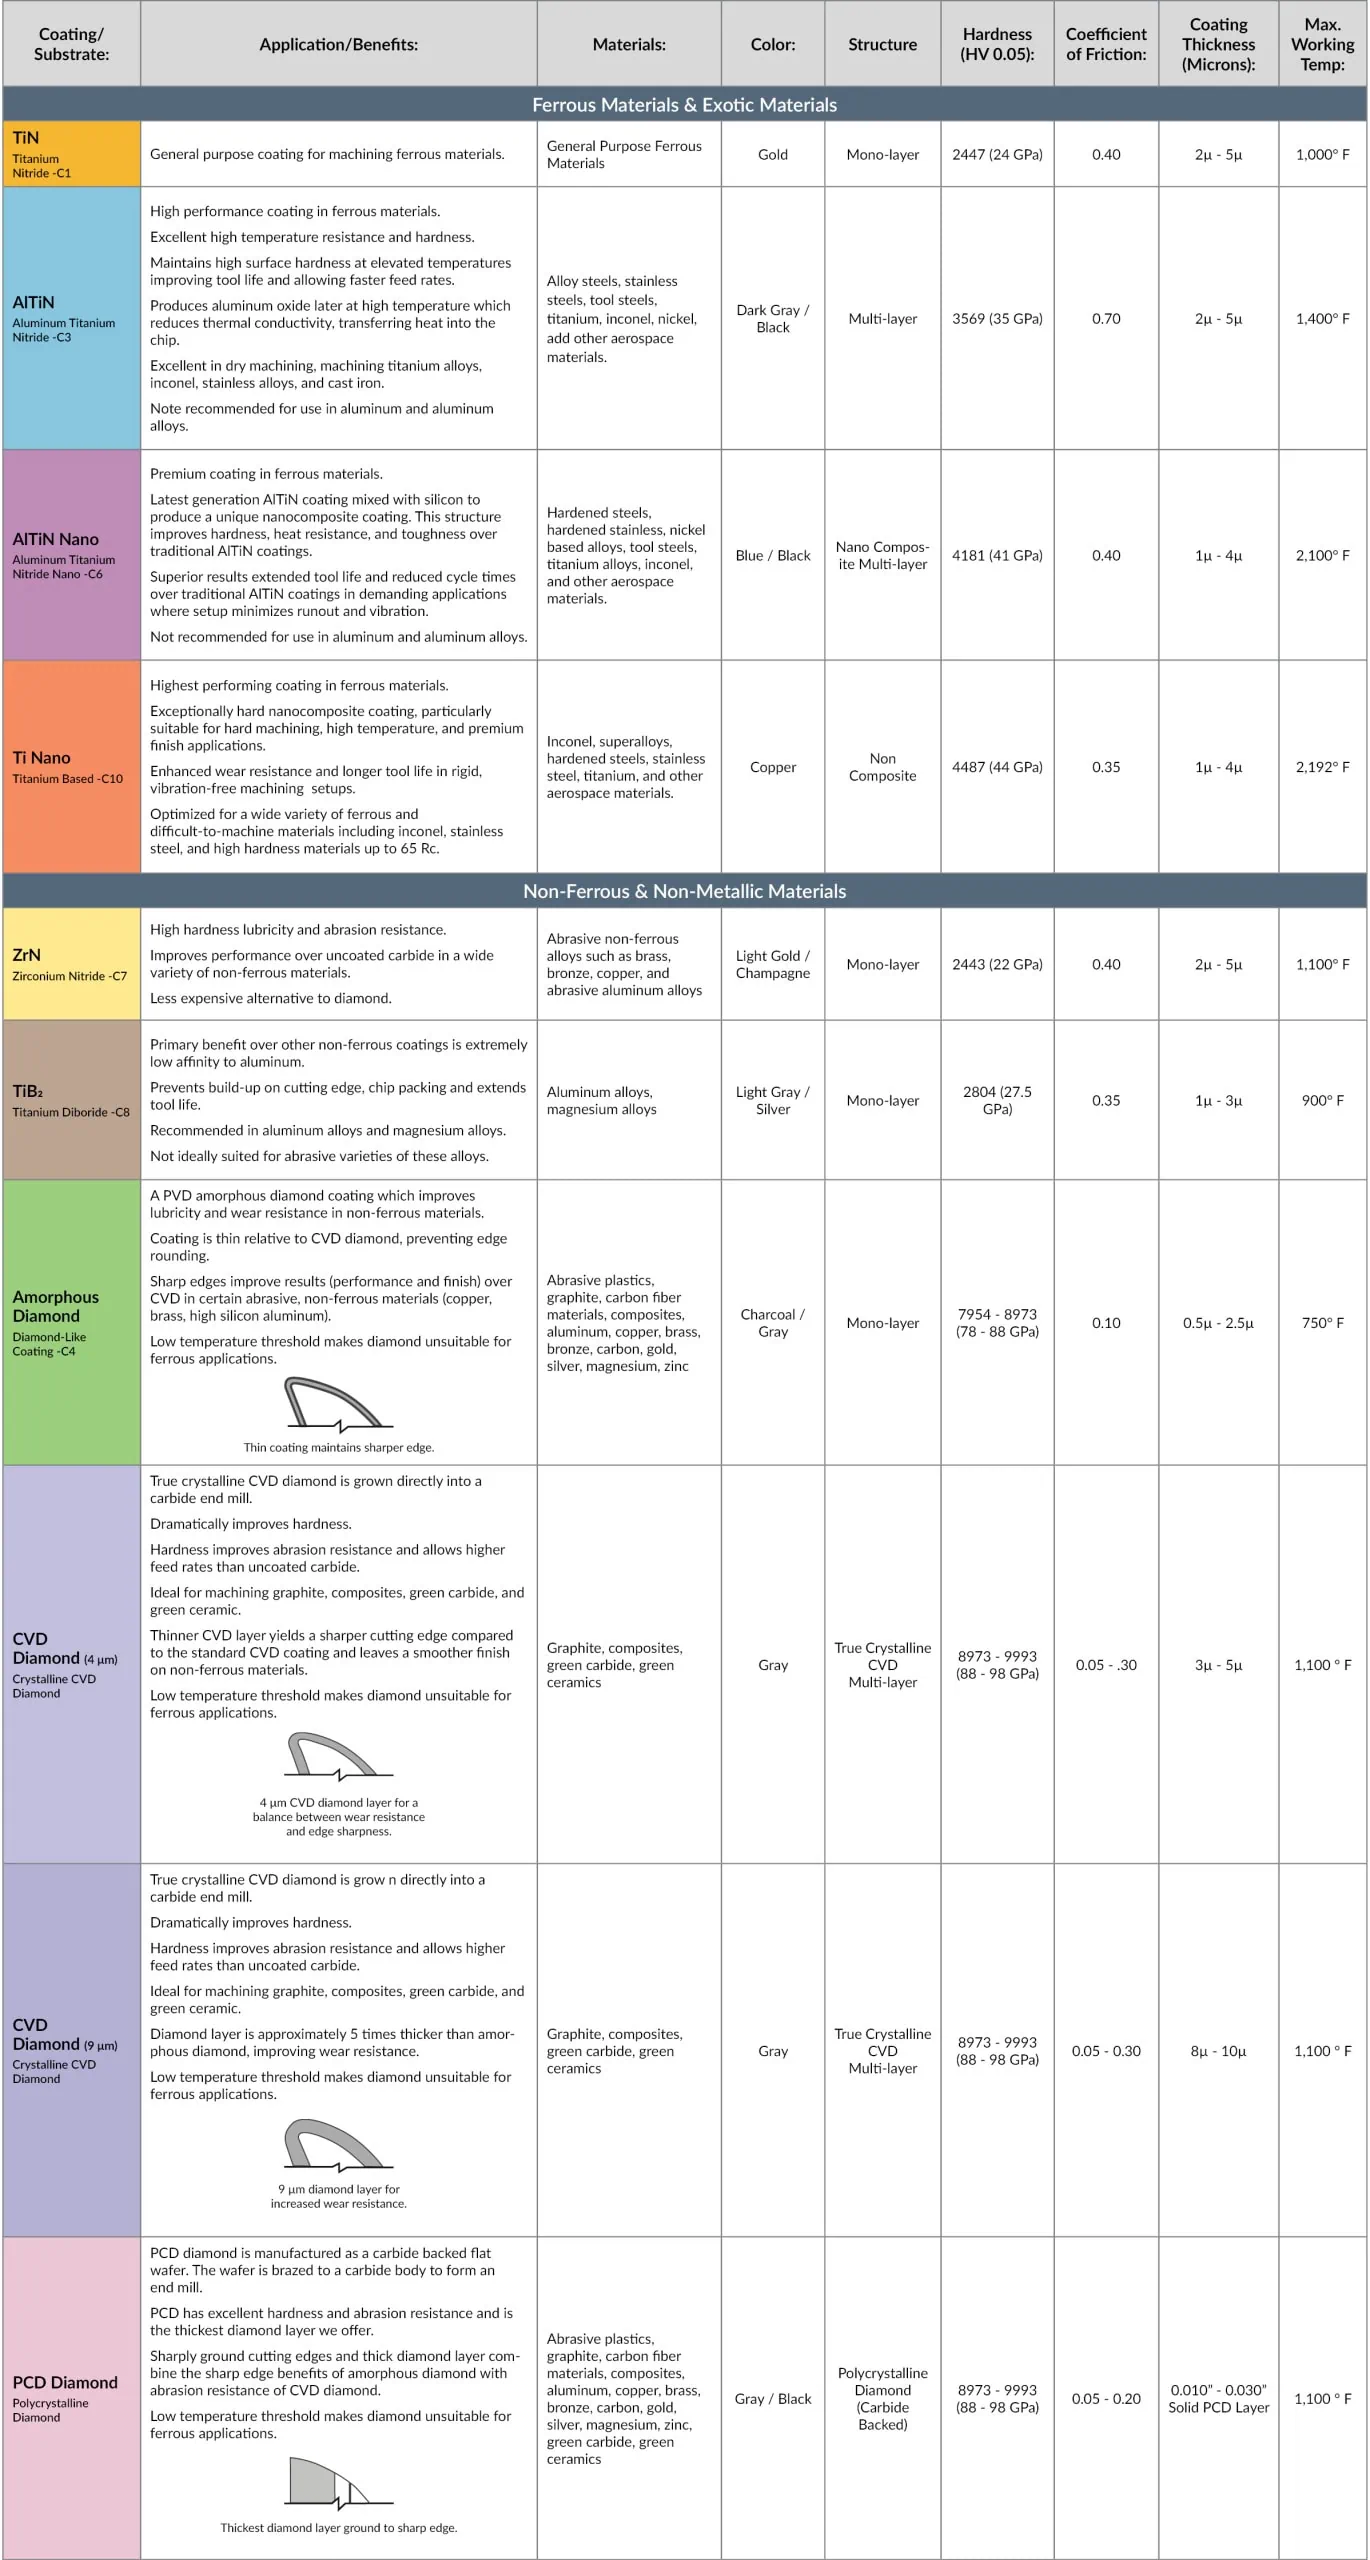
For example, our AlTiN and AlTiN-Nano coatings perform best in stainless steel and nickel alloys. For non-ferrous materials such as aluminum or copper, our Amorphous Diamond coating is ideal. As an alternative to our Amorphous Diamond coating, we also offer ZrN or TiB2 coatings.
A common misconception is that diamond-coated tools can be used on ferrous materials. Instead, this leads to rapid heat generation and premature tool failure.
Successfully Running Your Engraver
Selecting the correct engraving tool is just as important as understanding how to operate it properly. Even the highest-quality tool will be wasted if not used correctly. As with any machining operation, you must consider depth of cut, work holding methods, and appropriate speeds and feeds
Cutting Speeds and Feeds for Engraving
The tip is the most delicate area of the tool which makes running at the correct speed and feed rate crucial. Running at an incorrect speed and feed rate can cause deflection, which will lead to an inaccurate engraving, chipping, breaking, or a poor surface finish.
At Harvey, we recommend a minimum spindle speed of 6,000 RPM. Operating at higher RPMs, when possible, offers even better support for tool tip integrity.
Higher speeds ensure tool stability as it will be less likely to cause vibration and reduces heat buildup during operation. Running too slowly generates excess heat and vibration leading to chipping, breakage, or having a poor surface finish. To help maintain tool tip integrity, it is important to follow the recommended depth of cut and consider the way the engraver enters the material.
Determining Depth of Cut
Many machinists are unaware that taking cuts deeper than 0.009 inches can shorten the lifespan of a Harvey engraving tool. For depth of cut ranging from 0.001 inch to 0.009 inches, you can operate within our stated speed and feed guidelines. If the operation requires a deeper groove, the chip load must be reduced accordingly. For depths between 0.010 inches and 0.015 inches, reduce the chip load by 20%. For depths ranging from 0.016 inches to 0.020 inches, reduce the chip load by 30%. Depth of cut also influences visibility. A deeper cut made with a tool that has a smaller angle can provide similar visibility to a shallower cut made with a tool that has a larger angle.
The image below illustrates different engraving depths using a 30° included angle. From left to right, the depths are 0.009 inches, 0.015 inches, and 0.020 inches. As depth increases, visibility improves. When engaging the tool with the workpiece, it is best to ramp into the material to protect the tool tip.
We recommend a ramp angle of 1° to 3° for ferrous materials such as stainless steel, and 3° to 10° for non-ferrous materials like aluminum or copper. If ramping is not an option, you may plunge the tool into the material. However, the chip load must be reduced by 50% during entry. Once the desired depth is reached, you can return to the recommended running parameters. Another key consideration is ensuring the workpiece is securely held in place.
Workholding Considerations
Runout or vibration during engraving can result in uneven cuts and tool failure. To prevent this, ensure that engraving tools are held in a sturdy toolholder and that the workpiece is secured. A shrink-fit toolholder minimizes runout and provides excellent stability. While ER collets are acceptable, they wear overtime. To verify an ER collet’s suitability, place an indicator on the tool shank and rotate the tool within the collet. The goal is to achieve the least possible runout, ideally no more than 0.0003 inches.
The workpiece should also be properly secured, either in a vise or a fixture. To detect vibrations during operation, listen for irregular noise or feel for vibrations through the CNC machine door. For cooling, coolants are recommended for metallic workpieces, while an air blast is preferable for non-metallic materials such as plastic.
Conclusion
When selecting an engraving tool, it is essential to choose the correct geometry for the operation, as well as the appropriate coating for the material being machined. Regardless of tip geometry, the engraving tool’s tip is its most fragile part. Proper speed, feed rate, and depth of cut are crucial for maximizing tool life.
For metallic workpieces, a cooling method such as coolant is necessary, while non-metallic workpieces require an air blast. Before starting a new engraving operation, double-check tool runout and ensure that the workpiece is securely held in place.
By following these best practices, CNC engraving operations can achieve high precision, longevity, and optimal tool performance.
Are You Ready to Put Your Engraving Knowledge to Use?
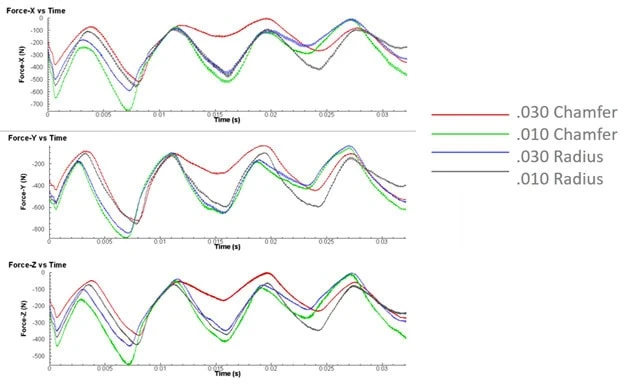
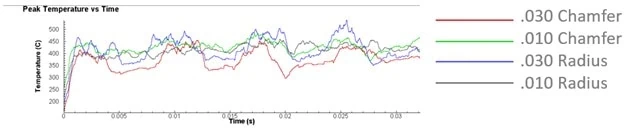
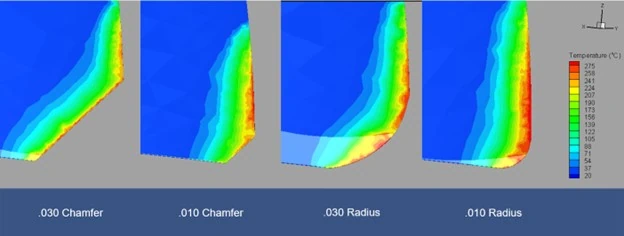
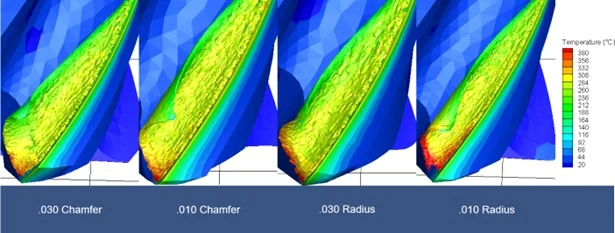
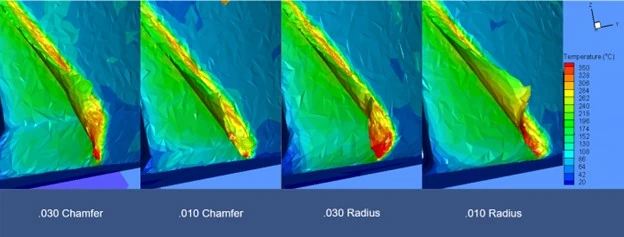
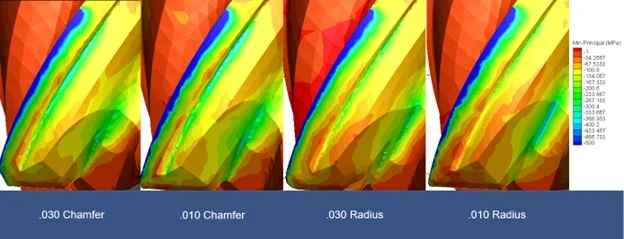
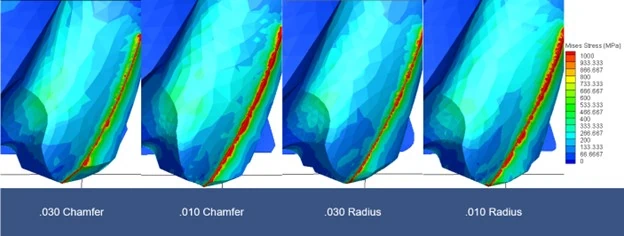
Using Finite Element Analysis (FEA) simulations by Third Wave Systems’ AdvantEdge CAE product, we tested different end mill corner geometries to compare their effects on both the tool and the workpiece. We studied and compared four 4 flute tools with either a 0.010” or 0.030” radius or chamfer. All tools were tested in 304 stainless steel at 1865 RPM, 244 SFM, and 0.0045 IPT for one revolution.
Both Corner Radius and Corner Chamfer tools offer advantages over Square End Mills by improving tool strength and reducing wear, though their benefits vary. One drawback of corner radius end mills is chip thinning along the radius, which can generate excess heat due to changes in chip thickness. This can lead to premature tool wear, poor surface finish, and potential work hardening. On the other hand, Corner Chamfers have the disadvantage of sharp corners where the chamfer meets the outer diameter (OD) and the end of the tool, causing local stress concentrations.
Force Analysis
The graphs above demonstrate the force exerted on the tool during cutting and how the corner size impacts the required force. As each flute engages, the forces peak in each direction. The 0.010” Chamfer generates the greatest force, while the 0.030” Chamfer requires the least. The forces with the radiused tools are very similar and fall between those of the two chamfered tools.
Temperature Analysis
The peak tool temperature graph shows the impact of chip thinning on corner radius tools and the overall corner size. The 0.030” Radius generated the most heat, while the 0.030” Chamfer generated the least. The temperature differences between the 0.010” Chamfer and 0.010” Radius was minimal, with the 0.010” Radius generated slightly less heat.
Chip and Workpiece Temperature
Understanding the temperature of the chip and workpiece is crucial for assessing tool performance. The contours above illustrate that the most heat is generated along the 0.030” Radius, followed by the 0.010” Radius. Corner Chamfer tools performed better, maintaining a lower overall temperature due to the absence of chip thinning.
Stress Analysis
The minimum principal stress on the backside of the flute indicates areas prone to tool failure. While there were slight differences between the chamfers and radii, the most notable finding was the reduction in stress with increased corner break size.
Similarly, the Mises stress analysis shows where stress is concentrated within the tool, potentially leading to failure. Again, the most significant observation was the reduction in stress with larger corner breaks.
Corner Chamfer vs. Corner Radius: Wrapped Up
Considering all factors, the 0.030” Corner Chamfer proved to be the best overall tool for 304 stainless steel. This is partly due to 304’s tendency to work harden, making excess heat generation particularly detrimental. When working with heat-sensitive materials, Corner Chamfer tools are preferable, especially during roughing, as they generate less heat due to the absence of chip thinning. Although there are minor stress concentrations at the sharp corners of Corner Chamfer tools, these are outweighed by the benefits of reduced heat generation. Larger radii exacerbate chip thinning’s impact on heat generation. While both tool styles offer advantages over square end mills, Corner Chamfer tools are more beneficial in high-heat applications where work hardening and tool wear are concerns.
Harvey Tool offers a range of Corner Chamfer Tools, with sizes ranging from 0.047” to 0.500” and various chamfer sizes to suit different applications.
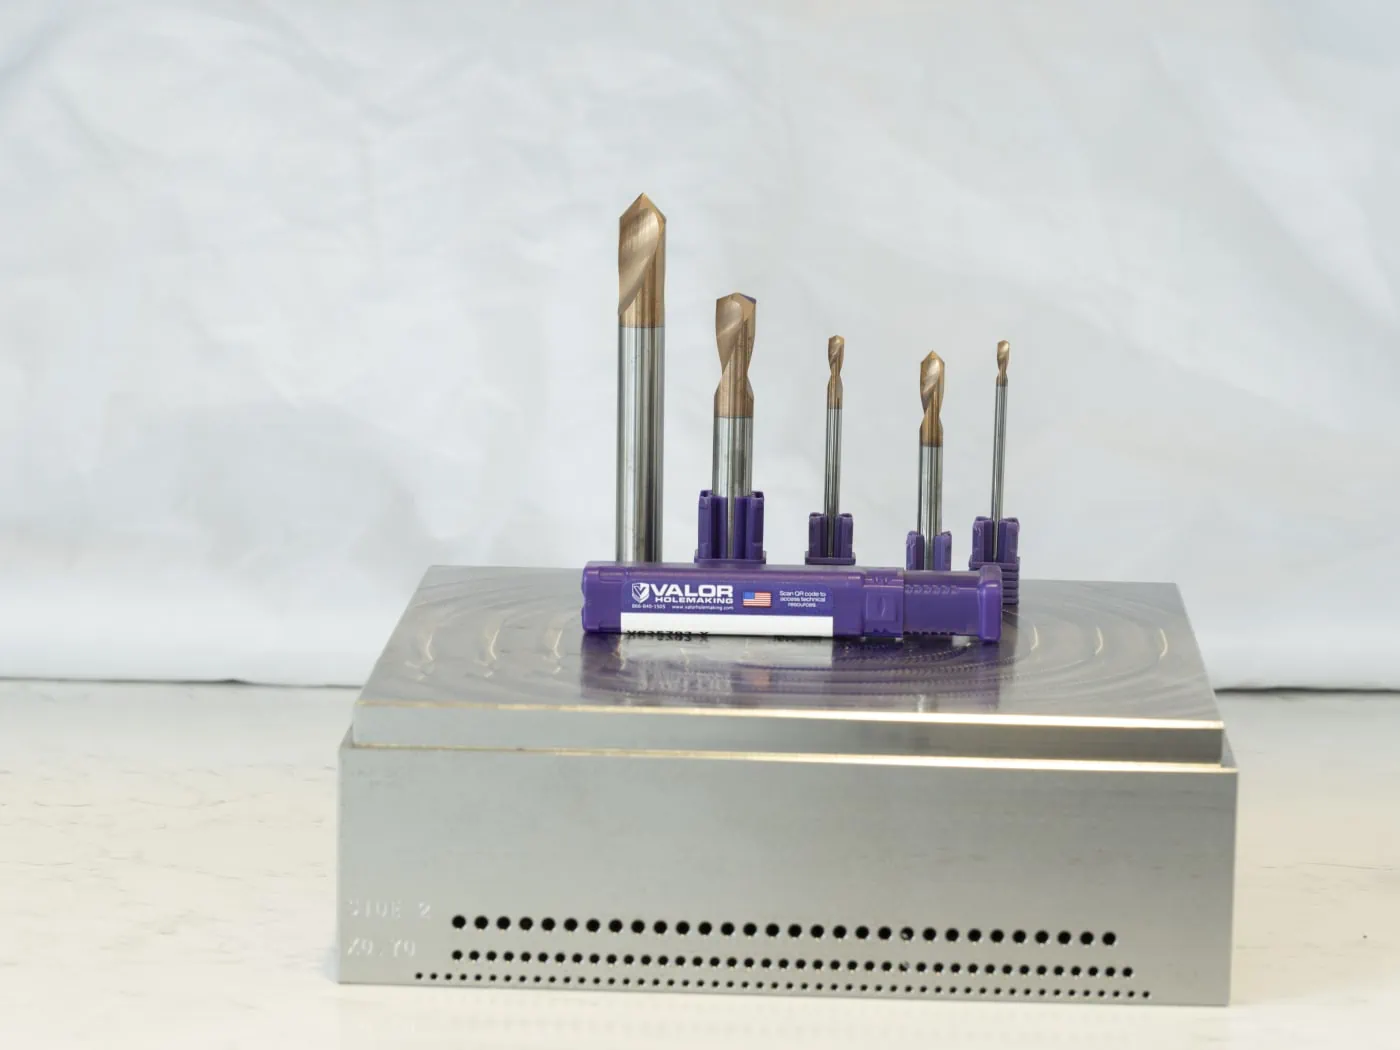
Drilling an ultra-precise hole can be tough. Material behavior, surface irregularities, and drill point geometry can all be factors leading to inaccurate holes. A Spot Drill, if used properly, will eliminate the chance of drill walking and will help to ensure a more accurate final product.
Choosing a Spot Drill
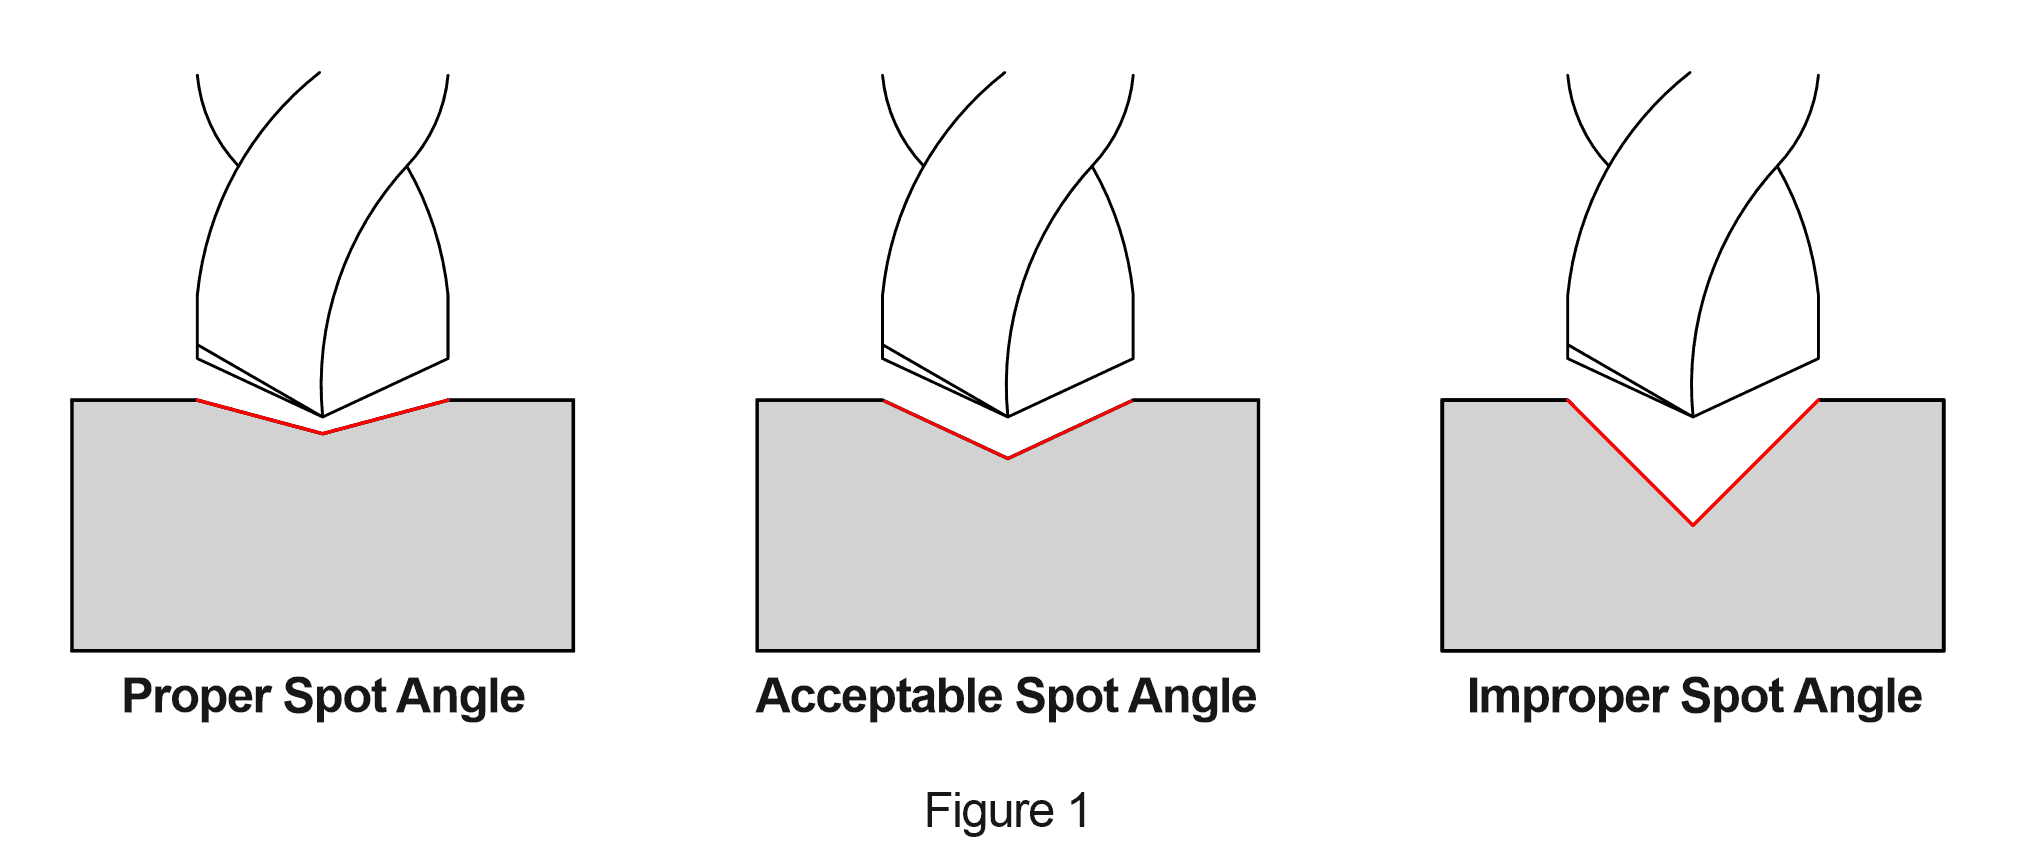
Ideally, the center of a carbide drill should always be the first point to contact your part. Therefore, a spotting drill should have a slightly larger point angle than that of your drill. Common drill point angles range from 118° to 140° and larger. Shallower drill angles are better suited to harder materials like steels due to increased engagement on the cutting edges. Aluminums can also benefit from these shallower angles through increased drill life. While these drills wear less and more evenly, they are more prone to walking, therefore creating a need for a proper high performance spot drill in a shallow angle to best match the chosen drill.
If a spotting drill with a smaller point angle than your drill is used, your drill may be damaged due to shock loading when the outer portion of its cutting surface contacts the workpiece before the center. Using a drill angle equal to the drill angle is also an acceptable situation. Figure 1 illustrates the desired effect. On the left, a drill is entering a previously drilled spot with a slightly larger angle than its point. On the right, a drill is approaching an area with an angle that is far too small for its point.
Marking Your Spot
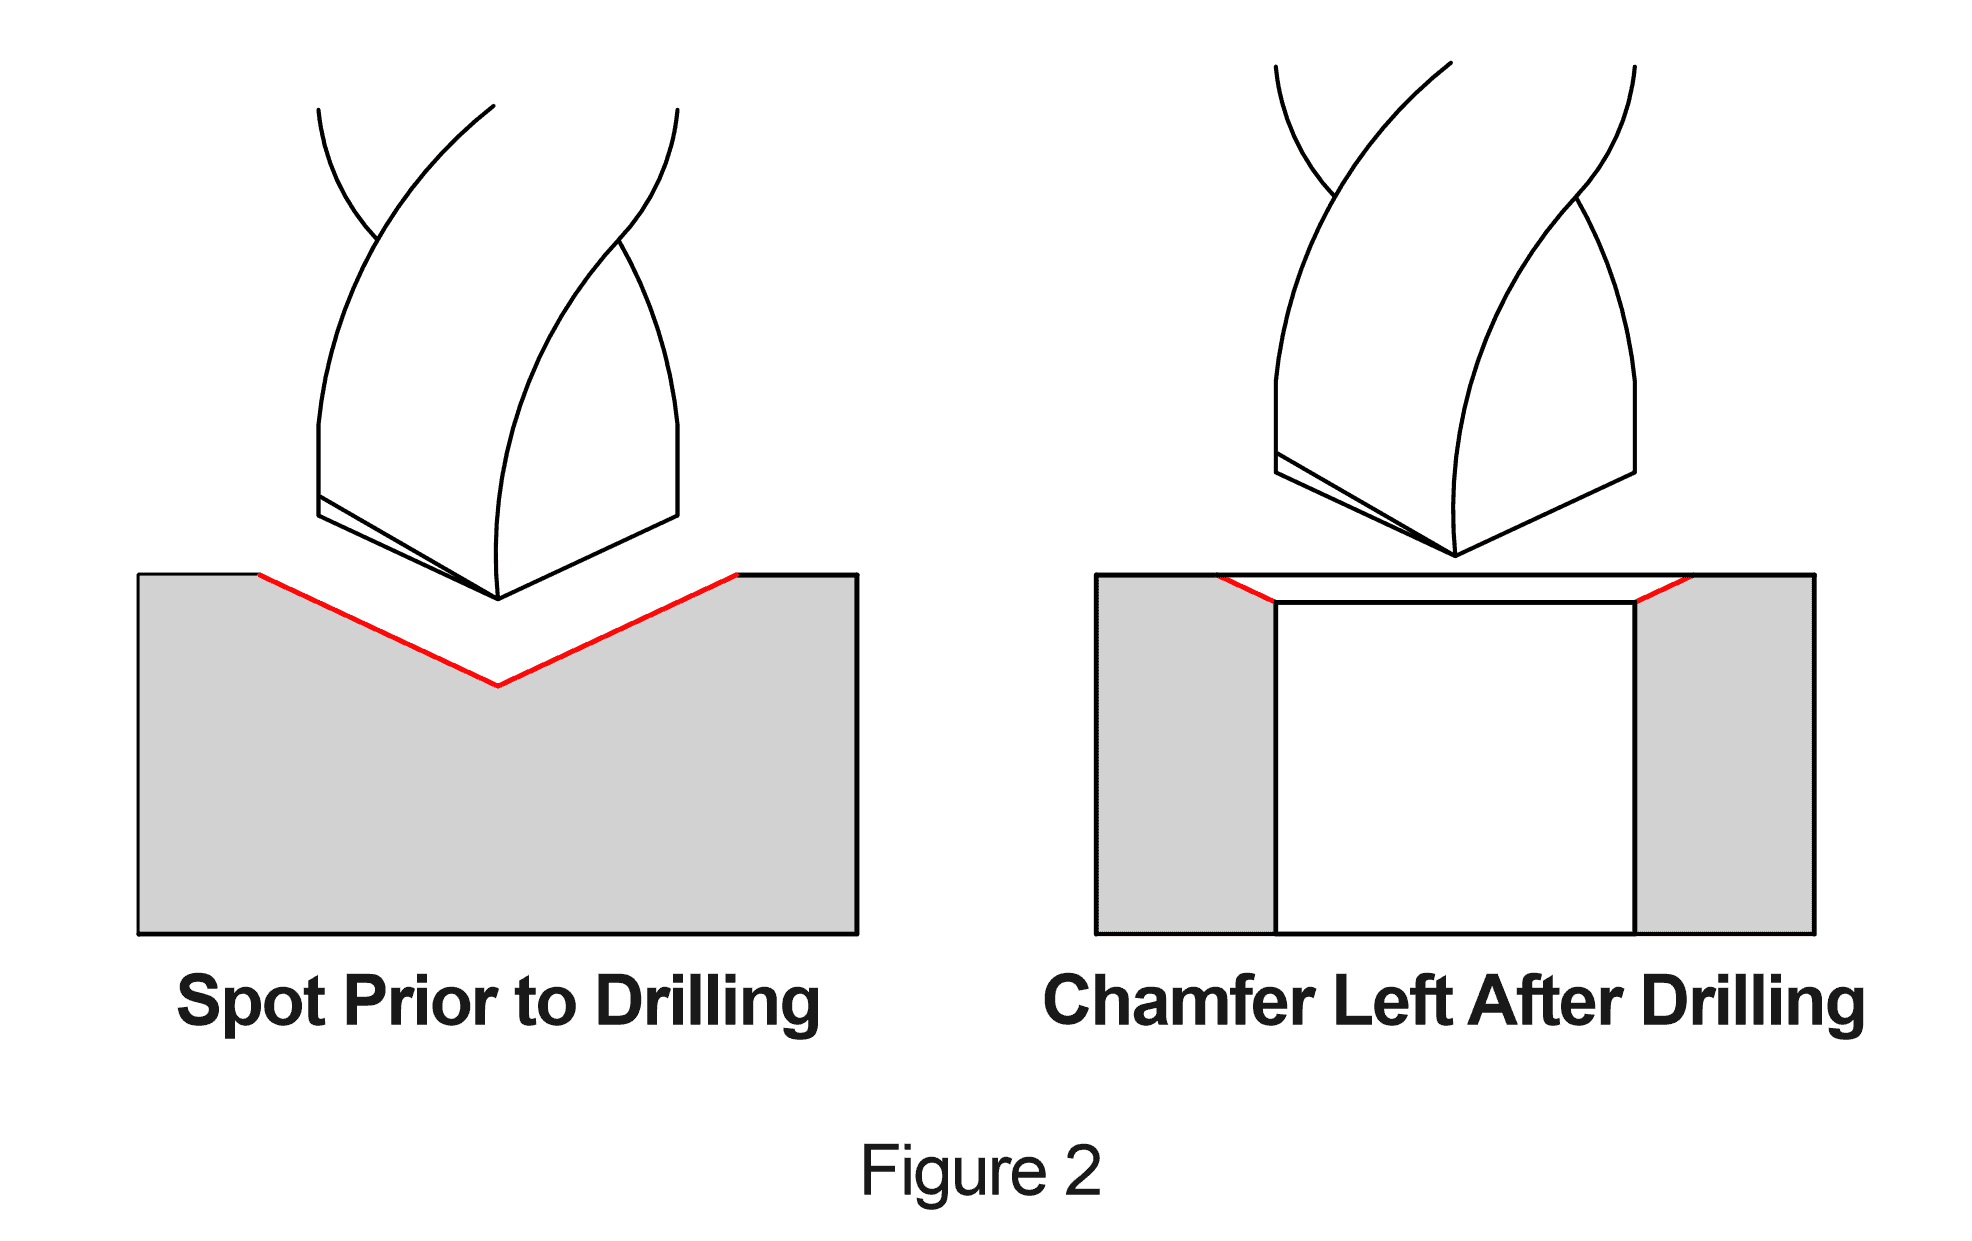
A Spotting Drill’s purpose is to create a small divot to correctly locate the center of a drill when initiating a plunge. However, some machinists choose to use these tools for a different reason – using it to chamfer the top of drilled holes. By leaving a chamfer, screw heads sit flush with the part once inserted.
What Happens if I Use a Spot Drill with an Improper Angle?
Using a larger angle drill will allow the drill to find the correct location by guiding the tip of the drill to the center. If the outer diameter of a carbide drill were to contact the workpiece first, the tool could chip. This would damage the workpiece and result in a defective tool. If the two flutes of the drill were slightly different from one another, one could come into contact before the other. This could lead to an inaccurate hole, and even counteract the purpose of spot drilling in the first place.
Avoiding CNC Drill Walking With a Spotting Drill
Few CNC machining applications demand precision like drilling. The diameter hole size, hole depth, part location, and finish are all important and provide little recourse if not up to specifications. That said, accuracy is paramount – and nothing leads to inaccurate final parts faster than drill walking, or the inadvertent straying from a drill’s intended location during the machining process. So how does drill walking occur, and how can one prevent it?
To understand drill walking, think about the act of striking a nail with a hammer, into a piece of wood. Firm contact to a sharp nail into an appropriate wood surface can result in an accurate, straight impact. But if other variables come into play – an uneven surface, a dull nail, an improper impact – that nail could enter a material at an angle, at an inaccurate location, or not at all. With CNC Drilling, the drill is obviously a critical element to a successful operation – a sharp, unworn cutting tool – when used properly, will go a long way toward an efficient and accurate final part.
To mitigate any variables working against you, such as an uneven part surface or a slightly used drill, a simple way to avoid “walking” is to utilize a Spotting Drill. This tool is engineered to leave a divot on the face of the part for a drill to engage during the holemaking process, keeping it properly aligned to avoid a drill from slipping off course.
When Won’t a Spot Drill Work for My Application?
When drilling into an extremely irregular surface, such as the side of a cylinder or an inclined plane, this tool may not be sufficient to keep holes in the correct position. For these applications, flat bottom versions or Flat Bottom Counterbores may be needed to creating accurate features.
https://www.harveyperformance.com/wp-content/uploads/2017/03/Feature-Image-Spotting-Drills-IMG.jpg5251400Tom Pylehttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngTom Pyle2022-08-25 10:52:002023-10-18 08:19:12Spot Drilling: The First Step to Precision Drilling
Proper tool coating plays a large role during the selection of a CNC cutting tool. At Harvey Tool, coatings are optimized for specific materials and alloys to ensure the highest tooling performance, possible. Each coating offers a unique benefit for the cutting tool: increased strength, enhanced lubricity, heat resistance, and wear mitigation, just to name a few.
In Benefits of Tool Coatings, the method of applying coatings to tools is examined. In this post, we’ll take a closer look at each Harvey Tool coating to examine its key properties, and to help you decide if it might add a boost to your next CNC application.
Harvey Tool offers a wide range of tool coating options for both ferrous and exotic materials, as well as non-ferrous and non-metallic materials. In the Harvey Tool catalog, coatings are often denoted in a -C# at the end of the product part number.
Harvey Tool Coatings for Ferrous and Exotic Materials
TiN
TiN, or Titanium Nitride (-C1), is a mono-layer coating meant for general purpose machining in ferrous materials. TiN improves wear resistance over uncoated tools and aids in decreasing built-up edge during machining. This coating, however, is not recommended for applications that generate extreme heat as its max working temperature is 1,000 °F. TiN is also not as hard as AlTiN and AlTiN Nano, meaning its less durable and may have a shorter tool life.
AlTiN, or Aluminum Titanium Nitride (-C3), is a common choice for machinists aiming to boost their tool performance in ferrous materials. This coating has a high working temperature of 1,400 °F, and features increased hardness. AlTiN excels in not only dry machining, due to its increased lubricity, but also in machining titanium alloys, Inconel, stainless alloys, and cast iron. To aid in its high heat threshold, the aluminum in this coating coverts to aluminum oxide at high temperatures which helps insulate the tool and transfer its heat into the formed chips.
AlTiN Nano or Aluminum Titanium Nitride Nano (-C6) is Harvey Tool’s premium coating for ferrous applications. This coating improves upon AlTiN by adding silicon to further increase the max working temperature to 2,100 °F while also increasing its hardness for increased tool life during demanding applications. Due to its penchant for demanding applications, AlTiN is recommended for hardened steels, hardened stainless, tool steels, titanium alloys, and aerospace materials. These applications often create high levels of heat that AlTiN Nano was designed to combat.
Note: AlTiN and AlTiN Nano are not recommended for use in Aluminum or Aluminum Alloys due to their high affinity to those materials.
Tool Coatings for Non-Ferrous and Non-Metallic Materials
TiB2
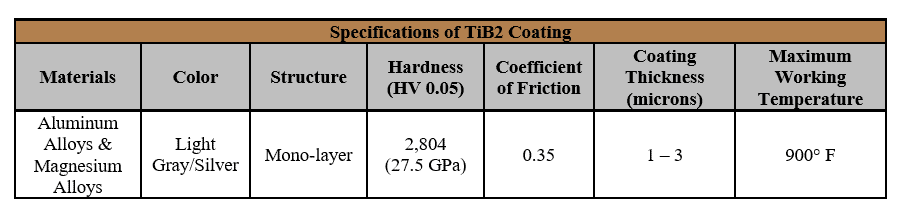
TiB2, or Titanium Diboride (-C8), is Harvey Tool’s “bread and butter” coating for non-abrasive aluminum alloys and magnesium alloys, as it has an extremely low affinity to aluminum as compared to other coatings. Aluminum creates lower working temperatures than ferrous materials, so this coating has a max working temperature of of a suitable 900 °F. TiB2 prevents built-up edge and chip packing, further extending its impressive tool life. TiB2 is not recommended for abrasive materials as the carbide is slightly weakened during the coating process. These materials can cause micro fractures that may damage the tool at high RPMs.
TiB2 can be found on a wide variety of Harvey Tool 2 and 3 flute tools as the premium option for high performance in aluminum alloys.
ZrN, or Zirconium Nitride (-C7), is a general-purpose coating for a wide variety of non-ferrous materials, including abrasive aluminum alloys. This tool coating is a lower cost alternative to diamond coatings, while still boasting impressive performance through its high hardness levels and overall abrasion resistance. ZrN has a max working temperature of 1,110 °F with strong lubricity in abrasive alloys. This coating is best suited for abrasives, such as brass, bronze, and copper, as well as abrasive aluminum alloys that should not be used with TiB2.
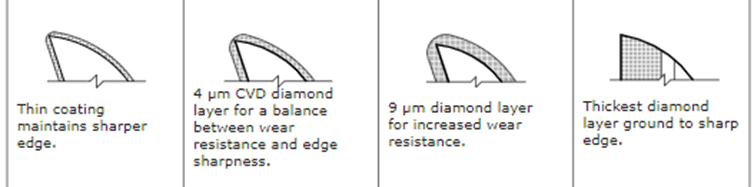
CVD Diamond, or Crystalline CVD Diamond, is a process where the coating is grown directly onto the carbide end mill. This process dramatically improves hardness over other coatings, improving tool life and abrasion resistance while also allowing for higher feed rates. The trade-off for increased wear resistance is a slight rounding of the cutting edge due to the coating application. Due to its increased wear resistance, CVD is best suited for highly abrasive materials such as graphite, composites, green carbide, and green ceramics. Similarly, these tool coatings have a max working temperature of 1,100 °F, meaning they are not well suited for ferrous applications.
Harvey Tool’s CVD Diamond Coating Options:
Amorphous, CVD 4 μm, CVD 9 μm, PCD Diamond
CVD Diamond (4 μm)
The 4 μm is thinner than the 9 μm allowing for a sharper cutting edge, which in effect leaves a smoother finish.
CVD Diamond 9 μm)
The 9 μm CVD tool coating offers improved wear resistance over the 4 μm CVD and Amorphous coatings due to its increased coating thickness.
Amorphous Diamond
Amorphous Diamond (-C4) is a PVD diamond coating which creates an exceptionally sharp edge as compared to CVD. This coating aids in performance and finish in abrasive non-ferrous applications, as it allows for greatly improved abrasion resistance during machining, while still maintaining a sharp cutting edge necessary for certain abrasives. Due to the thinness of the coating, edge rounding is prevented in relation to CVD diamond tooling. Amorphous Diamond is best suited for use in abrasive plastics, graphite, and carbon fiber, as well as aluminum and aluminum alloys with high silica content, due to their abrasiveness. The max working temp is only 750 °F, so it is not suited for use in ferrous machining applications.
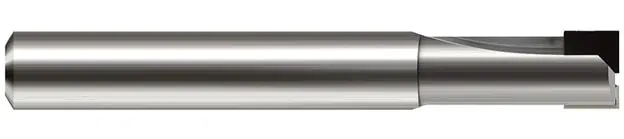
PCD Diamond, or Polycrystalline Diamond, is a tool coating that is brazed onto the carbide body. In comparison to the other diamond coatings, PCD does not face the same challenges of other coatings as it pertains to rounded cutting edges, as these edges are ground sharp. PCD has the edge benefits of Amorphous Diamond with the abrasion resistance of CVD Diamond. PCD is the thickest diamond layer offered by Harvey Tool, and excels due to its incredible hardness and abrasion resistance. This tool is best suited for all forms of abrasive, non-ferrous materials including abrasive plastics, graphite, carbon fiber, and composites. Similar to the other non-ferrous tool coatings, PCD is not suited for ferrous applications due to its working temperature of 1,100 °F.
When deciding on a coating for your application there are many factors to be considered. Different coatings often cross several applications with performance trade-offs between all of them. Harvey Tool offers a “Material Specific Selection” that allows users to choose tooling based upon what materials they are working with. Further, Harvey Tool’s technical team is always a phone call away to help in finding the right tool for your specific applications at 1-800-645-5609. Also, you can contact Harvey Tool via e-mail.
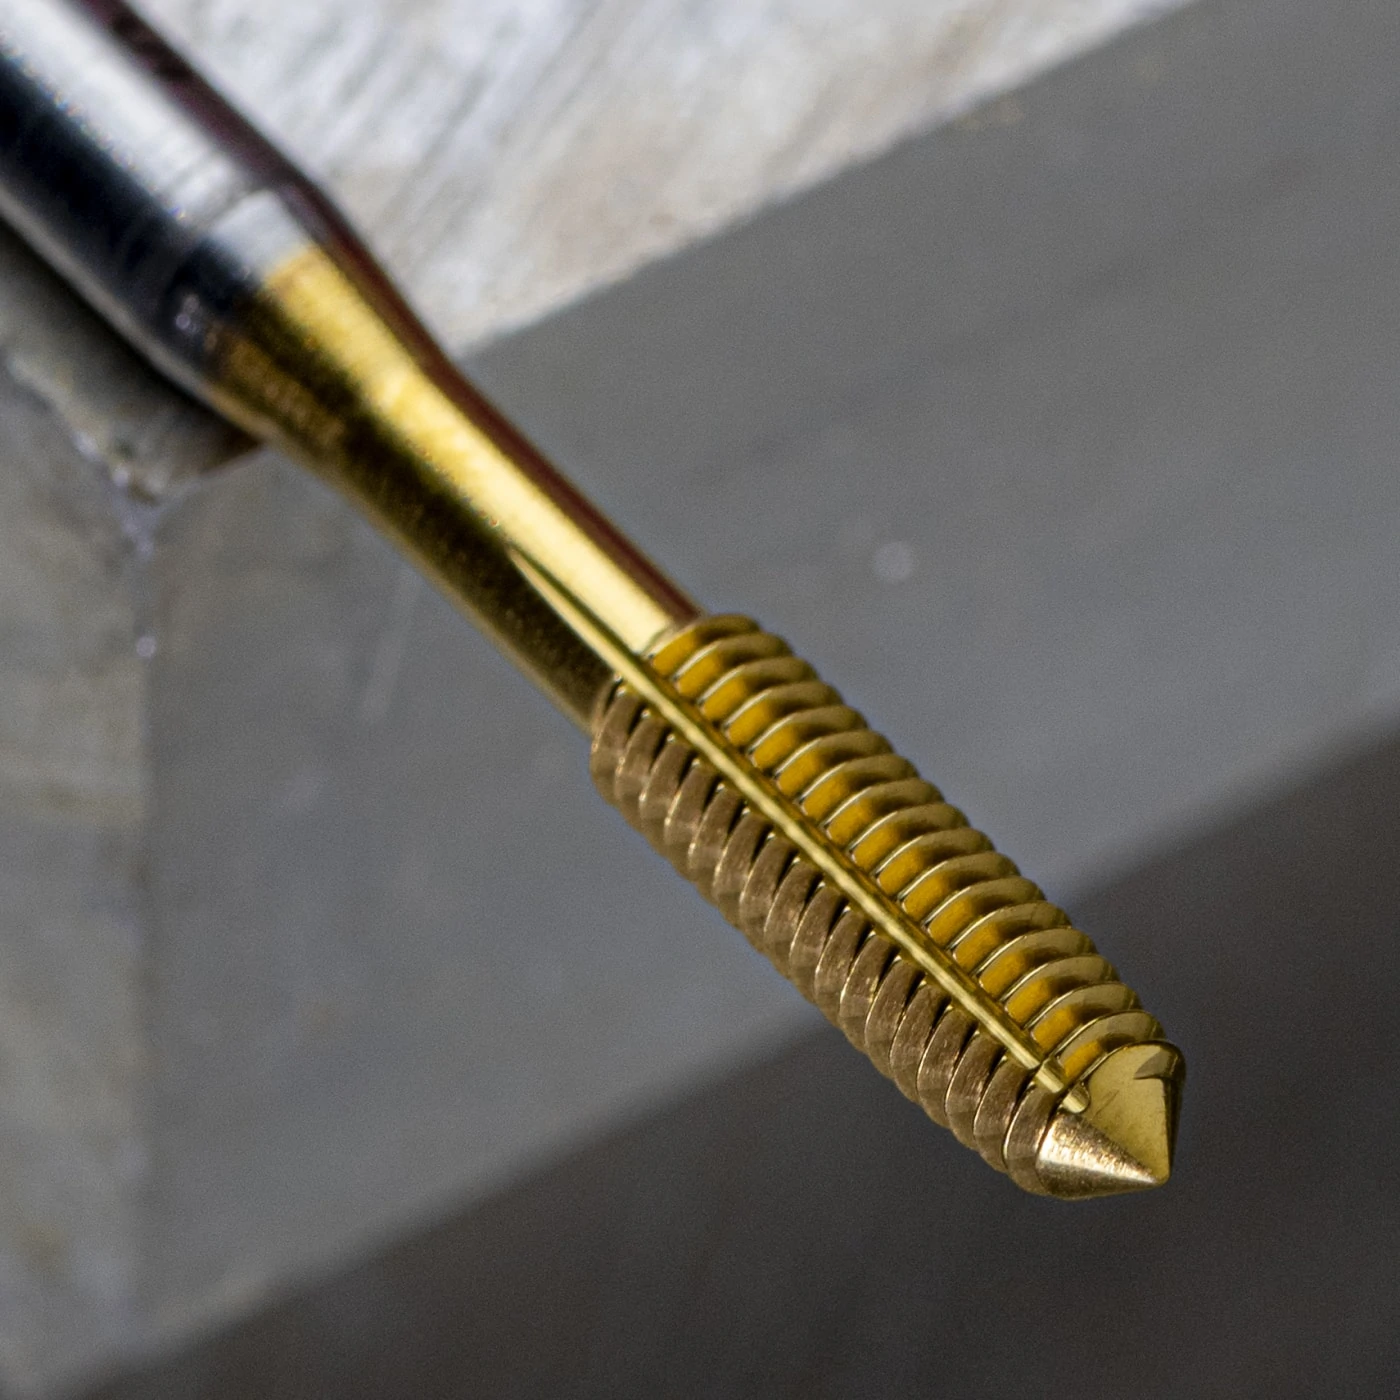
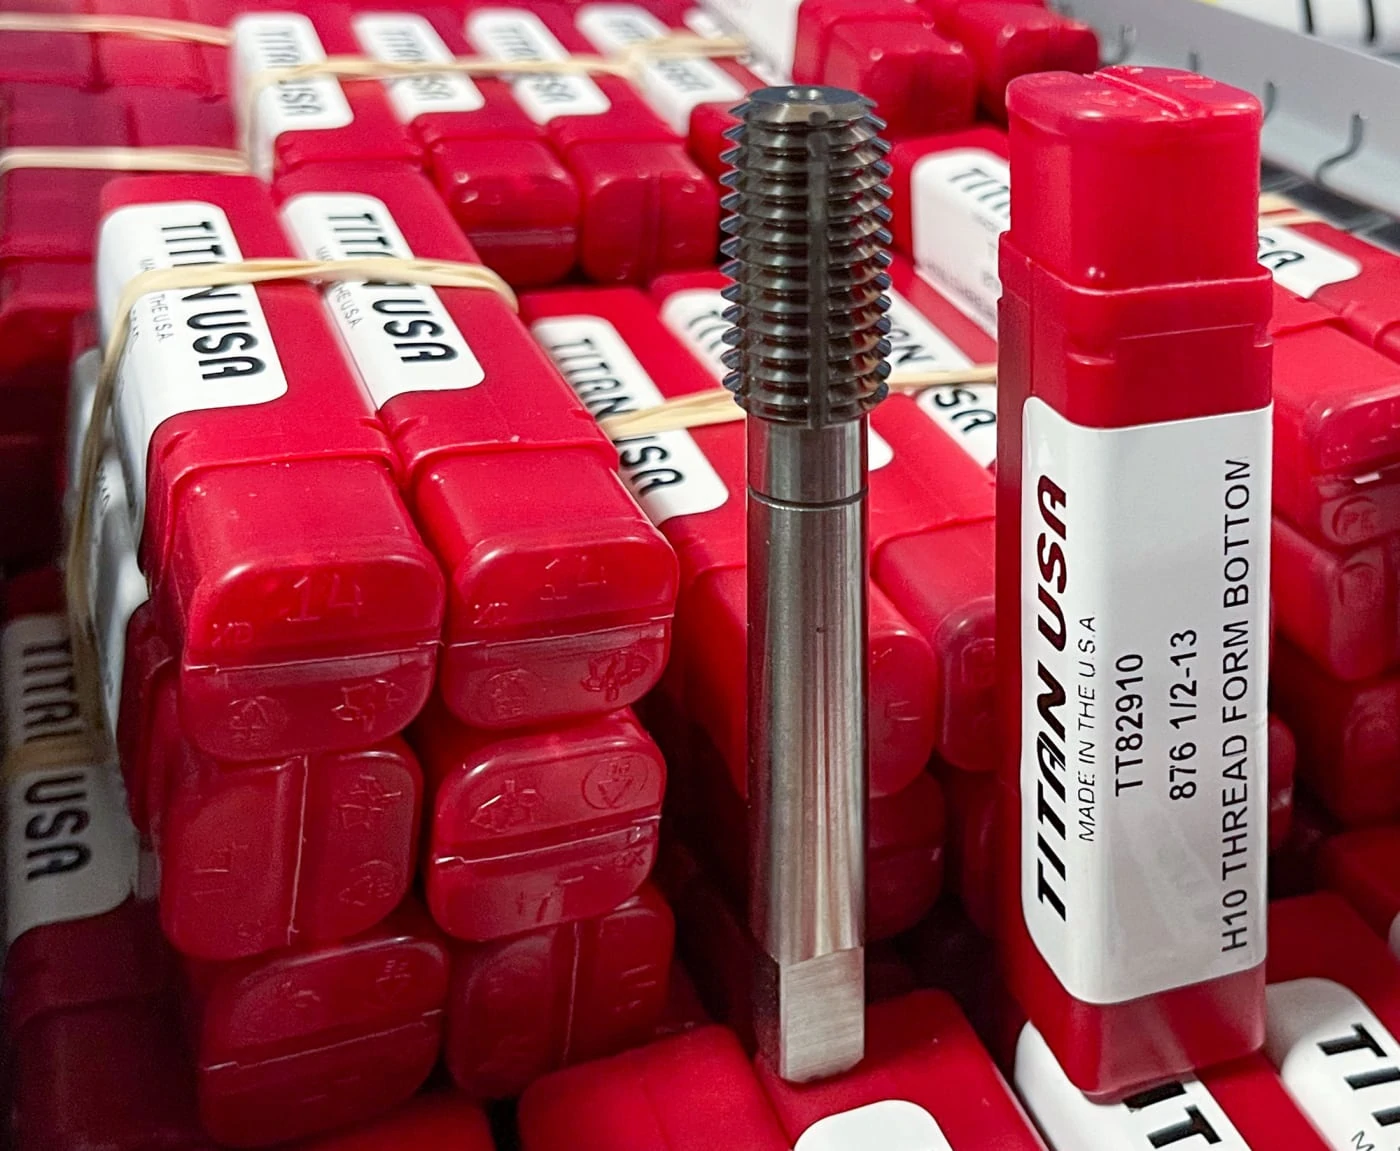
Unlike most CNC cutting tools, Thread Forming Taps, otherwise known as Form Taps, Forming Taps, or Roll Taps, work by molding the workpiece rather than cutting it. Because of this, Form Taps do not contain any flutes, as there is no cutting action taking place, nor are there any chips to evacuate. Below are 8 unique facts of Thread Forming Taps (and some may surprise you).
1. Chips Aren’t Formed
When using a Form Tap, chips are not formed, nor is any part material evacuated (Yes, you read that right). With thread forming, the tool is void of any flutes, as chip evacuation is not a concern. Form Taps quite literally mold the workpiece, rather than cut it, to produce threads. Material is displaced within a hole to make way for the threads being formed.
2. Cutting Oils Allow for Reduced Friction & Heat Generation
Did you know that Thread Forming Taps require good lubrication? But why is that the case if chips are not being evacuated, and how does lubrication enter the part with such a limited area between the tool and the perimeter of the hole being threaded? Despite the fact that chips aren’t being formed or evacuated, cutting oils aid the Form Tap as it interacts with the part material, and reduces friction and heat generation. Lube vent grooves are narrow channels engineered into the side of Forming Taps that are designed to provide just enough room for lubricant to make its way into – and out of – a part.
3. Only Certain Materials Are Recommended for Thread Forming
Not all materials are well suited for Thread Forming Taps. In fact, attempting to use a tap in the wrong material can result in significant part and tool damage. The best materials for this unique type of operation include aluminum, brass, copper, 300 stainless steel, and leaded steel. In other words, any material that leaves a stringy chip is a good candidate for cold forming threads. Materials that leave a powdery chip, such as cast iron, are likely too brittle, resulting in ineffective, porous threads.
4. Threads Produced Are Stronger Than Conventional Tapping Threads
Thread forming produces much stronger threads than conventional tapping methods, due to the displacements of the grain of the metal in the workpiece. Further, cutting taps produce chips, which may interfere with the tapping process.
5. Chip Evacuation is Never a Concern With Thread Forming
In conventional tapping applications, as with most machining applications, chip evacuation is a concern. This is especially true in blind holes, or holes with a bottom, as chips created at the very bottom of the hole oftentimes have a long distance to travel before being efficiently evacuated. With form taps, however, chip removal is never a concern.
6. Form Taps Offer Extended Tool Life
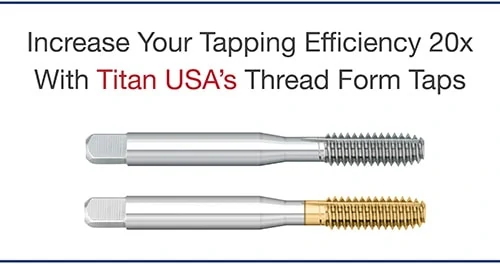
Thread Forming Taps are incredibly efficient, as their tool life is substantial (Up to 20x longer than cutting taps), as they have no cutting edges to dull. Further, Thread Forms can be run at faster speeds (Up to 2x faster than Cutting Taps).
Pro Tip: To prolong tool life even further, opt for a coated tool. Titan USA Form Taps, for example, are fully stocked in both uncoated and TiN coated styles.
7. A Simple Formula Will Help You Find the Right Drill Size
When selecting a Tap, you must be familiar with the following formula, which will help a machinist determine the proper drill size needed for creating the starter hole, before a Thread Forming Tap is used to finish the application:
Drill Size = Major Diameter – [(0.0068 x desired % of thread) / Threads Per Inch] Drill Size (mm) = Major Diameter – [(0.0068 x desired % of thread x pitch (mm)]
8. Thread Forming Taps Need a Larger Hole Size
Thread Form Taps require a larger pre-tap hole size than a cutting tap. This is because these tools impact the sides of the hole consistently during the thread forming process. If the pre-tap hole size is too small, the tool would have to work too hard to perform its job, resulting in excessive tool wear, torque, and possible breakage.
As an example, a ¼-20 cut tap requires a #7 drill size for the starter hole, whereas a ¼-20 roll tap requires a #1 drill size for 65% thread.
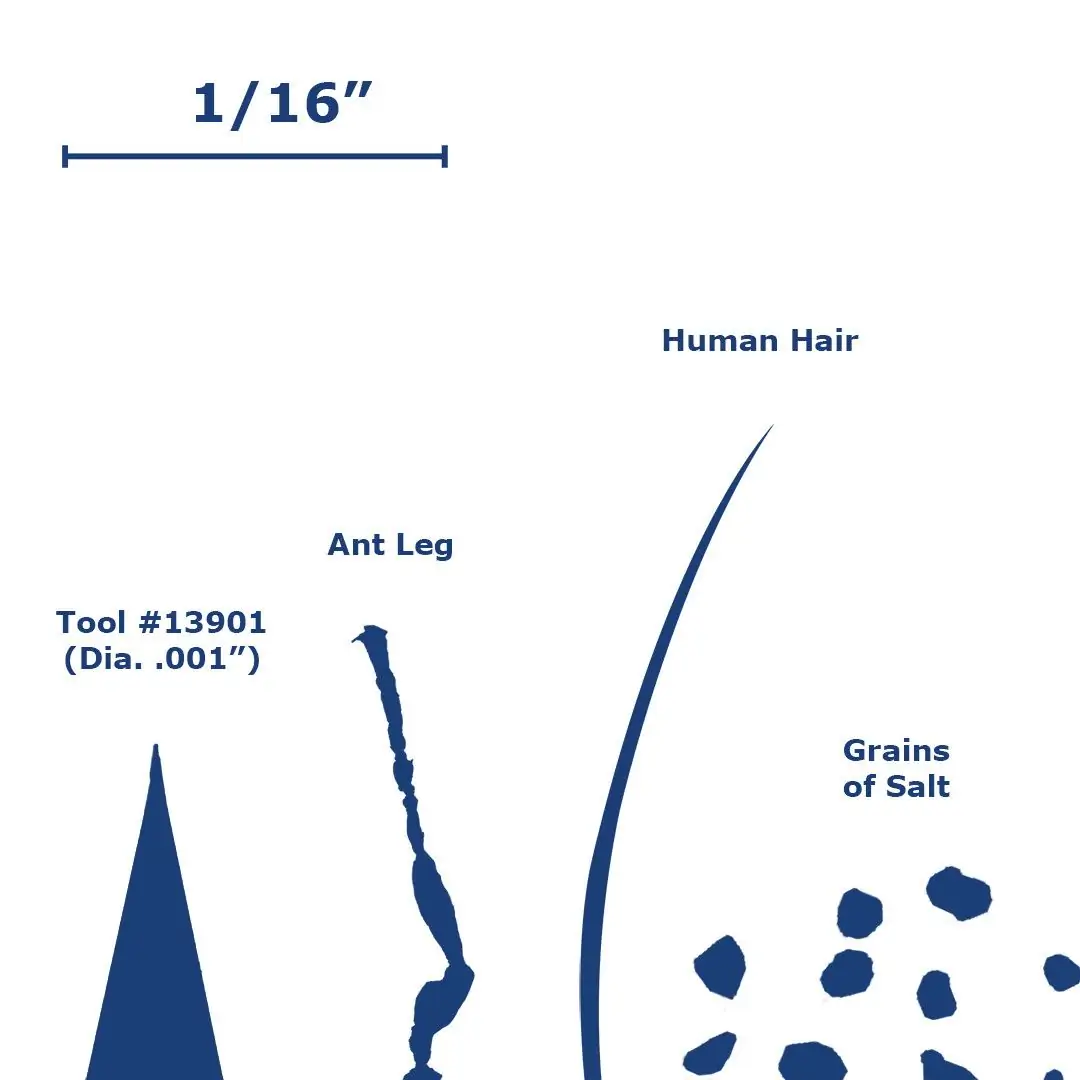
The machining industry generally considers micromachining and miniature end mills to be any end mill with a diameter under 1/8 of an inch. This is also often the point where tolerances must be held to a tighter window. Because the diameter of a tool is directly related to the strength of a tool, miniature end mills are considerably weaker than their larger counterparts, and therefore, lack of strength must be accounted for when micromachining. If you are using these tools in a repetitive application, then optimization of this process is key.
Size Comparison for Harvey Tool’s #13901 Square Miniature End Mill
Key Cutting Differences Between Conventional and Miniature End Mills
Runout
Runout during an operation has a much greater effect on miniature tools, as even a very small amount can have a large impact on the tool engagement and cutting forces. Runout causes the cutting forces to increase due to the uneven engagement of the flutes, prompting some flutes to wear faster than others in conventional tools, and breakage in miniature tools. Tool vibration also impacts the tool life, as the intermittent impacts can cause the tool to chip or, in the case of miniature tools, break. It is extremely important to check the runout of a setup before starting an operation. The example below demonstrates how much of a difference .001” of runout is between a .500” diameter tool and a .031” diameter tool.
The runout of an operation should not exceed 2% of the tool diameter. Excess runout will lead to a poor surface finish.
Chip Thickness
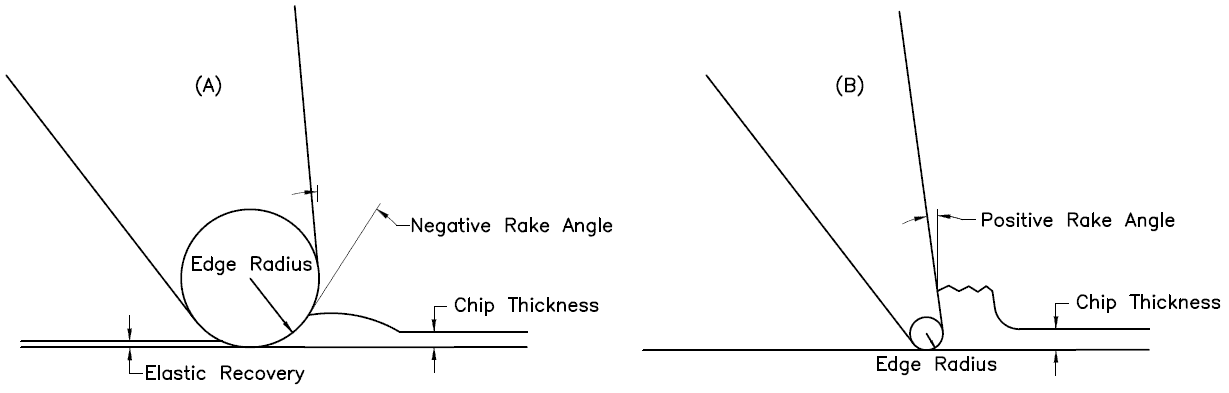
The ratio between the chip thickness and the edge radius (the edge prep) is much smaller for miniature tools. This phenomena is sometimes called “the size effect” and often leads to an error in the prediction of cutting forces. When the chip thickness-to-edge radius ratio is smaller, the cutter will be more or less ploughing the material rather than shearing it. This ploughing effect is essentially due to the negative rake angle created by the edge radius when cutting a chip with a small thickness.
If this thickness is less than a certain value (this value depends of the tool being used), the material will squeeze underneath the tool. Once the tool passes and there is no chip formation, part of the plowed material recovers elastically. This elastic recovery causes there to be higher cutting forces and friction due to the increased contact area between the tool and the workpiece. These two factors ultimately lead to a greater amount of tool wear and surface roughness.
Figure 1: (A) Miniature tool operation where the edge radius is greater than the chip thickness (B) Conventional operation where the edge radius is small than the chip thickness
Tool Deflection in Conventional vs. Micromachining Applications
Tool deflection has a much greater impact on the formation of chips and accuracy of the operation in micromachining operations, when compared to conventional operations. Cutting forces concentrated on the side of the tool cause it to bend in the direction opposite the feed. The magnitude of this deflection depends upon the rigidity of the tool and its distance extended from the spindle. Small diameter tools are inherently less stiff compared to larger diameter tools because they have much less material holding them in place during the operation. In theory, doubling the length sticking out of the holder will result in 8 times more deflection. Doubling the diameter of an end mill it will result in 16 times less deflection. If a miniature cutting tool breaks on the first pass, it is most likely due to the deflection force overcoming the strength of the carbide. Here are some ways you can minimize tool deflection.
Workpiece Homogeny
Workpiece homogeny becomes a questionable factor with decreasing tool diameter. This means that a material may not have uniform properties at an exceptionally small scale due to a number of factors, such as container surfaces, insoluble impurities, grain boundaries, and dislocations. This assumption is generally saved for tools that have a cutter diameter below .020”, as the cutting system needs to be extremely small in order for the homogeny of the microstructure of the material to be called into question.
Surface Finish
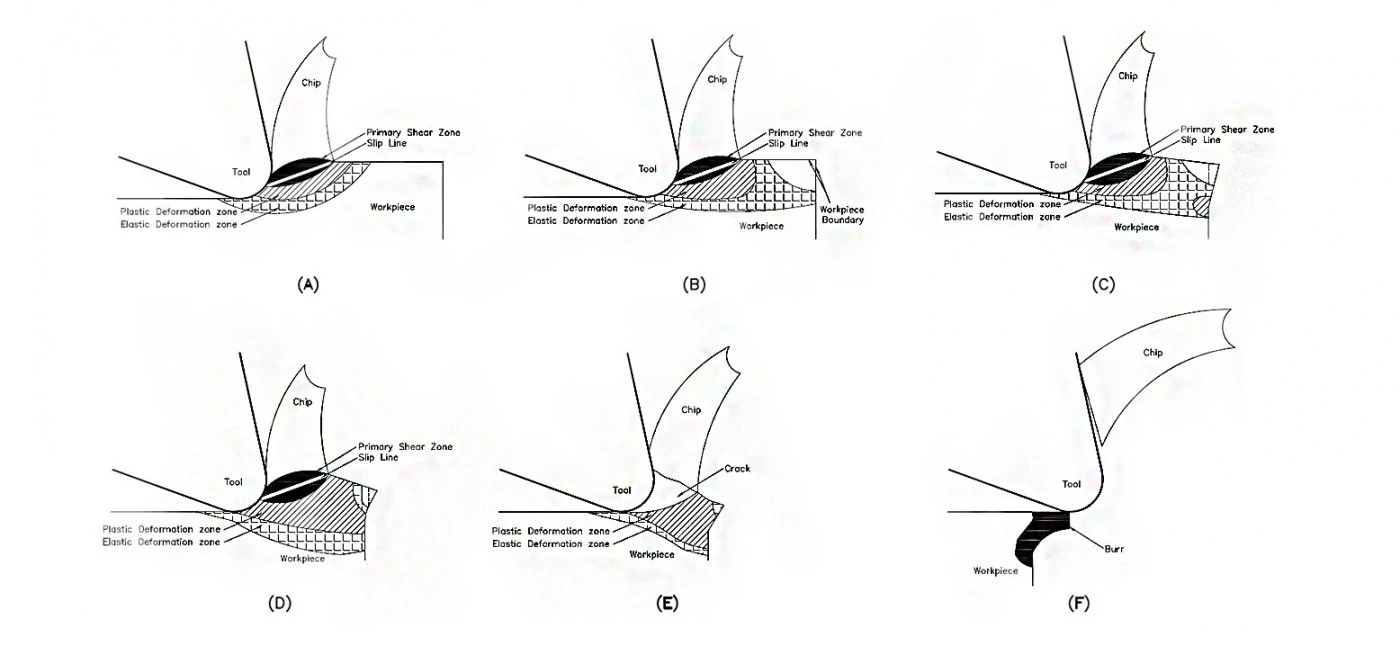
Micromachining may result in an increased amount of burrs and surface roughness when compared to conventional machining. In milling, burring increases as feed increases, and decreases as speed increases. During a machining operation, chips are created by the compression and shearing of the workpiece material along the primary shear zone. This shear zone can be seen in Figure 2 below. As stated before, the chip thickness-to-edge radius ratio is much higher in miniature applications. Therefore, plastic and elastic deformation zones are created during cutting and are located adjacent to the primary shear zone (Figure 2a). Consequently, when the cutting edge is close to the border of the workpiece, the elastic zone also reaches this border (Figure 2b). Plastic deformation spreads into this area as the cutting edge advances, and more plastic deformation forms at the border due to the connecting elastic deformation zones (Figure 2c). A permanent burr begins to form when the plastic deformation zones connect (Figure 2d) and are expanded once a chip cracks along the slip line (Figure 2e). When the chips finally break off from the edge of the workpiece, a burr is left behind (Figure 2f).
Figure 2: Burr formation mechanism using a miniature end mill
Tool Path Best Practices for Miniature End Mills
Because of the fragility of miniature tools, the tool path must be programmed in such a way as to avoid a sudden amount of cutting force, as well as permit the distribution of cutting forces along multiple axes. For these reasons, the following practices should be considered when writing a program for a miniature tool path:
Ramping Into a Part
Circular ramping is the best practice for moving down axially into a part, as it evenly distributes cutting forces along the x, y, and z planes. If you have to move into a part radially at a certain depth of cut, consider an arching tool path as this gradually loads cutting forces onto the tool instead of all at once.
Micromachining in Circular Paths
You should not use the same speeds and feed for a circular path as you would for a linear path. This is because of an effect called compounded angular velocity. Each tooth on a cutting tool has its own angular velocity when it is active in the spindle. When a circular tool path is used, another angular velocity component is added to the system and, therefore, the teeth on the outer portion of tool path are traveling at a substantially different speed than expected. The feed of the tool must be adjusted depending on whether it is an internal or external circular operation. To find out how to adjust your feed, check out this article on running in circles.
Do not approach a miniature slot the same way as you would a larger slot. With a miniature slot, you want as many flutes on the tool as possible, as this increases the rigidity of the tool through a larger core. This decreases the possibility of the tool breaking due to deflection. Because there is less room for chips to evacuate with a higher number of flutes, the axial engagement must be decreased. With larger diameter tools you may be stepping down 50% – 100% of the tool diameter. But when using miniature end mills with a higher flute count, only step down between 5% – 15%, depending on the size of the diameter and risk of deflection. The feed rate should be increased to compensate for the decreased axial engagement. The feed can be increased even high when using a ball nose end mill as chip thinning occurs at these light depths of cut and begins to act like a high feed mill.
Slowing Down Your Feed Around Corners
Corners of a part create an additional amount of cutting forces as more of the tool becomes engaged with the part. For this reason it is beneficial to slow down your feed when machining around corners to gradually introduce the tool to these forces.
This is somewhat of a tricky question to answer when it comes to micromachining. Climb milling should be utilized whenever a quality surface finish is called for on the part print. This type of tool path ultimately leads to more predictable/lower cutting forces and therefore higher quality surface finish. In climb milling, the cutter engages the maximum chip thickness at the beginning of the cut, giving it a tendency to push away from the workpiece. This can potentially cause chatter issues if the setup does not have enough rigidity. In conventional milling, as the cutter rotates back into the cut it pulls itself into the material and increases cutting forces. Conventional milling should be utilized for parts with long thin walls as well as delicate operations.
Combined Roughing and Finishing Operations
These operations should be considered when micromachining tall thin walled parts as in some cases there is not sufficient support for the part for a finishing pass.
Helpful Tips for Achieving Successful Micromachining Operations With Miniature End Mills
Try to minimize runout and deflection as much as possible when micromachining with miniature end mills. This can be achieved by using a shrink-fit or press-fit tool holder. Maximize the amount of shank contact with the collet while minimizing the amount of stick-out during an operation. Double check your print and make sure that you have the largest possible end mill because bigger tools mean less deflection.
Choose an appropriate depth of cut so that the chip thickness to edge radius ratio is not too small as this will cause a ploughing effect.
If possible, test the hardness of the workpiece before machining to confirm the mechanical properties of the material advertised by the vender. This gives the operator an idea of the quality of the material.
Use a coated tool if possible when working in ferrous materials due to the excess amount of heat that is generated when machining these types of metals. Tool coatings can increase tool life between 30%-200% and allows for higher speeds, which is key in micro-machining.
Consider using a support material to control the advent of burrs during a micromachining application. The support material is deposited on the workpiece surface to provide auxiliary support force as well as increase the stiffness of the original edge of the workpiece. During the operation, the support material burrs and is plastically deformed rather than the workpiece.
Use flood coolant to lower cutting forces and a greater surface finish.
Scrutinize the tool path that is to be applied as a few adjustments can go a long way in extending the life of a miniature tool.
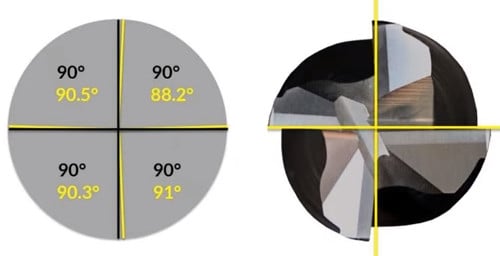
Double-check tool geometry to make sure it is appropriate for the material you are machining. When available, use variable pitch and variable helix tools as this will reduce harmonics at the exceptionally high RPMs that miniature tools are typically run at.
Figure 3: Variable pitch tool (yellow) vs. a non-variable pitch tool (black)
https://www.harveyperformance.com/wp-content/uploads/2020/07/Feature-Image-Machining-with-Miniature-End-Mills-IMG-1.jpg5251400Robert Keeverhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngRobert Keever2020-07-01 10:43:432025-11-12 15:59:31How to Optimize Miniature End Mill Performance
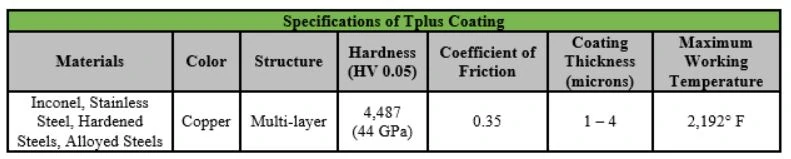
When working with difficult-to-machine materials, such as Inconel, stainless steel, or hardened steels, utilizing an effective coating is important for sustaining the life of your tool and perfecting the outcome of your part. While looking for the right coating, many machinists try out several before finding a solution that works – a process that wastes valuable time and money. One coating gaining popularity in applications involving tough materials is Helical Solutions’ Tplus coating. This post will explore what Tplus coating is (and isn’t), and when it might be best for your specific job.
What is Helical Solutions’ Tplus Coating?
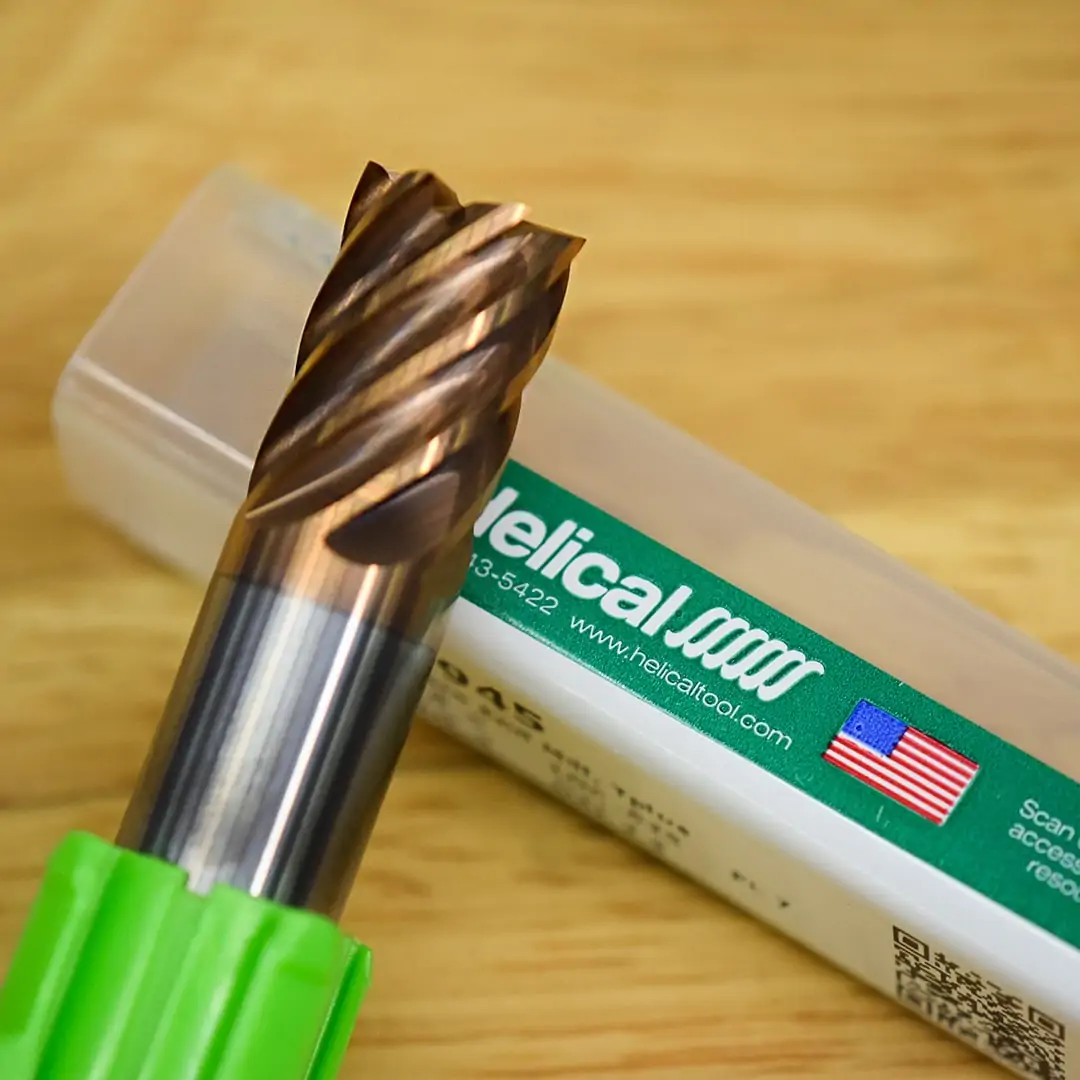
Helical’s Tplus coating is a Titanium-based, multi-layered coating that is applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a near-vacuum and distributes micron-thick layers evenly onto a properly prepared tool. Tplus is a premium, multi-layered, titanium coating that increases edge strength, wear resistance, and tool life.
When Should a Machinist Use Tplus Coating?
When Working in Difficult to Machine Materials
Tplus coating works great in difficult-to-machine materials such as Inconel, stainless steel, hardened steels, and other alloyed steels with a hardness up to 65 Rc. It provides high hardness (44 GPa) for your tool, creating stronger cutting edges and resulting in extended tool life.
When Working in High Temperature Applications
When you are running an application in a ferrous material where extreme heat and work hardening are a possibility, Tplus is a great solution, as it’s designed to withstand high temperatures (up to 2,192°).
In the absence of coolant, fear not! Tplus coating is a viable option since it can handle the heat of machining. The low coefficient of friction (0.35) guarantees great performance in dry machining and allows the coated tool to move throughout the part smoothly, creating less heat, which is extremely beneficial in applications without coolant.
In Large Production Runs
In high production runs is truly where this coating excels, as its properties allow your tool to remain in the spindle longer – creating more parts by avoiding time in swapping out a worn tool.
https://www.harveyperformance.com/wp-content/uploads/2019/08/Feature-Image-Tplus-Coatings-IMG.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2019-08-05 01:39:432024-02-08 15:31:01An In-Depth Look at Helical’s Tplus Coating for End Mills
Aluminum and magnesium alloys are common materials found in machine shops worldwide, and are known as an “easier” material to machine. However, machinists can still experience hiccups while machining this material if they are not prepared with the proper tooling.. When working with aluminum and magnesium alloys, it is important to choose a coating that will work to extend your tool’s life and aid in the removal of chips. A popular choice for this material bucket is Harvey Tool’s TiB2 coating.
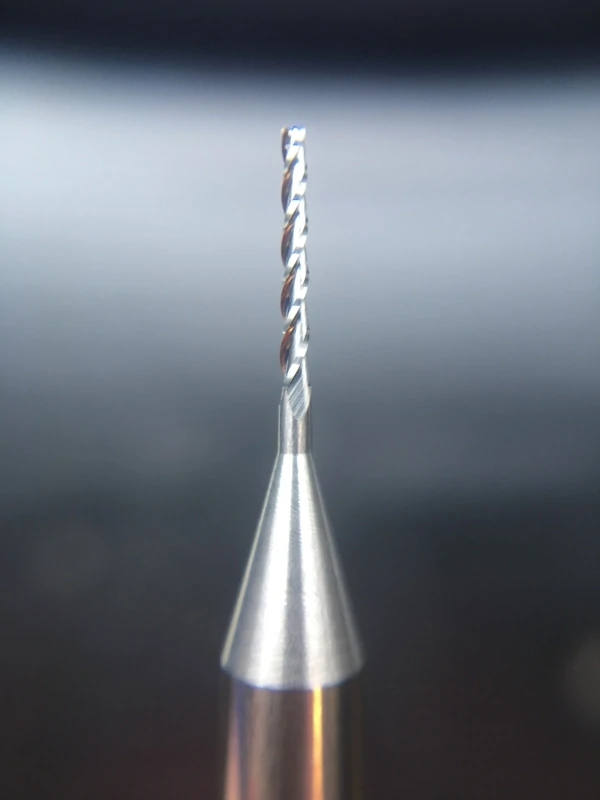
Harvey Tool’s TiB2 coating is a Titanium Diboride, ceramic-based coating that provides superb erosion resistance during machining. TiB2 is added to a tool by a method called Physical Vapor Deposition (PVD), which is conducted in a vacuum where particles are vaporized and applied onto a surface, forming thin layers of material onto the properly-prepped tool. This method enables the coating to be corrosion and tarnish resistant.
TiB2 is identified in Harvey Tool’s product catalog with a “-C8” following the sku number. It can be found offered in Harvey Tool’s lines of Variable Helix End Mills for Aluminum Alloys and Miniature High Performance Drills for Aluminum Alloys.
When Should a Machinist Use TiB2 Coating?
Chip Evacuation Concerns
TiB2 has an extremely low affinity to aluminum, which helps with the chip evacuation process. Simply, chips of a material are able to evacuate through chip valleys easier if they don’t have a high affinity to the coating being used. TiB2 coating does not chemically react with aluminum and magnesium, which allows for smoother chip evacuation, as the chips do not stick to the coating and create issues such as chip packing. This is a common machining mishap that can cause both part and tool damage, quickly derailing a machining operation. By using a coating that increases the lubricity of the tool, chips will not have a surface to stick to and will more smoothly evacuate from the flutes of the tool.
Large Production Runs
While an uncoated tool may work fine in some applications, not all applications can succeed without a tool coating. When working with large production runs where the tools need to hold up through the process of machining large numbers of parts, using a coating is always recommended because they extend the life of your tool.
When is TiB2 Coating Not Beneficial to My Application?
Extremely Abrasive Materials
During the PVD coating process, tools can reach a temperature in excess of 500° F, which can cause the toughness of the carbide to drop slightly. This process does not normally compromise the performance of the tool due to the coating being placed over the carbide. The coating then protects the slightly weakened edge and increases tool performance in recommended materials. Micro-fractures only start appearing when the tool is being run incredibly fast through highly abrasive materials, leading to a decrease in the life of the tool.
Extremely Soft Materials
The coating, while only a few microns thick at most, still provides an ever-so-slight rounded edge to the cutting edge of the tools it is placed on. It is important to take this into consideration, as using the sharpest tools possible when working with materials such as soft plastics is recommended. The sharpest edge possible decreases the likelihood of any “pushing” that might occur on the material and increases the likelihood of proper “shearing” when machining.
When Finish Is Vital
If your part’s finish is imperative to the final product, an uncoated tool may work better for your application. A coating, like stated above, creates a microscopic rounded surface to the cutting edge of the tool. When running tools at finishing speeds and feeds in materials like aluminum, a sharp edge can create the difference between a finished part that does – or does not – pass final inspection.
https://www.harveyperformance.com/wp-content/uploads/2019/03/Feature-Image-TiB2-Coatings-IMG-1.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2019-03-08 09:14:352023-10-24 10:54:05What to Know About Harvey Tool’s TiB2 Coating
Breaking and damaging an end mill is oftentimes an avoidable mistake that can be extremely costly for a machine shop. To save time, money, and your end mill it is important to learn some simple tips and tricks to extend tool life.
Properly Prepare Before the Tool Selection Process
The first step of any machining job is selecting the correct end mill for your material and application. However, this doesn’t mean that there should not be an adequate amount of legwork done beforehand to ensure the right decision on a tool is being made. Harvey Tool, Helical Solutions, Titan USA, and Corehog have thousands of different tools for different operations – a vast selection which, if unprepared – can easily result in selecting a tool that’s not the best for your job. To start your preparation, answer the 5 Questions to Ask Before Selecting an End Mill to help you quickly narrow down your selection and better understand the perfect tool you require.
Understand Your Tooling Requirements
It’s important to understand not only what your tool needs, but also general best practices to avoid common machining mishaps. For instance, it is important to use a tool with a length of cut only as long as needed, as the longer a tools length of cut is, the greater the chance of deflection or tool bending, which can decrease its effective life.
Another factor to consider is the coating composition on a tool. Harvey Tool and Helical Solutions offer many varieties of tool coatings for different materials. Some coatings increase lubricity, slowing tool wear, while others increase the hardness and abrasion resistance of the tool. Not all coatings increase your tool’s life in every material, however. Be wary of coatings that don’t perform well in your part’s material – such as the use of AlTiN coating in Aluminum (Both coating and material are aluminum-based and have a high affinity for each other, which can cause built-up edge and result in chip evacuation problems).
Consider Variable Helix & Pitch Geometry
A feature on many of our high performance end mills is variable helix or variable pitch geometry, which have differently-spaced flutes. As the tool cuts, there are different time intervals between the cutting edges contacting the workpiece, rather than simultaneously on each rotation. The varying time intervals minimizes chatter by reducing harmonics, increasing tool life and producing better results.
Ensure an Effective Tool Holding Strategy
Another factor in prolonging tool life is proper tool holding. A poor tool holding strategy can cause runout, pullout, and scrapped parts. Generally, the most secure connection has more points of contact between the tool holder and tool shank. Hydraulic and Shrink Fit Tool Holders provide increased performance over other tightening methods.
Helical also offers shank modifications to all stocked standards and special quotes, such as the ToughGRIP Shank, which provides added friction between the holder and the shank of the tool for a more secure grip; and the Haimer Safe-Lock™, which has grooves on the shank of the tool to help lock it into place in a tool holder.
Trust Your Running Parameters, and their Source
After selecting the correct end mill for your job, the next step is to run the tool at the proper speeds and feeds.
Run at the Correct Speed
Understanding the ideal speed to run your machine is key to prolonging tool life. If you run your tool too fast, it can cause suboptimal chip size, ineffective chip evacuation, or even total tool failure. Adversely, running your tool too slowly can result in deflection, bad finish, or decreased metal removal rates.
Push at the Best Feed Rate
Another critical parameter of speeds and feeds is finding the best possible feed rate for your job, for sake of both tool life and achieving maximum shop efficiency. Pushing your tool too aggressively can result in breakage, but being too conservative can lead to recutting chips and excess heat generation, accelerating tool wear.
Use Parameters from Your Tooling Manufacturer
A manufacturer’s speeds and feeds calculations take into account every tool dimension, even those not called out in a catalog and readily available to machinists. Because of this, it’s best to rely on running parameters from tooling manufacturers. Harvey Tool offers speeds and feeds charts for every one of its more than 21,000 tools featured in its catalog, helping machinists to confidently run their tool the first time.
Harvey Performance Company offers the Machining Advisor Pro application, a free, cutting-edge resource that generates custom running parameters for optimized machining with all of Helical Solutions’ and Harvey Tool’s products.
Opt for the Right Milling Strategy: Climb vs Conventional
There are two ways to cut material when milling: Climb Milling and Conventional Milling. In conventional milling, the cutter rotates against the feed. In this method, chips will start at theoretical zero and increase in size. Conventional milling is usually recommended for tools with higher toughness, or for breaking through case hardened materials.
In Climb Milling, the cutter rotates with the feed. Here, the chips start at maximum width and decrease, causing the heat generated to transfer into the chip instead of being left in the tool or work piece. Climb milling also produces a cleaner shear plane, causing less rubbing, decreasing heat, and improving tool life. When climb milling, chips will be removed behind the cutter, reducing your chances of recutting.
Utilize High Efficiency Milling
High Efficiency Milling (HEM), is a roughing technique that uses the theory of chip thinning by applying a smaller radial depth of cut (RDOC) and a larger axial depth of cut (ADOC). The parameters for HEM are similar to that of finishing, but with increased speeds and feeds, allowing for higher material removal rates (MRR). HEM utilizes the full length of cut instead of just a portion of the cutter, allowing heat to be distributed across the cutting edge, maximizing tool life and productivity. This reduces the possibility of accelerated tool wear and breakage.
Decide On Coolant Usage & Delivery
Coolant can be an extremely effective way to protect your tool from premature wear and possible tool breakage. There are many different types of coolant and methods of delivery to your tool. Coolant can come in the form of compressed air, water-based, straight oil-based, soluble oil-based, synthetic or semi-synthetic. It can be delivered as mist, flood, high pressure or minimum quantity lubricant.
Appropriate coolant type and delivery vary depending on your application and tool. For example, using a high pressure coolant with miniature tooling can lead to tool breakage due to the fragile nature of extremely small tools. In applications of materials that are soft and gummy, flood coolant washes away the long stringy chips to help avoid recutting and built-up edge, preventing extra tool wear.
Extend Your Tool’s Life
The ability to maximize tool life saves you time, money and headaches. To get the best possible outcome from your tool, you first need to be sure you’re using the best tool for your job. Once you find your tool, ensure that your speeds and feeds are accurate and are from your tooling manufacturer. Nobody knows the tools better than they do. Finally, think about how to run your tool: the rotation of your cutter, whether utilizing an HEM approach is best, and how to introduce coolant to your job.
https://www.harveyperformance.com/wp-content/uploads/2018/12/Featured-Image-Life-of-End-Mill-IMG.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2018-12-05 11:28:212023-10-24 09:56:33How to Extend the Life of Your End Mill