Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

The Key Differences Between Helical’s Tool Coatings

November 13, 2025/0 Comments/in CNC Machining, Helical Solutions, Large Featured, Tool Coatings, Tool Selection/by Michaela Martell

Tool coatings are added to protect against the forces that wear down cutting tools. They play a critical role in CNC machining by reducing heat generation and friction while enhancing overall tool performance. Below is an overview of Helical Solutions’ coating options, including which tool families they pair with, the applications they’re best suited for, and helpful application tips.

Helical Solutions demonstrates its commitment to performance by delivering high-performance carbide end mills and tools designed to reduce cycle times, improve part finishes, and extend tool life. This is achieved through a focus on exceptional quality and innovation, utilizing precision CNC manufacturing, advanced design techniques, and a world-class team of engineers and technical experts. Helical Solutions aims to be a true superior product performance, and responsive technical support.

The following information will help machinists understand the differences between Helical’s coating options and how to select the right one based on material and application.

What Are Tool Coatings and Why Are They Important?
Tool coatings are applied to a tool’s cutting surface through a process called PVD (Physical Vapor Deposition). PVD and CVD are two different types of coating applications, with PVD being the common process for Helical’s tools.

This near-vacuum process distributes micron-thick layers evenly onto a properly prepared tool, helping it maintain a sharper cutting edge. When selecting tool coatings, machinists should consider material type, coolant use, and how the

material and operation may affect the cutting edges. Understanding these factors is essential to extending tool life.

Some key benefits of coatings include improved thermal resistance, better chip evacuation, increased lubricity (which allows chips to slide more easily down the flute), and higher microhardness. These properties reduce tool wear, enhance performance in material-specific applications, and extend tool life during production runs.

Helical’s coating lineup is designed with specific materials and applications in mind. Selecting the right coating for your job can have a major impact on tool life, heat control, and overall performance.

How to Choose the Right Coating:

Choosing the proper coating for your application is crucial, as each Helical coating is optimized for specific materials. Consider the following when selecting:
– What material are you machining?
– Will the material work harden quickly under heat?
– What is its coefficient of friction?
– Will you be using coolant?
– What is your expected tool life for this production run?

Application Tips:

Coatings in Coolant Applications:

Most coatings perform better with coolant, but there are exceptions.

Tplus performs well in many materials, but when cutting hardened steels, the combination of high heat and coolant can cause thermal shock, resulting in tool fractures.

In composites and non-metallic materials—often machined with Dplus—using coolant can create a slurry and increase wear between the tool and workpiece. For these materials, dry machining is generally preferred.

Zplus vs. Nplus vs. Dplus

For aluminum and non-ferrous applications, coatings are found on Helical’s HVAL and HMAF tool families.

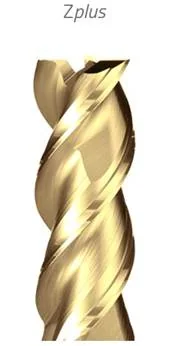
– Zplus is Helical’s longstanding coating for aluminum and non-ferrous materials.
– Nplus improves tool life compared to Zplus and features a harder, smoother coating—ideal for larger production jobs in tougher materials.
– Dplus is a tetrahedral amorphous carbon coating known for extreme wear resistance and performance in abrasive materials. For shops seeking a DLC-style coating, Dplus is Helical’s recommendation.

Uncoated (or bright) tools can be used in aluminum applications, but adding a coating generally improves productivity and helps prevent material from welding onto the tool.

Aplus vs. Tplus
– Aplus is a tough, multi-layer coating that enhances adhesion, edge retention, and heat resistance. It performs best in steels under 45 Rc. Helical’s HSV, HEV, and HSF tool families are excellent choices with this coating. Aplus is not recommended for aluminum, as it can cause galling (when material adheres to the tool), negatively impacting cutting performance and chip evacuation.

– Tplus is a premium coating offering top-tier performance in ferrous materials. It has a slight edge over Aplus, particularly in stainless steels and nickel alloys, and is optimal for cutting materials between 45 Rc and 65 Rc. It supports higher temperatures, maintains edge retention, and reduces wear. However, due to its hardness, it may generate more heat—and, as mentioned earlier, coolant can sometimes lead to thermal shock in these conditions.
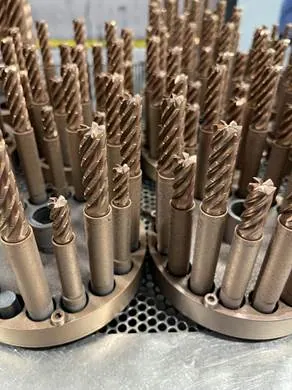
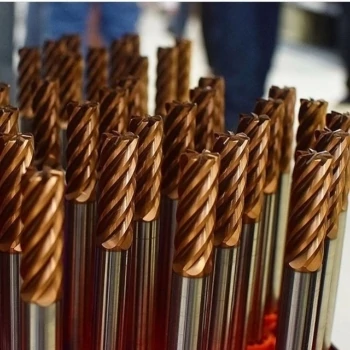
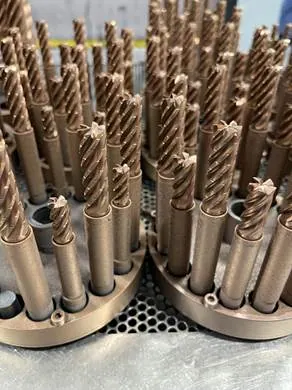
tplus coated helical end mills in holders following the coating process

Tplus has also shown success in titanium applications. Both Aplus and Tplus are suitable choices for these materials. You can find Tplus coatings on Helical’s HSV, HEV, and HVSS-6 tool families. The HVSS-6 line, in particular, has proven optimal for cutting 316 stainless steels.

There are no setup differences between these coatings when programming your machine. Speeds and feeds depend on the specific toolpath and family used, though coatings generally allow for higher cutting speeds. Choosing the correct coating for your material results in longer tool life and more efficient production.

Tool Storage Recommendations

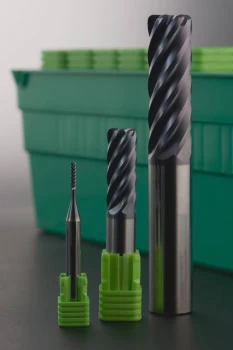
helical end mills in clear cases with green tops

For best results, Helical recommends storing tools in individual padded tubes rather than in shared bins. This prevents damage to flutes, cutting edges, and coatings. A clean, dry environment helps maintain tool quality and ensures consistent performance over time.

Conclusion

Tool coatings are essential for optimizing performance based on the material being machined. Helical’s coatings are engineered, tested, and proven to deliver the best results across specific materials and applications. By pairing the right tool family and coating, machinists can improve machining efficiency, enhance part quality, and extend tool life.

For more insights on cutting tool coatings, watch this episode of In the Loupe TV: Cutting Tool Coatings.

If you have additional questions about coatings or specific applications, contact Helical’s technical team for guidance at 1-866-543-5422 or by email. Helical’s experts are ready to help you find the ideal tool and coating combination for your needs.
https://www.harveyperformance.com/wp-content/uploads/2025/11/Helical-Tool-Coatings.jpg 525 1400 Michaela Martell http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Michaela Martell2025-11-13 09:29:232025-11-13 16:47:39The Key Differences Between Helical’s Tool Coatings

The Experts’ Guide to CNC Engraving

September 15, 2025/0 Comments/in CNC Machining, Harvey Tool, Large Featured, Machining 101, Machining Techniques, Milling, Milling, Specialty Tools, Tool Coatings, Tool Geometry, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

CNC engraving is a process that removes a small amount of material to create detailed images or shapes. Many manufacturers use this method for labeling parts or creating complex designs; however, not everyone is aware of the key techniques necessary for optimal results. When using an engraving tool, it is essential to consider several challenges that could affect both the tool and the operation.

Advantages of CNC Engraving

Compared to other engraving methods, CNC engraving is fast, consistent, and cost-effective. Thanks to their repeatability, CNC machines deliver consistent results when paired with a high-quality engraving tool. We suggest running the tool at a minimum of 6,000 RPM.

If your machine supports it, increasing the RPM can lead to even greater results. Running at lower speeds can negatively impact tool life. Choosing the right engraving tool requires considering production volume and tool engagement time. Key factors such as tip design, angle, and coating play a crucial role in maximizing efficiency and durability.

Proper Engraver Tool Selection

Most machinists understand that a square-corner end mill does not last as long as a corner-radius or ball-end mill due to its fragile cutting edge.

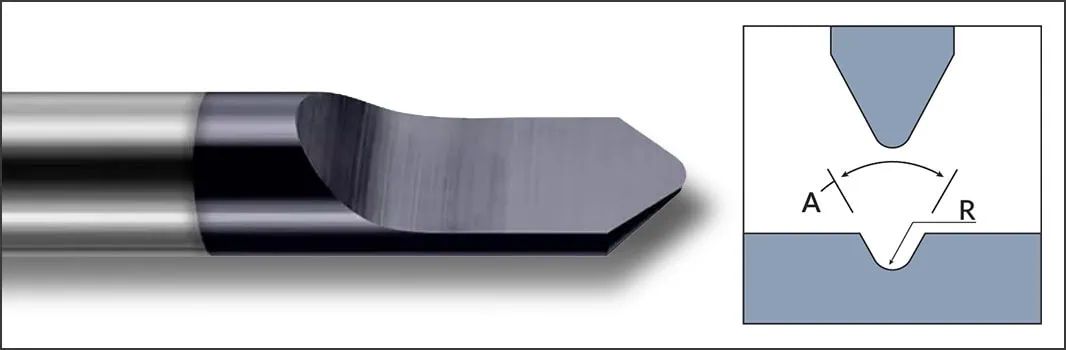
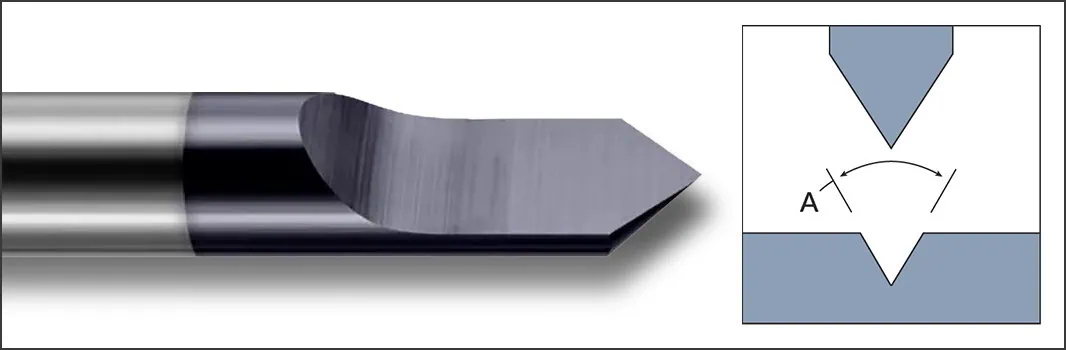
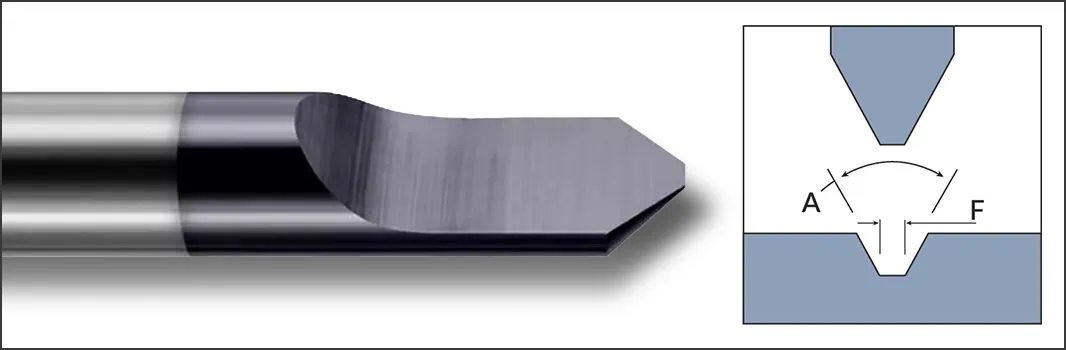
The same principle applies to CNC engraving tools. An engraver that comes to a sharp point is more fragile than one with a tipped-off or radius tip. For long production runs, consider using a tip-off or rounded tip design, as these geometries distribute cutting forces more evenly across the cutting edge, improving tool longevity. A tip-flat design will last longer than a pointed tip but not as long as a radius tip. If high-detail work is required, a pointed tip is preferable because it provides greater precision.

Pointed Tip Engraving Cutters
Tipped Off Engraving Cutters
Tip Radius Engraving Cutters

Environment and Detail Considerations

Similar to tip geometry, the engraving angle plays a critical role in visibility. The environment in which the engraving is used affects how well it can be seen. If the engraving is exposed to harsh conditions with elements like snow, mud, or dirt, debris can accumulate in the grooves, making it difficult to see and clean. A larger angle creates a wider groove, improving visibility and ease of cleaning.

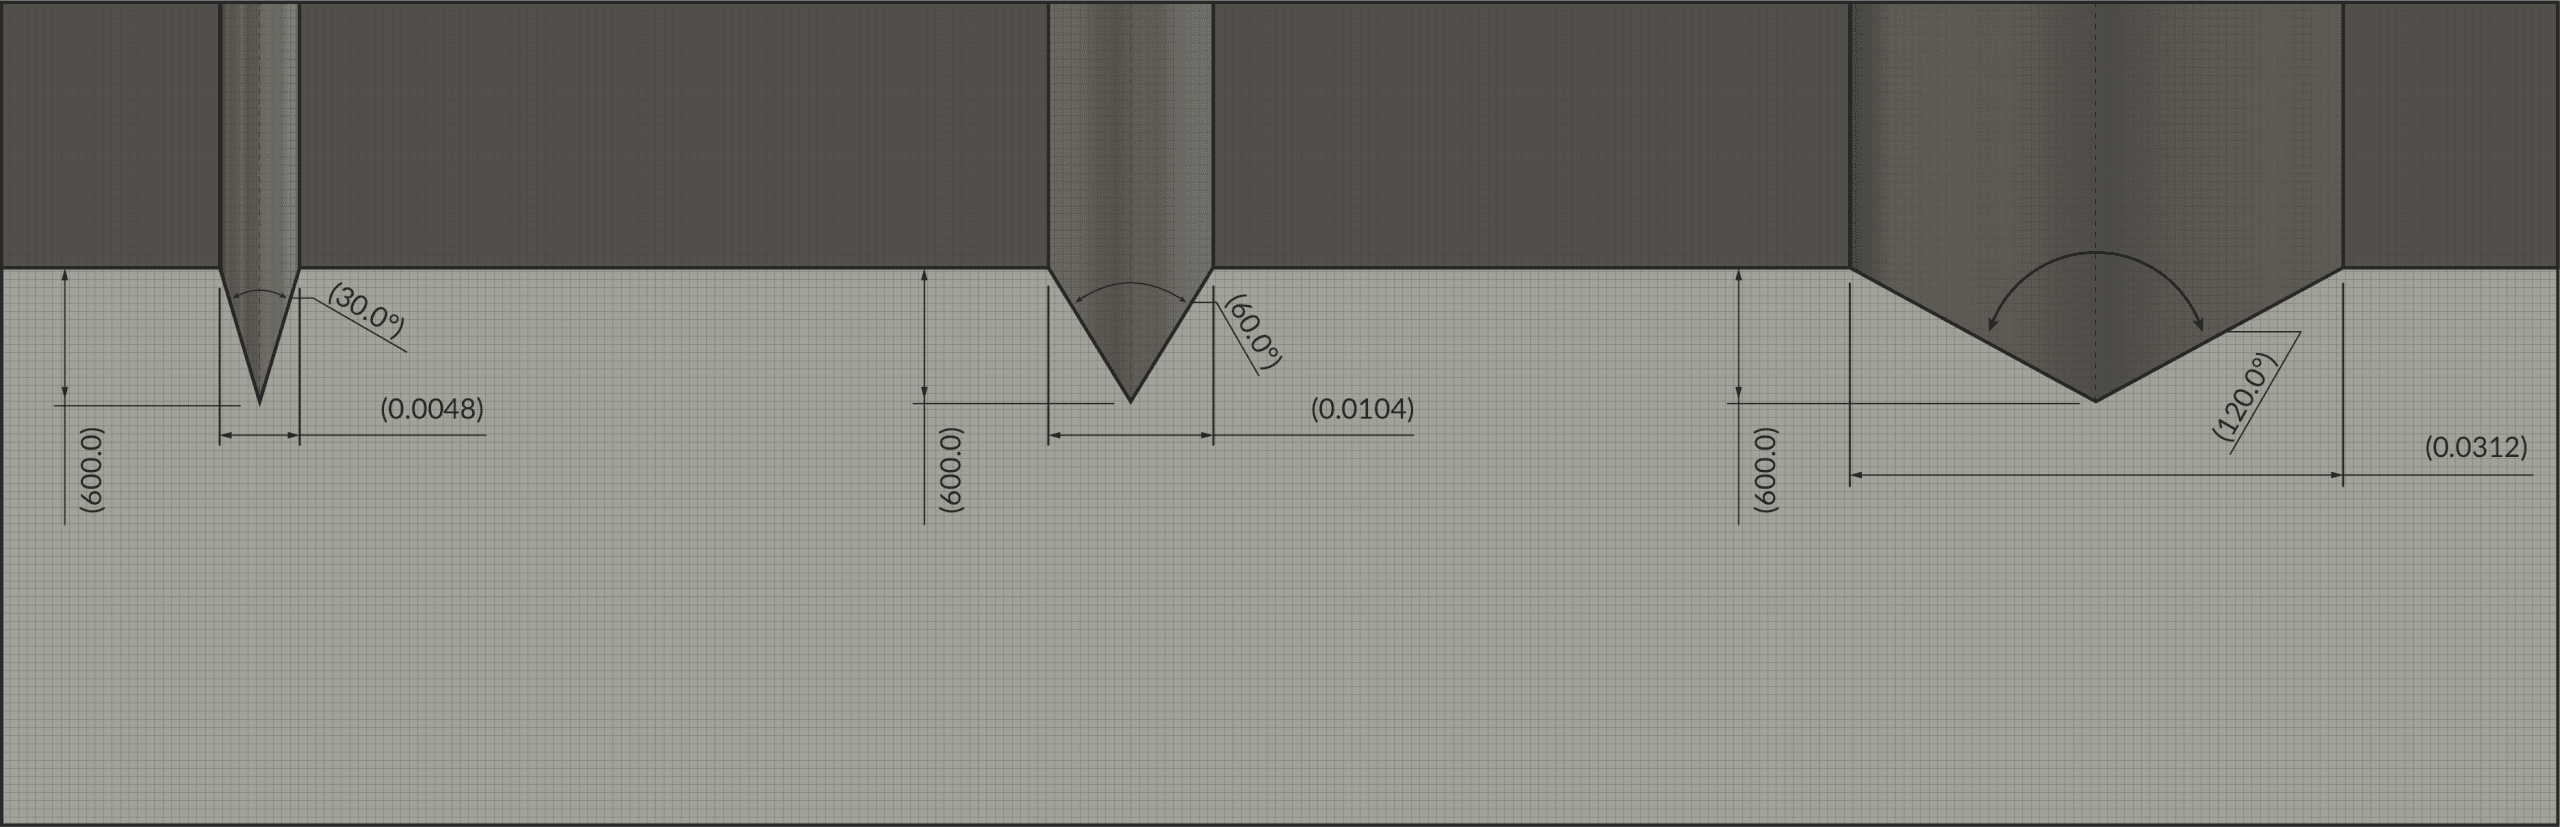
The image below illustrates three different engraving angles offered by Harvey: the leftmost groove is 30° included, the middle groove is 60° included, and the rightmost groove is 120° included. Each of these engravings is only 0.009 inches deep.

Notice that the 120° engraving is more visible at a distance due to increased surface exposure. If a job requires precision and detail, a smaller angle is preferable. While geometry significantly impacts engraving visibility and tool longevity, another key factor in tool performance is the choice of coating.

Choosing a Tool Coating

A coated engraving tool will last longer than an uncoated one because the coating provides a protective barrier between the tool and the workpiece. Additionally, coatings help reduce heat absorption, increase lubricity, and decrease tool wear. Selecting the right coating depends on the material being machined.

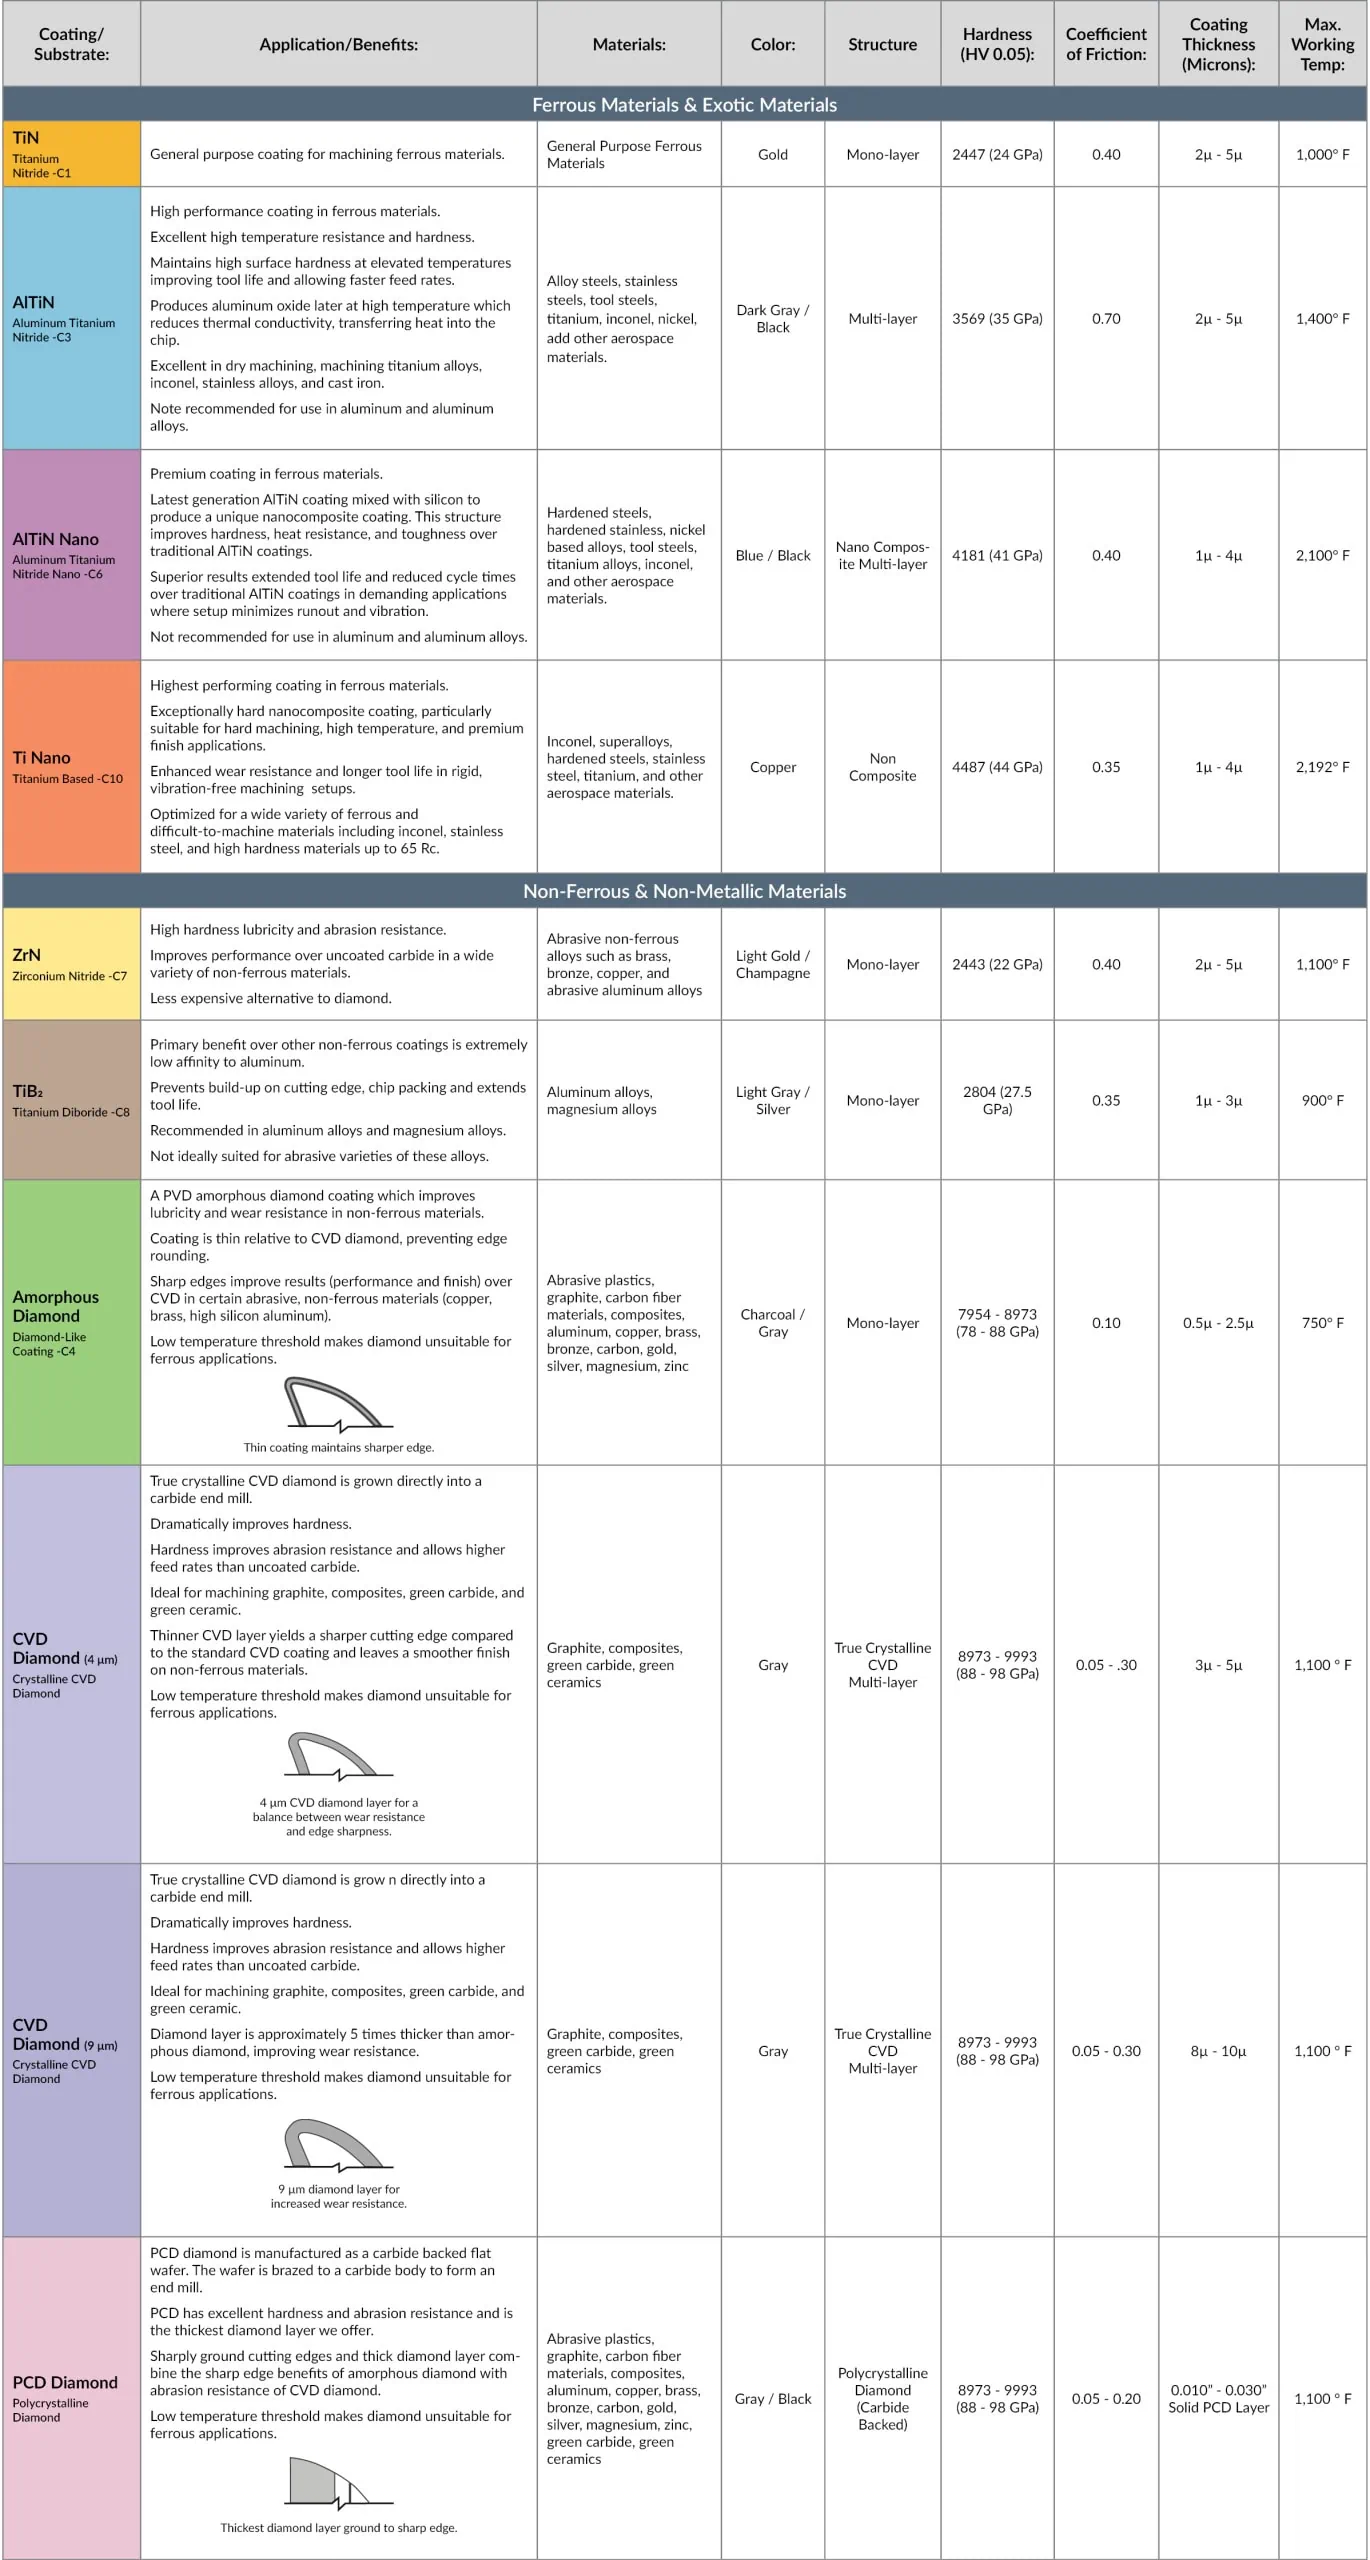
For example, our AlTiN and AlTiN-Nano coatings perform best in stainless steel and nickel alloys. For non-ferrous materials such as aluminum or copper, our Amorphous Diamond coating is ideal. As an alternative to our Amorphous Diamond coating, we also offer ZrN or TiB2 coatings.

A common misconception is that diamond-coated tools can be used on ferrous materials. Instead, this leads to rapid heat generation and premature tool failure.

Successfully Running Your Engraver

Selecting the correct engraving tool is just as important as understanding how to operate it properly. Even the highest-quality tool will be wasted if not used correctly. As with any machining operation, you must consider depth of cut, work holding methods, and appropriate speeds and feeds

Cutting Speeds and Feeds for Engraving 

The tip is the most delicate area of the tool which makes running at the correct speed and feed rate crucial. Running at an incorrect speed and feed rate can cause deflection, which will lead to an inaccurate engraving, chipping, breaking, or a poor surface finish.

At Harvey, we recommend a minimum spindle speed of 6,000 RPM. Operating at higher RPMs, when possible, offers even better support for tool tip integrity.

Higher speeds ensure tool stability as it will be less likely to cause vibration and reduces heat buildup during operation. Running too slowly generates excess heat and vibration leading to chipping, breakage, or having a poor surface finish. To help maintain tool tip integrity, it is important to follow the recommended depth of cut and consider the way the engraver enters the material.

Determining Depth of Cut

Many machinists are unaware that taking cuts deeper than 0.009 inches can shorten the lifespan of a Harvey engraving tool. For depth of cut ranging from 0.001 inch to 0.009 inches, you can operate within our stated speed and feed guidelines. If the operation requires a deeper groove, the chip load must be reduced accordingly. For depths between 0.010 inches and 0.015 inches, reduce the chip load by 20%. For depths ranging from 0.016 inches to 0.020 inches, reduce the chip load by 30%. Depth of cut also influences visibility. A deeper cut made with a tool that has a smaller angle can provide similar visibility to a shallower cut made with a tool that has a larger angle.

The image below illustrates different engraving depths using a 30° included angle. From left to right, the depths are 0.009 inches, 0.015 inches, and 0.020 inches. As depth increases, visibility improves. When engaging the tool with the workpiece, it is best to ramp into the material to protect the tool tip.

We recommend a ramp angle of 1° to 3° for ferrous materials such as stainless steel, and 3° to 10° for non-ferrous materials like aluminum or copper. If ramping is not an option, you may plunge the tool into the material. However, the chip load must be reduced by 50% during entry. Once the desired depth is reached, you can return to the recommended running parameters. Another key consideration is ensuring the workpiece is securely held in place.

Workholding Considerations

Runout or vibration during engraving can result in uneven cuts and tool failure. To prevent this, ensure that engraving tools are held in a sturdy toolholder and that the workpiece is secured. A shrink-fit toolholder minimizes runout and provides excellent stability. While ER collets are acceptable, they wear overtime. To verify an ER collet’s suitability, place an indicator on the tool shank and rotate the tool within the collet. The goal is to achieve the least possible runout, ideally no more than 0.0003 inches.

The workpiece should also be properly secured, either in a vise or a fixture. To detect vibrations during operation, listen for irregular noise or feel for vibrations through the CNC machine door. For cooling, coolants are recommended for metallic workpieces, while an air blast is preferable for non-metallic materials such as plastic.

Conclusion

When selecting an engraving tool, it is essential to choose the correct geometry for the operation, as well as the appropriate coating for the material being machined. Regardless of tip geometry, the engraving tool’s tip is its most fragile part. Proper speed, feed rate, and depth of cut are crucial for maximizing tool life.

For metallic workpieces, a cooling method such as coolant is necessary, while non-metallic workpieces require an air blast. Before starting a new engraving operation, double-check tool runout and ensure that the workpiece is securely held in place.

By following these best practices, CNC engraving operations can achieve high precision, longevity, and optimal tool performance.

Are You Ready to Put Your Engraving Knowledge to Use?

Browse Harvey Tool’s full selection of precision engravers, coatings, and geometries designed for optimal performance in a wide range of materials.

https://www.harveyperformance.com/wp-content/uploads/2025/09/Engraving-Tools-Featured.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-09-15 08:59:352025-09-16 09:46:49The Experts’ Guide to CNC Engraving

An In-Depth Look at Helical’s Tplus Coating for End Mills

August 5, 2019/0 Comments/in Helical Solutions, Material Specific, Milling, Steels, Tool Coatings, Tool Selection/by Harvey Performance Company

When working with difficult-to-machine materials, such as Inconel, stainless steel, or hardened steels, utilizing an effective coating is important for sustaining the life of your tool and perfecting the outcome of your part. While looking for the right coating, many machinists try out several before finding a solution that works – a process that wastes valuable time and money. One coating gaining popularity in applications involving tough materials is Helical Solutions’ Tplus coating. This post will explore what Tplus coating is (and isn’t), and when it might be best for your specific job.

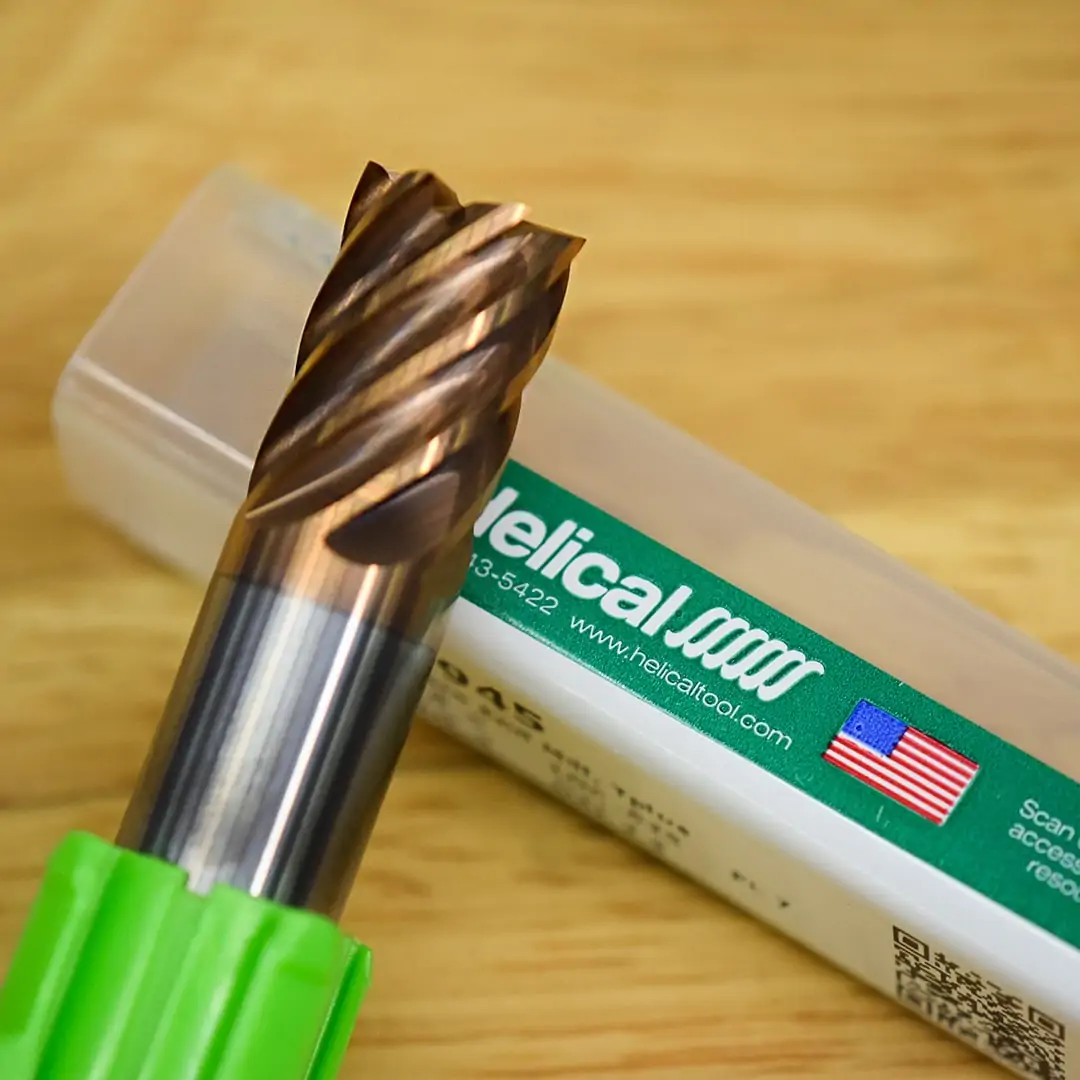
tplus coating on helical end mill

What is Helical Solutions’ Tplus Coating?

Helical’s Tplus coating is a Titanium-based, multi-layered coating that is applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a near-vacuum and distributes micron-thick layers evenly onto a properly prepared tool.  Tplus is a premium, multi-layered, titanium coating that increases edge strength, wear resistance, and tool life.

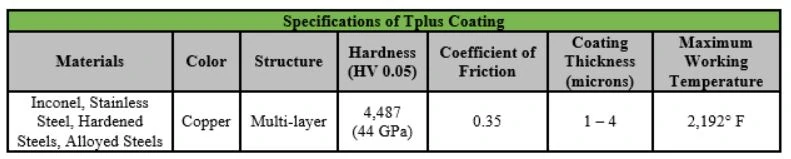
tplus coating specification chart

When Should a Machinist Use Tplus Coating?

When Working in Difficult to Machine Materials

Tplus coating works great in difficult-to-machine materials such as Inconel, stainless steel, hardened steels, and other alloyed steels with a hardness up to 65 Rc. It provides high hardness (44 GPa) for your tool, creating stronger cutting edges and resulting in extended tool life.

When Working in High Temperature Applications

When you are running an application in a ferrous material where extreme heat and work hardening are a possibility, Tplus is a great solution, as it’s designed to withstand high temperatures (up to 2,192°).

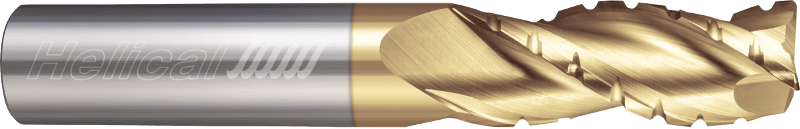
Helical Solutions’ 7 Flute Tplus End Mill

In Dry Machining Applications

In the absence of coolant, fear not! Tplus coating is a viable option since it can handle the heat of machining. The low coefficient of friction (0.35) guarantees great performance in dry machining and allows the coated tool to move throughout the part smoothly, creating less heat, which is extremely beneficial in applications without coolant.

In Large Production Runs

In high production runs is truly where this coating excels, as its properties allow your tool to remain in the spindle longer – creating more parts by avoiding time in swapping out a worn tool.

https://www.harveyperformance.com/wp-content/uploads/2019/08/Feature-Image-Tplus-Coatings-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-08-05 01:39:432024-02-08 15:31:01An In-Depth Look at Helical’s Tplus Coating for End Mills

What to Know About Helical Solution’s Zplus Coating

April 1, 2019/0 Comments/in Aluminum, CNC Machining, Helical Solutions, Machining Techniques, Material Specific, Tool Coatings, Tool Selection/by Harvey Performance Company

Non-ferrous and non-metallic materials are not usually considered difficult to machine, and therefore, machinists often overlook the use of tool coatings. But while these materials may not present the same machining difficulties as hardened steels and other ferrous materials, a coating can still vastly improve performance in non-ferrous applications. For instance, materials such as aluminum and graphite can cause machinists headaches because of the difficulty they often create from abrasion. To alleviate these issues in non-ferrous machining applications, a popular coating choice is Helical Solution’s Zplus coating.

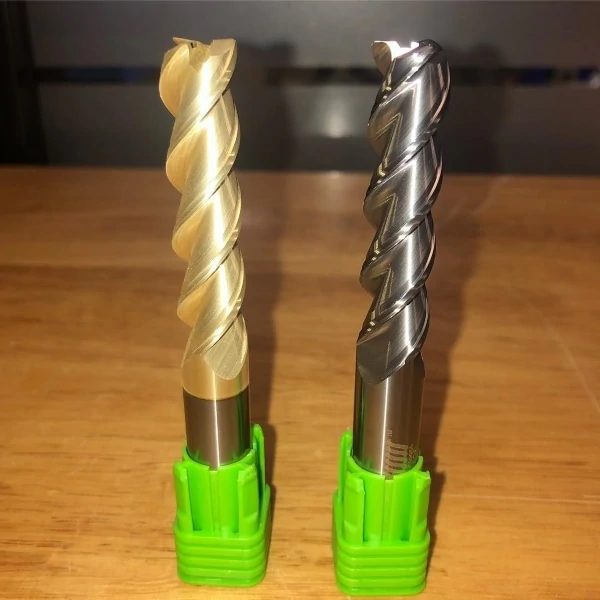
zplus coated helical chipbreaker end mill

What is Helical Solutions’ Zplus Coating?

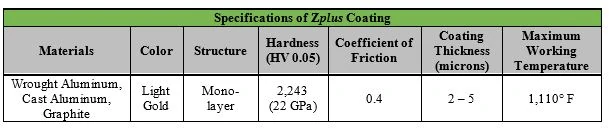
Helical’s Zplus is a Zirconium Nitride-based coating, applied by a Physical Vapor Deposition (PVD) process. This method of coating takes place in a vacuum and forms layers only microns thick onto the properly prepared tool. Zirconium Nitride does not chemically react to a variety of non-ferrous metals, increasing the lubricity of the tool and aiding in chip evacuation.

zplus coating specification chart

When Should a Machinist Use Helical Solution’s Zplus?

Working with Abrasive Materials

While Zplus was created initially for working in aluminum, its hardness level and maximum working temperature of 1,110°F enables it to work well in abrasive forms of other non-ferrous materials, as well. This coating decreases the coefficient of friction between the tool and the part, allowing it to move easier through more abrasive materials. This abrasion resistance decreases the rate of tool wear, prolonging tool life.

Concerns with Efficient Chip Evacuation

One of the primary functions of this coating is to increase the smoothness of the flutes of the tool, which allows for more efficient chip removal. By decreasing the amount of friction between the tool and the material, chips will not stick to the tool, helping to prevent chip packing. The increased lubricity and smoothness provided by the coating allows for a higher level of performance from the cutting tool. Zplus is also recommended for use in softer, gummy alloys, as the smooth surface encourages maximum lubricity within the material – this decreases the likelihood of those gummier chips sticking to the tool while machining.

Large Production Runs

Uncoated tools can work well in many forms of non-ferrous applications. However, to get a genuinely cost-effective tool for your job, the proper coating is highly recommended. Large production runs are known for putting a lot of wear and tear on tools due to their increased use, and by utilizing an appropriate coating, there can be a significant improvement in the tools working life.

3 flute corner radius end mill for aluminum

When is Zplus Coating Not Beneficial to My Application?

Finishing Applications

When your parts finish is vital to its final application, a machinist may want to consider going with an uncoated tool. As with any coating, ZrN will leave a very minor rounded edge on the tip of the cutting edge. The best finish often requires an extremely sharp tool, and an uncoated tool will have a sharper cutting edge than its coated version.

https://www.harveyperformance.com/wp-content/uploads/2019/04/Feature-Image-Zplus-Coatings-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-04-01 03:17:542023-10-24 10:53:44What to Know About Helical Solution’s Zplus Coating

What to Know About Harvey Tool’s TiB2 Coating

March 8, 2019/0 Comments/in Aluminum, CNC Machining, Harvey Tool, Material Specific, Milling, Tool Coatings, Tool Selection/by Harvey Performance Company

Aluminum and magnesium alloys are common materials found in machine shops worldwide, and are known as an “easier” material to machine. However, machinists can still experience hiccups while machining this material if they are not prepared with the proper tooling.. When working with aluminum and magnesium alloys, it is important to choose a coating that will work to extend your tool’s life and aid in the removal of chips. A popular choice for this material bucket is Harvey Tool’s TiB2 coating.

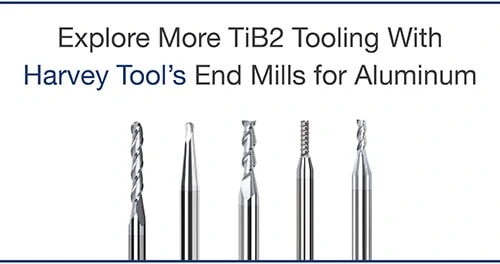
Explore More TiB2 Tooling With Harvey Tool’s End Mills for Aluminum

What is Harvey Tool’s TiB2 Coating?

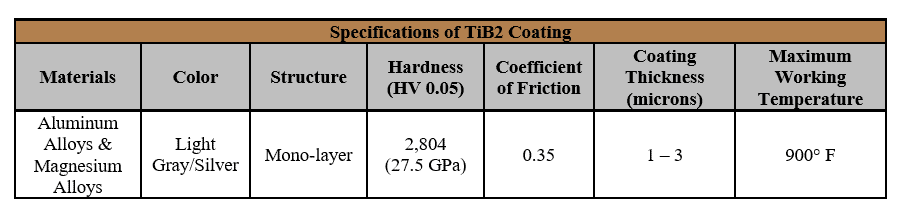
Harvey Tool’s TiB2 coating is a Titanium Diboride, ceramic-based coating that provides superb erosion resistance during machining. TiB2 is added to a tool by a method called Physical Vapor Deposition (PVD), which is conducted in a vacuum where particles are vaporized and applied onto a surface, forming thin layers of material onto the properly-prepped tool. This method enables the coating to be corrosion and tarnish resistant.

TiB2 Coating Specification chart

TiB2 is identified in Harvey Tool’s product catalog with a “-C8” following the sku number. It can be found offered in Harvey Tool’s lines of Variable Helix End Mills for Aluminum Alloys and Miniature High Performance Drills for Aluminum Alloys.

When Should a Machinist Use TiB2 Coating?

Chip Evacuation Concerns

TiB2 has an extremely low affinity to aluminum, which helps with the chip evacuation process. Simply, chips of a material are able to evacuate through chip valleys easier if they don’t have a high affinity to the coating being used. TiB2 coating does not chemically react with aluminum and magnesium, which allows for smoother chip evacuation, as the chips do not stick to the coating and create issues such as chip packing. This is a common machining mishap that can cause both part and tool damage, quickly derailing a machining operation. By using a coating that increases the lubricity of the tool, chips will not have a surface to stick to and will more smoothly evacuate from the flutes of the tool.

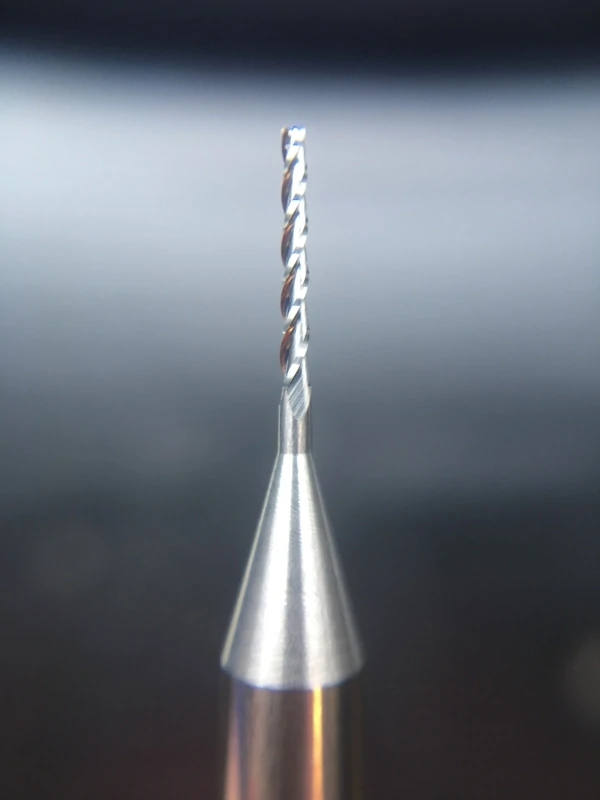
tib2 coated cnc end mill

Large Production Runs

While an uncoated tool may work fine in some applications, not all applications can succeed without a tool coating. When working with large production runs where the tools need to hold up through the process of machining large numbers of parts, using a coating is always recommended because they extend the life of your tool.

When is TiB2 Coating Not Beneficial to My Application?

Extremely Abrasive Materials

During the PVD coating process, tools can reach a temperature in excess of 500° F, which can cause the toughness of the carbide to drop slightly. This process does not normally compromise the performance of the tool due to the coating being placed over the carbide. The coating then protects the slightly weakened edge and increases tool performance in recommended materials. Micro-fractures only start appearing when the tool is being run incredibly fast through highly abrasive materials, leading to a decrease in the life of the tool.

Extremely Soft Materials

The coating, while only a few microns thick at most, still provides an ever-so-slight rounded edge to the cutting edge of the tools it is placed on. It is important to take this into consideration, as using the sharpest tools possible when working with materials such as soft plastics is recommended. The sharpest edge possible decreases the likelihood of any “pushing” that might occur on the material and increases the likelihood of proper “shearing” when machining.

When Finish Is Vital

If your part’s finish is imperative to the final product, an uncoated tool may work better for your application. A coating, like stated above, creates a microscopic rounded surface to the cutting edge of the tool. When running tools at finishing speeds and feeds in materials like aluminum, a sharp edge can create the difference between a finished part that does – or does not – pass final inspection.

https://www.harveyperformance.com/wp-content/uploads/2019/03/Feature-Image-TiB2-Coatings-IMG-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-03-08 09:14:352023-10-24 10:54:05What to Know About Harvey Tool’s TiB2 Coating

Shining a Light on Diamond End Mills

May 10, 2018/5 Comments/in CNC Machining, Tool Coatings, Tool Selection/by Robert Keever

Diamond tooling and diamond-coated end mills are a great option when machining highly abrasive materials, as the coating properties help to significantly increase tool life relative to uncoated carbide tools. Diamond tools and diamond-like coated tools are only recommended for non-ferrous applications, including highly abrasive materials ranging from graphite to green ceramics, as they have a tendency to break down in the presence of extreme heat.

Understanding the Properties of Diamond Coatings

To ensure proper diamond tooling selection, it’s critical to understand the unique properties and makeup of the coatings, as there are often several diamond coating variations to choose from. Harvey Tool, for example, stocks Amorphous Diamond, CVD Diamond, and PCD Diamond End Mills for customers looking to achieve significantly greater tool life when working in non-ferrous applications.

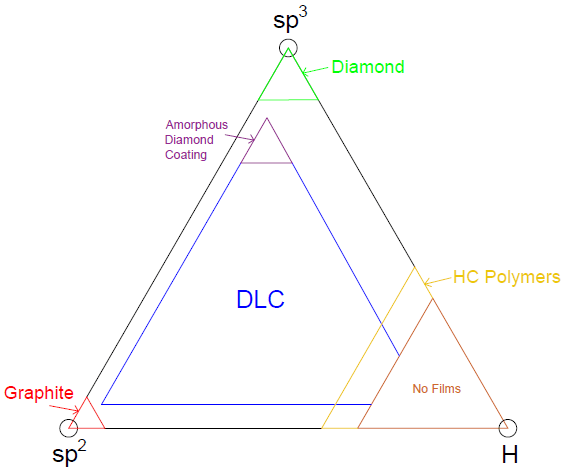
Diamond, the hardest known material on earth, obtains its strength from the structure of carbon molecules. Graphite, a relatively brittle material, can have the same chemical formula as diamond, but is a completely different material; while Graphite has a sp2 bonded hexagonal structure, diamond has a sp3 bonded cubic structure. The cubic structure is harder than the hexagonal structure as more single bonds can be formed to interweave the carbon into a stronger network of molecules.

diamond tool coatings

Amorphous Diamond Coating

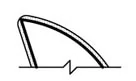
Amorphous Diamond is transferred onto carbide tools through a process called physical vapor deposition (PVD). This process spreads a mono-layer of DLC coating about 0.5 – 2.5 microns thick onto any given tool by evaporating a source material and allowing it to condense onto that tool over the course of a few hours.

amorphous diamond coating graphic showcasing thickness added

Chemical Vapor Deposition (CVD)

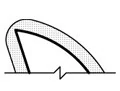
Chemical Vapor Deposition (CVD) is a coating process used to grow multiple layers of polycrystalline diamond onto carbide tooling. This procedure takes much longer than the standard PVD coating method. During the coating process, hydrogen molecules are dissociated from the carbon molecules deposited onto the tool, leaving a diamond matrix under the right temperature and pressure conditions. Under the wrong conditions, the tool may be simply coated in graphite. 6% cobalt carbide blanks allow for the best adhesion of diamond and a substrate. CVD diamond coated end mills have a typical thickness of coating that is between 8 and 10 microns thick.

CVD Diamond Coating graphic showcasing thickness added by coating

Polycrystalline Diamond (PCD)

Polycrystalline Diamond (PCD) is a synthetic diamond, meaning it is grown in a lab and contains mostly cubic structures. Diamond hardness ranges from about 80 GPa up to about 98 GPa. PCD end mills have the same diamond structure as CVD diamond tools but the binding technique is different. The diamond starts in a powdery form that is sintered onto a carbide plate using cobalt as a solvent metal substrate. This is done at an extreme temperature and pressure as the cobalt infiltrates the powder, causing the grains to grow together. This effectively creates a thick diamond wafer, between 010” and .030” in width, with a carbide base. This carbide base is then brazed onto the head an end mill and sharpened.

PCD Diamond Coating showcasing brazed on cutting edgeHow Diamond Coatings Differ

Coating Hardness & Thickness

Polycrystalline tools (CVD or sintered) have a much higher hardness, thickness, and max working temperature than Amorphous Diamond oated tools. As mentioned previously, a PCD tool consists of a diamond wafer brazed to a carbide body while a CVD tool is a carbide end mill with a relatively thick layer of polycrystalline diamond grown into it. This grown layer causes the CVD tools to have a rounded cutting edge compared to PCD and Amorphous Diamond coated tools. PCD tools have the thickest diamond layer that is ground to a sharp edge for maximum performance and tool life. The difference between PCD tools and CVD coated tools lies in the thickness of this coat and the sharpness of the cutting edge. Amorphous Diamond tools maintain a sharper edge than CVD coated tools because of their thin coating.

Flute Styles

Harvey Tool’s line of PCD end mills are all straight fluted, CVD coated tools are all helically fluted, and Amorphous Diamond tools are offered in a variety of options. The contrast between straight fluted and helically fluted can be seen in the images below, PCD (top) and CVD (bottom). Electrical discharge machining, grinding or erosion are used cut the PCD wafer to the specifications. The size of this wafer limits the range of diameters that can be achieved during manufacturing. In most situations a helically fluted tool would be preferred over a straight fluted tool but with true diamond tooling that is not the case. The materials that PCD tools and CVD coated tools are typically used to cut produce a powdery chip that does not require the same evacuation that a metallic or plastic chip necessitates.

PCD Diamond ball end mill

PCD Ball End Mill

CVD Diamond ball end mill

CVD Ball End Mill

Proper Uses

CVD tools are ideally suited for abrasive material not requiring a sharp cutting edge – typically materials that produce a powdery chip such as composites and graphite. Amorphous Diamond tools have a broad range of non-ferrous applications spanning from carbon fiber to precious metals but ceramics are typically outside their range as they can be too abrasive and wear away the coating. PCD tools overlap their CVD and DLC coated counterparts as they can be used for any non-ferrous abrasive material.

Cut to the Point

Harvey Tool carries physical vapor deposition diamond-like carbon coated tools, chemical vapor deposition diamond tools and polycrystalline diamond tools. PCD tools are composed of the thickest diamond wafer brazed onto a carbide shank and are ground to a sharp edge. CVD coated tools have the diamond grown into a carbide end mill. Amorphous Diamond coated tools have the DLC coated onto them through the PVD process. For more information on the diamond coating best suited for your operation, contact a Harvey Tool Tech Team Member for immediate help.

https://www.harveyperformance.com/wp-content/uploads/2018/05/Feature-Image-Diamond-End-Mills-IMG.jpg 525 1400 Robert Keever http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Robert Keever2018-05-10 10:51:482024-02-12 15:37:16Shining a Light on Diamond End Mills
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top