Complex parts require more than a single operation. Features such as contours, chamfers, engraved details, and precision holes often demand multiple tooling strategies working together throughout the machining process.
In the video below, watch a single component progress from a block of Ti-6Al-4V to a finished part through more than 10 machining applications, each supported by specialized Harvey Tool solutions.
Explore the full range of solutions available in the 2026 Harvey Tool Catalog, featuring more than 31,000 miniature and specialty cutting tools designed to support even the most demanding applications.
https://www.harveyperformance.com/wp-content/uploads/2026/02/Feature-Image-Harvey-Tool-2026-Catalog-Video-IMG.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2026-02-27 15:07:592026-03-31 09:47:45Machining a Complex Part with Harvey Tool
At Valor Holemaking, we know that drilling stainless steel and titanium isn’t just difficult, it’s one of the most demanding challenges manufacturers face. These materials are unforgiving, known for their toughness, low thermal conductivity, and tendency to work harden, which often result in significantly reduced tool life.
Our objective was to evaluate tool life, hole quality, and tolerance under production-level parameters. By benchmarking the performance of the Valor drill against several best-in-class competitors, we aimed to provide data-driven insight into how it performs in demanding stainless steel and titanium applications.
Testing in 316L Stainless Steel
Stainless Steel Testing Information
Material
AISI 316L (200 HB)
Valor Drill
SKU: V623060-X Diameter: 12.7 mm L/D: 5XD Coating: Val-Max-X
This chart displays the total number of holes drilled in AISI 316L stainless steel before tool failure or test completion. The Valor drill reached the testing limit of 2,000 holes with no signs of failure, while other tools showed significant variation in tool life, ranging from more than 200 holes to 1,300. This proves that this Valor high-performance drill can run longer, compared to that of top competitors, particularly in stainless steel where premature wear is common.
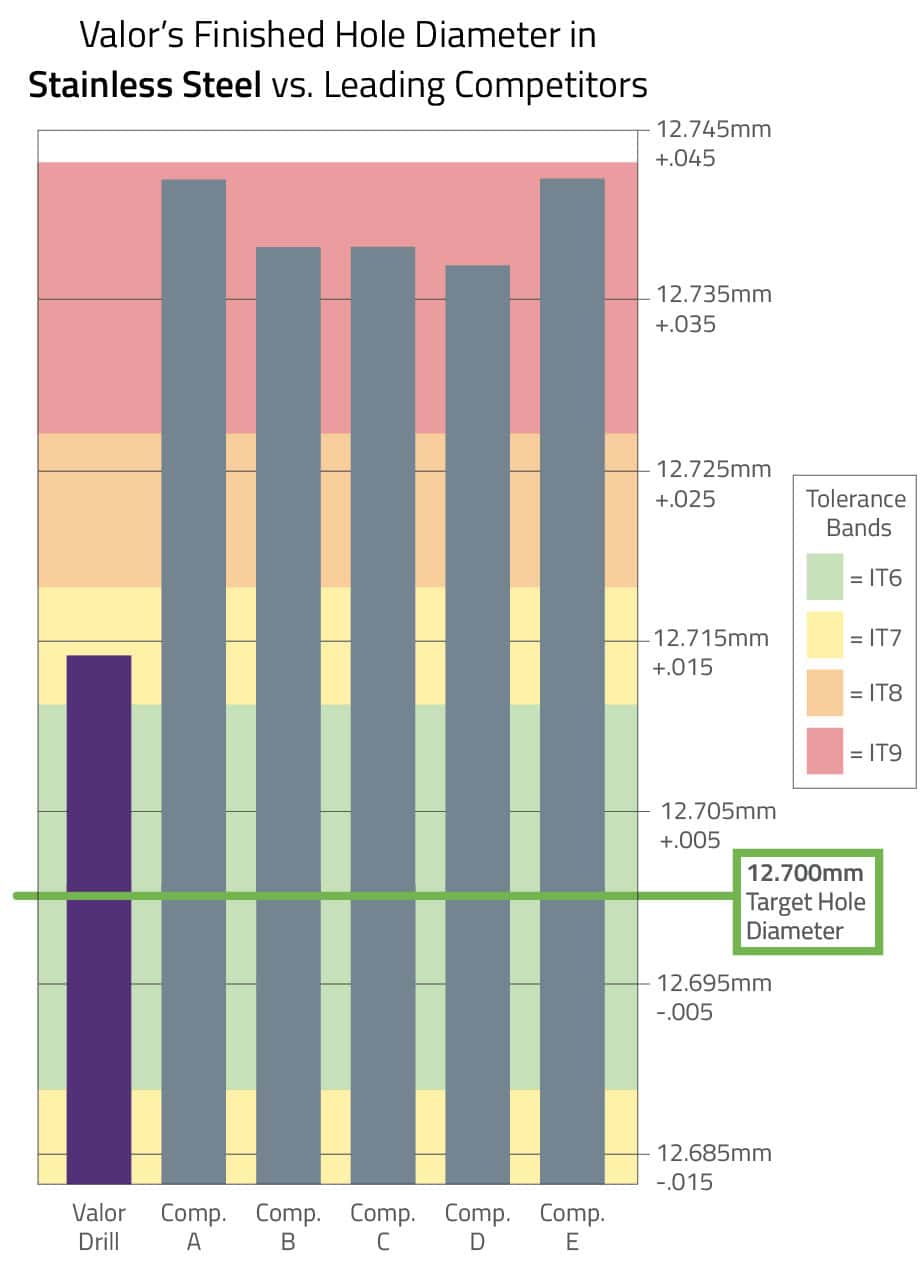
Finished Hole Diameter Consistency in Stainless Steel
The data in the chart to the left shows the average finished hole diameter across the test range for each tool. The Valor drill consistently held the nominal 12.7 mm diameter within the IT7 tolerance band. All competitors drifted into the IT9 range, indicative of inefficient chip formation or inefficient cutting.
Measuring hole diameter consistency of testing blocks
Valor Drill – Finished Hole Diameter Consistency Across 2,000 Holes
This chart displays the finished hole diameters measured from Valor’s drill over the course of 2,000 holes in 316L stainless steel. Each point represents an actual measurement, and the data shows the drill maintained exceptional consistency throughout the test. The variation across all holes was just 8 microns, with every measurement falling within the IT7 tolerance band.
What is an IT Band?
In the context of precision machining, IT stands for International Tolerance grade—a standardized system used to define the allowable variation in hole dimensions. The lower the IT number, the tighter the tolerance and the higher the precision. For example, a hole finished within IT6 tolerances is more precise than one within IT8.
IT band values vary depending on the nominal diameter of the hole being machined. In our testing, we focused on a 12.7 mm drill diameter, so the range of acceptable deviation for each IT band is scaled accordingly.
These results indicate that the Valor drill stayed stable in the cut, minimizing drift and taper even after 2,000 holes. For parts where positional accuracy is critical, this helps reduce the need for secondary operations or in-process adjustments.
Inspecting Tool Edge Wear
Testing in 6Al-4V Titanium
Titanium Testing Information
Material
6Al-4V (33HRC)
Valor Drill
SKU: V623060-X Diameter: 12.7 mm L/D: 5XD Coating: Val-Max-X
In this titanium drilling comparison, the chart illustrates total hole count before tool failure or the test’s 1,200-hole cap. The Valor drill, again, reached the maximum without failing, whereas all competitor tools experienced failure beforehand.
Finished Hole Diameter Consistency in Titanium
This chart compares the average finished hole diameters produced by Valor’s drill and several leading competitors in Ti-6Al-4V. Valor’s drill consistently held hole size within the IT6 tolerance band, the tightest shown, while other drills produced holes that fell into IT7 or IT8 ranges. This distinction highlights Valor’s ability to maintain high dimensional accuracy even in a challenging material like titanium. The tighter tolerance indicates better tool stability, less deflection, and more reliable performance across extended runs, which is critical for precision-focused industries like aerospace and medical manufacturing.
Valor Drill – Finished Hole Diameter Consistency Across 1,200 Holes
This chart illustrates the finished hole diameters recorded from Valor’s drill over the 1,200 holes drilled in titanium. Throughout the entire run, the drill consistently held dimensions within the IT6 tolerance band, with hole sizes deviating by only 9 microns from the nominal diameter (12.7mm).
Geometric Accuracy in Titanium
Valor’s drill also demonstrated tight geometric control throughout the titanium test.
True Position: 46 µm
Cylindricity: 23 µm
Straightness: 7 µm
These values remained consistent across all 1,200 holes, reinforcing the tool’s ability to cut clean, accurate features in a challenging material. This level of consistency is especially beneficial in aerospace or medical applications where tight tolerances are required.
Valor Holemaking Application Engineers Inspecting Drills After Test
Conclusion
These internal tests offer insight into how Valor High Performance Drills for Stainless Steel & Titanium perform under consistent parameters in stainless steel and titanium. In both tests, the drills showed the ability to maintain hole quality over extended cycles, potentially improving cost-efficiency and reducing downtime in production settings. While results may vary depending on material, fixturing, and machine setup, this testing provides a data-driven starting point for evaluating suitability in demanding drilling applications.
Carbon fiber is a woven cloth made of crystalline filaments of carbon cured with a polymer, which can be layered and shaped around a mold. It is an ideal material due to its impressive strength-to-weight ratio , meaning it’s very strong, but not heavy. Carbon fiber is five times lighter than steel with an equal elastic modulus, making it a better choice for many applications. Further, it is corrosion-resistant, non-flammable, and non-toxic, properties that make it an ideal material to use in aerospace, medical, construction, and military industries.
Machining Carbon Fiber
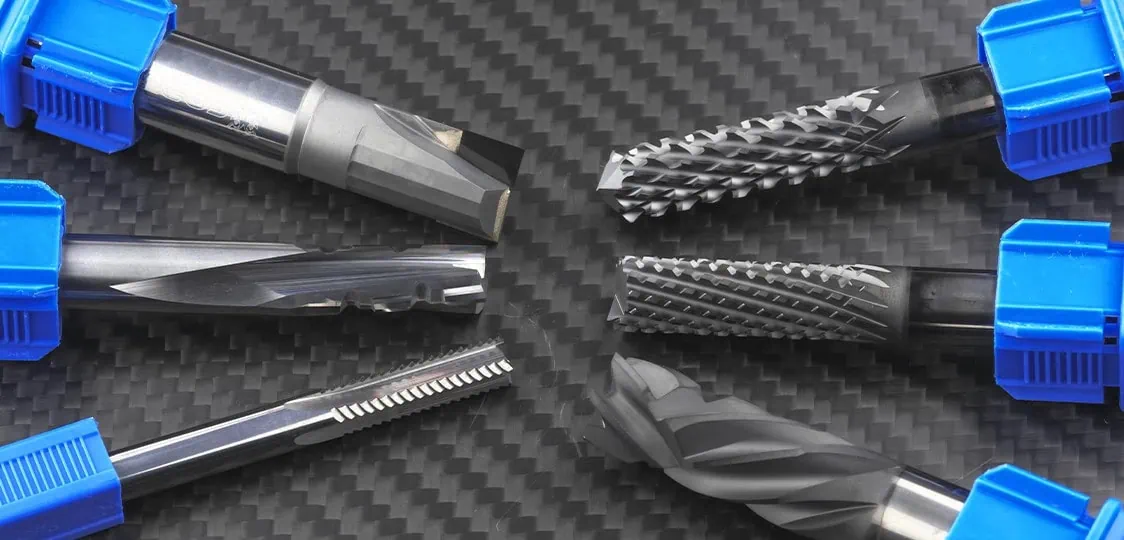
Machining Carbon Fiber can be challenging. The layered structure of the carbon fiber material can lead to delamination, uncut fibers, fiber tear-out, uneven tool wear, and poor surface finishes. Luckily, many cutting tool companies, like CoreHog, specially design tooling with different geometries that can help eliminate these manufacturing problems:
Straight Flute End Mills: Apply all the cutting forces radially, which helps prevent delamination.
Compression Cutters: Create opposite cutting forces, stabilizing material removal and preventing delamination, fiber pullout, and burrs along the surface.
Chipbreaker Cutters: Shear the fibers and shorten the chips, preventing fiber buildup around the cutter.
Diamond Cut End Mills: Utilize both left-hand and right-hand flutes to break up and shear through the fibers, ideal for roughing and profiling carbon fiber.
In the aerospace industry, carbon fiber is used in plane structures to replace alloys, creating lighter planes and thus, reducing fuel consumption. Recreational sports also utilize carbon fiber to decrease weight. It is often seen as a leading material in skis, bikes, and tennis rackets, as the lighter weight can help improve performance. In professional sports leagues like Formula 1 and NASCAR, carbon fiber has grown in prevalence in recent years. Another advantageous quality of carbon fiber is its suitability in X-ray machines, allowing imaging to pass through without interruption, making it useful in many medical devices and implants.
Recycling Carbon Fiber
Why is Recycling Carbon Fiber Difficult?
Carbon fiber sheets require a significant amount of energy to produce. These large sheets are then cut down to the part size needed, and the excess material is often discarded, increasing waste production. This material is not biodegradable and is typically sent to a landfill where it will remain permanently. Further complicating recycling, carbon fiber is built to hold its shape and strength and cannot be melted down and reshaped like many plastics. When recycled, its properties are heavily degraded, rendering it useless for applications that experience heavy forces or loads.
How is Carbon Fiber Recycled?
Solvolysis
Solvolysis uses a chemical solvent to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces, increasing the surface area. The solvent, chosen based on the polymers used in the carbon fiber, breaks down the polymer chains, separating the carbon fiber from the polymer. Techniques like centrifugation are used to separate the substances. The carbon fiber can be further purified to restore its properties and then combined with virgin fibers to create new fabric or used by itself. This process enables the recovery of carbon fiber without sacrificing material properties.
Pyrolysis
Pyrolytic utilizes heat to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces and then heated in a controlled environment with limited or no oxygen. At high temperatures, the polymer undergoes thermal decomposition, producing gases, vapors, and char. The gases and vapors can be used as an energy source or further processed, while the char, which is carbon fiber and any original additives, is purified to ensure mechanical properties are maintained. The resulting carbon fiber can be used alone or combined with virgin fibers. Pyrolysis is effective for high-quality fiber recovery and energy recovery from gas byproducts.
Carbon Fiber Considerations
As we innovate with new technology, it is important to consider its impact on our planet. Carbon fiber is an amazing material that can improve many aspects across industries; however, the waste generated is not going anywhere but a landfill. Many companies are investing in producing high-quality recycled carbon fiber. With a shift in focus to designing closed-loop systems for composite materials, the future looks bright.
https://www.harveyperformance.com/wp-content/uploads/2024/07/Feature-Image-Recyling-Carbon-Fiber-IMG.jpg5251400Sarah Wassonhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngSarah Wasson2024-07-08 12:00:402024-07-12 12:46:58Recycling Carbon Fiber: Importance & Process
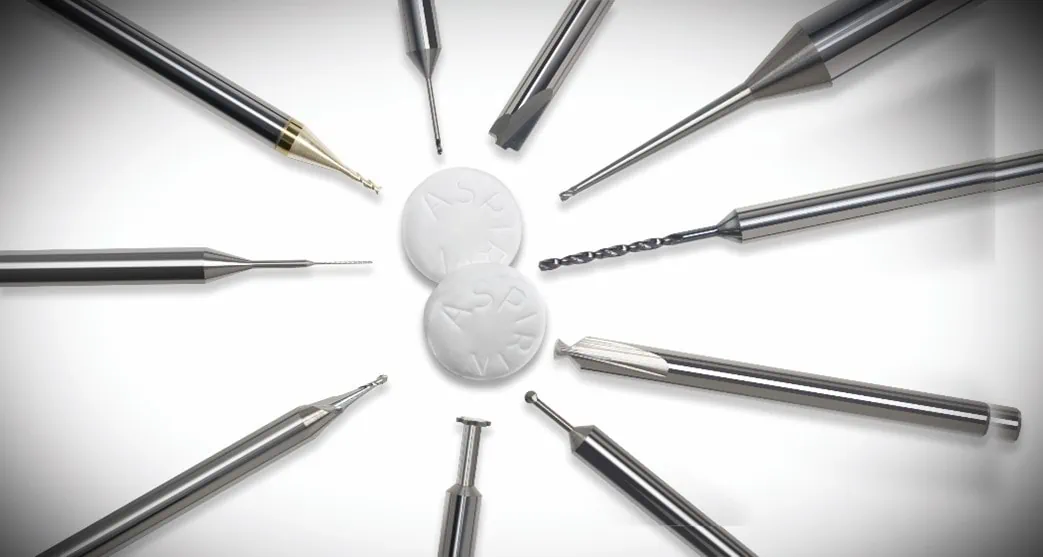
Machining Advisor Pro (MAP) was first introduced to the CNC Machining Industry in 2018 as a tool to quickly, seamlessly, and accurately deliver recommended running parameters to machinists using Helical Solutions end mills. then, thousands of users have utilized this cutting-edge resource, every day. In August 2022, a new and improved version of MAP was launched, optimized for Harvey Tool’s 27,000+ miniature and specialty cutting tools.
The following article is intended to introduce MAP 2.0 features. For more in depth information about MAP, including how to get started using it, please visit the original “In the Loupe,” post Get to Know Machining Advisor Pro.
New Map 2.0 Features
Addition of all Harvey Tool Products
With the release of MAP 2.0, users now have access to expertly tailored speeds and feeds parameters and recommendations to meet the exact demands of cutting tool and machine setup for all Harvey Tool products. This means that more than 27,000 Harvey Tool products are available in MAP and users can find their Specialty Profile Cutting Tools, Miniature End Mills, and Holemaking and Threading products to confidently use MAP generated speeds and feeds. With the addition of new products, there is now a new variety of operations to choose from, specific to the product selected.
New Strategy Option for Operations
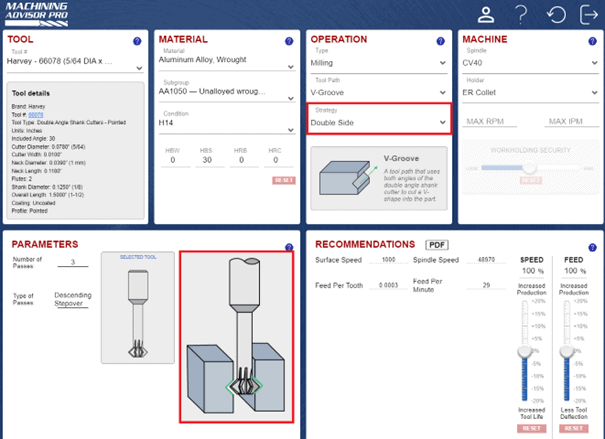
Before the MAP 2.0 update, there were only two drop down menus for operation: type and toolpath. With the new update, there is an additional third operation drop down menu titled “strategy.” This option allows for users to further refine their machining operation, but only for certain tools that require it. For example, when using a Double Angle Shank Cutter on MAP, users can choose from a list of toolpaths including deburring, chamfer, or v-groove.
Once selected, users will choose a strategy for the toolpath – single side or double side engagement. The use of this feature gives the user more flexibility in their operations and saves time by automating their operation calculations. This feature is available for a variety of different toolpaths within the application.
MAP Offline Mode
With the release of MAP 2.0, and the addition of over 27,000 Harvey tools, users now can work offline. The work offline feature is only available for the new Harvey Tools. To access this feature, users can select the “User Account” button in the top right and start the process to allow MAP to work offline. Activating the work offline mode will cache the Harvey Tool data and takes around 15-20 minutes to complete before allowing the user to work offline.
Having the ability to use MAP offline can be useful when users are unable to connect to the internet as you will still be able to access MAP on a desktop or mobile app, whenever and wherever you need it.
Stainless steel can be as common as Aluminum in many shops, especially when manufacturing parts for the aerospace and automotive industries. It is a fairly versatile material with many different alloys and grades which can accommodate a wide variety of applications. However, milling steel can also be immensely difficult. Stainless steels are notorious end mill assassins, so dialing in your speeds and feeds and selecting the proper tool is essential for machining success.
Material Properties
Stainless steels are high-alloy steels with superior corrosion resistance to carbon and low-alloy steels. This is largely due to their high chromium content, with most grades of stainless steel alloys containing at least 10% of the element.
Stainless steel can be broken out into one of five categories: Austenitic, Ferritic, Martensitic, Precipitation Hardened (PH), and Duplex. In each category, there is one basic, general purpose alloy. From there, small changes in composition are made to the base in order to create specific properties for various applications.
For reference, here are the properties of each of these groupings, as well as a few examples of the popular grades and their common uses.
Category
Properties
Popular Grades
Common Uses
Austenitic
Non-magnetic, outstanding corrosion and heat resistance.
304, 316
Food processing equipment, gutters, bolts, nuts, and other fasteners.
Ferritic
Magnetic, lower corrosion and heat resistance than Austenitic.
430, 446
Automotive parts and kitchen appliances.
Martensitic
Magnetic, moderate corrosion resistance – not for severe corrosion.
416, 420, 440
Knives, firearms, surgical instruments, and hand tools.
Precipitation Hardened (PH)
Strongest grade, heat treatable, severe corrosion resistance.
17-4 PH, 15-5 PH
Aerospace components.
Duplex
Stronger mixture of both Austenitic and Ferritic.
244, 2304, 2507
Water treatment plants, pressure vessels.
Tool Selection
Choosing the correct tooling for your application is crucial when machining stainless steel. Roughing, finishing, slotting, and high efficiency milling toolpaths can all be optimized for stainless steel by choosing the correct style of end mill.
Traditional Roughing
For traditional roughing, a 4 or 5 flute end mill is recommended. 5 flute end mills will allow for higher feed rates than their 4 flute counterparts, but either style would work well for roughing applications. Below is an excellent example of traditional roughing in 17-4 Stainless Steel.
Slotting
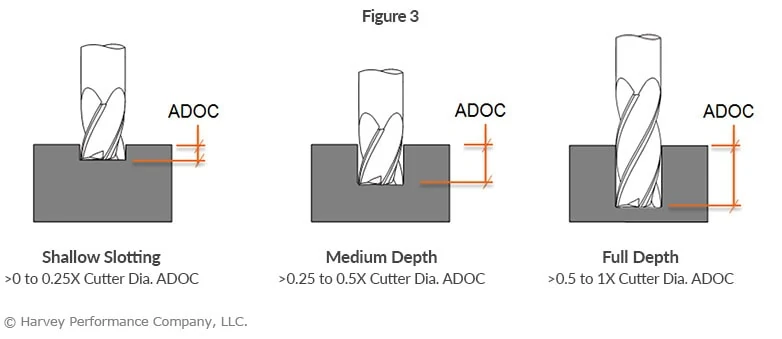
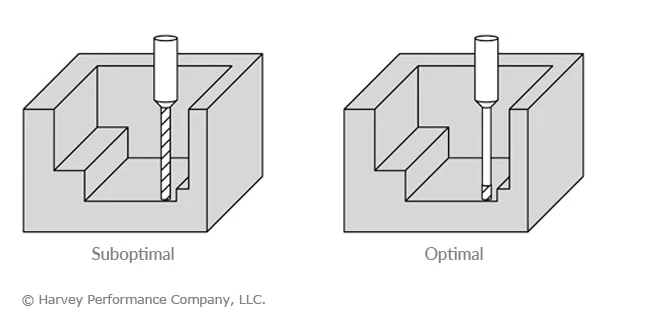
The axial engagement of a tool in a slotting operation should be suitable for the specific tool employed, as depicted in Figure 3. Employing an unsuitable method may result in tool deflection, potential damage, and compromised part quality. Chip evacuation is going to be key for slotting in stainless steel. For this reason, 4 flute tools are the best choice because the lower flute count allows for more efficient chip evacuation. Tools with chipbreaker geometry also make for effective slotting in stainless steel, as the smaller chips are easier to evacuate from the cut.
Finishing
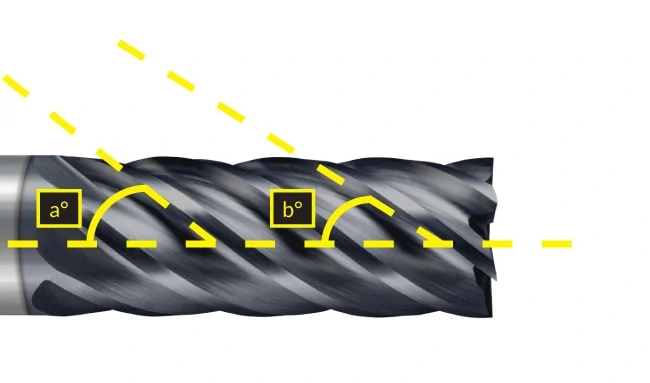
When finishing stainless steel parts, a high flute count and/or high helix is required for the best results. Finishing end mills for stainless steel will have a helix angle over 40 degrees, and a flute count of 5 or more. For more aggressive finishing toolpaths, flute count can range from 7 flutes to as high as 14. Below is a great example of a finishing run in 17-4 Stainless Steel.
High Efficiency Milling
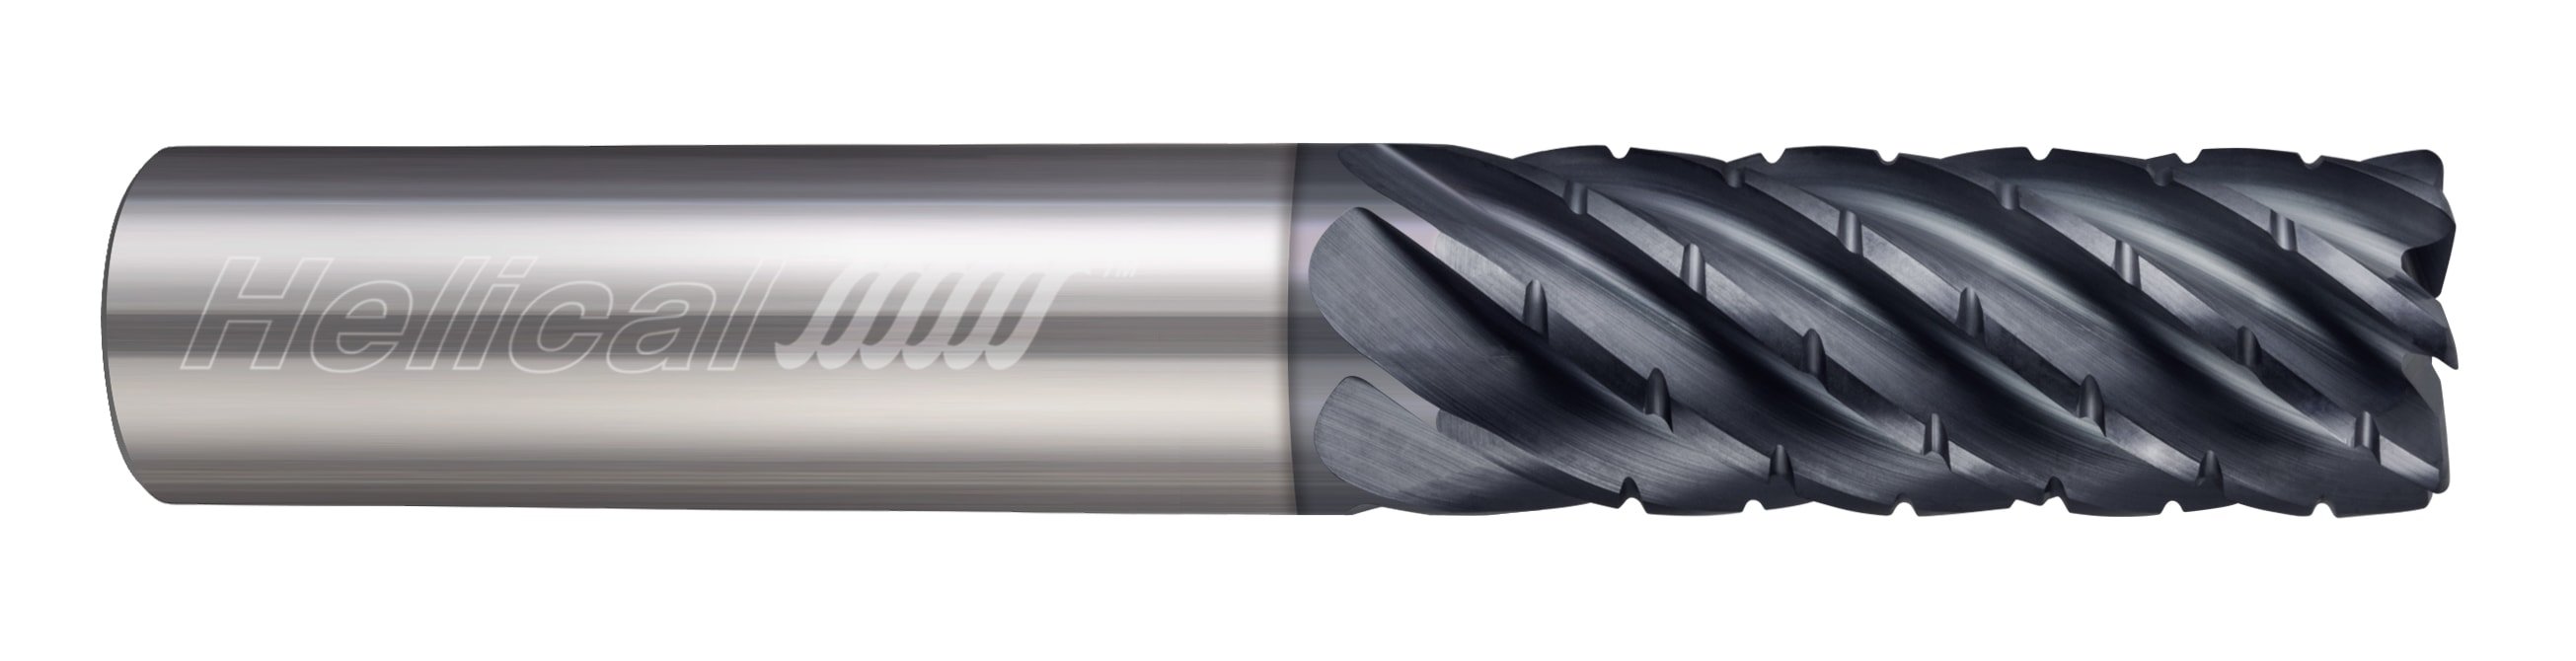
High Efficiency Milling (HEM) can be a very effective machining technique in stainless steels if the correct tools are selected. Chipbreaker roughers would make an excellent choice, in either 5 or 7 flute styles, while standard 5-7 flute, variable pitch end mills can also perform well in HEM toolpaths.
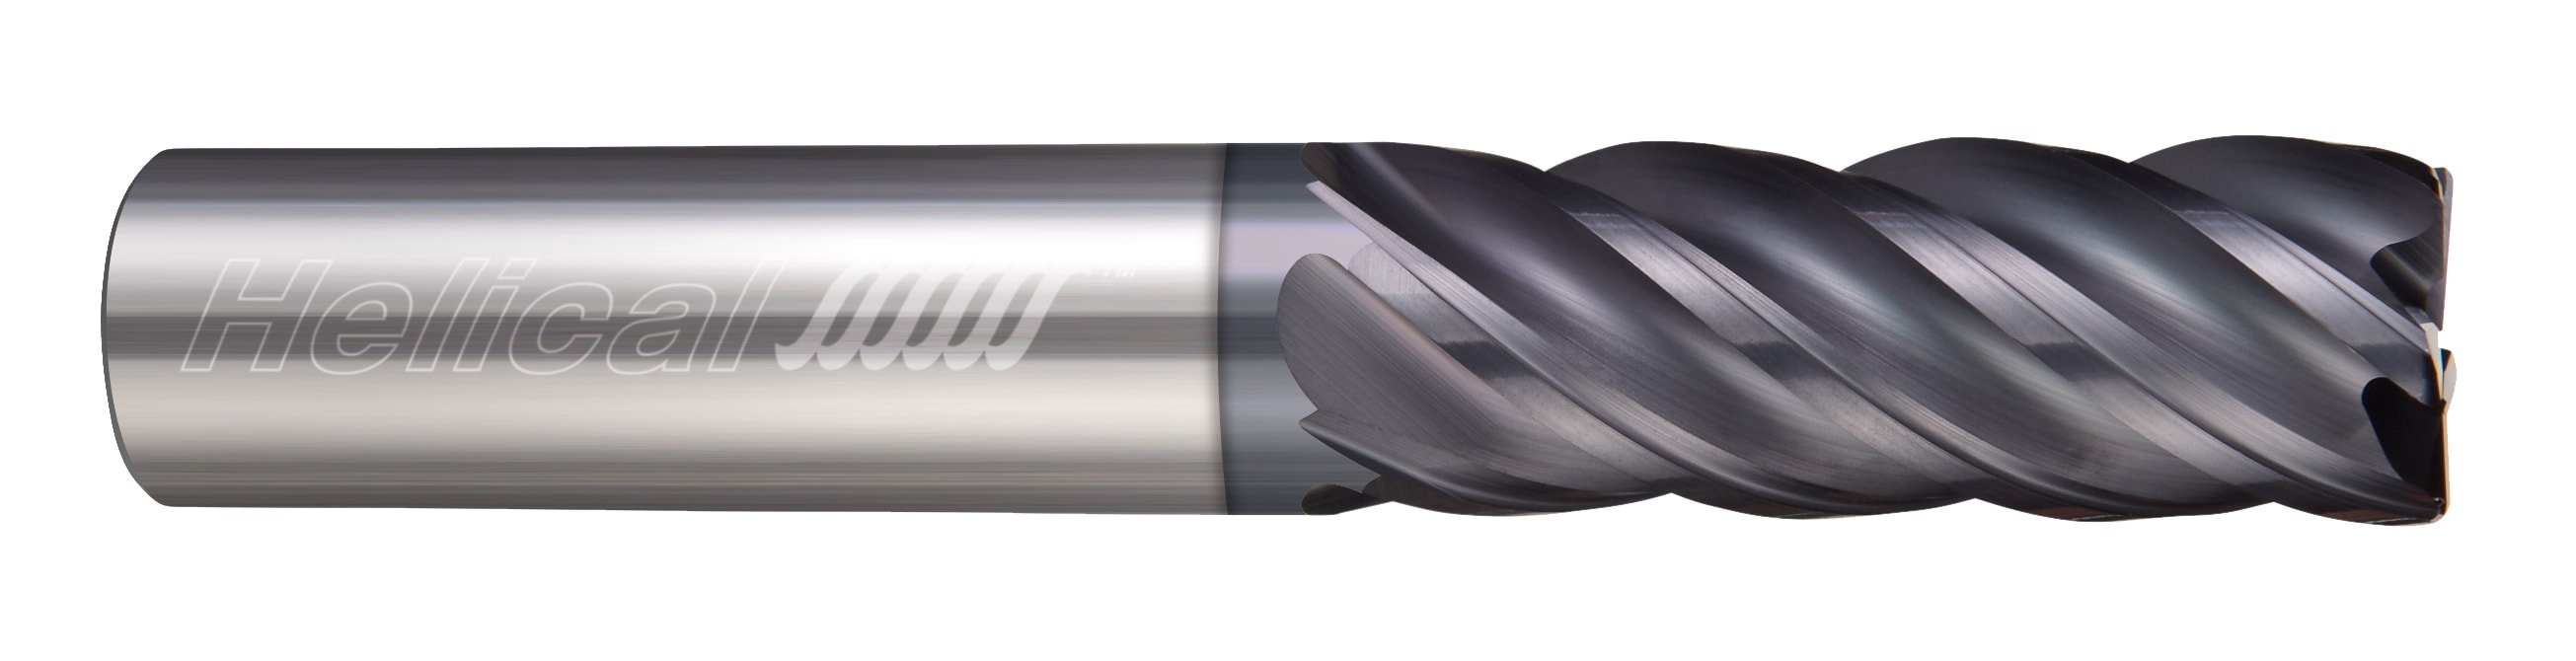
HEV-5
Helical Solutions offers the HEV-5 end mill, which is an extremely versatile tool for a variety of applications. The HEV-5 excels in finishing and HEM toolpaths, and also performs well above average in slotting and traditional roughing. Available in square, corner radius, and long reach styles, this well-rounded tool is an excellent choice to kickstart your tool crib and optimize it for stainless steel machining.
Running Parameters
While tool selection is a critical step to more effective machining, dialing in the proper running parameters is equally important. There are many factors that go into determining the running parameters for stainless steel machining, but there are some general guidelines to follow as a starting point.
Generally speaking, when machining stainless steels a SFM of between 100-350 is recommended, with a chip load ranging between .0005” for a 1/8” end mill up to .006” for a 1” end mill. A full breakdown of these general guidelines is available here.
Machining Advisor Pro
Machining Advisor Pro is a cutting edge resource designed to precisely calculate running parameters for high performance Helical Solutions end mills in materials like stainless steel, aluminum, and much more. Simply input your tool, your exact material grade, and machine setup and Machining Advisor Pro will generate fully customizable running parameters. This free resource allows you to push your tools harder, faster, and smarter to truly dominate the competition.
Stainless steel machining doesn’t have to be hard. By identifying the proper material grade for each part, selecting the perfect cutting tool, and optimizing running parameters, headaches from milling steel can become a thing of the past.
Running It Too Fast or Too Slow Can Impact Tool Life
Determining the right speeds and feeds for your tool and operation can be a complicated process, but understanding the ideal speed (RPM) is necessary before you start running your machine to ensure proper tool life. Running a tool too fast can cause suboptimal chip size or even catastrophic tool failure. Conversely, a low RPM can result in deflection, bad finish, or simply decreased metal removal rates. If you are unsure what the ideal RPM for your job is, contact the tool manufacturer.
Feeding It Too Little or Too Much
Another critical aspect of speeds and feeds, the best feed rate for a job varies considerably by tool type and workpiece material. If you run your tool with too slow of a feed rate, you run the risk of recutting chips and accelerating tool wear. If you run your tool with too fast of a feed rate, you can cause tool fracture. This is especially true with miniature tooling.
Using Traditional Roughing
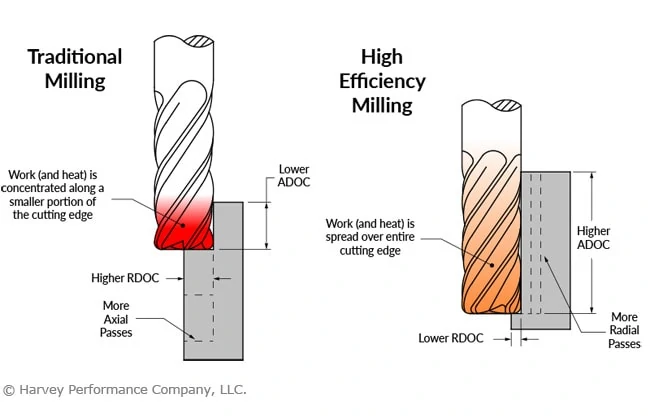
While traditional roughing is occasionally necessary or optimal, it is generally inferior to High Efficiency Milling (HEM). HEM is a roughing technique that uses a lower Radial Depth of Cut (RDOC) and a higher Axial Depth of Cut (ADOC). This spreads wear evenly across the cutting edge, dissipates heat, and reduces the chance of tool failure. Besides dramatically increasing tool life, HEM can also produce a better finish and higher metal removal rate, making it an all-around efficiency boost for your shop.
Using Improper Tool Holding and its Effect on Tool Life
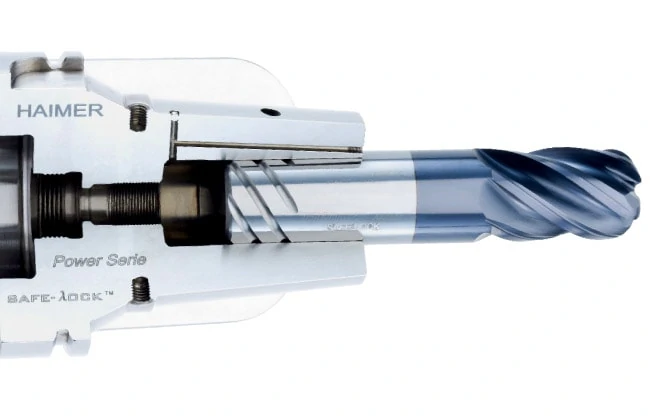
Proper running parameters have less of an impact in suboptimal tool holding situations. A poor machine-to-tool connection can cause tool runout, pullout, and scrapped parts. Generally speaking, the more points of contact a tool holder has with the tool’s shank, the more secure the connection. Hydraulic and shrink fit tool holders offer increased performance over mechanical tightening methods, as do certain shank modifications, like Helical’s ToughGRIP shanks and the Haimer Safe-Lock™.
Not Using Variable Helix/Pitch Geometry
A feature on a variety of high performance end mills, variable helix, or variable pitch, geometry is a subtle alteration to standard end mill geometry. This geometrical feature ensures that the time intervals between cutting edge contact with the workpiece are varied, rather than simultaneous with each tool rotation. This variation minimizes chatter by reducing harmonics, which increases tool life and produces superior results.
Choosing the Wrong Coating Can Wear on Tool Life
Despite being marginally more expensive, a tool with a coating optimized for your workpiece material can make all the difference. Many coatings increase lubricity, slowing natural tool wear, while others increase hardness and abrasion resistance. However, not all coatings are suitable to all materials, and the difference is most apparent in ferrous and non-ferrous materials. For example, an Aluminum Titanium Nitride (AlTiN) coating increases hardness and temperature resistance in ferrous materials, but has a high affinity to aluminum, causing workpiece adhesion to the cutting tool. A Titanium Diboride (TiB2) coating, on the other hand, has an extremely low affinity to aluminum, and prevents cutting edge build-up and chip packing, and extends tool life.
Using a Long Length of Cut
While a long length of cut (LOC) is absolutely necessary for some jobs, especially in finishing operations, it reduces the rigidity and strength of the cutting tool. As a general rule, a tool’s LOC should be only as long as needed to ensure that the tool retains as much of its original substrate as possible. The longer a tool’s LOC the more susceptible to deflection it becomes, in turn decreasing its effective tool life and increasing the chance of fracture.
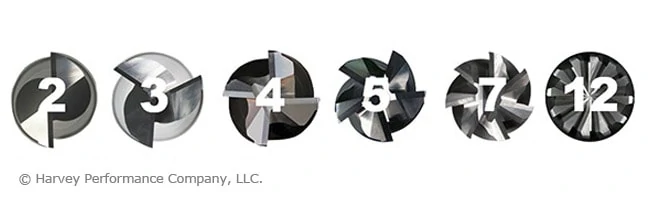
As simple as it seems, a tool’s flute count has a direct and notable impact on its performance and running parameters. A tool with a low flute count (2 to 3) has larger flute valleys and a smaller core. As with LOC, the less substrate remaining on a cutting tool, the weaker and less rigid it is. A tool with a high flute count (5 or higher) naturally has a larger core. However, high flute counts are not always better. Lower flute counts are typically used in aluminum and non-ferrous materials, partly because the softness of these materials allows more flexibility for increased metal removal rates, but also because of the properties of their chips. Non-ferrous materials usually produce longer, stringier chips and a lower flute count helps reduce chip recutting. Higher flute count tools are usually necessary for harder ferrous materials, both for their increased strength and because chip recutting is less of a concern since these materials often produce much smaller chips.
https://www.harveyperformance.com/wp-content/uploads/2018/02/Featured-Image-Killing-End-Mill-IMG.jpg3931400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2018-02-07 09:08:092023-10-12 09:59:088 Ways You’re Killing Your End Mill