Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

The Experts’ Guide to CNC Engraving

September 15, 2025/0 Comments/in CNC Machining, Harvey Tool, Large Featured, Machining 101, Machining Techniques, Milling, Milling, Specialty Tools, Tool Coatings, Tool Geometry, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

CNC engraving is a process that removes a small amount of material to create detailed images or shapes. Many manufacturers use this method for labeling parts or creating complex designs; however, not everyone is aware of the key techniques necessary for optimal results. When using an engraving tool, it is essential to consider several challenges that could affect both the tool and the operation.

Advantages of CNC Engraving

Compared to other engraving methods, CNC engraving is fast, consistent, and cost-effective. Thanks to their repeatability, CNC machines deliver consistent results when paired with a high-quality engraving tool. We suggest running the tool at a minimum of 6,000 RPM.

If your machine supports it, increasing the RPM can lead to even greater results. Running at lower speeds can negatively impact tool life. Choosing the right engraving tool requires considering production volume and tool engagement time. Key factors such as tip design, angle, and coating play a crucial role in maximizing efficiency and durability.

Proper Engraver Tool Selection

Most machinists understand that a square-corner end mill does not last as long as a corner-radius or ball-end mill due to its fragile cutting edge.

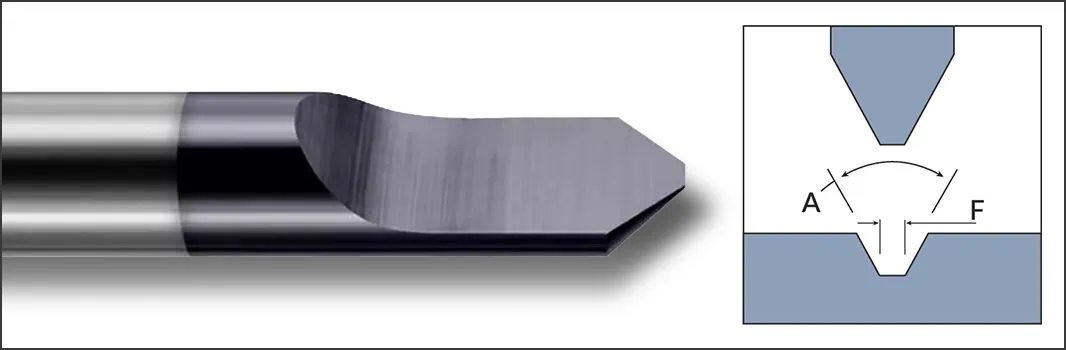
The same principle applies to CNC engraving tools. An engraver that comes to a sharp point is more fragile than one with a tipped-off or radius tip. For long production runs, consider using a tip-off or rounded tip design, as these geometries distribute cutting forces more evenly across the cutting edge, improving tool longevity. A tip-flat design will last longer than a pointed tip but not as long as a radius tip. If high-detail work is required, a pointed tip is preferable because it provides greater precision.
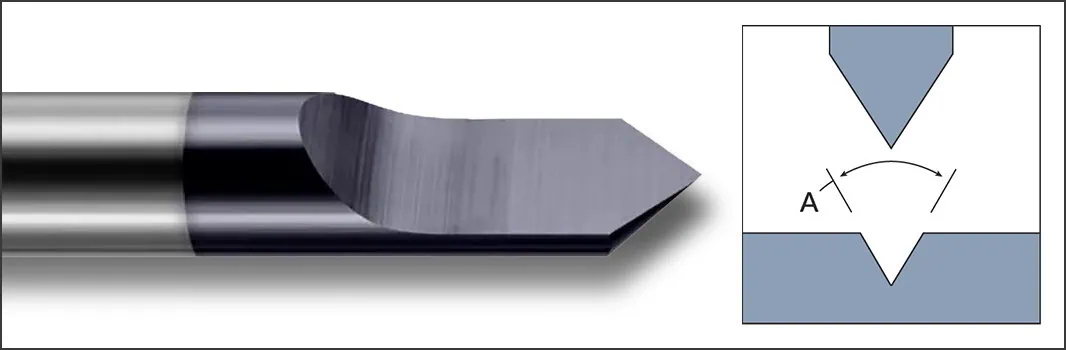
Pointed Tip Engraving Cutters
Tipped Off Engraving Cutters
Tip Radius Engraving Cutters

Environment and Detail Considerations

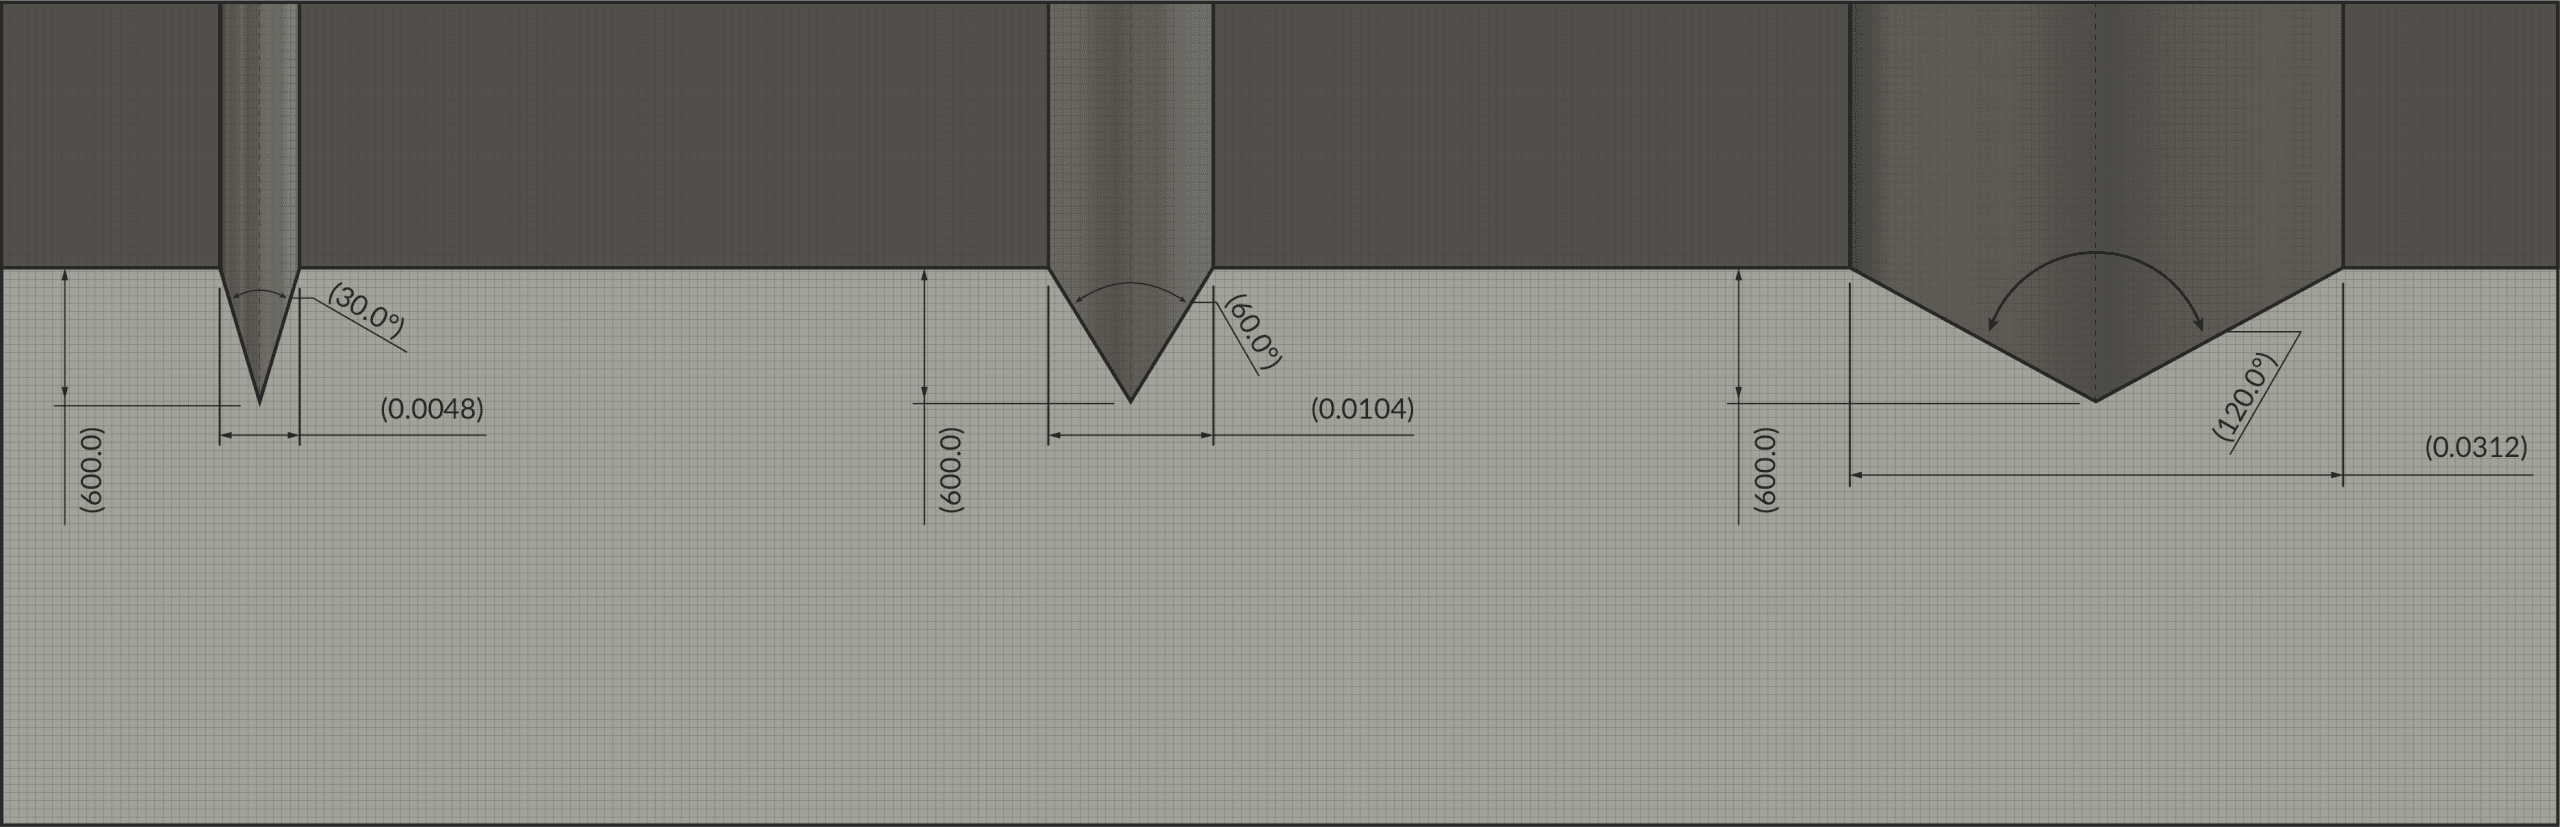
Similar to tip geometry, the engraving angle plays a critical role in visibility. The environment in which the engraving is used affects how well it can be seen. If the engraving is exposed to harsh conditions with elements like snow, mud, or dirt, debris can accumulate in the grooves, making it difficult to see and clean. A larger angle creates a wider groove, improving visibility and ease of cleaning.

The image below illustrates three different engraving angles offered by Harvey: the leftmost groove is 30° included, the middle groove is 60° included, and the rightmost groove is 120° included. Each of these engravings is only 0.009 inches deep.

Notice that the 120° engraving is more visible at a distance due to increased surface exposure. If a job requires precision and detail, a smaller angle is preferable. While geometry significantly impacts engraving visibility and tool longevity, another key factor in tool performance is the choice of coating.
Choosing a Tool Coating

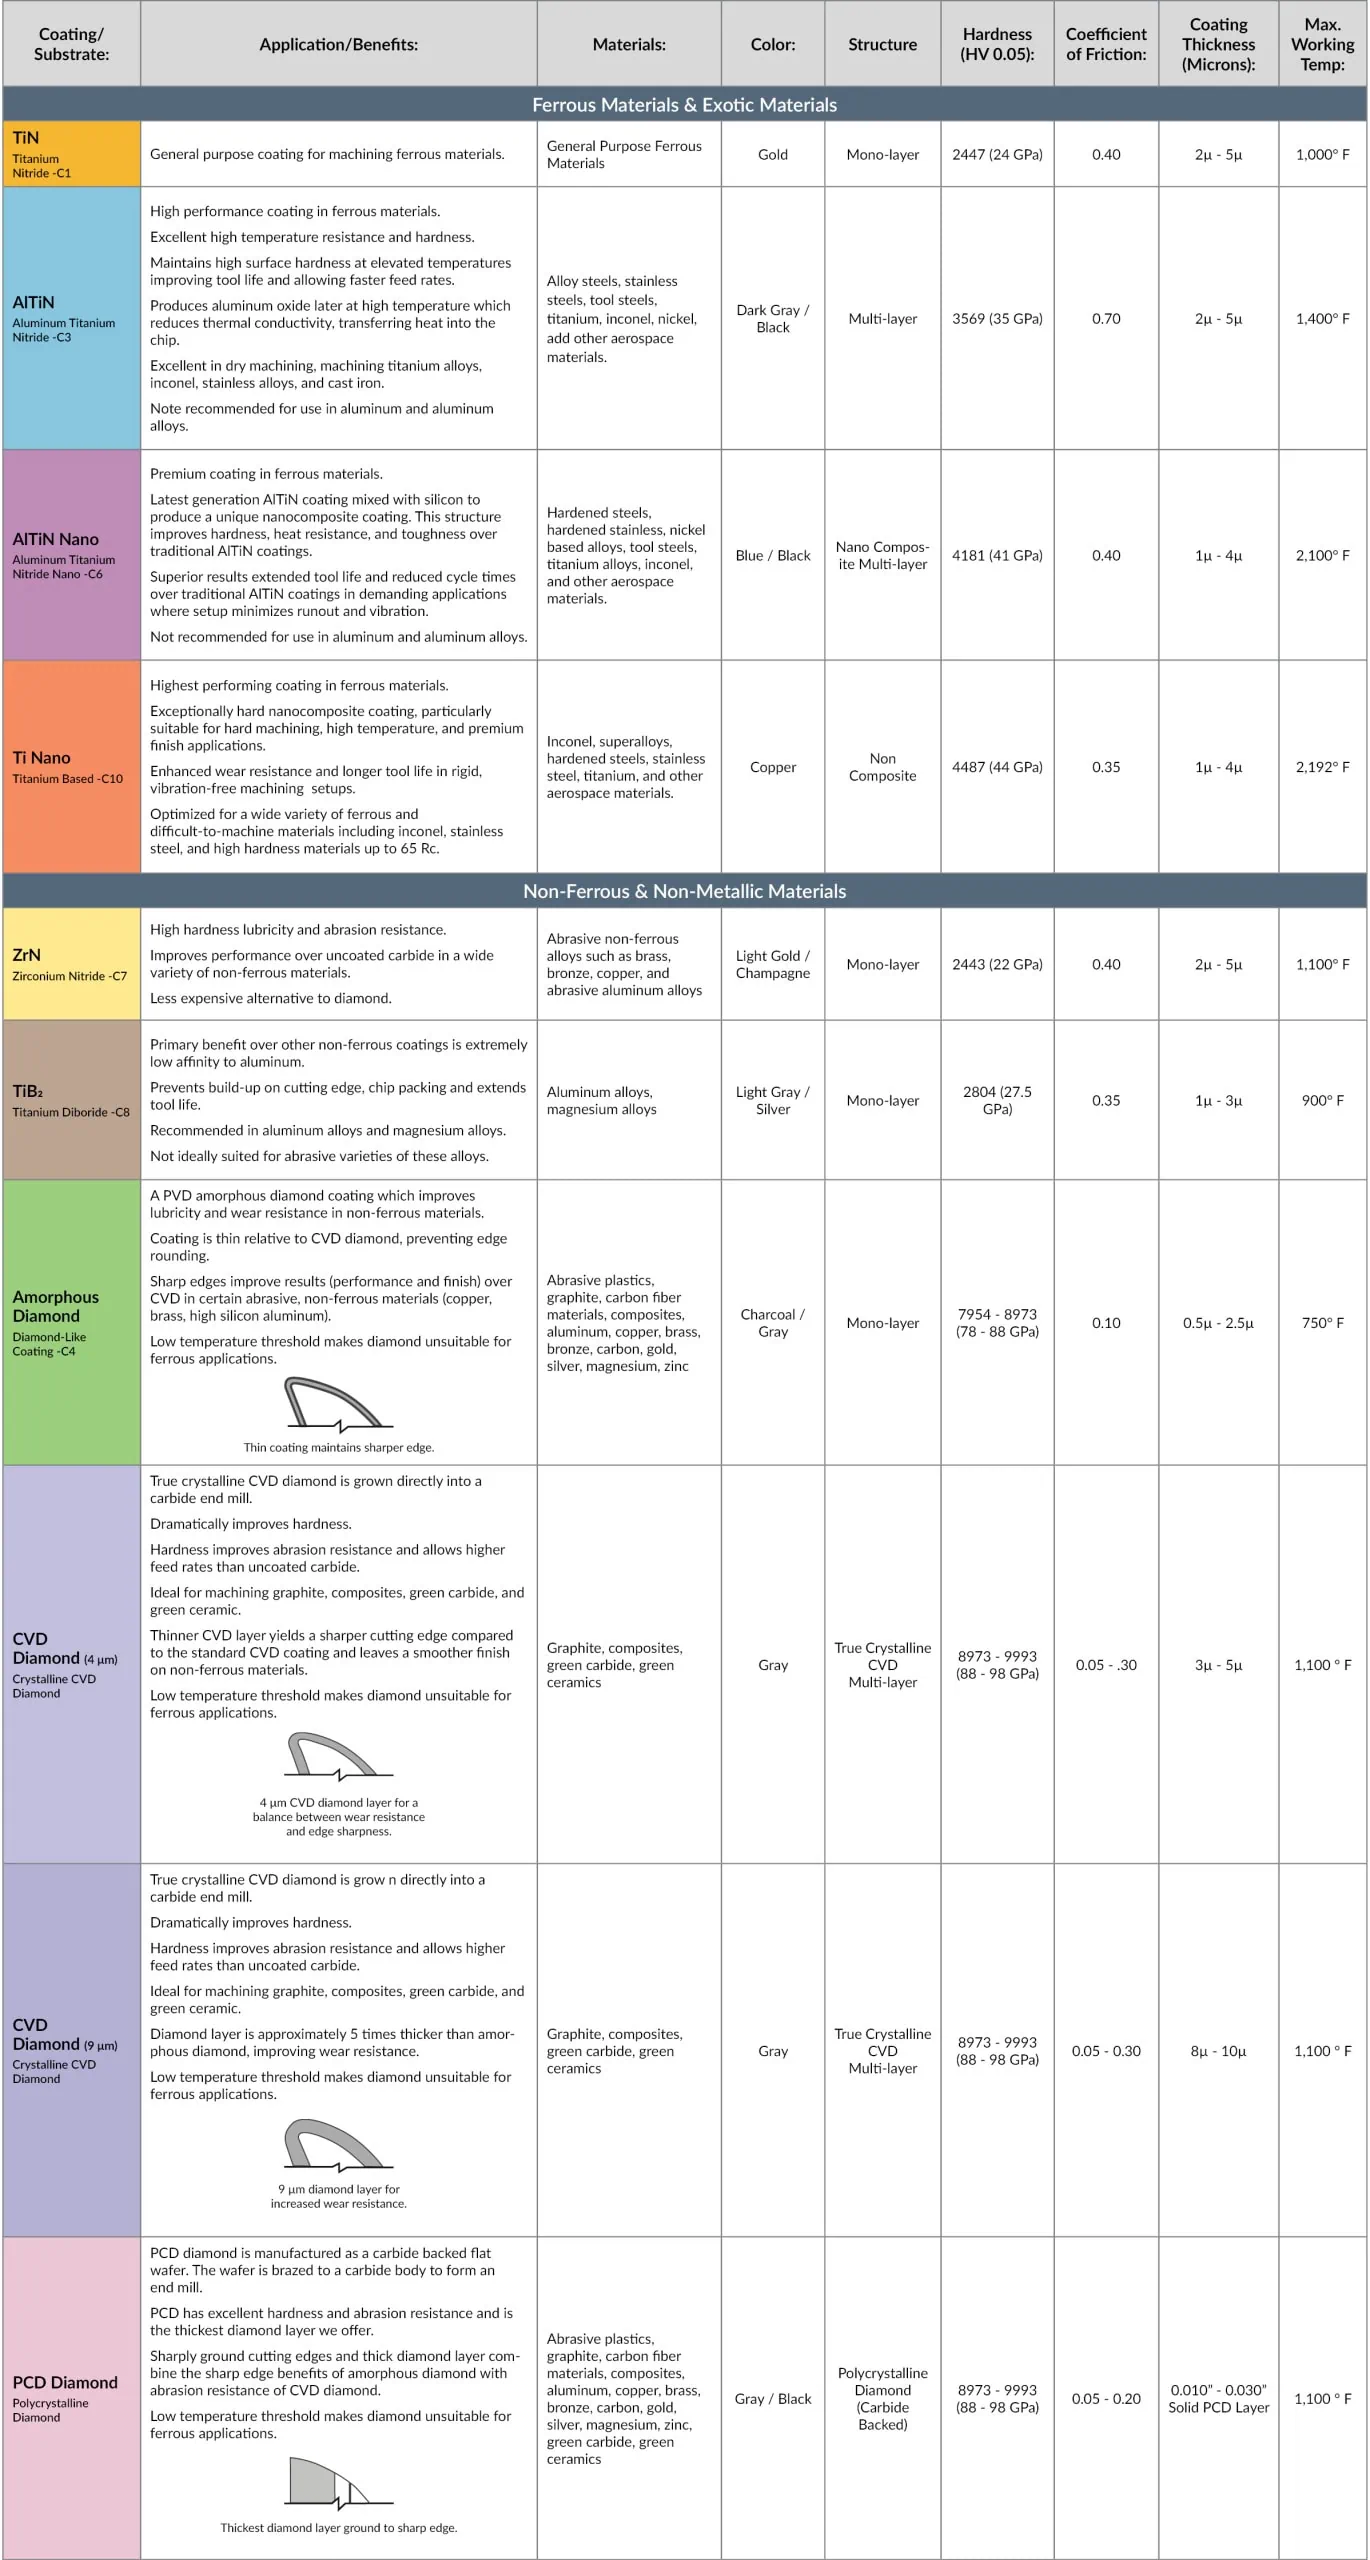
A coated engraving tool will last longer than an uncoated one because the coating provides a protective barrier between the tool and the workpiece. Additionally, coatings help reduce heat absorption, increase lubricity, and decrease tool wear. Selecting the right coating depends on the material being machined.

For example, our AlTiN and AlTiN-Nano coatings perform best in stainless steel and nickel alloys. For non-ferrous materials such as aluminum or copper, our Amorphous Diamond coating is ideal. As an alternative to our Amorphous Diamond coating, we also offer ZrN or TiB2 coatings.

A common misconception is that diamond-coated tools can be used on ferrous materials. Instead, this leads to rapid heat generation and premature tool failure.
Successfully Running Your Engraver

Selecting the correct engraving tool is just as important as understanding how to operate it properly. Even the highest-quality tool will be wasted if not used correctly. As with any machining operation, you must consider depth of cut, work holding methods, and appropriate speeds and feeds

Cutting Speeds and Feeds for Engraving 

The tip is the most delicate area of the tool which makes running at the correct speed and feed rate crucial. Running at an incorrect speed and feed rate can cause deflection, which will lead to an inaccurate engraving, chipping, breaking, or a poor surface finish.

At Harvey, we recommend a minimum spindle speed of 6,000 RPM. Operating at higher RPMs, when possible, offers even better support for tool tip integrity.

Higher speeds ensure tool stability as it will be less likely to cause vibration and reduces heat buildup during operation. Running too slowly generates excess heat and vibration leading to chipping, breakage, or having a poor surface finish. To help maintain tool tip integrity, it is important to follow the recommended depth of cut and consider the way the engraver enters the material.

Determining Depth of Cut

Many machinists are unaware that taking cuts deeper than 0.009 inches can shorten the lifespan of a Harvey engraving tool. For depth of cut ranging from 0.001 inch to 0.009 inches, you can operate within our stated speed and feed guidelines. If the operation requires a deeper groove, the chip load must be reduced accordingly. For depths between 0.010 inches and 0.015 inches, reduce the chip load by 20%. For depths ranging from 0.016 inches to 0.020 inches, reduce the chip load by 30%. Depth of cut also influences visibility. A deeper cut made with a tool that has a smaller angle can provide similar visibility to a shallower cut made with a tool that has a larger angle.

The image below illustrates different engraving depths using a 30° included angle. From left to right, the depths are 0.009 inches, 0.015 inches, and 0.020 inches. As depth increases, visibility improves. When engaging the tool with the workpiece, it is best to ramp into the material to protect the tool tip.

We recommend a ramp angle of 1° to 3° for ferrous materials such as stainless steel, and 3° to 10° for non-ferrous materials like aluminum or copper. If ramping is not an option, you may plunge the tool into the material. However, the chip load must be reduced by 50% during entry. Once the desired depth is reached, you can return to the recommended running parameters. Another key consideration is ensuring the workpiece is securely held in place.

Workholding Considerations

Runout or vibration during engraving can result in uneven cuts and tool failure. To prevent this, ensure that engraving tools are held in a sturdy toolholder and that the workpiece is secured. A shrink-fit toolholder minimizes runout and provides excellent stability. While ER collets are acceptable, they wear overtime. To verify an ER collet’s suitability, place an indicator on the tool shank and rotate the tool within the collet. The goal is to achieve the least possible runout, ideally no more than 0.0003 inches.

The workpiece should also be properly secured, either in a vise or a fixture. To detect vibrations during operation, listen for irregular noise or feel for vibrations through the CNC machine door. For cooling, coolants are recommended for metallic workpieces, while an air blast is preferable for non-metallic materials such as plastic.

Conclusion

When selecting an engraving tool, it is essential to choose the correct geometry for the operation, as well as the appropriate coating for the material being machined. Regardless of tip geometry, the engraving tool’s tip is its most fragile part. Proper speed, feed rate, and depth of cut are crucial for maximizing tool life.

For metallic workpieces, a cooling method such as coolant is necessary, while non-metallic workpieces require an air blast. Before starting a new engraving operation, double-check tool runout and ensure that the workpiece is securely held in place.

By following these best practices, CNC engraving operations can achieve high precision, longevity, and optimal tool performance.
Are You Ready to Put Your Engraving Knowledge to Use?

Browse Harvey Tool’s full selection of precision engravers, coatings, and geometries designed for optimal performance in a wide range of materials.

https://www.harveyperformance.com/wp-content/uploads/2025/09/Engraving-Tools-Featured.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-09-15 08:59:352025-09-16 09:46:49The Experts’ Guide to CNC Engraving

Corner Comparison: Corner Chamfer vs. Corner Radius

July 8, 2024/0 Comments/in CNC Machining, Milling, Milling, Tool Geometry, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

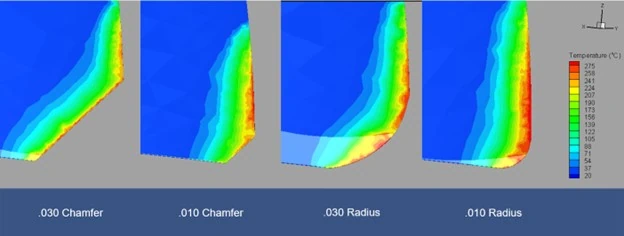
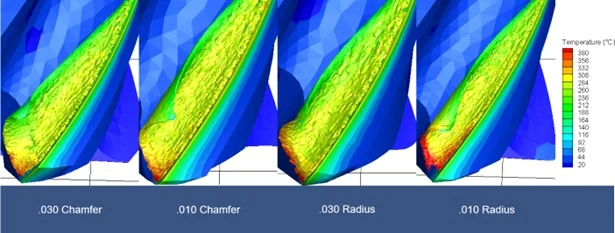
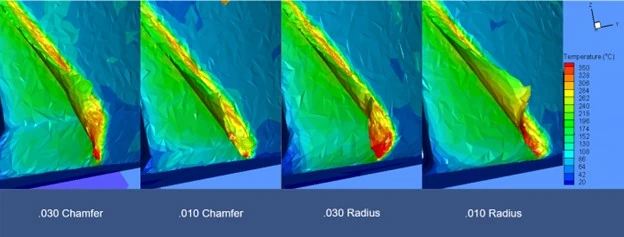
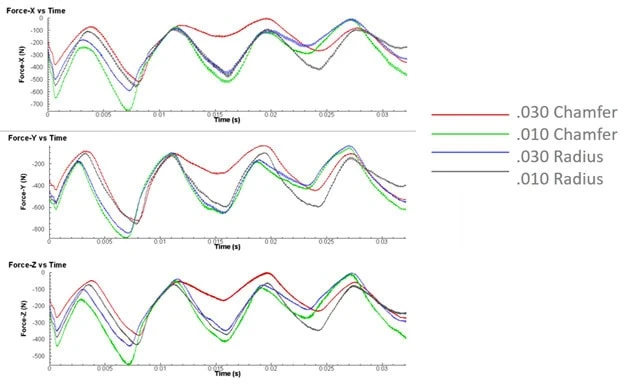
Using Finite Element Analysis (FEA) simulations by Third Wave Systems’ AdvantEdge CAE product, we tested different end mill corner geometries to compare their effects on both the tool and the workpiece. We studied and compared four 4 flute tools with either a 0.010” or 0.030” radius or chamfer. All tools were tested in 304 stainless steel at 1865 RPM, 244 SFM, and 0.0045 IPT for one revolution.

Both Corner Radius and Corner Chamfer tools offer advantages over Square End Mills by improving tool strength and reducing wear, though their benefits vary. One drawback of corner radius end mills is chip thinning along the radius, which can generate excess heat due to changes in chip thickness. This can lead to premature tool wear, poor surface finish, and potential work hardening. On the other hand, Corner Chamfers have the disadvantage of sharp corners where the chamfer meets the outer diameter (OD) and the end of the tool, causing local stress concentrations.

Force Analysis

The graphs above demonstrate the force exerted on the tool during cutting and how the corner size impacts the required force. As each flute engages, the forces peak in each direction. The 0.010” Chamfer generates the greatest force, while the 0.030” Chamfer requires the least. The forces with the radiused tools are very similar and fall between those of the two chamfered tools.

Temperature Analysis

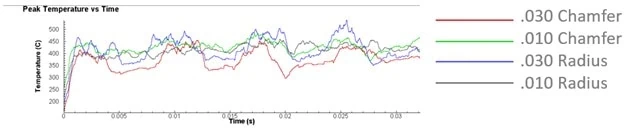
The peak tool temperature graph shows the impact of chip thinning on corner radius tools and the overall corner size. The 0.030” Radius generated the most heat, while the 0.030” Chamfer generated the least. The temperature differences between the 0.010” Chamfer and 0.010” Radius was minimal, with the 0.010” Radius generated slightly less heat.

Chip and Workpiece Temperature

Understanding the temperature of the chip and workpiece is crucial for assessing tool performance. The contours above illustrate that the most heat is generated along the 0.030” Radius, followed by the 0.010” Radius. Corner Chamfer tools performed better, maintaining a lower overall temperature due to the absence of chip thinning.
Stress Analysis

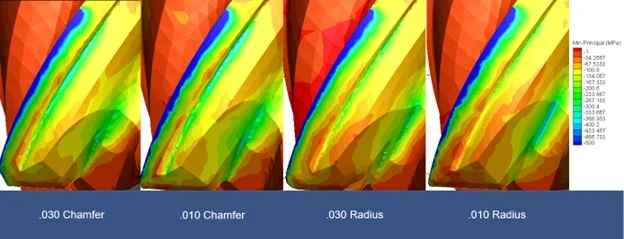
The minimum principal stress on the backside of the flute indicates areas prone to tool failure. While there were slight differences between the chamfers and radii, the most notable finding was the reduction in stress with increased corner break size.

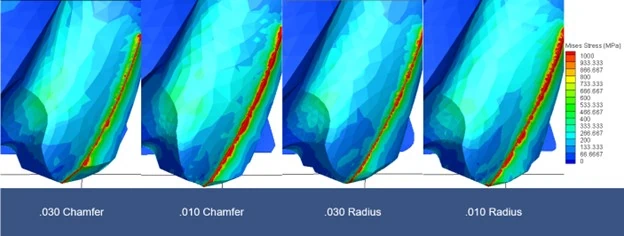
Similarly, the Mises stress analysis shows where stress is concentrated within the tool, potentially leading to failure. Again, the most significant observation was the reduction in stress with larger corner breaks.

Corner Chamfer vs. Corner Radius: Wrapped Up

Considering all factors, the 0.030” Corner Chamfer proved to be the best overall tool for 304 stainless steel. This is partly due to 304’s tendency to work harden, making excess heat generation particularly detrimental. When working with heat-sensitive materials, Corner Chamfer tools are preferable, especially during roughing, as they generate less heat due to the absence of chip thinning. Although there are minor stress concentrations at the sharp corners of Corner Chamfer tools, these are outweighed by the benefits of reduced heat generation. Larger radii exacerbate chip thinning’s impact on heat generation. While both tool styles offer advantages over square end mills, Corner Chamfer tools are more beneficial in high-heat applications where work hardening and tool wear are concerns.

Harvey Tool offers a range of Corner Chamfer Tools, with sizes ranging from 0.047” to 0.500” and various chamfer sizes to suit different applications.

https://www.harveyperformance.com/wp-content/uploads/2024/07/Featured-Image-FEA-Corner-Comparison.jpg 525 1399 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-07-08 12:15:282024-07-12 12:45:27Corner Comparison: Corner Chamfer vs. Corner Radius

Spot Drilling: The First Step to Precision Drilling

August 25, 2022/35 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Harvey Tool, Holemaking, Machining Techniques, Milling, Titan USA, Tool Selection, Troubleshooting Tips/by Tom Pyle

Drilling an ultra-precise hole can be tough. Material behavior, surface irregularities, and drill point geometry can all be factors leading to inaccurate holes. A Spot Drill, if used properly, will eliminate the chance of drill walking and will help to ensure a more accurate final product.

Choosing a Spot Drill

Ideally, the center of a carbide drill should always be the first point to contact your part. Therefore, a spotting drill should have a slightly larger point angle than that of your drill. Common drill point angles range from 118° to 140° and larger. Shallower drill angles are better suited to harder materials like steels due to increased engagement on the cutting edges. Aluminums can also benefit from these shallower angles through increased drill life. While these drills wear less and more evenly, they are more prone to walking, therefore creating a need for a proper high performance spot drill in a shallow angle to best match the chosen drill.

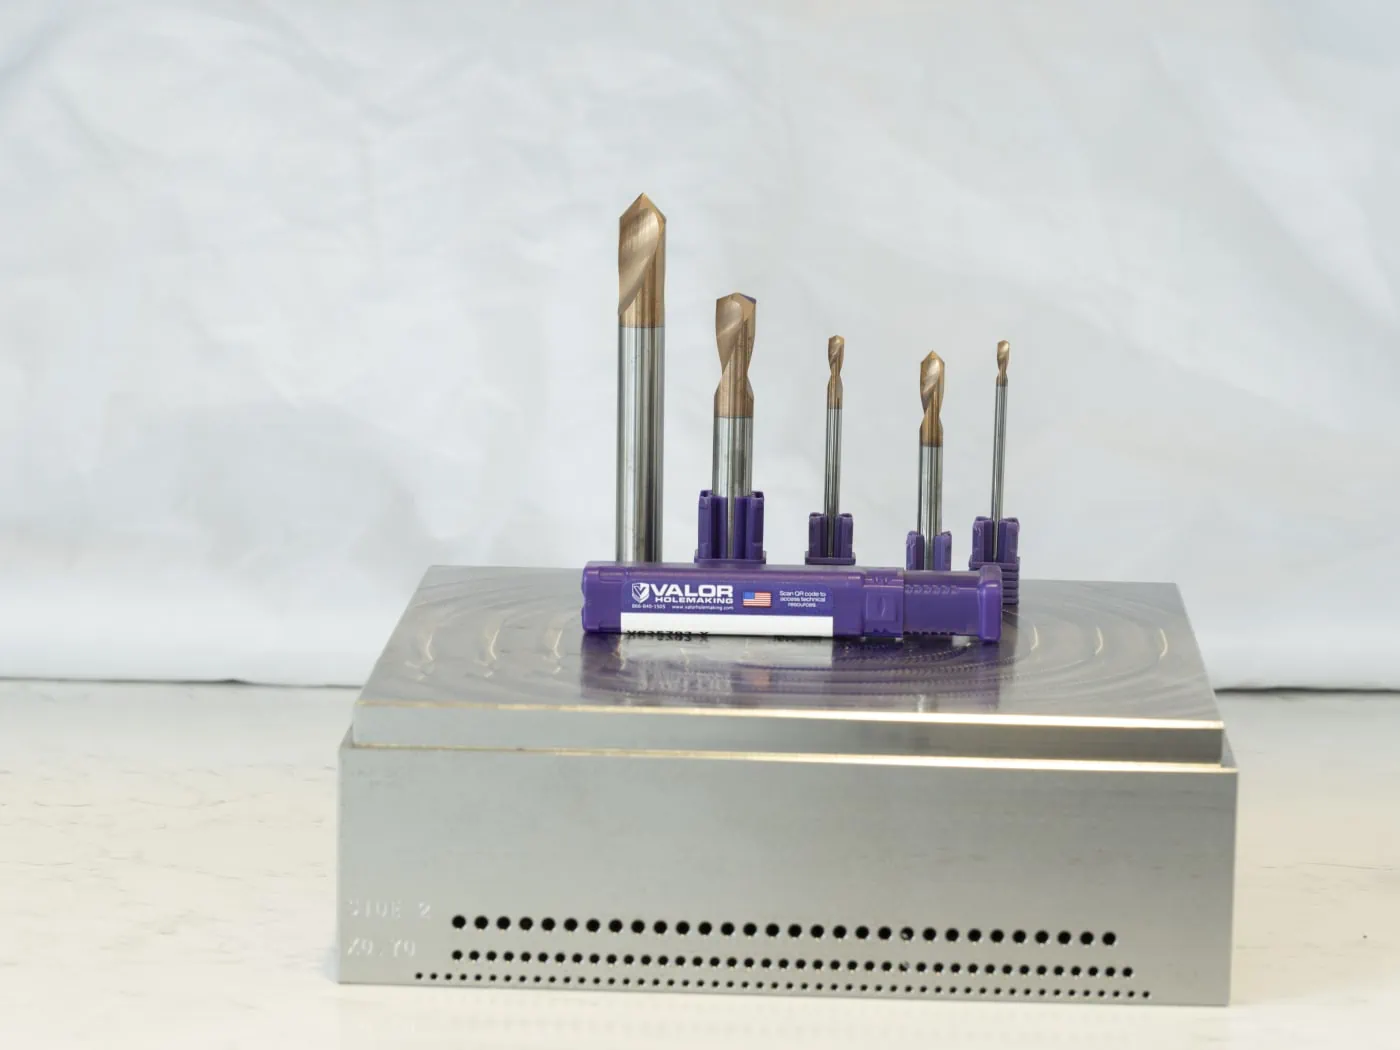
Five Valor holemaking high performance spot drills displayed on top of a workpiece with a purple product packaging container in front

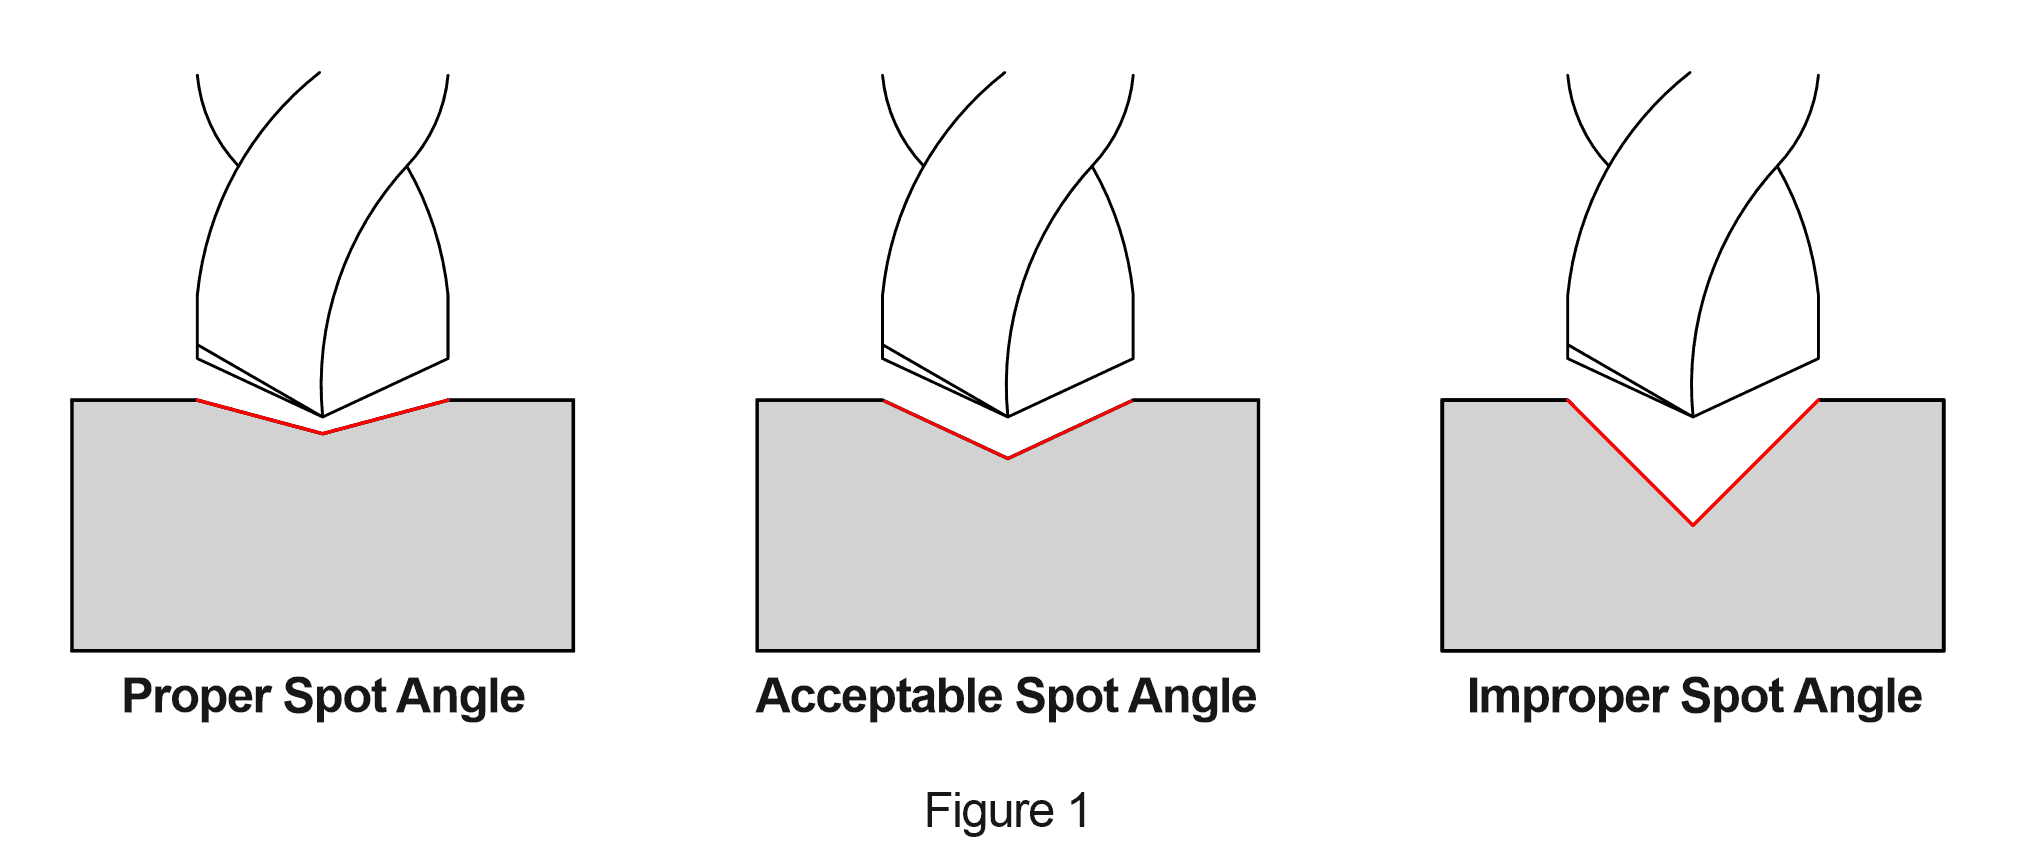
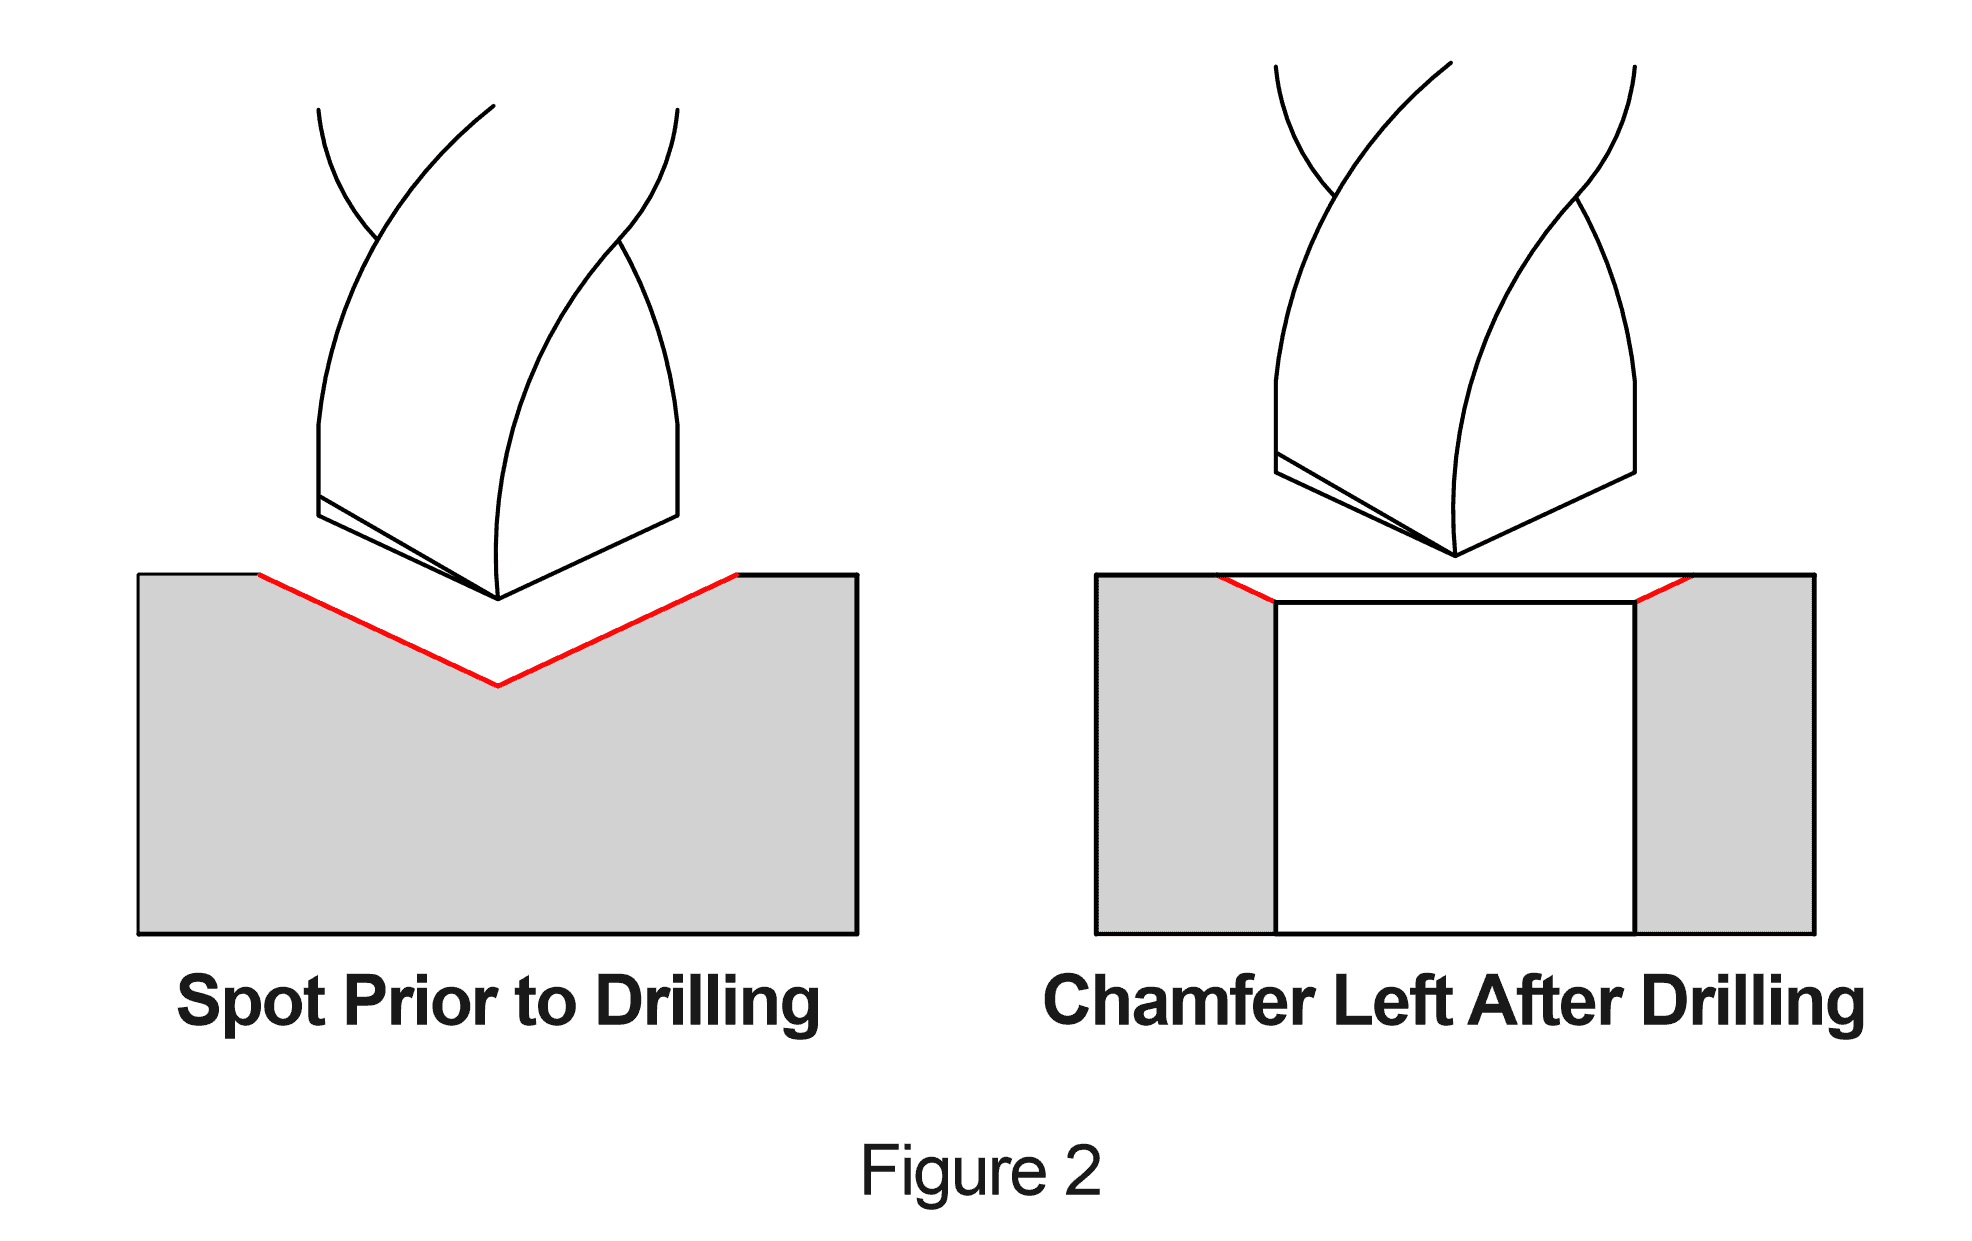
If a spotting drill with a smaller point angle than your drill is used, your drill may be damaged due to shock loading when the outer portion of its cutting surface contacts the workpiece before the center. Using a drill angle equal to the drill angle is also an acceptable situation. Figure 1 illustrates the desired effect. On the left, a drill is entering a previously drilled spot with a slightly larger angle than its point. On the right, a drill is approaching an area with an angle that is far too small for its point.

Proper Spot Angle Diagram

Marking Your Spot

A Spotting Drill’s purpose is to create a small divot to correctly locate the center of a drill when initiating a plunge. However, some machinists choose to use these tools for a different reason – using it to chamfer the top of drilled holes. By leaving a chamfer, screw heads sit flush with the part once inserted.

Spot Drill

What Happens if I Use a Spot Drill with an Improper Angle?

Using a larger angle drill will allow the drill to find the correct location by guiding the tip of the drill to the center. If the outer diameter of a carbide drill were to contact the workpiece first, the tool could chip. This would damage the workpiece and result in a defective tool. If the two flutes of the drill were slightly different from one another, one could come into contact before the other. This could lead to an inaccurate hole, and even counteract the purpose of spot drilling in the first place.

Avoiding CNC Drill Walking With a Spotting Drill

Few CNC machining applications demand precision like drilling. The diameter hole size, hole depth, part location, and finish are all important and provide little recourse if not up to specifications. That said, accuracy is paramount – and nothing leads to inaccurate final parts faster than drill walking, or the inadvertent straying from a drill’s intended location during the machining process. So how does drill walking occur, and how can one prevent it?

To understand drill walking, think about the act of striking a nail with a hammer, into a piece of wood. Firm contact to a sharp nail into an appropriate wood surface can result in an accurate, straight impact. But if other variables come into play – an uneven surface, a dull nail, an improper impact – that nail could enter a material at an angle, at an inaccurate location, or not at all. With CNC Drilling, the drill is obviously a critical element to a successful operation – a sharp, unworn cutting tool – when used properly, will go a long way toward an efficient and accurate final part.

To mitigate any variables working against you, such as an uneven part surface or a slightly used drill, a simple way to avoid “walking” is to utilize a Spotting Drill. This tool is engineered to leave a divot on the face of the part for a drill to engage during the holemaking process, keeping it properly aligned to avoid a drill from slipping off course.

When Won’t a Spot Drill Work for My Application?

When drilling into an extremely irregular surface, such as the side of a cylinder or an inclined plane, this tool may not be sufficient to keep holes in the correct position. For these applications, flat bottom versions or Flat Bottom Counterbores may be needed to creating accurate features.

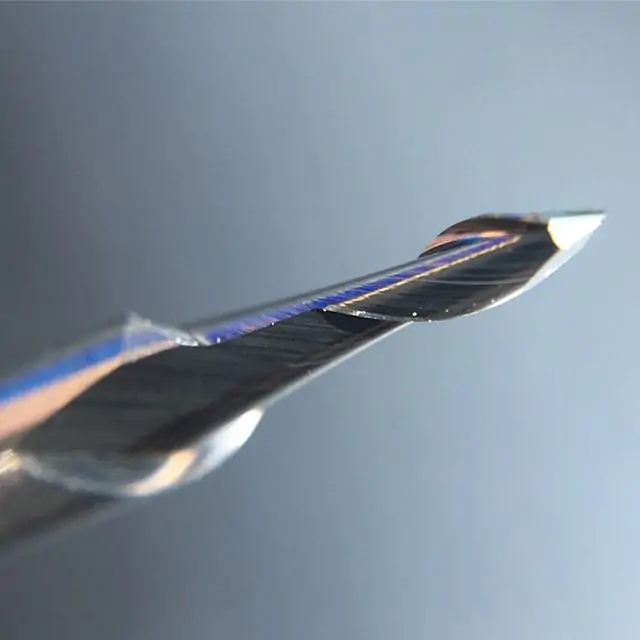
Harvey tool spot drill zoomed in on the tip of the drill
Harvey Tool Spot Drill
https://www.harveyperformance.com/wp-content/uploads/2017/03/Feature-Image-Spotting-Drills-IMG.jpg 525 1400 Tom Pyle http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Pyle2022-08-25 10:52:002023-10-18 08:19:12Spot Drilling: The First Step to Precision Drilling

Simplify Your Cutting Tool Orders

December 17, 2019/1 Comment/in CNC Machining, How-To's, Troubleshooting Tips/by Harvey Performance Company

With the launch of the new Helical Solutions website, Harvey Performance Company is proud to introduce a new way to order Helical cutting tools. Now, users of our new website are able to send a “shopping cart” of Helical tools they’re interested in directly to their distributor to place an order, or share it with a colleague. Let’s dive into the details about this functionality and learn how you can take advantage of the time savings associated with sending a “shopping cart” to your distributor for simplified ordering.

Get Started with a HelicalTool.com Account

First, you must create an account on HelicalTool.com. Having an account on the Helical website allows you to save and edit “shopping carts,” which can be sent to a distributor to place an order; choose a preferred distributor; auto-fill your information in any important forms; and to manage your shipping information.

Create Helical Account for Helical Shopping Cart

Now that you have an account, it is time to start creating your first “shopping cart.”

Creating a “Shopping Cart”

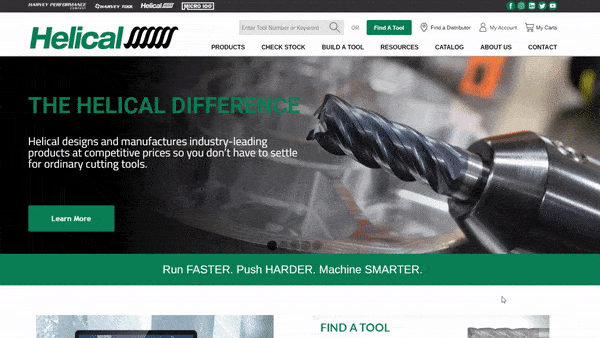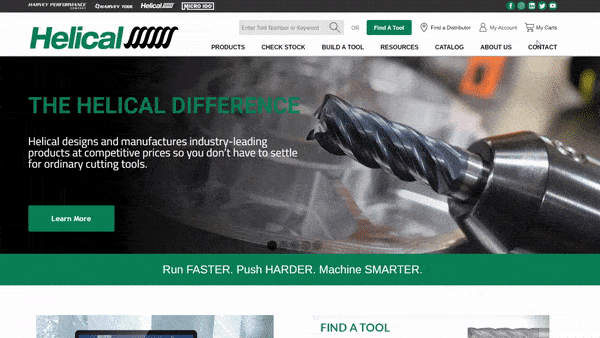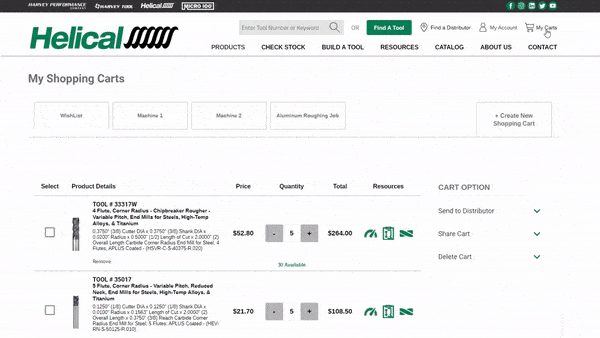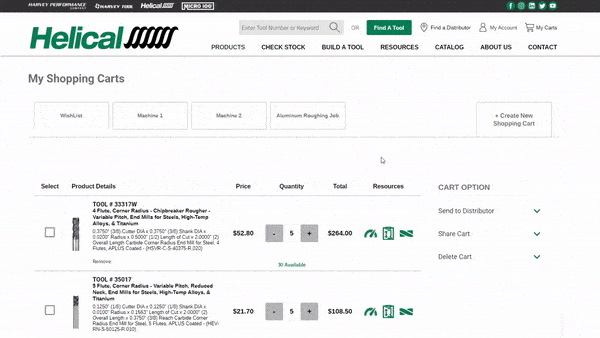
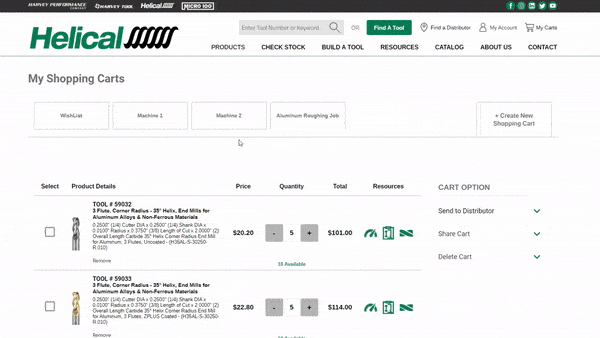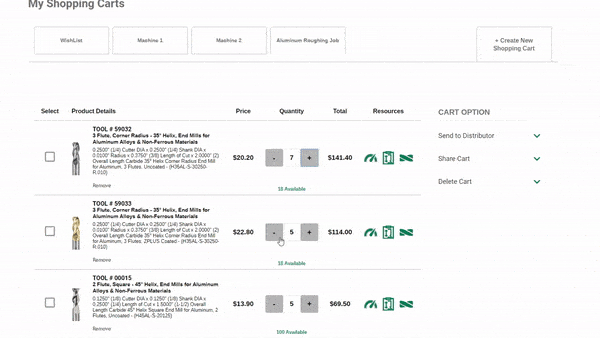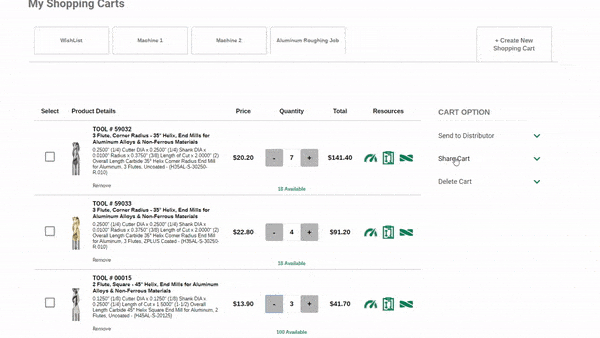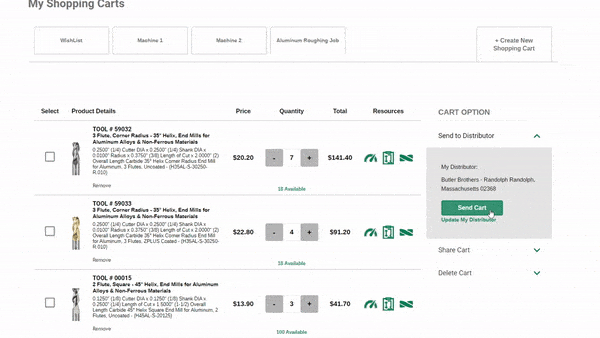
To begin creating a new shopping cart, simply click on the “My Carts” text in the top right menu. This will take you to the management portal, where you can add a new “shopping cart” by selecting “Create New Shopping Cart.”

Helical Solutions Order

Once complete, you can name your “shopping cart” anything you would like. One example might be creating a collection of tools for each of your jobs, or for different machines in the shop. In this case, we will name it “Aluminum Roughing Job.” You can create as many different “shopping carts” as you would like; they’ll never be removed from your account unless you choose to delete them, allowing you to go back to past tooling orders whenever you’d like.

Helical Solutions Website

Now that you have a “shopping cart” created, it is time to start adding tools to it!

Adding Tools to Your Helical “Shopping Cart”

There are multiple ways to add tooling to your “shopping cart,” but the easiest method is by heading to a product table. In this example, we will be adding tooling from our 3 Flute, Corner Radius – 35° Helix product line. We want to add a quantity of 5 of EDP #59033 to our “shopping cart.” To do this, simply click on the “Add To Cart” icon located in the table row next to pricing and tool descriptions. This will open up a small window where we can manage our selection. The first step will be to choose which “shopping cart” we want to add this tool to, so we will select our “Aluminum Roughing Job” collection.

Helical Online Ordering

Since this tool is offered uncoated and Zplus coated, we need to select which option we would like from the drop down menu. For this example, we will select the Zplus coated tool. Now, we simply need to update our quantity to “5”, and click “Add To Cart.” That tool will now appear in your “shopping cart” in the quantity selected.

If you need more information on a tool, you can click on an EDP number to be brought to the tool details page, where you can also add that EDP to your collection.

If you know the EDP number you need and want to check stock levels, use our Check Stock feature to check quantities on hand, and then add the tools to your “shopping cart” right from the Check Stock page.

Helical Shopping Cart checking stock

Now, it is time to send the “shopping cart” to place an order with your distributor!

Placing An Order With Your Distributor

Once you have completed adding tools to your Helical “shopping cart,” navigate back to the My Carts page to review it. From here, you can update quantities, see list pricing, and access valuable resources.

On the right side of the My Cart screen, you will see an option to “Send to Distributor.” Click on the text to expand the drop down. If you have previously added a preferred distributor from your account page and they are participating in our Shopping Cart Program, you will see their information in this area.

If you have not yet selected a preferred distributor, select “Update My Distributor.” This will bring you to a new page where you can select your state and see all participating distributors in your area. Select one distributor as your preferred distributor, and then head back to the My Cart page.

Now that you have a distributor selected, you can do a final review of the “shopping cart,” and then simply click “Send Cart.” This will send an email order directly to your distributor with all of your shipping information, your list of tools and requested quantities, and your contact information. You will also receive a copy of this email for your records.

Helical Shopping Cart Distributor

Within 1 business day, the distributor will follow up with you to confirm the order, process payment, and get the tools shipped out and on the way to your shop. No more phone calls or emails – just a single click, and your order is in the hands of our distributor partners.

To get started with this exciting new way to shop for Helical cutting tools, click here to begin creating an account on HelicalTool.com!

https://www.harveyperformance.com/wp-content/uploads/2019/12/Feature-Image-Simplify-Tool-Orders-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2019-12-17 05:51:492021-11-19 08:14:39Simplify Your Cutting Tool Orders

Using Tool Libraries in Autodesk HSM & Fusion 360

November 27, 2018/0 Comments/in CNC Programming, Machining 101, Troubleshooting Tips/by Harvey Performance Company

The days of modeling your tools in CAM are coming to an end. Harvey Performance Company has partnered with Autodesk to provide comprehensive Harvey Tool and Helical Solutions tool libraries to Fusion 360 and Autodesk HSM users. Now, users can access 3D models of every Harvey and Helical tool with a quick download and a few simple clicks. Keep reading to learn how to download these libraries, find the tool you are looking for, how to think about speeds and feeds for these libraries, and more.

Downloading Tool Libraries

On the Autodesk HSM Tools page, you will find Harvey Tool and Helical Solutions tool libraries. Clicking either of the previous links will bring you to that brand’s tool libraries. Right now, all of the two brands more than 27,000 tools are supported in the tool libraries.

Once on the page, there will be a download option for both Fusion and HSM. Select which software you are currently using to be prompted with a download for the correct file format.

From there, you will need to import the tool libraries from your Downloads folder into Fusion 360 or HSM. These tool libraries can be imported into your “Local” or “Cloud” libraries in Fusion 360, depending on where you would like them to appear. For HSM, simply import the HSMLIB file you have downloaded as you would any other tool library.

Curt Chan, Autodesk MFG Marketing Manager, takes a deeper dive into the process behind downloading, importing, and using CAM tool libraries to Fusion in the instructional video below.

For HSM users, jump to the 2:45 mark in this video from Autodesk’s Lars Christensen, who explains how to download and import these libraries into Autodesk HSM.


Selecting a Tool

Once you have downloaded and imported your tool libraries, selecting a specific tool or group of tools can be done in several ways.

Searching by Tool Number

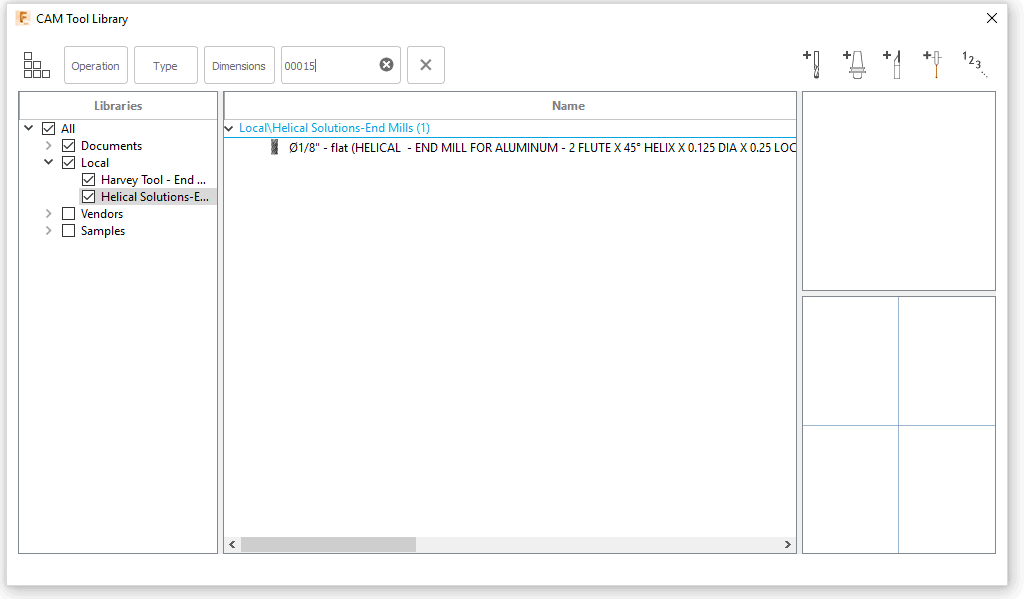
To search by tool number, simply enter the tool number into the search bar at the top of your tool library window. For example, if you are looking for Helical Tool EDP 00015, enter “00015” into the search bar and the results will narrow to show only that tool.

Fusion 360 Tool Libraries

In the default display settings for Fusion 360, the tool number is not displayed in the table of results, where you will find the tool name, flute count, cutter diameter, and other important information. If you would like to add the tool number to this list of available data, you can right click on the top menu bar where it says “Name” and select “Product ID” from the drop down menu. This will add the tool number (ex. 00015) to the list of information readily available to you in the table.

Harvey Tool Tool Libraries

Searching by Keyword

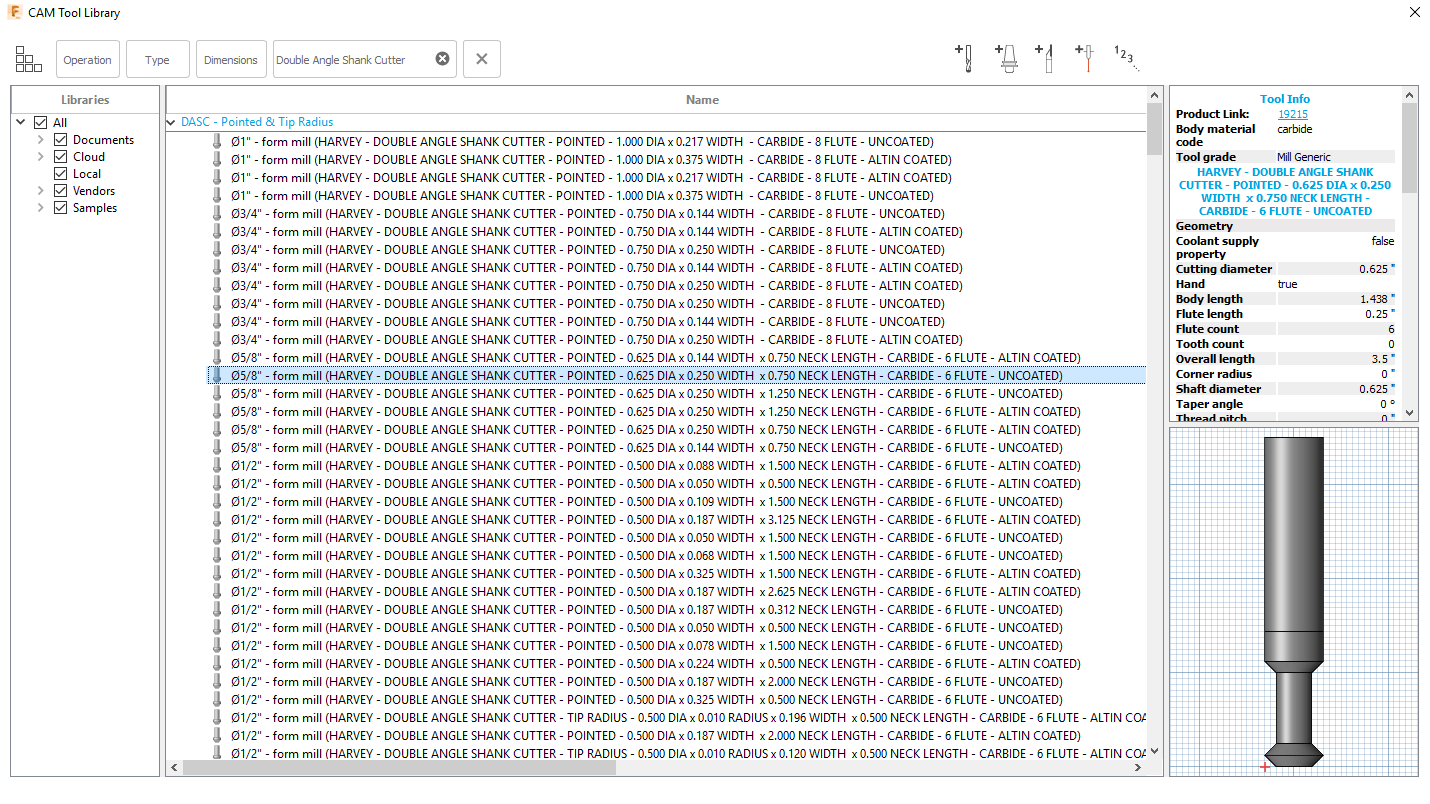
To search by a keyword, simply input the keyword into the search bar at the top of the tool library window. For example, if you are looking for metric tooling, you can search “metric” to filter by tools matching that keyword. This is helpful when searching for Specialty Profile tools which are not supported by the current profile filters, like the Harvey Tool Double Angle Shank Cutters seen in the example below.

Fusion 360 Tool Libraries

Searching by Tool Type

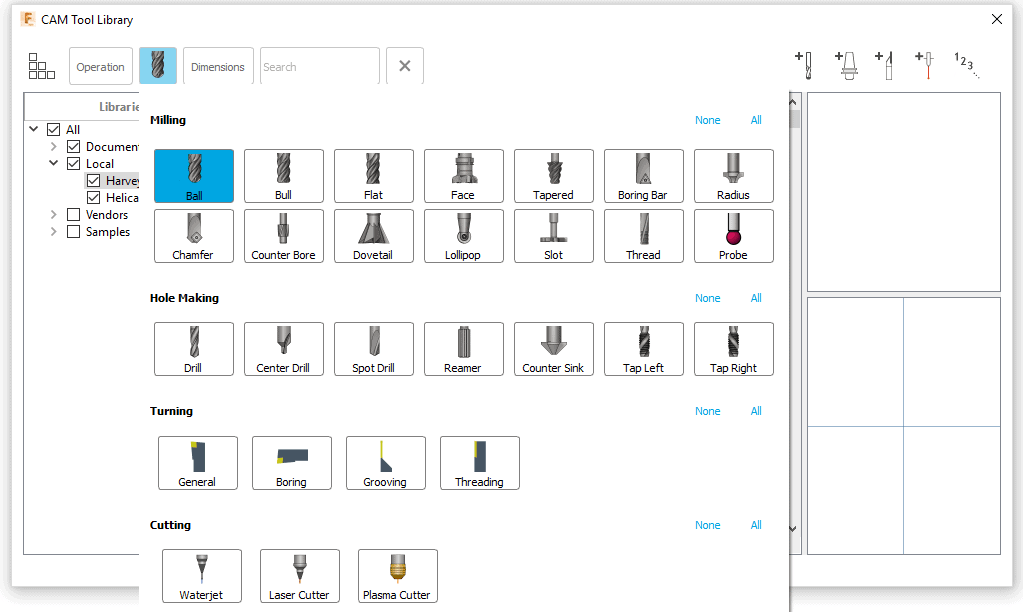
To search by tool type, click the “Type” button in the top menu of your tool library window. From there, you will be able to segment the tools by their profile. For example, if you only wanted to see Harvey Tool ball nose end mills, choose “Ball” and your tool results will filter accordingly.

CAM Tool Libraries

As more specialty profiles are added, these filters will allow you to filter by profiles such as chamfer, dovetail, drill, threadmill, and more. However, some specialty profile tools do not currently have a supported tool type. These tools show as “form tools” and are easier to find by searching by tool number or name. For example, there is not currently a profile filter for “Double Angle Shank Cutters” so you will not be able to sort by that profile. Instead, type “Double Angle Shank Cutter” into the search bar (see “Searching by Keyword”) to filter by that tool type.

Searching by Tool Dimensions

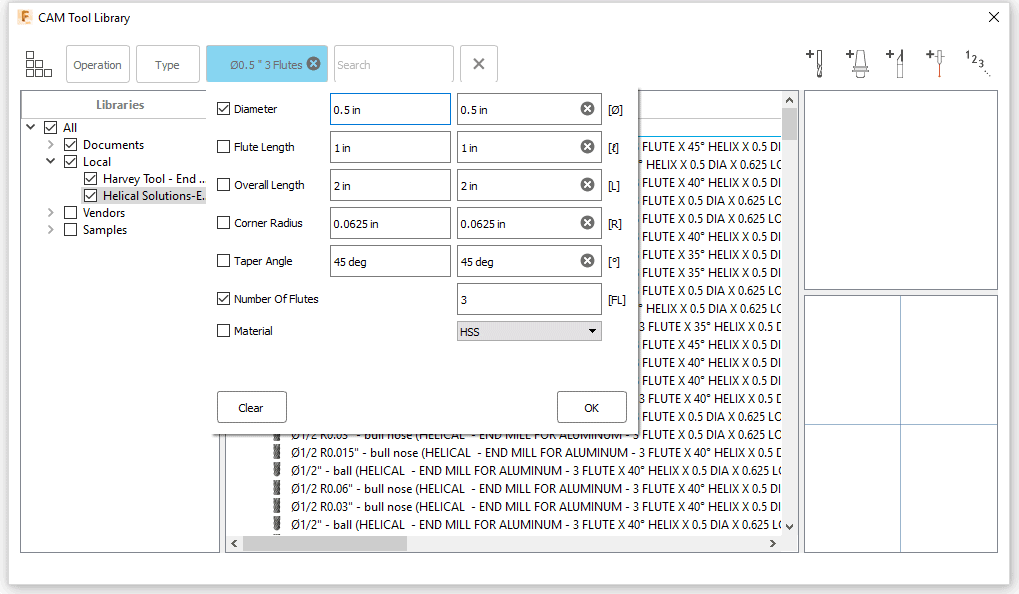
To search by tool dimensions, click the “Dimensions” button in the top menu of your tool library window. From there, you will be able to filter tools by your desired dimensions, including cutter diameter, flute count, overall length, radius, and flute length (also known as length of cut). For example, if you wanted to see Helical 3 flute end mills in a 0.5 inch diameter, you would check off the boxes next to “Diameter” and “Flute Count” and enter the values you are looking for. From there, the tool results will filter based on the selections you have made.

CAM Tool Libraries

Using Specialty Profile Tools

Due to the differences in naming conventions between manufacturers, some Harvey Tool/Helical specialty profile tools will not appear exactly as you think in Fusion 360/HSM. However, each tool does contain a description with the exact name of the tool. For example, Harvey Tool Drill/End Mills display in Fusion 360 as Spot Drills, but the description field will call them out as Drill/End Mill tools, as you can see below.

Below is a chart that will help you match up Harvey Tool/Helical tool names with the current Fusion 360 tool names.

Tool NameFusion 360 Name
Back Chamfer CutterDovetail Mill
Chamfer CuttersChamfer Mill
Corner Rounding End Mill – UnflaredRadius Mill
Dovetail CutterDovetail Mill
Drill/End MillSpot Drill
Engraving Cutter/Marking Cutter – Tip RadiusTapered Mill
Engraving Cutter – Tipped Off & PointedChamfer Mill
Keyseat CutterSlot Mill
Runner CutterTapered Mill
Undercutting End MillLollipop Mill
All Other Specialty ProfilesForm Mill

Speeds and Feeds

To ensure the best possible machining results, we have decided not to pre-populate speeds and feeds information into our tool libraries. Instead, we encourage machinists to access the speeds and feeds resources that we offer to dial accurate running parameters based on their material, application, and machine capabilities.

Harvey Tool Speeds & Feeds

To access speeds and feeds information for your Harvey Tool product, head to http://www.harveytool.com/cms/SpeedsFeeds_228.aspx to find speeds and feeds libraries for every tool.

If you are looking for tool specific speeds and feeds information, you will need to access the tool’s “Tech Info” page. You can reach these pages by clicking any of the hyperlinked tool numbers across all of our product tables. From there, simply click “Speeds & Feeds” to access the speeds and feeds PDF for that specific tool.

If you have further questions about speeds and feeds, please reach out to our Technical Support team. They can be reached Monday-Friday from 8 AM to 7 PM EST at 800-645-5609, or by email at [email protected].

Helical Solutions Speeds & Feeds

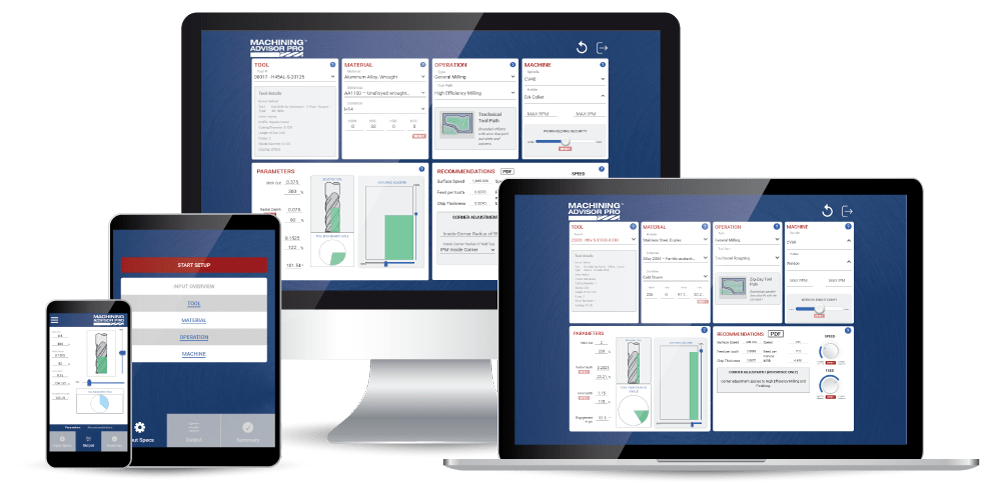
To access speeds and feeds information for your Helical Solutions end mills, we recommend using our Machining Advisor Pro application. Machining Advisor Pro (MAP) generates specialized machining parameters by pairing the unique geometries of your Helical Solutions end mill with your exact tool path, material, and machine setup. MAP is available free of charge as a web-based desktop app, or as a downloadable application on the App Store for iOS and Google Play.

machining advisor pro

To learn more about Machining Advisor Pro and get started today, visit www.machiningadvisorpro.com. If you have any questions about MAP, please reach out to us at [email protected].

If you have further questions about speeds and feeds, please reach out to our Technical Support team. They can be reached Monday-Friday from 8 AM to 7 PM EST at 866-543-5422, or by email at [email protected].


For additional questions or help using tool libraries, please send an email to [email protected]. If you would like to request a Harvey Performance Company tool library be added to your CAM package, please fill out the form here and let us know! We will be sure to notify you when your CAM package has available tool libraries.

https://www.harveyperformance.com/wp-content/uploads/2018/11/Feature-Image-HSM-Tool-Libraries-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-11-27 09:48:482024-02-09 11:36:18Using Tool Libraries in Autodesk HSM & Fusion 360

Tool Deflection & Its Remedies

May 3, 2018/6 Comments/in CNC Machining, How-To's, Machining 101, Troubleshooting Tips/by Jacob Concepcion

What is Tool Deflection?

Every machinist must be aware of tool deflection, as too much deflection can lead to catastrophic failure in the tool or workpiece. Deflection is the displacement of an object under a load causing curvature and/or fracture.

For Example: When looking at a diving board at rest without the pressure of a person’s weight upon it, the board is straight. But as the diver progresses down further to the end of the board, it bends further. Deflection in tooling can be thought of in a similar way.

Signs of Tool Deflection

  • Shortened tool life and/or tool breakage
  • Subpar surface finish
  • Part dimensional inaccuracies

Tool Deflection Remedies

Minimize Overhang

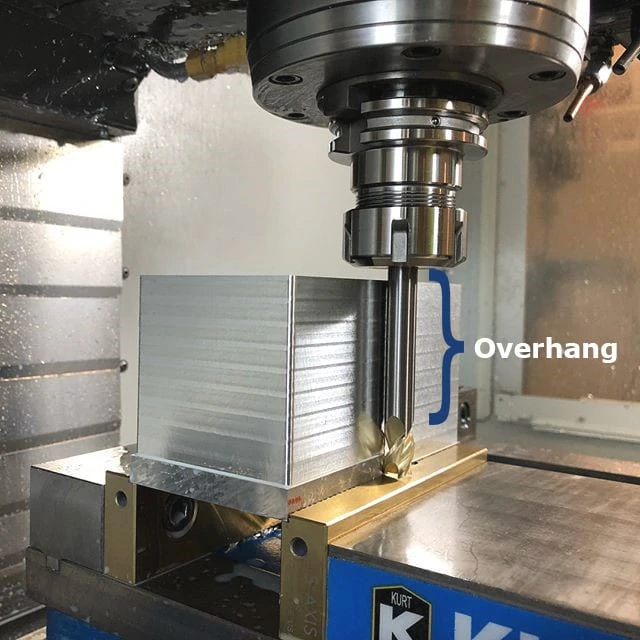
Overhang refers to the distance a tool is sticking out of the tool holder. Simply, as overhang increases, the tool’s likelihood of deflection increases. The larger distance a tool hangs out of the holder, the less shank there is to grip, and depending on the shank length, this could lead to harmonics in the tool that can cause fracture. Simply put, For optimal working conditions, minimize overhang by chucking the tool as much as possible.

extended reach tool in tool holder with overhang depth called out
Image Source: @NuevaPrecision

Long Flute vs. Long Reach

Another way to minimize deflection is having a full grasp on the differences between a long flute and a long reach tool. The reason for such a difference in rigidity between the two is the core diameter of the tool. The more material, the more rigid the tool; the shorter the length of flute, the more rigid the tool and the longer the tool life. While each tooling option has its benefits and necessary uses, using the right option for an operation is important.

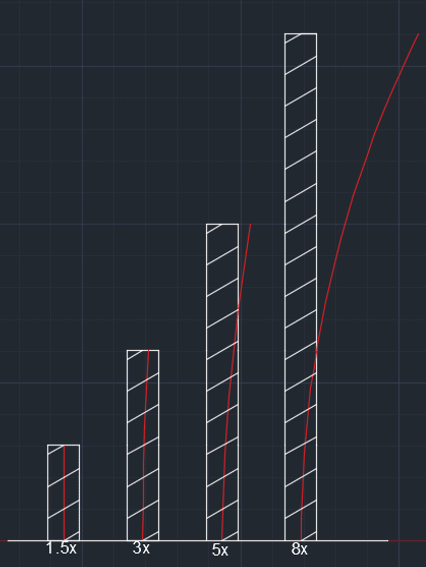
The below charts illustrate the relationship between force on the tip and length of flute showing how much the tool will deflect if only the tip is engaged while cutting. One of the key ways to get the longest life out of your tool is by increasing rigidity by selecting the smallest reach and length of cut on the largest diameter tool.

tool deflection in relation to length of tool

tool deflection graph

Click Here to Learn More About Proper Tool Holding and Runout

When to Opt for a Long Reach Tool

Reached tools are typically used to remove material where there is a gap that the shank would not fit in, but a noncutting extension of the cutter diameter would. This length of reach behind the cutting edge is also slightly reduced from the cutter diameter to prevent heeling (rubbing of noncutting surface against the part). Reached tools are one of the best tools to add to a tool crib because of their versatility and tool life.

long reach ball end mill
Long Reach Tool: Variable Helix End Mills for Exotic Alloys – Ball – Long Reach, Stub Flute

When to Opt for a Long Flute Tool

Long Flute tools have longer lengths of cut and are typically used for either maintaining a seamless wall on the side of a part, or within a slot for finishing applications. The core diameter is the same size throughout the cutting length, leading to more potential for deflection within a part. This possibly can lead to a tapered edge if too little of the cutting edge is engaged with a high feed rate. When cutting in deep slots, these tools are very effective. When using HEM, they are also very beneficial due to their chip evacuation capabilities that reached tools do not have.

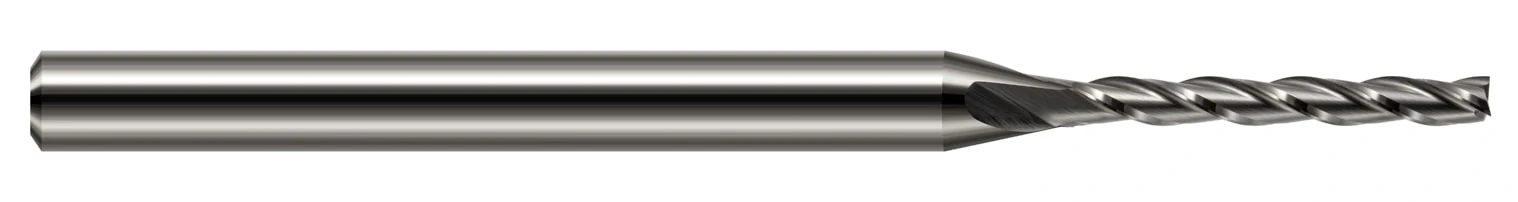
long flute end milling tool
Long Flute Tool: Miniature End Mills – Square Long Flute

Deflection & Tool Core Strength

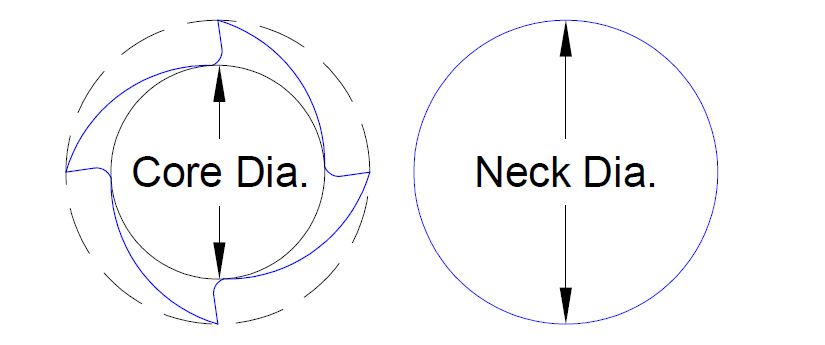
Diameter is an important factor when calculating deflection. Machinists oftentimes use the cutter diameter in the calculation of long flute tools, when in actuality the core diameter (shown below) is the necessary dimension. This is because the fluted portion of a tool has an absence of material in the flute valleys. For a reached tool, the core diameter would be used in the calculation until its reached portion, at which point it transitions to the neck diameter. When changing these values, it can lower deflection to a point where it is not noticeable for the reached tool but could affect critical dimensions in a long flute tool.

core diameter vs neck diameter infographic

Deflection Summarized

Tool deflection can cause damage to your tool and scrap your part if not properly accounted for prior to beginning a job. Be sure to minimize the distance from the tool holder to the tip of the tool to keep deflection to a minimum. For more information on ways to reduce tool deflection in your machining, view Diving into Depth of Cut.

https://www.harveyperformance.com/wp-content/uploads/2018/05/Featured-Image-Tool-Deflection-IMG.jpg 525 1400 Jacob Concepcion http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Jacob Concepcion2018-05-03 09:42:392024-03-05 16:25:18Tool Deflection & Its Remedies

5 Ways Your Shop is Inefficient

March 5, 2018/2 Comments/in Getting Started, Machining 101, Machining Techniques, Troubleshooting Tips/by Harvey Performance Company

5 Ways Your Shop is Inefficient

In today’s ultracompetitive industry, every machine shop seeks even the slightest edge to gain an advantage on their competition and boost their bottom line. However, what many machinists don’t know is that improving their shop’s efficiency might be easier than they thought. The following five ways your shop is inefficient will provide a clear starting point of where to look for machinists desperate to earn a competitive edge.

Premature Tool Decay / Tool Failure

If you’re finding that your tools are failing or breaking at an unacceptable rate, don’t mistake it for commonplace. It doesn’t have to be. Prolonging the life of your tooling starts with finding not just the right tool, but the best one; as well as running it in a way to get its optimal performance. Many machinists mistake premature tool failure with running parameters that were too aggressive. In fact, not pushing the tool to its full potential can actually cause it to decay at an accelerated rate in certain situations.
Tool failure can occur in many different ways: Abrasive Wear, Chipping, Thermal Cracking or Tool Fracture, just to name a few. Understanding each type and its causes can help you to quickly boost your shop’s efficiency by minimizing downtime and saving on replacement tool costs.

close up view of excessive tool wear on a cutting edge

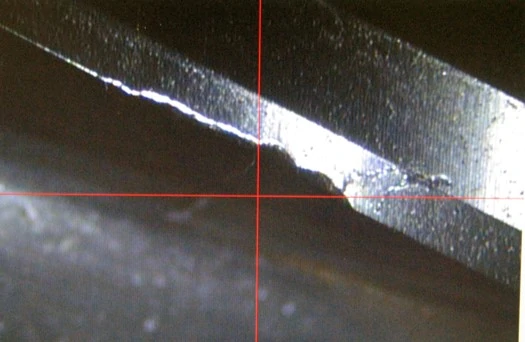
An example of a tool with excessive wear

For more information on tool wear, view Avoiding 4 Major Types of Tool Wear.

Subpar Part Finish

Your shop spends money to employ machinists, run machines, and buy cutting tools. Get your money’s worth, lead the industry, and ensure that you’re providing your customers with the highest quality product. Not only will this help to keep your buyer-seller relationship strong, but it will allow you the flexibility to increase your prices in the future, and will attract prospective customers.

Many factors influence part finish, including the material and its hardness, the speeds and feeds you’re running your tool at, tool deflection, and the tool-to-workpiece orientation.

For more information on ways to improve your part finish, view our Part Finish Reference Guide.

Inefficient Coolant Usage

One often forgotten expense of a machine shop is coolant – and it can be pricey. A 55-gallon drum of coolant can run more than $1,500. What’s worse is that coolant is often applied in excess of what’s required for the job. In fact, some machines even feature a Minimum Quantity Lubricant (MQL) functionality, which applies coolant as an extremely fine mist or aerosol, providing just enough coolant to perform a given operation effectively. While drowning a workpiece in coolant, known as a “Flood Coolant,” is sometimes needed, it is oftentimes utilized on jobs that would suffice with much less.

For more information about coolants and which method of application might be best for your job, view What You Need to Know About Coolant for CNC Machining.

Not Taking Advantage of Tool Versatility

Did you know that several CNC cutting tools can perform multiple operations? For example, a Chamfer Mill can chamfer, bevel, deburr, and countersink. Some Chamfer Mills can even be used as a Spotting Drill. Of course, the complexity of the job will dictate your ability to reap the benefits of a tool’s versatility. For instance, a Spotting Drill is obviously the best option for spotting a hole. If performing a simple operation, though, don’t go out of your way to buy additional tooling when what’s already in your carousel can handle it.

two helical solutions chamfer mills

To learn more about versatile tools that can perform multiple applications, check out Multi-Functional Tools Every Shop Should Have.

High Machine Downtime Makes Your Shop Inefficient

What use is a machine that’s not running beside making your shop inefficient? Minimizing machine downtime is a key way to ensure that your shop is reaching its efficiency pinnacle. This can be accomplished a variety of ways, including keeping like-parts together. This allows for a simple swap-in, swap-out of material to be machined by the same cutting tool. This saves valuable time swapping out tooling, and lets your machine to do its job for more time per workday. Production planning is a key factor to running an efficient machine shop.

https://www.harveyperformance.com/wp-content/uploads/2018/03/Featured-Image-Shop-Inefficient-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-03-05 14:30:062023-10-12 14:34:385 Ways Your Shop is Inefficient

8 Ways You’re Killing Your End Mill

February 7, 2018/8 Comments/in CNC Machining, Quick Tips, Tech Tips, Trending Now, Troubleshooting Tips/by Harvey Performance Company


Running It Too Fast or Too Slow Can Impact Tool Life

Determining the right speeds and feeds for your tool and operation can be a complicated process, but understanding the ideal speed (RPM) is necessary before you start running your machine to ensure proper tool life. Running a tool too fast can cause suboptimal chip size or even catastrophic tool failure. Conversely, a low RPM can result in deflection, bad finish, or simply decreased metal removal rates. If you are unsure what the ideal RPM for your job is, contact the tool manufacturer.

Feeding It Too Little or Too Much

Another critical aspect of speeds and feeds, the best feed rate for a job varies considerably by tool type and workpiece material. If you run your tool with too slow of a feed rate, you run the risk of recutting chips and accelerating tool wear. If you run your tool with too fast of a feed rate, you can cause tool fracture. This is especially true with miniature tooling.

Using Traditional Roughing

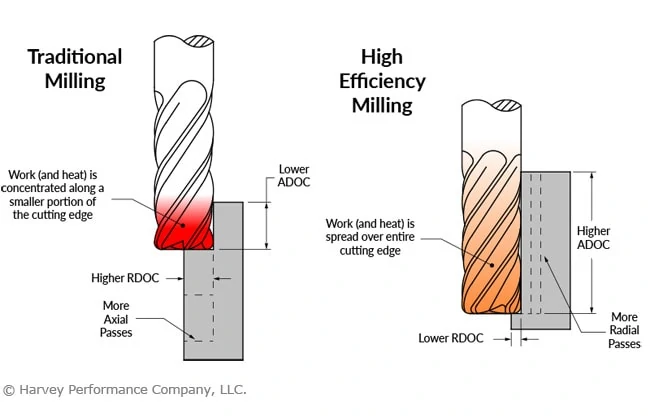
infographic of traditional versus high efficiency milling depths of cut and heat generation

While traditional roughing is occasionally necessary or optimal, it is generally inferior to High Efficiency Milling (HEM). HEM is a roughing technique that uses a lower Radial Depth of Cut (RDOC) and a higher Axial Depth of Cut (ADOC). This spreads wear evenly across the cutting edge, dissipates heat, and reduces the chance of tool failure. Besides dramatically increasing tool life, HEM can also produce a better finish and higher metal removal rate, making it an all-around efficiency boost for your shop.

Using Improper Tool Holding and its Effect on Tool Life

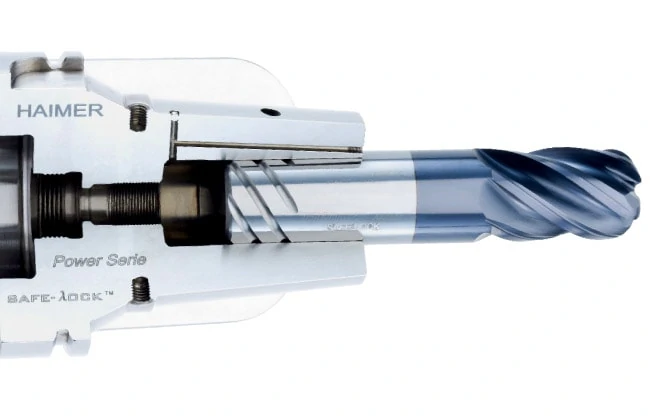
end mill held in haimer safe-lock tool holder

Proper running parameters have less of an impact in suboptimal tool holding situations. A poor machine-to-tool connection can cause tool runout, pullout, and scrapped parts. Generally speaking, the more points of contact a tool holder has with the tool’s shank, the more secure the connection. Hydraulic and shrink fit tool holders offer increased performance over mechanical tightening methods, as do certain shank modifications, like Helical’s ToughGRIP shanks and the Haimer Safe-Lock™.

Not Using Variable Helix/Pitch Geometry

infographic showcasing intricacies variable helix end mill

A feature on a variety of high performance end mills, variable helix, or variable pitch, geometry is a subtle alteration to standard end mill geometry. This geometrical feature ensures that the time intervals between cutting edge contact with the workpiece are varied, rather than simultaneous with each tool rotation. This variation minimizes chatter by reducing harmonics, which increases tool life and produces superior results.

Choosing the Wrong Coating Can Wear on Tool Life

four different corner rounding end mills with different tool coatings

Despite being marginally more expensive, a tool with a coating optimized for your workpiece material can make all the difference. Many coatings increase lubricity, slowing natural tool wear, while others increase hardness and abrasion resistance. However, not all coatings are suitable to all materials, and the difference is most apparent in ferrous and non-ferrous materials. For example, an Aluminum Titanium Nitride (AlTiN) coating increases hardness and temperature resistance in ferrous materials, but has a high affinity to aluminum, causing workpiece adhesion to the cutting tool. A Titanium Diboride (TiB2) coating, on the other hand, has an extremely low affinity to aluminum, and prevents cutting edge build-up and chip packing, and extends tool life.

Using a Long Length of Cut

optimal length of cut for proper tool life

While a long length of cut (LOC) is absolutely necessary for some jobs, especially in finishing operations, it reduces the rigidity and strength of the cutting tool. As a general rule, a tool’s LOC should be only as long as needed to ensure that the tool retains as much of its original substrate as possible. The longer a tool’s LOC the more susceptible to deflection it becomes, in turn decreasing its effective tool life and increasing the chance of fracture.

Free Resource: Download the 50+ Page High Efficiency Milling (HEM) Guidebook Today

Choosing the Wrong Flute Count

infographic of face of end mills with varying flute counts

As simple as it seems, a tool’s flute count has a direct and notable impact on its performance and running parameters. A tool with a low flute count (2 to 3) has larger flute valleys and a smaller core. As with LOC, the less substrate remaining on a cutting tool, the weaker and less rigid it is. A tool with a high flute count (5 or higher) naturally has a larger core. However, high flute counts are not always better. Lower flute counts are typically used in aluminum and non-ferrous materials, partly because the softness of these materials allows more flexibility for increased metal removal rates, but also because of the properties of their chips. Non-ferrous materials usually produce longer, stringier chips and a lower flute count helps reduce chip recutting. Higher flute count tools are usually necessary for harder ferrous materials, both for their increased strength and because chip recutting is less of a concern since these materials often produce much smaller chips.

https://www.harveyperformance.com/wp-content/uploads/2018/02/Featured-Image-Killing-End-Mill-IMG.jpg 393 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-02-07 09:08:092023-10-12 09:59:088 Ways You’re Killing Your End Mill

What You Need to Know About Coolant for CNC Machining

December 5, 2017/9 Comments/in CNC Machining, Quick Tips, Tech Tips, Titan USA, Troubleshooting Tips/by Harvey Performance Company

Coolant in purpose is widely understood – it’s used to temper high temperatures common during machining, and aid in chip evacuation. However, there are several types and styles, each with its own benefits and drawbacks. Knowing which cnc coolant – or if any – is appropriate for your job can help to boost your shop’s profitability, capability, and overall machining performance.

Coolant or Lubricant Purpose

Coolant and lubricant are terms used interchangeably, though not all coolants are lubricants. Compressed air, for example, has no lubricating purpose but works only as a cooling option. Direct coolants – those which make physical contact with a part – can be compressed air, water, oil, synthetics, or semi-synthetics. When directed to the cutting action of a tool, these can help to fend off high temperatures that could lead to melting, warping, discoloration, or tool failure. Additionally, coolant can help evacuate chips from a part, preventing chip recutting and aiding in part finish.

Coolant can be expensive, however, and wasteful if not necessary. Understanding the amount of coolant needed for your job can help your shop’s efficiency.

Click Here to Shop Harvey Tool’s Fully Stocked Offering of Deep Hole Coolant Through Drills

Types of Coolant Delivery

CNC coolant is delivered in several different forms – both in properties and pressure. The most common forms include air, mist, flood coolant, high pressure, and Minimum Quantity Lubricant (MQL). Choosing the wrong pressure can lead to part or tool damage, whereas choosing the wrong amount can lead to exhausted shop resources.

Air: Cools and clears chips, but has no lubricity purpose. Air coolant does not cool as efficiently as water or oil-based coolants. For more sensitive materials, air coolant is often preferred over types that come in direct contact with the part. This is true with many plastics, where thermal shock – or rapid expansion and contraction of a part – can occur if direct coolant is applied.

Mist: This type of low pressure coolant is sufficient for instances where chip evacuation and heat are not major concerns. Because the pressure applied is not great in a mist, the part and tool do not undergo additional stresses.

Flood: This low pressure method creates lubricity and flushes chips from a part to avoid chip recutting, a common and tool damaging occurrence.
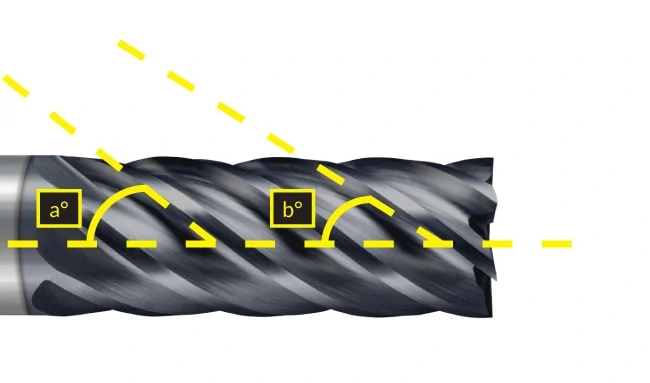
High Pressure: Similar to flood coolant, but delivered in greater than 1,000 psi. This is a great option for chip removal and evacuation, as it blasts the chips away from the part. While this method will effectively cool a part immediately, the pressure can be high enough to break miniature diameter tooling. This method is used often in deep pocket or drilling operations, and can be delivered via coolant through tooling, or coolant grooves built into the tool itself. Harvey Tool offers Coolant Through Drills, while Titan USA proudly offers Coolant-Fed ThreadMills

Minimum Quantity Lubricant (MQL): Every machine shop focuses on how to gain a competitive advantage – to spend less, make more, and boost shop efficiency. That’s why many shops are opting for MQL, along with its obvious environmental benefits. Using only the necessary amount of coolant will dramatically reduce costs and wasted material. This type of lubricant is applied as an aerosol, or an extremely fine mist, to provide just enough coolant to perform a given operation effectively.

To see all of these coolant styles in action, check out the video below from our partners at CimQuest.

In Conclusion

CNC coolant is all-too-often overlooked as a major component of a machining operation. The type of coolant or lubricant, and the pressure at which it’s applied, is vital to both machining success and optimum shop efficiency. Coolant can be applied as compressed air, mist, in a flooding property, or as high pressure. Certain machines also are MQL able, meaning they can effectively restrict the amount of coolant being applied to the very amount necessary to avoid being wasteful.

https://www.harveyperformance.com/wp-content/uploads/2017/12/Feature-Image-Coolant-for-CNC-Machining-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-12-05 15:09:342022-04-20 16:52:22What You Need to Know About Coolant for CNC Machining

3 Steps to Shutting up Tool Chatter

November 8, 2017/26 Comments/in CNC Machining, How-To's, Quick Tips, Troubleshooting Tips/by Harvey Performance Company

What is Chatter in Machining?

Cutting tools undergo a great deal of force during the machining process, which cause vibrations – also known as chatter or harmonics. Avoiding these vibrations entirely is not possible, though minimizing them is pivotal for machining success. Vibrations become damaging when proper machining steps are not followed. This leads to strong, part-ruining chatter. In these situations, parts have what is known as “chatter marks,” or clear vibration marks along the surface of a part. Tools can experience an increased rate of wear due to excess vibration.

zoomed in image of excessive tool wear from cnc machining
An example of a tool with excessive wear.

Shut Up Tool Chatter With Harvey Tool’s Material Specific Tooling

How to Reduce Chatter in Machining

Select the Right Tool for Your Job

It seems elementary, but selecting the best tool for your application can be confusing. With so many different geometric styles for tooling – overall length, length of cut, reach, number of flutes – it can sometimes be difficult to narrow down one specific tool for your job. Oftentimes, machinists opt for general purpose tooling that can perform a variety of operations, overlooking the option that’s optimized for one material and job.

Use Material Specific Tooling

Opting for Material Specific Tooling is helpful, as each material has different needs. For example, steels are machined differently than aluminum materials. Everything from the chip size, to chip evacuation, is different. Variable Helix or Variable Pitch designs help to minimize chatter by reducing harmonics, which are caused by the cutting edge having repeated contact with the workpiece. In order to reduce harmonics, the time intervals between flute contact with the workpiece are varied.
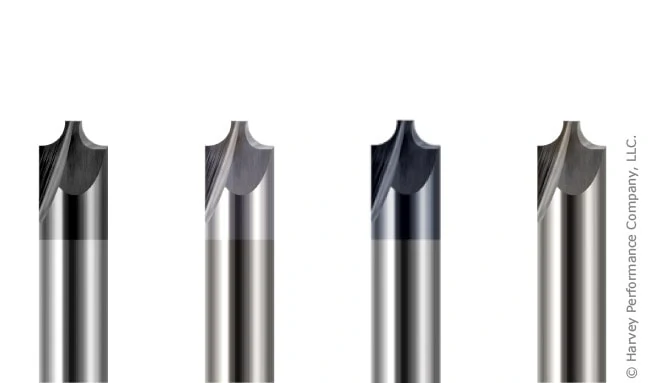
helical reduced neck tool in cnc machine next to part

Consider Tool Length

Overall length is another important factor to consider when deciding on a tool for your job. The more overhang, or length the tool hangs from the spindle, the less secure the spindle-to-tool connection is, and the more vibration. Ensuring that your tool is only as long as needed for your operation is important to minimizing chatter and harmonics. If machining deep within a part, opt for reached tooling or an extended reach tool holder to help solidify the connection.

Ensure a Secure Connection

Tool Holder & Shank Relationship

When it comes to secure tool holding approaches, both the tool shank and the collet are important. A loose tool, unsurprisingly, has more ability to move, or vibrate, during machining. With this in mind, Helical offers Shank Configurations to help the connection including the ToughGRIP Shank, which replaces a smooth, mirror-like surface with a rougher, coarser one for increased friction. Helical is also a licensee of the HAIMER Safe-Lock™, added grooves on the shank of a tool that work opposite of the spindle rotation, securely fastening the tool in place.
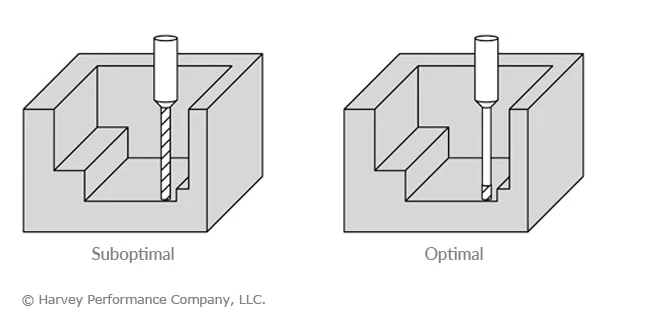
image of three end mills secured in their respective tool holders

Choosing Collet Types

Machinists must also know the different types of collets available to them to identify if a better solution might be necessary. For example, Hydraulic Tool Holders or Shrink Fit Tool Holders promote a stronger connection than a Mechanical Spindle Tightening method.
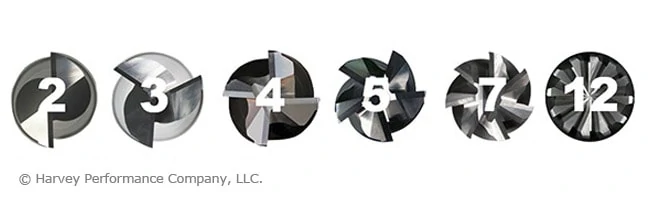
For more information, see Key Tool Holding Considerations

harvey tool material specific tooling ad with 4 end mills pictured side-by-side

Selecting a Chatter Minimizing Strategy

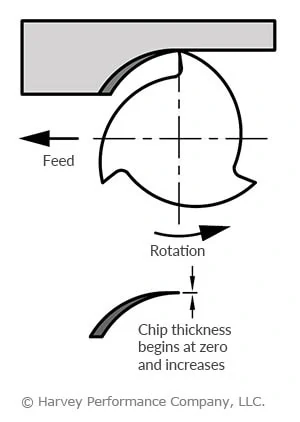
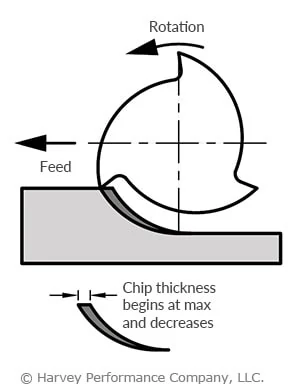
How a tool is run can mean the difference between stellar job results and a ruined part. This includes both the parameters a tool is run at, as well as the direction by which it rotates – either a Conventional Milling or a Climb Milling technique. The key distinction between these two methods lies in the relationship between the cutter’s rotation and the direction of the feed.

Conventional Milling

In conventional milling, the chip width starts from zero and increases gradually, causing the process of heat generation onto the workpiece rather than the chips. Heat generation causes deformities and tool failure such as work hardening, creating more headaches for a machinist. For this reason, conventional milling is generally only recommended for tools with high toughness or for breaking into case hardened materials.

conventional milling example with feed and rotation direction showcasing chip thickness

Climb Milling

Most modern machine shops will use a climb milling technique, or when the chip width starts at its maximum and decreases during the cut. Climb Milling will offer a more consistent cut than traditional methods, and puts less stress on the tool. Think of it like weight lifting – doing the heavy lifting will be easiest at the beginning of your workout. Similarly, a cut in which the thickest chip is removed first helps the tool maintain its strength. Because the chip cutting process is more swift, vibrations are minimized.

climb milling illustration with rotation and feed directions and chip thickness relation

For more information, see Climb Milling Vs. Conventional Milling

In Conclusion

Vibrations are unavoidable during the machining process, but minimizing them can mean the difference between successful machining and scrapped parts. Following three simple rules can help to keep your chatter and harmonics under control, including: Selecting the right tool, ensuring a secure machine-tool connection, and using it in a climb milling strategy. Both Harvey Tool and Helical Solutions have tools that can help, including shank modifications and Variable Helix or Variable Pitch end mills.

https://www.harveyperformance.com/wp-content/uploads/2017/11/Feature-Image-Tool-Chatter-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-11-08 09:30:472023-12-01 16:08:473 Steps to Shutting up Tool Chatter
Page 1 of 3123
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top