
Chipbreaker vs. Knuckle Rougher End Mills
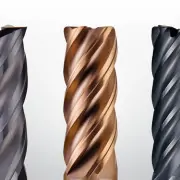
Knuckle Roughers and Chipbreakers are common profiles found on roughing end mills that, while fairly similar in appearance, actually serve different functions. Chipbreakers refer to the notches along the cutting edge of a tool that work to break up chips to prevent common evacuation mishaps. Knuckle Roughers refer to the serrated cutting edge of a tool, which works to enhance cutting action for an overall smoother operation.
Determining the appropriate style of tool is a very important first step to a successful roughing application.
Increase Your Roughing Efficiency With Helical Solutions’ Chipbreakers
Understanding the Two Styles
Chipbreaker End Mills
To aid chip evacuation, Chipbreaker End Mills feature a notched profile along the cutting edge that break down long chips into smaller, more manageable pieces. These tools are often utilized in aluminum jobs, as long, stringy chips are common with that material.
Each notch is offset flute-to-flute to enhance the surface finish on the part. This works by ensuring that as each flute rotates and impacts a part, following flutes work to clean up any marks or extra material that was left behind by the first pass. This leaves a semi-finished surface on your part.
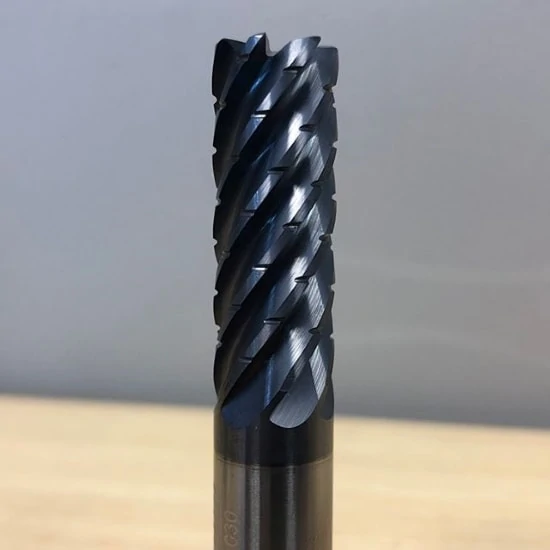
In addition to improving chip control and reducing cutting resistance, these tools also help in decreasing heat load within the chips. This delays tool wear along the cutting edge and improves cutting performance. Not only are these tools great for hogging out a great deal of material, but they can be utilized in a wide array of jobs – from aluminum to steels. Further, a machinist can take full advantage of the unique benefits this tool possesses by utilizing High Efficiency Milling toolpaths, meant to promote efficiency and boost tool life.
Knuckle Roughers
Knuckle Rougher End Mills have a serrated cutting edge that generates significantly smaller chips than a standard end mill cutting edge. This allows for smoother machining and a more efficient metal removal process, similar to Chipbreaker End Mills. However, the serrations chop the chips down to much finer sizes, which allows more chips into the flutes during the evacuation process without any packing occurring.
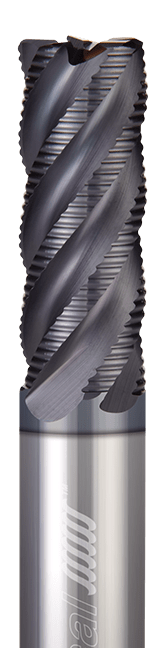
Designed for steels, Knuckle Rougher End Mills are built to withstand harder materials and feature a large core. Because of this, these tools are great for roughing out a lot of material. However, due to the profile on the cutting edge, tracks along the wall can sometimes be left on a part. If finish is a concern, be sure to come in with a finishing tool after the roughing operation. Knuckle Roughers have proven the ability to run at higher chip loads, compared to similar end mills, which makes this a highly desired style for roughing. Further, this style of rougher causes a lot of heat and friction within the chips, so it’s important to run flood coolant when running this tool.
Key Differences Between Knuckle Roughers & Chipbreakers
While the two geometries offer similar benefits, it’s important to understand the distinct differences between them. Chipbreakers feature offset notches, which help to leave an acceptable finish on the walls of a part. Simply, the material left on an initial flute pass is removed by subsequent passes. A Knuckle Rougher does not feature this offset geometry, which can leave track marks on your part. Where part finish is of upmost importance, utilize a Knuckle Rougher to first hog out a great deal of steel, and work a final pass with a Finishing End Mill.
A unique benefit of Knuckle Roughers is the grind they possess – a cylindrical grind, compared to a relieved grind of a Chipbreaker End Mill. Because of this, Knuckle Roughers are easier to resharpen. Therefore, instead of buying a new tool, resharpening this profile is often a cheaper alternative.


What toolpath styles are most effective with knuckle roughers? I have tried some HEM strategies with poor results. (Havent tried helical brand roughers yet) I was wondering if these roughing tools were best used with large stepovers and rigid setups to achieve a good MRR. Or am I missing something?
Hi Morgan,
This is a tough question, and is one that we will likely be able to answer better if we know more information about your specific application. However, the knuckle rougher is not generally a tool that we’d associate with HEM, as they’re a bit of an older geometry than chipbreakers. They’re better for more traditional paths, rather than HEM.
Please give our tech team a call at 800-645-5609 and we’d be happy to help you determine the best toolpath for your specific job.
I generally use 1/2 inch carbide AlTiN coated end mills for manual machining stainless steel whenever that size can get the job done. Most common is a stub length (5/8 LOC) double end plain-cut mill which is least expensive per end and does a great job for most parts. One double mill lasts a long time. With relatively small LOC the chips are small enough to get by. If that is too short, I use a chip breaker type, which maintains small chips and produces a smooth enough finish for my work without a separate finish mill.
I like the knuckle type for exposed surfaces on some parts. I leave the surface rough as it makes a nice decorative appearance.