
Contouring Considerations
What is Contouring?
Contouring a part means creating a fine finish on an irregular or uneven surface. Dissimilar to finishing a flat or even part, cnc contouring involves the finishing of a rounded, curved, or otherwise uniquely shaped part.
CNC Contouring & 5-Axis Machining
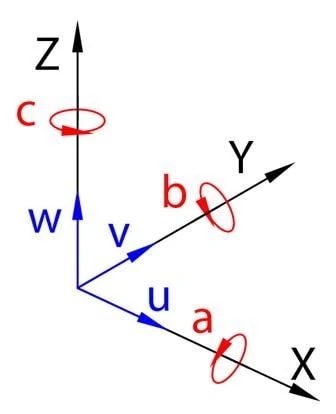
5-axis machines are particularly suitable for contouring applications. Because contouring involves the finishing of an intricate or unique part, the multiple axes of movement in play with 5-axis Machining allow for the tool to access tough-to-reach areas, as well as follow intricate tool paths.
Recent Advances
Advanced CAM software can now write the G-Code (the step-by-step program needed to create a finished part) for a machinists application, which has drastically simplified contouring applications. Simply, rather than spend several hours writing the code for an application, the software now handles this step. Despite these advances, most young machinists are still required to write their own G-Codes early on in their careers to gain valuable familiarity with the machines and their abilities. CAM software, for many, is a luxury earned with time.
Benefits of Advanced CAM Software
Increased Time Savings
Because contouring requires very specific tooling movements and rapidly changing cutting parameters, ridding machinists of the burden of writing their own complex code can save valuable prep time and reduce machining downtime.
Reduced Cycle Times
Generated G-Codes can cut several minutes off of a cycle time by removing redundancies within the application. Rather than contouring an area of the part that does not require it, or has been machined already, the CAM Software locates the very specific areas that require machining time and attention to maximize efficiency.
Improved Consistency
CAM Programs that are packaged with CAD Software such as SolidWorks are typically the best in terms of consistency and ability to handle complex designs. While the CAD Software helps a machinist generate the part, the CAM Program tells a machine how to make it.
Proper Tips
Utilize Proper Cut Depths
Prior to running a contouring operation, an initial roughing cut is taken to remove material in steps on the Z-axis so to leave a limited amount of material for the final contouring pass. In this step, it’s pivotal to leave the right amount of material for contouring — too much material for the contouring pass can result in poor surface finish or a damaged part or tool, while too little material can lead to prolonged cycle time, decreased productivity and a sub par end result.
The contouring application should remove from .010″ to 25% of the tool’s cutter diameter. During contouring, it’s possible for the feeds to decrease while speeds increases, leading to a much smoother finish. It is also important to keep in mind that throughout the finishing cut, the amount of engagement between the tool’s cutting edge and the part will vary regularly – even within a single pass.
Use Best Suited Tooling
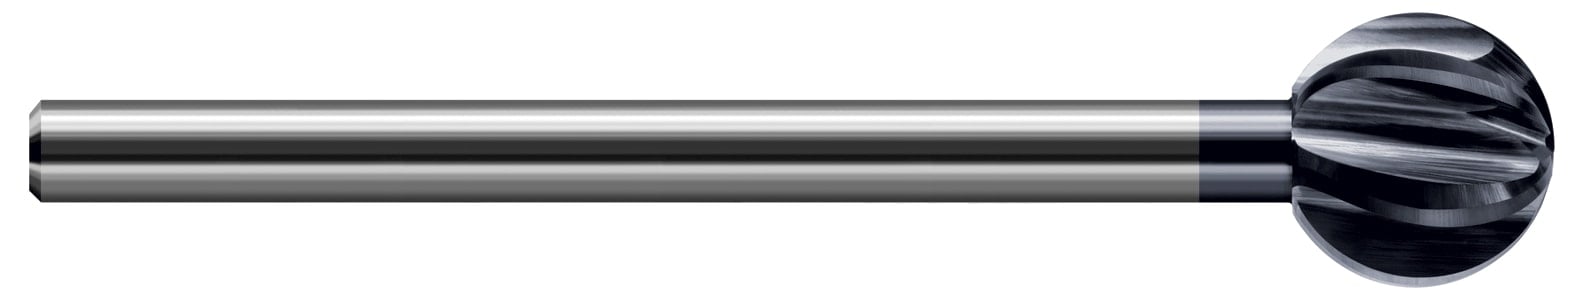
Ideal tool selection for contouring operations begins by choosing the proper profile of the tool. A large radius or ball profile is very often used for this operation because it does not leave as much evidence of a tool path. Rather, they effectively smooth the material along the face of the part. Undercutting End Mills, also known as lollipop cutters, have spherical ball profiles that make them excellent choices for contouring applications. Harvey Tool’s 300° Reduced Shank Undercutting End Mill, for example, features a high flute count to benefit part finish for light cut depths, while maintaining the ability to reach tough areas of the front or back side of a part.
Fact-Check G-Code
While advanced CAM Software will create the G-Code for an application, saving a machinist valuable time and money, accuracy of this code is still vitally important to the overall outcome of the final product. Machinists must look for issues such as wrong tool call out, rapids that come too close to the material, or even offsets that need correcting. Failure to look G-Code over prior to beginning machining can result in catastrophic machine failure and hundreds of thousands of dollars worth of damage.
Inserting an M01 – or a notation to the machine in the G-Code to stop and await machinist approval before moving on to the next step – can help a machinist to ensure that everything is approved with a next phase of an operation, or if any redundancy is set to occur, prior to continuation.
Contouring Summarized
CNC contouring is most often used in 5-axis machines as a finishing operation for uniquely shaped or intricate parts. After an initial roughing pass, the contouring operation – done most often with Undercutting End Mills or Ball End Mills, removes anywhere from .010″ to 25% of the cutter diameter in material from the part to ensure proper part specifications are met and a fine finish is achieved. During contouring, cut only at recommended depths, ensure that G-Code is correct, and use tooling best suited for this operation.



Leave a Reply
Want to join the discussion?Feel free to contribute!