
What You Need to Know About Coolant for CNC Machining
Coolant in purpose is widely understood – it’s used to temper high temperatures common during machining, and aid in chip evacuation. However, there are several types and styles, each with its own benefits and drawbacks. Knowing which cnc coolant – or if any – is appropriate for your job can help to boost your shop’s profitability, capability, and overall machining performance.
Coolant or Lubricant Purpose
Coolant and lubricant are terms used interchangeably, though not all coolants are lubricants. Compressed air, for example, has no lubricating purpose but works only as a cooling option. Direct coolants – those which make physical contact with a part – can be compressed air, water, oil, synthetics, or semi-synthetics. When directed to the cutting action of a tool, these can help to fend off high temperatures that could lead to melting, warping, discoloration, or tool failure. Additionally, coolant can help evacuate chips from a part, preventing chip recutting and aiding in part finish.
Coolant can be expensive, however, and wasteful if not necessary. Understanding the amount of coolant needed for your job can help your shop’s efficiency.
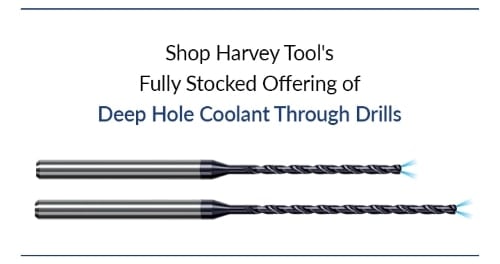
Click Here to Shop Harvey Tool’s Fully Stocked Offering of Deep Hole Coolant Through Drills
Types of Coolant Delivery
CNC coolant is delivered in several different forms – both in properties and pressure. The most common forms include air, mist, flood coolant, high pressure, and Minimum Quantity Lubricant (MQL). Choosing the wrong pressure can lead to part or tool damage, whereas choosing the wrong amount can lead to exhausted shop resources.
Air: Cools and clears chips, but has no lubricity purpose. Air coolant does not cool as efficiently as water or oil-based coolants. For more sensitive materials, air coolant is often preferred over types that come in direct contact with the part. This is true with many plastics, where thermal shock – or rapid expansion and contraction of a part – can occur if direct coolant is applied.
Mist: This type of low pressure coolant is sufficient for instances where chip evacuation and heat are not major concerns. Because the pressure applied is not great in a mist, the part and tool do not undergo additional stresses.
Flood: This low pressure method creates lubricity and flushes chips from a part to avoid chip recutting, a common and tool damaging occurrence.
High Pressure: Similar to flood coolant, but delivered in greater than 1,000 psi. This is a great option for chip removal and evacuation, as it blasts the chips away from the part. While this method will effectively cool a part immediately, the pressure can be high enough to break miniature diameter tooling. This method is used often in deep pocket or drilling operations, and can be delivered via coolant through tooling, or coolant grooves built into the tool itself. Harvey Tool offers Coolant Through Drills, while Titan USA proudly offers Coolant-Fed ThreadMills
Minimum Quantity Lubricant (MQL): Every machine shop focuses on how to gain a competitive advantage – to spend less, make more, and boost shop efficiency. That’s why many shops are opting for MQL, along with its obvious environmental benefits. Using only the necessary amount of coolant will dramatically reduce costs and wasted material. This type of lubricant is applied as an aerosol, or an extremely fine mist, to provide just enough coolant to perform a given operation effectively.
To see all of these coolant styles in action, check out the video below from our partners at CimQuest.
In Conclusion
CNC coolant is all-too-often overlooked as a major component of a machining operation. The type of coolant or lubricant, and the pressure at which it’s applied, is vital to both machining success and optimum shop efficiency. Coolant can be applied as compressed air, mist, in a flooding property, or as high pressure. Certain machines also are MQL able, meaning they can effectively restrict the amount of coolant being applied to the very amount necessary to avoid being wasteful.


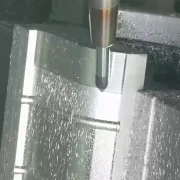


In the actual cutting process (especially in the processing of aluminum), often have similar problems (stick knife, broken cutter, broken tap, rotten teeth, etc.), excluding tools and machine tools, the type of coolant or lubricant, and the pressure at which it’s applied, is vital to both machining success and optimum shop efficiency.
Thanks for the informative read about the coolant for CNC machining. To be honest, I didn’t know that this could be delivered in different forms, like high pressure and how it’s ideal for chip removal or evacuation. It’s cool that there could be so many different applications that this could be used for. I’m kind of interested to learn of the more unique ones that are not as common.
Thanks for the informative blog on CNC coolant. I got to learn a lot especially types of ‘Types of Coolant Delivery.’ I didn’t know
Coolant is delivered in several different forms.
Looking for more such pieces from you. Great post!
Well written and descriptive topic on coolant
This is a great article. Very informative. I think it would be important to provide information on the benefits of changing coolant and what happens as it starts to break down on a molecular level as well. We are experiencing some of these issues at my company. Maintenance seems to not understand the importance of clean coolant. Not only does it effect cutting, it ends up being a health hazard as mold begins to appear.
Great Post!Thank you so much for sharing this kind of wonderful things.
Yes, coolant quality and flow are critical in tool life and surface finish when CNC Machining.
Well written.
As you mentioned, coolant helps prevent overheating and melting. Is there a way to figure out which intake your machine is equip with, and which coolant it takes? My brother recently started working in a cnc machining plant. I wonder if I could see how they work and cool.
Try Googling the make and model to find out the information you are looking for. That would be the easiest way.