
Depth of Cut: Peripheral, Slotting, and HEM Approaches
The following is just one of several blog posts relevant to High Efficiency Milling. To achieve a full understanding of this popular machining method, view any of the additional HEM posts below!
Introduction to High Efficiency Milling I High Speed Machining vs. HEM I How to Combat Chip Thinning I How to Avoid 4 Major Types of Tool Wear I Intro to Trochoidal Milling
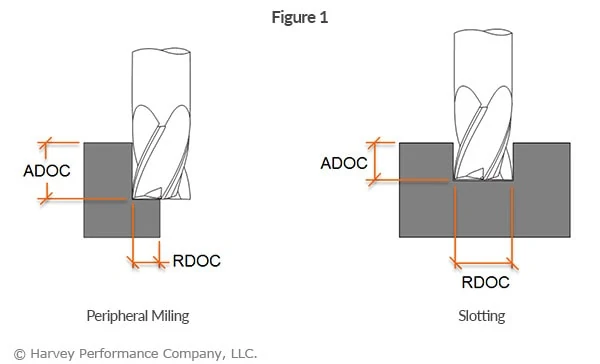
Every machining operation entails a radial and axial depth of cut strategy. Radial depth of cut (RDOC), the distance a tool is stepping over into a workpiece; and Axial depth of cut (ADOC), the distance a tool engages a workpiece along its centerline, are the backbones of machining. Machining to appropriate depths – whether slotting or peripheral milling (profiling, roughing, and finishing), is vital to your machining success (Figure 1).
Below, you will be introduced to the traditional methods for both peripheral milling and slotting. Additionally, High Efficiency Milling (HEM) strategies – and appropriate cutting depths for this method – will be explained.
Quick Definitions:
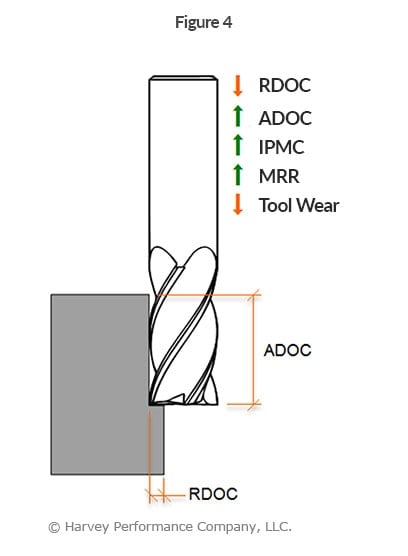
Radial Depth of Cut (RDOC): The distance a tool is stepping over into a workpiece. Also referred to as Stepover, Cut Width, or XY.
Axial Depth of Cut (ADOC): The distance a tool engages a workpiece along its centerline. Also referred to as Stepdown, or Cut Depth.
Peripheral Milling: An application in which only a percentage of the tool’s cutter diameter is engaging a part.
Slotting: An application in which the tool’s entire cutter diameter is engaging a part.
High Efficiency Milling (HEM): A newer machining strategy in which a light RDOC and heavy ADOC is paired with increased feed rates to achieve higher material removal rates and decreased tool wear.
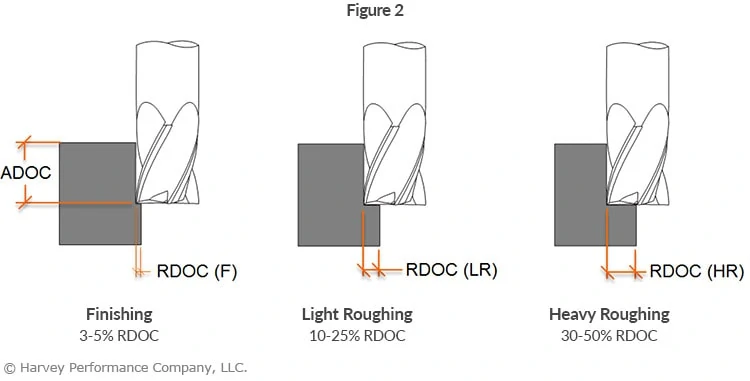
Peripheral Milling Styles and Appropriate RDOC
The amount a tool engages a workpiece radially during peripheral milling is dependent upon the operation being performed (Figure 2). In finishing applications, smaller amounts of material are removed from a wall, equating to about 3-5% of the cutter diameter per radial pass. In heavy roughing applications, 30-50% of the tool’s cutter diameter is engaged with the part. Although heavy roughing involves a higher RDOC than finishing, the ADOC is most often smaller than for finishing due to load on the tool.
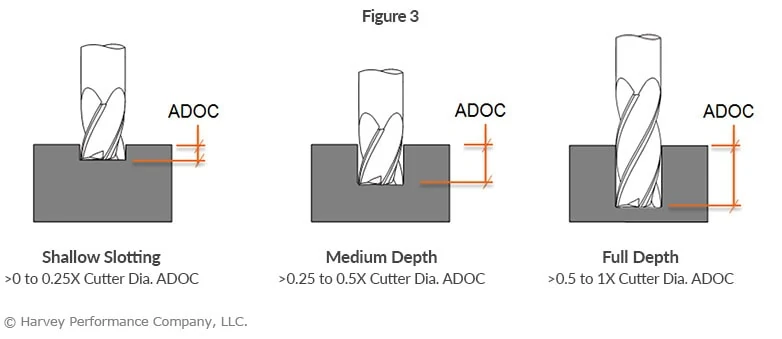
Slotting Styles and Appropriate ADOC Engagement
The amount a tool engages a part axially during a slotting operation must be appropriate for the tool being used (Figure 3). Using an inappropriate approach could lead to tool deflection and damage, and poor part quality.
End mills come in various length of cut options, as well as numerous reached options. Choosing the tool that allows the completion of a project with the least deflection, and highest productivity, is critical. As the ADOC needed to slot can be lower, a stub length of cut is often the strongest and most appropriate tool choice. As slot depths increase, longer lengths of cut become necessary, but reached tooling should be used where allowable.
Depth of Cut Strategy for High Efficiency Milling (HEM)
Pairing a light RDOC and heavy ADOC with high performance toolpaths is a machining strategy known as High Efficiency Milling or HEM. With this machining style, feed rates can be increased and cuts are kept uniform to evenly distribute stresses across the cutting portion of the tool, prolonging tool life.
Traditional Strategy
- Heavy RDOC
- Light ADOC
- Conservative Feed Rate
Newer Strategy – High Efficiency Milling (HEM)
- Light RDOC
- Heavy ADOC
- Increased Feed Rate
Click Here to Access Our Free Educational Webinar on High Efficiency Milling
HEM involves using 7-30% of the tool diameter radially and up to twice the cutter diameter axially, paired with increased feed rates (Figure 4). Accounting for chip thinning, this combination of running parameters can result in noticeably higher metal removal rates (MRR). Modern CAM software often offers a complete high performance solution with built-in features for HEM toolpaths. These principals can also be applied to trochoidal toolpaths for slotting applications.



I need all of these tips and tricks in a book form. Any suggestions?
Hi Rich – thanks for your comment. We think that is a great idea! We will let you know as soon as something like that becomes available.
A searchable app would be an option. These are concise tips worth the handy access at the machine.
Hi John,
We actually have an HEM Guidebook which you can download that has a lot of helpful tips on things like Depth of Cut and High Efficiency Milling techniques. You can download that by going to http://www.harveyperformance.com/HEM-Guidebook
If you are on the go and at a machine, the blog optimized for viewing on a mobile device as well, and a search option is available! Hopefully that will help you access this information more easily when you are away from your desk.
Rich,
It took some searching but I found a good solution to getting this into book form. Follow the steps below.
1. If you are in an office setting use the key combination: ctrl + p. Follow the steps provided on the screen.
2. Once this step has been completed find a local binding apparatus; this is a helpful tool for obtaining book form. Use it wisely.
Hope this helps
Good luck!
Great insights on optimizing cutting depths! I really appreciate the practical tips and examples you included. It’s amazing how such a small adjustment can lead to significant improvements in efficiency and tool life. Looking forward to trying these techniques in my own work!