
How to Maximize High Balance End Mills
High speed machining is becoming increasingly widespread in machine shops all over the world due to the proven benefits of greater efficiency and productivity through increased spindle speeds and metal removal rates. However, at such high spindle speeds, otherwise negligible errors and imperfections can cause negative effects such as reduced tool life, poor surface finish, and wear on the machine itself. Many of these negative effects stem from an increase in total centrifugal forces leading to vibration, commonly referred to in the industry as chatter. A key contributor to vibrations and one of the more controllable factors, is tool unbalance.
Why Balance is Critical to Machining
Unbalance is the extent to which the tool’s center of mass diverges from its axis of rotation. Small levels of unbalance may be indistinguishable at lower RPMs, but as centrifugal force increases, small variations in the tool’s center of mass can cause substantial detrimental effects on its performance. High Balance End Mills are often used to help solve the problem of vibrations at the increased spindle speeds. Balancing is used to make compensation for the intrinsic unsymmetrical distribution of mass, which is typically completed by removing mass of a calculated amount and orientation.
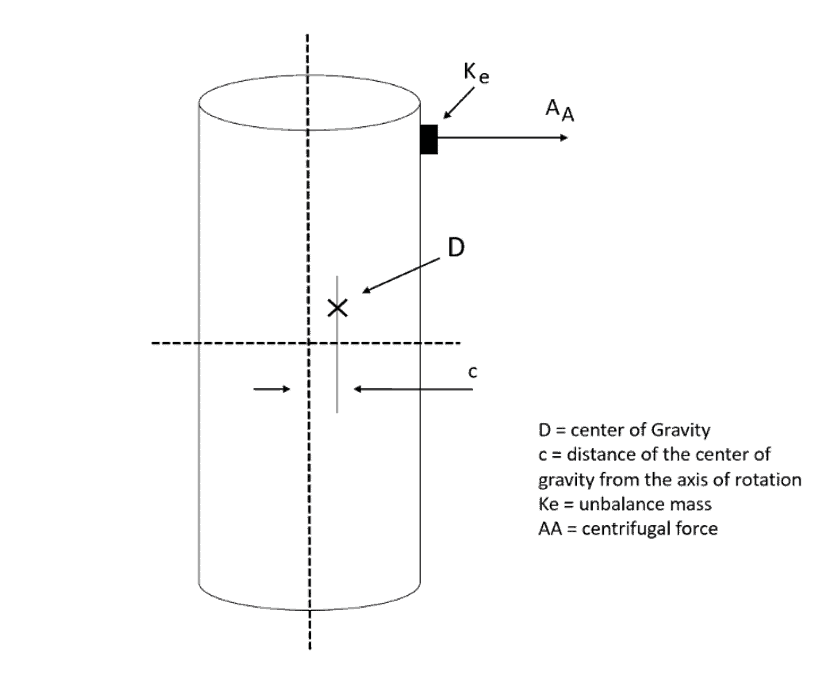
Image Source: Haimer; Fundamentals of Balancing
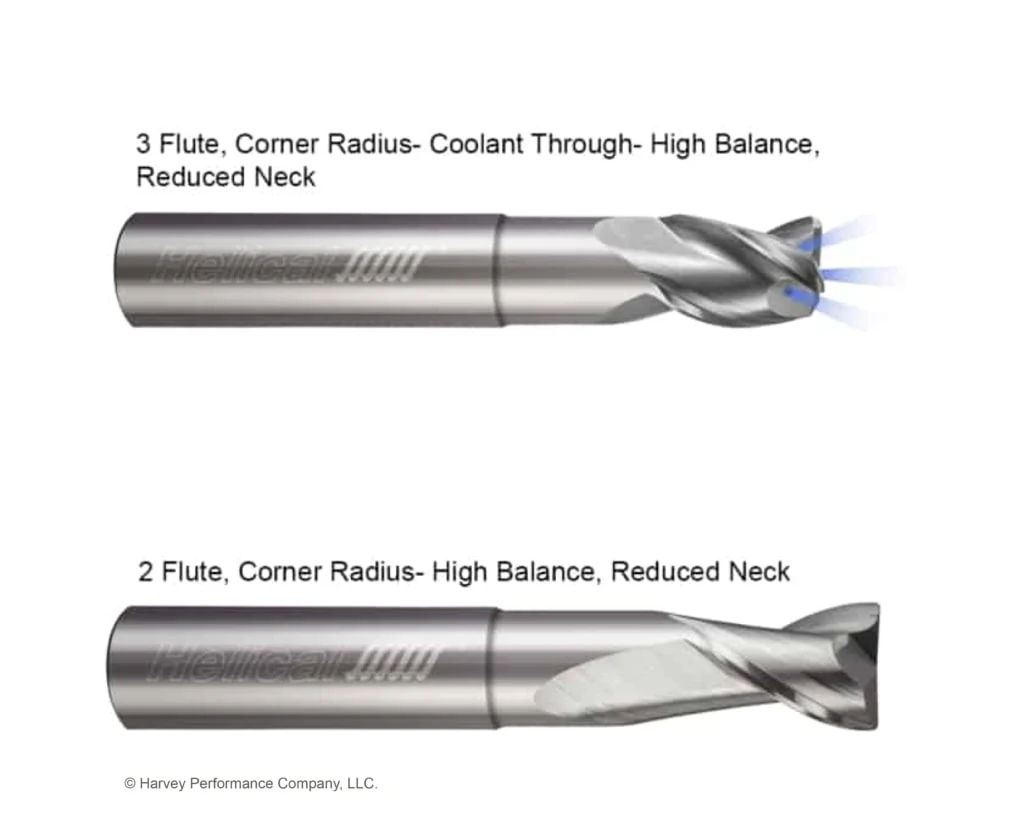
Helical Solutions offers High Balance End Mills in both 2 and 3 flute options (see Figure 2), square and corner radius, along with coolant-through on the 3 fluted tools. These end mills are balanced at the industry standard of G2.5 at 33,000 RPM: G stands for the potential damage due to unbalance, which can be expressed as “Balancing Quality Grade” or G and 2.5 is the vibration velocity in MM per second. These tools are designed specifically to increase performance in highly balanced machining centers that are capable of elevated RPMs and feed rates. With high balance tooling, improved surface finishes are also achieved due to reduced vibrations during the machining process. Additionally, these end mills have been designed around current high-end tool holding, and come in a variety of neck lengths at specific overall lengths. These dimensional combinations result in maximum rigidity and reduced excess stick out, allowing for optimal performance and the ability to push the tools to the limit.
High Balanced Tooling Cost Benefits
Machinists who choose to use High Balance End Mills will see certain benefits at the spindle, but also in their wallets. Cost benefits of opting to run this type of tool include:
- Longer tool life
- Longer spindle lifetime
- Reduced machine down time
Utilizing Tap Testers
What Tap Testers Do
Vibrations are your applications worst enemy, especially at elevated RPMs and feed rates. Using resources such as a Tap Tester can help decrease vibrations and allow you to get the most out of your High Balance End Mills by generating cutting performance predictions and chatter limits.
How Tap Testing Works
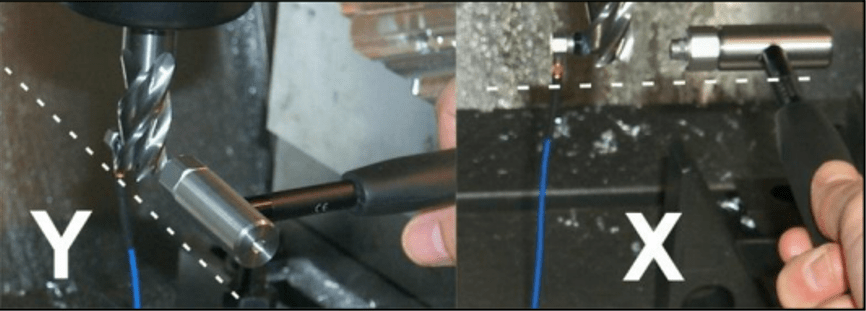
Image Source: Manufacturing Automation Laboratories Inc.
Tap Testing generates cutting performance predictions and chatter limits. In a tap test, the machine-tool structure is “excited,” or tested, by being hit with an impulse hammer. In milling, the machine-tool structure is usually flexible in all three directions: X, Y, and Z, but in milling applications where High Balance Tooling is used, the flexibility is commonly only considered in two planes – the X and Y directions. By hitting the X and Y directions with the impulse hammer, the impact will excite the structure over a certain frequency range that is dependent on the hammer’s size, the type of tool being used, and the structure itself. The frequencies generated from the initial hit will produce enough information that both the impact force measurement and the displacement/accelerometer measurement are available. Combining these two measurements will result in the Frequency Response Function, which is a plot of the dynamic stiffness of the structure in frequencies.
After the information from the Tap Test is gathered, it will then process the information into useful cutting parameters for all spindles speeds such as cut depths, speed rates, and feed rates. In knowing the optimum running parameters, vibrations can be minimized and the tool can be utilized to its full potential.
High Balanced Tooling Summarized
Keeping vibrations at bay during the machining process is extremely important to machining success. Because one cause of vibration is tool unbalance, utilizing a balanced tool will result in a smoother job, a cleaner final product, and a longer life of both the tool and spindle. Machinists who choose to use High Balance Tooling can utilize a Tap Tester, or a method for generating the perfect running parameters for your tool and machine setup to ensure that machining vibration is as minimal as possible.



Trackbacks & Pingbacks
[…] Harvey Tools: How To Maximize High Balance End Mills […]
Leave a Reply
Want to join the discussion?Feel free to contribute!