Circular Interpolation: Machining Circular Tool Paths
When machining, proper speeds and feeds are very important to avoid breakage and maximize performance. Traditional end milling formulas use Surface Footage (SFM) and Chip Load (IPT) to calculate Speed (RPM) and Feed (IPM) rates. These formulas dictate the correct machining parameters for use in a linear path in which the end mill’s centerline is travelling in a straight line. Since not all parts are made of flat surfaces, end mills will invariably need to move in a non-linear path. In the case of machining circular tool paths, the path of the end mill’s centerline is circular. Not surprisingly, this is referred to as Circular Interpolation.
Decrease Cycle Times and Increase Shop Efficiency. Download Our HEM Guidebook.
Cutting Circular Tool Paths
All rotating end mills have their own angular velocity at the outside diameter. But when the tool path is circular, there is an additional component that is introduced, resulting in a compound angular velocity. Basically, this means the velocity of the outside diameter is travelling at a substantially different velocity than originally expected. The cause of the compound angular velocity is seen in the disparity between the tool path lengths.
Internal Circular Tool Paths
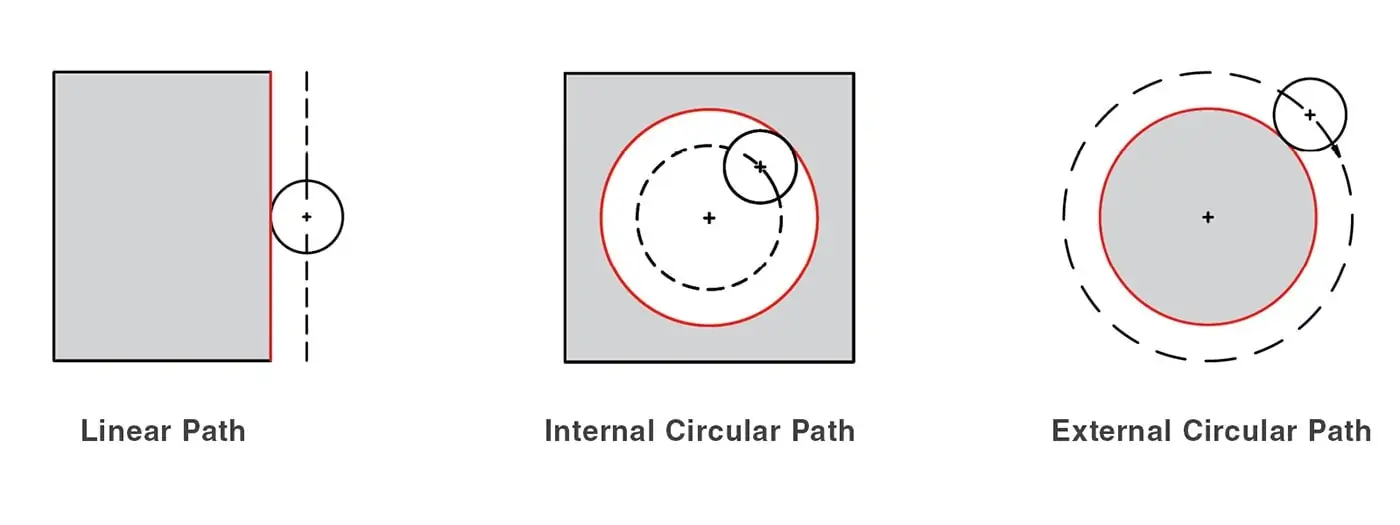
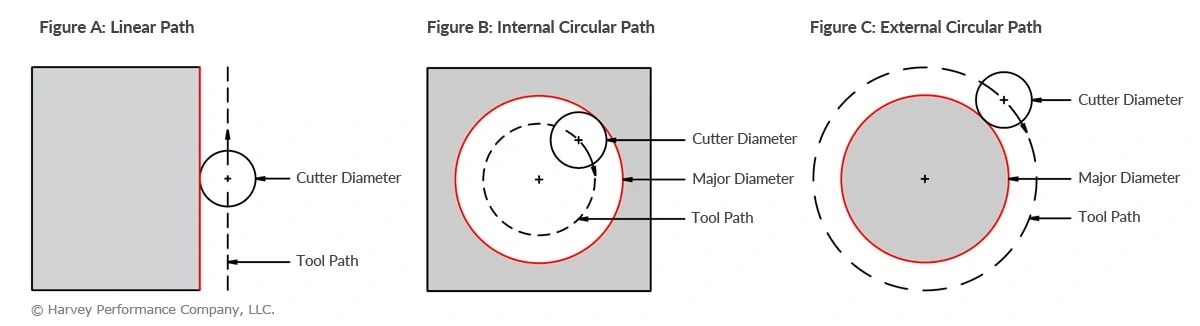
Figure A shows the cross section of a cutting tool on a linear path, with the teeth having angular velocity due to tool rotation, and the center of the tool having a linear feed. Note that the tool path length will always be equal to the length of the machined edge. Figure B shows the same cutting tool on an internal circular path, as done when machining a hole. In this case, the angular velocity of the teeth is changed as a result of an additional component from the circular path of the tool’s center. The diameter of the tool path is smaller than that of the major diameter being cut. Or, in other words, the tool path length is shorter than the machined edge length, increasing the angular velocity of the teeth. To prevent overfeeding and the possibility of tool breakage, the increased angular velocity of the teeth must be made the same as in the linear case in Figure A. The formula below can be used to properly lower the feed rate for internal machining:
Internal Adjusted Feed = (Major Diameter-Cutter Diameter) / (Major Diameter) × Linear Feed
External Circular Tool Paths
Figure C shows the same cutting tool on an external circular path, as done when machining a post. In this case, the diameter of the tool path is larger than the major diameter being cut. This means that the tool path length is longer than the machined edge length, resulting in a decreased angular velocity. To prevent premature dulling and poor tool life due to over-speeding, use the formula below to properly raise the feed rate for external machining. In this way, the decreased angular velocity of the teeth is made the same as in the linear case in Figure A.
External Adjusted Feed = (Major Diameter+Cutter Diameter) / (Major Diameter) × Linear Feed
Optimize Your Performance
By adjusting the feed in the manner provided, internal applications can avoid tool breakage and costly down time. Further, external applications can enjoy optimized performance and shorter cycle times. It should also be noted that this approach can be applied to parts with radiused corners, elliptical features and when helical interpolation is required.



That is great information thank you!
This information will help me with internal vs external threadmilling.
Great information and something I was never taught by my previous boss/teacher
Very important information that very few fellows take in consideration when programming. I keep telling my coworkers how important it is, the difference looks minimal but is actually exponential. I also use it when threadmilling to have the right feed!
Thanks!
JS
Thank you for the explanation, this explains why my half inch end Mill run so much better than my 3/4 inch.
Does this change if you’re doing climb milling rather than conventional milling?
Hi Will,
These adjustments are independent whether you are climb milling or conventional milling. The only thing you need to know is the Major Diameter and the Cutter Diameter and if you are programing an Internal Circular Path or External Circular Path.
Climb milling and conventional milling would play a bigger part on your finish but that is also impacted by many other variables.
I think I must be missing something. For External Circular Tool Paths the equation is :
External Adjusted Feed = (Major Ø + Cutter Ø) / Major Ø * Linear Feed
So if I was to use a ½” Ø end mill to cut a 1.0” Ø post with a linear feed of 5.0 IPM my equation is:
External Adjusted Feed = (1.0 + .5) / 1.0 * 5.0
Answer: External Adjusted Feed = .3 IPM
Am I to add the .3 IPM to the 5.0 IPM Linear Feed? If that is the case why not add that calculation to the equation? Or am I misinterpreting the equation altogether?
Great question Jason. you would want to add the .3 IPM to your 5.0 IPM. You must keep the equation separate from your normal IPM calculation because you need to determine the original IPM before you can calculate the adjusted IPM.
Guy Petrillo is mistaken. Jason H. you are not fallowing order of operations, PEMDAS, Parenthesis, Exponents, Multiplication, Division, Addition, Subtraction. The sequence of operations for (1.0+.5)/1.0*5.0 should result in 7.5, because 1.0+.5=1.5 next should be 1.5/1=1.5 then finally 1.5*5=7.5. If you plug the whole equation into a calculator (1+.5)/1*5= it should come out with 7.5
My apologies Tom is correct. The equation is ((Major Diameter – Cutter Diameter)/Major Diameter) = Adjustment percentage. You then take that adjustment percentage and multiply that by your feedrate to get your adjusted feedrate.
Listen to Tom R, he has it correct. You are calculating an adjusted feed rate in IPM, not a adjustment percentage.
Follow PEMDAS or BEDMAS. Here in Canada, it is BEDMAS.
Either way you will get the correct answer when following the equation in this case.
You must fallow order of operations PEMDAS, Parenthesis, Exponents, Multiplication, Division, Addition, Subtraction.
You must take (Major Diameter – Cutter Diameter) / Major Diameter and then multiply the results by the Intended Feed Rate, to get your adjusted feed rate. Most people seem to be taking (MD-CD) and dividing by (MD*Intended Feed Rate). If you plug the whole equation into a calculator (MD-CD)/MD*IFR It will give you the adjusted feed rate not the amount to adjust.
Example for ID:
3.125_ ID
.625_ Cutter
Intended feed rate_ 10.0 IPM
(3.125 – .625) / 3.125 * 10.0 = 8.0
Start with, 3.125 – .625 = 2.5
Then, 2.5 / 3.125 = .8
Finally, .8*10. + 8.0
Your adjusted feed rate is 8.0IPM
Funny that everyone was quick to jump on “order of operations” without actually looking at where the error came from which is that he divided by the linear feed rather than multiplied as it’s supposed to be. Basically, formula was written correctly in the comment but if you do the formula but rather then multiply by 5, you divide by 5, you get .3 as the original commentor got and thus was following correct order of operations but must have accidently used the wrong operator in the formula.
Could someone give an example of the actual math with figures used, I’m making some kind of a mistake on an internal pocket correction. This is what I did, 1.5″ ID, .5″ cutter. 1.5″-.5″ divided by 1.5″ X 5.0 IPM.
1.5-.5 = 1.0
1.5 X 5.0 = 75
1 / 75 = .0133
This answer (.0133) obviously is wrong, I just don’t know what mistake I’m making.
Thanks for helping me get right!
Hello Jake, great question! It looks as though you made a simple error here. When multiplying the ID and IPM you get 75, you have misplaced the decimal. The correct answer should be 7.5, giving you a final answer of 0.133.
Jake you need to fallow order of operations, PEMDAS, Parenthesis, Exponents, Multiplication, Division, Additions, Subtraction. The equation (1.5-.5)/1.5*5 should result in 3 1/3. The correct order of operations would be (1.5-.5)=1, then, 1 / 1.5 = 2/3, finally, 2/3 * 5 =3 1/3. If you plug the whole equation into a calculator you will see the same answer (1.5 – .5) / 1.5 * 5 = 3.3333
My apologies Tom is correct. The equation is ((Major Diameter – Cutter Diameter)/Major Diameter) = Adjustment percentage. You then take that adjustment percentage and multiply that by your feedrate to get your adjusted feedrate.
So if you add the IAF to original IPM for external, do you subtract it for an internal being the length is shorter?
Yes, you would want to slow down the IPM in an internal tool path as to not overfeed your tool.
If done correctly the equation will result in an adjusted feed rate, not an amount to adjust. You must fallow order of operations PEMDAS, Parenthesis, Exponents, Multiplication, Division, Addition, Subtraction.
You must take (Major Diameter – Cutter Diameter) / Major Diameter and then multiply the results by the Intended Feed Rate, to get your adjusted feed rate. Most people seem to be taking (MD-CD) and dividing by (MD*Intended Feed Rate). If you plug the whole equation into a calculator (MD-CD)/MD*IFR It will give you the adjusted feed rate not the amount to adjust.
Example for ID:
3.125_ ID
.625_ Cutter
Intended feed rate_ 10.0 IPM
(3.125 – .625) / 3.125 * 10.0 = 8.0
Start with, 3.125 – .625 = 2.5
Then, 2.5 / 3.125 = .8
Finally, .8*10. + 8.0
Your adjusted feed rate is 8.0IPM
I agree the equation is confusing. no where in the article does it say to add or subtract your results from your existing feed rate. if I hadn’t read the comments I would’ve never known this is what was intended. with that said, i’m not sure adding or subtracting is correct. If i’m understanding the article correctly, you’re trying to ratio the difference between the tool path & major dias..
You must fallow order of operations PEMDAS, Parenthesis, Exponents, Multiplication, Division, Addition, Subtraction.
You must take (Major Diameter – Cutter Diameter) / Major Diameter and then multiply the results by the Intended Feed Rate, to get your adjusted feed rate. Most people seem to be taking (MD-CD) and dividing by (MD*Intended Feed Rate). If you plug the whole equation into a calculator (MD-CD)/MD*IFR It will give you the adjusted feed rate not the amount to adjust.
Example for ID:
3.125_ ID
.625_ Cutter
Intended feed rate_ 10.0 IPM
(3.125 – .625) / 3.125 * 10.0 = 8.0
Start with, 3.125 – .625 = 2.5
Then, 2.5 / 3.125 = .8
Finally, .8*10. + 8.0
Your adjusted feed rate is 8.0IPM
Tom your formula has one mistake that can confuse some people.
in your example you have “Finally..8 * 10. + 8.0”
What you should have is “Finally. .8 * 10. = 8.0”
just a typo but if someone is already struggling with this math it might confuse them.
spot on explanation otherwise.
Nothing should be confusing about it. You have to read and consider particular word usage and the meaning of the words chosen for the result of the formula (i.e., “Internal Adjusted Feed” and “External Adjusted Feed”). The key word is “Adjusted” and the fact that it is past tense (i.e., meaning adjustment already accounted for.
Now if the result was written as something like “Internal (or External) Adjustment Percentage (or Factor), then it would indicate that there is still another step that needed to be done because of the “Adjustment” rather than “Adjusted”.
Can anyone help me to how to write MATLAB code for the extract distance for G and M code G02 and G03 For example N195 G02 X25.456 Y.052 I4.211 J13.875
N196 X-1.875 Y44.246 I36.544 J53.149