
Optimizing Material Removal Rates
What is the Material Removal Rate?
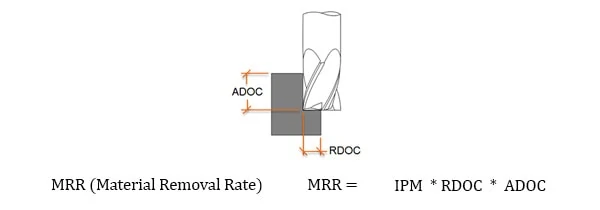
Material Removal Rate (MRR), otherwise known as Metal Removal Rate, is the measurement for how much material is removed from a part in a given period of time. Every shop aims to create more parts in a shorter period of time, or to maximize money made while also minimizing money spent. One of the first places these machinists turn is to MRR, which encompasses Radial Depth of Cut (RDOC), Axial Depth of Cut (ADOC), and Inches Per Minute (IPM) to create the MRR triangle where all three figures impact each other. If you’re aiming to boost your shop’s efficiency, increasing your MRR even minimally can result in big gains by decreasing cycle times and ultimately freeing up machines for increased productivity.
Click Here to Download the High Efficiency Milling (HEM) Guidebook
How to Calculate MRR In Machining
Material Removal Rate Formula
The Material Removal Rate equation is RDOC x ADOC x Feed Rate (IPM). As an example, if your RDOC is .500″, your ADOC is .100″ and your Feed Rate is 41.5 inches per minute, you’d calculate MRR the following way:
MRR = .500″ x .100″ x 41.5 in/min = 2.08 cubic inches per minute.
Optimizing Efficiency
A machinists’ depth of cut strategy is directly related to the Material Removal Rate. Using the proper RDOC and ADOC combination can boost MRR rates, shaving minutes off of cycle times and opening the door for greater production. Utilizing the right approach for your tool can also result in prolonged tool life, minimizing the rate of normal tool wear. Combining the ideal feed rate with your ADOC and RDOC to run at your tool’s “sweet spot” can pay immediate and long term dividends for machine shops.
The following MRR machining chart illustrates how a 1/2″, 5-flute tool will perform in Steel when varying ADOC and RDOC parameters are used. You can see that by varying the ADOC and RDOC, a higher feed rate is achievable, and thus, a higher MRR. In this case, pairing a high ADOC, low RDOC approach with an increased feed rate was most beneficial. This method has become known as High Efficiency Milling.
| Axial Depth of Cut | Radial Depth of Cut | Feed Rate | Material Removal Rate |
| .125″ | .200″ | 19.5 IPM | .488 in.³/min. |
| .250″ | .150″ | 26.2 IPM | .983 in.³/min. |
| .500″ | .100″ | 41.5 IPM | 2.08 in.³/min. |
| .750″ | .050″ | 89.2 IPM | 3.35 in.³/min. |
| 1.00″ | .025″ | 193 IPM | 4.83 in.³/min. |
High Efficiency Milling
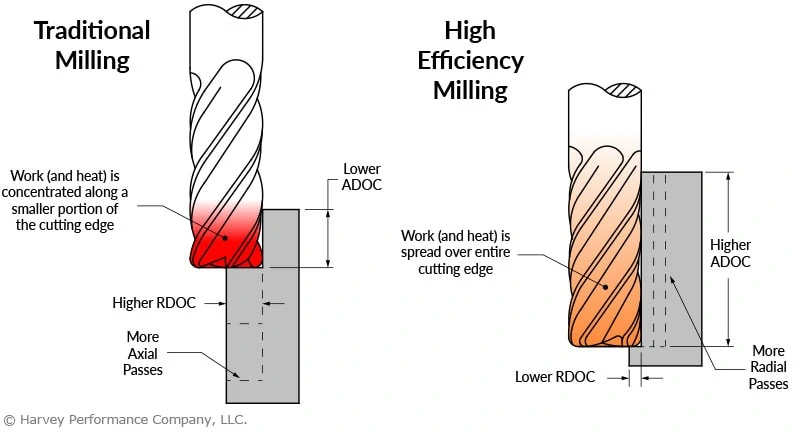
High Efficiency Milling (HEM) is a milling technique for roughing that utilizes a lower RDOC and a higher ADOC strategy. This spreads wear evenly across the cutting edge, dissipates heat, and reduces the chance of tool failure. This results in a greater ability to increase your MRR in machining, while maintaining and even prolonging tool life versus traditional machining methods.
HEM VS Traditional Milling
The image referenced below compares the differences between traditional milling and the newer High Efficiency Milling technique in achieving adequate material removal. A traditional milling strategy requires the application of work and heat along a smaller portion of the cutting edge, while the HEM technique disperses heat more evenly across the entire cutting edge. This method calls for more radial passes which utilize a larger portion of the cutting edge, as opposed to axial passes that lead to a higher likelihood of tool failure over time.
Obviously, with higher MRR’s, chip evacuation becomes vitally important as more chips are evacuated in a shorter period of time. Utilizing a tool best suited for the operation – in terms of quality and flute count – will help to alleviate the additional workload. For softer materials lower flute count tools will traditionally be the best choice. The thinner core allows for deeper flute valleys which aid in enhanced chip evacuation and ultimately increased MRR. On the other hand, harder materials require higher flute count tools with shallower flute valleys. This leads to less material removed per tooth, however tool life is substantially increased over the historic usage of lower flute count tools in these materials.
Additionally, a tool coating optimized for your workpiece material can significantly help with chip packing. First, tool coatings increase heat resistance of the tool allowing for faster cutting speeds leading to increased MRR. Secondly, coatings increase the lubricity of the cutting tool allowing for enhanced chip evacuation and lessened friction. This enhanced chip evacuation allows for the most efficient metal removal rate possible.
Further, compressed air or coolant can help to properly remove chips from the tool and workpiece. There are different three types of coolant delivery methods one could utilize in increasing metal removal rate.
Compressed Air
While having no lubricity purpose, the air coolant delivery method is made to cool and clear chips. This method does not cool as effectively as other coolant-based solutions, however it is preferred for more sensitive materials where thermal shock is a concern.
Flood
Flooding is a low pressure coolant delivery method which creates lubricity in order to evacuate chips from a part. This is necessary to prevent chip recutting which is likely to damage a cutting tool. This method of delivery is the most common choice for the widest range of machining operations.
High Pressure
This method is similar to flood coolant, however it is used to instantly cool a part and blast chips away with a high pressure of delivery. While highly effective at chip evacuation, this option is most likely to damage or break more fragile cutting tools. High pressure coolant delivery is most often utilized in deep pocket machining and drilling operations due to its increased ability to flush chips.
In conclusion, optimizing workplace efficiency is vital to sustained success and continued growth in every business. This is especially true in machine shops, as even a very minor adjustment in operating processes can result in a massive boost in company revenue. Proper machining methods will boost MRR, minimize cycle times, prolong tool life, and maximize shop efficiency.


Great insights on optimizing material removal rates! I especially appreciated the detailed breakdown of the factors influencing MRR and the practical tips you provided. Implementing these strategies could really enhance machining efficiency in our operations. Looking forward to trying out some of your recommendations!