Multi-Start Thread Reference Guide
A multi-start thread consists of two or more intertwined threads running parallel to one another. Intertwining threads allow the lead distance of a thread to be increased without changing its pitch. A double start thread will have a lead distance double that of a single start thread of the same pitch, a triple start thread will have a lead distance three times longer than a single start thread of the same pitch, and so on.
Shop Harvey Tool’s Comprehensive Offering of Fully Stocked Threadmills
By maintaining a constant pitch, the depth of the thread, measured from crest to root, will also remain constant. This allows multi-start threads to maintain a shallow thread depth relative to their longer lead distance. Another design advantage of a multi-start thread is that more contact surface is engaged in a single thread rotation. A common example is a cap on a plastic water bottle. The cap will screw on in one quick turn but because a multi start thread was used there are multiple threads fully engaged to securely hold the cap in place.
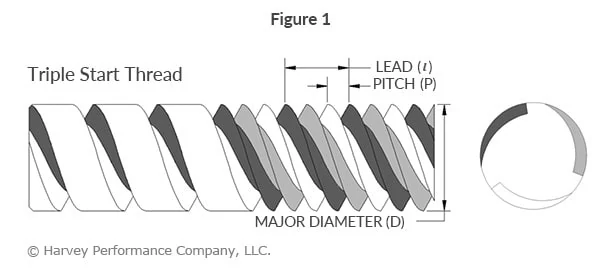
Figure 1 displays a triple start thread with each thread represented in a different shade. The left side of the image represents a triple start thread with just one of the three threads completed. This unfinished view shows how each individual thread is milled at a specific lead distance before the part is indexed and the remaining threads are milled. The right side of the image displays the completed triple start thread with the front view showing how the start of each thread is evenly spaced. The starting points of a double start thread begin 180° apart and the starting points of a triple start thread begin 120° apart.
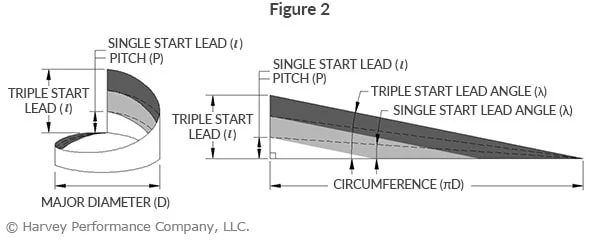
Figure 2 displays the triangle that can be formed using the relationship between the lead distance and the circumference of a thread. It is this relationship that determines the lead angle of a thread. The lead angle is the helix angle of the thread based on the lead distance. A single start thread has a lead distance equal to its pitch and in turn has a relatively small lead angle. Multi-start threads have a longer lead distance and therefore a larger lead angle. The graphic depicted on the right is a view of the lead triangle if it were to be unwound to better visualize this lead angle. The dashed lines represent the lead angle of a single start thread and double start thread of the same pitch and circumference for comparison. The colors represent each of the three intertwined threads of the triple start thread depicted in Figure 1.
Lead Angle Formula
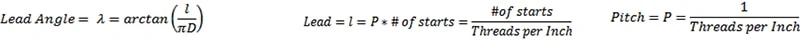
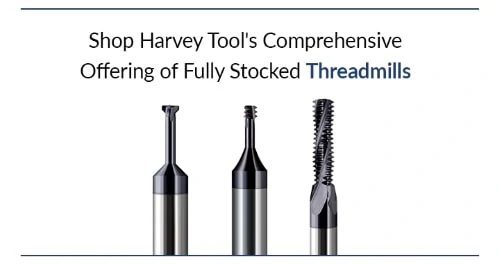
The charts below display the information for all common UN/Metric threads as well as the lead and lead angle for double and triple start versions of each thread. The lead angle represented in the chart is a function of a thread’s lead and major diameter as seen in the equation above. It is important to be aware of this lead angle equation when manufacturing a multi-start thread. The cutting tool used to mill the thread must have a relief angle greater than the lead angle of the thread for clearance purposes. All Harvey Tool Single Form Thread Milling Cutters can mill a single, double, and triple start thread without interference.
Machining a Multi-Start Thread
- Use the table or equation to determine the pitch, lead, and lead angle of the multi-start thread.
- Use a single form thread mill to helically interpolate the first thread at the correct lead. *The thread mill used must have a relief angle greater than that of the multi-start thread’s lead angle in order to machine the thread.
- Index to the next starting location and mill the remaining parallel thread/threads.
Click here for the full chart – starting on Page 2.




*The thread mill used must have a relief angle greater than that of the multi start thread’s lead angle in order to machine the thread.
When the thread mill is rotating does it not become a disc and relief angle on the tool has no effect? The relief is created from the difference in the tool diameter verses thread major diameter. I had this problem when trying to thread mill a 10-24 double lead internal thread. Thread would go oversize before you could get to full diameter because of tool distorting form.
Thanks for the comment, John. The relief angle does have an affect, as it limits the max lead angle you can have for the tool to effectively cut the part. When you helix down into the hole, it can rub on the backside of the cutting edge if the lead angle is greater than the relief angle. Please give our tech team a call if you run into any more problems, as many thread milling operations are case-by-case scenarios. Our Harvey Tool tech team can be reached at 800-645-5609.
I have a doubt that can we use UN-1.125-8 Multi start( 2 or 3) thread for horizontal axial loading ?
And also how to calculate the torque requirement and stress generated for same above case, if any one can please suggest any material.
Hi Pradeep, thanks for your question! For this case, it might be best if you call in to talk with our technical support team. It seems like we’d need more information from you in order to give you an accurate answer. Our tech team can be reached at 800-645-5609. Thanks!
How to do double thread ?
Please rply with program sample
Hello Karthi,
Please give our technical support team for help. They will be able to go into great detail on how to mill a double thread as well as be able to provide a sample program. Please call 800-645-5609.
How will be the force diffrence for single type Lead screw and Multiple type what are the advantages and disadvantages of type start threads
Great question! Your forces are much higher on the tool when cutting a multiple start thread. You have to feed the tool on a lathe 3x as fast on a 3 start thread versus a single start.
The shaft of the fastener is threaded which means the cylindrical body of the bolt has a running helical ridge which is called the crest. Between each of these crests, there are spaces called roots. These form the thread on the fastener. From Gi bolt manufacturers to hex bolt manufacturers ensure that fasteners come with the perfect threads.
Nice Blog Thanx For Sharing The Detail We Are At Nishant Steel Industries is ISO certified leading Fasteners manufacturer of high tensile hot and cold forged fasteners made in India.
Can we produce multi start (4 start) acme threads by thread rolling process
I would like some insight on an overwire measurement of a two lead external thread.
they gave a mil-std-1373 for reference, but ask for a thread that is not listed in that (1.625 – 0.1P – 0.2L ds)
They did, however, provide major, minor and pitch diameters with tolerances. I thought I would use the pee dee thread chart for 10 threads per inch, but I am worried the calculated results will not be accurate this way.
Any insight would be appreciated, Thanks
Hi Shawn,
Please reach out to our technicians in order to best assist you. You can give a call (800 645 5609 then 2 for tech) or email ([email protected]) in order to receive direct assistance from our team.
There is aluminium parts with 3 start thread of acme profile but each thread start and end need to be merged with root diameter in external thread. Any program available in CNC turning? Thank you.
Another and simpler way of machining a multi-lead thread is to use a multi-form thread mill and advance the tool in multiple pitches depending on the number of leads desired. Using a 4-40 thread as an example, the pitch is .025. For a single lead thread, you would obviously advance the tool one pitch (.025) for the desired thread. Now, if you wanted a double lead thread, you would advance the tool two (2) pitches (.050). You would do the same ratio for a triple lead thread. I worked at a medical implant shop, and that’s how we did double and triple lead threads, depending on the requirement. I have to admit, I still can’t wrap my head around how this all works.
As an apprentice centre lathe turner in the 1960s I machined many 3 and 4 start square threads on a lathe (even a 5 start on one occasion). These threads were used on the ‘reversing gear’ on steam locomotives.
As explained in this guide it is a matter of using trigonometry to ascertain the ‘lead angle’ and hand grinding a single point cutting tool with relief on the leading and trailing edge of the cutting tool. After the first thread is cut it is just a matter of using the compound slide to progress to the next thread and so on.
Basically, it is just a matter of progression of single start thread matching.