
Optimize Roughing With Chipbreaker Tooling
What is Chipbreaker Tooling?
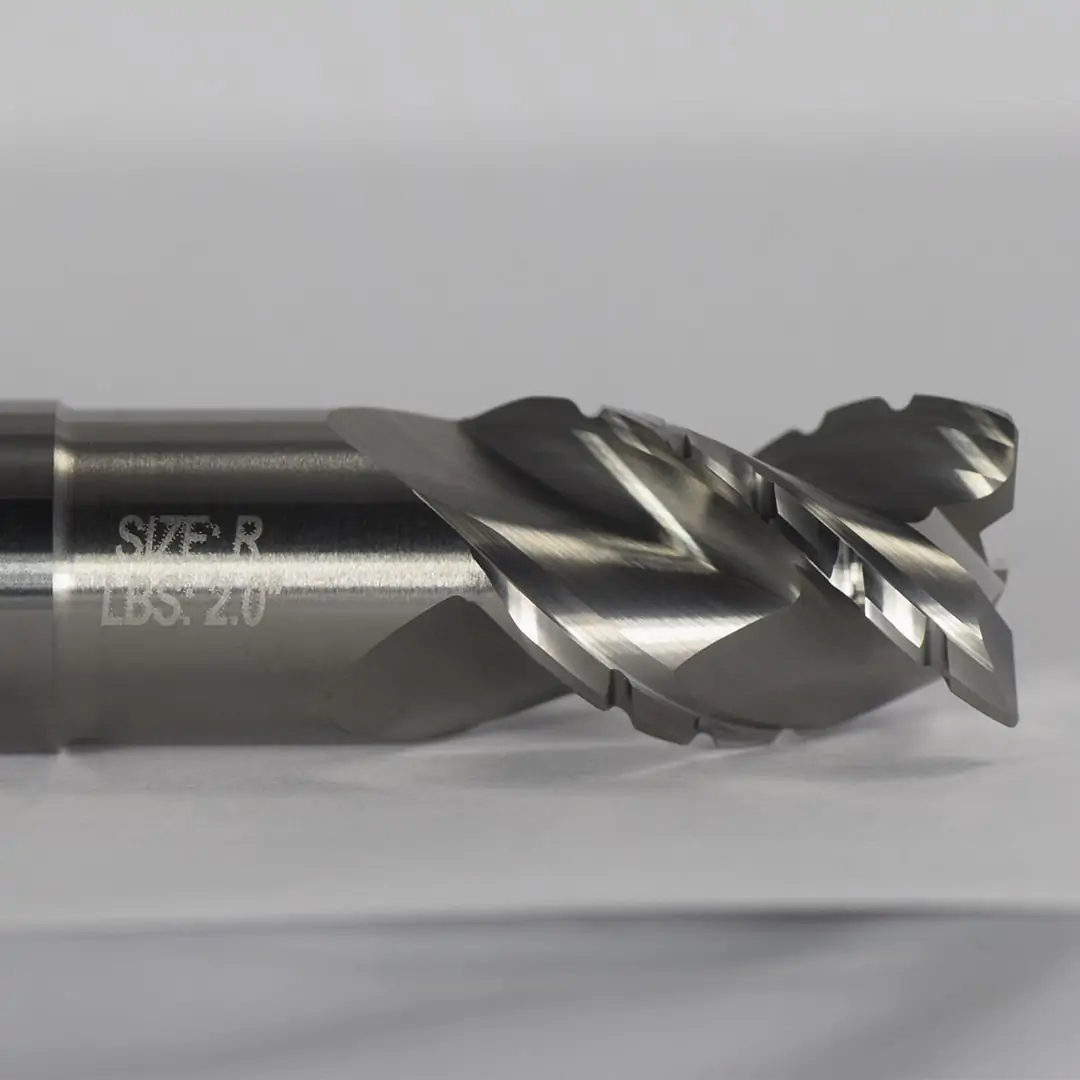
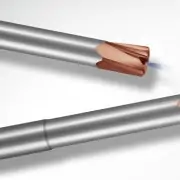
Chipbreaker End Mills feature unique notch profiles, creating a serrated cutting edge. These dividers break otherwise long, stringy chips into small, easily-managed swarf that can be cleanly evacuated from the part. But why is a chipbreaker necessary for some jobs, and not others? How does the geometry of this unique tool impact its proper running parameters? In this post, we’ll answer these questions and others to discover the very real benefits of this unique cutting geometry.
How Chipbreaker Tooling Works
As a tool rotates and its cutting edge impacts a workpiece, material is sheared off from a part, creating chips. When that cutting process is interrupted, as is the case with breaks in the cutting portion of the tool, chips become smaller in length and are thus easier to evacuate. Because the chipbreakers are offset flute-to-flute, a proper, flat surface finish is achieved as each flute cleans up any excess material left behind from previously passed flutes.
Benefits of Chipbreaker Tooling
Machining Efficiency
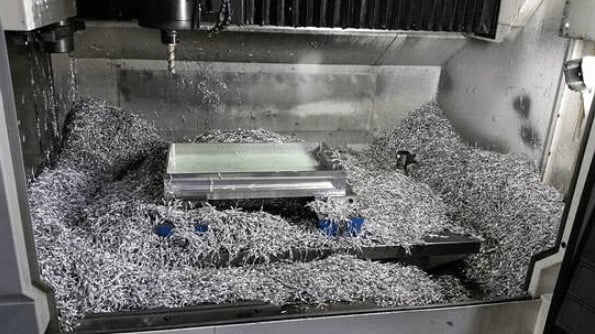
When chips are removed from the part, they begin to pile in the machine. For extensive operations, where a great deal of material is hogged out, chip accumulation can very rapidly get in the way of the spindle or part. With larger chips, accumulation occurs much faster, leaving machinists to stop their machine regularly to remove the waste. As any machinist knows, a stopped machine equates to lost money.
Prolonged Tool Life
Inefficient chip evacuation can lead to chip recutting, or when the the tool impacts and cuts chips left behind during the machining process. This adds stresses on the tool and accelerates rate of wear on the cutting edge. Chipbreaker tooling creates small chips that are easily evacuated from a part, thus minimizing the risk of recutting.
Accelerated Running Parameters
A Harvey Performance Company Application Engineer recently observed the power of a chipbreaker tool firsthand while visiting a customer’s shop in Minnesota. The customer was roughing a great amount of 4340 Steel. Running at the parameters below, the tool was able to run uninterrupted for two hours!
| Helical Part No. | 33737 |
| Material | 4340 Steel |
| ADOC | 2.545″ |
| RDOC | .125″ |
| Speed | 2,800 RPM |
| Feed | 78 IPM |
| Material Removal Rate | 24.8 Cubic In/Min |
Chipbreaker Product Offering
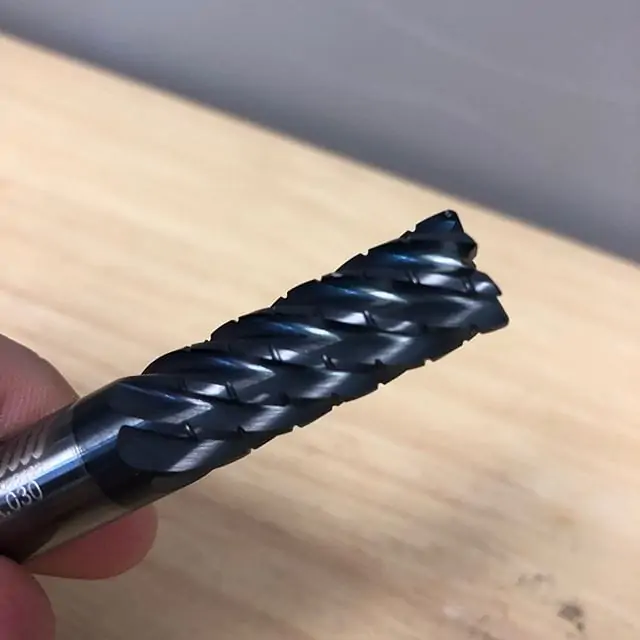
Chipbreaker Geometry is often utilized in aluminum jobs and with other materials where long, stringy chips are common. Materials that produce a powdery chip, such as graphite, should not be machined with a chipbreaker tool, as chip evacuation would not be a concern. Helical Solutions’ line of chipbreaker tooling includes a 3-flute option for aluminum and non-ferrous materials, and its reduced neck counterpart. Additionally, Helical offers a 4-flute rougher with chipbreaker geometry for high-temp alloys and stainless steels. Harvey Tool’s expansive product offering includes a composite cutting end mill with chipbreaker geometry.
In Summary
Chipbreaker geometry, or grooves within the cutting face of the tool, break down chips into small, manageable pieces during the machining process. This geometry can boost shop efficiency by minimizing machine downtime to clear large chips from the machining center, improve tool life by minimizing cutting forces exerted on the tool during machining, and allow for more accelerated running parameters.



When will you start to offer this in your 5, 6, and even 7-flute tools?
With their stronger core and already excellent design, those are the tools that really lend themselves to the deep cuts to maximize removal.
Hi, Jim! Thanks for your comment. Actually, we’ve already planned to offer chipbreaker tooling with more flutes. Stay tuned to Helical for 5 and 7 flute options, coming in our next catalog this February!
I was wondering why you show them doing high speed cutting but then on the actual tool page when you go to the speeds and feeds you do not have data for this? Is this something that will be added in the future?
Hi Bryce,
The speeds and feeds we provide on both our website and in the catalog are traditional speeds and feeds only, as the charts would become too cumbersome with more data. For more advanced machining operations check out the Helical Milling Advisor, which is designed to provide recommendations for various milling options, including high efficiency machining.
So I guess you don’t have an answer because what I said was true. It’s ok. I bought one from another supplier to try and sure enough, it leaves horizontal lines. The other supplier doesn’t try to hide it, though. I will surely keep you guys out of the running for any future tooling needs we have since you’re not interested in answering valid questions.
Hello – I am not sure what you are referring to here. We do not have any previous comments from you on this post, but we would be happy to answer any questions you have on these tools. You can either respond here, or you can email [email protected] and they would be happy to help you out. Let us know if we can be of any more help!
I posted a question a few weeks ago asking about how big the horizontal lines these endmills were likely to produce would be. The question sat for about a week waiting for approval, then went away without being approved.
I figured you were not interested in answering the question, hence my response.
I got the info I needed from a more responsive supplier. No need to respond here, and feel free to delete this and my previous comment.
We apologize for any inconvenience this may have caused you. In the future for the quickest response possible about our tools send an email to [email protected].