
Harvey Tool Coatings: Maximizing Tool Performance
Proper tool coating plays a large role during the selection of a CNC cutting tool. At Harvey Tool, coatings are optimized for specific materials and alloys to ensure the highest tooling performance, possible. Each coating offers a unique benefit for the cutting tool: increased strength, enhanced lubricity, heat resistance, and wear mitigation, just to name a few.
In Benefits of Tool Coatings, the method of applying coatings to tools is examined. In this post, we’ll take a closer look at each Harvey Tool coating to examine its key properties, and to help you decide if it might add a boost to your next CNC application.
Harvey Tool offers a wide range of tool coating options for both ferrous and exotic materials, as well as non-ferrous and non-metallic materials. In the Harvey Tool catalog, coatings are often denoted in a -C# at the end of the product part number.
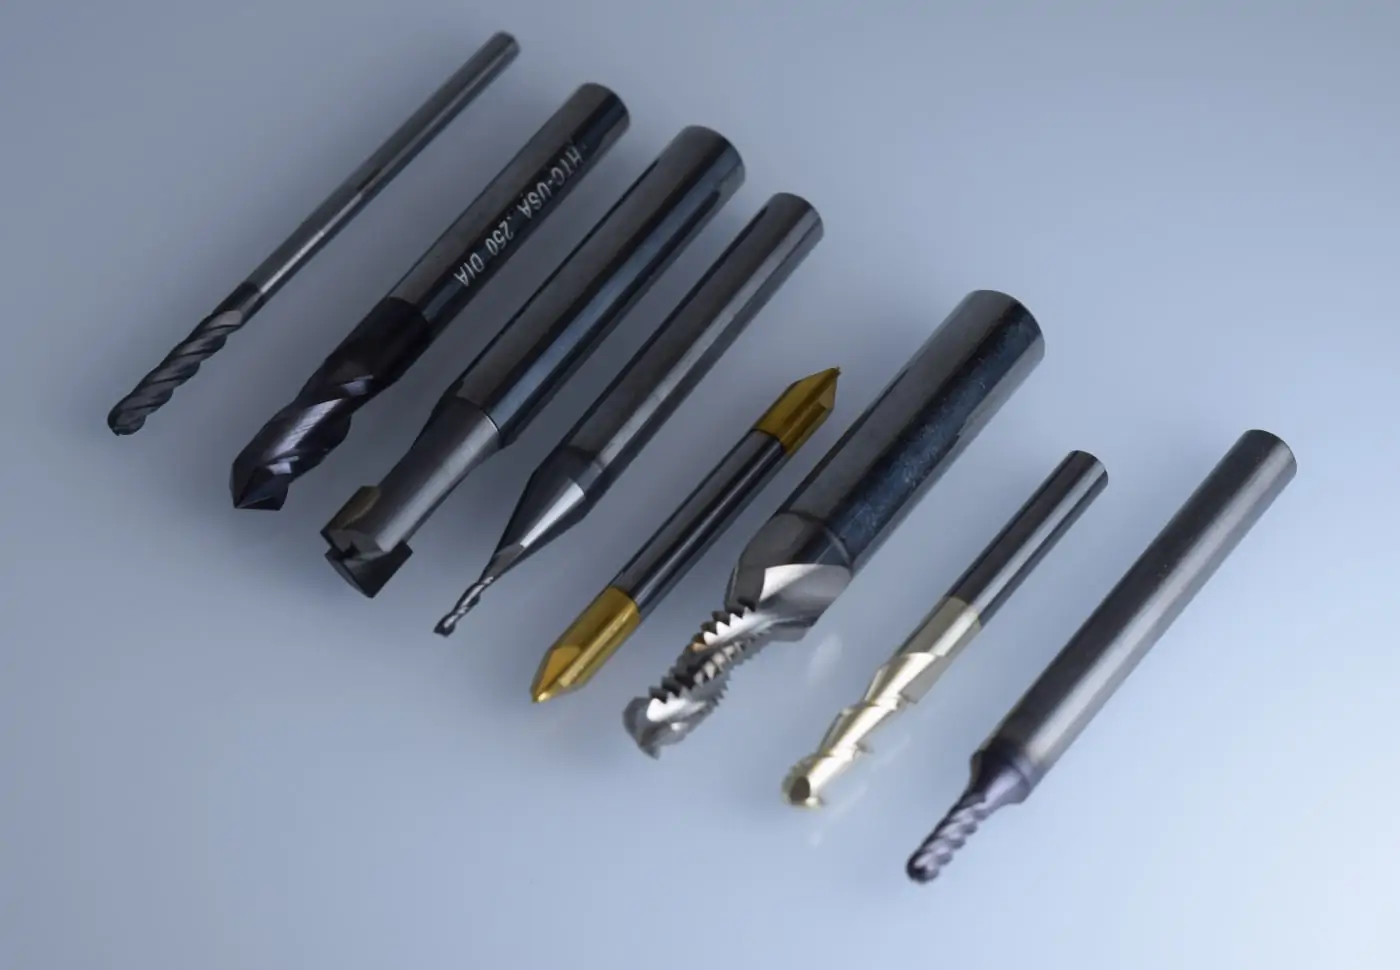
Harvey Tool Coatings for Ferrous and Exotic Materials
TiN
TiN, or Titanium Nitride (-C1), is a mono-layer coating meant for general purpose machining in ferrous materials. TiN improves wear resistance over uncoated tools and aids in decreasing built-up edge during machining. This coating, however, is not recommended for applications that generate extreme heat as its max working temperature is 1,000 °F. TiN is also not as hard as AlTiN and AlTiN Nano, meaning its less durable and may have a shorter tool life.
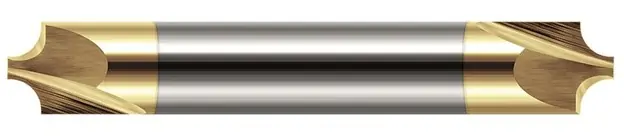
Harvey Tool 46062-C1
AlTiN
AlTiN, or Aluminum Titanium Nitride (-C3), is a common choice for machinists aiming to boost their tool performance in ferrous materials. This coating has a high working temperature of 1,400 °F, and features increased hardness. AlTiN excels in not only dry machining, due to its increased lubricity, but also in machining titanium alloys, Inconel, stainless alloys, and cast iron. To aid in its high heat threshold, the aluminum in this coating coverts to aluminum oxide at high temperatures which helps insulate the tool and transfer its heat into the formed chips.
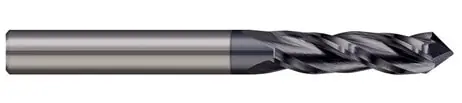
Harvey Tool 823816-C3
AlTiN Nano
AlTiN Nano or Aluminum Titanium Nitride Nano (-C6) is Harvey Tool’s premium coating for ferrous applications. This coating improves upon AlTiN by adding silicon to further increase the max working temperature to 2,100 °F while also increasing its hardness for increased tool life during demanding applications. Due to its penchant for demanding applications, AlTiN is recommended for hardened steels, hardened stainless, tool steels, titanium alloys, and aerospace materials. These applications often create high levels of heat that AlTiN Nano was designed to combat.
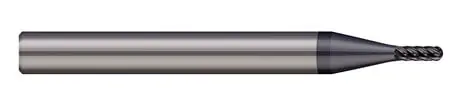
Harvey Tool 843508-C6
Note: AlTiN and AlTiN Nano are not recommended for use in Aluminum or Aluminum Alloys due to their high affinity to those materials.
Tool Coatings for Non-Ferrous and Non-Metallic Materials
TiB2
TiB2, or Titanium Diboride (-C8), is Harvey Tool’s “bread and butter” coating for non-abrasive aluminum alloys and magnesium alloys, as it has an extremely low affinity to aluminum as compared to other coatings. Aluminum creates lower working temperatures than ferrous materials, so this coating has a max working temperature of of a suitable 900 °F. TiB2 prevents built-up edge and chip packing, further extending its impressive tool life. TiB2 is not recommended for abrasive materials as the carbide is slightly weakened during the coating process. These materials can cause micro fractures that may damage the tool at high RPMs.
TiB2 can be found on a wide variety of Harvey Tool 2 and 3 flute tools as the premium option for high performance in aluminum alloys.
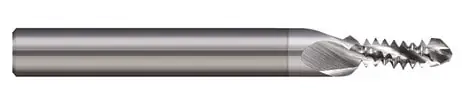
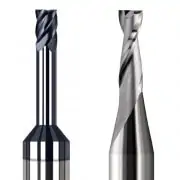
Harvey Tool 820654-C8
ZrN
ZrN, or Zirconium Nitride (-C7), is a general-purpose coating for a wide variety of non-ferrous materials, including abrasive aluminum alloys. This tool coating is a lower cost alternative to diamond coatings, while still boasting impressive performance through its high hardness levels and overall abrasion resistance. ZrN has a max working temperature of 1,110 °F with strong lubricity in abrasive alloys. This coating is best suited for abrasives, such as brass, bronze, and copper, as well as abrasive aluminum alloys that should not be used with TiB2.
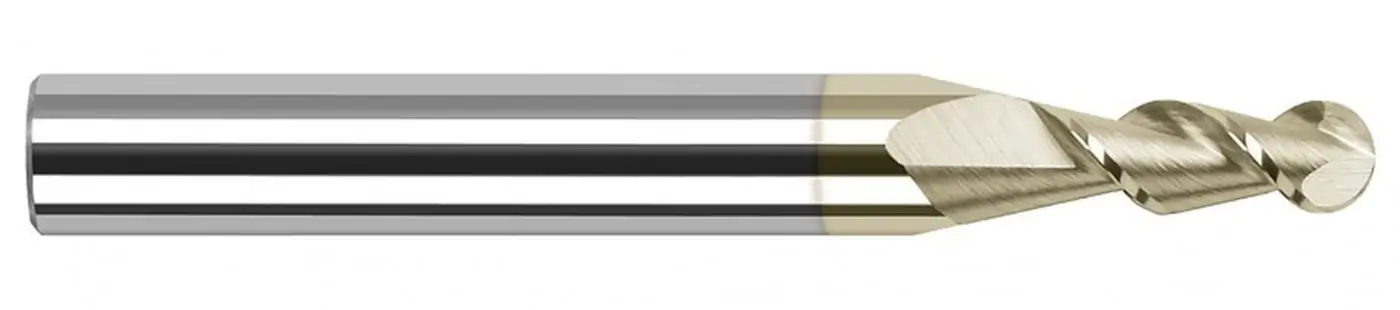
Harvey Tool 27912-C7
CVD Diamond Tool Coatings
CVD Diamond, or Crystalline CVD Diamond, is a process where the coating is grown directly onto the carbide end mill. This process dramatically improves hardness over other coatings, improving tool life and abrasion resistance while also allowing for higher feed rates. The trade-off for increased wear resistance is a slight rounding of the cutting edge due to the coating application. Due to its increased wear resistance, CVD is best suited for highly abrasive materials such as graphite, composites, green carbide, and green ceramics. Similarly, these tool coatings have a max working temperature of 1,100 °F, meaning they are not well suited for ferrous applications.
Harvey Tool’s CVD Diamond Coating Options:
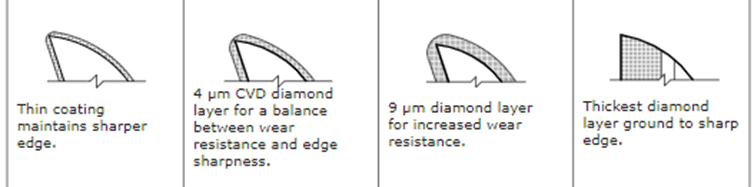
Amorphous, CVD 4 μm, CVD 9 μm, PCD Diamond
CVD Diamond (4 μm)
The 4 μm is thinner than the 9 μm allowing for a sharper cutting edge, which in effect leaves a smoother finish.
CVD Diamond 9 μm)
The 9 μm CVD tool coating offers improved wear resistance over the 4 μm CVD and Amorphous coatings due to its increased coating thickness.
Amorphous Diamond
Amorphous Diamond (-C4) is a PVD diamond coating which creates an exceptionally sharp edge as compared to CVD. This coating aids in performance and finish in abrasive non-ferrous applications, as it allows for greatly improved abrasion resistance during machining, while still maintaining a sharp cutting edge necessary for certain abrasives. Due to the thinness of the coating, edge rounding is prevented in relation to CVD diamond tooling. Amorphous Diamond is best suited for use in abrasive plastics, graphite, and carbon fiber, as well as aluminum and aluminum alloys with high silica content, due to their abrasiveness. The max working temp is only 750 °F, so it is not suited for use in ferrous machining applications.
Harvey Tool 809362-C4
PCD Diamond
PCD Diamond, or Polycrystalline Diamond, is a tool coating that is brazed onto the carbide body. In comparison to the other diamond coatings, PCD does not face the same challenges of other coatings as it pertains to rounded cutting edges, as these edges are ground sharp. PCD has the edge benefits of Amorphous Diamond with the abrasion resistance of CVD Diamond. PCD is the thickest diamond layer offered by Harvey Tool, and excels due to its incredible hardness and abrasion resistance. This tool is best suited for all forms of abrasive, non-ferrous materials including abrasive plastics, graphite, carbon fiber, and composites. Similar to the other non-ferrous tool coatings, PCD is not suited for ferrous applications due to its working temperature of 1,100 °F.
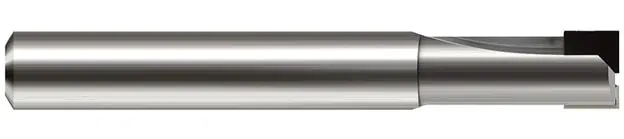
Harvey Tool 12120
Tool Coating Summary
When deciding on a coating for your application there are many factors to be considered. Different coatings often cross several applications with performance trade-offs between all of them. Harvey Tool offers a “Material Specific Selection” that allows users to choose tooling based upon what materials they are working with. Further, Harvey Tool’s technical team is always a phone call away to help in finding the right tool for your specific applications at 1-800-645-5609. Also, you can contact Harvey Tool via e-mail.


Leave a Reply
Want to join the discussion?Feel free to contribute!