Milling 4140 Steel With Helical Feed & HEM Mill
Watch this video of Automag pushing Helical’s 5 Flute Combination Feed & HEM End Mill to the limits by running pocket and plunge milling applications without coolant.
Helical’s Combination Feed and HEM End Mills feature a specialized end profile and OD geometry for both High Feed and High Efficiency Milling (HEM) applications. The variable pitch and offset chipbreaker geometry offer optimal chip evacuation, minimized harmonics, and reduced tool pressure.
These tools offer outstanding performance and high temperature resistance in a wide range of ferrous materials, including low and medium alloy steels, tool steels, cast iron, titanium, and titanium alloys. Tplus coated and offered in 4 and 5 flute styles, these multi-functional tools were made to wow you.
Click here to explore the full Helical Solutions offering of Combination Feed & HEM End Mills
Pocket Milling
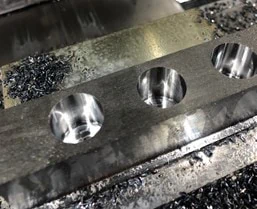
Automag used Helical’s 84496 end mill to pocket mill without coolant at 1040 SFM and 550 IPM to achieve a total depth of 1” at .020” depth per revolution. This ½” diameter tool created multiple .980” diameter holes in 4140 Steel with zero signs of tool failure.

Plunge Milling
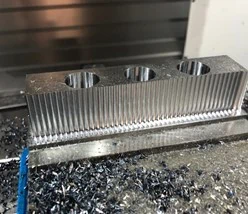
Automag used the same 5 flute tool to plunge mill the sides of the part without coolant at 1308 SFM and 1040 IPM with a 47% spindle load and .125” step-over. Running Helical’s 5 Flute Combination Feed & HEM End Mill the fastest the HAAS will run, resulted in no signs of tool failure.


I’d say there is a huge mistake here. There is no way that machine is moving at 550ipm. 60 ipm max is what i see.
This may be programmed at 550 but there might be percentage reduction in the toolpath somewhere. Plus, a Haas won’t show you actual feed-rate, only the programmed rate. So, if the machine is slowing down to maintain accuracy, it doesn’t show it on the screen. I would like further proof that this is in fact ACTUALLY moving at 550.
Yeah I was just looking at that. They say it’s a Ø.980″ and that tool is Ø.500″. That makes a Ø.480 toolpath circle. I paused the video and counted the revolutions for 1 second. I estimated 1.8 revolutions in 1 second. The circumference of that toolpath circle is 1.5080″, so 1.5080″ x 1.8 x 60s = 162ipm. Even if you factor it out for the chip load at the circumference of the Ø.980″, it only comes out to about 332ipm.
A HAAS doesn’t have the spindle torque or, acceleration rate, to pull off the prescribed numbers; but, it would be interesting to see the end mill run on a machine that was actually capable of those speeds and feeds.
I think the above is likely valid.
My question is, what is the lifespan of that tool.
Whenever I see sparks , its not if its going to fail but when.
Having said that ,Its usually soon.
Why would you use a solid carbide end mill for a process thats ideally suited to an insert cutter.
Inserts are relatively inexpensive vs a solid carbide end mill.
Obviosly, its a very good cutter IMO wrong application.