
Ramping to Success
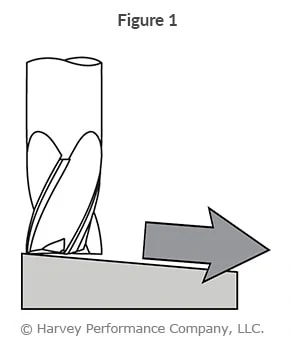
Poor tool life and premature tool failure are concerns in every machining application. Something as simple as tool path selection – and how a tool first enters a part – can make all the difference. Tool entry has a great deal of influence on its overall success, as it’s one of the most punishing operations for a cutter. Ramping into a part, via a circular or linear toolpath, is one of the most popular and oftentimes the most successful methods (Figure 1). Below, learn what ramping is, its benefits, and in which situations it can be used.
Check Out Our Micromachining Webinar to Get More Life Out of Your Miniature Cutting Tools
What is Ramping?
Ramping refers to simultaneous radial and axial motion of a cutting tool, making an angular tool path. Oftentimes, this method is used to approach a part when there is a need to create closed forms such as pockets, cavities, engravings, and holes. In doing so, the need to plunge with an end mill or drill to create a starting point is eliminated. Ramping is particularly important in micromachining where even the slightest imbalance in cutting forces can cause tool failure.
There are two types of ramping toolpaths: Linear and Circular (Figure 2 ).
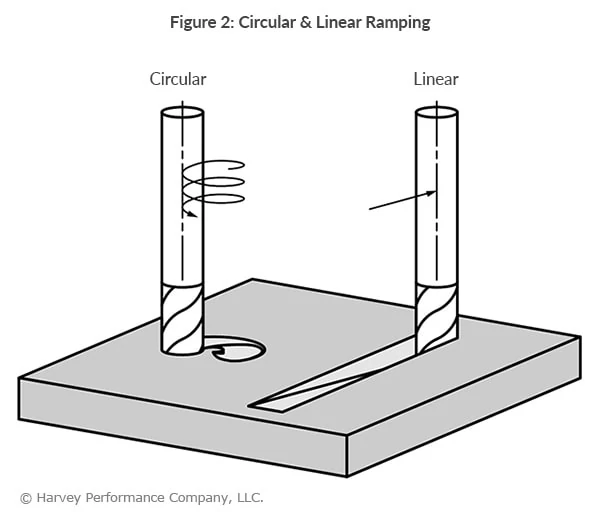
Linear Ramping involves moving a cutting tool along two axes (the z-axis and one of the x, y axes). This method has significant more radial engagement with complementary increased cutting forces distributed across only two axes.
Circular Ramping (Helical Interpolation) has a spiral motion of the cutting tool that engages all three axes (x, y, and z axes). This method typically has less radial engagement on the cutting tool, with the cutting forces distributed across the three different axes. This is the recommended method, as it ensures the longest tool life.
Suggested Starting Ramp Angles:
Soft/Non-Ferrous Materials: 3° – 10°
Hard/Ferrous Materials 1° – 3°
Benefits of Ramping
When a tool enters the part via a Ramping method, it gradually increases in depth, preventing any shock loading on end mills. This reduces costs resulting from unnecessary tool breakage. Ramping produces smaller chips when compared to plunging, which makes chip evacuation faster and easier. As a result, cycle time can be decreased by running the end mill at faster parameters. Ramping also creates an extra space in the tool changer that would otherwise be occupied by a drill purposed with machining a starter hole.
Arcing
Similar to ramping in both method and benefit, arcing is another technique of approaching a workpiece (See Figure 3).
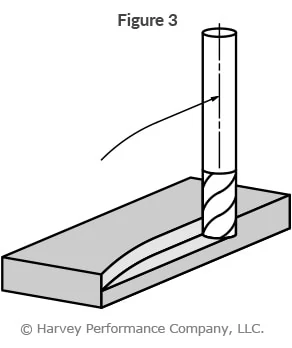
While ramping enters the part from the top, arcing enters from the side. The end mill follows a curved tool path (or arc) when milling, thus gradually increasing the load on the tool as the tool enters the part, as well as gradually decreasing the load as the tool exits the part. In this way, shock loading and possible tool breakage are avoided.
For more information on ramping, arcing, and other tool entry methods, please see Helical Solutions’ “Types of Tool Entry.”



I usually ramp endmills at 1 degree- most of the material we cut is unforgiving and I don’t like to risk breaking a tool. The trickiest angle to figure out is when helical milling or ramp milling a counterbore. If you are helical milling a .500 counterbore with a .375 diameter endmill, the actual distance you are traveling is .125 (diameter of cutter path) times Pi or .125 x 3.1415 =.3927. So if you want to ramp down at 1 degree multiply .017 (one degree per inch) x .3927 =.0067 per revolution is a one degree ramp inside that counterbore. This can be applied to any size tool when you have to pay attention to the angle or how much the tool can handle for depth of cut. Many high feed mill inserts can only take a small depth of cut- so even if you are milling a 4 inch circle, your ramp has to be to a depth and not an angle.