
Successful Slotting With Miniature Cutting Tools
Whether your tool is a 1” diameter powerhouse rougher or a .032” precision end mill, slotting is one of the hardest operations on the tool. During slotting operations, a lot of force and pressure is placed on the entire cutting edge of the tool. This results in slower speeds and feeds and increased tool wear, making it one of the nastier processes even for the best cutting tools.
With miniature tooling (for the purposes of this blog, under 1/8” diameter) the game changes. The way we approach miniature tooling is completely different as it relates to slotting. In these instances, it is vitally important to select the correct tool for these operations. A few of the suggestions may surprise you if you are used to working with larger tooling, but rest assured, these are tried and tested recommendations which will dramatically increase your success rate in miniature slotting applications.
Use as Many Flutes as Possible
When running traditional slotting toolpaths, the biggest concern with the cutting tool is getting the best chip evacuation by using the proper flute count. Traditionally speaking, you want to use the fewest amount of flutes possible. In Aluminum/Non-Ferrous jobs, this is typically no more than 2/3 flutes, and in Steel/Ferrous applications, 4 flutes is recommended. The lower flute count leaves room for the chips to evacuate so you are not re-cutting chips and clogging the flutes on your tool in deep slots.
Achieve Increased Efficiency With Miniature Tooling – Utilize Harvey Tool’s Speeds & Feeds Charts Today
When slotting with miniature tools, the biggest concerns are with tool rigidity, deflection, and core strength. With micro-slotting we are not “slotting”, but rather we are “making a slot”. In traditional slotting, we may drive a ½” tool down 2xD into the part to make a full slot, and the tool can handle it! But this technique simply isn’t possible with a smaller tool.
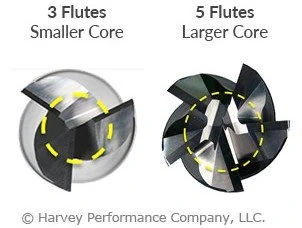
For example, let’s take a .015” end mill. If we are making a slot that is .015” deep with that tool, we are likely going to take a .001” to .002” axial depth per pass. In this case, chips are no longer your problem since it is not a traditional slotting toolpath. Rigidity and core strength are now key, which means we need to add as many flutes as possible! Even in materials like Aluminum, 4 or 5 flutes will be a much better option at smaller diameters than traditional 2/3 flute tools. By choosing a tool with a higher flute count, some end users have seen their tool life increase upwards of 50 to 100 times over tools with lower flute counts and less rigidity and strength.
Use the Strongest Corner Possible When Slotting
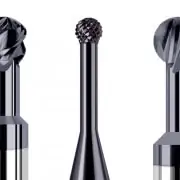
Outside of making sure you have a strong core on your miniature tools while making a slot, you also need to take a hard look at your corner strength. Putting a corner radius on your tooling is a great step and does improve the corner strength of the tool considerably over a square profile tool. However, if we want the strongest tip geometry, using a ball nose end mill should also be considered.
A ball nose end mill will give you the strongest possible tip of the three most common profiles. The end geometry on the ball nose can almost work as a high feed end mill, allowing for faster feed rates on the light axial passes that are required for micro-slotting. The lead angle on the ball nose also allows for axial chip thinning, which will give you better tool life and allow you to decrease your cycle times.
Finding the Right Tool for Miniature Slotting Operations
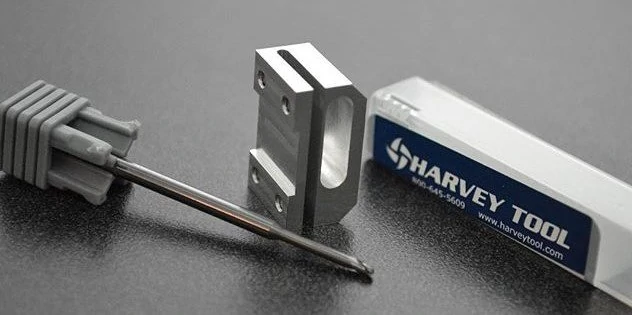
Precision and accuracy are paramount when it comes to miniature tooling, regardless of whether you are slotting, roughing, or even simply looking to make a hole in a part. With the guidelines above, it is also important to have a variety of tooling options available to cater to your specific slotting needs. Harvey Tool offers 5 flute end mills down to .015” in diameter, which are a great option for a stronger tool with a high flute count for slotting operations.
If you are looking to upgrade your corner strength, Harvey Tool also offers a wide selection of miniature end mills in corner radius and ball nose profiles, with dozens of reach, length of cut, and flute count options. Speeds and feeds information for all of these tools is also available, making your programming of these difficult toolpaths just a little bit easier.
Achieving Slotting Success: Summary
To wrap things up, there are three major items to focus on when it comes to miniature slotting: flute count, corner strength, and the depth of your axial passes.
It is vital to ensure you are using a corner radius or ball nose tool and putting as many flutes as you can on your tool when possible. This keeps the tool rigid and avoids deflection while providing superior core strength.
For your axial passes, take light passes with multiple stepdowns. Working your tool almost as a high feed end mill will make for a successful slotting operation, even at the most minuscule diameters.



This is an amazing work for cnc machines.
Thanks for sharing the informative post regarding successful slotting with miniature cutting tools. You mentioned very well the suggestions for used to working with larger tooling that will dramatically increase your success rate in miniature slotting applications. Greate post, Keep it up!