Micro 100 Broaching Tools: Everything You Need to Know
With the release of Micro 100’s 2025 Spring Catalog comes a new family of broaching tools, marking their debut within both the Micro 100 and Harvey Performance brands. Alongside this tooling launch are several differences in application methods and recommended running parameters.
What is Broaching?
Broaching, while performed in a lathe, is slightly different from the classic boring and grooving operations we encounter daily.
In a traditional turning operation, the workpiece rotates while the tool remains stationary. In a broaching operation, neither the workpiece nor the tool spins. Instead, the tool advances toward the workpiece and removes material in very small increments, similar to planing a block of wood.
Micro 100’s Offering
All broaches come on a Micro 100 Quick-Change shank, with sizes ranging from .1875” to .375”, depending on the broach size. These QC broaching tools are coolant-fed to promote better chip evacuation. An optional nACRo coating is available, enhancing resistance to wear and heat, which is especially useful in applications involving difficult-to-machine materials.
Keyway Broaches
Keyway broaches, as their name suggests, are used to cut keyways commonly found in power transmission applications involving gears and pulleys.
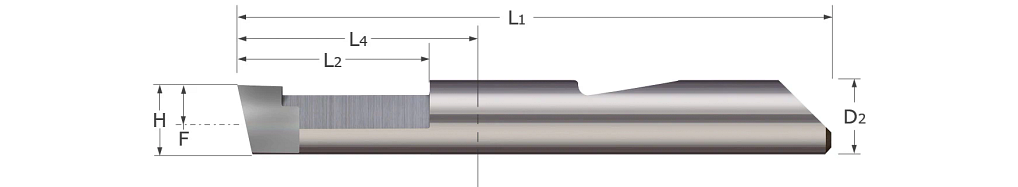
Micro 100 offers two styles of keyway broaches, available in both standard and metric sizing. This offering provides machinists with a range of sizes that are necessary to meet their application needs.
Imperial Offering
Micro 100’s standard-sized broaches come in widths of .0938”, .1250”, .1875”, and .2500”. Maximum broach depths of .500”, 1.000”, or 1.500” are available, depending on the broach width.
Metric Offering
Our metric keyway broaches are available in nominal widths from 2 mm to 6 mm. Each size is measured according to the desired fit and offered in C11, JS9, or P9 tolerance grades.
C11 reflects a “loose fit” tolerance, useful in applications where the keyway may be exposed to corrosion, dust, or other contaminants, or where deformation may occur.
JS9 represents a “normal fit”—not a press fit, but not a loose fit either. This is often required in situations where the key needs to be adjusted or shifted without much force or difficulty.
The tightest of the three offered tolerance classes is P9, which represents a “press fit.” In this case, the keyway is cut slightly smaller than the key, forcing it into the slot to create a very tight and secure connection.
Square Broaching
Micro 100 also offers square broaching tools. These broaches, like the keyway style, are pushed into the workpiece and remove material in multiple passes. They are primarily used to create the square socket found at the top of certain screws, commonly seen in machinery, construction, or other industrial applications.

Our square broaches come in metric sizes and can cut square holes ranging from 1.5 mm to 4.0 mm. When examining the geometry of these tools, you’ll notice they are cut to one corner of the square profile. Unlike keyway broaches, they must be rotated 90° when one corner is cut to create the remainder of the square form.
Although they have a fixed broach width, our square broaches are capable of cutting a range of square sizes. Take our QBRSQ-1520, for example—it features a .056” width and can cut squares from .059” to .078” (1.5 mm to 2.0 mm). When selecting a tool, it’s important to base your choice on the desired finished hole size, rather than the width of the cutter itself.
Hexagonal Broaching
The final option in Micro 100’s broaching lineup is our hexagonal broach style. These tools function similarly to the square broaches mentioned earlier, with the form created in six portions. Our hexagonal broaches can cut forms as small as .078” (2.0 mm) and up to .315” (8.0 mm). As with the square broaches, it’s important to select a tool based on the desired finish size of the hole, rather than the tooth width itself.
Hexagonal holes are often designed to work in conjunction with Allen keys. They are also commonly used for socket head cap screws. These fasteners are widely used across various industries, including automotive and construction settings.
What to do Before Making Your First Chips
Before making a cut with Micro 100’s broaching tools, there are a few important things to ensure are in place. Due to the high force involved in broaching, your machine should be equipped with a mechanical spindle lock. This lock helps achieve a higher-quality finish and, more importantly, improves feature accuracy.
The use of coolant is also strongly encouraged whenever possible, as it helps increase tool life, improve surface finish, and enhance chip evacuation. If your application requires broaching within a blind hole, be sure to create a cross hole or relief groove at the bottom of the hole to allow chips to evacuate properly.
Mastering Square & Hexagonal Broaching
To begin, the broach dimensions must be measured accurately and programmed into the machine. Ensure the tool is positioned at the 12 o’clock location to allow proper chip evacuation.
If cutting a hexagonal profile, the pre-drill should be approximately 1.035 times the desired feature size (1.1× for a square profile).
Before the first pass is made, visually check the tool path by positioning the tool at the starting point of the stroke, and program a stop there to verify correct alignment.
After each pass, ensure the tool is radially clear of the groove before fully retracting it. On the final return stroke, completely remove the broach from the hole. Finally, rotate the workpiece by 60 degrees—90 degrees for a square profile—and repeat the cutting process for the remaining corners.
Best Practices for Keyway Broaching
Keyway broaches require an additional calculation to determine the correct starting position for the first pass. An example calculation is provided below.
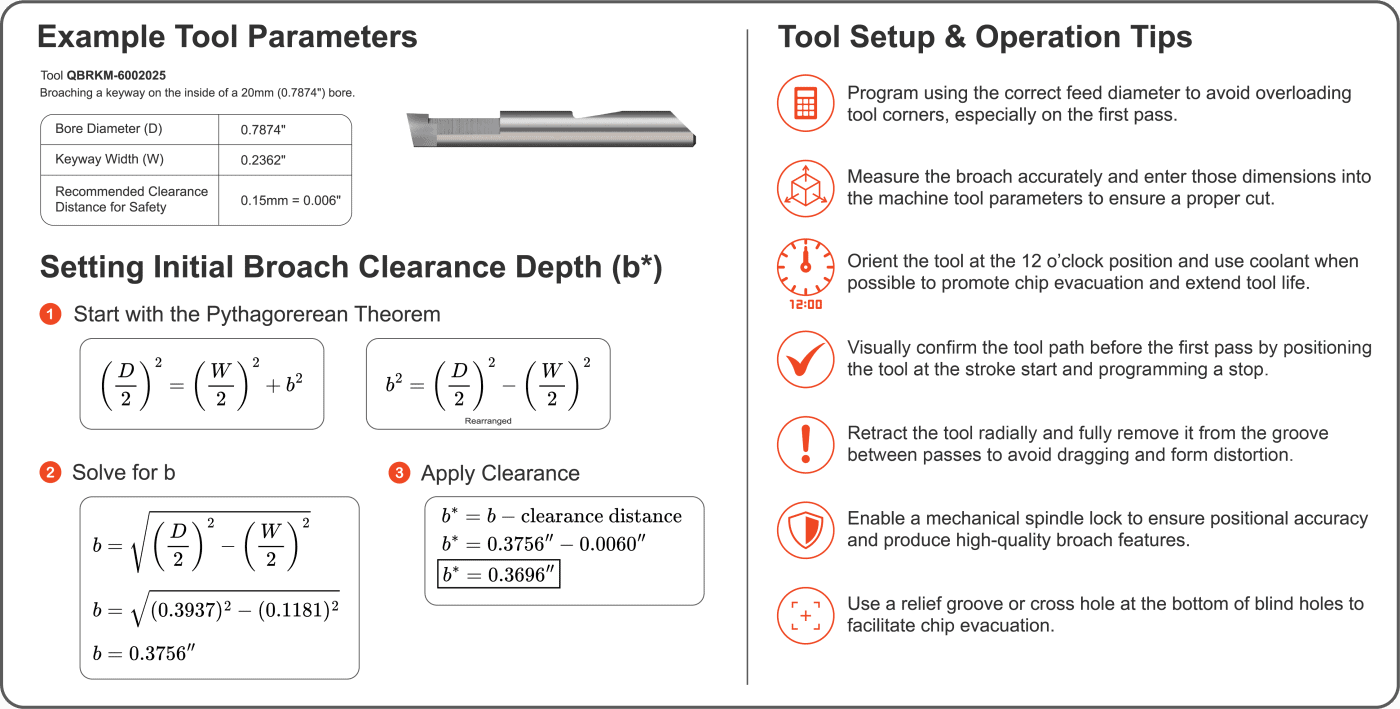

After the initial pass is completed, continue cutting normally until the desired keyway size is met. As with square and hex broaching, ensure the tool is radially clear of the groove after each pass before retracting. On the final return stroke, completely remove the broach from the hole.
In Summary
Micro 100s offering of broaching tools is fit for a large variety of broaching applications you may come across. Whether square, standard, or hexagonal, metric or imperial, Micro 100 has the tools to help you cut every step of the way.
To see the full range of tooling that Micro 100 has to offer, please visit our website micro100.com.
For any further questions regarding our broaching tools or Micro 100 as a whole, please don’t hesitate to call us at +1 844-393-8665 or email us at [email protected].