Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Tag Archive for: CNC

Drill Substrate Guide: HSS vs Cobalt vs Carbide

February 5, 2026/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Tool Selection/by Isabella Luciano

Drilling applications require careful consideration of material, production volume, and machine setup to ensure optimal hole quality, tool life, and cost. Harvey Performance Company offers drills in three primary substrates: carbide, cobalt, and high-speed steel (HSS). This guide breaks down the differences between the drilling substrate options and helps you choose the right tool for your specific application.

Solid Carbide Drills

Advantages of Carbide Drills

  1. Extreme Hardness and Wear Resistance
    • Carbide drills maintain sharp cutting edges longer than HSS or cobalt, even in abrasive materials. This reduces tool changes and helps to maintain consistent hole quality.
  2. High Heat Tolerance
    • Carbide can withstand cutting temperatures above 2,100°F (1,150°C), allowing higher speeds and feeds for faster material removal and shorter cycle times.
  3. Precision Machining
    • Carbide maintains tight tolerances and excellent surface finish in hard steels, tool steels, ceramics, composites, and high-temperature alloys, making it ideal for precise, high-performance applications.
  4. Long-term Cost Efficiency
    • Although the initial cost is higher, carbide’s longer tool life reduces frequent tool changes, lowering overall costs in high-volume production.

Drawbacks of Carbide as a Drill Substrate

  1. Brittle Nature
    • Carbide is more prone to chipping or breaking if the machine setup is not rigid, feed rates are too aggressive, or vibration is present.
  2. Regrinding Requirements
    • Carbide usually requires CNC grinding equipment for precise sharpening, unlike HSS, which can often be reground using conventional machines.
  3. Initial Investment
    • Carbide has a higher upfront cost, which may not be justified for use in short runs or soft materials, where less expensive HSS or cobalt drills can provide adequate performance.

What are the Ideal Applications for Carbide Drills?

Carbide drills excel in:

  • Large production runs requiring consistent tool life
  • Hard materials above 45 HRC, such as tool steels and high-temperature alloys
  • Applications requiring high-speed cutting and maximum material removal
  • Situations demanding precise hole tolerances and surface finish

Example: Valor Holemaking High Performance Carbide Drills are engineered to provide unmatched precision and repeatability in difficult-to-machine materials. Material-specific geometries and coolant-through designs improve heat management and tool life in demanding applications.

High Speed Steel (HSS) Drills

Advantages of HSS Drills

  1. Tough and Durable
    • High Speed Steel is the least brittle of the three materials, reducing the risk of breakage during less rigid setups.
  2. Easier to Regrind
    • HSS Drills can be sharpened and reconditioned using conventional grinding equipment, which reduces shop complexity and cost.
  3. Cost-Effective
    • The lower cost-per-tool makes HSS ideal for small jobs or low-volume production where long-term tool life is less critical.
  4. Versatile for Soft Materials
    • HSS performs well in most non-ferrous metals providing reliable results for general-purpose machining without the higher cost of harder substrates.

Drawbacks of High Speed Steel Drills

  1. Limited Heat Tolerance
    • High Speed Steel Drills can only handle cutting temperatures up to 1,100°F (600°C), restricting cutting speeds and material removal rates.
  2. Shorter Tool Life
    • HSS Edges dull faster than cobalt or carbide, requiring more frequent replacement, affecting productivity.
  3. Not Ideal for Very Hard Materials
    • High speed steel tools cannot reliably machine steels above 45 HRC or high-temperature alloys.

What are the Ideal Applications for HSS Drills?

HSS drills are ideal for:

  • Soft materials like aluminum, brass, and other non-ferrous metals
  • Small production runs or one-off jobs where tool life is less critical
  • Shops without CNC grinding capability
  • Situations where cost and ease of regrind outweigh long-term performance

Example: Titan USA High Speed Steel Drills provide reliable performance for general-purpose machining and softer materials, offering versatility for low- to medium-volume operations.

Cobalt Drills

Advantages to Cobalt Drilling

  1. Intermediate Hardness
    • Cobalt is harder than HSS but less brittle than carbide, providing a balance of toughness and wear resistance.
  2. Higher Heat Resistance
    • Cutting temperatures up to 1,580–1,616°F (860–880°C) enable faster speeds and feeds than HSS.
  3. Moderate Cost
    • Cobalt drills offer longer tool life than HSS without the higher upfront cost of carbide.
  4. Capability for Harder Materials
    • Can machine steels up to 58 HRC, handling materials that high speed steel struggles with, while remaining more forgiving than carbide.

Cobalt Drill Disadvantages

  1. Less Wear-Resistant than Carbide
    • While cobalt drills are harder than HSS, they are still not as wear-resistant as carbide. In extremely abrasive materials, cobalt drills will wear much faster than solid carbide, which can increase tool changes and impact long-term cost in high-production runs.
  2. Slightly More Brittle than HSS
    • Cobalt is harder than HSS, making it more prone to chipping or breakage. Regrinding may require careful handling or CNC equipment to maintain geometry.
  3. Not Suitable for Extreme High-Temperature Alloys or Very Hard Materials
    • Cobalt cannot maintain performance in very hard steels or high-temperature alloys. Carbide is needed for materials above 60 HRC or extreme heat applications.

What Applications are Ideal for Cobalt Drills?

Cobalt drills work well for:

  • Medium-volume jobs with harder materials
  • Applications requiring more speed and heat tolerance than HSS
  • Shops seeking a balance of cost, tool life, and performance

Example: Titan USA Cobalt Drills are a solid choice for harder-to-machine materials that do not require carbide, providing longevity and moderate speed capabilities.

What Factors Influence What Drill Substrate to Choose?

Every drilling job is unique, and the optimal drill substrate depends on your specific requirements. Key considerations include:

  • Material Hardness
  • Production Volume and Job Size
  • Machine Rigidity
  • Budget
  • Regrinding Capabilities
  • Desired Cutting Speed and Material Removal Rate

No drill fits every job, and these factors are intended as a guide to help machinists choose the right substrate to improve efficiency, precision, and cost-effectiveness.
https://www.harveyperformance.com/wp-content/uploads/2026/02/TitanUSA-Drills-033-PM-0325-001.jpg 525 1400 Isabella Luciano http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Isabella Luciano2026-02-05 16:22:522026-02-05 16:22:56Drill Substrate Guide: HSS vs Cobalt vs Carbide

The Experts’ Guide to CNC Engraving

September 15, 2025/0 Comments/in CNC Machining, Harvey Tool, Large Featured, Machining 101, Machining Techniques, Milling, Milling, Specialty Tools, Tool Coatings, Tool Geometry, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

CNC engraving is a process that removes a small amount of material to create detailed images or shapes. Many manufacturers use this method for labeling parts or creating complex designs; however, not everyone is aware of the key techniques necessary for optimal results. When using an engraving tool, it is essential to consider several challenges that could affect both the tool and the operation.

Advantages of CNC Engraving

Compared to other engraving methods, CNC engraving is fast, consistent, and cost-effective. Thanks to their repeatability, CNC machines deliver consistent results when paired with a high-quality engraving tool. We suggest running the tool at a minimum of 6,000 RPM.

If your machine supports it, increasing the RPM can lead to even greater results. Running at lower speeds can negatively impact tool life. Choosing the right engraving tool requires considering production volume and tool engagement time. Key factors such as tip design, angle, and coating play a crucial role in maximizing efficiency and durability.

Proper Engraver Tool Selection

Most machinists understand that a square-corner end mill does not last as long as a corner-radius or ball-end mill due to its fragile cutting edge.

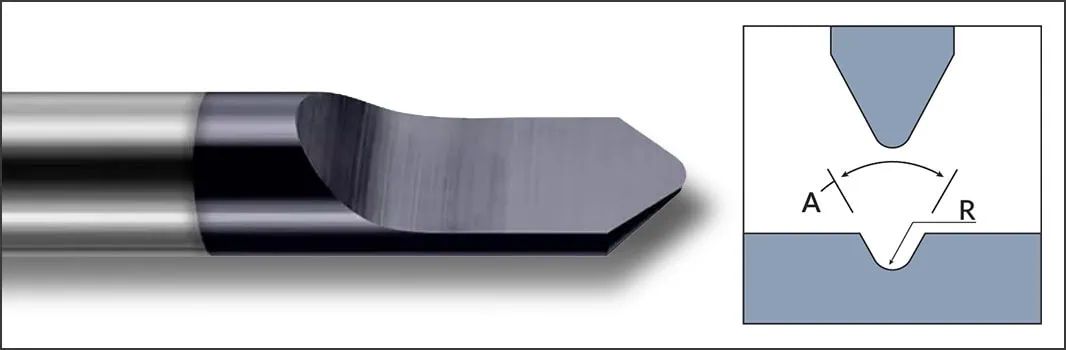
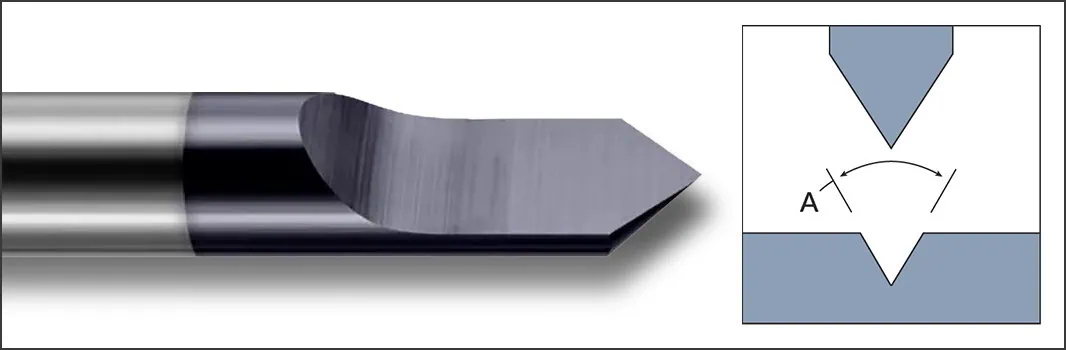
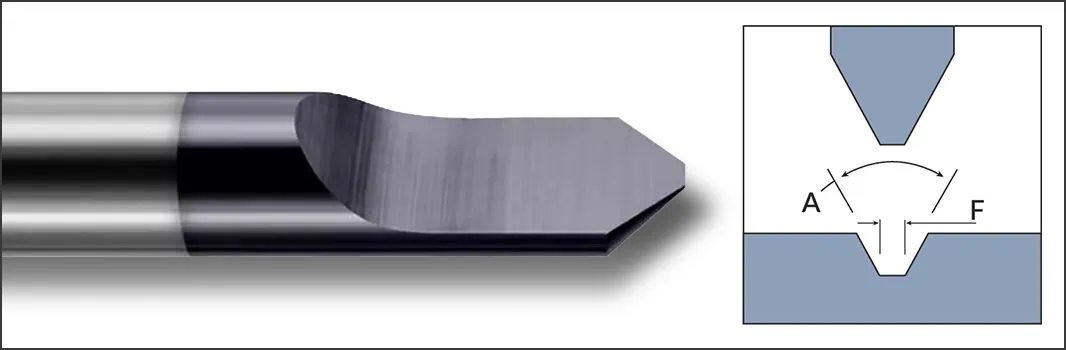
The same principle applies to CNC engraving tools. An engraver that comes to a sharp point is more fragile than one with a tipped-off or radius tip. For long production runs, consider using a tip-off or rounded tip design, as these geometries distribute cutting forces more evenly across the cutting edge, improving tool longevity. A tip-flat design will last longer than a pointed tip but not as long as a radius tip. If high-detail work is required, a pointed tip is preferable because it provides greater precision.

Pointed Tip Engraving Cutters
Tipped Off Engraving Cutters
Tip Radius Engraving Cutters

Environment and Detail Considerations

Similar to tip geometry, the engraving angle plays a critical role in visibility. The environment in which the engraving is used affects how well it can be seen. If the engraving is exposed to harsh conditions with elements like snow, mud, or dirt, debris can accumulate in the grooves, making it difficult to see and clean. A larger angle creates a wider groove, improving visibility and ease of cleaning.

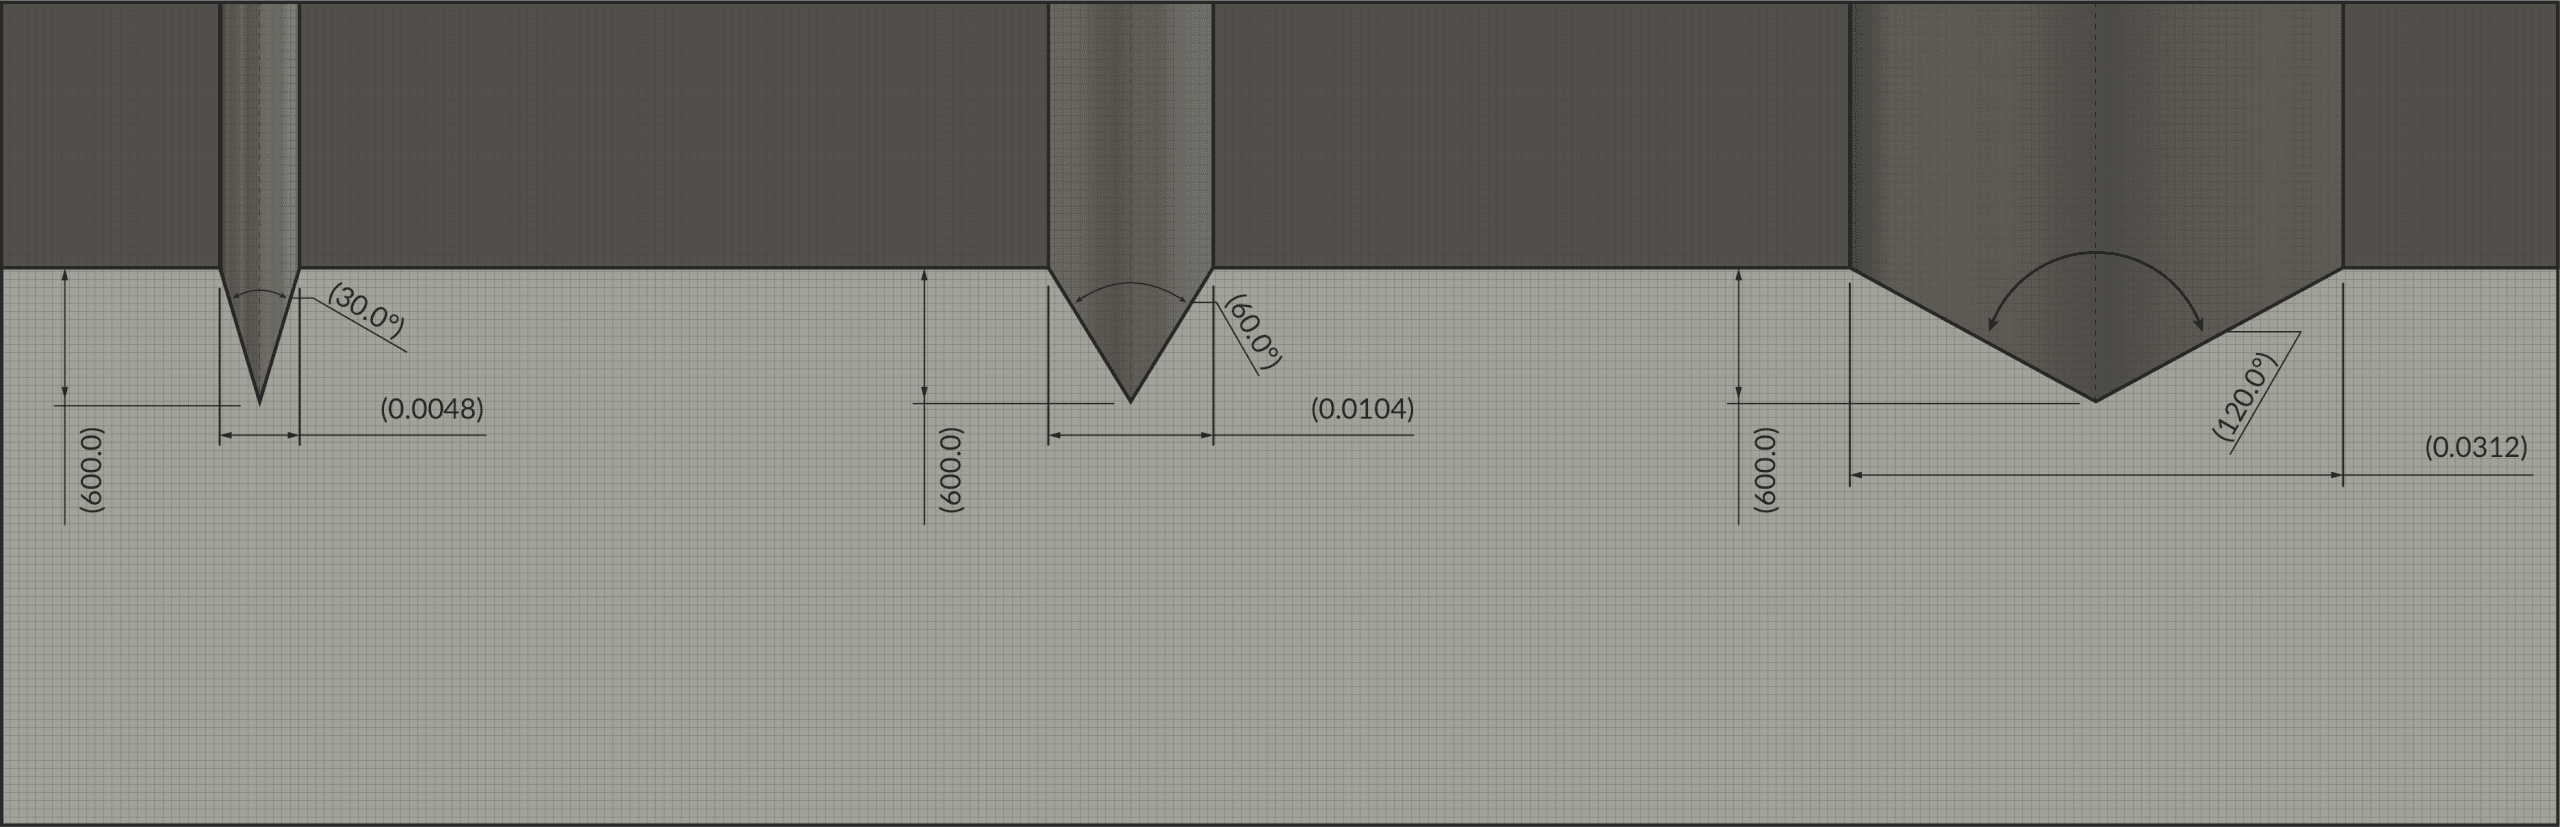
The image below illustrates three different engraving angles offered by Harvey: the leftmost groove is 30° included, the middle groove is 60° included, and the rightmost groove is 120° included. Each of these engravings is only 0.009 inches deep.

Notice that the 120° engraving is more visible at a distance due to increased surface exposure. If a job requires precision and detail, a smaller angle is preferable. While geometry significantly impacts engraving visibility and tool longevity, another key factor in tool performance is the choice of coating.

Choosing a Tool Coating

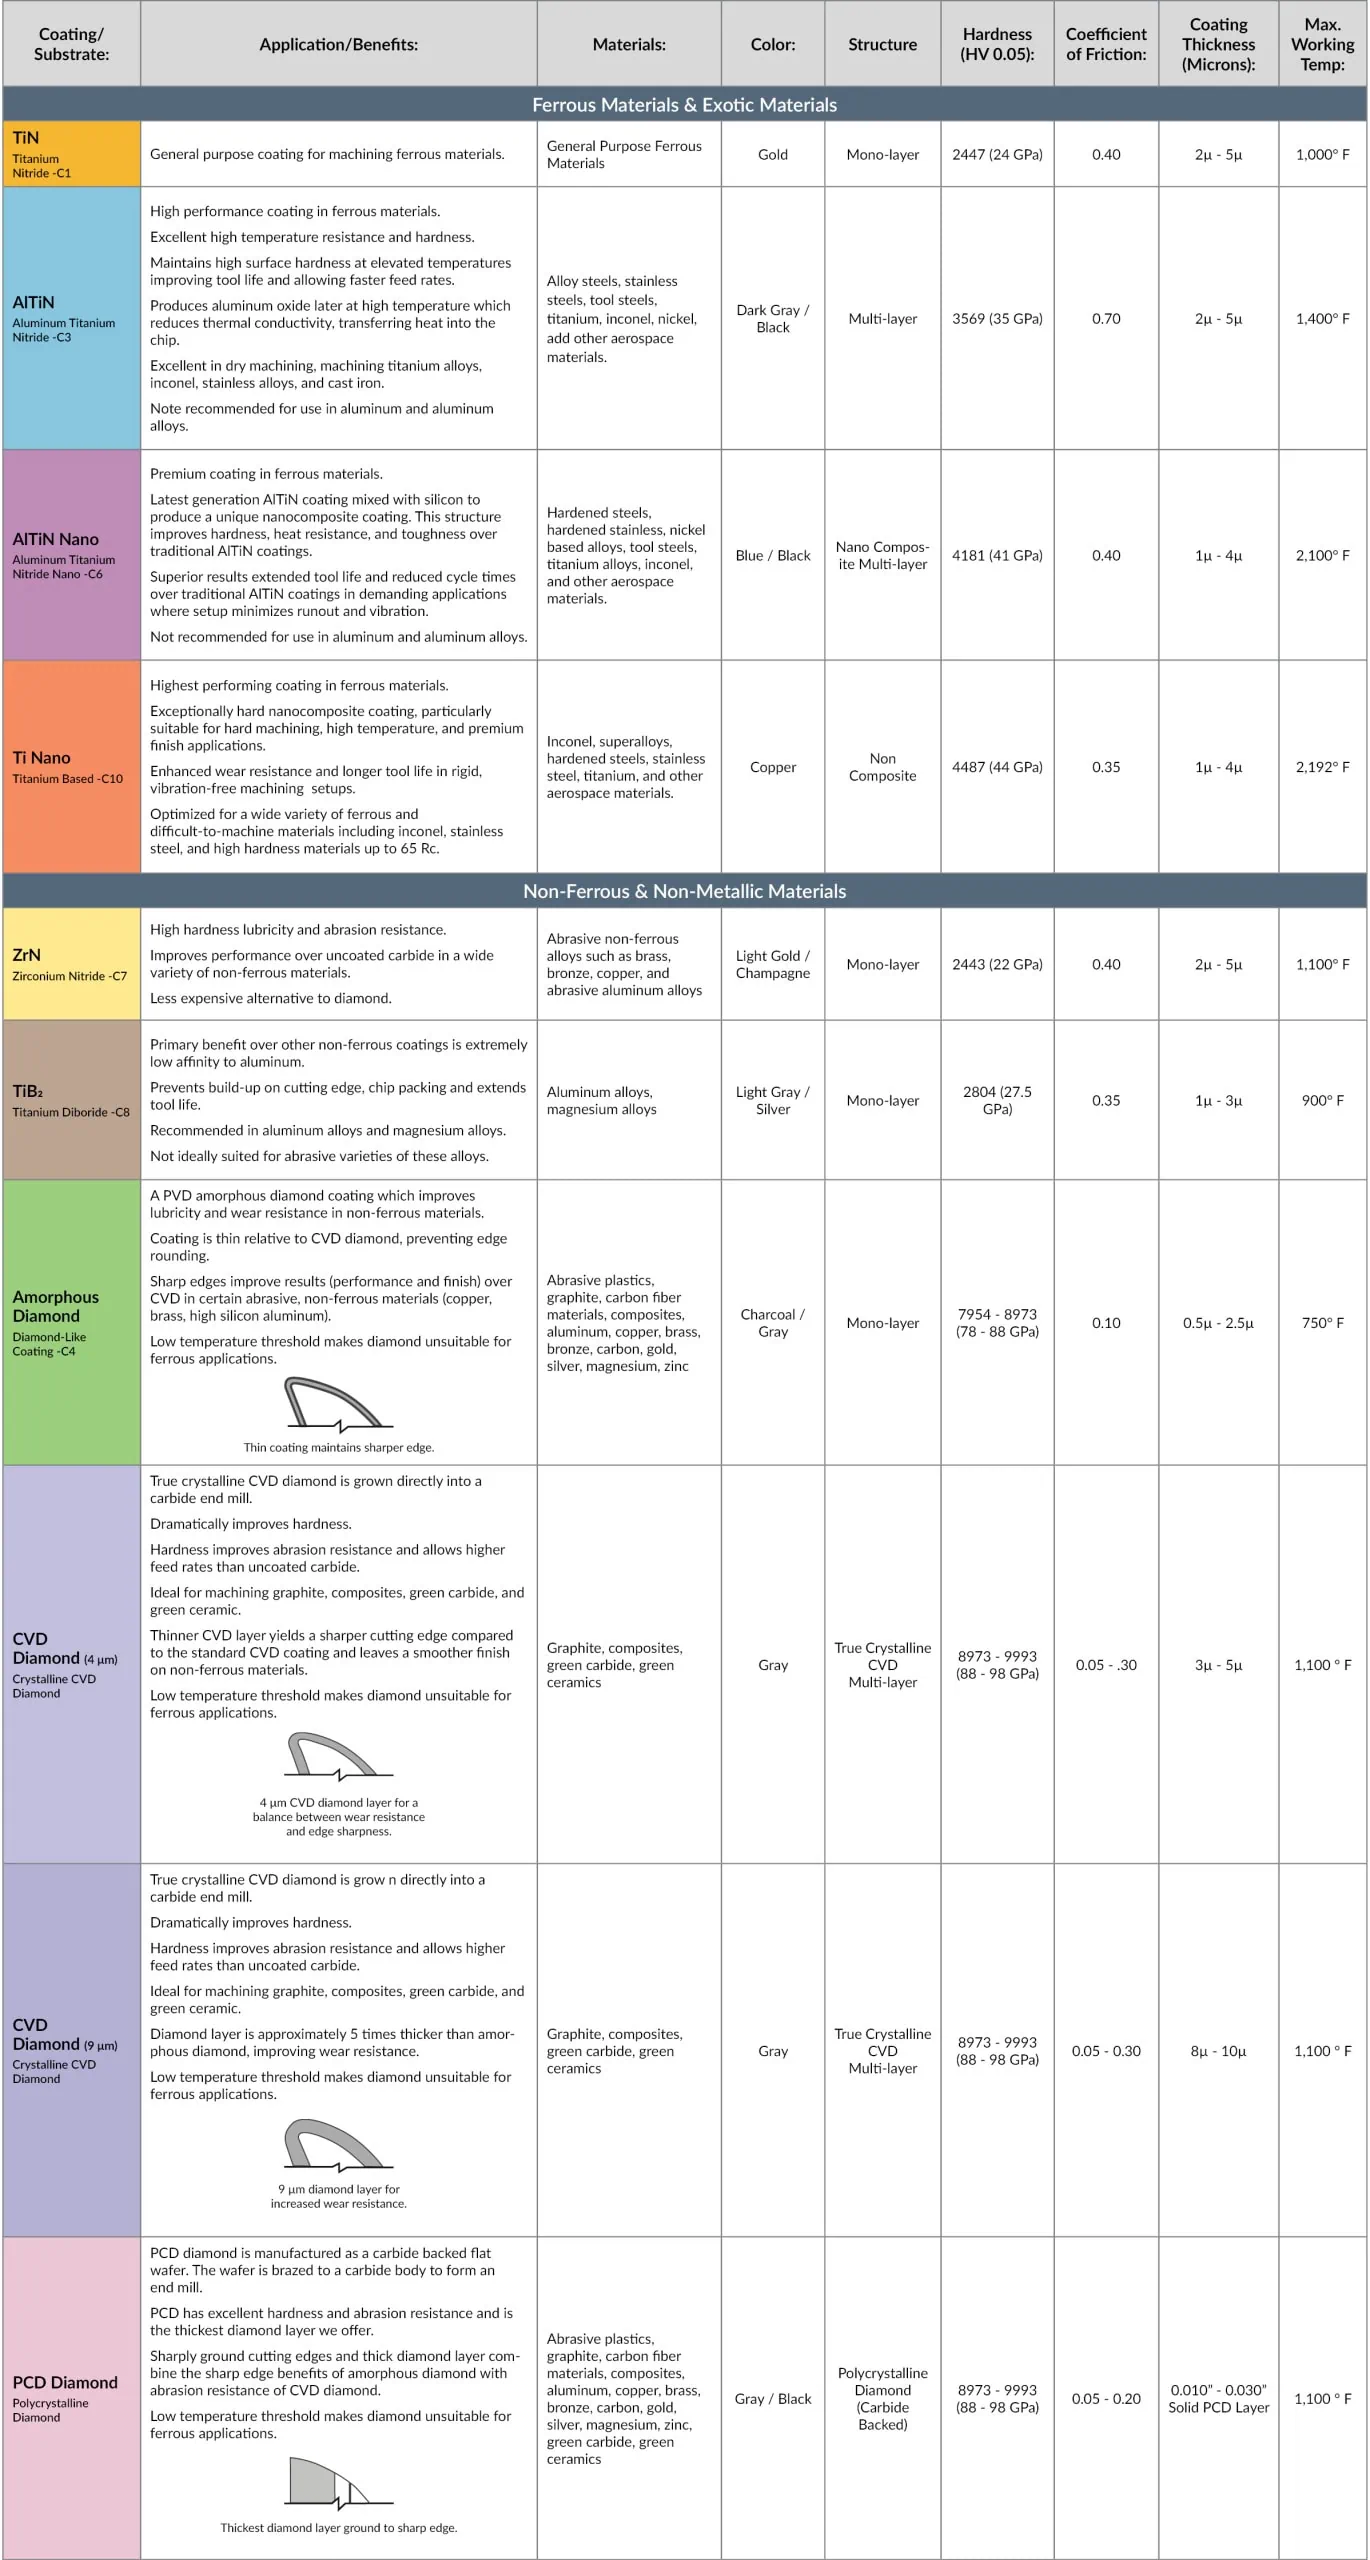
A coated engraving tool will last longer than an uncoated one because the coating provides a protective barrier between the tool and the workpiece. Additionally, coatings help reduce heat absorption, increase lubricity, and decrease tool wear. Selecting the right coating depends on the material being machined.

For example, our AlTiN and AlTiN-Nano coatings perform best in stainless steel and nickel alloys. For non-ferrous materials such as aluminum or copper, our Amorphous Diamond coating is ideal. As an alternative to our Amorphous Diamond coating, we also offer ZrN or TiB2 coatings.

A common misconception is that diamond-coated tools can be used on ferrous materials. Instead, this leads to rapid heat generation and premature tool failure.

Successfully Running Your Engraver

Selecting the correct engraving tool is just as important as understanding how to operate it properly. Even the highest-quality tool will be wasted if not used correctly. As with any machining operation, you must consider depth of cut, work holding methods, and appropriate speeds and feeds

Cutting Speeds and Feeds for Engraving 

The tip is the most delicate area of the tool which makes running at the correct speed and feed rate crucial. Running at an incorrect speed and feed rate can cause deflection, which will lead to an inaccurate engraving, chipping, breaking, or a poor surface finish.

At Harvey, we recommend a minimum spindle speed of 6,000 RPM. Operating at higher RPMs, when possible, offers even better support for tool tip integrity.

Higher speeds ensure tool stability as it will be less likely to cause vibration and reduces heat buildup during operation. Running too slowly generates excess heat and vibration leading to chipping, breakage, or having a poor surface finish. To help maintain tool tip integrity, it is important to follow the recommended depth of cut and consider the way the engraver enters the material.

Determining Depth of Cut

Many machinists are unaware that taking cuts deeper than 0.009 inches can shorten the lifespan of a Harvey engraving tool. For depth of cut ranging from 0.001 inch to 0.009 inches, you can operate within our stated speed and feed guidelines. If the operation requires a deeper groove, the chip load must be reduced accordingly. For depths between 0.010 inches and 0.015 inches, reduce the chip load by 20%. For depths ranging from 0.016 inches to 0.020 inches, reduce the chip load by 30%. Depth of cut also influences visibility. A deeper cut made with a tool that has a smaller angle can provide similar visibility to a shallower cut made with a tool that has a larger angle.

The image below illustrates different engraving depths using a 30° included angle. From left to right, the depths are 0.009 inches, 0.015 inches, and 0.020 inches. As depth increases, visibility improves. When engaging the tool with the workpiece, it is best to ramp into the material to protect the tool tip.

We recommend a ramp angle of 1° to 3° for ferrous materials such as stainless steel, and 3° to 10° for non-ferrous materials like aluminum or copper. If ramping is not an option, you may plunge the tool into the material. However, the chip load must be reduced by 50% during entry. Once the desired depth is reached, you can return to the recommended running parameters. Another key consideration is ensuring the workpiece is securely held in place.

Workholding Considerations

Runout or vibration during engraving can result in uneven cuts and tool failure. To prevent this, ensure that engraving tools are held in a sturdy toolholder and that the workpiece is secured. A shrink-fit toolholder minimizes runout and provides excellent stability. While ER collets are acceptable, they wear overtime. To verify an ER collet’s suitability, place an indicator on the tool shank and rotate the tool within the collet. The goal is to achieve the least possible runout, ideally no more than 0.0003 inches.

The workpiece should also be properly secured, either in a vise or a fixture. To detect vibrations during operation, listen for irregular noise or feel for vibrations through the CNC machine door. For cooling, coolants are recommended for metallic workpieces, while an air blast is preferable for non-metallic materials such as plastic.

Conclusion

When selecting an engraving tool, it is essential to choose the correct geometry for the operation, as well as the appropriate coating for the material being machined. Regardless of tip geometry, the engraving tool’s tip is its most fragile part. Proper speed, feed rate, and depth of cut are crucial for maximizing tool life.

For metallic workpieces, a cooling method such as coolant is necessary, while non-metallic workpieces require an air blast. Before starting a new engraving operation, double-check tool runout and ensure that the workpiece is securely held in place.

By following these best practices, CNC engraving operations can achieve high precision, longevity, and optimal tool performance.

Are You Ready to Put Your Engraving Knowledge to Use?

Browse Harvey Tool’s full selection of precision engravers, coatings, and geometries designed for optimal performance in a wide range of materials.

https://www.harveyperformance.com/wp-content/uploads/2025/09/Engraving-Tools-Featured.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-09-15 08:59:352025-09-16 09:46:49The Experts’ Guide to CNC Engraving
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top