Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Tag Archive for: Cutting Tools

ITL TV: Stop the Chatter: How End Mill Geometry Reduces Vibration

April 28, 2026/0 Comments/in In the Loupe TV/by Harvey Performance Company

Chatter at the machine is one of the most frustrating problems a machinist can face. In this episode of In The Loupe TV, Cutting Tool Counselor Don Grandt explains how modern end mill geometry tackles the problem at its source by breaking up impact frequency.

Don walks through three key design features found on high-performance end mills: variable pitch, variable helix, and progressive helix. Each one works to disrupt the harmonic patterns that cause vibration, giving you a cleaner finish, longer tool life, and more consistent cutting action.

If you’re still running symmetrical end mills for finish work, this is the episode that will change how you spec your tools.

Watch More From In The Loupe TV

https://www.harveyperformance.com/wp-content/uploads/2026/04/Thumbnail-for-WordPress.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2026-04-28 16:34:082026-06-26 09:31:41ITL TV: Stop the Chatter: How End Mill Geometry Reduces Vibration

Micro 100 Broaching Tools: Everything You Need to Know

November 20, 2025/0 Comments/in Large Featured, Micro 100, Tool Information Guides, Tool Selection, Turning/by Steven Velazquez

With the release of Micro 100’s 2025 Spring Catalog comes a new family of broaching tools, marking their debut within both the Micro 100 and Harvey Performance brands. Alongside this tooling launch are several differences in application methods and recommended running parameters.

What is Broaching?

Broaching, while performed in a lathe, is slightly different from the classic boring and grooving operations we encounter daily.

In a traditional turning operation, the workpiece rotates while the tool remains stationary. In a broaching operation, neither the workpiece nor the tool spins. Instead, the tool advances toward the workpiece and removes material in very small increments, similar to planing a block of wood.

Micro 100’s Offering

All broaches come on a Micro 100 Quick-Change shank, with sizes ranging from .1875” to .375”, depending on the broach size. These QC broaching tools are coolant-fed to promote better chip evacuation. An optional nACRo coating is available, enhancing resistance to wear and heat, which is especially useful in applications involving difficult-to-machine materials.

Keyway Broaches

Keyway broaches, as their name suggests, are used to cut keyways commonly found in power transmission applications involving gears and pulleys.

Micro 100 offers two styles of keyway broaches, available in both standard and metric sizing. This offering provides machinists with a range of sizes that are necessary to meet their application needs.

Imperial Offering

Micro 100’s standard-sized broaches come in widths of .0938”, .1250”, .1875”, and .2500”. Maximum broach depths of .500”, 1.000”, or 1.500” are available, depending on the broach width.

Metric Offering

Our metric keyway broaches are available in nominal widths from 2 mm to 6 mm. Each size is measured according to the desired fit and offered in C11, JS9, or P9 tolerance grades.

C11 reflects a “loose fit” tolerance, useful in applications where the keyway may be exposed to corrosion, dust, or other contaminants, or where deformation may occur.

JS9 represents a “normal fit”—not a press fit, but not a loose fit either. This is often required in situations where the key needs to be adjusted or shifted without much force or difficulty.

The tightest of the three offered tolerance classes is P9, which represents a “press fit.” In this case, the keyway is cut slightly smaller than the key, forcing it into the slot to create a very tight and secure connection.

Square Broaching

Micro 100 also offers square broaching tools. These broaches, like the keyway style, are pushed into the workpiece and remove material in multiple passes. They are primarily used to create the square socket found at the top of certain screws, commonly seen in machinery, construction, or other industrial applications.

Our square broaches come in metric sizes and can cut square holes ranging from 1.5 mm to 4.0 mm. When examining the geometry of these tools, you’ll notice they are cut to one corner of the square profile. Unlike keyway broaches, they must be rotated 90° when one corner is cut to create the remainder of the square form.

Although they have a fixed broach width, our square broaches are capable of cutting a range of square sizes. Take our QBRSQ-1520, for example—it features a .056” width and can cut squares from .059” to .078” (1.5 mm to 2.0 mm). When selecting a tool, it’s important to base your choice on the desired finished hole size, rather than the width of the cutter itself.

Hexagonal Broaching

The final option in Micro 100’s broaching lineup is our hexagonal broach style. These tools function similarly to the square broaches mentioned earlier, with the form created in six portions. Our hexagonal broaches can cut forms as small as .078” (2.0 mm) and up to .315” (8.0 mm). As with the square broaches, it’s important to select a tool based on the desired finish size of the hole, rather than the tooth width itself.

Hexagonal holes are often designed to work in conjunction with Allen keys. They are also commonly used for socket head cap screws. These fasteners are widely used across various industries, including automotive and construction settings.

What to do Before Making Your First Chips

Before making a cut with Micro 100’s broaching tools, there are a few important things to ensure are in place. Due to the high force involved in broaching, your machine should be equipped with a mechanical spindle lock. This lock helps achieve a higher-quality finish and, more importantly, improves feature accuracy.

The use of coolant is also strongly encouraged whenever possible, as it helps increase tool life, improve surface finish, and enhance chip evacuation. If your application requires broaching within a blind hole, be sure to create a cross hole or relief groove at the bottom of the hole to allow chips to evacuate properly.

Mastering Square & Hexagonal Broaching

To begin, the broach dimensions must be measured accurately and programmed into the machine. Ensure the tool is positioned at the 12 o’clock location to allow proper chip evacuation.

If cutting a hexagonal profile, the pre-drill should be approximately 1.035 times the desired feature size (1.1× for a square profile).

Before the first pass is made, visually check the tool path by positioning the tool at the starting point of the stroke, and program a stop there to verify correct alignment.

After each pass, ensure the tool is radially clear of the groove before fully retracting it. On the final return stroke, completely remove the broach from the hole. Finally, rotate the workpiece by 60 degrees—90 degrees for a square profile—and repeat the cutting process for the remaining corners.

Best Practices for Keyway Broaching

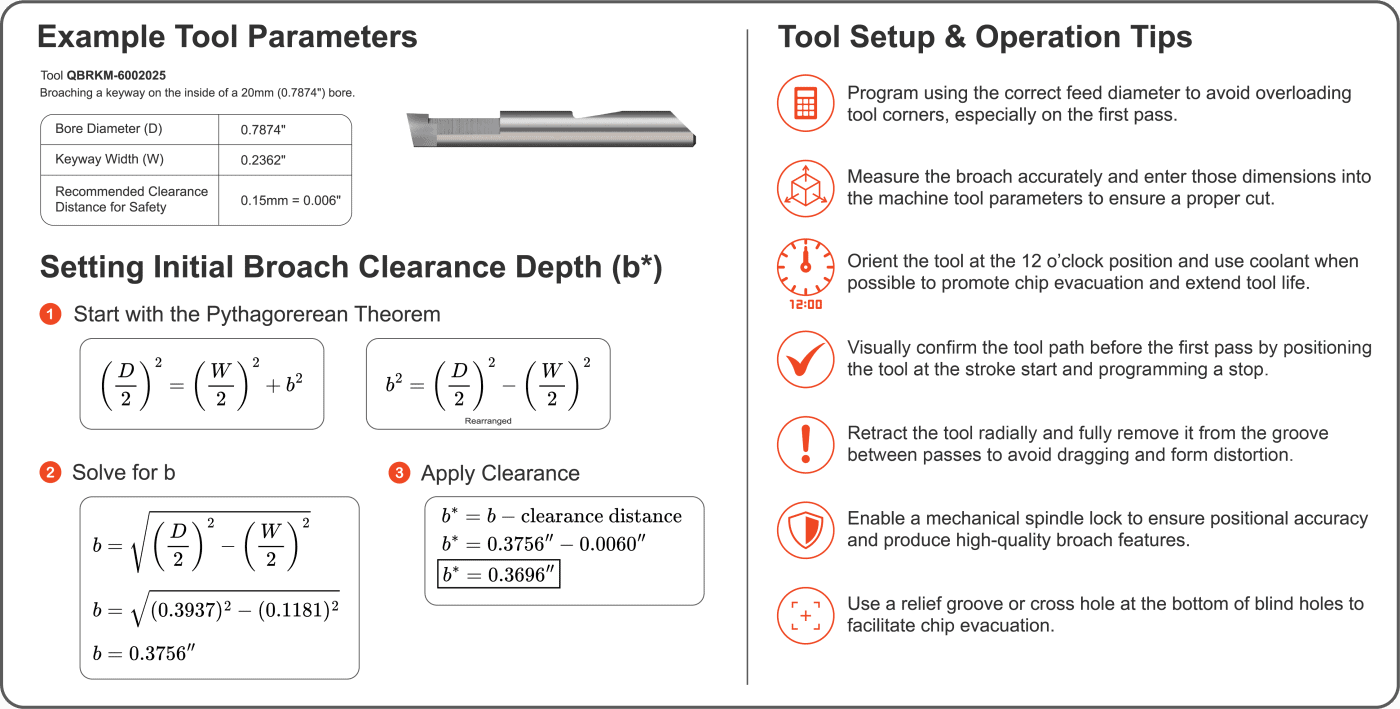
Keyway broaches require an additional calculation to determine the correct starting position for the first pass. An example calculation is provided below.

After the initial pass is completed, continue cutting normally until the desired keyway size is met. As with square and hex broaching, ensure the tool is radially clear of the groove after each pass before retracting. On the final return stroke, completely remove the broach from the hole.

In Summary

Micro 100s offering of broaching tools is fit for a large variety of broaching applications you may come across. Whether square, standard, or hexagonal, metric or imperial, Micro 100 has the tools to help you cut every step of the way.

To see the full range of tooling that Micro 100 has to offer, please visit our website micro100.com.

For any further questions regarding our broaching tools or Micro 100 as a whole, please don’t hesitate to call us at +1 844-393-8665 or email us at [email protected].

https://www.harveyperformance.com/wp-content/uploads/2025/11/Broaching-Featured-Image-Rev-01.jpg 525 1400 Steven Velazquez http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Steven Velazquez2025-11-20 11:30:002025-12-03 14:09:16Micro 100 Broaching Tools: Everything You Need to Know

Supporting Precision in Mold, Tool & Die Applications

July 15, 2025/0 Comments/in Large Featured, Milling, Specialty Tools, Tool Selection/by Harvey Performance Company

Mold, Tool, and Die manufacturing demands a high level of precision. Whether you’re machining hardened tool steels, creating detailed mold cavities, or producing dies with complex geometries, the tooling used plays a critical role in ensuring consistent, repeatable results. To explore the full selection of tools relevant to this industry, including application-specific geometries and coatings, visit Harvey Tool’s Mold, Tool & Die Featured Solutions page.

Harvey Tool offers a comprehensive range of tools specifically engineered to meet the unique challenges of the Mold, Tool & Die industry. From tools designed to reach deep cavities to those that maintain surface finish in demanding materials, this offering is built to support precision and reliability throughout the machining process.

Tools included in this lineup are:

  • CVD Diamond End Mills– This Harvey Tool lineup of Diamond Tooling for Non-Ferrous Materials features true crystalline CVD diamond on a solid carbide substrate, making it ideal for machining graphite, composites, green carbide, and green ceramics.
  • End Mills for Hardened Steels– Engineered for hardened steels from 46Rc to 68Rc, this tool includes the latest generation AlTiN Nano coating for enhanced hardness and thermal resistance.

  • End Mills for Aluminum Alloys– We know a part is only as successful as its finish. That’s why our aluminum finishing solutions are crafted for mirror-like surface quality.   

  • End Mills for Medium Alloy Steels– Engineered for versatility, these CNC-ground, AlTiN-coated tools excel in machining stainless, tool, and medium alloy steels.
  • Miniature Tapered End Mills– Tackling deep part features? Harvey Tool’s tapered Miniature End Mills offer unique geometries that take the challenge out of tough-to-reach cuts.

Diamond End Mills for Abrasive and Non-Ferrous Materials

Diamond tooling is essential to many moldmaking processes, particularly during electrode production and when machining non-metallic materials. Harvey Tool’s offering includes a wide selection of Diamond End Mills designed for use in abrasive and non-ferrous materials such as graphite, green carbide, green ceramics, and composites—materials commonly encountered in mold and die work.

These tools feature a CVD (Chemical Vapor Deposition) coating to promote longer tool life and uphold tight tolerances over extended machining cycles.

Highlighted tooling includes:

  • Finishers – Ball Profile (CVD Diamond)
    With available radii as small as 0.005″, these tools are ideal for finishing high-detail electrodes and intricate features.
  • Finishers – Corner Radius (CVD Diamond)
    Designed for applications requiring edge strength and tight tolerances, available with corner radii from 0.005″ to 0.0625″.
  • Standard Ball and Square Profiles (CVD Diamond)
    Feature reduced neck geometries for improved clearance in deep cavity or long-reach work.

Diamond End Mills are frequently used in electrode machining for EDM (Electrical Discharge Machining), where precision in non-metallic workpieces directly influences final mold quality.

All tools in the Mold, Tool & Die offering are fully stocked and available to ship same day, helping to reduce lead times and keep your production on schedule.

To view the full offering, including tools with specialized geometries and coatings, visit the Mold, Tool & Die Solutions page.

https://www.harveyperformance.com/wp-content/uploads/2025/07/Mold-Tool-Die-Featued-Image.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-07-15 08:02:462025-11-10 10:42:08Supporting Precision in Mold, Tool & Die Applications

The Benefits of Combined Drill & Countersinks

April 4, 2025/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Tom Delaney

Two of the most frequently recurring operations across a variety of applications are CNC drilling and countersinking. Since these two processes are often interdependent, managing space in the tool crib and time lost on tool changes can become cumbersome when using dedicated tools for each operation. Using combined drill and countersinks eliminates these concerns and has become a go-to tool across machine shops.  

valor holemaking combined drill and countersink tools on a table with a slide caliper and ruler
Variety of Combined Drill & Countersinks

What is a Combination Drill & Countersink Tool?

A Combined Drill & Countersink is a specialized tool designed to perform two critical operations in one step: drilling a hole and creating a countersink. These tools are typically short and rigid, ideal for producing either a shallow conic or a center hole. Their double-ended design minimizes downtime by enabling quick transitions between tasks.

Valor Holemaking’s Combined Drill & Countersink

Key Features of Combined Drill & Countersinks

They feature a smaller drilling pilot and larger diameter countersink. The drill pilot resembles a spot drill, making it useful for predrilling applications. The stub length of the drill mitigates deflection and ensures accurate location of a hole’s center. When preparing a spot hole for a longer drill, it prevents walking or wobbling off-center. 

Common Applications for Combined Drill & Countersinks

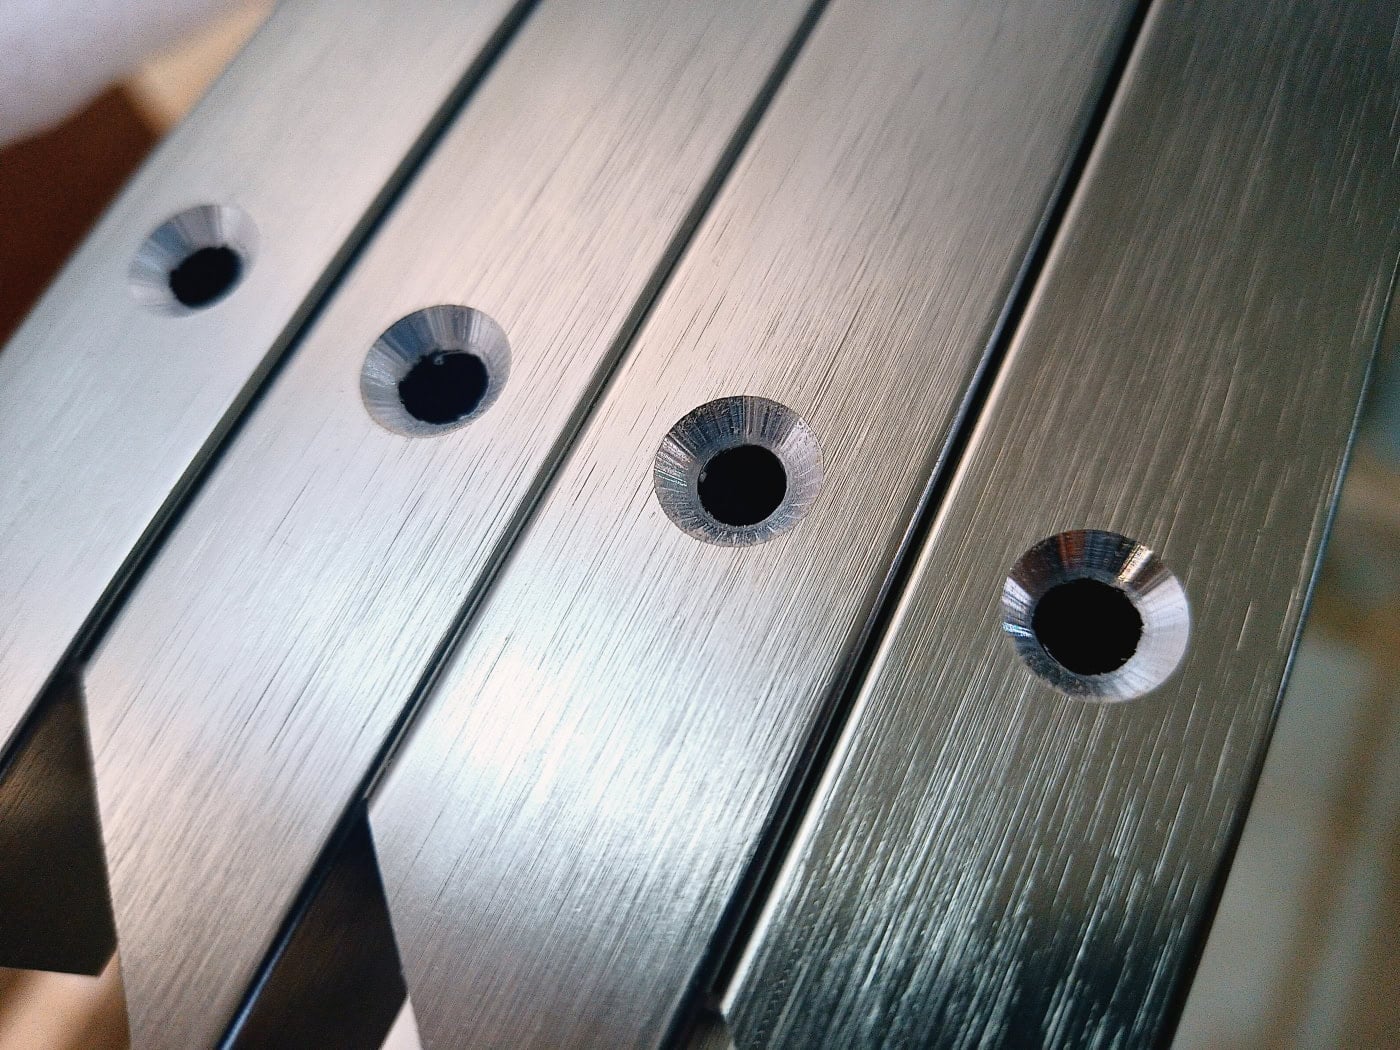
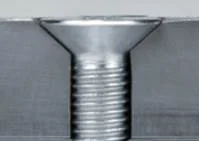
Many holemaking applications begin with spotting and end with countersinking, making combination multi-functional tools cost-effective and time efficient. As the tool drills into the material, the larger countersink diameter chamfers the top edges, allowing fasteners to sit flush with the surface.

Where and How to Use a Combined Drill & Countersink

The primary use of a combined drill and countersink is to create center holes in materials that will be turned between two centers. These centers help accurately position a workpiece along its axis between a lathe chuck and tailstock. Live centers are used in applications requiring a high level of concentricity and support. They typically feature a 60° included angle, which is the angle most combined drills and countersinks are manufactured with. For this reason, combined drill and countersinks are often referred to as center drills.

Combined drill and countersinks are also essential in any application where screws need to sit flush in the workpiece. Holes need to be drilled and countersunk across all industries. Flush-mounted fasteners are required in applications such as aircraft panels and structural components, automotive engine components, boat hulls and marine components, electronic device housings, and covers of all types.

Example of countersunk hole

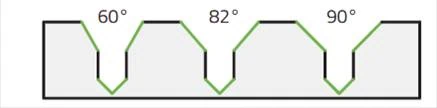
Types of Combination Drill/sinks: 60°, 82°, and 90° Angles

Harvey Tool and Valor Holemaking offer combined drill and countersinks in 60°, 82°, and 90° included angles. While 60° tools are most commonly used for center drilling, 82° and 90° included angles are designed to match the angles of the most popular flat and oval head screws. These tools allow users to create countersunk fastener holes in a single step.

Important Tips for Running Combination Drills

When running a combined drill-and-countersink, it is important to ensure that chiploads (IPR) are based on the drill diameter. Since the drill diameter is always smaller than the chamfer area, it is safer to use parameters designed for the drill portion of the tool rather than calculating an effective cutter diameter for the chamfer.

Valor Holemaking Combined Drill & Countersink in the Spindle

Why These Tools Are Essential in Machining

Combined drill & countersinks are cost-effective and efficient tools to have in your arsenal. Whether you’re preparing a workpiece for turning between centers, spot drilling, or creating countersunk holes for fasteners, these reliable tools complete the job quickly and effectively.

https://www.harveyperformance.com/wp-content/uploads/2025/04/Benefits-of-Combined-Countersink-Featured-Image.jpg 525 1400 Tom Delaney http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Tom Delaney2025-04-04 11:38:162025-11-10 12:55:06The Benefits of Combined Drill & Countersinks

A Closer Look at Helical Solutions’ Tapered End Mills

January 29, 2025/0 Comments/in CNC Machining, Helical Solutions, Machining 101, Machining Techniques, Milling, Specialty Tools, Tool Geometry, Tool Information Guides, Tool Selection/by Thomas Donahue

Helical Solutions offers a variety of Tapered End Mills designed to enhance performance and efficiency in tapered wall applications. In this blog post, we’ll dive into the geometry of tapered end mills and explore their common applications to understand when they could be utilized to optimize your CNC machining application.

Tapered End Mill Geometry

Tapered End Mills bring many advantages to machining compared to standard end mills, but what is a Tapered End Mill? A standard end mill will have the same cutting diameter throughout the whole length of cut, whereas a taper mills starts at the shank or neck at a larger diameter and tapers down at a specific angle.

The angle of the taper can vary, but Helical Solutions’ tools feature angles ranging from .05° to 5°, which allows for a broad spectrum of cutting operations. A tapered length of cut or tapered neck can also provide increased strength and rigidity, compared to that of a standard end mill. Having a tapered length of cut makes it easier to create flat tapered walls on 3-axis machines and leads to a better finish.

Tapered End Mill

Standard End Mill

Common Taper Mill Applications

Tapered End Mills are used in any machining process that requires an angled surface. These tools are engineered for light profiling and finishing applications in mold and die pockets and other tapered wall applications.

Mold & Die Applications

Mold and die applications are a mass production manufacturing method that consists of shaping different types of metals and other materials. Molds are used to shape metals, allowing them to become solid in the mold, while dies use a mechanical force to cut the material into the desired shape.

A couple examples of mold and die applications are plastic bottles, car body parts, electronic components, cutlery, coins, and metal stamping parts.

Mold Tool & Die Example

Tapered End Mills Profiles

Taper mills are great for profiling with the ball nose version, and for light finishing and creating required draft angles with the square version. Which style is right for you?

Ball Nose Taper Mills

Ball Nose Tapered End Mills are great for profiling because the full radius at the bottom eliminates sharp edges, which leads to a smoother process.

Square Profile Tooling

The square version of the tapered end mill has a higher flute count and helix angle with a sharp cutting edge. This is better for light finishes on the walls of tools.

The draft angle determined in the design process is the amount of mold design can be tapered. A draft angle is a strategic angle or slope designed in the mold. The tapered angle in the tool allows for the draft angle to be formed easier compared to a straight shanked end mill. Having a draft angle in the mold allows for easier removal of the part so it does not get stuck to the mold.

Helical Solutions’ Tapered End Mills

Helical Solutions’ offering of Tapered End Mills feature a tapered profile design, variable pitch geometry for reduced harmonics and increased feed rates, and Aplus coating for increased performance in Cast Iron, Steel, and even Stainless Steel. These tools are offered in a 4 Flute Ball style, and a 5 Flute Square style, so you can select the end profile that best suits your specific toolpath.

Helical’s Tapered End Mills

4 Flute Ball (HTPR-4)

Helical’s 4 Flute Ball Tapered End Mills (HTPR-4) are fully stocked in 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a ball nose profile, allowing them to excel in a variety of different applications from 3D contouring and profiling to slotting. A Ball Nose End Mill has a full form radius, allowing machinists to utilize the entire radius when contouring and finishing a 3D surface.

5 Flute Square (HPTR-5)

Helical’s 5 Flute Square Tapered End Mills (HTPR-5) is also is also fully stocked 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a square profile for more precise finishing and the 5 flute design creates a larger core, allowing for better tool strength in roughing applications.

Taper Mill Tooling Wrapped-up

By understanding the unique features and advantages of this tooling, machinists can make informed decisions and achieve superior results in their projects. These feature unique geometry that enhances machining capabilities and ensures reliability and accuracy across a range of tapered wall applications.

https://www.harveyperformance.com/wp-content/uploads/2025/01/DSC_0434.jpg 525 1400 Thomas Donahue http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Thomas Donahue2025-01-29 15:55:382025-01-30 09:14:54A Closer Look at Helical Solutions’ Tapered End Mills

Harvey Performance Company – CNC Cutting Tool Survey 

January 6, 2025/0 Comments/in No Index/by Harvey Performance Company

To thank survey respondents for completing this survey, we will randomly select 1 winner each day on the following days: 

Week 1: Monday, January 5th through Friday January 9th 2026 (5 winners).

All survey submissions will be entered for a chance to win one of five $250 Digital Visa Gift Cards. Winners will be selected at random at approximately 4:45 PM EST on the dates specified above and will be announced on the official Harvey Performance Company social media channels, including LinkedIn, Instagram, and Facebook. Winners will also be notified via email or phone. Please note that an email address is required to facilitate the delivery of the digital gift card. 

At Harvey Performance Company, we are committed to delivering exceptional products and services, and your perspectives play a pivotal role in shaping our future endeavors. This survey has been crafted with the intention of understanding how our brands are currently serving you, our valued customers. 

How to Participate 

To enter the giveaway, simply complete the survey. Please note that providing your email address is required to facilitate prize delivery should you be selected as a winner. 

Official Contest Rules 

Contest Dates: 

The contest will run from Monday, January 5th, 2026, to Friday, January 9th, 2026. Entries that are submitted before or after the contest period will not be considered for the giveaway. 

Prizes: 
All completed submissions will be considered for one of the five $250 Digital Visa Gift Card prizes.
Winners will be selected at random at approximately 4:45 PM EST on the dates specified above and will be announced on the official Harvey Performance Company social media channels, including LinkedIn, Instagram, and Facebook. Winners will also be notified via email or phone. Please note that an email address is required to facilitate the delivery of the digital gift card. 

Full Details: 
NO PURCHASE IS NECESSARY TO ENTER OR WIN. MAKING A PURCHASE WILL NOT INCREASE YOUR CHANCES OF WINNING. ENTRY INTO THIS GIVEWAY CONSTITUTES THE ACCEPTANCE OF THESE OFFICIAL RULES. VOID WHERE PROHIBITED BY LAW. 

By participating in the Harvey Performance CNC Cutting Tooling Survey, you agree to these official rules (the “Rules”), which are a contract, so read them carefully before participating. Without limitation, this contract includes indemnities to the Released Parties (defined below) from you and a limitation of your rights and remedies. You must follow these Rules to enter and be eligible to receive a prize in connection with the survey giveaway. 

DURATION:  Begins on Monday January 5th, 2026, at 8:00 AM EST and ends January 9th, 2026, at 5:15 PM EST (“Survey Period”).  The computer clock of Harvey Performance Company, LLC (“Sponsor”) is the official time-keeping device for the survey giveaway. 

ELIGIBILITY: The survey giveaway is open only to legal permanent residents of the United States (excluding Puerto Rico, and the U.S. Territories and Possessions) who are 21 years of age or older as of the date of entry. Employees, officers, and directors of Sponsor along with its affiliates, subsidiaries, advertising, contest, fulfillment, and marketing agencies, (collectively, “Promotion Parties”) their immediate families (parent, child, sibling & spouse, and their respective spouses, regardless of where they reside) and persons living in the same households as such individuals (whether related or not) are not eligible to participate in survey giveaway. By participating, you agree to these Rules and to the decisions of the Sponsor, which are final and binding in all respects.  In addition, to be eligible to win: (i) consent to the use of your rights of publicity, (ii) assume all tax liabilities, (iii) waive all claims against Sponsor and Promotion Parties, and (iv) consent to the publication of your full first name, last name initial, and/or the city and state in which you work or live (v) confirm your eligibility (collectively “Affidavits and Waivers”). This survey giveaway is void in any jurisdiction not listed above and where prohibited by law, rule, or regulation. 

HOW TO ENTER: Follow the directions and complete the survey and submission form at the end of the survey.  

An email address is required to be entered to win, however we may call you if your name is selected. Otherwise, you will not be contacted regarding the outcome. 

PRIVACY POLICY:  Information collected in connection with this Sweepstakes will be used in accordance with Sponsor’s Official Privacy Policy (available at https://www.harveyperformance.com/privacy-policy/ and these Rules. In the event of any discrepancy between Sponsor’s Privacy Policy and these Rules, Sponsor’s Privacy Policy shall control and govern. 

LIMITATIONS: The maximum number of entries allowed during the Sweepstakes is 1 per person. 

Sponsor is not responsible for any entry that is lost, late, misdirected or undeliverable, whether due to system errors, omissions, interruption, deletions, defects, delay in operations or transmissions, theft or destruction or failures, faulty transmissions or other telecommunications malfunctions, entries not received resulting from any hardware or software failures of any kind, lost or unavailable network connections, failed, incomplete or garbled computer or telephone transmissions, typographical or system errors and failures, faulty trans-missions, technical malfunctions, or otherwise. 

In the event of a dispute regarding the identity of the person submitting an entry, the entry will be deemed submitted by the authorized account holder at the time of entry. The authorized account holder is the natural person who is assigned to the account by Sponsor, the organization that is responsible for assigning accounts to customers. Potential winners may be required to show proof of being the authorized account holder. 

Any attempt by an entrant to obtain more than the stated number of entries by using multiple/different email addresses, identities, registrations, logins, and/ or any other methods, including, but not limited to, automated entry, will void that entrant’s entries and that entrant may be disqualified from the Sweepstakes. Multiple participants are not permitted to share the same email  

Sponsor will not verify receipt of entries for entrants. All entries submitted become the sole property of Sponsor. Sponsor reserves the right to disqualify those entries deemed to be inappropriate or in violation of this survey giveaway (as defined solely by Sponsor). 

Entries are void if they are incomplete, irregular, or submitted improperly. Personal information (if any) collected through the Entry Form will be used only for purposes of (i) selecting and contacting the winners, and (ii) as identified in the Privacy Policy. 

ODDS OF WINNING: The actual odds of winning will depend upon the actual number of total entries received for this survey giveaway, regardless of the means of entry. 

LIABILITY LIMITATION:  The Sponsor assumes no responsibility or liability for (a) lost, late, stolen, undelivered, inaccurate, incomplete, delayed, misdirected, damaged or garbled registrations, entries, URLs, or emails; (b) any incorrect or inaccurate entry information, or for any faulty or failed electronic data transmissions; (c) any unauthorized access to, or theft, destruction or alteration of entries or registrations at any point in the operation of this survey giveaway; (d) any technical malfunction, failure, error, omission, interruption, deletion, defect, delay in operation or communications line failure, regardless of cause, with regard to any equipment, systems, networks, lines, cable, satellites, servers, computers or providers utilized in any aspect of the operation of the survey giveaway; (e) inaccessibility or unavailability of the Internet or the Sponsor’s web site or any combination thereof or for computer hardware or software malfunctions, failures or difficulties, or other errors or difficulties of any kind whether human, mechanical, electronic, computer, network, typographical, printing or otherwise relating to or in connection with the survey giveaway, including, without limitation, errors or difficulties which may occur in connection with the administration of the survey giveaway, the processing of Entries, social networking posts, or registrations, the announcement of the prizes, or in any other  survey giveaway related materials; or (f) any injury or damage to participants or to any other person’s computer which may be related to or resulting from any attempt to participate in the survey giveaway. If, for any reason, the survey giveaway (or any part thereof) is not capable of running as planned for reasons which may include, without limitation, infection by computer virus, tampering, unauthorized intervention, fraud, technical failures, or any other causes which may corrupt or affect the administration, security, fairness, integrity or proper conduct of this survey giveaway, then the Sponsor reserve the right at their sole discretion to cancel, terminate, modify or suspend the survey giveaway in whole or in part. If terminated, the Sponsor will award the prizes from among all non-suspect, eligible Entries received for the survey giveaway up to the time of such action. 

RELEASES: All participants, as a condition of participation in this survey giveaway, agree to release, hold harmless and indemnify the Sponsor, its offers, directors, accountants, attorneys, and agents (“Released Parties”) from and against any and all liability, claims, damages, or actions of any kind whatsoever for injuries, damages, or losses to persons or property which may be sustained, in whole or in part, directly or indirectly, in connection with (i) participation in any aspect of the survey giveaway, (ii) the receipt, ownership or use of the prize awarded, including any travel associated with any prize, (iii) participant’s registration material on any related website, or (iv) any typographical or other error in these Rules.   

NO WARRANTIES: NEITHER SPONSOR NOR ANY OF THE RELEASED PARTIES HAVE MADE OR MAKE OR ARE RESPONSIBLE OR LIABLE FOR ANY WARRANTY, REPRESENTATION OR GUARANTEE, EXPRESS OR IMPLIED, RELATIVE TO THISSURVEY GIVEAWAY OR A PRIZE, INCLUDING BUT NOT LIMITED TO, ITS QUALITY OR FITNESS OR MERCHANTABILITY, AND ALL PRIZES ARE TENDERED TO ENTRANTS ON AN “AS IS” BASIS.  THERE ARE NO WARRANTIES REGARDING ANY PRIZE OR THE USE OF THE GIFT CARD. 

RANDOM DRAWING: Five (5) prize winner(s) will be randomly selected for the Survey giveaway to receive a $250 Digital Visa gift card. All decisions on all matters pertaining to the survey giveaway are final. The sponsor reserves the right to substitute a prize of equal or greater value. 

WINNER NOTIFICATION: Random selection of the potential prize winner will occur every day during the first two weeks of the survey giveaway Period from among all eligible entries received. Prize drawing will be conducted at Sponsor’s headquarters. The prize winner will be notified by e-mail and/or phone, in Sponsor’s discretion, within 5 days from the date of the winner selection. The winner will also be announced on the Harvey Performance Companies individual Social Media channels (LinkedIn, Instagram and Facebook). 

The designated prize winner will have 5 days from notification to claim the prize. Sponsor and its affiliates, subsidiaries, employees, agents, officers and directors, advertising and promotion agencies, and their respective officers, directors, employees, and their respective agents, will not be liable for unsuccessful efforts to notify a winner. 

The prize will be delivered via e-mail. No prize transfer, assignment or substitution by winner permitted. All federal, state and local taxes, fees and surcharges on prizes are the sole responsibility of the prize winner. If the prize winner declines the prize, fails to claim the prize, is unavailable for prize fulfillment, fails to abide by these Rules, or is ineligible, Sponsor may select an alternate winner from all remaining eligible entries. 

By entering this survey giveaway, each entrant gives his/her express permission to be contacted by the Sponsor by telephone, e-mail and/or postal mail for survey giveaway purposes. 

The winner, by acceptance of Prize, grants to Sponsor, and each of its respective designees, the right to publicize the winner’s name, address (city and state of residence), photograph, voice, statements and/or other likeness and prize information for advertising, promotional, trade and/or any other purpose in any media or format now known or hereafter devised, throughout the world, in perpetuity, without limitation and without further compensation, consideration, permission or notification, unless prohibited by law. 

THIRD PARTY & SOCIAL MEDIA:  This Sweepstakes is in no way sponsored by, endorsed by, associated with, or administered by Facebook, Instagram, Twitter, WhatsApp, Tumblr, Google, YouTube, WeChat, or WhatsApp (collectively “Social Media Sites”).  By entering this event, you agree to hold all Social Media Sites harmless for and from any potential claims you may have related to or arising out of this Sweepstakes. 

MISCELLANEOUS CONDITIONS: Sponsor reserves the right at its sole discretion to cancel, terminate, modify, or suspend the survey giveaway. 

Sponsor assumes no responsibility for any error, omission, interruption, deletion, defect, or delay in operation or transmission; communications line failure; theft or destruction of or unauthorized access to survey giveaway entries or entry forms; or alteration of entries or entry forms. Sponsor reserves the right to correct clerical or typographical errors in promotional materials or any materials related to the survey giveaway.  

WINNER NAME: To obtain the name of the winner, send a request to [email protected]  

CHOICE OF LAW AND JURISDICTION: This survey giveaway is governed by the internal substantive laws of Nevada, without regard to its conflicts of law provisions. 

https://www.harveyperformance.com/wp-content/uploads/2023/11/Helical-7-Flute-Square-Endmill-001-Gorham-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2025-01-06 14:20:242025-12-03 08:30:58Harvey Performance Company – CNC Cutting Tool Survey 

Mastering Precision: Pilot Drills in CNC Machining

December 10, 2024/4 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Getting Started, Holemaking, Large Featured, Machining 101, Machining Techniques, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Emily Van Volkom

When it comes to achieving precision in CNC drilling applications, the choice of tools and techniques can make a significant difference in the outcome. One essential element that often doesn’t get the spotlight it deserves is the Pilot Drill. This blog post will explore the importance of pilot drills, their applications, and best practices for integrating them into your CNC machining processes.

What is a Pilot Drill?

A pilot drill is used to create a guide hole in deep drilling applications where precision is required. This guide hole keeps the drill on center, maintaining straightness throughout the cut. By creating a pilot hole, machinists can also improve the quality of the finished product and extend the life of their tools.

The Importance of Pilot Drills in CNC Machining

1. Enhanced Accuracy

The primary advantage of using a pilot drill is the enhanced accuracy it provides. When working with harder materials or complex geometries, a small pilot hole helps maintain the alignment of the longer drill, reducing the risk of misalignment and defects.

2. Extended Tool Life

Using a pilot drill can significantly extend the life of your deep-hole drilling tools. By first creating a pilot hole, the chasing drill experiences less stress, reducing wear and tear, and the chance of breakage, ultimately leading to cost savings from longer tool life.

3. Improved Chip Removal

Pilot drilling can enhance chip removal, particularly in deep-hole drilling scenarios. The smaller pilot hole allows for better coolant flow, which is crucial for effective chip evacuation and maintaining optimal cutting temperatures.

Applications of Pilot Drills

Pilot drills are versatile and can be used in various applications, including:

  1. Deep-hole Drilling: Pilot holes create a guide when drilling deep holes for improved centering and straightness.
  2. Tapping Operations: A pilot hole can facilitate easier and more accurate tapping.
  3. Reaming: When preparing for reaming operations, a pilot drill can ensure the hole is properly aligned and sized.
  4. Screw and Bolt Holes: Pilot holes are essential for ensuring screws and bolts are inserted correctly and securely.

Best Practices for Using Pilot Drills

1. Application      

Piloting is recommended for tighter tolerance holes when drilling at depths of 8xD or greater. Valor Holemaking provides a custom tolerance of +0.0002/+0.0005 (+0.005mm/+0.013mm) to create the perfect oversized guide hole for their traditional drill lines capable of drilling 8xD or greater. Valor Holemaking’s Pilot Drills also include a +2/+1 deg angle tolerance to ensure a larger angle than the chasing drill. Piloting depth is recommended as 3xD for all applications drilling 8xD or greater.

2. Choose the Right Size and Point Angle

Selecting the appropriate size for your pilot drill is crucial. As a rule of thumb, the diameter of the pilot hole should be slightly larger than the diameter of the final hole. This allows for optimal support for the chasing drill while preventing excessive material removal. The pilot drill’s point angle should be equal to or larger than the succeeding drill. This allows the tip of the succeeding drill to engage the material before the flank does (see figure below).

3. Optimize Feed Rates

When using a pilot drill, ensure that the feed rates are optimized for both the pilot and the larger drill. Adjusting the feed rate can improve performance and reduce the risk of tool breakage. Valor Holemaking’s downloadable speeds and feeds tables and Machining Adviser Pro are excellent resources, and you can always consult Valor Holemaking’s Tech Team for further assistance!

4. Use Proper Coolants

Effective cooling and lubrication are vital in metal machining. Ensure that your pilot drill is adequately cooled with flood coolant or adjust speeds and feeds to maintain tool integrity and enhance cutting performance.

5. Maintain Tool Condition

Regularly check the condition of your pilot drills. Worn or damaged pilot drills can lead to inaccuracies and affect the performance of subsequent operations.

6. Integrate with CNC Programming

Incorporate pilot drilling into your CNC programs to ensure that it’s executed at the right stage of your machining process. Program one revolution or brief dwell at the bottom of the pilot hole to ensure a clean surface. This will help streamline operations and improve overall efficiency.


Conclusion

Pilot drills may seem like a small detail in the larger scope of CNC machining, but their impact on precision, tool life, and overall efficiency is significant. By understanding their importance and implementing best practices, machinists can enhance their processes and achieve superior results. Whether you’re a seasoned CNC operator or just starting out, incorporating pilot drills into your workflow is a smart move that can lead to greater accuracy and success in metal machining.


https://www.harveyperformance.com/wp-content/uploads/2024/12/Featured-Image-Pilot-Drills-IMG.jpg 525 1400 Emily Van Volkom http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Emily Van Volkom2024-12-10 13:53:412025-01-30 09:11:16Mastering Precision: Pilot Drills in CNC Machining

Mastering CNC Drilling: Geometries and Key Factors

August 9, 2024/0 Comments/in CNC Machining, Drilling, Drilling & Holemaking, Holemaking, Large Featured, Machining 101, Material Specific, Tool Geometry, Tool Information Guides, Tool Selection/by Harvey Performance Company

Selecting the proper drill for a specific application is essential to ensuring a successful cnc drilling job. Achieving a perfectly machined hole can often be challenging. There are many machining woes that can occur when drilling into a material. These can greatly affect hole quality, and regardless of the material being machined, there is often zero margin for error to ensure all components meet specifications.

To ensure you are selecting and using the correct drill, you need not only a deep understanding of drill geometries, but also the factors that influence the performance of the drill and quality of the hole. In this comprehensive guide, we’ll dive into drill geometries, while also exploring the performance factors that determine CNC drilling results. Furthermore, we’ll connect these to the strategic decisions that drive the tool selection process, so you can gain a competitive edge at the spindle.

Performance Factors Influencing CNC Drilling Success

Part Material

Different materials require different drill geometries and cutting speeds to maintain hole quality and prevent excessive wear. With different types of materials, whether it be a softer non-ferrous material like aluminum or a harder ferrous material like stainless steels, you’ll face different challenges as you manufacture your part. To ensure that you’re getting the best performance and tool life possible features and geometries must be considered.

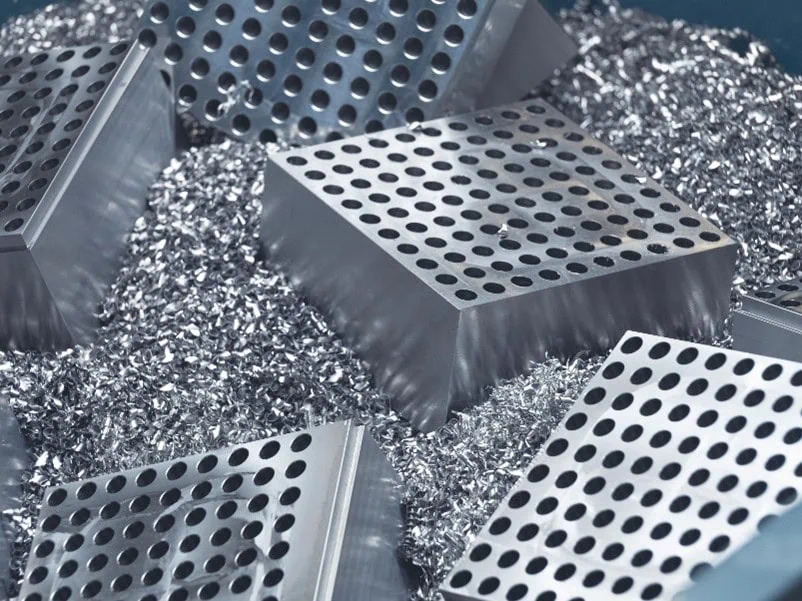
metal blocks that have many holes from cnc drilling operations

CNC Drill Geometries

It is important to understand the different geometries of a drill to understand how they affect an application. For an in depth dive into drill geometries, read 10 CNC Drill Geometries Every Machinist Must Know. This breaks down the unique aspects of geometries and how they affect the cnc drilling process.

Drill Geometries and Drill Walking

CNC drill walking occurs when a drill lacks sufficient engagement with the material. This causes it to deviate from its intended tool path, leading to inaccuracies in hole placement and dimensions. This occurs due to various factors, often including improper drill geometry choice. Understanding how different drill geometries influence drill walking is crucial to ensure you’re achieving precision and consistency in every hole.

Point Angles

The point angle dictates cutting forces and chip evacuation. Choosing the right angle, such as 118° or 135°, based on material hardness, ensures efficient drilling and prevents walking. The shallower the point angle, the better the distribution of cutting forces on the material. Higher angles walk less, as the point grabs into the material easier. Machinists must weight these options when choosing the proper drill.

Web Thickness

Web thickness is the distance between cutting edges or flutes at the face of the drill. This is where stability is generated in a tool. Webs that are too thin can increase the likelihood of breakages, while webs that are too thick will generate unnecessary cutting forces. Finding the proper blend of stability and cutting force is a common struggle for machinists.

CNC Drill Length Considerations

Flute and overall length impact stability and chip evacuation. Matching these lengths to drilling depth prevents deflection and enhances hole quality.

While it may be easiest to purchase a long drill that will work in a variety of scenarios, it is not the best choice to ensure precision. Machinists should best match their required depth to the effective depth of a drill. This ensures that the tool will be as rigid as possible, generating the straightest holes.

As tool length increases, rigidity decreases. Therefore, a properly matched drill will be as rigid as the situation allows. This affords the machinist with the best possible outcome for their unique drilling application.

Coolant-Through Drilling

Proper cooling and lubrication extends tool life and ensures excellent hole quality. If your machine is equipped with the option to run through spindle coolant tooling, it can be extremely beneficial to your application. Unlike an end mill, where chips often have the ability to evacuate outward from the tool, the chips in a drilling operating are held captive inside the feature as it’s being drilled. Here, chips are only able to evacuate through the drill fluting

Through spindle coolant not only cools and lubricates a drill at the point of material removal, but also forcibly evacuates the chips. This can increase your tool’s life while reducing or removing the need for peck cycles all together. This means faster cycle times and higher production rates for your product.

On the other hand, coolant can be fed externally, and sprayed onto the tooling. This will aid in cooling and lubricity. The downside is it is less efficient than utilizing a coolant-through drill. In deep hole drilling applications, external coolant is often ineffective for chip evacuation efforts, and is not the ideal choice for the best results.

Speeds & Feeds

Optimizing speeds & feeds is essential for efficient and accurate drilling. There is not a “one size fits all approach” for speeds & feeds, as all tools and materials require a slightly different approach.

Finding the right balance for each material prevents tool wear and ensures effective chip evacuation. Valor Holemaking offers comprehensive starting parameters in the form of Speeds & Feeds Charts and each tool is also supported by Machining Advisor Pro. This tool allows machinist to custom generate speeds & feeds based off the exact tool path, material, and machine setup.

Rigidity and Stability

A sturdy machining setup reduces vibrations during drilling, improving hole quality. The same can be said about the drill within. A rigid tool is a stable tool, especially as the depth requirements increase. Stability is especially important for drilling heavy-duty materials. This can be impacted by several factors, most importantly the quality of the tool and its design, as well as its chip management capabilities. High precision and high-performance solid carbide drills are designed for the utmost rigidity to ensure repeatability time after time and part after part.

Software and Programming

CNC programming software simplifies creating and editing drilling programs. Compatibility with common CAD/CAM software streamlines integration. Much like machine quality, proper programming is an important step in ensuring precision in CNC drilling applications. CAD/CAM integration ensures the correct dimensions are input to the software to best ensure the tool correctly fits the required parameters.

Exploring CNC Drilling Geometries & Key Factors: Wrapped Up

There are many different drill geometries and factors that can directly impact a drill’s performance and hole quality. Understanding these features can greatly assist in your tool selection process, allowing you to improve productivity and hole quality, so you can gain a competitive edge at the spindle. Drilling is often the most precise aspect of machining, so mastering geometries is critical to success.

https://www.harveyperformance.com/wp-content/uploads/2024/08/Featured-Image-Mastering-CNC-Drilling.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2024-08-09 14:34:572025-11-12 16:00:33Mastering CNC Drilling: Geometries and Key Factors

HSS vs Cobalt vs Carbide: Choosing a Tool Substrate

July 31, 2024/0 Comments/in CNC Machining, Large Featured, Titan USA, Tool Information Guides, Tool Selection/by Allison House

Do you know which cutting tool substrate is right for you? Popular cutting tool manufacturers, such as Titan USA, oftentimes sell high speed steel, cobalt, and solid carbide cutting tools – but which is right for your application? This article will serve as a guide to the benefits of each material, and the best choice for specific applications.

At the same time, do you understand the differences of high speed steel vs cobalt vs carbide? Follow along for the key differences of the three substrates.

High Speed Steel Tooling

Titan USA High speed steel reamer with callouts

When it comes to high speed steel tooling, this will be the most economical choice among the three substrate options. The above image shows a Titan USA High Speed Steel Reamer.

High speed steel is known for its high working hardness and excellent toughness. While maintaining a rigid set up should always be a priority, high speed steel tooling can excel in situations where a rigid set-up can’t be obtained, and where there is potential for excessive tool holder overhang. The toughness of high speed steel over cobalt and solid carbide makes it less prone to brittle fracture or chipping. These tools can be used in a variety of ferrous materials, such as steel and iron, and non-ferrous materials such as brass, copper, and aluminum alloys.  However, high speed steel should not be used in hardened versions of these materials.

This substrate is not without its drawbacks, too, though. High speed steel tooling will need to be run at slower cutting speeds than cobalt or solid carbide tooling, which could potentially make it less ideal for high production runs.

Cobalt Tooling

Titan usa cobalt reamer with dimension callouts


For most situations, cobalt is going to offer an intermediate option when compared to high speed steel and solid carbide options. The image above shows a Titan USA Cobalt Reamer.

Cobalt can be run even faster than high speed steel tooling. It can also be used in most hardened and abrasive materials such as bronze, stainless steel, cast iron, and titanium.

However, a cobalt bit will not retain its edge sharpness for as long as a solid carbide bit, and it will be more prone to brittle failure than high speed steel tooling in non-rigid set ups.

If you have a desire to run at faster running parameters than what high speed steel tooling offers, or if you are running in a hardened material, cobalt may be your next consideration. While it will typically have a higher cost than high speed steel tooling, it would be a more economical option than solid carbide.   


Solid Carbide Tooling

Titan USA Carbide reamer with dimension callouts

Solid carbide will be the premier material substrate offered for most cutting tool selections, as it offers high edge sharpness that allows tooling to be run at the fastest running parameters offered among the three material substrates. The above image shows a Titan USA Solid Carbide Reamer.

Although solid carbide tends to be the most expensive substrate option, the ability to run at high speeds and feeds allows you to reduce your cutting time. This increased productivity can prove to be more economical for higher production jobs. Solid carbide tooling is going to have the highest heat and wear resistance, allowing the tooling to last longer and require less replacement.

Further, solid carbide is a good choice when dealing with hardened materials or high temp alloys. For example, it can be used in hardened steels, titanium alloys, and nickel alloys up to 45RC. When paired with material specific tool geometries and coatings, solid carbide can even be used in materials up to 68Rc.

One downside to solid carbide tooling is that its high hardness can make it more susceptible to brittle failure and therefore may not be a good choice when dealing with non-rigid set ups. For example, solid carbide can be more prone to chipping or breaking when encountering interrupted cuts, vibrations, or shocks.

Substrate Options

Substrate Options

When browsing the different material options offered by Titan USA, this article can act as a helpful guide for choosing the right tool for your application.  For more information on the different tooling styles offered in high speed steel, solid carbide, and cobalt, please visit the Titan USA website at https://www.titancuttingtools.com/ .

Sources:

  1. Chitnis, Rohit. “HSS vs Cobalt vs Carbide Drill Bits: What to Choose.” Benchmark Abrasives, Benchmark Abrasives, 29 June 2022, benchmarkabrasives.com/blogs/news/hss-vs-cobalt-vs-carbide-drill-bits-what-to-choose.
  2. “A Comprehensive Guide to Pros and Cons of Carbide Tools and HSS.” TJ Grinding, 8 May 2018, tjgrinding.com/blog-post/comprehensive-guide-pros-and-cons-carbide-tools-and-hss.
  3. “High-Speed Steel vs Carbide Tools: AIMS Industrial.” AIMS Industrial Supplies, www.aimsindustrial.com.au/blog/hss-vs-carbide. Accessed 17 June 2024.
  4. Startoolinc. “The Difference between High speed steel & Carbide End Mills.” Tool Talk, 11 Feb. 2020, tooltalk.blog/the-difference-between-high-speed-steel-carbide-end-mills/#:~:text=Compared%20to%20HSS%2C%20carbide%20tools,to%20face%20milling%20and%20beyond.
https://www.harveyperformance.com/wp-content/uploads/2024/07/Featured-Image-Selecting-Cutting-Tool-Substrate.jpg 525 1400 Allison House http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Allison House2024-07-31 16:29:122025-11-12 15:58:06HSS vs Cobalt vs Carbide: Choosing a Tool Substrate

2023 CNC Cutting Tool Survey

November 30, 2023/0 Comments/in No Index/by Harvey Performance Company

To thank survey respondents for completing this survey, we will randomly select three respondents to receive a $500 Visa Gift Card.

At Harvey Performance Company, we are committed to delivering exceptional products and services, and your perspectives play a pivotal role in shaping our future endeavors. This survey has been crafted with the intention of understanding how our brands are currently serving you, our valued customers.

How to Participate

All you need to do is complete the survey to enter the giveaway.

Official Contest Rules

Contest Dates:

The contest will run from November 30, 2023, to December 14, 2023. Entries that are submitted before or after the contest period will not be considered for the giveaway.

Prizes

All submissions will be considered for one of the three $500 Visa gift card prizes.

Winners of the giveaway will be chosen at random on December 15, 2023, and will be notified by email or phone.

Full Details:

NO PURCHASE IS NECESSARY TO ENTER OR WIN. MAKING A PURCHASE WILL NOT INCREASE YOUR CHANCES OF WINNING. APPLICABLE ONLY IN THE UNITED STATES and CANADA. ENTRY INTO THIS GIVEWAY CONSTITUTES THE ACCEPTANCE OF THESE OFFICIAL RULES. VOID WHERE PROHIBITED BY LAW.

By participating in the Harvey Performance CNC Cutting Tooling Survey, you agree to these official rules (the “Rules”), which are a contract, so read them carefully before participating. Without limitation, this contract includes indemnities to the Released Parties (defined below) from you and a limitation of your rights and remedies. You must follow these Rules to enter and be eligible to receive a prize in connection with the survey giveaway.

DURATION:  Begins on November 30th, 2023, at 8:00 AM EST and ends December 14th, 2023, at 5 PM EST (“Survey Period”).  The computer clock of Harvey Performance Company, LLC (“Sponsor”) is the official time-keeping device for the survey giveaway.

ELIGIBILITY: The survey giveaway is open only to legal permanent residents of the United States (excluding Puerto Rico, and the U.S. Territories and Possessions) who are 21 years of age or older as of the date of entry. Employees, officers, and directors of Sponsor along with its affiliates, subsidiaries, advertising, contest, fulfillment, and marketing agencies, (collectively, “Promotion Parties”) their immediate families (parent, child, sibling & spouse, and their respective spouses, regardless of where they reside) and persons living in the same households as such individuals (whether related or not) are not eligible to participate in survey giveaway. By participating, you agree to these Rules and to the decisions of the Sponsor, which are final and binding in all respects.  In addition, to be eligible to win, you must also execute and return Sponsor’s forms for you to: (i) consent to the use of your rights of publicity, (ii) assume all tax liabilities, (iii) waive all claims against Sponsor and Promotion Parties, and (iv) confirm your eligibility (collectively “Affidavits and Waivers”). This survey giveaway is void in any jurisdiction not listed above and where prohibited by law, rule, or regulation.

HOW TO ENTER: Follow the directions and complete the survey and submission form at the end of the survey.

If you do not provide an email address, we will call you if your name is selected. Otherwise, you will not be contacted regarding the outcome.

PRIVACY POLICY:  Information collected in connection with this Sweepstakes will be used in accordance with Sponsor’s Official Privacy Policy (available at https://www.harveyperformance.com/privacy-policy/ and these Rules. In the event of any discrepancy between Sponsor’s Privacy Policy and these Rules, Sponsor’s Privacy Policy shall control and govern.

LIMITATIONS: The maximum number of entries allowed during the Sweepstakes is 1 per person.

Sponsor is not responsible for any entry that is lost, late, misdirected or undeliverable, whether due to system errors, omissions, interruption, deletions, defects, delay in operations or transmissions, theft or destruction or failures, faulty transmissions or other telecommunications malfunctions, entries not received resulting from any hardware or software failures of any kind, lost or unavailable network connections, failed, incomplete or garbled computer or telephone transmissions, typographical or system errors and failures, faulty trans-missions, technical malfunctions, or otherwise.

In the event of a dispute regarding the identity of the person submitting an entry, the entry will be deemed submitted by the authorized account holder at the time of entry. The authorized account holder is the natural person who is assigned to the account by Sponsor, the organization that is responsible for assigning accounts to customers. Potential winners may be required to show proof of being the authorized account holder.

Any attempt by an entrant to obtain more than the stated number of entries by using multiple/different email addresses, identities, registrations, logins, and/ or any other methods, including, but not limited to, automated entry, will void that entrant’s entries and that entrant may be disqualified from the Sweepstakes. Multiple participants are not permitted to share the same email

Sponsor will not verify receipt of entries for entrants. All entries submitted become the sole property of Sponsor. Sponsor reserves the right to disqualify those entries deemed to be inappropriate or in violation of this survey giveaway (as defined solely by Sponsor).

Entries are void if they are incomplete, irregular, or submitted improperly. Personal information (if any) collected through the Entry Form will be used only for purposes of (i) selecting and contacting the winners, and (ii) as identified in the Privacy Policy.

ODDS OF WINNING: The actual odds of winning will depend upon the actual number of total entries received for this survey giveaway, regardless of the means of entry.

LIABILITY LIMITATION:  The Sponsor assumes no responsibility or liability for (a) lost, late, stolen, undelivered, inaccurate, incomplete, delayed, misdirected, damaged or garbled registrations, entries, URLs, or emails; (b) any incorrect or inaccurate entry information, or for any faulty or failed electronic data transmissions; (c) any unauthorized access to, or theft, destruction or alteration of entries or registrations at any point in the operation of this survey giveaway; (d) any technical malfunction, failure, error, omission, interruption, deletion, defect, delay in operation or communications line failure, regardless of cause, with regard to any equipment, systems, networks, lines, cable, satellites, servers, computers or providers utilized in any aspect of the operation of the survey giveaway; (e) inaccessibility or unavailability of the Internet or the Sponsor’s web site or any combination thereof or for computer hardware or software malfunctions, failures or difficulties, or other errors or difficulties of any kind whether human, mechanical, electronic, computer, network, typographical, printing or otherwise relating to or in connection with the survey giveaway, including, without limitation, errors or difficulties which may occur in connection with the administration of the survey giveaway, the processing of Entries, social networking posts, or registrations, the announcement of the prizes, or in any other  survey giveaway related materials; or (f) any injury or damage to participants or to any other person’s computer which may be related to or resulting from any attempt to participate in the survey giveaway. If, for any reason, the survey giveaway (or any part thereof) is not capable of running as planned for reasons which may include, without limitation, infection by computer virus, tampering, unauthorized intervention, fraud, technical failures, or any other causes which may corrupt or affect the administration, security, fairness, integrity or proper conduct of this survey giveaway, then the Sponsor reserve the right at their sole discretion to cancel, terminate, modify or suspend the survey giveaway in whole or in part. If terminated, the Sponsor will award the prizes from among all non-suspect, eligible Entries received for the survey giveaway up to the time of such action.

RELEASES: All participants, as a condition of participation in this survey giveaway, agree to release, hold harmless and indemnify the Sponsor, its offers, directors, accountants, attorneys, and agents (“Released Parties”) from and against any and all liability, claims, damages, or actions of any kind whatsoever for injuries, damages, or losses to persons or property which may be sustained, in whole or in part, directly or indirectly, in connection with (i) participation in any aspect of the survey giveaway, (ii) the receipt, ownership or use of the prize awarded, including any travel associated with any prize, (iii) participant’s registration material on any related website, or (iv) any typographical or other error in these Rules.

NO WARRANTIES: NEITHER SPONSOR NOR ANY OF THE RELEASED PARTIES HAVE MADE OR MAKE OR ARE RESPONSIBLE OR LIABLE FOR ANY WARRANTY, REPRESENTATION OR GUARANTEE, EXPRESS OR IMPLIED, RELATIVE TO THISSURVEY GIVEAWAY OR A PRIZE, INCLUDING BUT NOT LIMITED TO, ITS QUALITY OR FITNESS OR MERCHANTABILITY, AND ALL PRIZES ARE TENDERED TO ENTRANTS ON AN “AS IS” BASIS.  THERE ARE NO WARRANTIES REGARDING ANY PRIZE OR THE USE OF THE GIFT CARD.

RANDOM DRAWING: Three (3) prize winner(s) will be randomly selected for the Survey giveaway to receive a $500 Visa gift card. All decisions on all matters pertaining to the survey giveaway are final. The sponsor reserves the right to substitute a prize of equal or greater value.

WINNER NOTIFICATION: Random selection of the potential prize winner will occur during the first week that immediately follows the survey giveaway Period from among all eligible entries received. Prize drawing will be conducted at Sponsor’s headquarters. The prize winner will be notified by e-mail, phone, or regular mail, in Sponsor’s discretion, within 30 days from the date of the winner selection.

The designated prize winner will have 14 days from notification to claim the prize and return all release and eligibility forms. Sponsor and its affiliates, subsidiaries, employees, agents, officers and directors, advertising and promotion agencies, and their respective officers, directors, employees, and their respective agents, will not be liable for unsuccessful efforts to notify a winner.

The prize will be delivered via e-mail. No prize transfer, assignment or substitution by winner permitted. All federal, state and local taxes, fees and surcharges on prizes are the sole responsibility of the prize winner. If the prize winner declines the prize, fails to claim the prize, is unavailable for prize fulfillment, fails to abide by these Rules, or is ineligible, Sponsor may select an alternate winner from all remaining eligible entries.

By entering this survey giveaway, each entrant gives his/her express permission to be contacted by the Sponsor by telephone, e-mail and/or postal mail for survey giveaway purposes.

The winner, by acceptance of Prize, grants to Sponsor, and each of its respective designees, the right to publicize the winner’s name, address (city and state of residence), photograph, voice, statements and/or other likeness and prize information for advertising, promotional, trade and/or any other purpose in any media or format now known or hereafter devised, throughout the world, in perpetuity, without limitation and without further compensation, consideration, permission or notification, unless prohibited by law.

Before being declared a winner, each selected entrant will be required to sign a confirmation and acceptance confirming compliance with the these Rules and acceptance of the prize as offered. The confirmation and acceptance must be returned within 7 business days of the notification date indicated on the documents, unless otherwise stated, or the selected entrant will be disqualified, and the prize forfeited.

THIRD PARTY & SOCIAL MEDIA:  This Sweepstakes is in no way sponsored by, endorsed by, associated with, or administered by Facebook, Instagram, Twitter, WhatsApp, Tumblr, Google, YouTube, WeChat, or WhatsApp (collectively “Social Media Sites”).  By entering this event, you agree to hold all Social Media Sites harmless for and from any potential claims you may have related to or arising out of this Sweepstakes. Do we need this clause? We are not requiring the recipient to follow us on social media.

MISCELLANEOUS CONDITIONS: Sponsor reserves the right at its sole discretion to cancel, terminate, modify, or suspend the survey giveaway.

Sponsor assumes no responsibility for any error, omission, interruption, deletion, defect, or delay in operation or transmission; communications line failure; theft or destruction of or unauthorized access to survey giveaway entries or entry forms; or alteration of entries or entry forms. Sponsor reserves the right to correct clerical or typographical errors in promotional materials or any materials related to the survey giveaway.

WINNER NAME: To obtain the name of the winner, send a request to [email protected]

CHOICE OF LAW AND JURISDICTION: This survey giveaway is governed by the internal substantive laws of Nevada, without regard to its conflicts of law provisions.
https://www.harveyperformance.com/wp-content/uploads/2023/11/Helical-7-Flute-Square-Endmill-001-Gorham-1.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2023-11-30 08:00:002023-12-06 15:20:492023 CNC Cutting Tool Survey
Page 1 of 10123›»
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top