Harvey Performance Company
  • About Us
    • Company Overview
    • Our Unique Strengths
    • Our Partners
    • Our History
    • Our Locations
    • Sustainability
    • Giving Back
      • Giving Back
      • One Tree Planted
    • News
      • News
      • Press
  • Our Brands
    • Harvey Tool
    • Helical Solutions
    • Micro 100
    • Titan USA
    • CoreHog
    • Valor Holemaking
    • ATA Air Tools
    • ATA SGSPRO
    • Garryson
    • Industrial Tooling Corporation (ITC)
    • Karnasch
    • Van Hoorn Carbide
  • Products
    • Milling
    • Drilling
    • Grinding
    • Micro Tools
    • Sinking
    • Sawing
    • Composite Tools
    • Threading
    • Turning
    • Beveling
    • Reaming
    • Air Tools
  • Solutions
    • Aerospace
    • Automotive
    • Defense
    • Energy
    • Foundries
    • Marine
    • Medical
    • Mold & Die
    • Oil & Gas
    • Power Generation
    • Rail
  • Resources
    • CAM & TDM Tool Libraries
    • Machining Advisor Pro
    • In the Loupe Blog
    • Webinars
  • Careers
  • Contact Us
  • Menu Menu
  • Link to LinkedIn
  • Link to Facebook

Tag Archive for: left hand spiral

Recycling Carbon Fiber: Importance & Process

July 8, 2024/0 Comments/in CNC Machining, Composites, How-To's, Material Specific, Milling, Trending Now/by Sarah Wasson

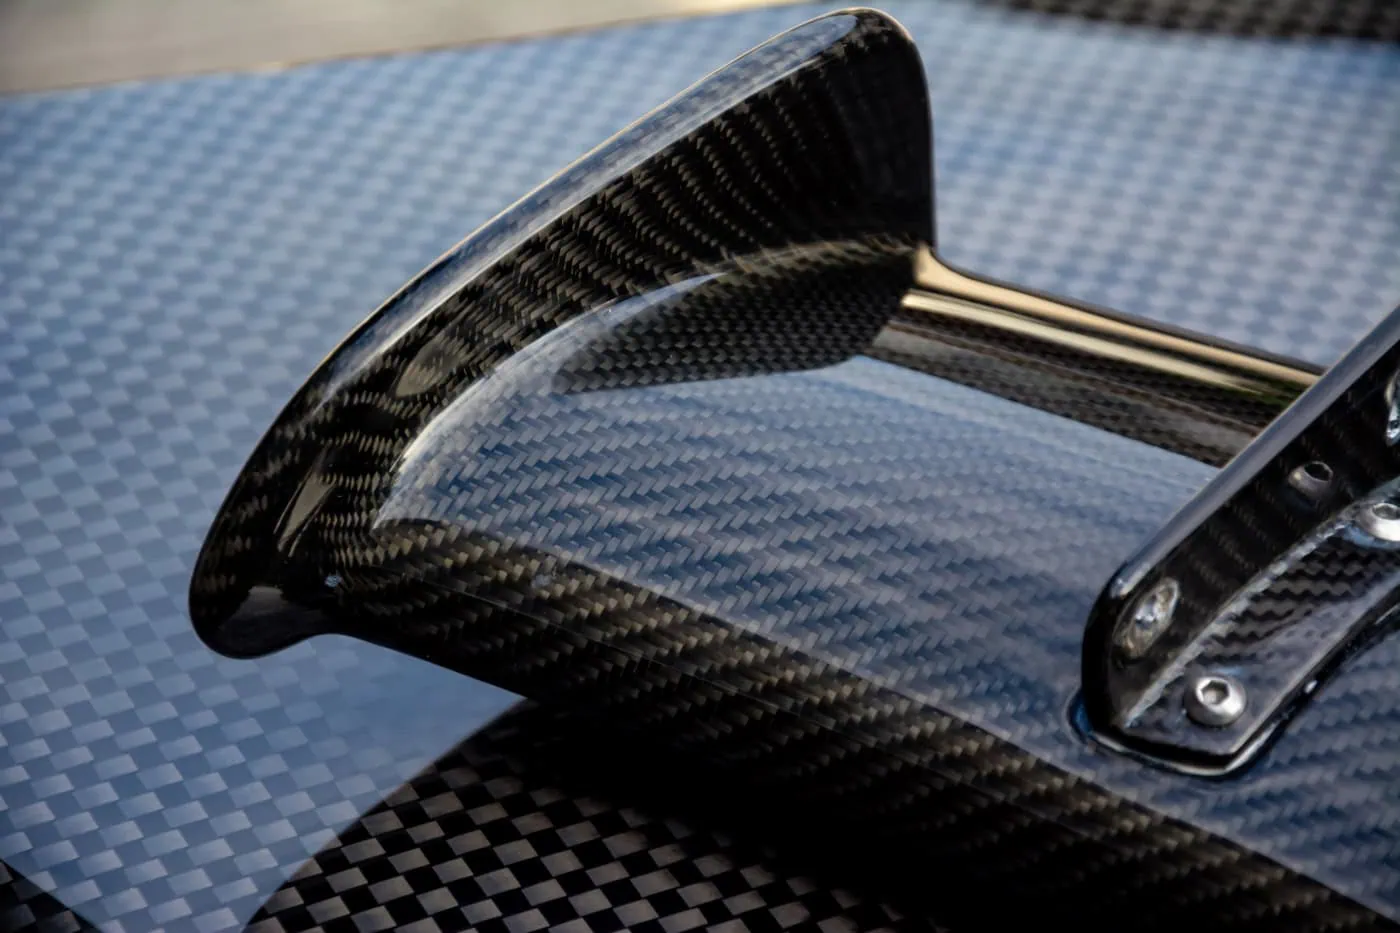
Carbon fiber is a woven cloth made of crystalline filaments of carbon cured with a polymer, which can be layered and shaped around a mold. It is an ideal material due to its impressive strength-to-weight ratio , meaning it’s very strong, but not heavy. Carbon fiber is five times lighter than steel with an equal elastic modulus, making it a better choice for many applications. Further, it is corrosion-resistant, non-flammable, and non-toxic, properties that make it an ideal material to use in aerospace, medical, construction, and military industries.
Machining Carbon Fiber

Machining Carbon Fiber can be challenging. The layered structure of the carbon fiber material can lead to delamination, uncut fibers, fiber tear-out, uneven tool wear, and poor surface finishes. Luckily, many cutting tool companies, like CoreHog, specially design tooling with different geometries that can help eliminate these manufacturing problems:

  • Straight Flute End Mills: Apply all the cutting forces radially, which helps prevent delamination.
  • Compression Cutters: Create opposite cutting forces, stabilizing material removal and preventing delamination, fiber pullout, and burrs along the surface.
  • Chipbreaker Cutters: Shear the fibers and shorten the chips, preventing fiber buildup around the cutter.
  • Diamond Cut End Mills: Utilize both left-hand and right-hand flutes to break up and shear through the fibers, ideal for roughing and profiling carbon fiber.
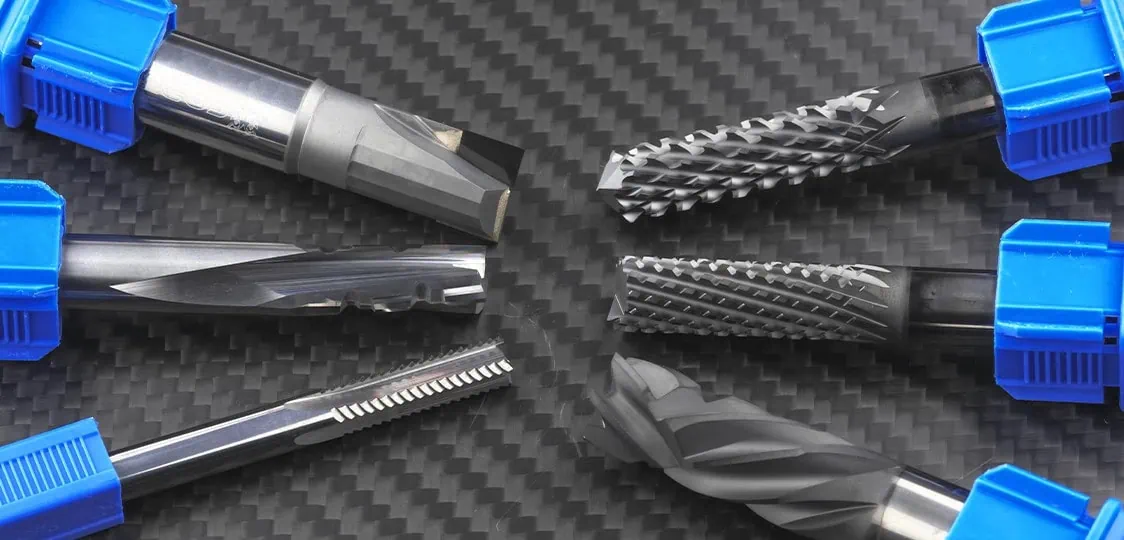
Explore CoreHog’s Wide Offering of Composite-Laminate Cutters, each specially engineered to cut difficult-to-machine laminate materials like carbon fiber.

Common Carbon Fiber Applications

In the aerospace industry, carbon fiber is used in plane structures to replace alloys, creating lighter planes and thus, reducing fuel consumption. Recreational sports also utilize carbon fiber to decrease weight. It is often seen as a leading material in skis, bikes, and tennis rackets, as the lighter weight can help improve performance. In professional sports leagues like Formula 1 and NASCAR, carbon fiber has grown in prevalence in recent years. Another advantageous quality of carbon fiber is its suitability in X-ray machines, allowing imaging to pass through without interruption, making it useful in many medical devices and implants.
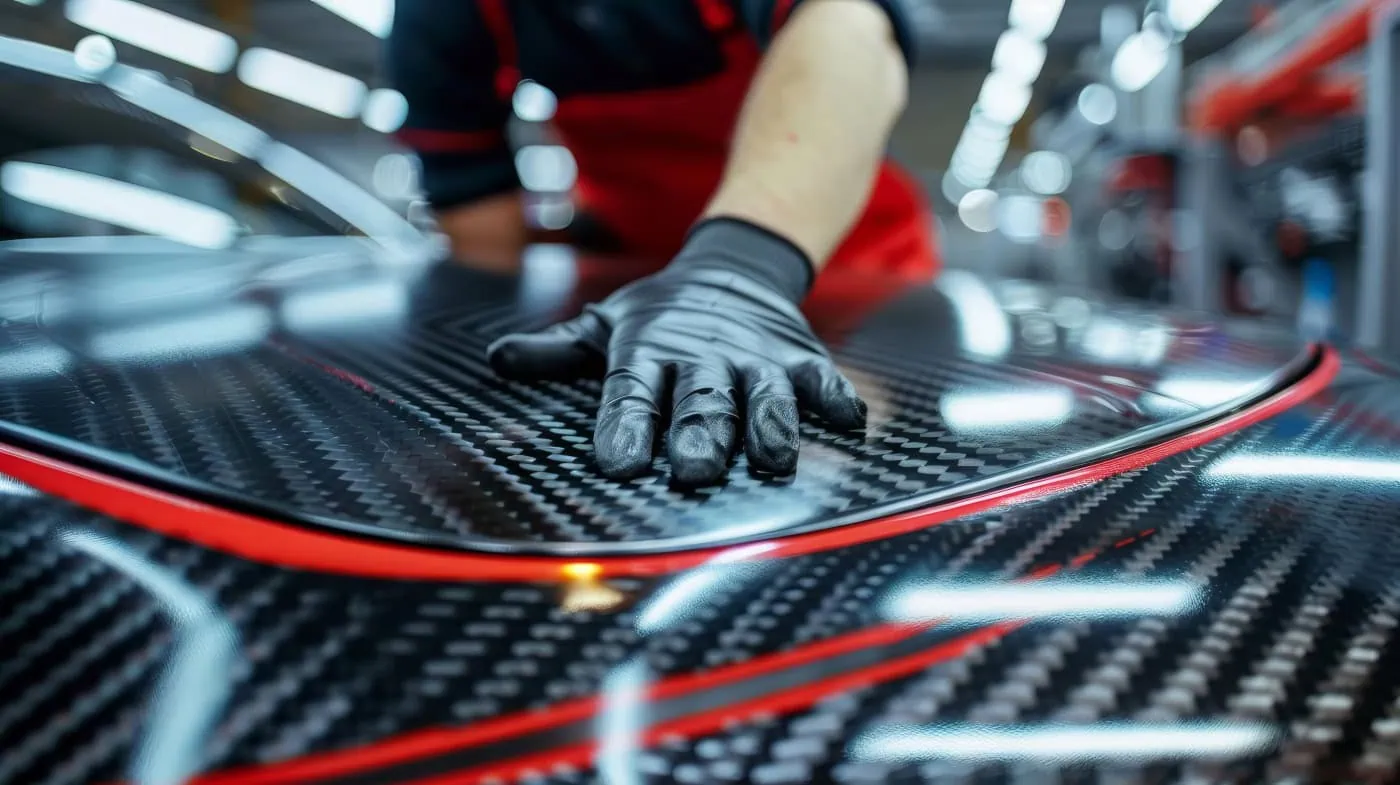
Recycling Carbon Fiber

Why is Recycling Carbon Fiber Difficult?

Carbon fiber sheets require a significant amount of energy to produce. These large sheets are then cut down to the part size needed, and the excess material is often discarded, increasing waste production. This material is not biodegradable and is typically sent to a landfill where it will remain permanently. Further complicating recycling, carbon fiber is built to hold its shape and strength and cannot be melted down and reshaped like many plastics. When recycled, its properties are heavily degraded, rendering it useless for applications that experience heavy forces or loads.

How is Carbon Fiber Recycled?

Solvolysis

Solvolysis uses a chemical solvent to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces, increasing the surface area. The solvent, chosen based on the polymers used in the carbon fiber, breaks down the polymer chains, separating the carbon fiber from the polymer. Techniques like centrifugation are used to separate the substances. The carbon fiber can be further purified to restore its properties and then combined with virgin fibers to create new fabric or used by itself. This process enables the recovery of carbon fiber without sacrificing material properties.

Pyrolysis

Pyrolytic utilizes heat to break down the polymer encasing the carbon fiber cloth. The waste carbon fiber is shredded into smaller pieces and then heated in a controlled environment with limited or no oxygen. At high temperatures, the polymer undergoes thermal decomposition, producing gases, vapors, and char. The gases and vapors can be used as an energy source or further processed, while the char, which is carbon fiber and any original additives, is purified to ensure mechanical properties are maintained. The resulting carbon fiber can be used alone or combined with virgin fibers. Pyrolysis is effective for high-quality fiber recovery and energy recovery from gas byproducts.

Carbon Fiber Considerations

As we innovate with new technology, it is important to consider its impact on our planet. Carbon fiber is an amazing material that can improve many aspects across industries; however, the waste generated is not going anywhere but a landfill. Many companies are investing in producing high-quality recycled carbon fiber. With a shift in focus to designing closed-loop systems for composite materials, the future looks bright.
https://www.harveyperformance.com/wp-content/uploads/2024/07/Feature-Image-Recyling-Carbon-Fiber-IMG.jpg 525 1400 Sarah Wasson http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Sarah Wasson2024-07-08 12:00:402024-07-12 12:46:58Recycling Carbon Fiber: Importance & Process

Experience the Benefits of Staggered Tooth Keyseats

September 19, 2018/0 Comments/in CNC Machining, Tool Information Guides, Tool Selection/by Harvey Performance Company

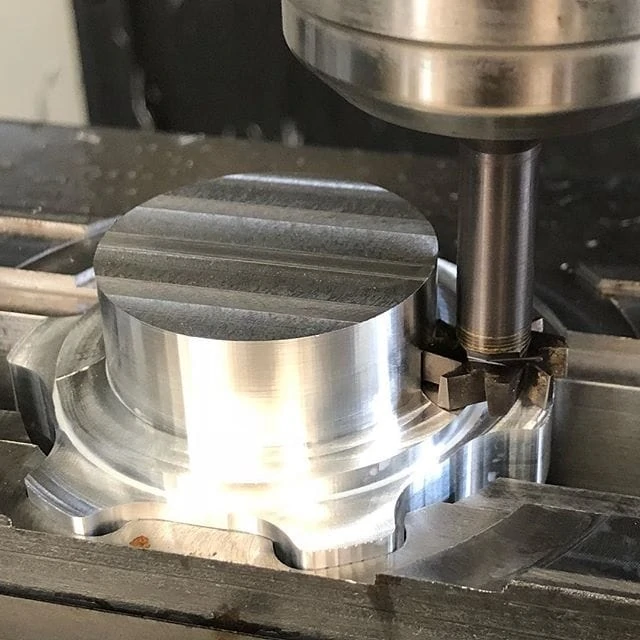
Keyseat Cutters, also known as Woodruff Cutters, Keyway Cutters, and T-Slot Cutters, are commonly used in machine shops. Many machinists opt to use this tool to put a slot on the side of a part in an efficient manner, rather than rotating the workpiece and using a traditional end mill. A Staggered Tooth Keyseat Cutter has alternating right-hand and left hand shear flutes and is right-hand cut, whereas a traditional keyseat cutter has all straight flutes and is right-hand cut. Simply, the unique geometry of a Staggered Tooth Keyseat Cutter gives the tool its own set of advantages including the ability to index within the slot, increase feed rates, and achieve better part finish.

face of a staggered tooth keyseat cutter

Three Key Benefits

Indexing

The alternating right-and-left-hand flutes of a Harvey Tool Staggered Tooth Keyseat Cutters are relieved on both sides of its head, meaning that it allows for both end cutting and back cutting. This adds to the versatility of the staggered tooth keyseat cutter, where one singular tool can be indexed axially within a slot to expand the slot to a specific uncommon dimension. This can save space in a machinist’s magazine and reduce machine time by eliminating the need to swap to a new tool.

Increased Feed Rates

Due to the unique geometry of a Staggered Tooth Keyseat Cutter, chips evacuate efficiently and at a faster rate than that of a Straight Flute Keyseat Cutter. The unique flutes of Staggered Tooth Keyseat Cutters are a combination of right-and-left-hand shear flutes, but both types are right-hand cutting. This results in the tool’s teeth alternating between upcut and downcut. Chip packing and chip recutting is less of a concern with running this tool, and results in increased chip loads compared to that of a standard keyseat with the same number of flutes. Because of this, the tool can account for chiploads of about 10% higher than the norm, resulting in heightened feed rates and shorter cycle times overall.

Better Part Finish

Staggered Tooth Keyseat Cutters have “teeth”, or flutes, that are ground at an angle creating a shear flute geometry. This geometry minimizes chip recutting, chip dragging and reduces the force needed to cut into the material. Chip recutting and dragging are minimized because chips are evacuated out of the top and bottom of the head on the side of the cutter that is not engaged in the material. Shear flutes also reduce vibrations that can lead to chatter and poor finish. By minimizing cutting forces, vibration, and chatter, a machinist can expect a better part finish.

staggered tooth keyseat cutter working in a cnc machine

Image courtesy of @edc_machining

Staggered Tooth Keyseat Cutter Diverse Product Offering

On top of the higher performance one will experience when using the Stagger Tooth Keyseats, there are also multiple options available with various combinations to suit multiple machining needs. This style is offered in a square, square reduced shank and corner radius profile which helps if a fillet or sharp corner is needed. The square and corner radius tools are offered in diameters ranging from 1/8” to 5/8”, and the square reduced shank tool is offered in diameteres ranging from 3/4″ to 1-1/2″. The increased diameter comes with an increase of radial depth of cut, allowing deeper slots to be achievable. Within the most popular cutter diameters, ¼”, 3/8”, and ½” there are also deep slotting options with even greater radial depth of cuts for increased slot depths. On top of the diameters and radii, there are also multiple cutter widths to choose from to create different slots in one go. Finally, an uncoated and AlTiN coatings are available to further increase tool life and performance depending on the material that is being cut.

Opt for a Smoother Operation

A Staggered Tooth Keyseat Cutter adds versatility to a tool magazine. It can be indexed axially to expand slots to make multiple widths, allowing machinists to progress operations in a more efficient manner where tool changes are not required. Further, this tool will help to reduce harmonics and chatter, as well as minimize recutting. This works to create a smoother operation with less force on the cutter, resulting in a better finish compared to a Standard Keyseat Cutter.

For more information on Harvey Tool Staggered Tooth Keyseat Cutters and its applications, visit Harvey Tool’s Keyseat Cutter page.

https://www.harveyperformance.com/wp-content/uploads/2018/09/Featured-Image-Benefits-of-Staggered-Tooth-Keyseats-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2018-09-19 10:35:552023-10-24 10:45:04Experience the Benefits of Staggered Tooth Keyseats

Avoid Composite Delamination With Compression Cutters

September 12, 2017/0 Comments/in CNC Machining, Composites, How-To's, Machining Techniques, Tool Selection, Troubleshooting Tips/by Harvey Performance Company

Composites are a group of materials made up of at least two unique constituents that, when combined, produce mechanical and physical properties favorable for a wide array of applications. These materials usually contain a binding ingredient, known as a matrix, filled with particles or fibers called reinforcements. Composites have become increasingly popular in the Aerospace, Automotive, and Sporting Goods industries because they can combine the strength of metal, the light weight of plastic, and the rigidity of ceramics.

Unfortunately, composite materials present some unique challenges to machinists. Many composites are very abrasive and can severely reduce tool life, while others can melt and burn if heat generation is not properly controlled. Even if these potential problems are avoided, the wrong tool can leave the part with other quality issues, including delamination.

While composites such as G10 and FR4 are considered “fibrous”, composites can also be “layered,” such as laminated sheets of PEEK and aluminum. Layered composites are vulnerable to delamination, when the layers of the material are separated by a tool’s cutting forces. This yields less structurally sound parts, defeating the purpose of the combined material properties in the first place. In many cases, a single delaminated hole can result in a scrapped part.

Using Compression Cutter End Mills in Composite Materials

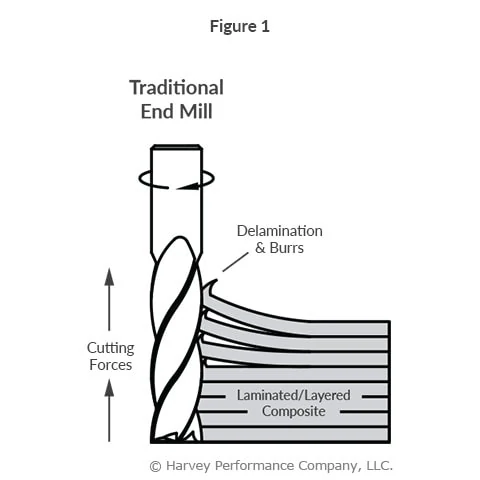
Composite materials are generally machined with standard metal cutting end mills, which generate exclusively up or down cutting forces, depending on if they have right or left hand flute geometry. These uni-directional forces cause delamination (Figure 1).

infographic of delamination with traditional end mill due to upward cutting forces

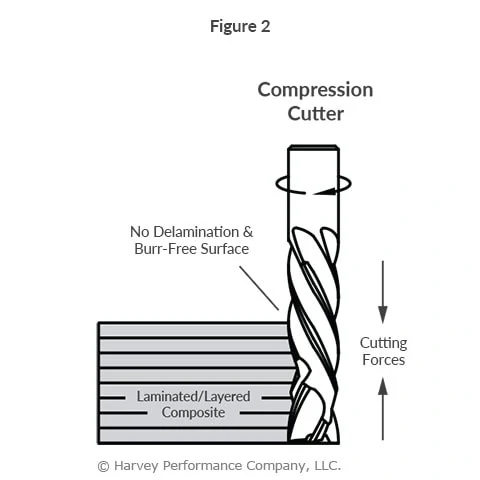
Conversely, compression cutters are designed with both up and down-cut flutes. The top portion of the length of cut, closest to the shank, has a left hand spiral, forcing chips down. The bottom portion of the length of cut, closest to the end, has a right hand spiral, forcing chips up. When cutting, the opposing flute directions generate counteracting up-cut and down-cut forces. The opposing cutting forces stabilize the material removal, which compresses the composite layers, combatting delamination on the top and bottom of a workpiece (Figure 2).

infographic of no delamination due to even cutting forces with compression cutter end mill

Since compression cutters do not pull up or press down on a workpiece, they leave an excellent finish on layered composites and lightweight materials like plywood. It is important to note, however, that compression cutters are suited specifically to profiling, as the benefits of the up and down-cut geometry are not utilized in slotting or plunging operations.

Something as simple as choosing a tool suited to a specific composite material can have significant effects on the quality of the final part. Consider utilizing tools optimized for different composites and operations or learn how to select the right drill for composite holemaking.

https://www.harveyperformance.com/wp-content/uploads/2017/09/Feature-Image-Compression-Cutters-IMG.jpg 525 1400 Harvey Performance Company http://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.png Harvey Performance Company2017-09-12 16:00:532025-11-12 16:00:14Avoid Composite Delamination With Compression Cutters
BLOG HOME

Search In the Loupe

More results...

Browse by Topic

How-To’s
Technical Tips
Tools In Action
Featured Customers
Tool Guides

Free Drilling Guidebook

DOWNLOAD

Recent Posts

  • Machining a Complex Part with Harvey Tool
  • Drill Substrate Guide: HSS vs Cobalt vs Carbide
  • The Key Differences Between Helical’s Tool Coatings

Stay In The Loupe!

Sign up to receive a monthly recap of:
– The latest machining solutions
– Machining tips and tricks
– A recap of our most popular posts

SIGN UP

Contact Us


Address
428 Newburyport Turnpike
Rowley, MA 01969

Website
www.harveyperformance.com

Phone
Harvey Tool Tech: 1.800.645.5609
Helical Solutions Tech: 1.866.543.5422
Micro 100 Tech: 1.800.421.8065
Titan USA Tech: 1.888.482.6872

Email
[email protected]
[email protected]
[email protected]
[email protected]
[email protected]

CONTACT US

428 Newburyport Turnpike
Rowley, MA 01969-1729

844-393-8665

[email protected]

HARVEY PERFORMANCE

Company Overview
Our Unique Strengths
Industries Served
Careers
Sustainability
Privacy Policy

OUR BRANDS

Harvey Tool
Helical Solutions
Micro 100
Titan USA
CoreHog
Valor Holemaking

OUR BRANDS

ATA Air Tools
ATA SGSPRO
Garryson
Industrial Tooling Corporation (ITC)
Karnasch
Van Hoorn Carbide

Copyright © 2022 Harvey Performance Company, LLC
  • Link to LinkedIn
  • Link to Facebook
Scroll to top Scroll to top Scroll to top