
The Secret Mechanics of High Feed End Mills
A High Feed End Mill is a type of High-Efficiency Milling (HEM) tool with a specialized end profile that allows the tool to utilize chip thinning to have dramatically increased feed rates. These tools are meant to operate with an extremely low axial depth so that the cutting action takes place along the curved edge of the bottom profile. This allows for a few different phenomena to occur:
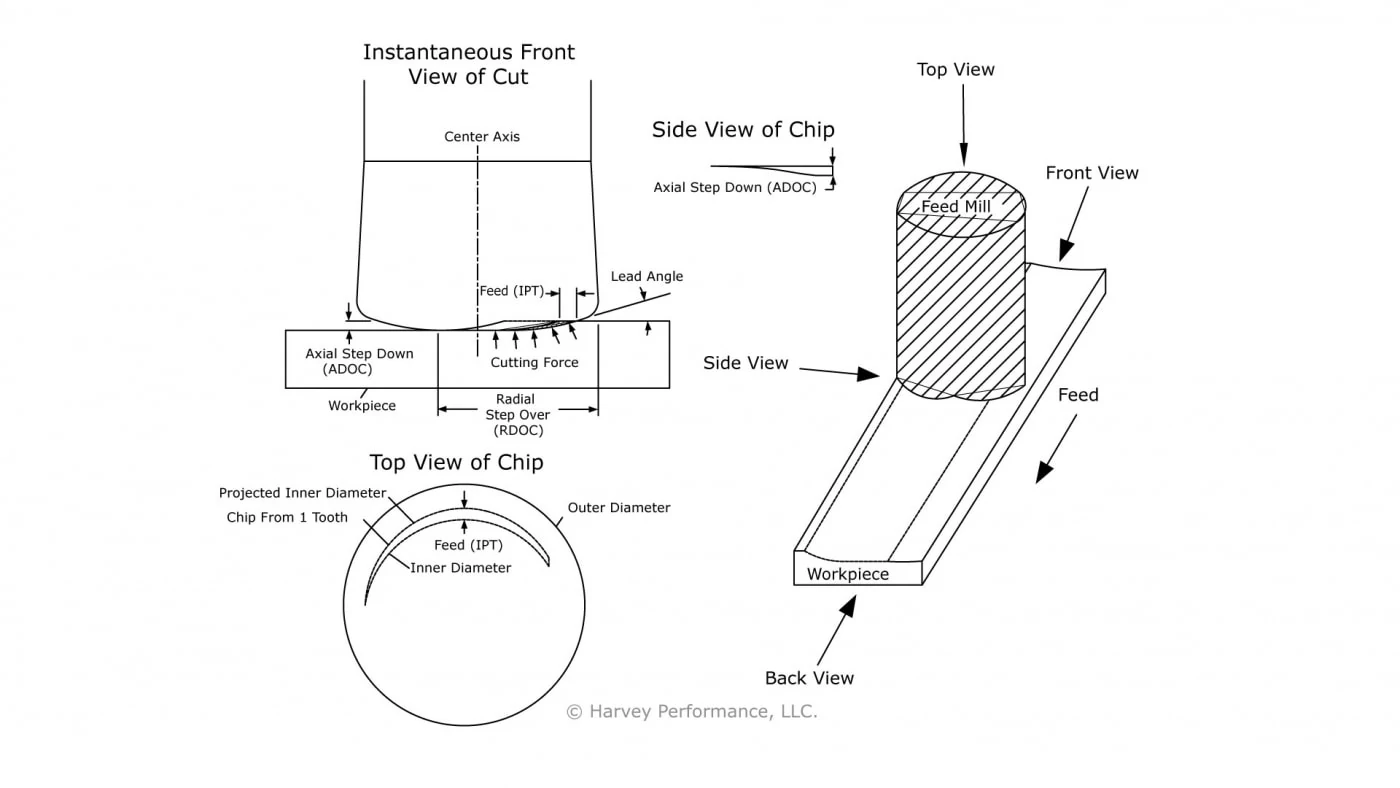
- The low lead angle causes most of the cutting force to be transferred axially back into the spindle. This amounts to less deflection, as there is much less radial force pushing the cutter off its center axis.
- The extended curved profile of the bottom edge causes a chip thinning effect that allows for aggressive feed rates.
The Low Lead Angle of a High Feed End Mill
As seen in Figure 1 below, when a High Feed End Mill is properly engaged in a workpiece, the low lead angle, combined with a low axial depth of cut, transfers the majority of the cutting force upward along the center axis of the tool. A low amount of radial force allows for longer reaches to be employed without the adverse effects of chatter, which will lead to tool failure. This is beneficial for applications that require a low amount of radial force, such as machining thin walls or contouring deep pockets.
Feed Mills Have Aggressive Feed Rates
Figure 1 also depicts an instantaneous snapshot of the chip being formed when engaged in a proper roughing tool path. Notice how the chip (marked by diagonal lines) thins as it approaches the center axis of the tool. This is due to the curved geometry of the bottom edge. Because of this chip thinning phenomenon, the feed of the tool must be increased so that the tool is actively engaged in cutting and does not rub against the workpiece. Rubbing will increase friction, which in turn raises the level of heat around the cutting zone and causes premature tool wear. Because this tool requires an increased chip load to maintain a viable cutting edge, the tool has been given the name “High Feed Mill.”
Other Phenomena Due to Curved Geometry of Bottom Edge
The curved geometry of the bottom edge also sanctions for the following actions to occur:
- A programmable radius being added to a CAM tool path
- Scallops forming during facing operations
- Different-shaped chips created during slotting applications, compared to HEM roughing
Programmable Radius
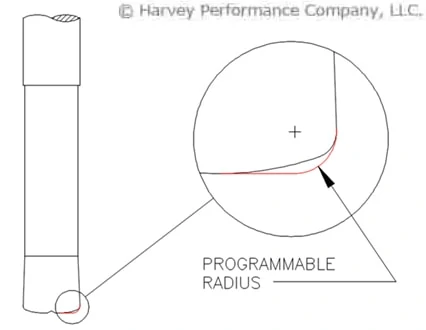
Helical Solutions’ High Feed End Mills has a double radius bottom edge design. Because of this, the exact profile cannot be easily programmed by some CAM software. Therefore, a theoretical radius is used to allow for easy integration. Simply program a bullnose tool path and use the theoretical radius (seen below in Figure 2) from the dimensions table as the corner radius.
Managing Scallops
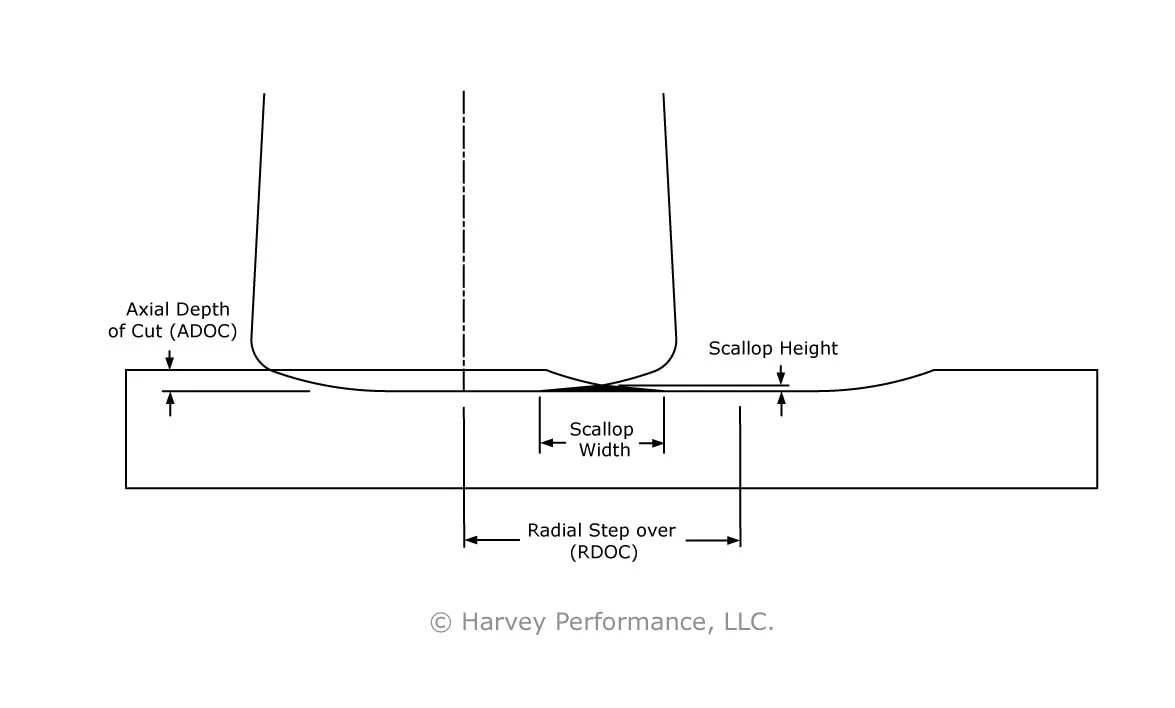
A scallop is a cusp of material left behind by cutting tools with curved profiles. Three major factors that determine the height and width of scallops are:
- Axial Depth of Cut
- Radial Depth of Cut
- Curvature of Bottom Edge or Lead Angle
Figure 3 below is a depiction of the scallop profile of a typical roughing cut with a 65% radial step over and 4% axial depth of cut. The shaded region represents the scallop that is left behind after 2 roughing passes and runs parallel to the tool path.
Figures 4 and 5 show the effects of radial and axial depth of cuts on the height and width of scallops. These figures should be viewed in the context of Figure 3. Percentage by diameter is used rather than standard units of measurement to show that this effect can be predicted at any tool size. Figure 4 shows that a scallop begins to form when the tool is programmed to have a radial step over between 35% and 40%. The height increases exponentially until it is maximized at the axial depth of cut. Figure 5 shows that there is a linear relationship between the radial step over and scallop width. No relationship is seen between scallop width and axial depth of cut as long as ADOC and the radius of curvature of the bottom cutting edge remains consistent.
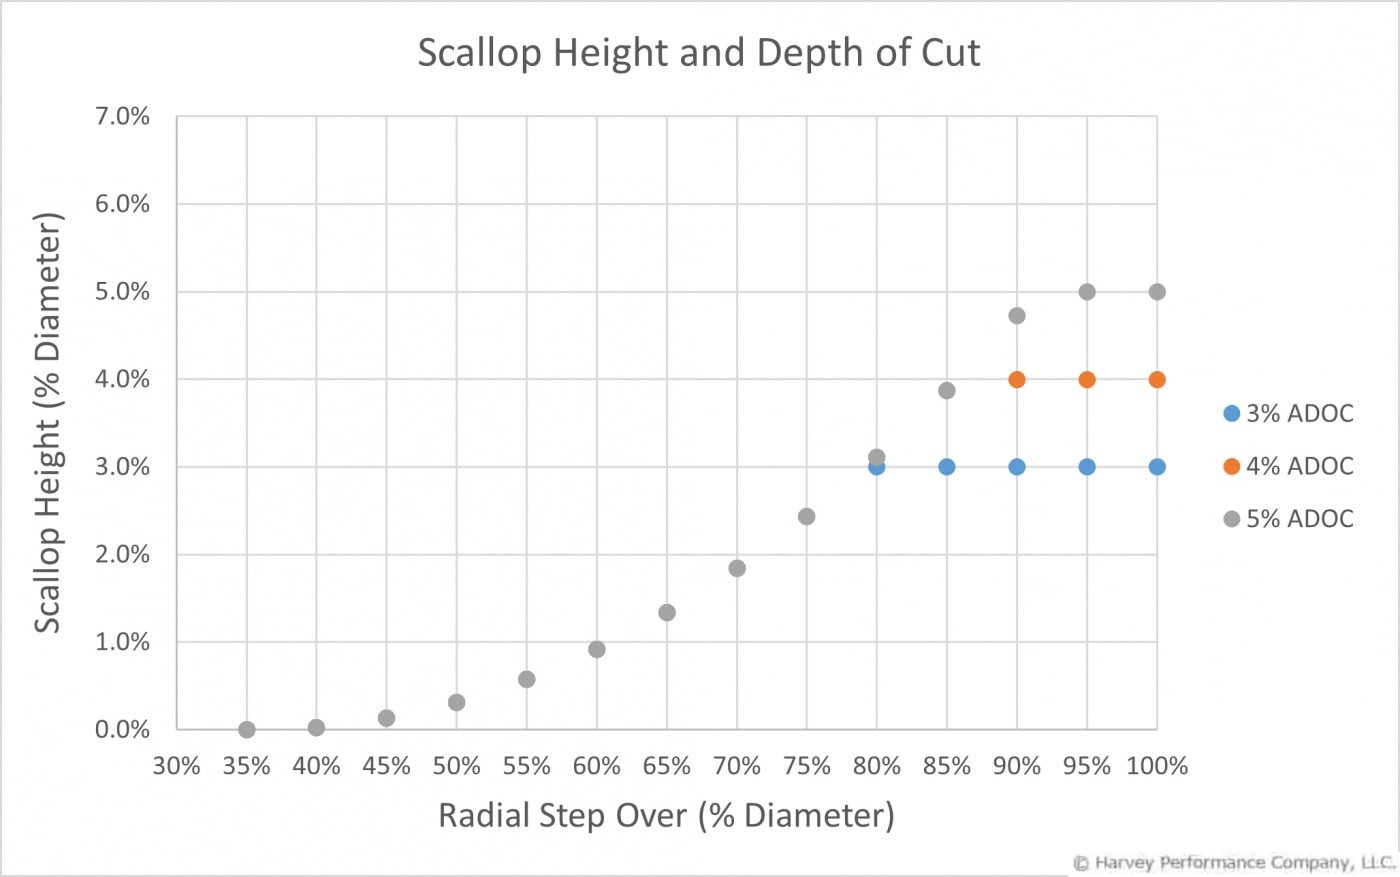
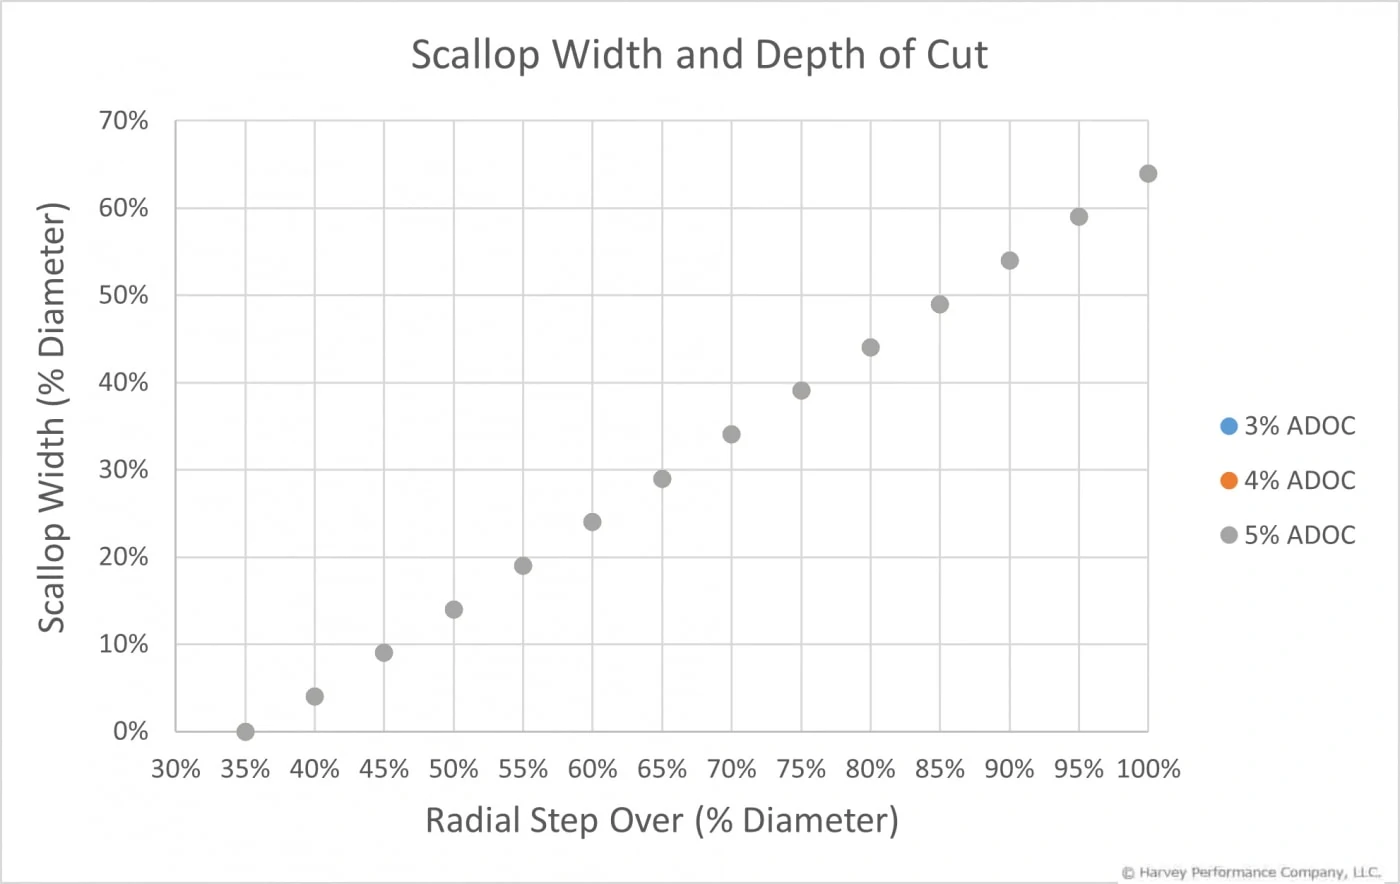
From the graphs in Figures 4 and 5 we get the following equations for scallop dimensions.
Notes regarding these equations:
- These equations are only applicable for Helical Solutions High Feed End Mills
- These equations are approximations
- Scallop height equation is inaccurate after the axial depth of cut is reached
- RDOC is in terms of diameter percentage (.55 x Diameter, .65 x Diameter, etc…)
Shop Helical Solutions’ Fully Stock Selection of High Feed End Mills
Curvature of the Bottom Edge of High Feed End Mills
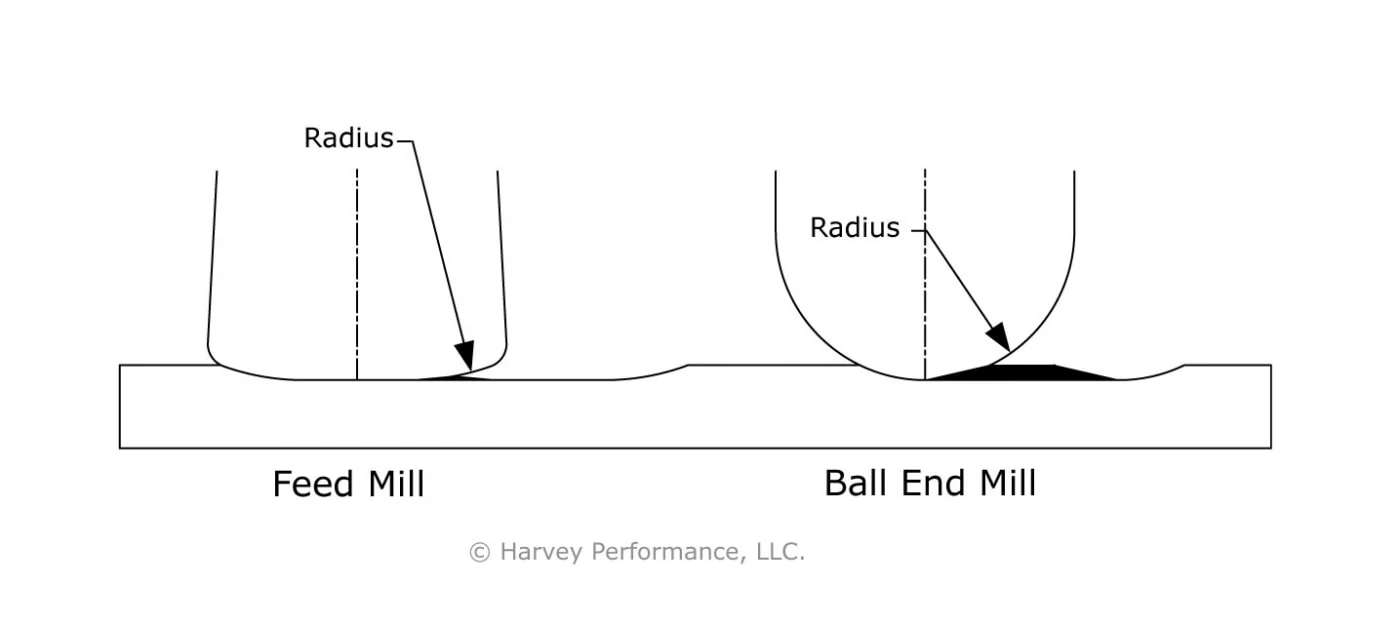
The smaller the radius of curvature, the larger the height of the scallop. For example, the large partial radius of the Helical Solutions High Feed End Mill bottom cutting edge will leave a smaller scallop when compared to a ball end mill programmed with the same tool path. Figure 6 shows a side by side comparison of a ball end mill and high feed mill with the same radial and axial depth of cut. The scallop width and height are noticeably greater for the ball end mill because it has a smaller radius of curvature.
Full Slotting
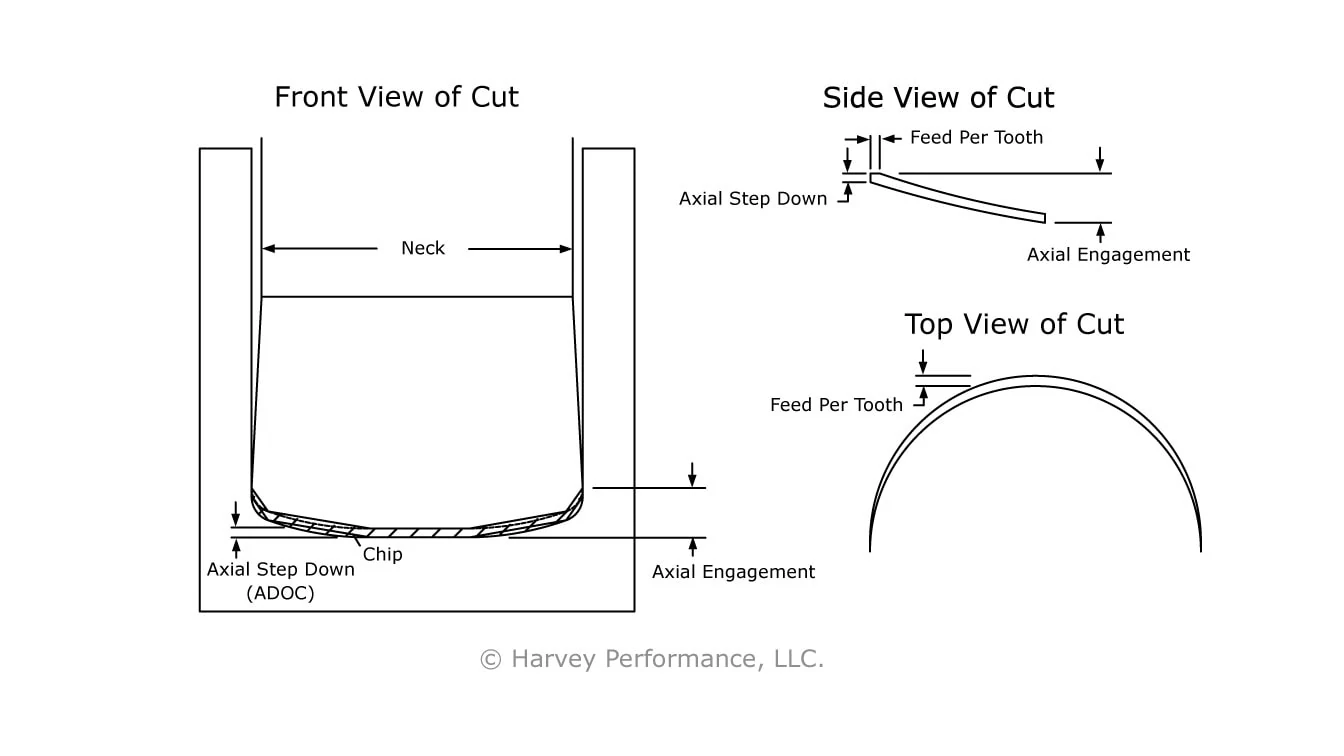
When slotting, the feed rate should be greatly reduced relative to roughing as a greater portion of the bottom cutting edge is engaged. As shown in Figure 7, the axial step down does not equate to the axial engagement. Once engaged in a full slot, the chip becomes a complex shape. When viewing the chip from the side, you can see that the tool is not cutting the entirety of the axial engagement at one point in time. The chip follows the contour on the slot cut in the form of the bottom edge of the tool. Because of this phenomenon, the chip dips down to the lowest point of the slot and then back up to the highest point of axial engagement along the side. This creates a long thin chip that can clog up the small flute valleys of the tool, leading to premature tool failure. This can be solved by decreasing the feed rate and increasing the amount of coolant used in the operation.
In summary, the curved profile of the bottom edge of the tool allows for higher feed rates when high feed milling, because of the chipping thinning effect it creates with its low lead angle. This low lead angle also distributes cutting forces axially rather than radially, reducing the amount of chatter that a normal end mill might experience under the same conditions. Machinists must be careful though as the curved bottom edge also allows for the formation of scallops, requires a programmable radius when using some CAM packages, and make slotting not nearly as productive as roughing operations.

As a member of Harvey Performance Company’s New Product Development team, Robert strategized new products to introduce with each new catalog released by Harvey Performance Company’s collection of brands.


Thanks for sharing this very informative blog post regarding the secret mechanics of high feed end mill.
High Feed Mill is a great method to achieve high metal removal, utilize the full capability of today’s machines and achieve long tool life.