
Most Common Methods of Tool Entry
Tool entry is pivotal to machining success, as it’s one of the most punishing operations for a cutter. Entering a part in a way that’s not ideal for the tool or operation could lead to a damaged part or exhausted shop resources. Below, we’ll explore the most common part entry methods, as well as tips for how to perform them successfully.
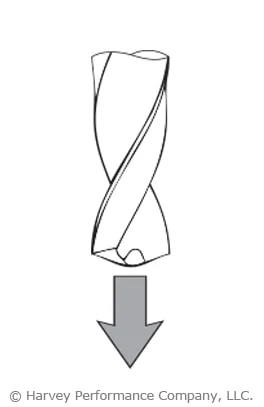
Pre-Drilled Hole
Pre-drilling a hole to full pocket depth (and 5-10% larger than the end mill diameter) is the safest practice of dropping your end mill into a pocket. This method ensures the least amount of end work abuse and premature tool wear. It also facilitates smoother chip evacuation, reducing the risk of chip buildup and potential tool breakage. Machinists often use this technique when working with materials prone to chip welding or built-up edge formation, ensuring consistent machining performance.
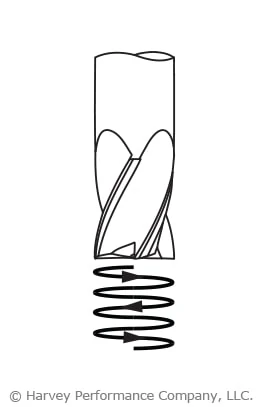
Helical Interpolation
Helical Interpolation is a very common and safe practice of tool entry with ferrous materials. Employing corner radius end mills during this operation will decrease tool wear and lessen corner breakdown. With this method, use a programmed helix diameter of greater than 110-120% of the cutter diameter. Moreover, helical interpolation offers advantages in achieving precise surface finishes, making it a preferred choice for applications requiring high precision and surface quality, such as aerospace and medical device manufacturing.
Ramping-In
This type of operation can be very successful, but institutes many different torsional forces the cutter must withstand. A strong core is key for this method, as is room for proper chip evacuation. Using tools with a corner radius, which strengthen its cutting portion, will help. Additionally, ramping-in allows for efficient material removal with reduced axial forces, minimizing workpiece distortion and enhancing dimensional accuracy. Machinists often employ this technique in contouring and pocketing operations, where maintaining part integrity is crucial.
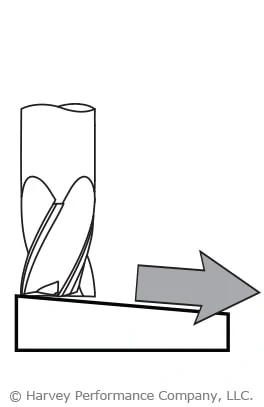
Suggested Starting Ramp Angles:
Hard/Ferrous Materials: 1°-3°
Soft/Non-Ferrous Materials: 3°-10°
For more information on this popular tool entry method, see Ramping to Success.
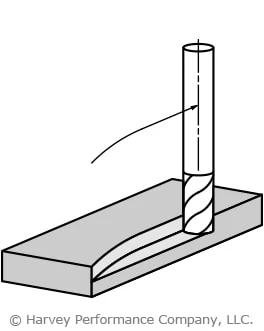
Arcing
This method of tool entry is similar to ramping in both method and benefit. However, while ramping enters the part from the top, arcing does so from the side. The end mill follows a curved tool path, or arc, when milling, this gradually increasing the load on the tool as it enters the part. Additionally, the load put on the tool decreases as it exits the part, helping to avoid shock loading and tool breakage. Machinists often utilize this technique in mold making, die sinking, and 3D contouring operations, enhancing productivity and surface finish quality.
Straight Plunge
This is a common, yet often problematic method of entering a part. A straight plunge into a part can easily lead to tool breakage. If opting for this machining method, however, certain criteria must be met for best chances of machining success. The tool must be center cutting, as end milling incorporates a flat entry point making chip evacuation extremely difficult. Drill bits are intended for straight plunging, however, and should be used for this type of operation.

Straight Tool Entry
Straight entry into the part takes a toll on the cutter, as does a straight plunge. Until the cutter is fully engaged, the feed rate upon entry is recommended to be reduced by at least 50% during this operation. Machinists often resort to straight tool entry in simple machining operations with limited tool access or where other entry methods are impractical. However, it’s crucial to monitor tool wear and chip evacuation carefully to prevent chip buildup and potential tool breakage. Adjusting cutting parameters based on material properties and part geometry can further enhance machining efficiency and tool life.

Roll-In Tool Entry
Rolling into the cut ensures a cutter to work its way to full engagement and naturally acquire proper chip thickness. The feed rate in this scenario should be reduced by 50%. Roll-in tool entry is particularly advantageous in slotting and profiling operations, where maintaining consistent chip thickness is critical for surface finish quality and dimensional accuracy. Machinists often utilize this technique in high-speed machining applications, maximizing material removal rates while minimizing tool wear and heat generation.

Mastering various tool entry techniques is essential for machining success. By understanding and implementing these methods effectively, machinists can optimize performance while prolonging the lifespan of their tools. Continual evaluation of cutting conditions and adaptation of entry strategies based on material properties and part geometry are key to achieving superior machining results.



Is helical interpolation really *only* recommended for ferrous materials? Is actually it not recommended for non-ferrous materials like aluminum, or is it just not as necessary in those cases?
Hello Ian,
Great question! Helical Interpolation is not only for ferrous material we stated in the article, “Helical Interpolation is a very common and safe practice of tool entry with ferrous materials”. Helical Interpolation is also recommended in non-ferrous material.
Thanks Guy!
What would you think about a counterbored hole that already had the main hole drilled and now I want to use interpolation to get my endmill down to the depth of the counterbore instead of plunging it down? (the endmill is just a bit bigger than the hole and a bit smaller than the counterbore). I won’t be able to interpolate more than the tool diameter in this case but the predrilled hole might make up for that? Also, what is your recommendation on speeds and feeds of interpolation?
Hello Reuven,
Great question! If you are able to start the interpolation toolpath before the end mill touches the material you should be able to get to your desired depth. Without information into the whole application it is tough to be able to recommend speeds and feeds for this application, but one place you can look is another blog post “Speeds and Feeds 101” this should provide some help. If you need further help please reach out to our tech team at [email protected] with all your information and application information and they will be able to help you.
Could please explain more about Roll in entry. How to decide the radius and angle of the rolling arc? How it will generate optimised thick chip during entry?