Climb Milling vs. Conventional Milling
There are two distinct ways to cut materials when CNC milling: Conventional Milling (Up) and Climb Milling (Down). The difference between these two techniques is the relationship of the rotation of the cutter to the direction of feed. In Conventional Milling, the cutter rotates against the direction of the feed. During Climb Milling, the cutter rotates with the feed.
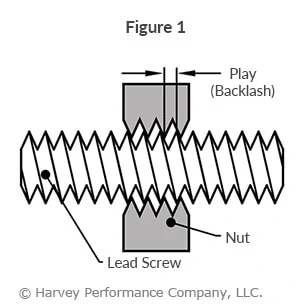
Conventional Milling is the traditional approach when cutting because the backlash, or the play between the lead screw and the nut in the machine table, is eliminated as seen in Figure 1 below. Recently, however, Climb Milling has been recognized as the preferred way to approach a workpiece since most machines today compensate for backlash or have a backlash eliminator.
Key Conventional and Climb Milling Properties:
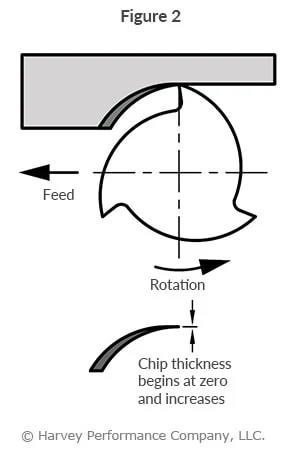
Conventional Milling (Figure 2)
As previously stated, traditionally conventional milling has been the common choice for most machinists. This is where the cutting edge of the tool is actually rotating away from the direction of the feed. An example of this is seen in Figure 2 below. Until recently, this has been the common choice due to backlash however, the rise of climb milling has caused machinists or machines to adapt and compensate for this issue.
That is not to say there aren’t benefits to climb milling. For example, this strategy offers a machinist more control and less vibration than its climb milling counterpart. Similarly, for materials that traditionally chatter or tear, conventional milling would be the proper strategy to choose. On the other hand, here are some reasons why it might be most beneficial to adopt a climb milling strategy:
- Chip width starts from zero and increases which causes more heat to diffuse into the workpiece and produces work hardening
- Tool rubs more at the beginning of the cut causing faster tool wear and decreases tool life
- Chips are carried upward by the tooth and fall in front of cutter creating a marred finish and re-cutting of chips
- Upwards forces created in horizontal milling* tend to lift the workpiece, more intricate and expansive work holdings are needed to lessen the lift created*
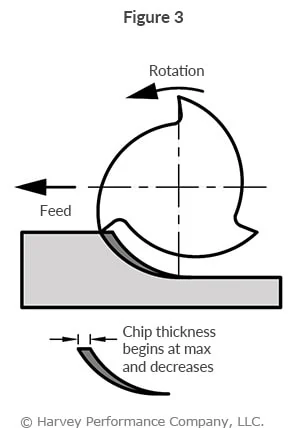
Climb Milling (Figure 3)
As machinists are always trying to find ways to increase efficiency and tool life, climb milling has gotten a lot of recent traction in the space. Less heat is generated within the tool, and friction is more easily mitigated. These two alone lead to longer tool life, allowing for more parts completed per tool, lowering a shops bottom line. Also, climb milling can lead to a better surface finish due to how the chips are formed at the cutting edge.
With more modern machines now compensating for backlash or utilize backlash eliminators, it has become a much easier strategy to adopt within shops. While we went over some reasons why climb milling is not an effective strategy above, here are some reasons why a machinist may want to explore climb milling:
- Chip width starts from maximum and decreases so heat generated will more likely transfer to the chip
- Creates cleaner shear plane which causes the tool to rub less and increases tool life
- Chips are removed behind the cutter which reduces the chance of chip recutting
- Downwards forces in horizontal milling is created that helps hold the workpiece down, less complex work holdings are need when coupled with these forces
- Horizontal milling is when the center line of the tool is parallel to the work piece
When to Choose Conventional or Climb Milling
Climb Milling is generally the best way to machine parts today since it reduces the load from the cutting edge, leaves a better surface finish, and improves tool life. During Conventional Milling, the cutter tends to dig into the workpiece and may cause the part to be cut out of tolerance.
However, though Climb Milling is often the current preferred way to machine parts, there are times when Conventional Milling is the necessary milling style. One such example is if your machine does not counteract backlash. In this case, Conventional Milling should be implemented. Without accounting for backlash, breakage can occur due to the forces within the machine during tool engagement.
In addition, conventional milling should also be utilized on casting, forgings or when the part is case hardened. This is due to the cut beginning under the surface of the material, where it will gradually build a chip. Climb milling into these materials will see maximum chip thickness on engagement, which could lead to premature failure of the cutting edge due to the forces generated.




Thank you very much for this highly valuable information.
This is one of those left hand cutters! How about turning the tool, and cutter the correct direction. G41 climb cutting on the right side. G42 or conventional cutting on the left. Sorry I couldn’t help myself.
It depends on your perspective. Are they showing a view looking down at the work piece or looking up from the workpiece.
There can only be one way to interpret the cut because machines only turn in one direction. In the examples the view has to be from under the workpiece looking up at the tool
Technically, machines can go either direction (M03 or M04 in Gcode), but basically everyone uses M03 in 99.9% of cases
Great article. I’ve had to use conventional milling when for example, I’d have my thin unsupported part sticking out of work holding with the tool path contouring around the part (think milling end while cutting a part in a lathe) with the material flexing would cause snapping while climbing because it wants to take a large bite as opposed to ramping the cut in. But yeah, 95% or more is climbing.
Very informative article.practical metal removal techniques explained , having possible implications on tool life.
Good Article! Thank you very much!
“Conventional Milling should be… utilized on casting, forgings”
In my head, I logically organize castings as least processed, forgings as most processed, and everything else (hot rolled, cold rolled, extruded) somewhere in between. So to me, that part seems to say ‘use conventional milling for everything’, which is obviously not right. Could you show me where I went wrong,? More specific examples, like case hardening, why a particular direction of cut is preferred for a chunk of metal with unknown provenance.
Thank you for the question Dustin! We would suggest conventional milling when your material has a rough surface, such as cast iron, or is anodized because when conventional milling your cut is scooping underneath the surface to remove your material making it easier on your tool. Also, you want to conventional mill when using a dovetail cutter that has a weak neck diameter because this will help relieve the pressure on the neck of your tool.
This is great info. I have always conventional milled with face mill to remove the scale off of titanium. Tool life is increased and getting under that scale to machine it off instead of slamming the insert into the scale each time. Once scale has been removed, go back to climb cutting.
Thanks for this very clear and informative explanation. It has been decades since I worked in a factory. Back then the Bridgeport milling machines had terrible backlash. They would chatter or jump when using climb milling. Plus, if one was approaching the end of a cut, one wouldn’t know if the tool would grab at that point and pull the work past the past the desired end point. I almost exclusively used conventional milling and couldn’t understand why many people on YT now talk about using climb milling.
A 60 year old worn out manual Bridgeport is all I have to work with. (It is in better shape than my 65 year old worn out body.) I rarely climb mill anything, specially not steel. But if the cut is really light, and I want a good finish, I climb mill. , I apply some drag with the table lock screw, and that seems to eliminate the chatter.
Hey there, first of all thank you so much for this post and honestly I was searching for the same information from last few days. Keep posting and keep sharing..
I want to mill a slot, that needs to be as smooth & accurate as possible.
.375 wide 187 deep & .625 long.
I DON’T think you can do that in 1 or 2 steps.
Please, enlighten me!
Bridgeport 2600 max rpm.
Hey Ronald, our tech team would love to be able to help you out and enlighten you! Send an email to [email protected]
Added uses for conventional cutting:
Never climb cut across the end of an upstanding thin rib in aluminum or plastic (You will rip it off). Use reduced feed and conventional cut it or use multiple small depth cuts. Commonly made cutting to length T or L extrusions. You’ll only make this mistake once.
It helps to conventional cut torched or burnt out steel plate rough profiles first, then switch to climb cut after you mill through the slag. Same principal as case hardened material. Corn-Cob or serrated cutters work nice here too.
I think you left out force vectors during cutting. This can influence tool defection and taper on the side wall on the part. The force vectors are different magnitudes between climb and convectional cutting, so this impacts work holding and this parts or this walls.
That was supposed to say “thin parts or thin walls”. maybe autocorrect changed it
I have a Warco 16B milling machine. This is a medium size manual hobby mill. I am confused as people recommend Conventional and Climb milling in about even numbers, this goes for YouTube too.
What would you recommend on this type of machine?
Your help would be appreciated as I last worked in industry in 1979 so I am extremely out of date.
I generally mill Conventionally.
Great question Graham! There are many factors that go into choosing which method is best for you. Please send an email to [email protected] with all your information and they will be able to help you out as soon as possible.
Thanks
I like what you said about chip width working. I need a milling machine for some steel. I’ll have to get a dye-cutter that is discounted.
nice car racing game i eally love in it maja aa gaya graphik very nice
What would be your recommendation for cutting composites such as carbon or glass?
Hi Thomas,
Below is the selection of tooling we offer for composite material.
https://www.harveytool.com/products/material-specific-end-mills/composites
This page will also have speeds and feeds available on how to properly run each tool.
Have seen this article several times. One consideration is roughing, my observation is that the load against the cutter when cutting in the conventional direction is lower and reduces the risk of tool breakage. Another is where the tool-paths leave “posts” in corners and so-fourth when hogging out parts, conventional milling will not grab into a post and break the cutter. Another application is when making long thin flats in rod shaped parts either on a indexing head or on a swiss type automatic lathe through a guide bushing, the conventional path will produce less taper and more parallel surfaces. Just a few thoughts.
Great explanation of the differences between climb milling and conventional milling! I appreciate how you highlighted the advantages of climb milling, especially in reducing tool wear. It’s very informative for someone looking to refine their machining techniques. Thanks for sharing!