Complex parts require more than a single operation. Features such as contours, chamfers, engraved details, and precision holes often demand multiple tooling strategies working together throughout the machining process.
In the video below, watch a single component progress from a block of Ti-6Al-4V to a finished part through more than 10 machining applications, each supported by specialized Harvey Tool solutions.
Explore the full range of solutions available in the 2026 Harvey Tool Catalog, featuring more than 31,000 miniature and specialty cutting tools designed to support even the most demanding applications.
https://www.harveyperformance.com/wp-content/uploads/2026/02/Feature-Image-Harvey-Tool-2026-Catalog-Video-IMG.jpg5251400Harvey Performance Companyhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngHarvey Performance Company2026-02-27 15:07:592026-03-31 09:47:45Machining a Complex Part with Harvey Tool
Drilling applications require careful consideration of material, production volume, and machine setup to ensure optimal hole quality, tool life, and cost. Harvey Performance Company offers drills in three primary substrates: carbide, cobalt, and high-speed steel (HSS). This guide breaks down the differences between the drilling substrate options and helps you choose the right tool for your specific application.
Solid Carbide Drills
Advantages of Carbide Drills
Extreme Hardness and Wear Resistance
Carbide drills maintain sharp cutting edges longer than HSS or cobalt, even in abrasive materials. This reduces tool changes and helps to maintain consistent hole quality.
High Heat Tolerance
Carbide can withstand cutting temperatures above 2,100°F (1,150°C), allowing higher speeds and feeds for faster material removal and shorter cycle times.
Precision Machining
Carbide maintains tight tolerances and excellent surface finish in hard steels, tool steels, ceramics, composites, and high-temperature alloys, making it ideal for precise, high-performance applications.
Long-term Cost Efficiency
Although the initial cost is higher, carbide’s longer tool life reduces frequent tool changes, lowering overall costs in high-volume production.
Drawbacks of Carbide as a Drill Substrate
Brittle Nature
Carbide is more prone to chipping or breaking if the machine setup is not rigid, feed rates are too aggressive, or vibration is present.
Regrinding Requirements
Carbide usually requires CNC grinding equipment for precise sharpening, unlike HSS, which can often be reground using conventional machines.
Initial Investment
Carbide has a higher upfront cost, which may not be justified for use in short runs or soft materials, where less expensive HSS or cobalt drills can provide adequate performance.
What are the Ideal Applications for Carbide Drills?
Carbide drills excel in:
Large production runs requiring consistent tool life
Hard materials above 45 HRC, such as tool steels and high-temperature alloys
Applications requiring high-speed cutting and maximum material removal
Situations demanding precise hole tolerances and surface finish
Example: Valor Holemaking High Performance Carbide Drills are engineered to provide unmatched precision and repeatability in difficult-to-machine materials. Material-specific geometries and coolant-through designs improve heat management and tool life in demanding applications.
High Speed Steel (HSS) Drills
Advantages of HSS Drills
Tough and Durable
High Speed Steel is the least brittle of the three materials, reducing the risk of breakage during less rigid setups.
Easier to Regrind
HSS Drills can be sharpened and reconditioned using conventional grinding equipment, which reduces shop complexity and cost.
Cost-Effective
The lower cost-per-tool makes HSS ideal for small jobs or low-volume production where long-term tool life is less critical.
Versatile for Soft Materials
HSS performs well in most non-ferrous metals providing reliable results for general-purpose machining without the higher cost of harder substrates.
Drawbacks of High Speed Steel Drills
Limited Heat Tolerance
High Speed Steel Drills can only handle cutting temperatures up to 1,100°F (600°C), restricting cutting speeds and material removal rates.
Shorter Tool Life
HSS Edges dull faster than cobalt or carbide, requiring more frequent replacement, affecting productivity.
Not Ideal for Very Hard Materials
High speed steel tools cannot reliably machine steels above 45 HRC or high-temperature alloys.
What are the Ideal Applications for HSS Drills?
HSS drills are ideal for:
Soft materials like aluminum, brass, and other non-ferrous metals
Small production runs or one-off jobs where tool life is less critical
Shops without CNC grinding capability
Situations where cost and ease of regrind outweigh long-term performance
Example: Titan USA High Speed Steel Drills provide reliable performance for general-purpose machining and softer materials, offering versatility for low- to medium-volume operations.
Cobalt Drills
Advantages to Cobalt Drilling
Intermediate Hardness
Cobalt is harder than HSS but less brittle than carbide, providing a balance of toughness and wear resistance.
Higher Heat Resistance
Cutting temperatures up to 1,580–1,616°F (860–880°C) enable faster speeds and feeds than HSS.
Moderate Cost
Cobalt drills offer longer tool life than HSS without the higher upfront cost of carbide.
Capability for Harder Materials
Can machine steels up to 58 HRC, handling materials that high speed steel struggles with, while remaining more forgiving than carbide.
Cobalt Drill Disadvantages
Less Wear-Resistant than Carbide
While cobalt drills are harder than HSS, they are still not as wear-resistant as carbide. In extremely abrasive materials, cobalt drills will wear much faster than solid carbide, which can increase tool changes and impact long-term cost in high-production runs.
Slightly More Brittle than HSS
Cobalt is harder than HSS, making it more prone to chipping or breakage. Regrinding may require careful handling or CNC equipment to maintain geometry.
Not Suitable for Extreme High-Temperature Alloys or Very Hard Materials
Cobalt cannot maintain performance in very hard steels or high-temperature alloys. Carbide is needed for materials above 60 HRC or extreme heat applications.
What Applications are Ideal for Cobalt Drills?
Cobalt drills work well for:
Medium-volume jobs with harder materials
Applications requiring more speed and heat tolerance than HSS
Shops seeking a balance of cost, tool life, and performance
Example: Titan USA Cobalt Drills are a solid choice for harder-to-machine materials that do not require carbide, providing longevity and moderate speed capabilities.
What Factors Influence What Drill Substrate to Choose?
Every drilling job is unique, and the optimal drill substrate depends on your specific requirements. Key considerations include:
Material Hardness
Production Volume and Job Size
Machine Rigidity
Budget
Regrinding Capabilities
Desired Cutting Speed and Material Removal Rate
No drill fits every job, and these factors are intended as a guide to help machinists choose the right substrate to improve efficiency, precision, and cost-effectiveness.
https://www.harveyperformance.com/wp-content/uploads/2026/02/TitanUSA-Drills-033-PM-0325-001.jpg5251400Isabella Lucianohttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngIsabella Luciano2026-02-05 16:22:522026-02-05 16:22:56Drill Substrate Guide: HSS vs Cobalt vs Carbide
With the release of Micro 100’s 2025 Spring Catalog comes a new family of broaching tools, marking their debut within both the Micro 100 and Harvey Performance brands. Alongside this tooling launch are several differences in application methods and recommended running parameters.
What is Broaching?
Broaching, while performed in a lathe, is slightly different from the classic boring and grooving operations we encounter daily.
In a traditional turning operation, the workpiece rotates while the tool remains stationary. In a broaching operation, neither the workpiece nor the tool spins. Instead, the tool advances toward the workpiece and removes material in very small increments, similar to planing a block of wood.
Micro 100’s Offering
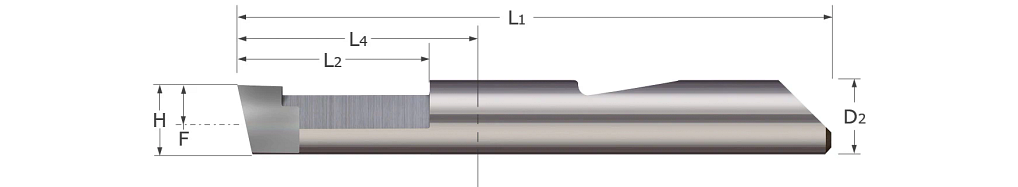
All broaches come on a Micro 100 Quick-Change shank, with sizes ranging from .1875” to .375”, depending on the broach size. These QC broaching tools are coolant-fed to promote better chip evacuation. An optional nACRo coating is available, enhancing resistance to wear and heat, which is especially useful in applications involving difficult-to-machine materials.
Keyway Broaches
Keyway broaches, as their name suggests, are used to cut keyways commonly found in power transmission applications involving gears and pulleys.
Micro 100 offers two styles of keyway broaches, available in both standard and metric sizing. This offering provides machinists with a range of sizes that are necessary to meet their application needs.
Imperial Offering
Micro 100’s standard-sized broaches come in widths of .0938”, .1250”, .1875”, and .2500”. Maximum broach depths of .500”, 1.000”, or 1.500” are available, depending on the broach width.
Metric Offering
Our metric keyway broaches are available in nominal widths from 2 mm to 6 mm. Each size is measured according to the desired fit and offered in C11, JS9, or P9 tolerance grades.
C11 reflects a “loose fit” tolerance, useful in applications where the keyway may be exposed to corrosion, dust, or other contaminants, or where deformation may occur.
JS9 represents a “normal fit”—not a press fit, but not a loose fit either. This is often required in situations where the key needs to be adjusted or shifted without much force or difficulty.
The tightest of the three offered tolerance classes is P9, which represents a “press fit.” In this case, the keyway is cut slightly smaller than the key, forcing it into the slot to create a very tight and secure connection.
Square Broaching
Micro 100 also offers square broaching tools. These broaches, like the keyway style, are pushed into the workpiece and remove material in multiple passes. They are primarily used to create the square socket found at the top of certain screws, commonly seen in machinery, construction, or other industrial applications.
Our square broaches come in metric sizes and can cut square holes ranging from 1.5 mm to 4.0 mm. When examining the geometry of these tools, you’ll notice they are cut to one corner of the square profile. Unlike keyway broaches, they must be rotated 90° when one corner is cut to create the remainder of the square form.
Although they have a fixed broach width, our square broaches are capable of cutting a range of square sizes. Take our QBRSQ-1520, for example—it features a .056” width and can cut squares from .059” to .078” (1.5 mm to 2.0 mm). When selecting a tool, it’s important to base your choice on the desired finished hole size, rather than the width of the cutter itself.
Hexagonal Broaching
The final option in Micro 100’s broaching lineup is our hexagonal broach style. These tools function similarly to the square broaches mentioned earlier, with the form created in six portions. Our hexagonal broaches can cut forms as small as .078” (2.0 mm) and up to .315” (8.0 mm). As with the square broaches, it’s important to select a tool based on the desired finish size of the hole, rather than the tooth width itself.
Hexagonal holes are often designed to work in conjunction with Allen keys. They are also commonly used for socket head cap screws. These fasteners are widely used across various industries, including automotive and construction settings.
What to do Before Making Your First Chips
Before making a cut with Micro 100’s broaching tools, there are a few important things to ensure are in place. Due to the high force involved in broaching, your machine should be equipped with a mechanical spindle lock. This lock helps achieve a higher-quality finish and, more importantly, improves feature accuracy.
The use of coolant is also strongly encouraged whenever possible, as it helps increase tool life, improve surface finish, and enhance chip evacuation. If your application requires broaching within a blind hole, be sure to create a cross hole or relief groove at the bottom of the hole to allow chips to evacuate properly.
Mastering Square & Hexagonal Broaching
To begin, the broach dimensions must be measured accurately and programmed into the machine. Ensure the tool is positioned at the 12 o’clock location to allow proper chip evacuation.
If cutting a hexagonal profile, the pre-drill should be approximately 1.035 times the desired feature size (1.1× for a square profile).
Before the first pass is made, visually check the tool path by positioning the tool at the starting point of the stroke, and program a stop there to verify correct alignment.
After each pass, ensure the tool is radially clear of the groove before fully retracting it. On the final return stroke, completely remove the broach from the hole. Finally, rotate the workpiece by 60 degrees—90 degrees for a square profile—and repeat the cutting process for the remaining corners.
Best Practices for Keyway Broaching
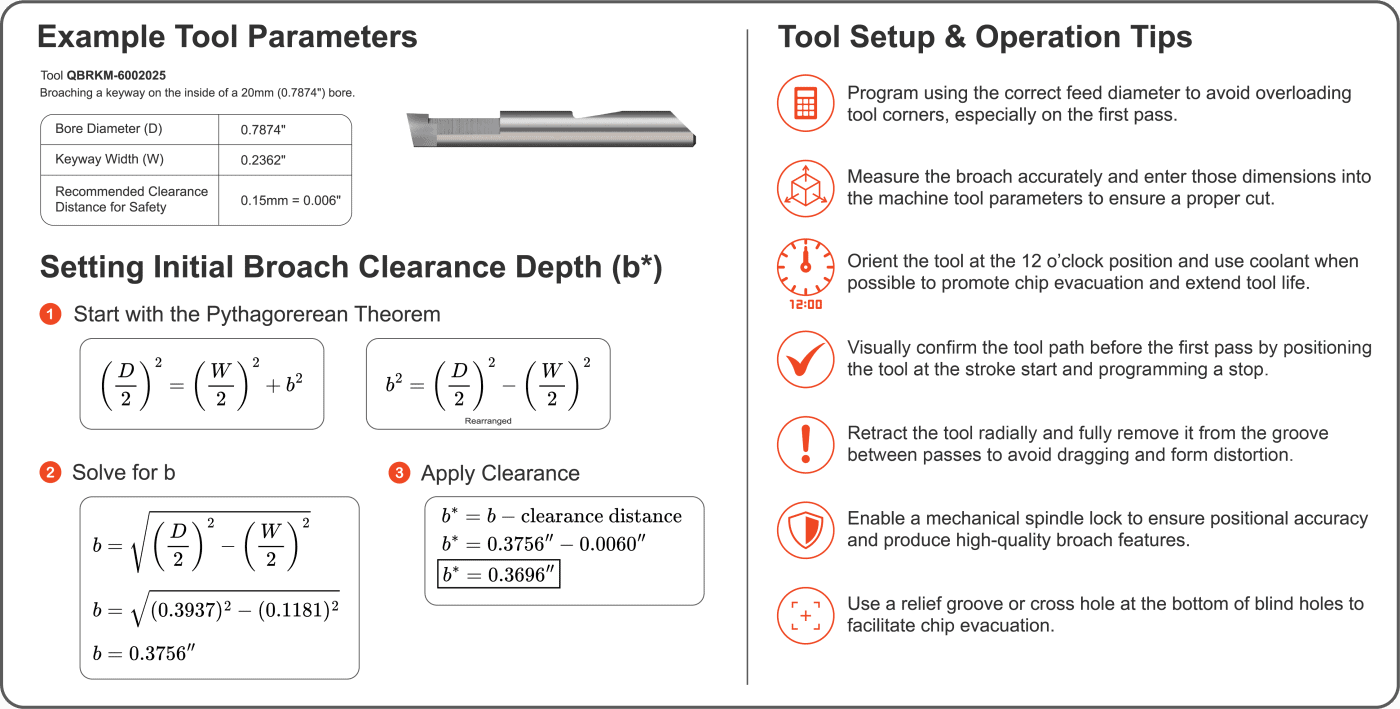
Keyway broaches require an additional calculation to determine the correct starting position for the first pass. An example calculation is provided below.
After the initial pass is completed, continue cutting normally until the desired keyway size is met. As with square and hex broaching, ensure the tool is radially clear of the groove after each pass before retracting. On the final return stroke, completely remove the broach from the hole.
In Summary
Micro 100s offering of broaching tools is fit for a large variety of broaching applications you may come across. Whether square, standard, or hexagonal, metric or imperial, Micro 100 has the tools to help you cut every step of the way.
To see the full range of tooling that Micro 100 has to offer, please visit our website micro100.com.
For any further questions regarding our broaching tools or Micro 100 as a whole, please don’t hesitate to call us at +1 844-393-8665 or email us at [email protected].
https://www.harveyperformance.com/wp-content/uploads/2025/11/Broaching-Featured-Image-Rev-01.jpg5251400Steven Velazquezhttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngSteven Velazquez2025-11-20 11:30:002025-12-03 14:09:16Micro 100 Broaching Tools: Everything You Need to Know
Tool coatings are added to protect against the forces that wear down cutting tools. They play a critical role in CNC machining by reducing heat generation and friction while enhancing overall tool performance. Below is an overview of Helical Solutions’ coating options, including which tool families they pair with, the applications they’re best suited for, and helpful application tips.
Helical Solutions demonstrates its commitment to performance by delivering high-performance carbide end mills and tools designed to reduce cycle times, improve part finishes, and extend tool life. This is achieved through a focus on exceptional quality and innovation, utilizing precision CNC manufacturing, advanced design techniques, and a world-class team of engineers and technical experts. Helical Solutions aims to be a true superior product performance, and responsive technical support.
The following information will help machinists understand the differences between Helical’s coating options and how to select the right one based on material and application.
What Are Tool Coatings and Why Are They Important?
Tool coatings are applied to a tool’s cutting surface through a process called PVD (Physical Vapor Deposition). PVD and CVD are two different types of coating applications, with PVD being the common process for Helical’s tools.
This near-vacuum process distributes micron-thick layers evenly onto a properly prepared tool, helping it maintain a sharper cutting edge. When selecting tool coatings, machinists should consider material type, coolant use, and how the
material and operation may affect the cutting edges. Understanding these factors is essential to extending tool life.
Some key benefits of coatings include improved thermal resistance, better chip evacuation, increased lubricity (which allows chips to slide more easily down the flute), and higher microhardness. These properties reduce tool wear, enhance performance in material-specific applications, and extend tool life during production runs.
Helical’s coating lineup is designed with specific materials and applications in mind. Selecting the right coating for your job can have a major impact on tool life, heat control, and overall performance.
How to Choose the Right Coating:
Choosing the proper coating for your application is crucial, as each Helical coating is optimized for specific materials. Consider the following when selecting: – What material are you machining? – Will the material work harden quickly under heat? – What is its coefficient of friction? – Will you be using coolant? – What is your expected tool life for this production run?
Application Tips:
Coatings in Coolant Applications:
Most coatings perform better with coolant, but there are exceptions.
Tplus performs well in many materials, but when cutting hardened steels, the combination of high heat and coolant can cause thermal shock, resulting in tool fractures.
In composites and non-metallic materials—often machined with Dplus—using coolant can create a slurry and increase wear between the tool and workpiece. For these materials, dry machining is generally preferred.
Zplus vs. Nplus vs. Dplus
For aluminum and non-ferrous applications, coatings are found on Helical’s HVAL and HMAF tool families.
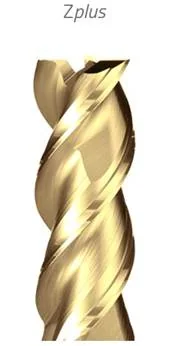
– Zplus is Helical’s longstanding coating for aluminum and non-ferrous materials. – Nplus improves tool life compared to Zplus and features a harder, smoother coating—ideal for larger production jobs in tougher materials. – Dplus is a tetrahedral amorphous carbon coating known for extreme wear resistance and performance in abrasive materials. For shops seeking a DLC-style coating, Dplus is Helical’s recommendation.
Uncoated (or bright) tools can be used in aluminum applications, but adding a coating generally improves productivity and helps prevent material from welding onto the tool.
Aplus vs. Tplus
– Aplus is a tough, multi-layer coating that enhances adhesion, edge retention, and heat resistance. It performs best in steels under 45 Rc. Helical’s HSV, HEV, and HSF tool families are excellent choices with this coating. Aplus is not recommended for aluminum, as it can cause galling (when material adheres to the tool), negatively impacting cutting performance and chip evacuation.
– Tplus is a premium coating offering top-tier performance in ferrous materials. It has a slight edge over Aplus, particularly in stainless steels and nickel alloys, and is optimal for cutting materials between 45 Rc and 65 Rc. It supports higher temperatures, maintains edge retention, and reduces wear. However, due to its hardness, it may generate more heat—and, as mentioned earlier, coolant can sometimes lead to thermal shock in these conditions.
Tplus has also shown success in titanium applications. Both Aplus and Tplus are suitable choices for these materials. You can find Tplus coatings on Helical’s HSV, HEV, and HVSS-6 tool families. The HVSS-6 line, in particular, has proven optimal for cutting 316 stainless steels.
There are no setup differences between these coatings when programming your machine. Speeds and feeds depend on the specific toolpath and family used, though coatings generally allow for higher cutting speeds. Choosing the correct coating for your material results in longer tool life and more efficient production.
Tool Storage Recommendations
For best results, Helical recommends storing tools in individual padded tubes rather than in shared bins. This prevents damage to flutes, cutting edges, and coatings. A clean, dry environment helps maintain tool quality and ensures consistent performance over time.
Conclusion
Tool coatings are essential for optimizing performance based on the material being machined. Helical’s coatings are engineered, tested, and proven to deliver the best results across specific materials and applications. By pairing the right tool family and coating, machinists can improve machining efficiency, enhance part quality, and extend tool life.
If you have additional questions about coatings or specific applications, contact Helical’s technical team for guidance at 1-866-543-5422 or by email. Helical’s experts are ready to help you find the ideal tool and coating combination for your needs.
CNC engraving is a process that removes a small amount of material to create detailed images or shapes. Many manufacturers use this method for labeling parts or creating complex designs; however, not everyone is aware of the key techniques necessary for optimal results. When using an engraving tool, it is essential to consider several challenges that could affect both the tool and the operation.
Advantages of CNC Engraving
Compared to other engraving methods, CNC engraving is fast, consistent, and cost-effective. Thanks to their repeatability, CNC machines deliver consistent results when paired with a high-quality engraving tool. We suggest running the tool at a minimum of 6,000 RPM.
If your machine supports it, increasing the RPM can lead to even greater results. Running at lower speeds can negatively impact tool life. Choosing the right engraving tool requires considering production volume and tool engagement time. Key factors such as tip design, angle, and coating play a crucial role in maximizing efficiency and durability.
Proper Engraver Tool Selection
Most machinists understand that a square-corner end mill does not last as long as a corner-radius or ball-end mill due to its fragile cutting edge.
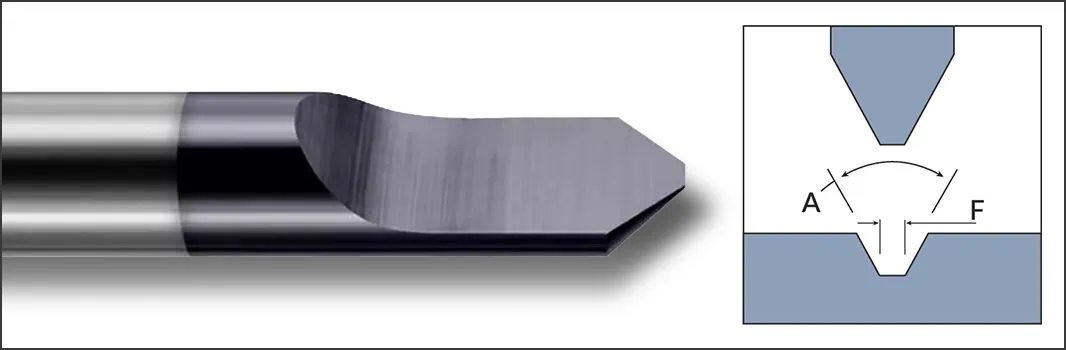
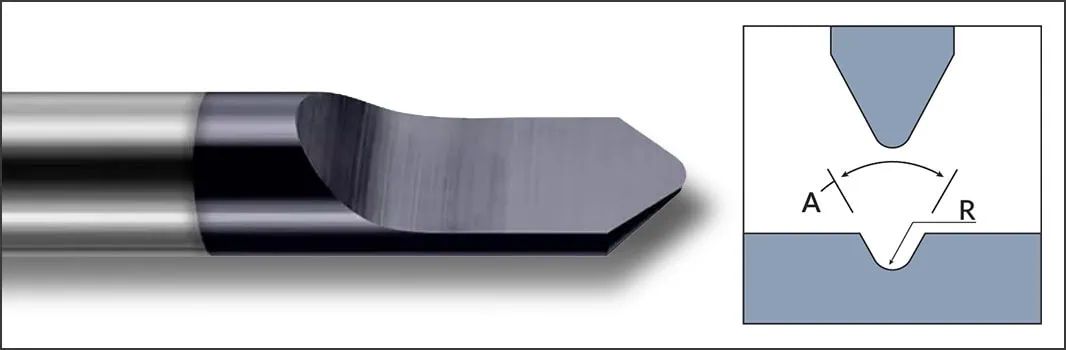
The same principle applies to CNC engraving tools. An engraver that comes to a sharp point is more fragile than one with a tipped-off or radius tip. For long production runs, consider using a tip-off or rounded tip design, as these geometries distribute cutting forces more evenly across the cutting edge, improving tool longevity. A tip-flat design will last longer than a pointed tip but not as long as a radius tip. If high-detail work is required, a pointed tip is preferable because it provides greater precision.
Similar to tip geometry, the engraving angle plays a critical role in visibility. The environment in which the engraving is used affects how well it can be seen. If the engraving is exposed to harsh conditions with elements like snow, mud, or dirt, debris can accumulate in the grooves, making it difficult to see and clean. A larger angle creates a wider groove, improving visibility and ease of cleaning.
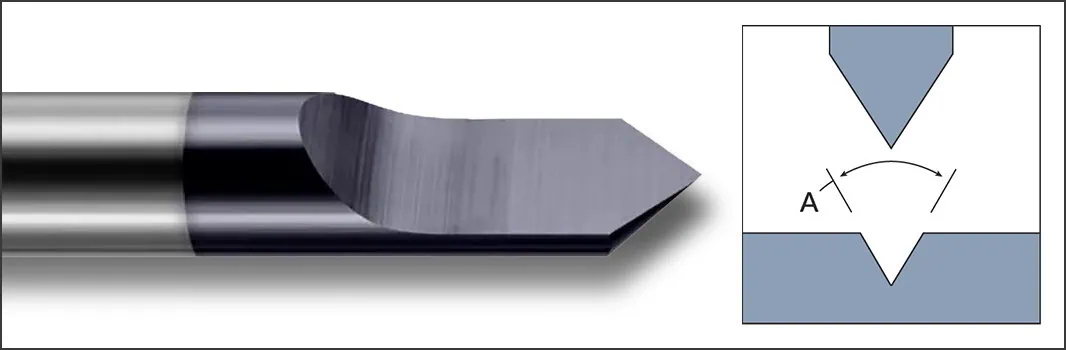
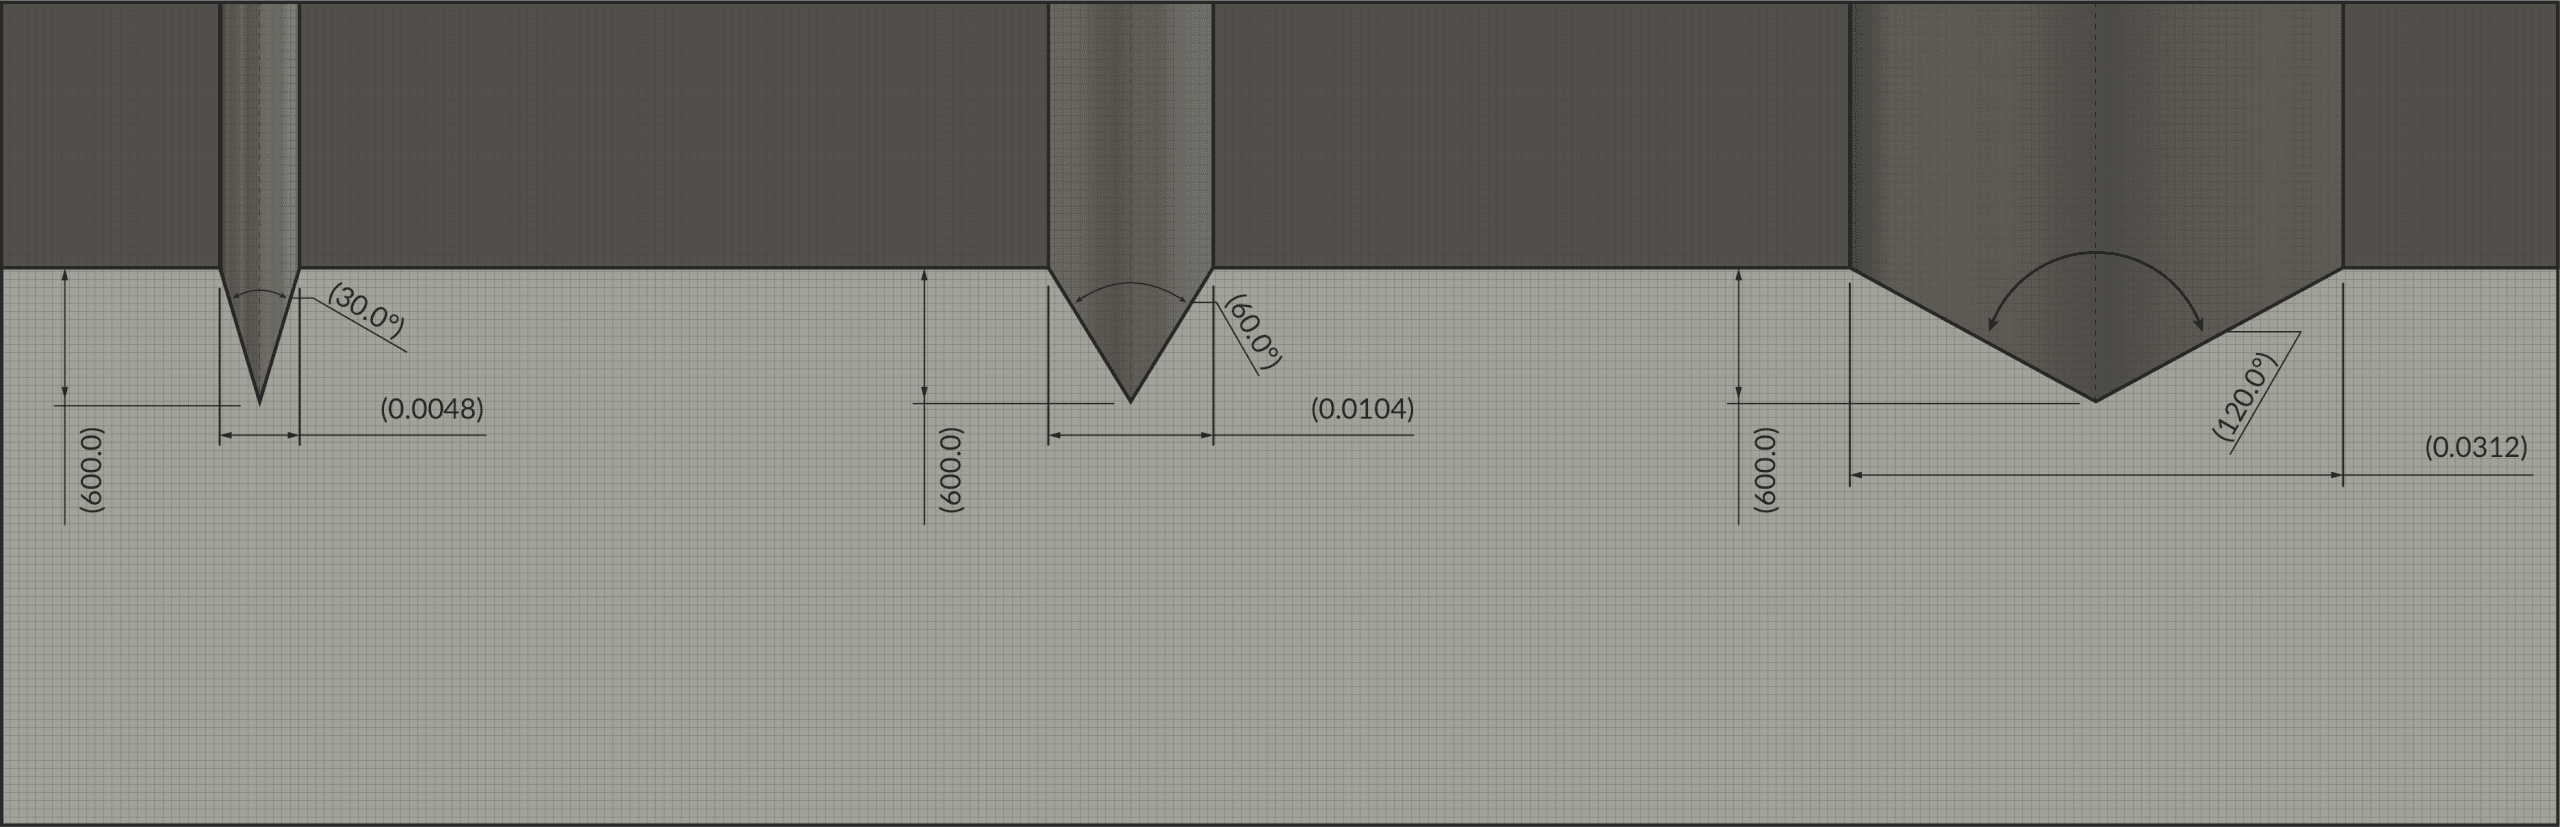
The image below illustrates three different engraving angles offered by Harvey: the leftmost groove is 30° included, the middle groove is 60° included, and the rightmost groove is 120° included. Each of these engravings is only 0.009 inches deep.
Notice that the 120° engraving is more visible at a distance due to increased surface exposure. If a job requires precision and detail, a smaller angle is preferable. While geometry significantly impacts engraving visibility and tool longevity, another key factor in tool performance is the choice of coating.
Choosing a Tool Coating
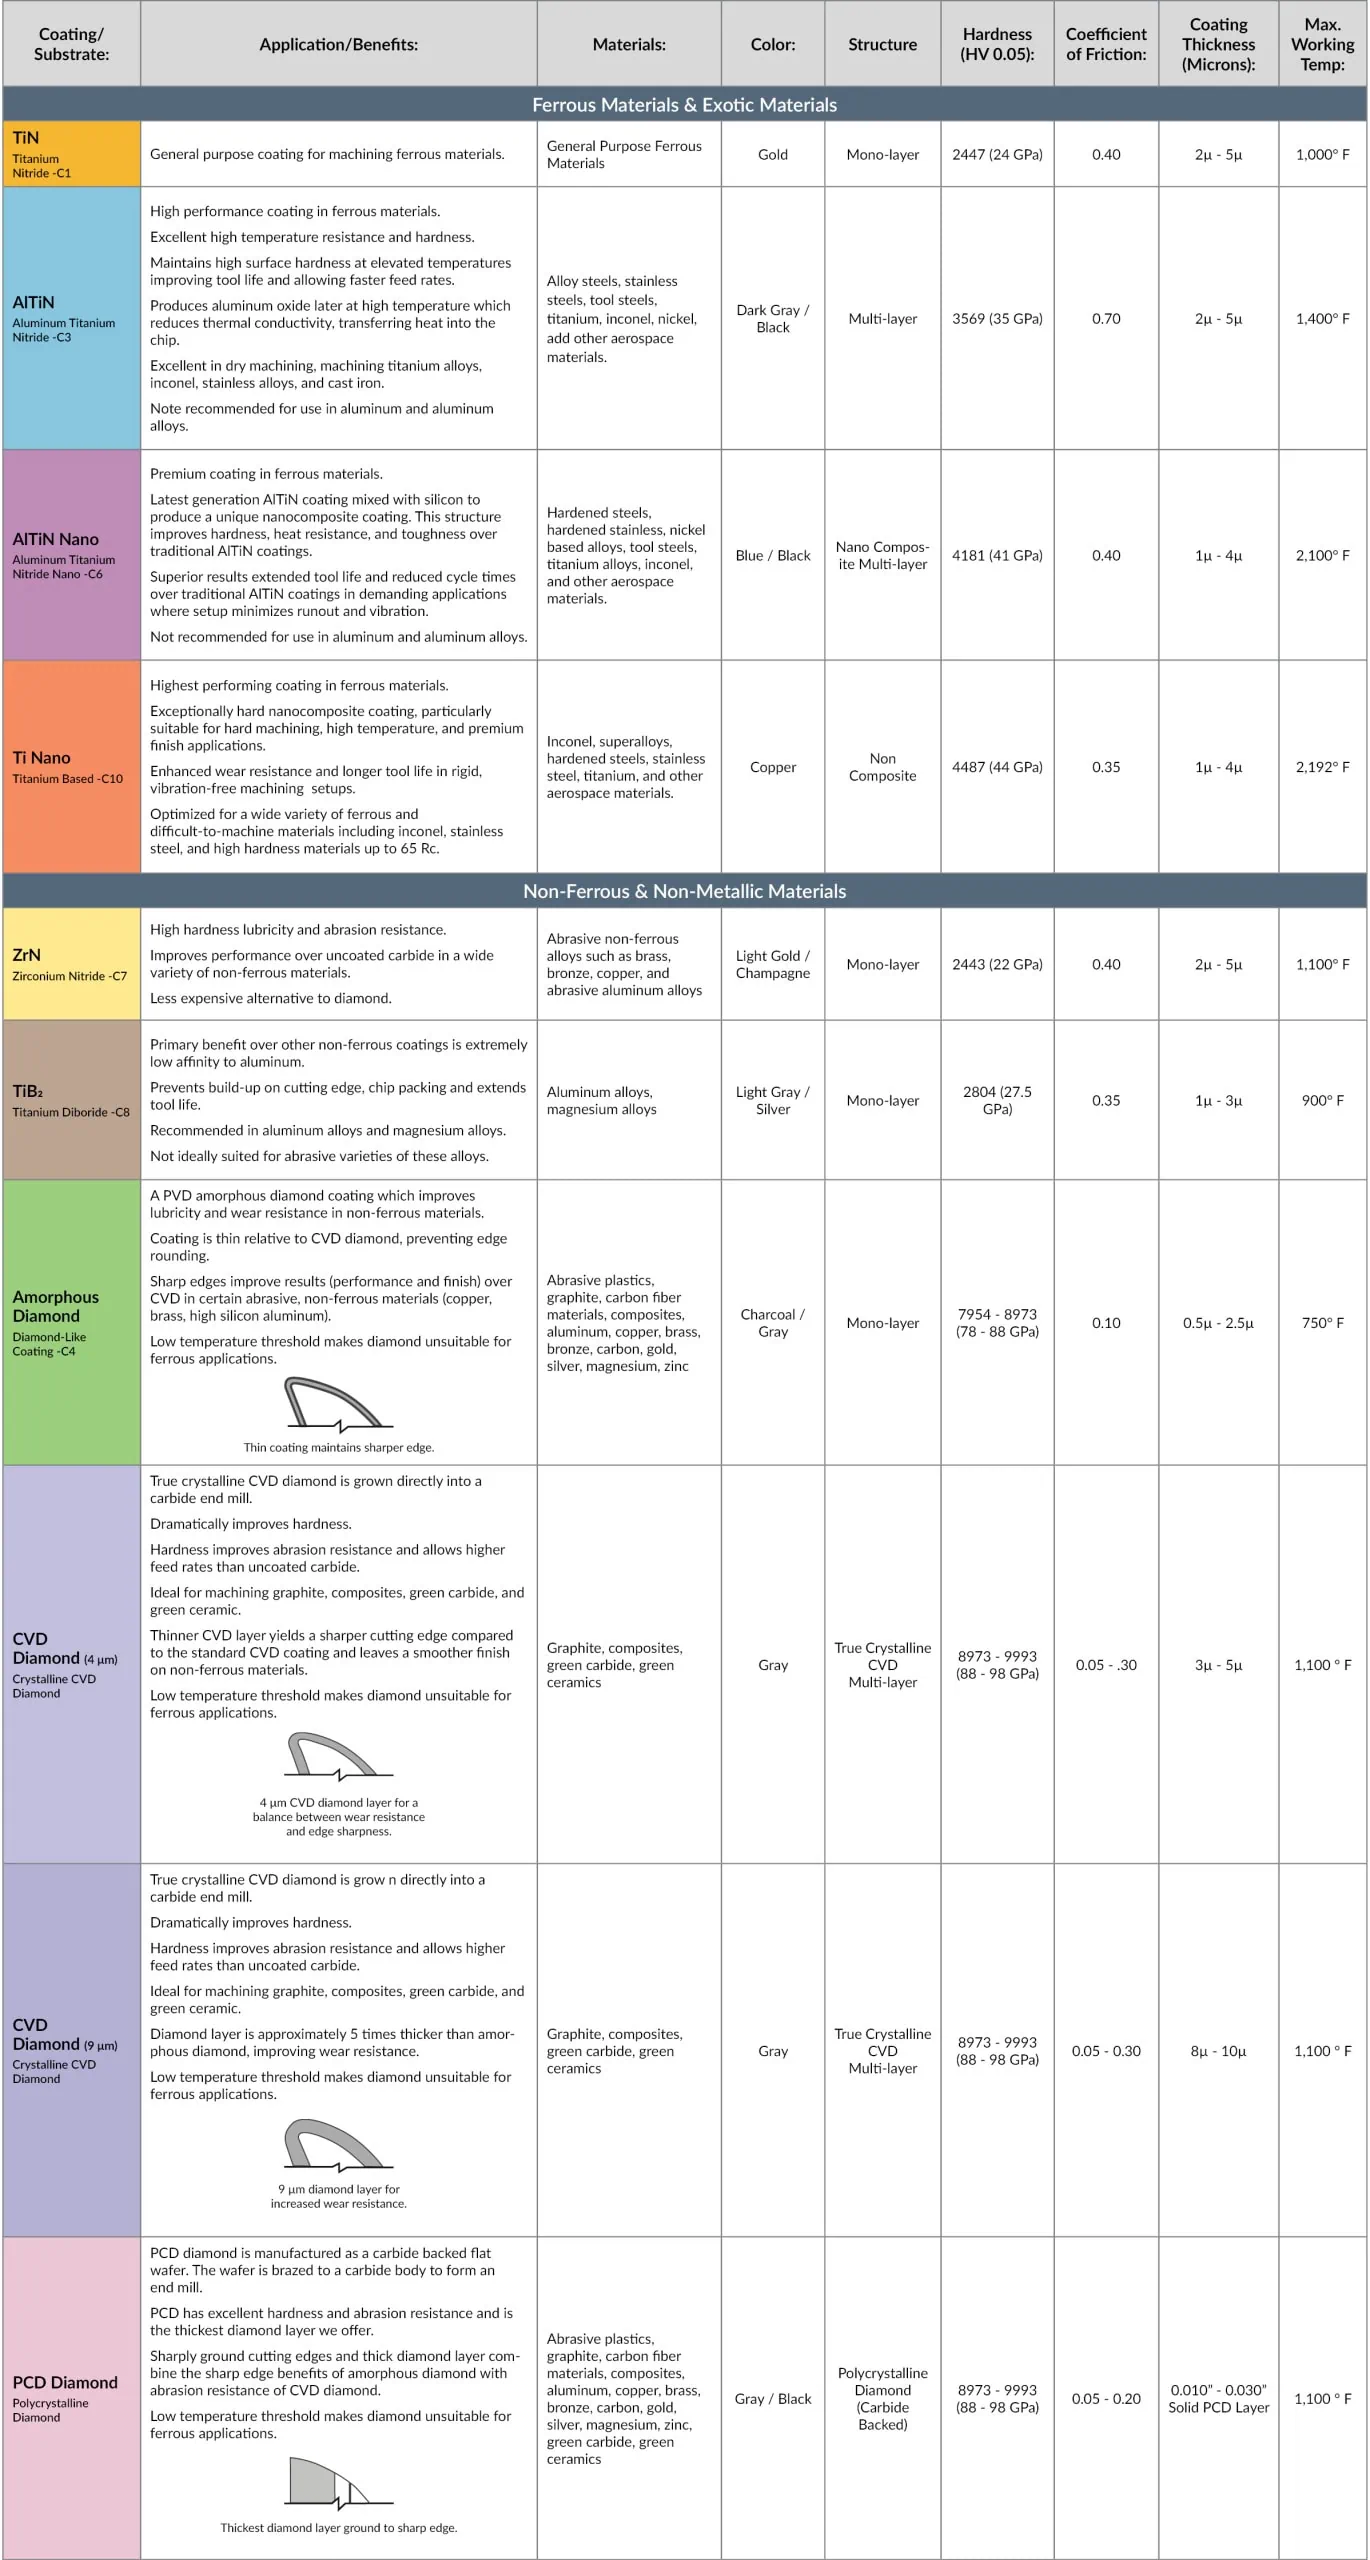
A coated engraving tool will last longer than an uncoated one because the coating provides a protective barrier between the tool and the workpiece. Additionally, coatings help reduce heat absorption, increase lubricity, and decrease tool wear. Selecting the right coating depends on the material being machined.
For example, our AlTiN and AlTiN-Nano coatings perform best in stainless steel and nickel alloys. For non-ferrous materials such as aluminum or copper, our Amorphous Diamond coating is ideal. As an alternative to our Amorphous Diamond coating, we also offer ZrN or TiB2 coatings.
A common misconception is that diamond-coated tools can be used on ferrous materials. Instead, this leads to rapid heat generation and premature tool failure.
Successfully Running Your Engraver
Selecting the correct engraving tool is just as important as understanding how to operate it properly. Even the highest-quality tool will be wasted if not used correctly. As with any machining operation, you must consider depth of cut, work holding methods, and appropriate speeds and feeds
Cutting Speeds and Feeds for Engraving
The tip is the most delicate area of the tool which makes running at the correct speed and feed rate crucial. Running at an incorrect speed and feed rate can cause deflection, which will lead to an inaccurate engraving, chipping, breaking, or a poor surface finish.
At Harvey, we recommend a minimum spindle speed of 6,000 RPM. Operating at higher RPMs, when possible, offers even better support for tool tip integrity.
Higher speeds ensure tool stability as it will be less likely to cause vibration and reduces heat buildup during operation. Running too slowly generates excess heat and vibration leading to chipping, breakage, or having a poor surface finish. To help maintain tool tip integrity, it is important to follow the recommended depth of cut and consider the way the engraver enters the material.
Determining Depth of Cut
Many machinists are unaware that taking cuts deeper than 0.009 inches can shorten the lifespan of a Harvey engraving tool. For depth of cut ranging from 0.001 inch to 0.009 inches, you can operate within our stated speed and feed guidelines. If the operation requires a deeper groove, the chip load must be reduced accordingly. For depths between 0.010 inches and 0.015 inches, reduce the chip load by 20%. For depths ranging from 0.016 inches to 0.020 inches, reduce the chip load by 30%. Depth of cut also influences visibility. A deeper cut made with a tool that has a smaller angle can provide similar visibility to a shallower cut made with a tool that has a larger angle.
The image below illustrates different engraving depths using a 30° included angle. From left to right, the depths are 0.009 inches, 0.015 inches, and 0.020 inches. As depth increases, visibility improves. When engaging the tool with the workpiece, it is best to ramp into the material to protect the tool tip.
We recommend a ramp angle of 1° to 3° for ferrous materials such as stainless steel, and 3° to 10° for non-ferrous materials like aluminum or copper. If ramping is not an option, you may plunge the tool into the material. However, the chip load must be reduced by 50% during entry. Once the desired depth is reached, you can return to the recommended running parameters. Another key consideration is ensuring the workpiece is securely held in place.
Workholding Considerations
Runout or vibration during engraving can result in uneven cuts and tool failure. To prevent this, ensure that engraving tools are held in a sturdy toolholder and that the workpiece is secured. A shrink-fit toolholder minimizes runout and provides excellent stability. While ER collets are acceptable, they wear overtime. To verify an ER collet’s suitability, place an indicator on the tool shank and rotate the tool within the collet. The goal is to achieve the least possible runout, ideally no more than 0.0003 inches.
The workpiece should also be properly secured, either in a vise or a fixture. To detect vibrations during operation, listen for irregular noise or feel for vibrations through the CNC machine door. For cooling, coolants are recommended for metallic workpieces, while an air blast is preferable for non-metallic materials such as plastic.
Conclusion
When selecting an engraving tool, it is essential to choose the correct geometry for the operation, as well as the appropriate coating for the material being machined. Regardless of tip geometry, the engraving tool’s tip is its most fragile part. Proper speed, feed rate, and depth of cut are crucial for maximizing tool life.
For metallic workpieces, a cooling method such as coolant is necessary, while non-metallic workpieces require an air blast. Before starting a new engraving operation, double-check tool runout and ensure that the workpiece is securely held in place.
By following these best practices, CNC engraving operations can achieve high precision, longevity, and optimal tool performance.
Are You Ready to Put Your Engraving Knowledge to Use?
At Valor Holemaking, we know that drilling stainless steel and titanium isn’t just difficult, it’s one of the most demanding challenges manufacturers face. These materials are unforgiving, known for their toughness, low thermal conductivity, and tendency to work harden, which often result in significantly reduced tool life.
Our objective was to evaluate tool life, hole quality, and tolerance under production-level parameters. By benchmarking the performance of the Valor drill against several best-in-class competitors, we aimed to provide data-driven insight into how it performs in demanding stainless steel and titanium applications.
Testing in 316L Stainless Steel
Stainless Steel Testing Information
Material
AISI 316L (200 HB)
Valor Drill
SKU: V623060-X Diameter: 12.7 mm L/D: 5XD Coating: Val-Max-X
This chart displays the total number of holes drilled in AISI 316L stainless steel before tool failure or test completion. The Valor drill reached the testing limit of 2,000 holes with no signs of failure, while other tools showed significant variation in tool life, ranging from more than 200 holes to 1,300. This proves that this Valor high-performance drill can run longer, compared to that of top competitors, particularly in stainless steel where premature wear is common.
Finished Hole Diameter Consistency in Stainless Steel
The data in the chart to the left shows the average finished hole diameter across the test range for each tool. The Valor drill consistently held the nominal 12.7 mm diameter within the IT7 tolerance band. All competitors drifted into the IT9 range, indicative of inefficient chip formation or inefficient cutting.
Measuring hole diameter consistency of testing blocks
Valor Drill – Finished Hole Diameter Consistency Across 2,000 Holes
This chart displays the finished hole diameters measured from Valor’s drill over the course of 2,000 holes in 316L stainless steel. Each point represents an actual measurement, and the data shows the drill maintained exceptional consistency throughout the test. The variation across all holes was just 8 microns, with every measurement falling within the IT7 tolerance band.
What is an IT Band?
In the context of precision machining, IT stands for International Tolerance grade—a standardized system used to define the allowable variation in hole dimensions. The lower the IT number, the tighter the tolerance and the higher the precision. For example, a hole finished within IT6 tolerances is more precise than one within IT8.
IT band values vary depending on the nominal diameter of the hole being machined. In our testing, we focused on a 12.7 mm drill diameter, so the range of acceptable deviation for each IT band is scaled accordingly.
These results indicate that the Valor drill stayed stable in the cut, minimizing drift and taper even after 2,000 holes. For parts where positional accuracy is critical, this helps reduce the need for secondary operations or in-process adjustments.
Inspecting Tool Edge Wear
Testing in 6Al-4V Titanium
Titanium Testing Information
Material
6Al-4V (33HRC)
Valor Drill
SKU: V623060-X Diameter: 12.7 mm L/D: 5XD Coating: Val-Max-X
In this titanium drilling comparison, the chart illustrates total hole count before tool failure or the test’s 1,200-hole cap. The Valor drill, again, reached the maximum without failing, whereas all competitor tools experienced failure beforehand.
Finished Hole Diameter Consistency in Titanium
This chart compares the average finished hole diameters produced by Valor’s drill and several leading competitors in Ti-6Al-4V. Valor’s drill consistently held hole size within the IT6 tolerance band, the tightest shown, while other drills produced holes that fell into IT7 or IT8 ranges. This distinction highlights Valor’s ability to maintain high dimensional accuracy even in a challenging material like titanium. The tighter tolerance indicates better tool stability, less deflection, and more reliable performance across extended runs, which is critical for precision-focused industries like aerospace and medical manufacturing.
Valor Drill – Finished Hole Diameter Consistency Across 1,200 Holes
This chart illustrates the finished hole diameters recorded from Valor’s drill over the 1,200 holes drilled in titanium. Throughout the entire run, the drill consistently held dimensions within the IT6 tolerance band, with hole sizes deviating by only 9 microns from the nominal diameter (12.7mm).
Geometric Accuracy in Titanium
Valor’s drill also demonstrated tight geometric control throughout the titanium test.
True Position: 46 µm
Cylindricity: 23 µm
Straightness: 7 µm
These values remained consistent across all 1,200 holes, reinforcing the tool’s ability to cut clean, accurate features in a challenging material. This level of consistency is especially beneficial in aerospace or medical applications where tight tolerances are required.
Valor Holemaking Application Engineers Inspecting Drills After Test
Conclusion
These internal tests offer insight into how Valor High Performance Drills for Stainless Steel & Titanium perform under consistent parameters in stainless steel and titanium. In both tests, the drills showed the ability to maintain hole quality over extended cycles, potentially improving cost-efficiency and reducing downtime in production settings. While results may vary depending on material, fixturing, and machine setup, this testing provides a data-driven starting point for evaluating suitability in demanding drilling applications.
Harvey Performance Company’s Don Grandt Employs a Novel “Heavy Radial Efficiency Milling” or “HREM” Technique to Boost Tool Life and Minimize Heat Generation in Titanium
For all the characteristics that make Titanium ideal for extreme conditions, such as its high strength, low density, and corrosion resistant properties, it also makes it very difficult to machine. A modern approach to machining, High Efficiency Milling (HEM), helps. It involves using the theory of chip thinning by applying a smaller Radial Depth of Cut (RDOC), and a larger Axial Depth of Cut (ADOC). This method puts the vast majority of an end mill’s cutting edge to work, evenly distributing heat throughout it. An HEM toolpath works by taking more radial passes with a lower RDOC.
But from experience, Harvey Performance Company National Applications Engineer and “Cutting Tool Counselor,” Don Grandt, has found that there’s a better way to machine titanium. Rather than HEM, Don employs a strategy he calls “Heavy Radial Efficiency Milling (HREM)”, something he’s developed over time with a tried and true “Theory, Science, Experience (TSE) Triple Knowledge Approach” to machining.
The Theory:
In switching from a regular toolpath to a standard HEM toolpath, machinists are permitted to increase the surface foot and boost material removal rates because there is less heat generated at the cutting edge due to the lighter radial depth of cut being utilized.
In titanium, specifically, recommended parameters for HEM are often in the ballpark of 400-500 SFM and 121-152 M/Min, with a radial step over of 6% of the cutting diameter. This allows you to increase the speed to achieve higher feed rates.
However, Don has noticed that most of the heat is coming from the SFM or M/Min when machining titanium, and not the RDOC, thus prematurely fatiguing the cutting edge of the tool in HEM toolpaths. He uses the “MRR Triangle” to compensate for this.
In a 2022 episode of In the Loupe TV, a collection of videos Don creates to educate the machining industry on popular machining methods, tips, tricks, and more, he dives into the Material Removal Rate Triangle, explaining that it’s a representation of how IPM, ADOC, and RDOC interact.
“Each one of these things…contributes to your MRR, material removal rate. I know I don’t want to change that, I don’t want to stop it, and I don’t want to slow the customer down. So what do I do?
Three things (IPM, ADOC, and RDOC) are bringing in the heat. Which one’s causing the most heat? That’s what I want to find out. Because guess what? If I find out which one’s causing the most heat, and I can bring that down, then I can bring one of my other things over, adjust it, keep my MRR, and stay productive.”
In this case, Don opts to increase the RDOC while running the tool at lower SFM-M/MIN, the backbone of the “HREM” toolpath. An illustration of this toolpath, compared to a traditional and standard HEM toolpath, is below.
The Science:
While Don’s strategy can be utilized using any End Mill for Titanium, including Harvey Tool’s offering of Variable Pitch End Mills for Titanium Alloys, the below comparison of HEM vs. HREM toolpaths showcases a 6 Flute Helical Solutions End Mill for Titanium.
HEM vs. HREM Parameters Comparison (3.51 Cubes of Material)
HEM Parameters for ½”, 6 Flute Tool in Ti6AL4V
HREM Parameters for ½”, 6 Flute Tool in Ti6AL4v
ADOC
1.0
1.0
RDOC
.030/6% Stepover
.130/27% Stepover
SFM
400
220
RPM
3056
1680
FPT
.0064
.0026
IPM
118
27
Spindle Load
31%
40%
This chart compares an HEM toolpath to an HREM toolpath, using the same Helical Solutions End Mill in Ti6AL4V Titanium.
Notice that in this independent study, the ADOC remains consistent, the IPM decreases, but the RDOC is substantially increased.
The change in parameters, utilizing the MRR Triangle as a model, generates consistent results in both time and MRR output, so what’s the benefit of making the change? Tool life. And again, it boils down to heat generation.
Toolpath Results
Traditional HEM Strategy
“HREM” Strategy
HEM Parameters for ½”, 6 Flute Tool in Ti6AL4V
HREM Parameters for ½”, 6 Flute Tool in Ti6AL4v
Max Tangential Force
228
397
Peak Tool Temperature
1,218° F / 660° C
857° F / 458° C
Cubes of Material Removed
3.51 Cubes of Ti6AL4V
3.51 Cubes of Ti6AL4V
Here, we can identify that, though more max tangential force is applied to the tool in the HREM method, significantly less heat is generated.
While any cutting tool will generate heat, controlling it is pivotal to prolonging the life of your tool.
The Experience:
From the example above, where the same Helical Solutions End Mill for Titanium was utilized, you can see that by simply increasing the RDOC and slowing down the feed, while accommodating the chip with more flutes, the MRR remains consistent but the cutting edge of the tool faired much better.
Toolpath Results
HEM Example
HREM Example
Before Utilizing an HREM Strategy
While HREM can be beneficial in extending the life of your cutting tool when machining titanium, there are several things that machinists must be mindful of before beginning. Notably, an HREM strategy will add more tangential force to your setup, meaning that fixturing, horsepower, and bending force must be properly accounted for.
In addition, the longer the tool’s length of cut, the less radial there is to be had. This means that if a tool’s length of cut is 2x the diameter, the maximum RDOC will be 27%. With 2.5x length of cut, the maximum radial will only be 20%. As the length of cut increases, the radial decreases, meaning that machinists must make adjustments accordingly to reduce the SFM and, in turn, reduce heat generation and built-up edge (BUE).
Harvey Performance Company Brand Tooling Best Suited for HREM
Leading cutting tool brands Helical Solutions and Harvey Tool offer several cutting tool options specifically designed for the machining of Titanium Alloys. Helical’s offering is extensive, with options ranging from roughers to 5, 6, 7, and multi-flute finishers. Included in this range of fully stocked product is the popular HVTI-6 line, which is optimized specifically for advanced machining toolpaths, such as HEM and HREM, in Titanium.
Harvey Tool’s Material Specific End Mill offering includes options for Titanium Alloys, as well. Featuring variable pitch geometry, options include both square and corner radius profiles. A new Variable Pitch End Mills for Titanium Alloys – Ball offering is set to be released in August 2025.
In Conclusion
By rethinking conventional titanium machining strategies, Don’s “Heavy Radial Efficiency Milling” (HREM) approach challenges the standard High Efficiency Milling (HEM) model with proven results. Through his “Theory, Science, Experience” methodology, Don demonstrates that increasing radial engagement while reducing surface speed can significantly lower tool temperatures and extend tool life, all without sacrificing productivity. Backed by data and real-world trials, HREM offers a compelling alternative for shops looking to optimize titanium machining performance in the most demanding applications.
Mold, Tool, and Die manufacturing demands a high level of precision. Whether you’re machining hardened tool steels, creating detailed mold cavities, or producing dies with complex geometries, the tooling used plays a critical role in ensuring consistent, repeatable results. To explore the full selection of tools relevant to this industry, including application-specific geometries and coatings, visit Harvey Tool’s Mold, Tool & Die Featured Solutions page.
Harvey Tool offers a comprehensive range of tools specifically engineered to meet the unique challenges of the Mold, Tool & Die industry. From tools designed to reach deep cavities to those that maintain surface finish in demanding materials, this offering is built to support precision and reliability throughout the machining process.
Tools included in this lineup are:
CVD Diamond End Mills– This Harvey Tool lineup of Diamond Tooling for Non-Ferrous Materials features true crystalline CVD diamond on a solid carbide substrate, making it ideal for machining graphite, composites, green carbide, and green ceramics.
End Mills for Hardened Steels– Engineered for hardened steels from 46Rc to 68Rc, this tool includes the latest generation AlTiN Nano coating for enhanced hardness and thermal resistance.
End Mills for Aluminum Alloys– We know a part is only as successful as its finish. That’s why our aluminum finishing solutions are crafted for mirror-like surface quality.
End Mills for Medium Alloy Steels– Engineered for versatility, these CNC-ground, AlTiN-coated tools excel in machining stainless, tool, and medium alloy steels.
Miniature Tapered End Mills– Tackling deep part features? Harvey Tool’s tapered Miniature End Mills offer unique geometries that take the challenge out of tough-to-reach cuts.
Diamond tooling is essential to many moldmaking processes, particularly during electrode production and when machining non-metallic materials. Harvey Tool’s offering includes a wide selection of Diamond End Mills designed for use in abrasive and non-ferrous materials such as graphite, green carbide, green ceramics, and composites—materials commonly encountered in mold and die work.
These tools feature a CVD (Chemical Vapor Deposition) coating to promote longer tool life and uphold tight tolerances over extended machining cycles.
Highlighted tooling includes:
Finishers – Ball Profile (CVD Diamond) With available radii as small as 0.005″, these tools are ideal for finishing high-detail electrodes and intricate features.
Finishers – Corner Radius (CVD Diamond) Designed for applications requiring edge strength and tight tolerances, available with corner radii from 0.005″ to 0.0625″.
Diamond End Mills are frequently used in electrode machining for EDM (Electrical Discharge Machining), where precision in non-metallic workpieces directly influences final mold quality.
All tools in the Mold, Tool & Die offering are fully stocked and available to ship same day, helping to reduce lead times and keep your production on schedule.
Two of the most frequently recurring operations across a variety of applications are CNC drilling and countersinking. Since these two processes are often interdependent, managing space in the tool crib and time lost on tool changes can become cumbersome when using dedicated tools for each operation. Using combined drill and countersinks eliminates these concerns and has become a go-to tool across machine shops.
Variety of Combined Drill & Countersinks
What is a Combination Drill & Countersink Tool?
A Combined Drill & Countersink is a specialized tool designed to perform two critical operations in one step: drilling a hole and creating a countersink. These tools are typically short and rigid, ideal for producing either a shallow conic or a center hole. Their double-ended design minimizes downtime by enabling quick transitions between tasks.
Valor Holemaking’s Combined Drill & Countersink
Key Features of Combined Drill & Countersinks
They feature a smaller drilling pilot and larger diameter countersink. The drill pilot resembles a spot drill, making it useful for predrilling applications. The stub length of the drill mitigates deflection and ensures accurate location of a hole’s center. When preparing a spot hole for a longer drill, it prevents walking or wobbling off-center.
Common Applications for Combined Drill & Countersinks
Many holemaking applications begin with spotting and end with countersinking, making combination multi-functional tools cost-effective and time efficient. As the tool drills into the material, the larger countersink diameter chamfers the top edges, allowing fasteners to sit flush with the surface.
Where and How to Use a Combined Drill & Countersink
The primary use of a combined drill and countersink is to create center holes in materials that will be turned between two centers. These centers help accurately position a workpiece along its axis between a lathe chuck and tailstock. Live centers are used in applications requiring a high level of concentricity and support. They typically feature a 60° included angle, which is the angle most combined drills and countersinks are manufactured with. For this reason, combined drill and countersinks are often referred to as center drills.
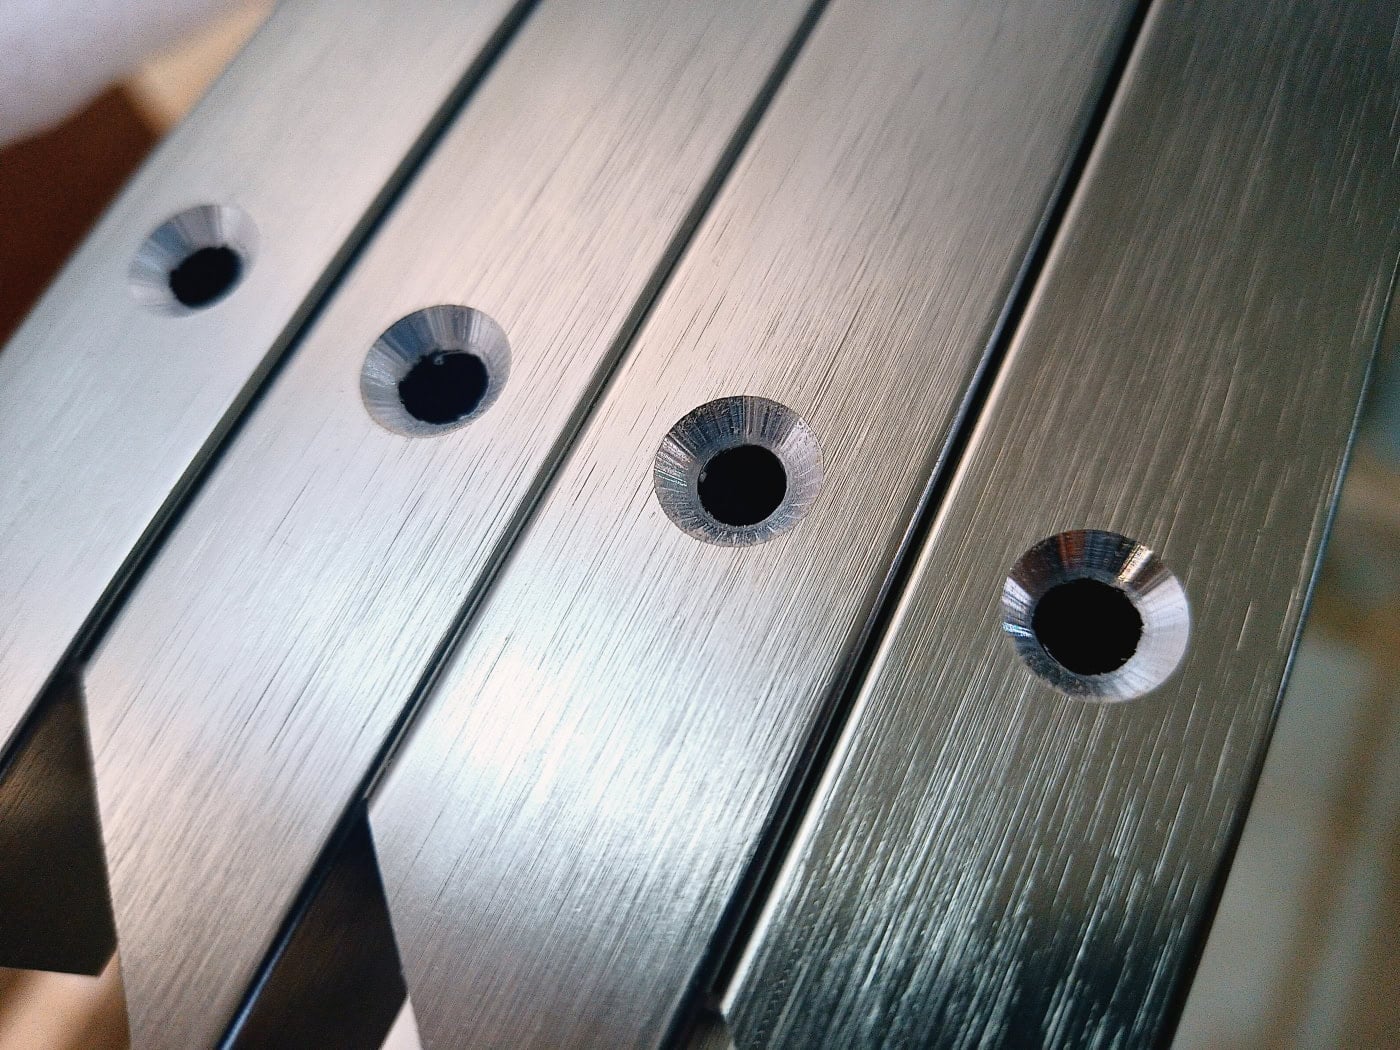
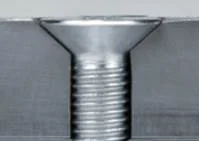
Combined drill and countersinks are also essential in any application where screws need to sit flush in the workpiece. Holes need to be drilled and countersunk across all industries. Flush-mounted fasteners are required in applications such as aircraft panels and structural components, automotive engine components, boat hulls and marine components, electronic device housings, and covers of all types.
Example of countersunk hole
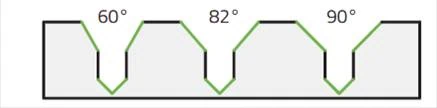
Types of Combination Drill/sinks: 60°, 82°, and 90° Angles
Harvey Tool and Valor Holemaking offer combined drill and countersinks in 60°, 82°, and 90° included angles. While 60° tools are most commonly used for center drilling, 82° and 90° included angles are designed to match the angles of the most popular flat and oval head screws. These tools allow users to create countersunk fastener holes in a single step.
Important Tips for Running Combination Drills
When running a combined drill-and-countersink, it is important to ensure that chiploads (IPR) are based on the drill diameter. Since the drill diameter is always smaller than the chamfer area, it is safer to use parameters designed for the drill portion of the tool rather than calculating an effective cutter diameter for the chamfer.
Valor Holemaking Combined Drill & Countersink in the Spindle
Why These Tools Are Essential in Machining
Combined drill & countersinks are cost-effective and efficient tools to have in your arsenal. Whether you’re preparing a workpiece for turning between centers, spot drilling, or creating countersunk holes for fasteners, these reliable tools complete the job quickly and effectively.
Helical Solutions offers a variety of Tapered End Mills designed to enhance performance and efficiency in tapered wall applications. In this blog post, we’ll dive into the geometry of tapered end mills and explore their common applications to understand when they could be utilized to optimize your CNC machining application.
Tapered End Mill Geometry
Tapered End Mills bring many advantages to machining compared to standard end mills, but what is a Tapered End Mill? A standard end mill will have the same cutting diameter throughout the whole length of cut, whereas a taper mills starts at the shank or neck at a larger diameter and tapers down at a specific angle.
The angle of the taper can vary, but Helical Solutions’ tools feature angles ranging from .05° to 5°, which allows for a broad spectrum of cutting operations. A tapered length of cut or tapered neck can also provide increased strength and rigidity, compared to that of a standard end mill. Having a tapered length of cut makes it easier to create flat tapered walls on 3-axis machines and leads to a better finish.
Tapered End Mill
Standard End Mill
Common Taper Mill Applications
Tapered End Mills are used in any machining process that requires an angled surface. These tools are engineered for light profiling and finishing applications in mold and die pockets and other tapered wall applications.
Mold & Die Applications
Mold and die applications are a mass production manufacturing method that consists of shaping different types of metals and other materials. Molds are used to shape metals, allowing them to become solid in the mold, while dies use a mechanical force to cut the material into the desired shape.
A couple examples of mold and die applications are plastic bottles, car body parts, electronic components, cutlery, coins, and metal stamping parts.
Mold Tool & Die Example
Tapered End Mills Profiles
Taper mills are great for profiling with the ball nose version, and for light finishing and creating required draft angles with the square version. Which style is right for you?
Ball Nose Taper Mills
Ball Nose Tapered End Mills are great for profiling because the full radius at the bottom eliminates sharp edges, which leads to a smoother process.
Square Profile Tooling
The square version of the tapered end mill has a higher flute count and helix angle with a sharp cutting edge. This is better for light finishes on the walls of tools.
The draft angle determined in the design process is the amount of mold design can be tapered. A draft angle is a strategic angle or slope designed in the mold. The tapered angle in the tool allows for the draft angle to be formed easier compared to a straight shanked end mill. Having a draft angle in the mold allows for easier removal of the part so it does not get stuck to the mold.
Helical Solutions’ Tapered End Mills
Helical Solutions’ offering of Tapered End Mills feature a tapered profile design, variable pitch geometry for reduced harmonics and increased feed rates, and Aplus coating for increased performance in Cast Iron, Steel, and even Stainless Steel. These tools are offered in a 4 Flute Ball style, and a 5 Flute Square style, so you can select the end profile that best suits your specific toolpath.
Helical’s Tapered End Mills
4 Flute Ball (HTPR-4)
Helical’s 4 Flute Ball Tapered End Mills (HTPR-4) are fully stocked in 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a ball nose profile, allowing them to excel in a variety of different applications from 3D contouring and profiling to slotting. A Ball Nose End Mill has a full form radius, allowing machinists to utilize the entire radius when contouring and finishing a 3D surface.
5 Flute Square (HPTR-5)
Helical’s 5 Flute Square Tapered End Mills (HTPR-5) is also is also fully stocked 6 different angles per side (0.5°, 1°, 1.5°, 2°, 3°, 5°), and in 3 different cutter diameters (1/8”, 3/16”, ¼”). These tools feature a square profile for more precise finishing and the 5 flute design creates a larger core, allowing for better tool strength in roughing applications.
Taper Mill Tooling Wrapped-up
By understanding the unique features and advantages of this tooling, machinists can make informed decisions and achieve superior results in their projects. These feature unique geometry that enhances machining capabilities and ensures reliability and accuracy across a range of tapered wall applications.
https://www.harveyperformance.com/wp-content/uploads/2025/01/DSC_0434.jpg5251400Thomas Donahuehttp://www.harveyperformance.com/wp-content/uploads/2018/08/Logo_HarveyPerformanceCompany-4.pngThomas Donahue2025-01-29 15:55:382025-01-30 09:14:54A Closer Look at Helical Solutions’ Tapered End Mills